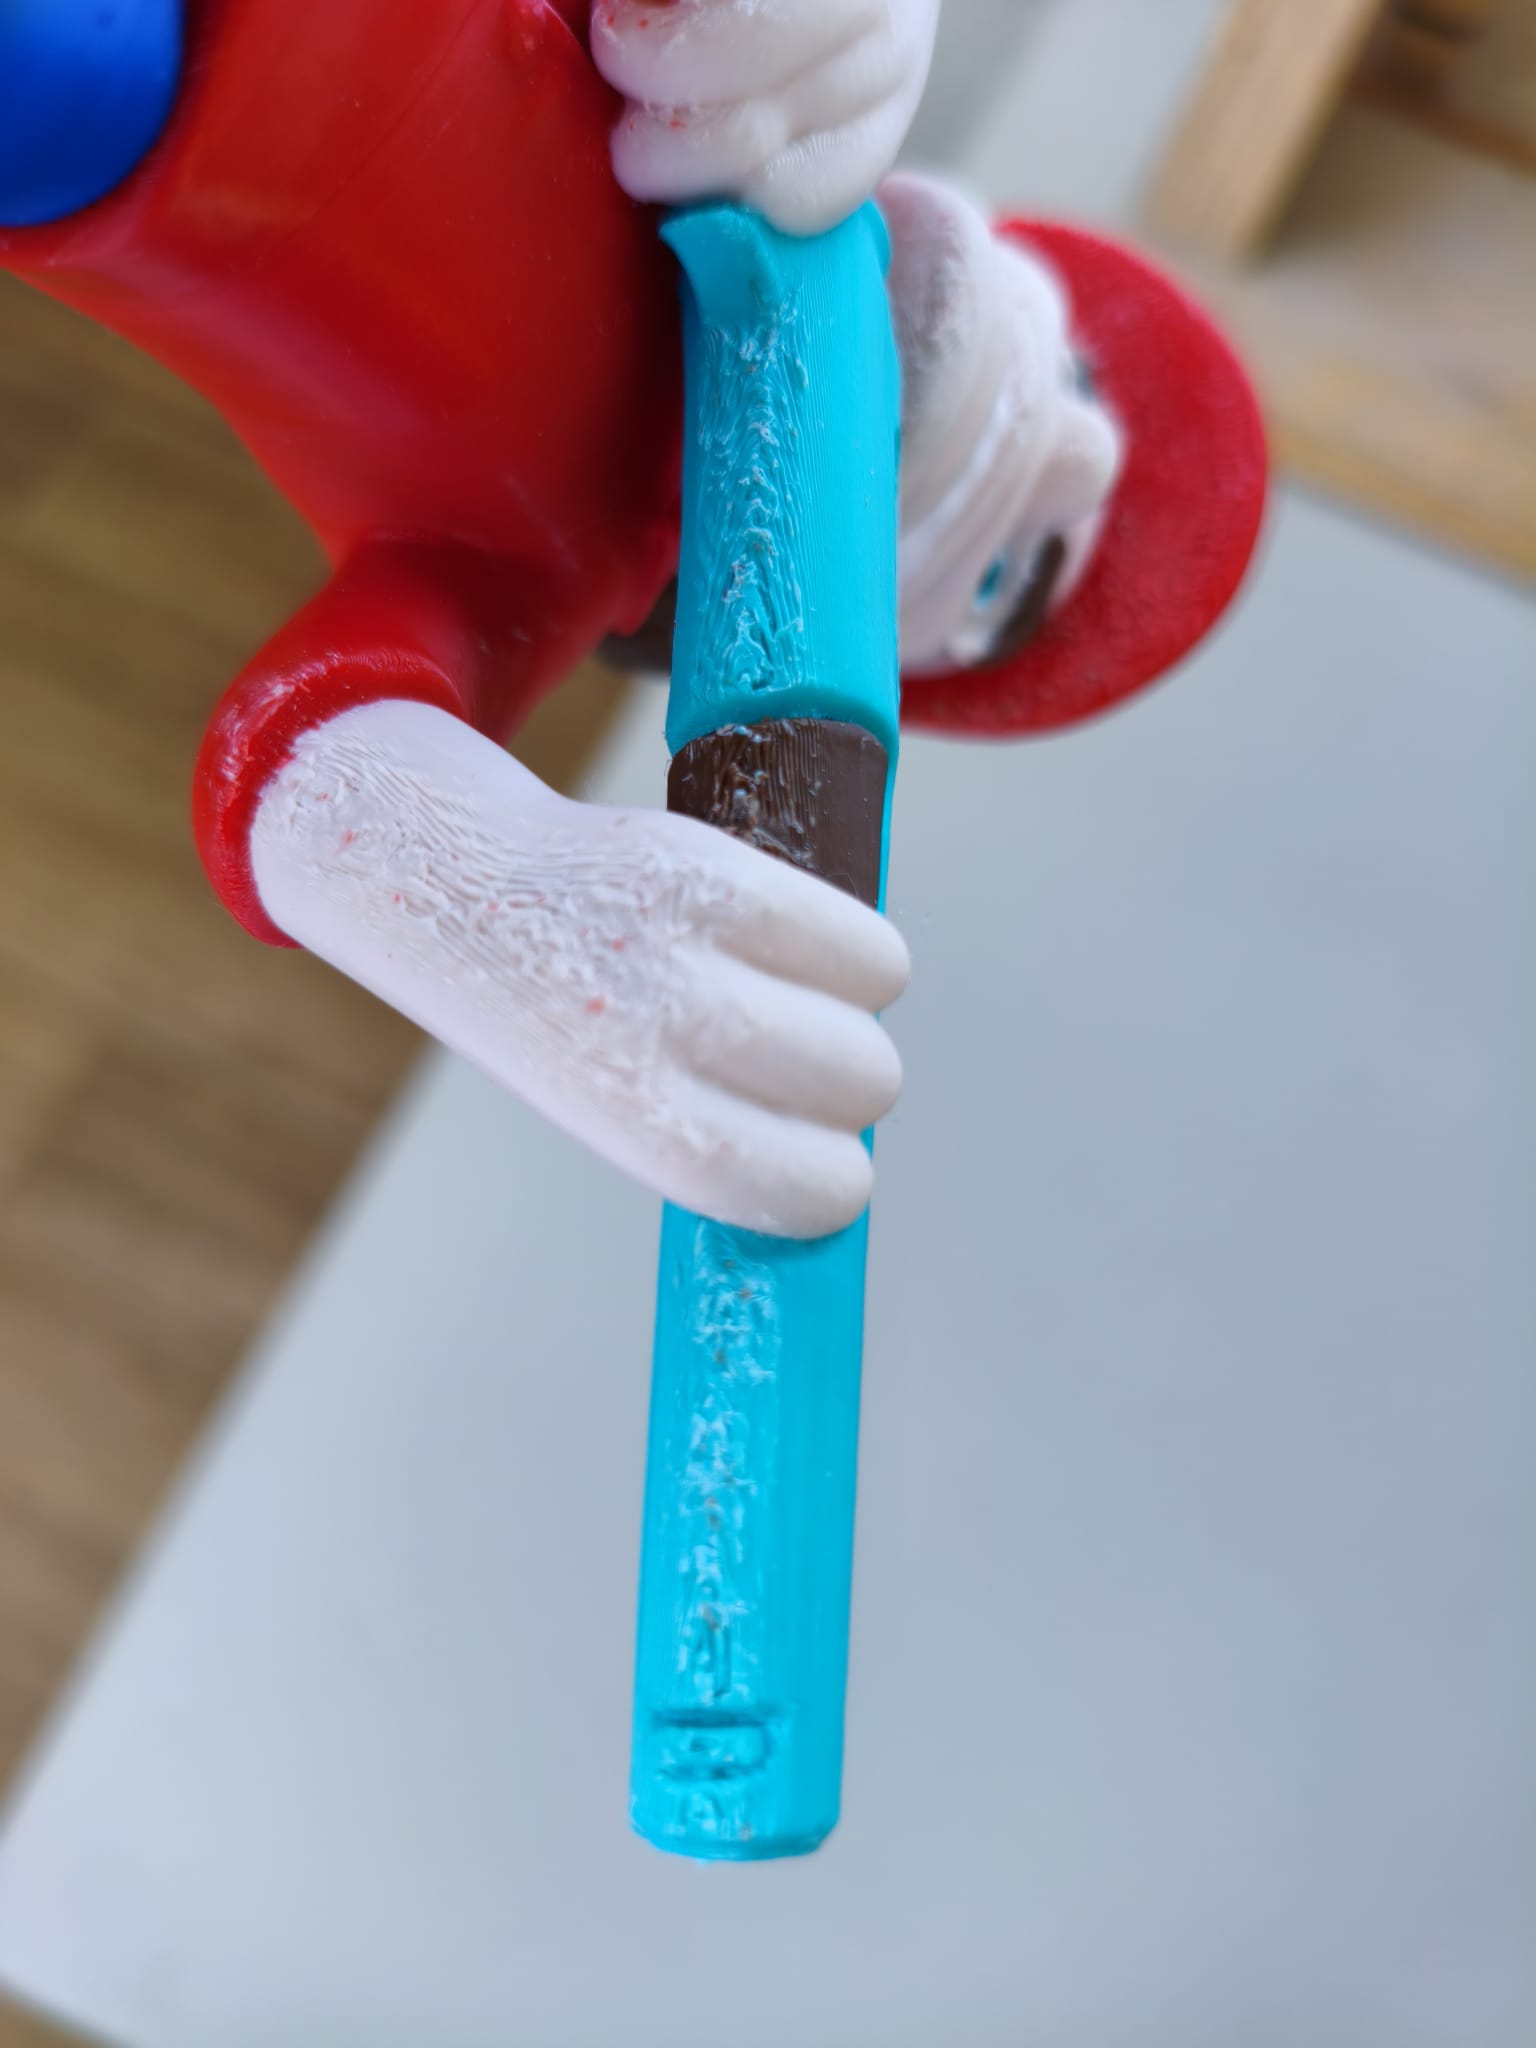
I usually print multicolor prints, and usually use maximal layer height, for reduced print time & filament usage.
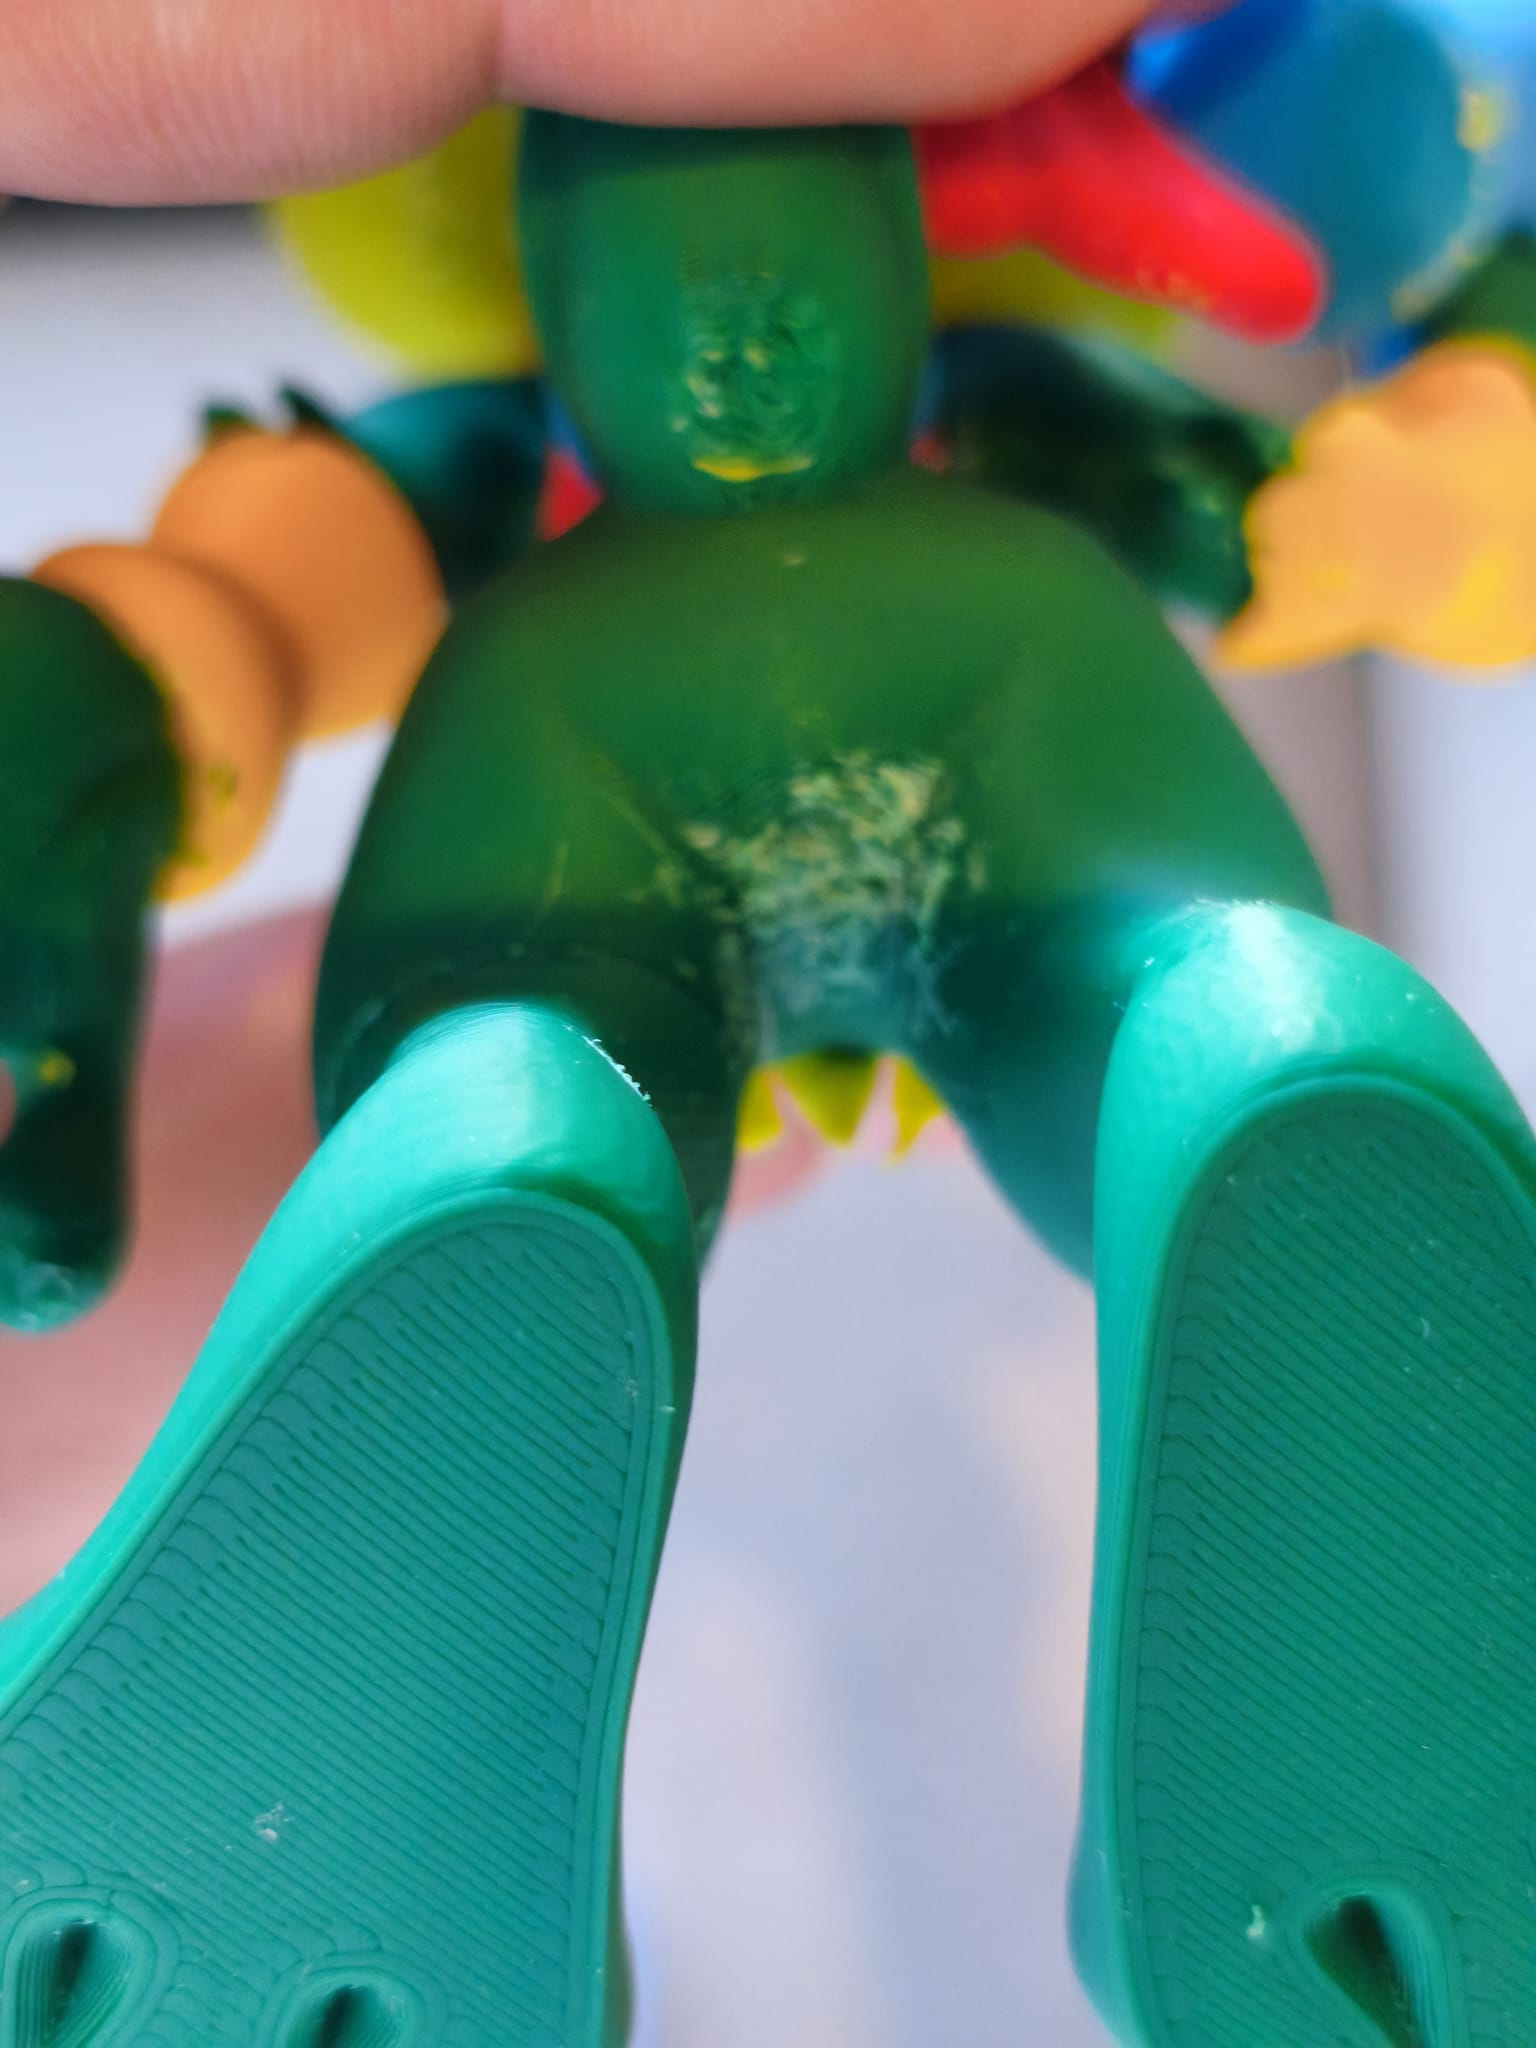
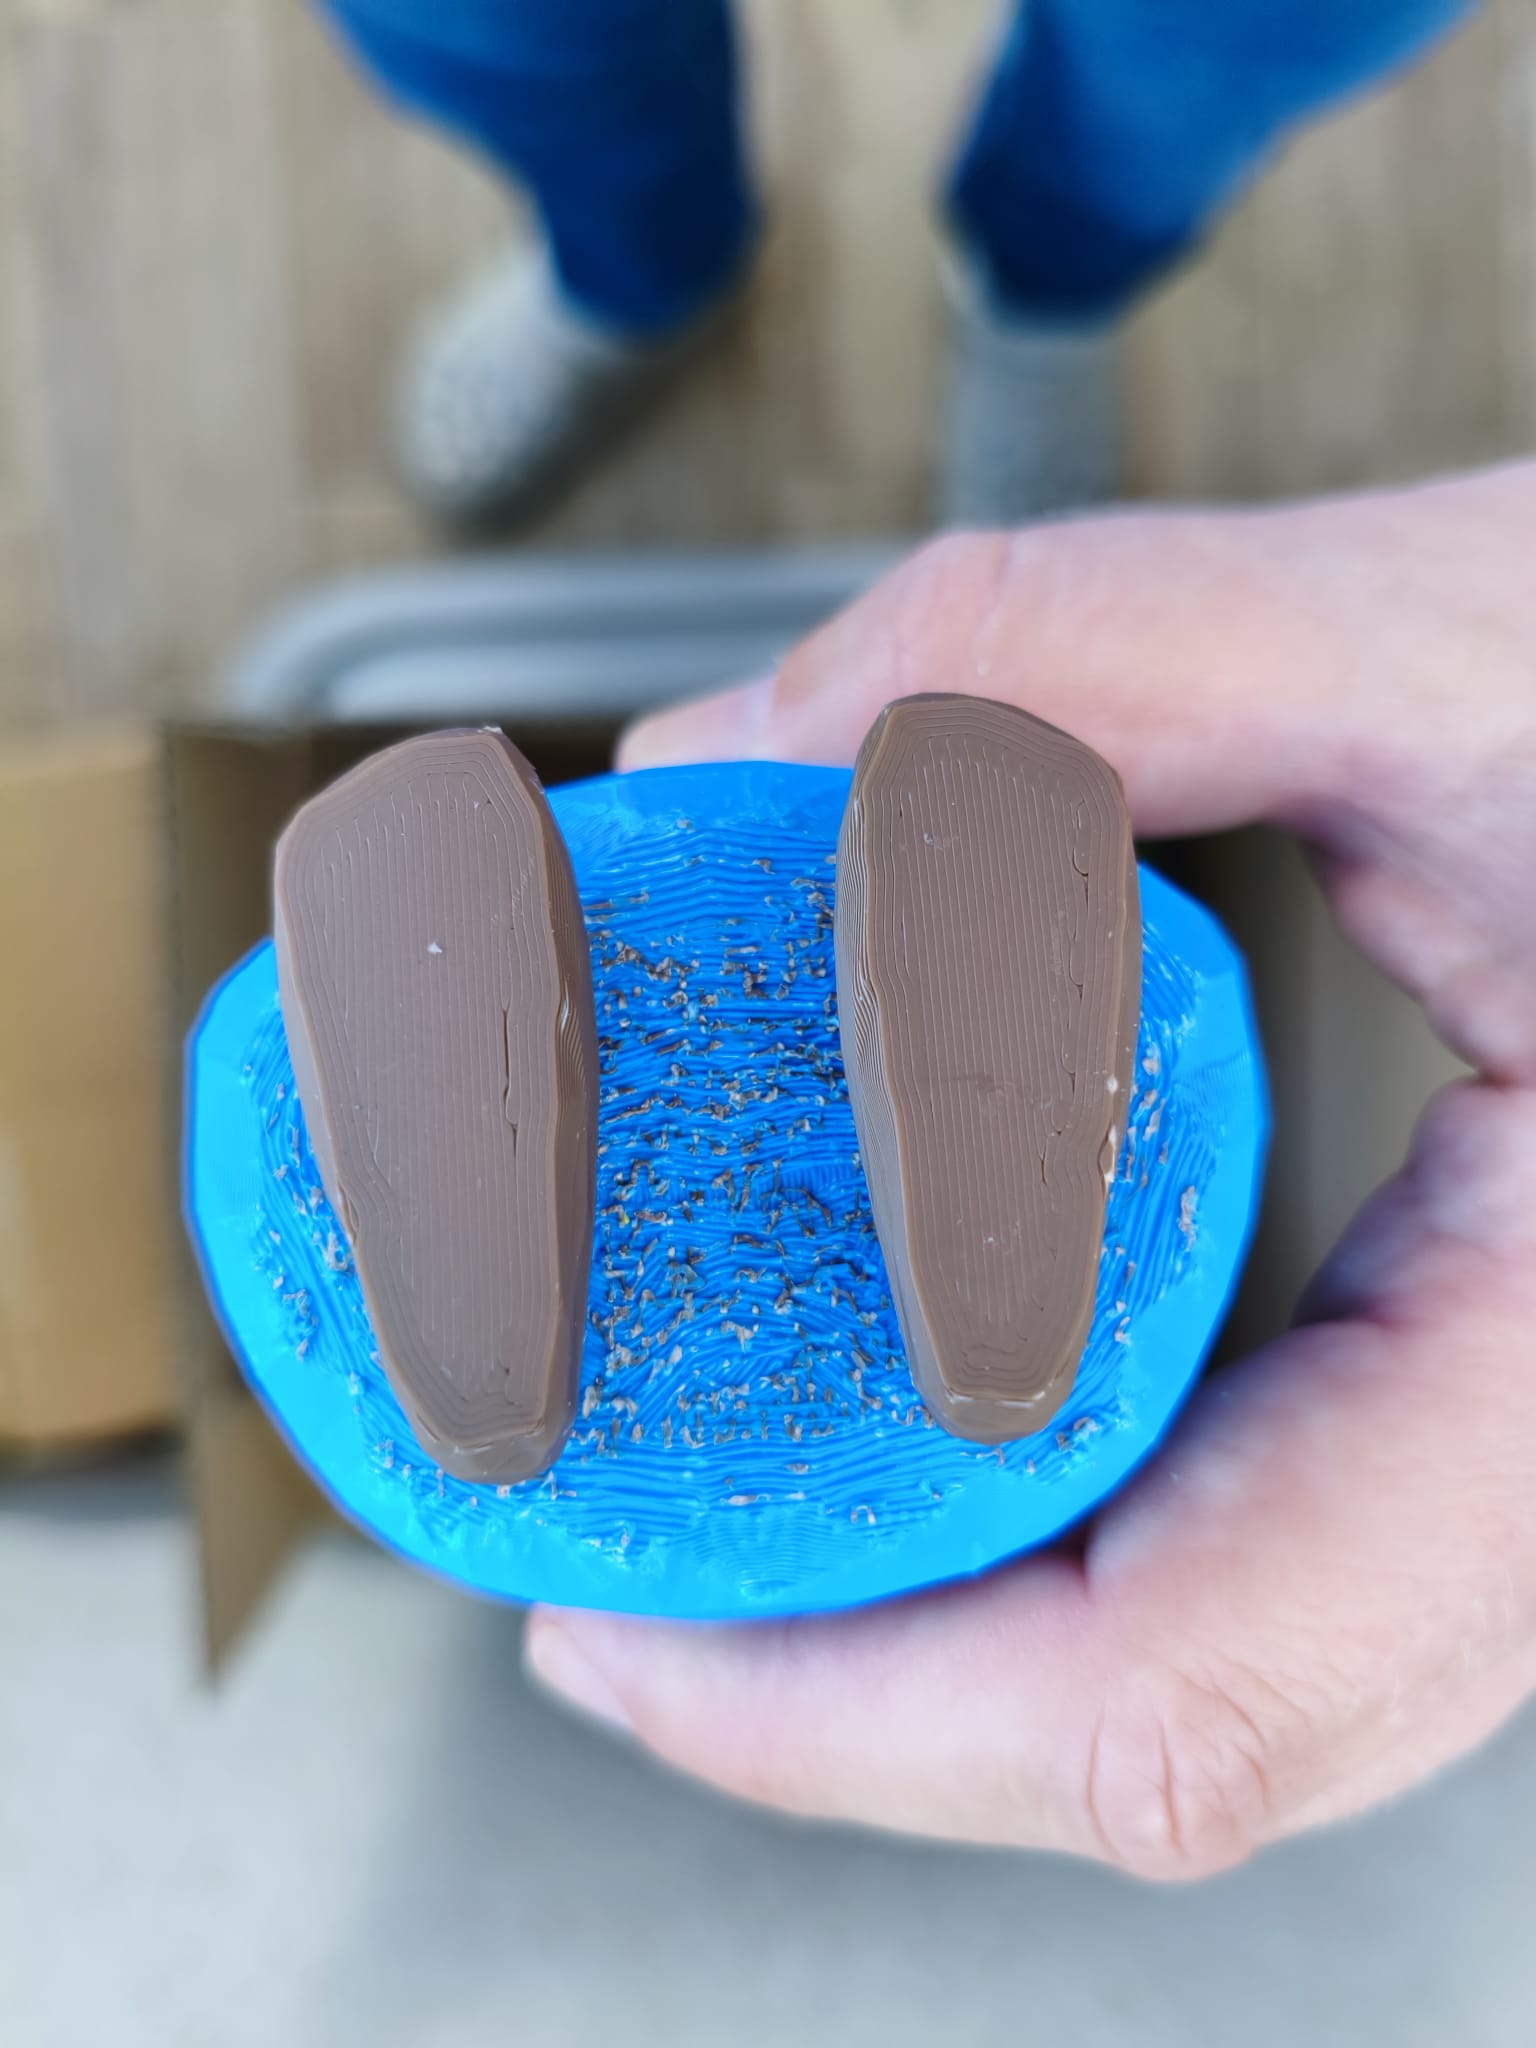
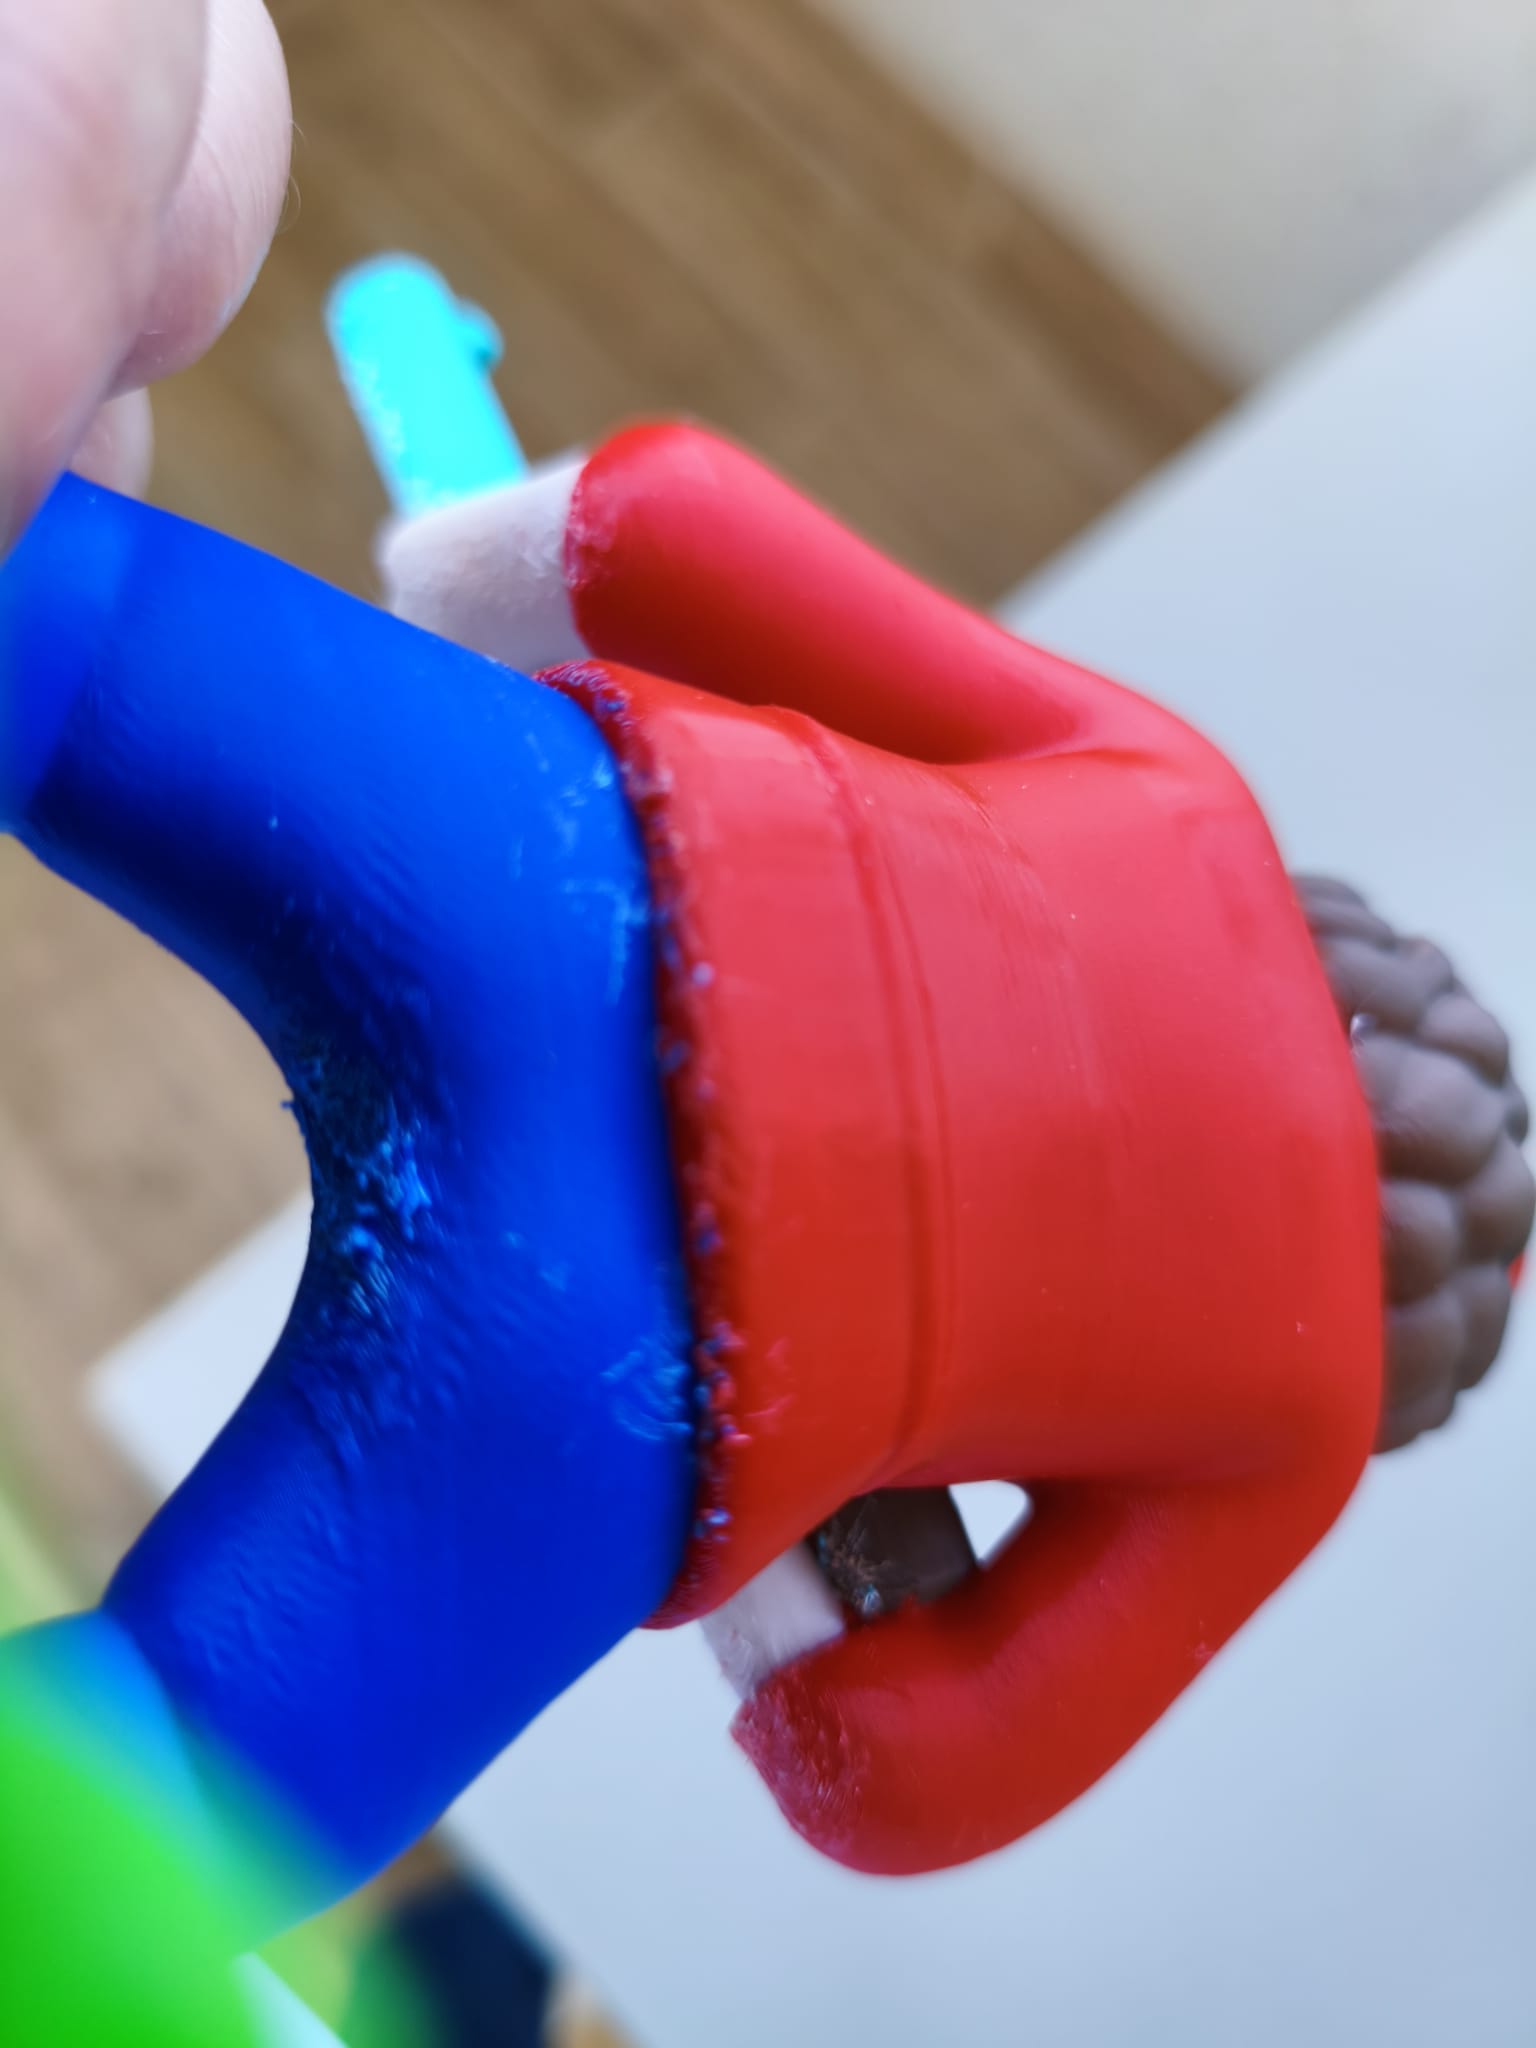
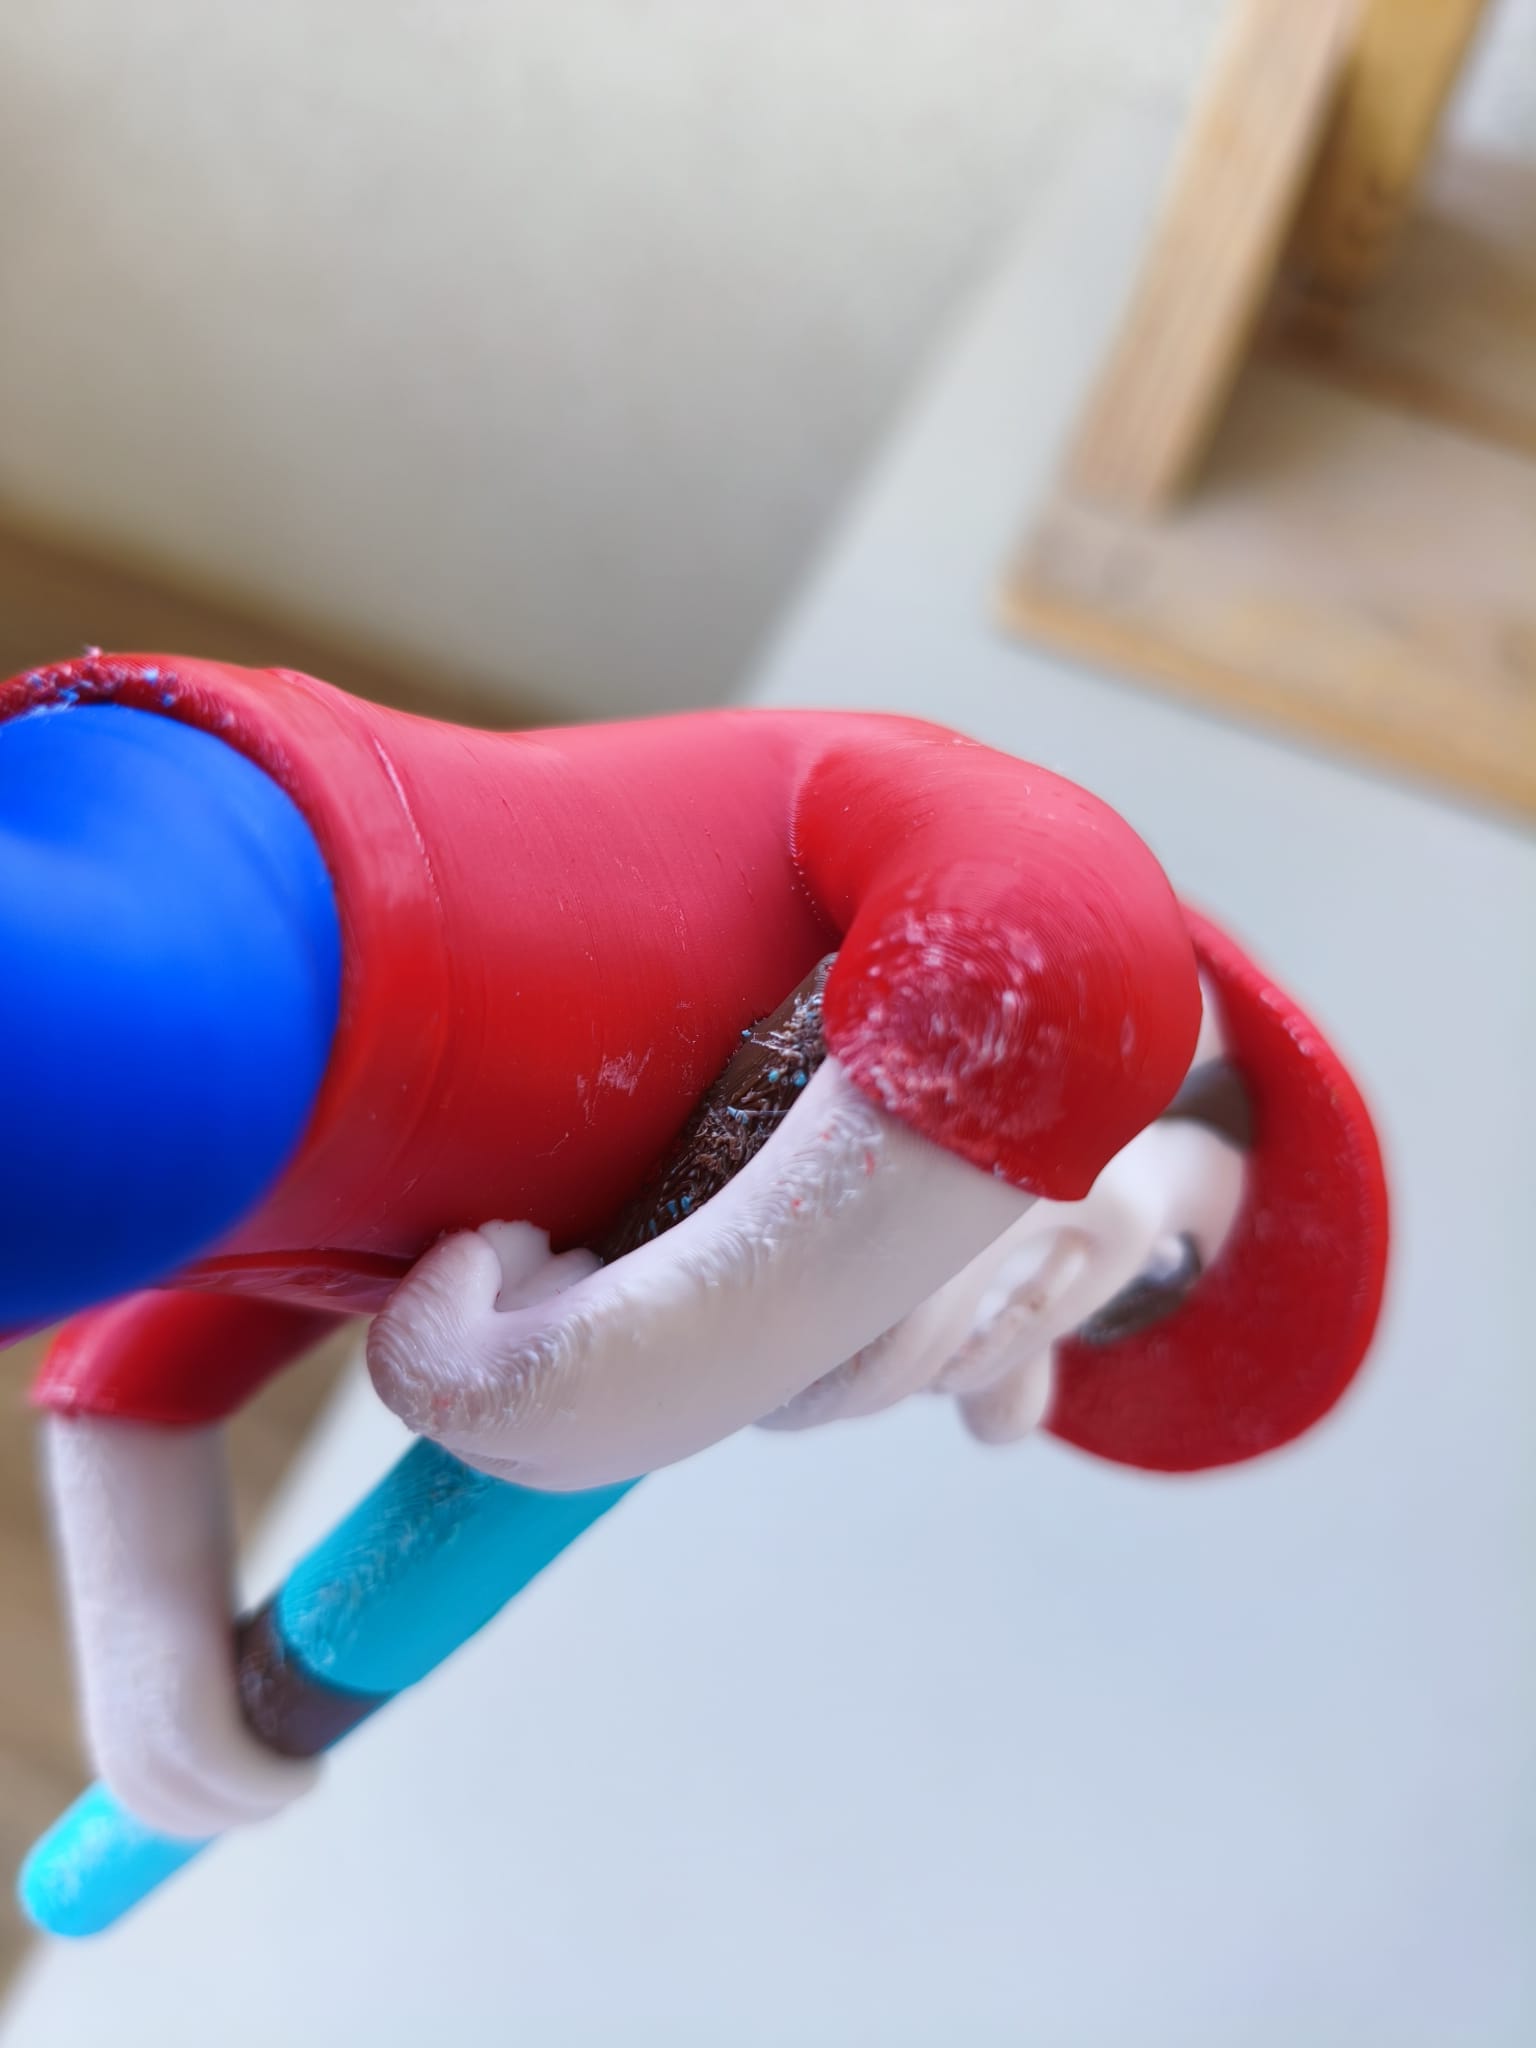
But the downside of that, is that the finished result often comes out coarse. Often things printed at an angle don’t look smooth, or removing the supports leaves a coarse surface.
I’ve seen people recommend varnish or nail polish. However, I tried transparent varnish, but didn’t see any discernable results. Only white residue when I use too much.
I also tried different sanding papers, and a small dremel with fine sanding bits - but in all instances, the sanding produced good results to the touch, but not visually. Visually there are always scratch marks, that affect the appearance of the model.
Does anyone have a way of making the surface of PLA prints look smoother, without affecting the colors?
Variable layer height is great. Especially combined with “combine infill”. It’ll take a little longer, but I tend to compare print time + post-processing time to the print time using variable layer height.
You can also adjust the height range in the machine settings in Studio. For PLA, 0.04mm is pretty easy with a .4mm nozzle or larger. 0.03 is doable, but out-of synch with the stepper motor pitch. “Multi-color interlayer” uses a speed trick (to 350mm/s) to push all the way down to 0.02mm layer height.
Even with the increased print time, it can be much shorter and, more importantly: hassle-free, than a fast, coarse print with long post-processing.
&
PS: Just in case you have trouble finding the slicers machine settings:
Sorry, that’s a very interesting read - but not quite what I was asking.
I’m printing multicolor prints of 8-12 colors, so in order to reduce print time & filament am forced to always use maximal layer height.
I acknowledge that having a lower layer height, will obviously lead to better quality of final result. But that is not my question here.
My question is: given my print results are “rough around the edges”, which post-processing materials/methods can be used to give them better visual finish?
For multicolor PLA, a few light coats of clear acrylic spray may work better than dry sanding. Let each coat cure, then lightly wet-sand with 1000–2000 grit before applying a final satin or matte clear coat. It will not remove deep layer steps, but it can reduce scratches and improve the visual finish without covering the colors. Test it on a small sample first, as some clear coats can slightly change the gloss or darken the colors.
Indeed. However, I feel that you are already overly constraining yourself by mandating a print time minimization rather than a total time (and effort) reduction.
Regarding your question:
3D Gloop! Print Smoothing: 101 — 3D Gloop! is a common recommendation for cases such as yours. I haven’t used it myself though. Note that it recommends post-application sanding and polishing.
A thick, glossy clear coat (typically applied in many thin layers) can greatly improve looks. But for PLA, you’ll want to use a primer first. Most tend to be grey though…
Sanding: You have been there, done that,… Your printer can do many, many extra layers while you sand, grind and polish… Especially at “Draft” quality…
To provide a little context on the topic - that is, to follow up on your comment - simply a continuation. So, to add to that:
Print in draft mode, then dip the 3D object in a magical chemical solution, and it looks like it was printed with a 0.2 nozzle. If that existed, everyone would use it.
It’s actually a very straightforward calculation: the time it takes to print versus the time it takes to do the follow-up work. Then you have to weigh those factors against each other.
But, as the person who started this thread also mentioned in the other one, he really doesn’t want to change the 3D model, the print settings, the orientation, or the workflow - and the use of support filament. So, unfortunately, the options are pretty limited.
Things like sanding and applying primer - all of that has already been ruled out.
This isn’t a discussion, it’s a dead end.
Especially in the context of the other topic, which provides a broader picture of what is to be achieved. Long-time users who had offered help were subsequently blocked and ignored. In fact, 3MF files have already been modified for him: As a result, users were added to the ignore list by him because “that wasn’t what the thread starter wanted”.
The idea is to make something as perfect as possible using the fastest and worst unoptimised settings, with as little post-processing as possible, without distorting the colours. That doesn’t exist.
The problem is the inability to adapt the workflow at all.
Polysmooth! Although I’m not sure if polymaker still produces that line.
I remember years ago using a self leveling resin like product you could paint on your models to get them smooth and glossy. Forget the name though. Feel like it has a skull as part of the product packaging.
Higher print quality settings is the way to go though. Even if you do some post processing, the higher quality your print, the better time you’re gonna have
To my poor eyesight (and guessing) these all look like support contact points. If true, this is less about multiple colours or even layer heights (although thick ones pronounce the issue), and all about using a support interface instead.
Use a filament that won’t bond as the support interface. If you use PLA, have a PETG or support for PLA filament set.
The support interface is only used when there is contact between the support and the model. After printing, the model should be far cleaner.
You can also use a heat source, like a lighter to improve the quality.
As mentioned in the other thread - the problem was not the advice offered (or lack thereof).
The problem was toxic forum members who think that bashing & abusing other people in personal attacks in order to elevate their own “standing” is somehow a valid form of online discourse.
As I stated in the other thread: I’m not interested in advice from toxic people, filled with Ad Hominem attacks on myself, my character or my skills. Even if the advice itself is valid, the personal attacks and abuse are not, and never will be.
I agree with @MalcTheOracle that the pics all focus on support interfaces which are usually printed with a specified z-distance to allow removal. This causes lines above to sag a little, so they look like they do.
To counter this, a z-distance of 0mm must be set. If using the same type of material, it’ll fuze with the model, making removal even worse.
Since PETG and PLA bond quite badly, you can use a PETG interface material for the interface. Just select a loaded PETG as a support interface and the slicer will drop z-distance to 0mm if confirmed by the user.
In some cases, it can be neccessary to play a little with the nozzle temps but it generally works quite well on smooth overhangs.
You can also go to water soluble support interfaces. I prefer BVOH over PVA personally. But those is a little bit more difficult to work with.
It might be best to simply let this matter go. All the posts were removed long ago - yours, mine, and everyone else’s. Calling some of the forum’s most genuinely helpful members toxic doesn’t really reflect who they are; they’ve spent years building a reputation for kindness and support - and no, I’m not talking about myself.
I hope that someday you’ll see that most people truly were trying to help, even if a few jokes may have missed the mark.
“Often things printed at an angle don’t look smooth, or removing the supports leaves a coarse surface.”
Indeed - the supports are one of the major factor of imperfections I’m trying to remove.
Printing PLA with PETG or “PLA support” interfaces are indeed valid options to improving supports visually. I’m aware. The problem is they add both print time and filament usage to the print.
Again, not something impossible. Just a solution I’m already aware of, and am checking other options.
I’m not sure you’re referring to the same thread I’m referring to.
In any case, there were toxic responses (I can provide you with examples via a DM if you’re interested|). And I’m done discussing it here. This is not the aim of this thread/post.
Letting things go, is a good advice. I suggest you yourself follow it as well. I’m referring to comments like this ones for example, where you try to paint me in a negative light (as stubborn/unwilling to adapt, adding people to ignore list without reason, etc.):
If you are not going to paint the model, your only real option is vapour smoothing.
edit That being said I am told Galactic Armoury (a cosplay company) has some tutoral videos on no paint cosplay, but it requires the models be designed to print in a specific orientation to improve surface quality - and are very large making the layers less noticable. 2nd Dynasty on myMinfactory have also started to explore this with their newer kits (I think the Skolpadda), but again, their kits are designed that way from the start.
Changing orientation is a good idea - I definitely do it when possible.
In some case even printing the model upside down entirely can bring about both better quality of the finished results, and reduction of supports needed (thus reducing both filament and print times).
I usually print characters from games and this usually works well with humans/creatures with hats on their heads.
 &