Reason: When AMS HT is trying to load the filament, it stops just a cm before the extruder and reports loading error.
When you open to lid of the printer and lift the PFTE tube with your hand, loading goes without problems – so the problem is in the tight circle and bend of the tube!
It would be much better if Bambu Lab would correct the firmware so, the extruder would move towards the front of the printer when loading filament, so the PTFE tube would extend to maximum/optimal length!
The AMS HT is very capable of loading filaments with the extruder parked over the waste chute.
If you’re seeing filament loading fail due to the final bends coming into the extruder, you have a problem with your PTFE setup, and it’s only going to get worse with use.
Disconnect your PTFE at the AMS unit and manually feed a piece of PETG through the tubing all the way to the toolhead, feeling for areas that the filament hangs up on drags on, etc. These are signs there are issues in that particular spot that need to be resolved.
Also, you should consider printing the tube guides that Bambu includes in the Filament Track Switch mount on MakerWorld, I recommend them for anyone with AMS units who are having PTFE issues. A lot of resistance comes in right at the point where the PTFE exits the AMS in some cases.
If you post pictures of your setup we can take a look and suggest improvements as well.
Thanks for your answer, but I sincerely doubt the PTFE setup is the reason for filament resistance.
This is a completely new environment.
Bought two/three weeks ago (P2S and a week later AMS HT) .
Used all/only the original PTFE tubes.
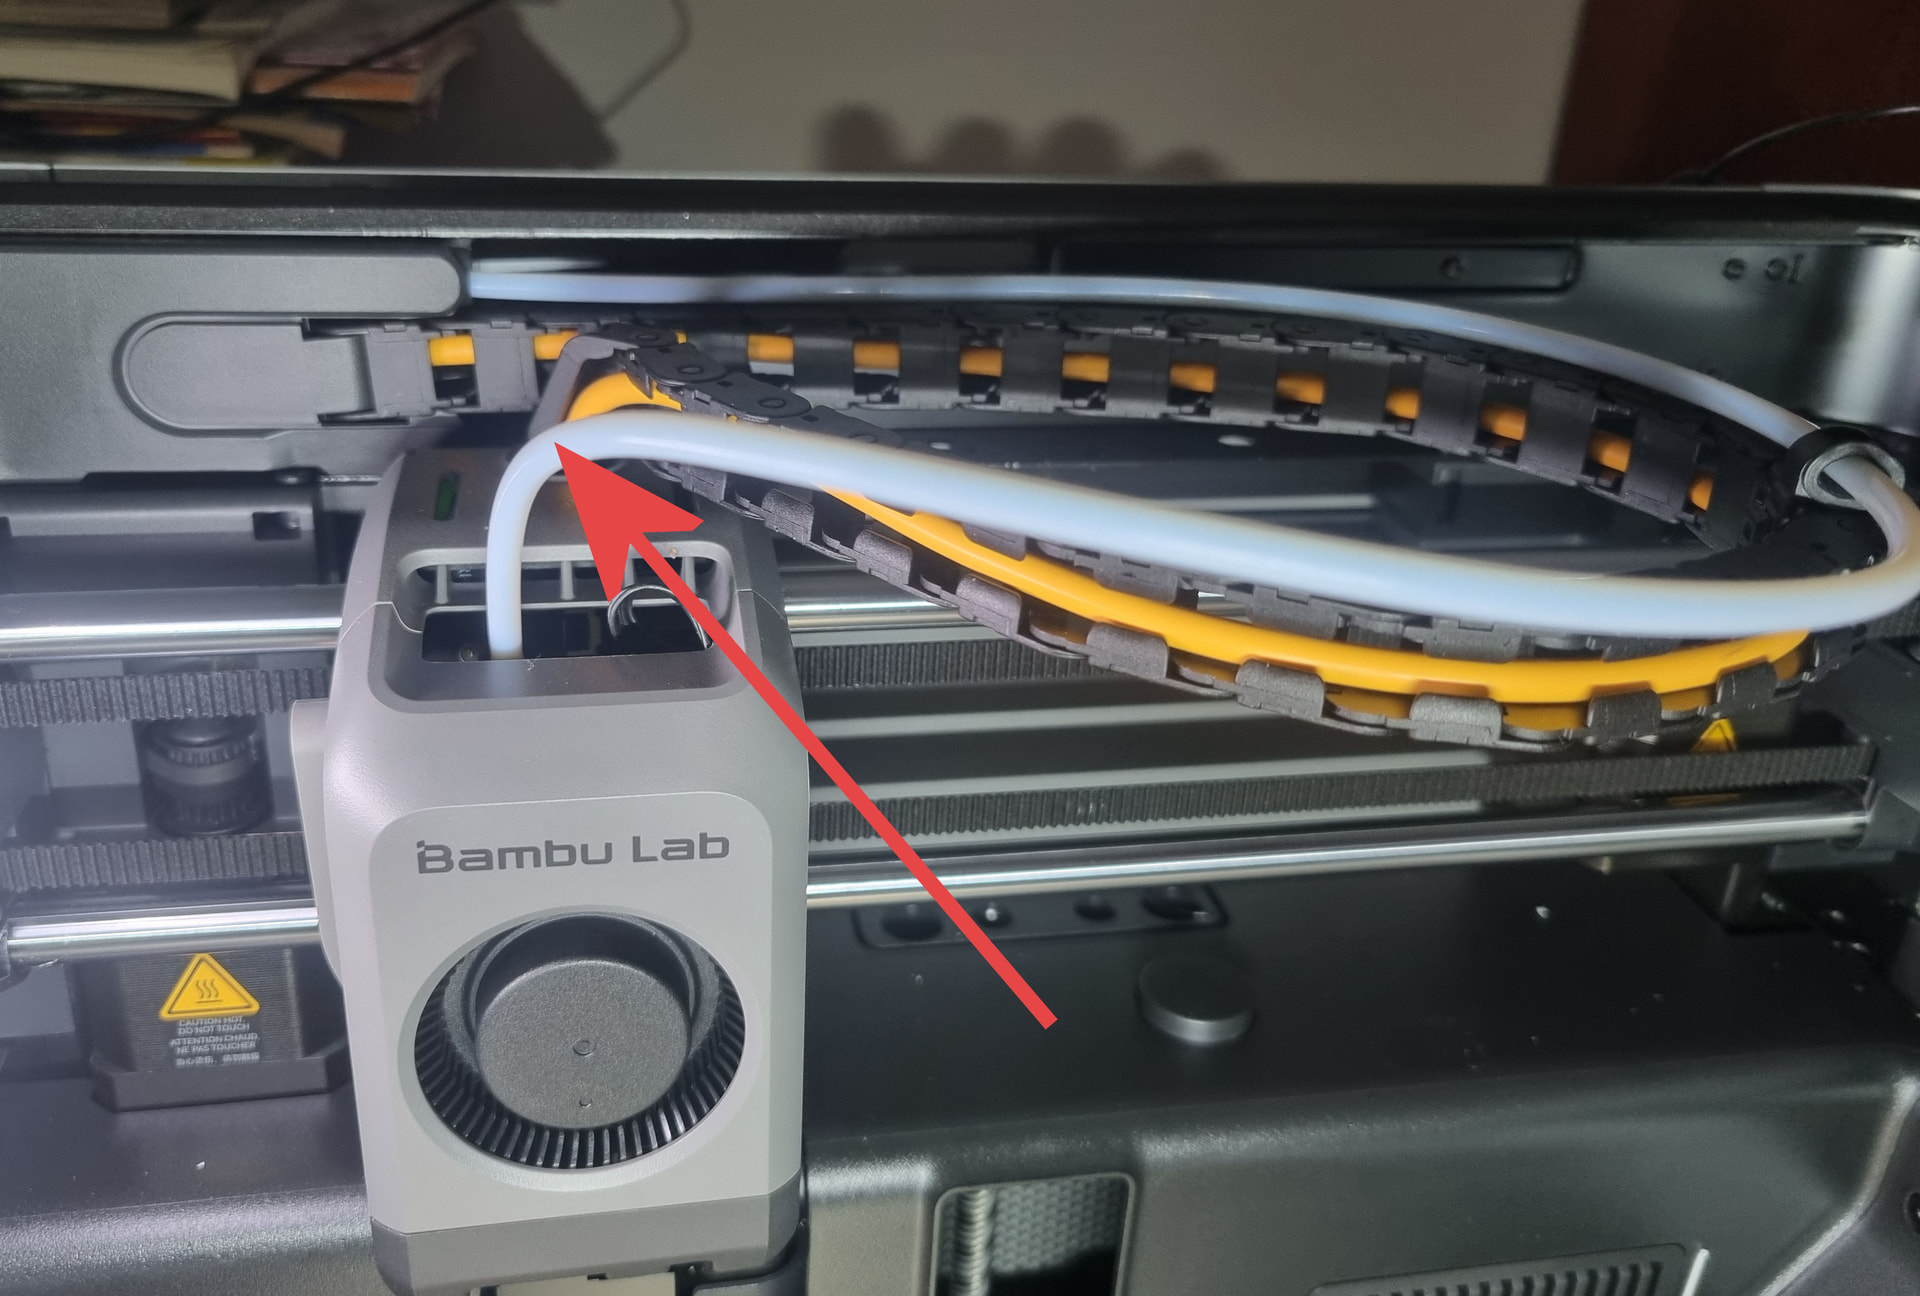
When loading, I can watch through the white PTFE precisely where filament stops. It is always cc 1 cm in front of extruder.
As mentioned above, when I open the lid and lift the internal PTFE just a few cm up, just so, that last bend in front of extruder straightens up a bit, loading works impeccably. This makes me convinced, that bending of internal tube is just a little too big and causes too much friction.
Pictures:
1 – internal tubing. I marked with an arrow where filament stops and start retrieving.
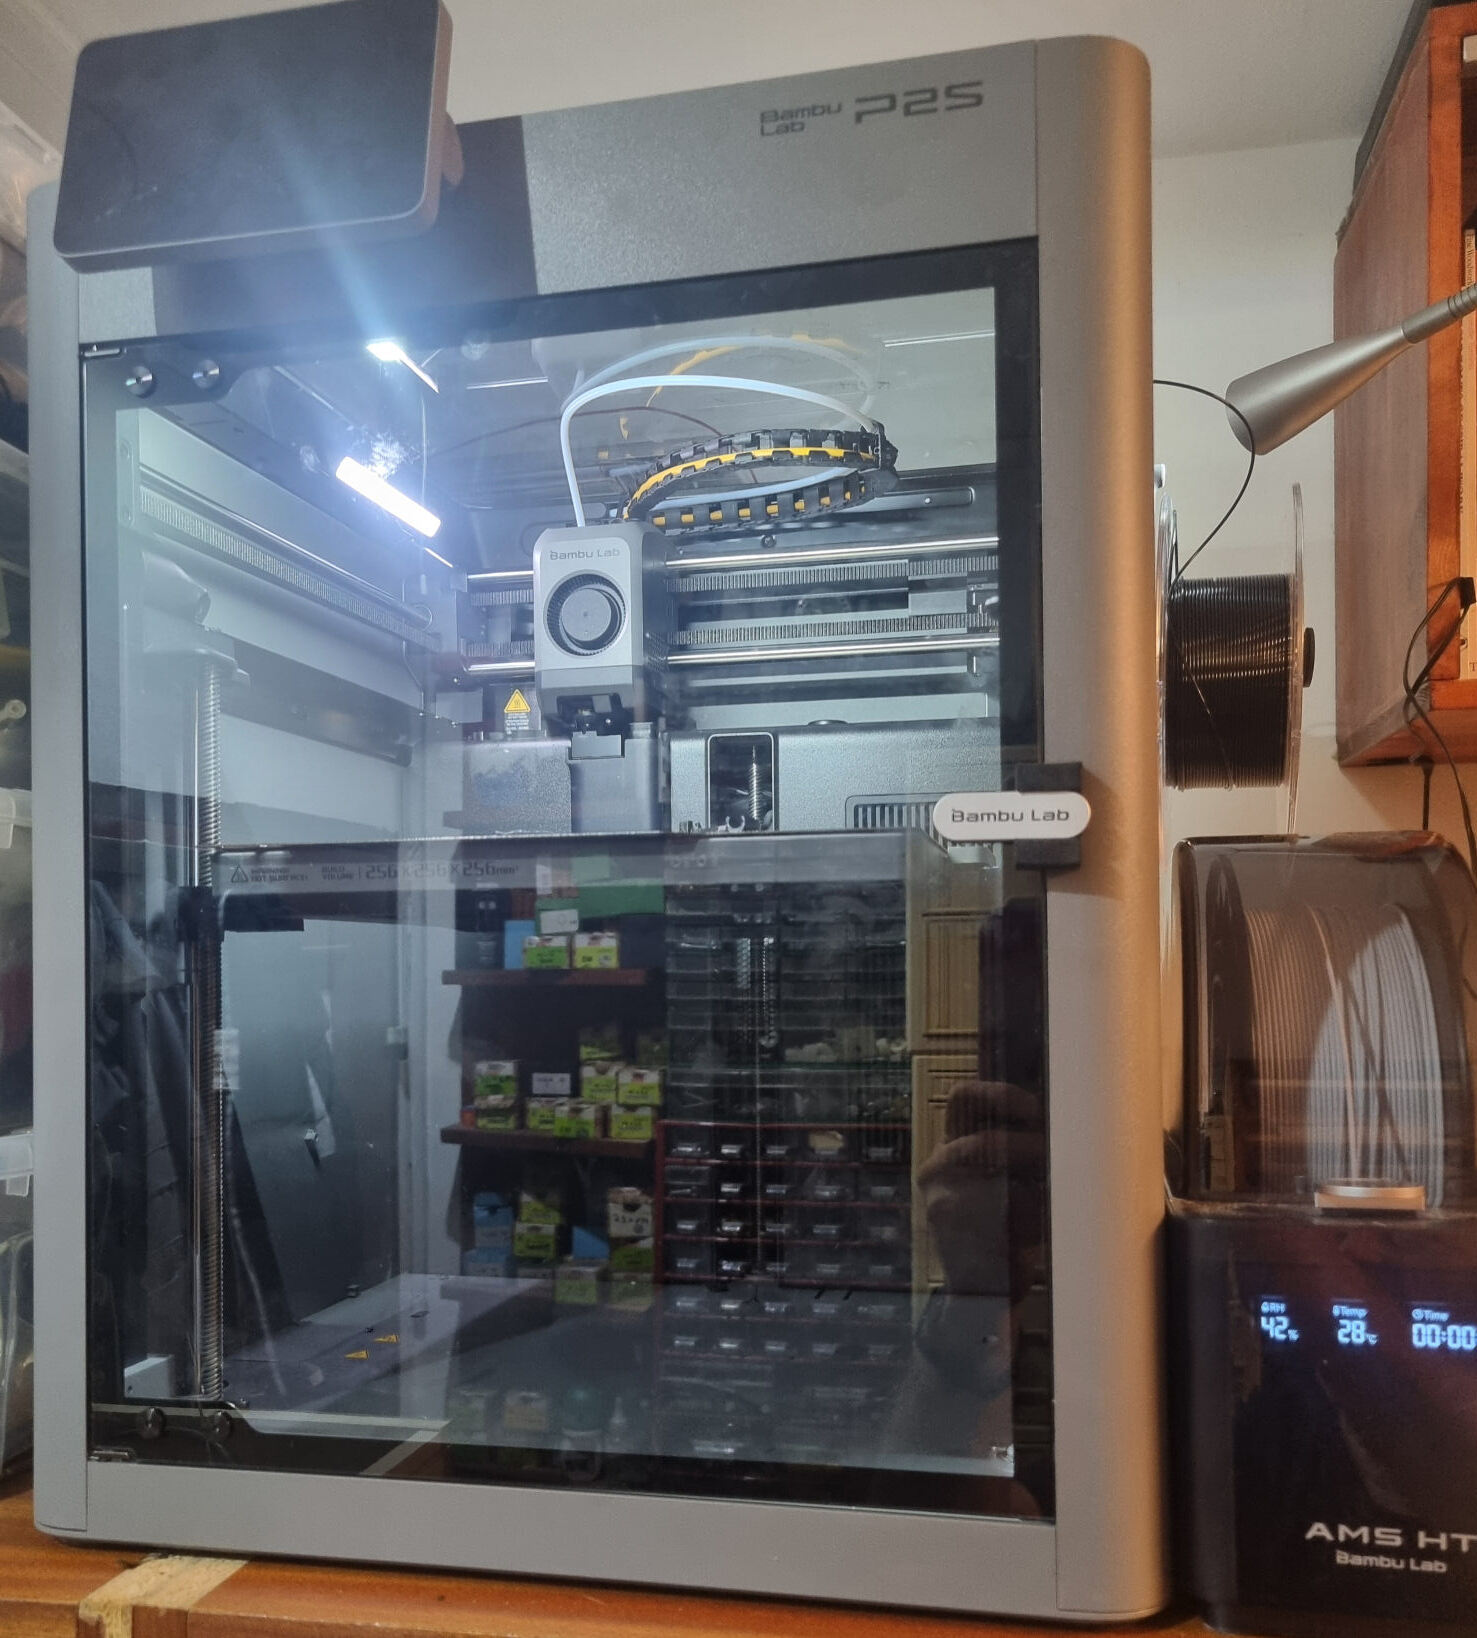
2 – Front, just to see that AMS is on the side.
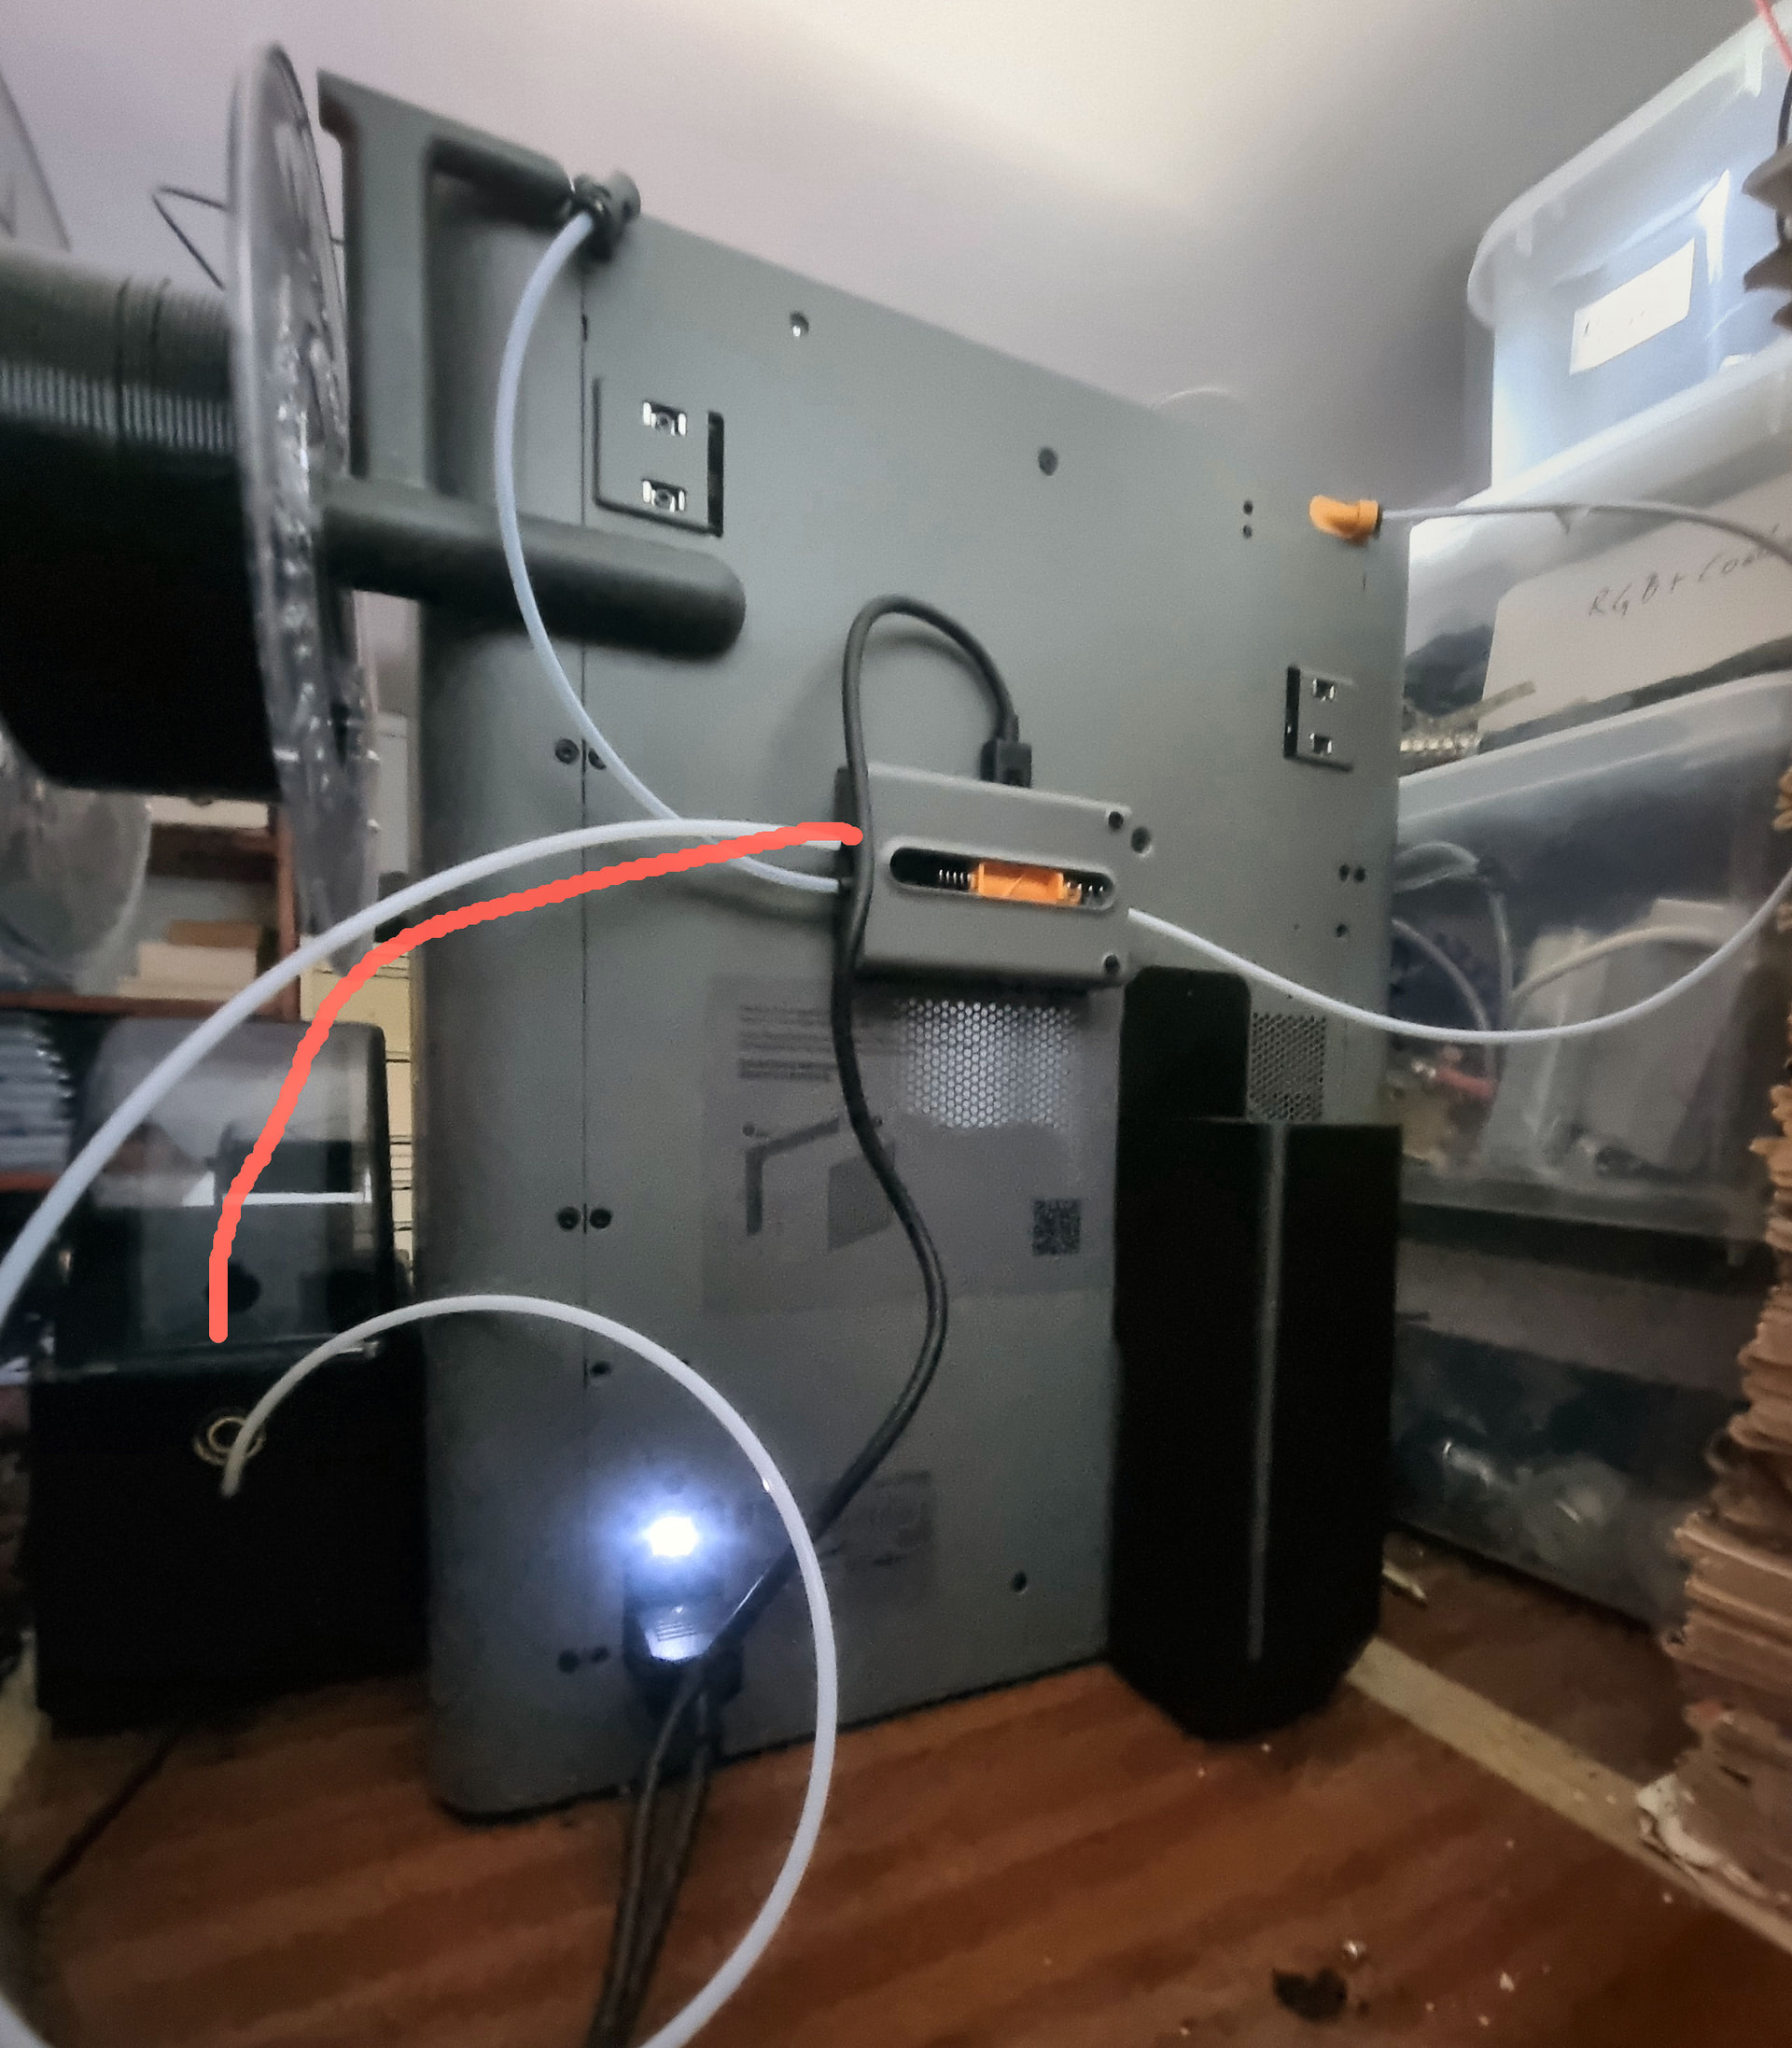
3 – Back. I marked with red, how it was when I used the shortest PTFE from AMS HT to the buffer. Now I replaced it with a longer tube, so the AMS does not need to sit on some stand for shorter tube to reach the buffer. I expect that it is better to shorten this one, but the loading error was not dependent on this.
I will try to use that tube holders you mentioned. I already printed one which is attached to the extruder.
Not really relevant. PTFE tubes cut out of square happen all the time, same with badly cut tubes that leave a crushed or partially obstructed opening.
Also, we frequently get people here who think they’ve inserted PTFEs all the way into connections, but don’t.
That’s why testing the entire path and checking every connection point matters.
Yes. That means all the cumulative resistance that the entire length of PTFE is generating reaches the limit of the AMS motor. We all know the last bend going into the extruder is a bit tight, but a whole lot of people load filament with no issues despite that.
Anyhow, your setup has unnecessary resistance because 1) Your PTFE from the HT to the buffer is way too long and 2) your PTFE from the buffer to the printer is also too long, and 3) it actually looks like your PTFE inside the printer to the extruder is too long as well, that would force the PTFE into a tighter curve than is necessary, further increasing drag.
CarbonForge
Yes. That means all the cumulative resistance that the entire length of PTFE is generating reaches the limit of the AMS motor. We all know the last bend going into the extruder is a bit tight, but a whole lot of people load filament with no issues despite that.
I disagree. If a cumulative resistance would be of any value (in my case), then when using longer tubes, blockage should appear earlier. And this is not the case. Always at the same point, with short and with long tubes. And I am underlining: when I lift the internal tube just a little bit, loading works. So the problem is precisely and only there. And if internal tube would not be so bent…
But you are correct: all the tubes now are too long, I will shorten them and see, what will happen. I am rather busy in the following days, but I will report the results. I also agree that most of users have no such problems, but judging by the number of topics of this type, not so few, do.
As mentioned above, I had problems with loading filament from AMS HT.
The situation was :
Absolutely new equipment (P2S and AMS HT), and of course included PTFE tubes.
Filament stopped loading just at the last bend towards the extruder head.
Just a small manual move of the internal tube helped to start loading.
Replacing the long tube from AMS to buffer with a very short one, made no difference.
What I had done:
I cut both ends of PTFE of both outside tubes (from AMS to buffer and from buffer to entrance of the printer)
I used a reamer to ensure that hole is round and without leftover edges from cutting.
And now it feeds without problems.
(My) conclusion is:
Even absolutely new tubes can have a problem although you cannot see it with naked eye.
I still think that Bambu Lab should change the loading/booting process. That preparing before printer starts really working, when there is all those gymnastics of moving head, table up and down, heat on and off, is a perfect position to move extruder head to the front position and load filament, just to improve the firmware and avoid users spend hours of searching for solution.