Background:
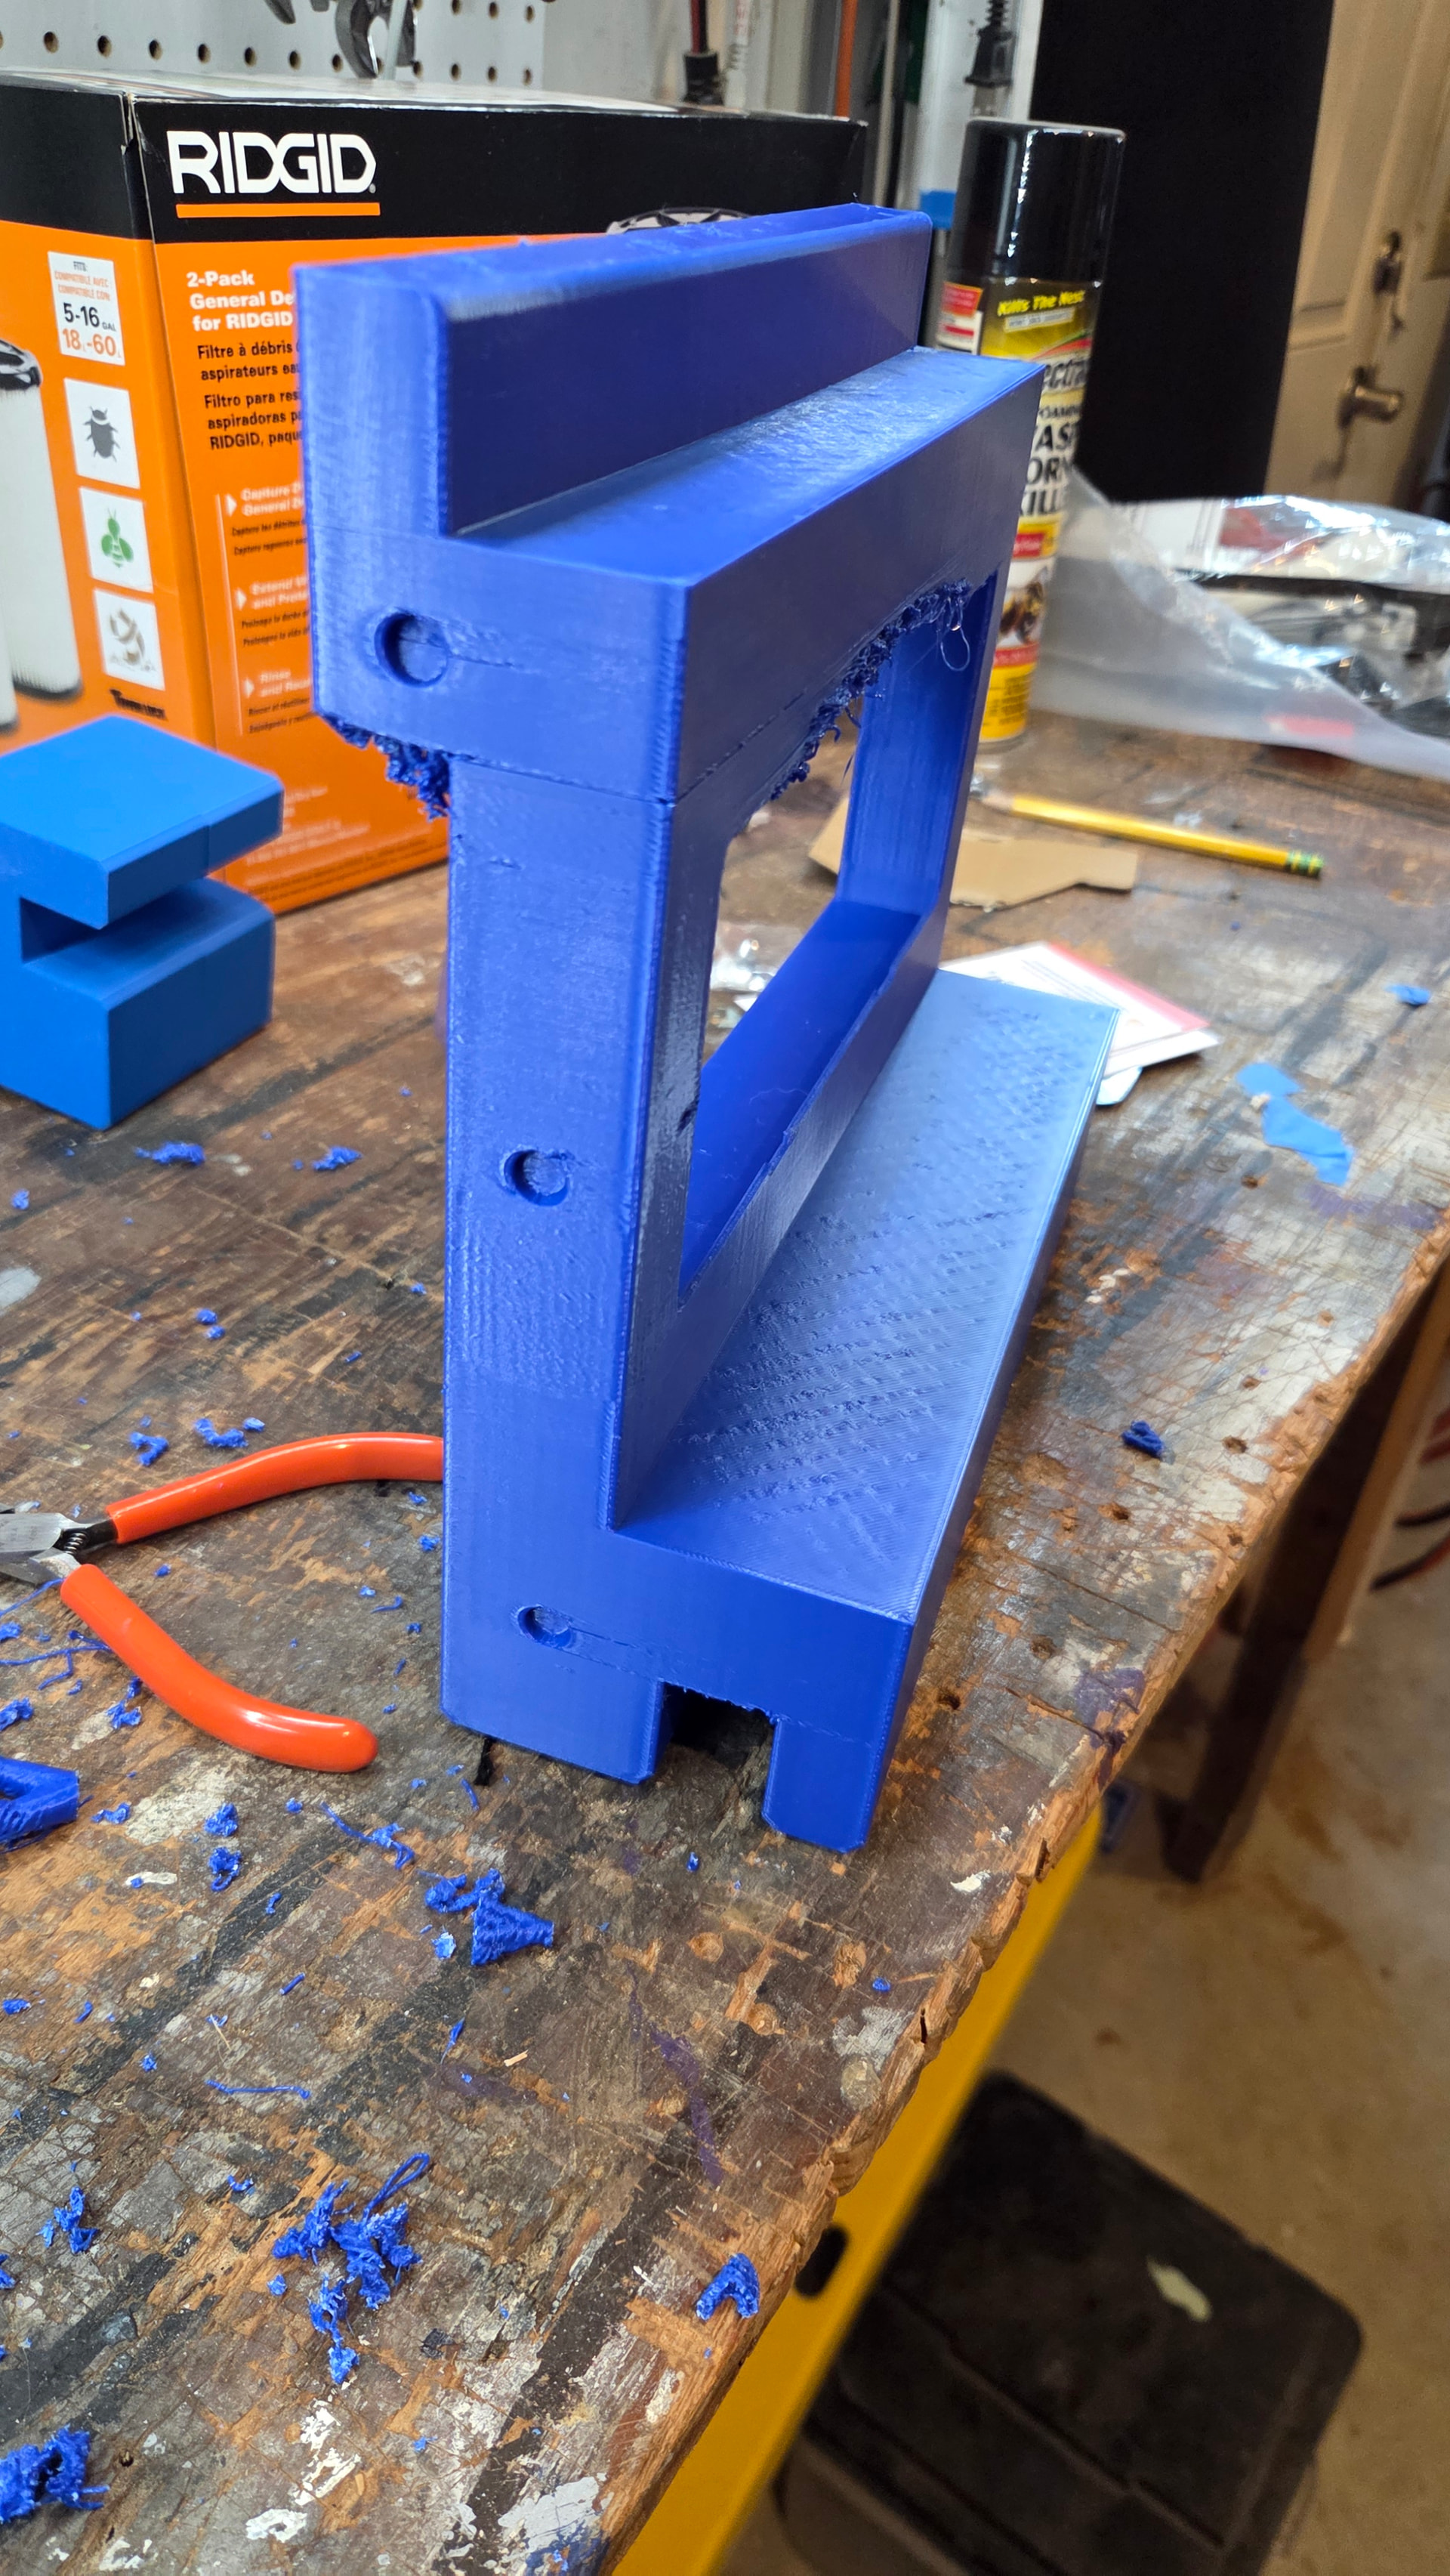
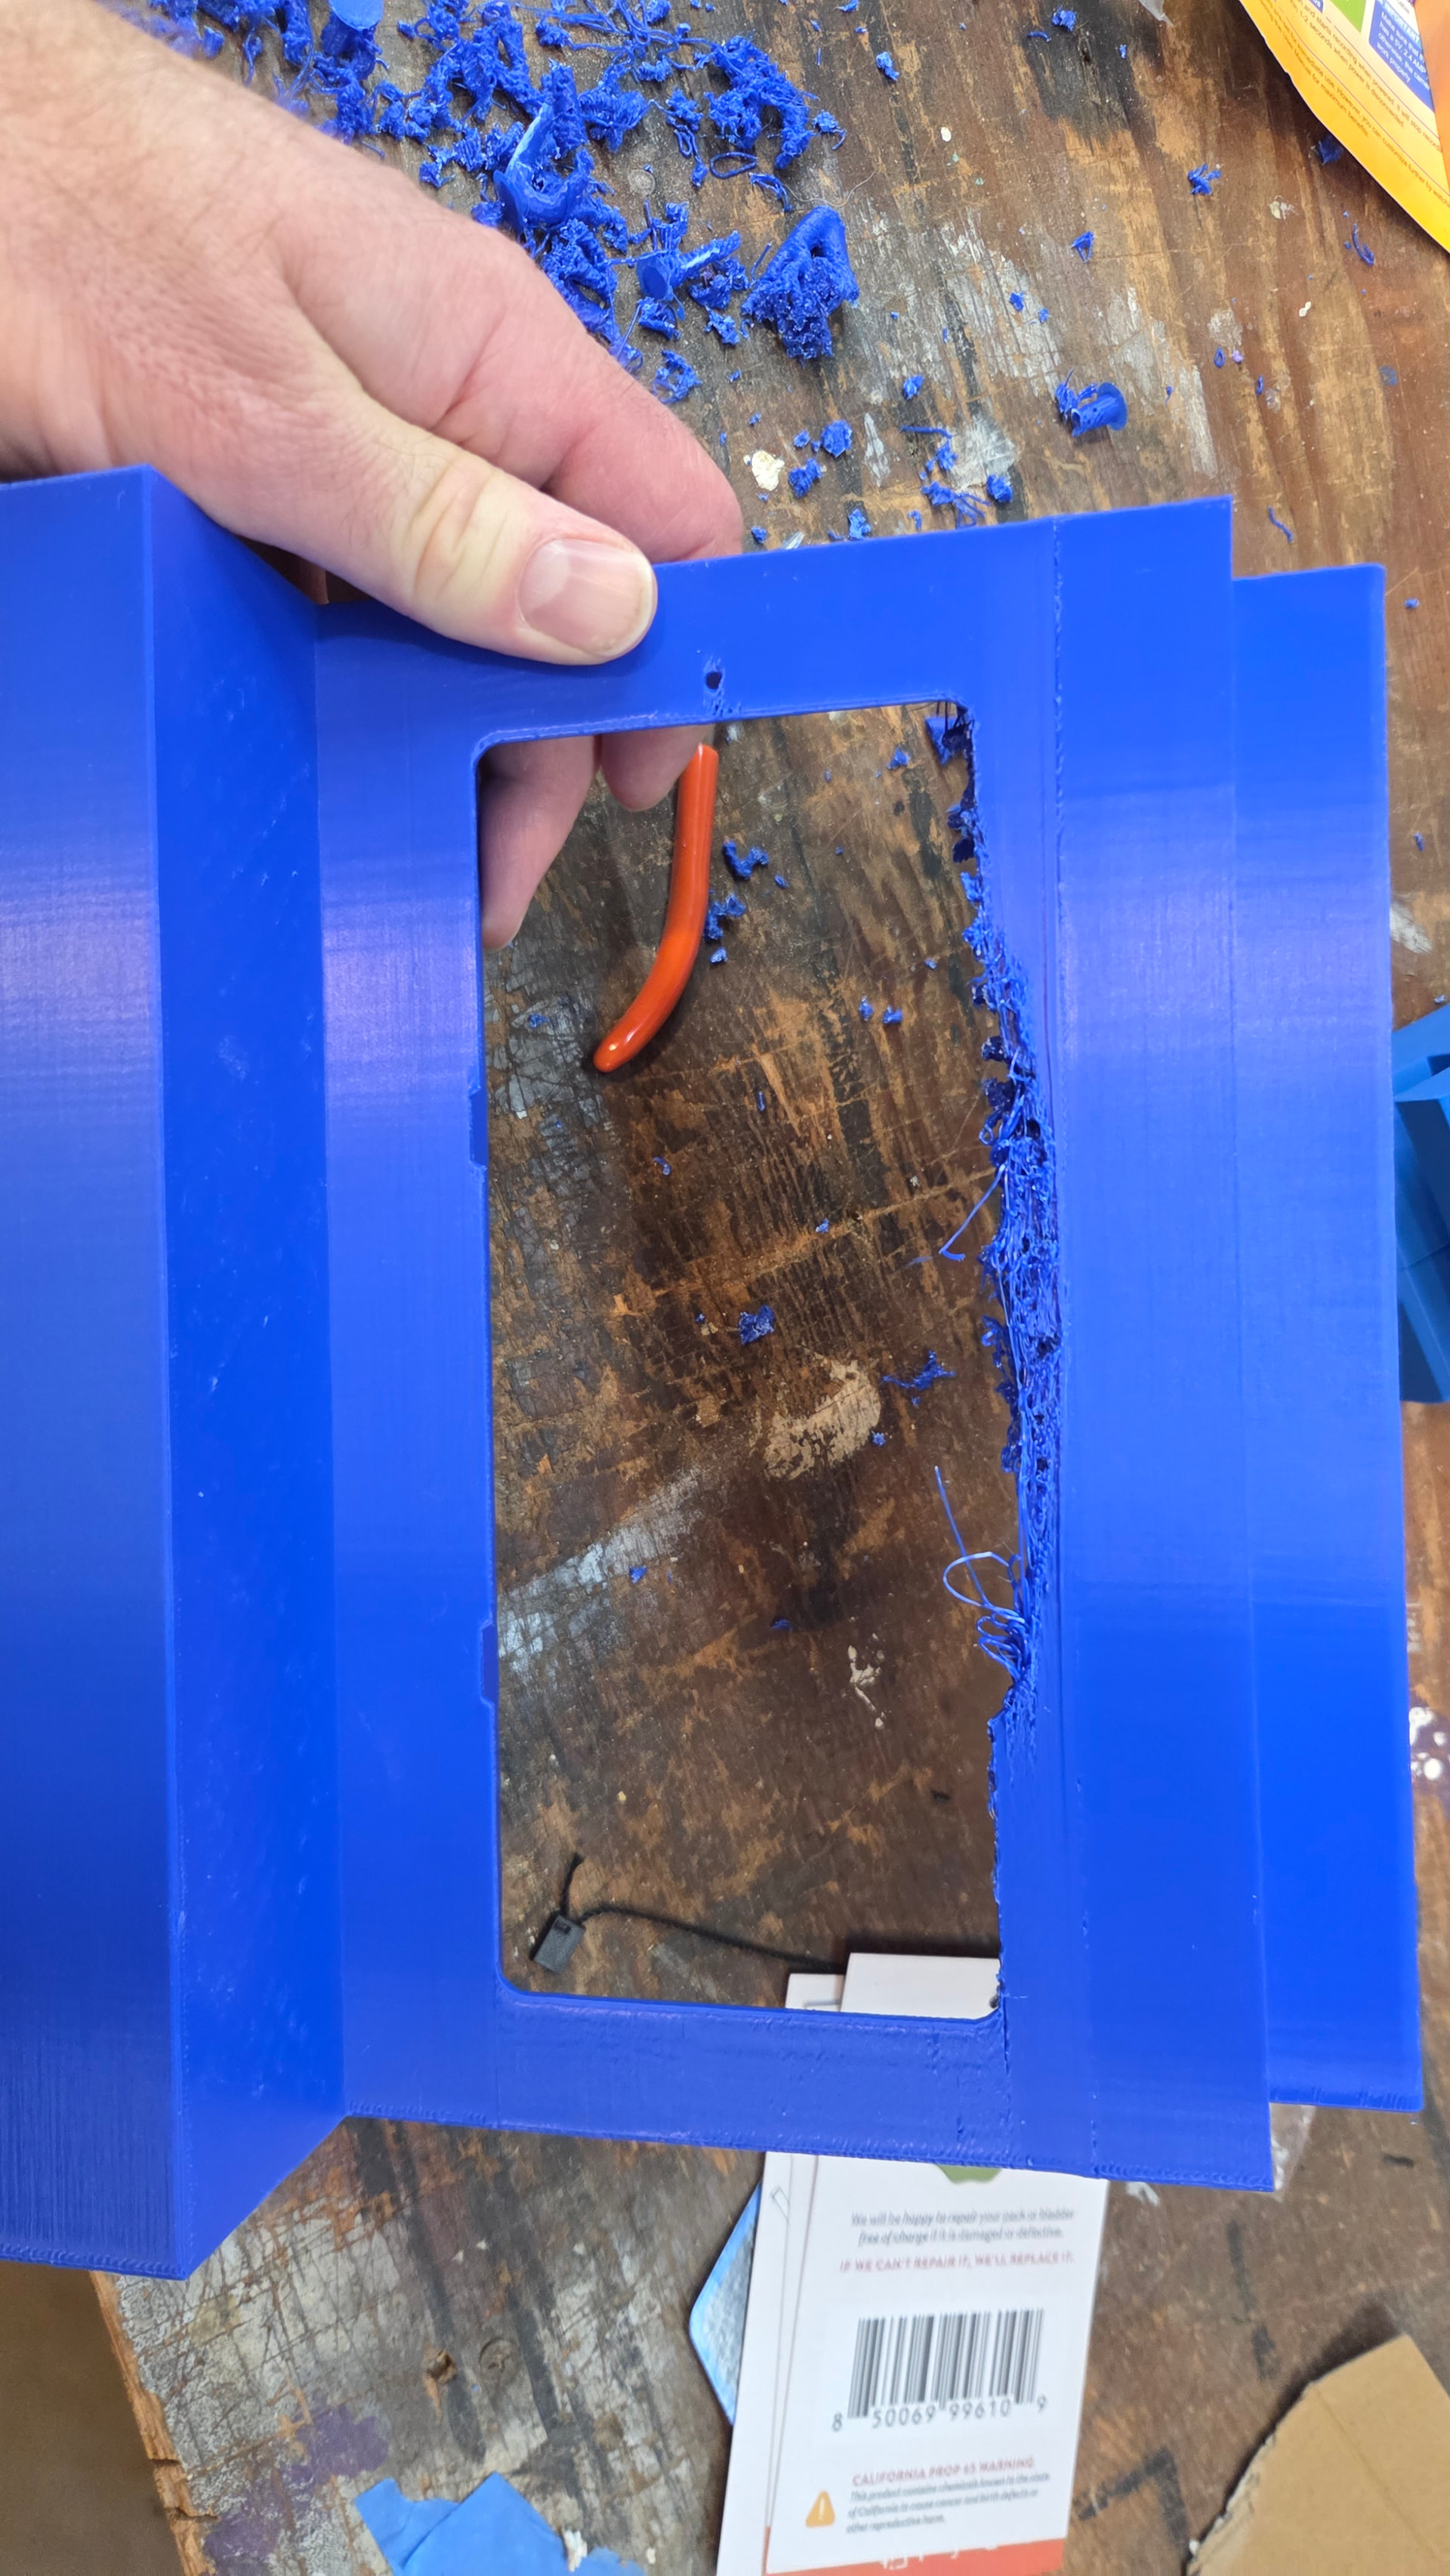
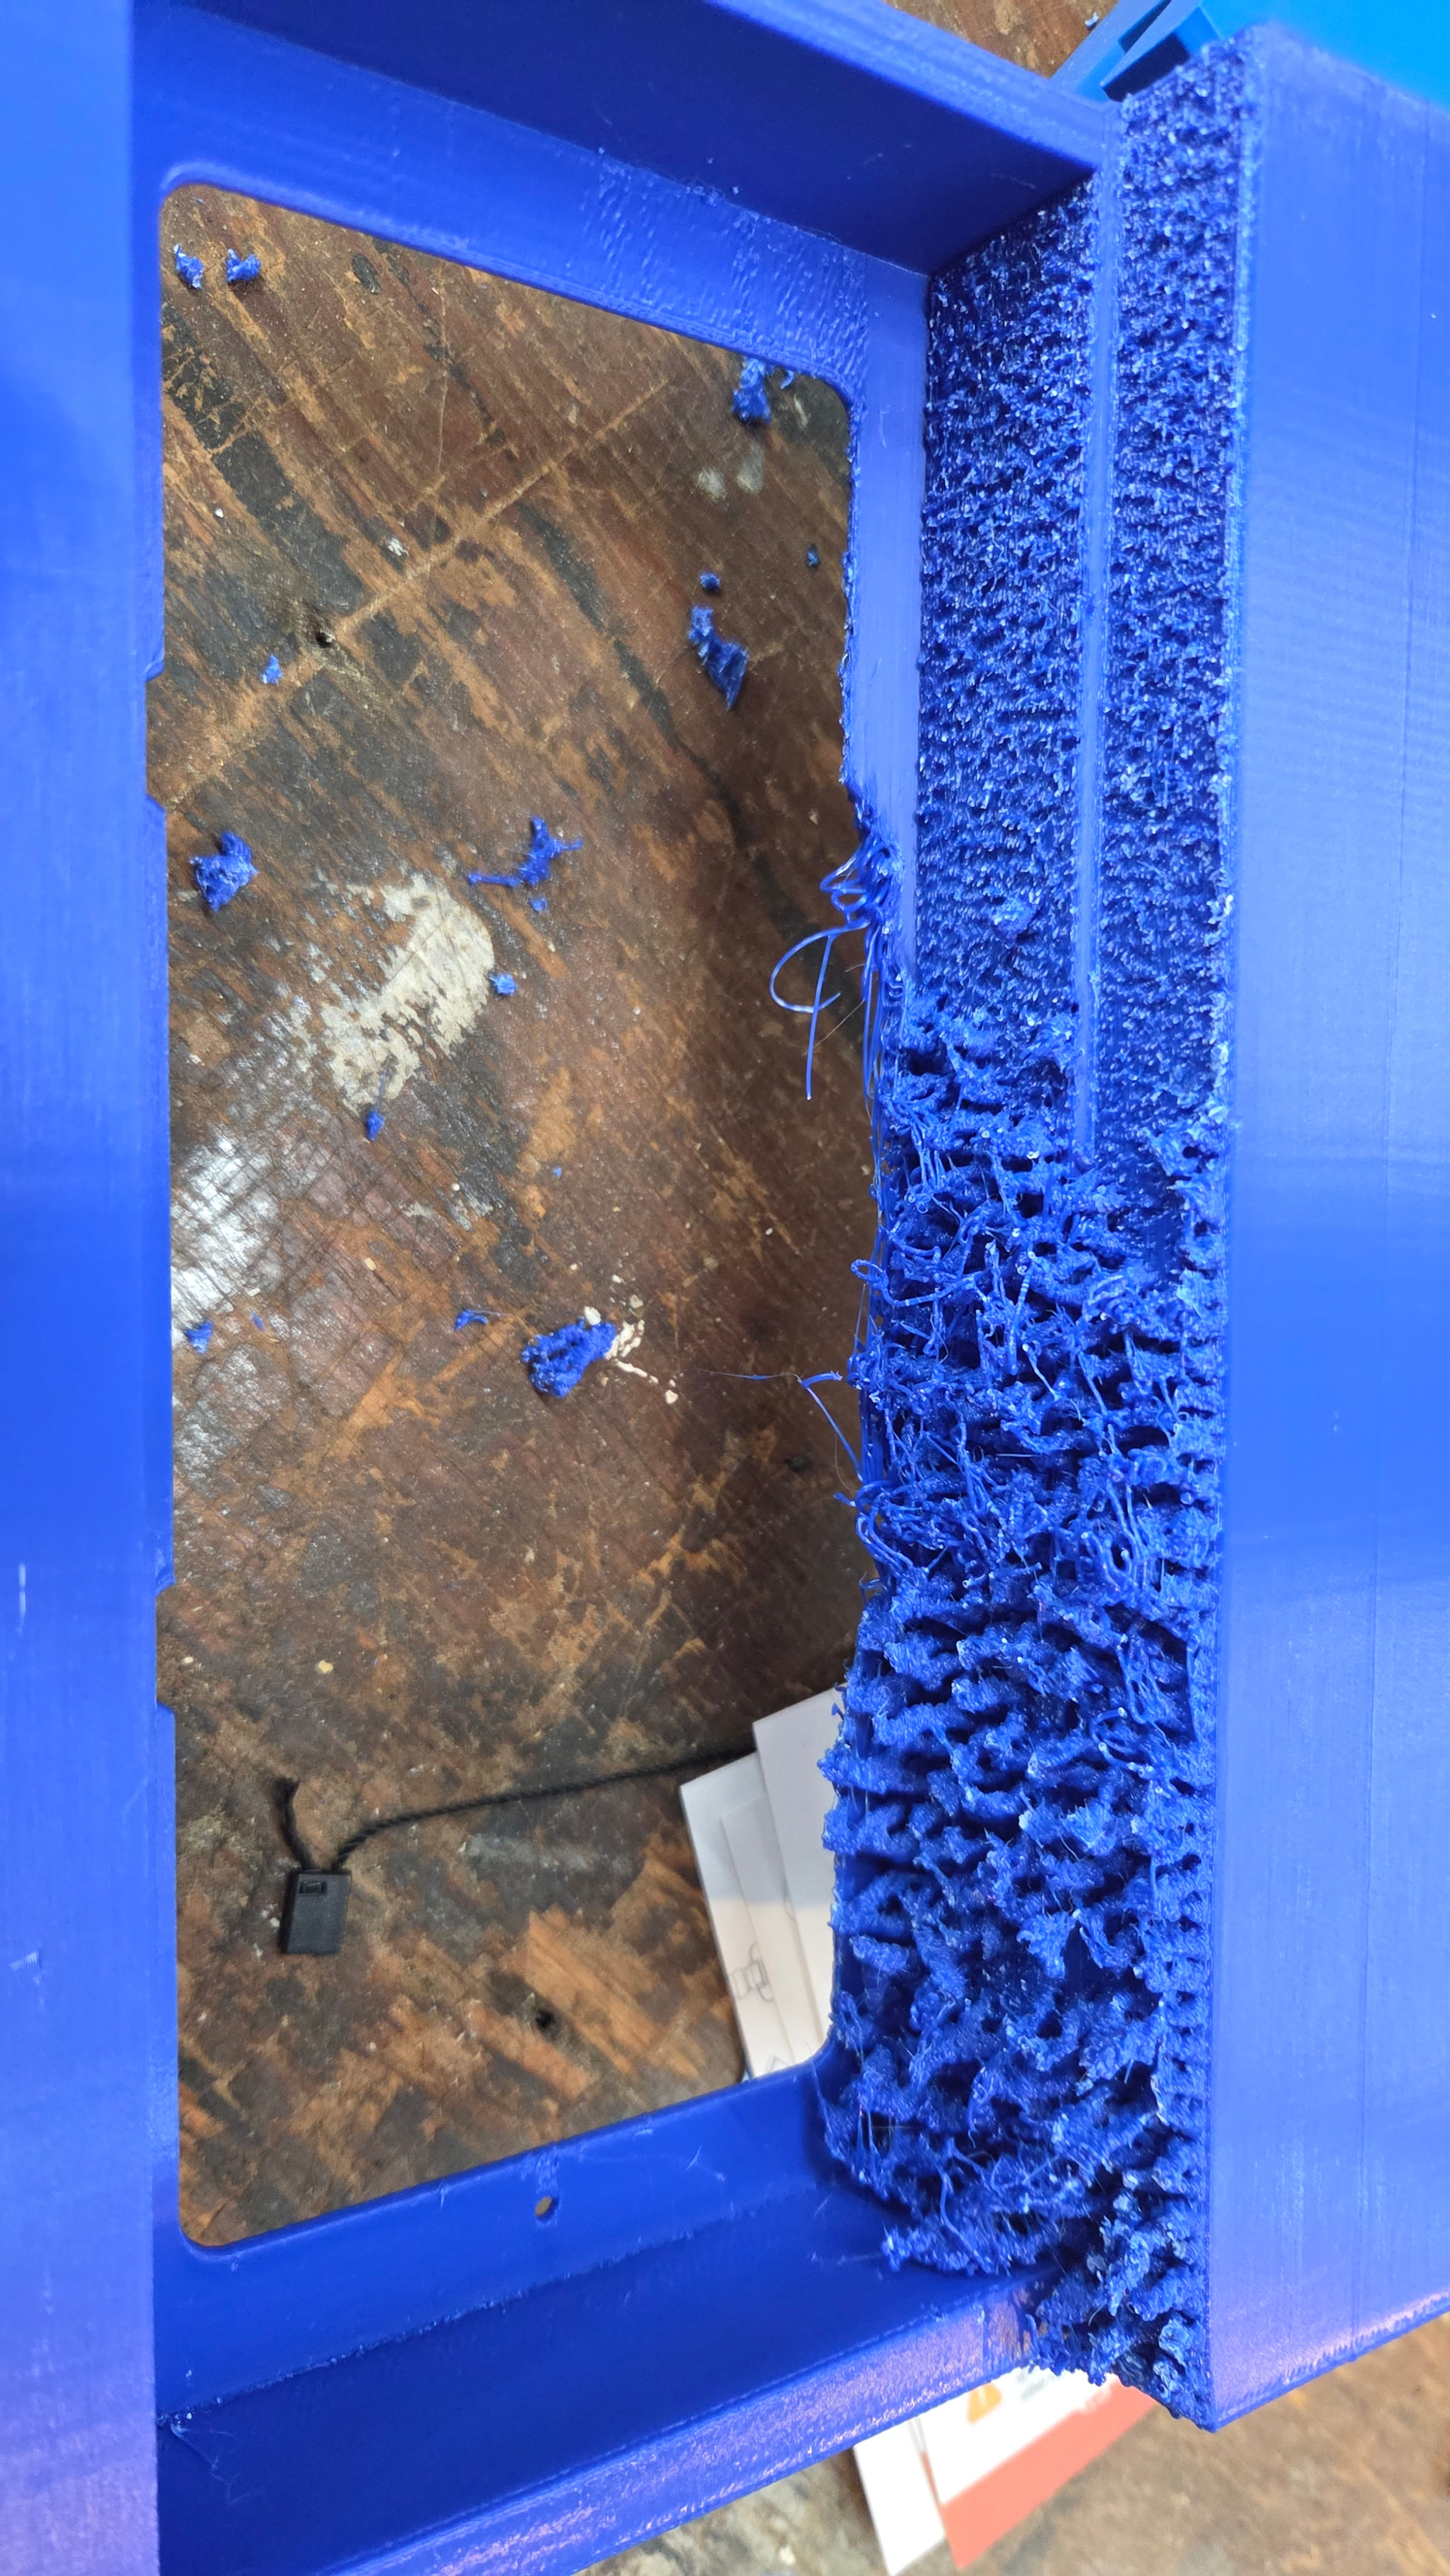
I am trying to print an adaptor for our floor air conditioner’s window exhaust port. The one the came with the AC sucks and falls out of the window all the time. The window is 39” wide, so I broke this print into 5 pieces. This is the biggest piece and has the feature for mounting the exhaust duct. I printed it in the orientation shown, The rectangular cutout is .070” thick to interface with the snap features on the duct. This piece just barely fit in the work envelope of my printer so I printed it vertically (tall and skinny). You can see that it failed the rectangular cut out and the support surfaces are pretty roughly and tough to de-burr. I am looking for some advice on how to go about printing this better.
Here is the setup:
-
Printer - Bambu P1S.
-
I just upgraded hot end and extruder to the hardened steel version before this. Did one PLA test print that came out fine. Then printed this
-
Print material - ABS
-
AMS system loaded the ABS fine and the Bambu app knew it was ABS material.
-
I left all default print quality/strength etc settings - except I enabled supports
- At end of print, one big support from roughly the center of the rectangular cutout had broken off the plate.
I think that because the PLA test print (.070” thick flat piece with the duct interface geometry) came out alright that anything to do with the extruder/hot end upgrade is unlikely, however, I recogize that issues like this can be thermally related.
I think that the orientation of the print, the geometry (skinny/tall, high overhangs) led to poor support generation or adhesion. My thought was to lay it down on one side or the other. I am curious to get some feedback on this idea.
You can see the .070” thick section with the pocket on the backside. Would you orient this part pocket side down or pocket side up? I think pocket side up likely will print better, but open to some input here too.