H2C Nozzle scaping in EVERY print

I am going insane.

I have not made more than a couple of good prints with my brand new H2C.

I am a noob but have been diving into things as much as I comprehend at my current state.

I am printing with PETG.

Almost all prints fail, and I cant figure out why.

Initial layers always have some issues. Sometimes I get several hours in before issues - sometimes it is the initial layers. They all fail:
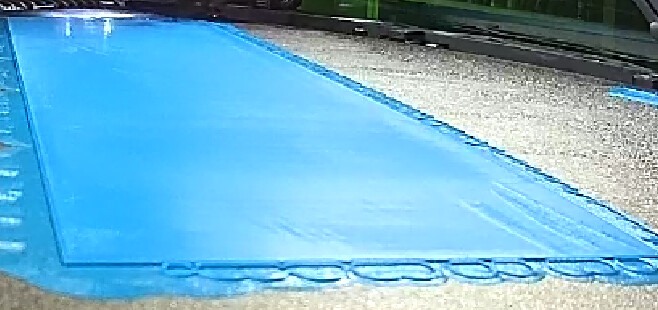
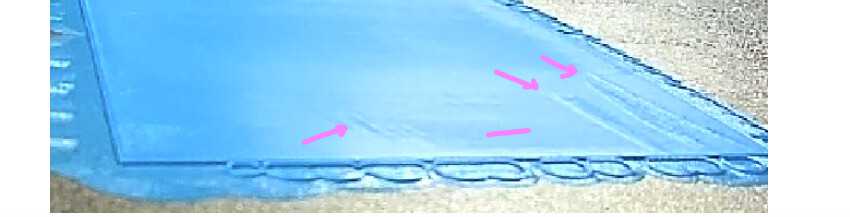
Looks good but there are already some errors.

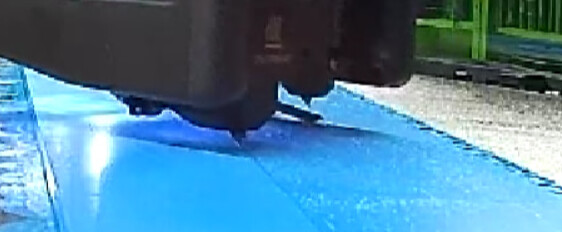
Next layer - heavy nozzle scraping - print WILL fail again.
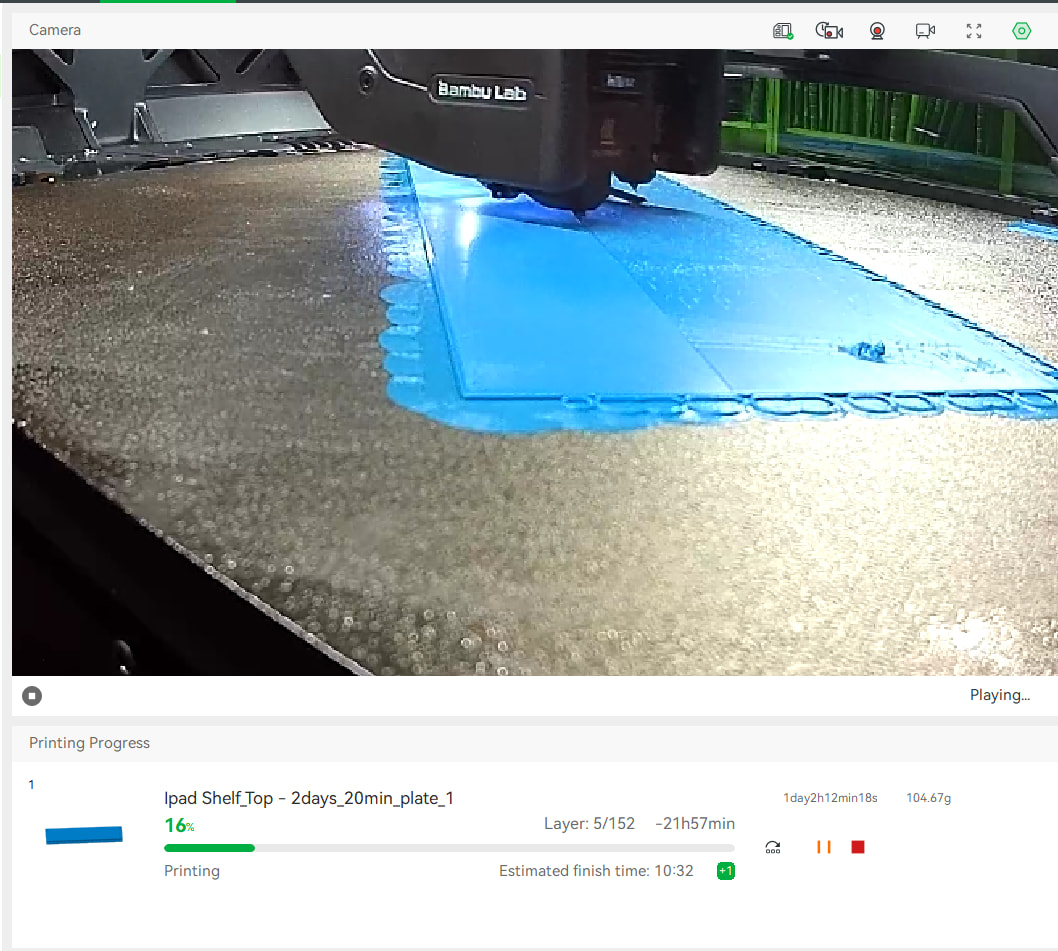
This seems to always happen and I cannot get 1 print to work since I started trying finer prints with 0,2 nozzle.

What I’ve done:

Flow has been calibrated to 1.06.

PEI temperature has been tried with 70, 75 and 80 degrees - this one is 80 and still failing, butthis time there doenst seem to be warping - had warping on 70 and 75 - but I did not use glue. This one 80 degrees and glue - no warping.

I am printing at Nozzle temperature 230 degrees - Initial 245. Calibration found no stringing at 230 but stringing at higher temps.

I have calibrated the machine several times.

I have tightened the screws behind the nozzle holder which has helped a lot - but now prints just fail later instead of sooner.

And yes - I dried my filament. It is 18% at the moment.

I ALWAYS get nozzle scaping at some point and it leads to every single print being ruined and 95% of them can’t be finished. The other 5% has such bad scraping they are just too fugly.

Can anyone tell me what settings I am missing or screwing up? The printer is useless at 0.2 nozzle - but most of my 0.4 also fail, though a few can actually be used.

Does anyone know why this is?
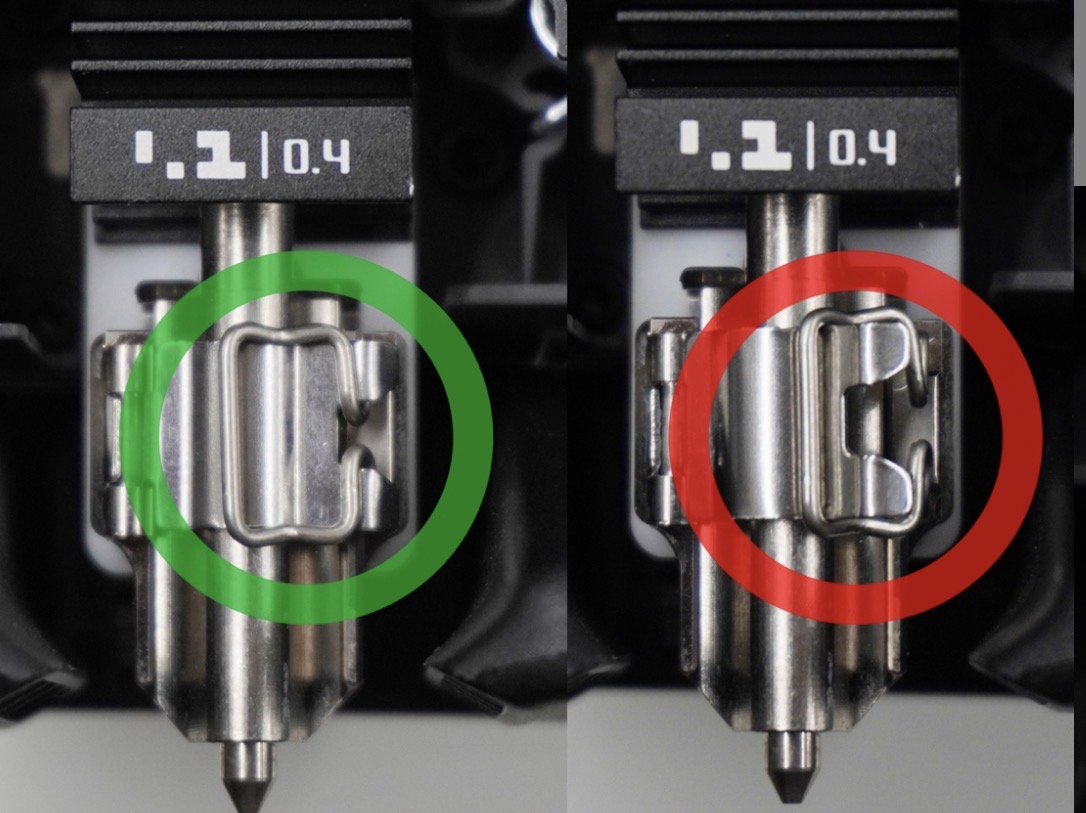
I’d check your left nozzle latch first thing. It’s got a terrible design that’s easy to latch incorrectly which can cause scraping. Pic attached showing the correct way. I doubt it’s the problem because normally the scraping will be much more pronounced, but it’s worth checking and just takes a second.

Any chance it’s the flow blocker bracket doing the scraping? Hard to tell from the picture, but it does look a bit low to me.

Does it make a difference which side nozzle you use?

Printer fully calibrated, I assume. Perhaps post an example project that fails like this… may or may not be revealing. Does seem like a systemic issue, but that could be some incorrect base setting I suppose.

-Max

I checked for this. This is not the issue. Mine is latched like the left side of the picture.

No. I’ve been looking at it as it scrapes. It is the nozzle. Problem is bambulab does not have a Z-offset so I cant experiment with that. It can only auto Z-calibrate.. I don’t know what I am doing wrong for this to happen on every print.

I will post pictures when I get back to the office on monday.

@ronnyburger This might be a frustrating troubleshooting process - but bear with us please.

I agree that your nozzle is doing the scraping, but that’s a symptom of a bigger problem - we need to get to the root cause.

The flow blocker is obviously bent and not blocking ooze from the inactive nozzle - it would be a problem for both extruder sides. If the nozzles are allowed to ooze freely, it will drop blobs of material that can be caught and torn up on the current print.

There’s a bigger potential problem on the NEXT print’s nozzle offset calibration though - if nozzles are oozing and it just doesn’t want to come off during the offset calibration phase then that calibration will be off and the entire next print will be compromised.

I recommend starting here and making sure all of the steps are followed:

A few other questions:

  1. Has it ever given nozzle offset calibration errors?
  2. How do single-nozzle prints go, for both left and right sides of the printer?
  3. Is the nozzle offset calibration sensor at the back of the bed clean and in good shape?

If you haven’t already, put in a ticket with Bambu support, so there’s a paper trail in case this is a persistent error and you need to push for a warranty replacement of the whole machine - there’s a limited window for that.

this is a huge misconception in the 3d printing community
Z offset is a static offset for the entire print, every 0.20mm layer is still exactly planned to be 0.200000000mm between each other, no matter what your z offset is. You’re just changing where the nozzle is in absolute space, all relative space inbetween each of your thousand layers is the same. That one layer that was being worked on where you changed z offset is the only one that would be less than 0.20000mm and then every single subsequent goes back to being exactly 0.20000000000mm
Z offset will not effect you if every single layer is scraping on the last

IMO if its a software/slice problem, this right here looks like too much flowrate, piling and pushing into the final corner of a long flat area.


Additionally on a 0.2mm nozzle, textured PEI can be unreliable, smooth or satin may be of help.

I agree, the flow blocker looks bent, even if it is not touching the part.

People often think it’s a problem but this is 100% a carryover from old style printers.

For a given two-color left/right nozzle print on the H2C, the offset value (the tip to tip vertical measurement between both nozzles) is a single fixed value and shouldn’t ever need to change during the print.

The nozzles aren’t (supposed to be) moving in their mounts, and the length of the nozzles doesn’t change. The left nozzle just moves up and down, the “active” height position should always be the same, and the “stowed” height position should never change. Then, the printer only needs to apply that offset to the bed height when the given “offset” nozzle is active and that ensures both nozzles are working at the same height relative to the bed for each layer.

…which has me thinking now…

  1. Which nozzle does the scraping when it happens? Is it the left, the right, or both?

  2. Which nozzle holder did you tighten screws on? Which screws?

  3. Are there ever any weird sounds or behaviors when nozzles are changing?

I’m starting to think it’s something in the change mechanism misbehaving, either a bit of debris, an alignment issue, or something else, that’s resulting in inconsistent positioning of the left nozzle in the “active” position, or inconsistent holding of the induction nozzle.

It calibrates at the beginning of the print, gets an offset value, but that value doesn’t remain consistent for every nozzle change, and at some point in the print when it shifts you get the drag beginning.

Still fix the blocker issue, but this may be the way we want to go to figure this out.

another thing to add:

loose hotend screws? i.e. the 4 tiny ones that mount the heater block to the extruder?

Welcome to the forum @ronnyburger :smiley:

I think the key items (flow blocker in need of replacement, flow appears too high) have been mentioned a few times already. Although your nozzle temp appears rather low. With PETG Basic on the H2C, I start at 245°C (first layer only) but occasionally go all the way up to 260-265°C.

Since your catchphrase highlights you enjoying FDM and feeling new to it, there may nevertheless be a few additional notes that you may find helpful. In particular as you mentioned a few further troubles that are quite common.

PETG can be rather temperamental. And that is even when discounting the many brand differences and type differences (Basic, Transluscent, HF, Matte,…). PETG in general has a few characteristics than can make printing challenging:

  1. It reacts quite sensitively to moisture
  2. It loves to stick to the nozzle

So it is usually a less frustrating experience to get comfy with PLA first and then move on to PETG while keeping a few “rules” in mind:

  1. New filament has frequently travelled the 7-seas in not-fully moisture proof bags with a tiny satchel of dessiccant. So drying a roll after opening can make a big difference. However, the driers RH does not give any indication as to the moisture in the filament. Best to stick to recommended times and temps.
  2. Overextrusion is worse for PETG than other filaments as it quickly accumulates on the nozzle. Wipe-on-retract can help to reduce nozzle pick-up. Also, do not ever use the default “Grid” infill with PETG.
  3. Sooner or later you are likely to run into warping and/or curling. That happens with higher prints than the ones shown in the pic’s.

Did some of your prints fail higher up? That could explain not only a lot of print failures, but also the bent flow blocker.

On another topic:

I too have found the 0.2mm nozzles to be a bit of a challenge on the H2C. Originally, I struggled with “extruder overload” errors in longer prints (i.e. heat creep). However, running the troubleshooting chain from the nozzle through the extruder, the toolhead PTFE, the buffer,… I finally found a badly seated in-AMS2 PTFE to increase friction just that bit too much. And keeping the door open for PLA helped as well.
As for the troubles with the 0.4mm, a bent flow blocker can cause a lot of havoc.

Finally, just to double check, since you mentioned that you have already tightened the screws behind the nozzle holder. You have no nozzle movement whatsoever in z when you wriggle them? Just to rule out mechanical issues.

Hope some of this is helpful,
:crossed_fingers: & :four_leaf_clover:

  1. Yes a little handful of times. Usually I just run the calibration again and it goes through
  2. I haven’t paid attention to this detail. I will have to monitor this as the current print only runs on 1 nozzle I haven’t paid attention for other prints.
  3. Yes. The printer is brand new and it has no signs of wear.

Thanks for the tip about the Flow Blocker. I had not noticed this was a problem, as the printer was delivered that way. Thought it was correct out of factory.

I have adjusted the flowblocker to sit right at the nozzletip. I had around 5mm of air between the blocker and the nozzle. Let’s see if that removes some blobs.

Thank you for your input. I only have the PEI and Engineering plates. I guess I have to go get an upgrade at test that out :slight_smile:

  1. Not sure. I have only used the left one on this print - have not paid much attention to what nozzle I have used for other prints. It depends on what color is on which AMS unit.
  2. The left one - I unscrewed the holder, and on the back I tightned 3 of 4 screws. 3 of them had a little give the 4th was solid.
  3. No strange sounds. For now I am trying to get some quality prints with 0.2 nozzle so no nozzle changes. When manually changing nozzles it sounds “normal” although I am a beginner and have no experience with what “unnormal” would sound. But it doesn’t sound “wrong”

If there is some sort of debris somewhere that causes a misalignment. Where do I look for that?

I can tighten all of them quite a bit, but they also seem to be on a spring, so maybe they are not supposed to be tight?

Don’t know if I messed something up now that I tried tightening them all.

I loosened them again as it is probably by default that they aren’t tight?

Updated:

I see I messed up… you’re asking about the hotend scews - not plate screws :man_facepalming:

I have already tightened them on the back and screwed the block back on. The screws are not loose…

Thanks :slight_smile:

I did a PETG print Calibration print and it showed that 230 was ideal. 250 Degrees also came out fine, so I will test with 250 next.

Thank you. I didn’t realize that. I will have to dry the filament with the recommended ours instead of a target RH.

Didn’t know this. Noted.

Yes. Including on the lastest print, but the print height is still quite low. I will make a post about this later.

Interesting. I am not familiar with the troubleshooting chain. I can guess what it is, but is there some documentation that shows me what to be aware of as I go through the machine?

No nozzle movement. They both seem to be on there quite solid, and do not wiggle at all.

Indeed it was. Thank you. I have a few things to go over now :slight_smile:

The print actually finished. I did not expect that.

It stopped with “Extrusion Overloaded” many, many times but after cleaning the nozzle and restarting a multitude of times, it actually finished.

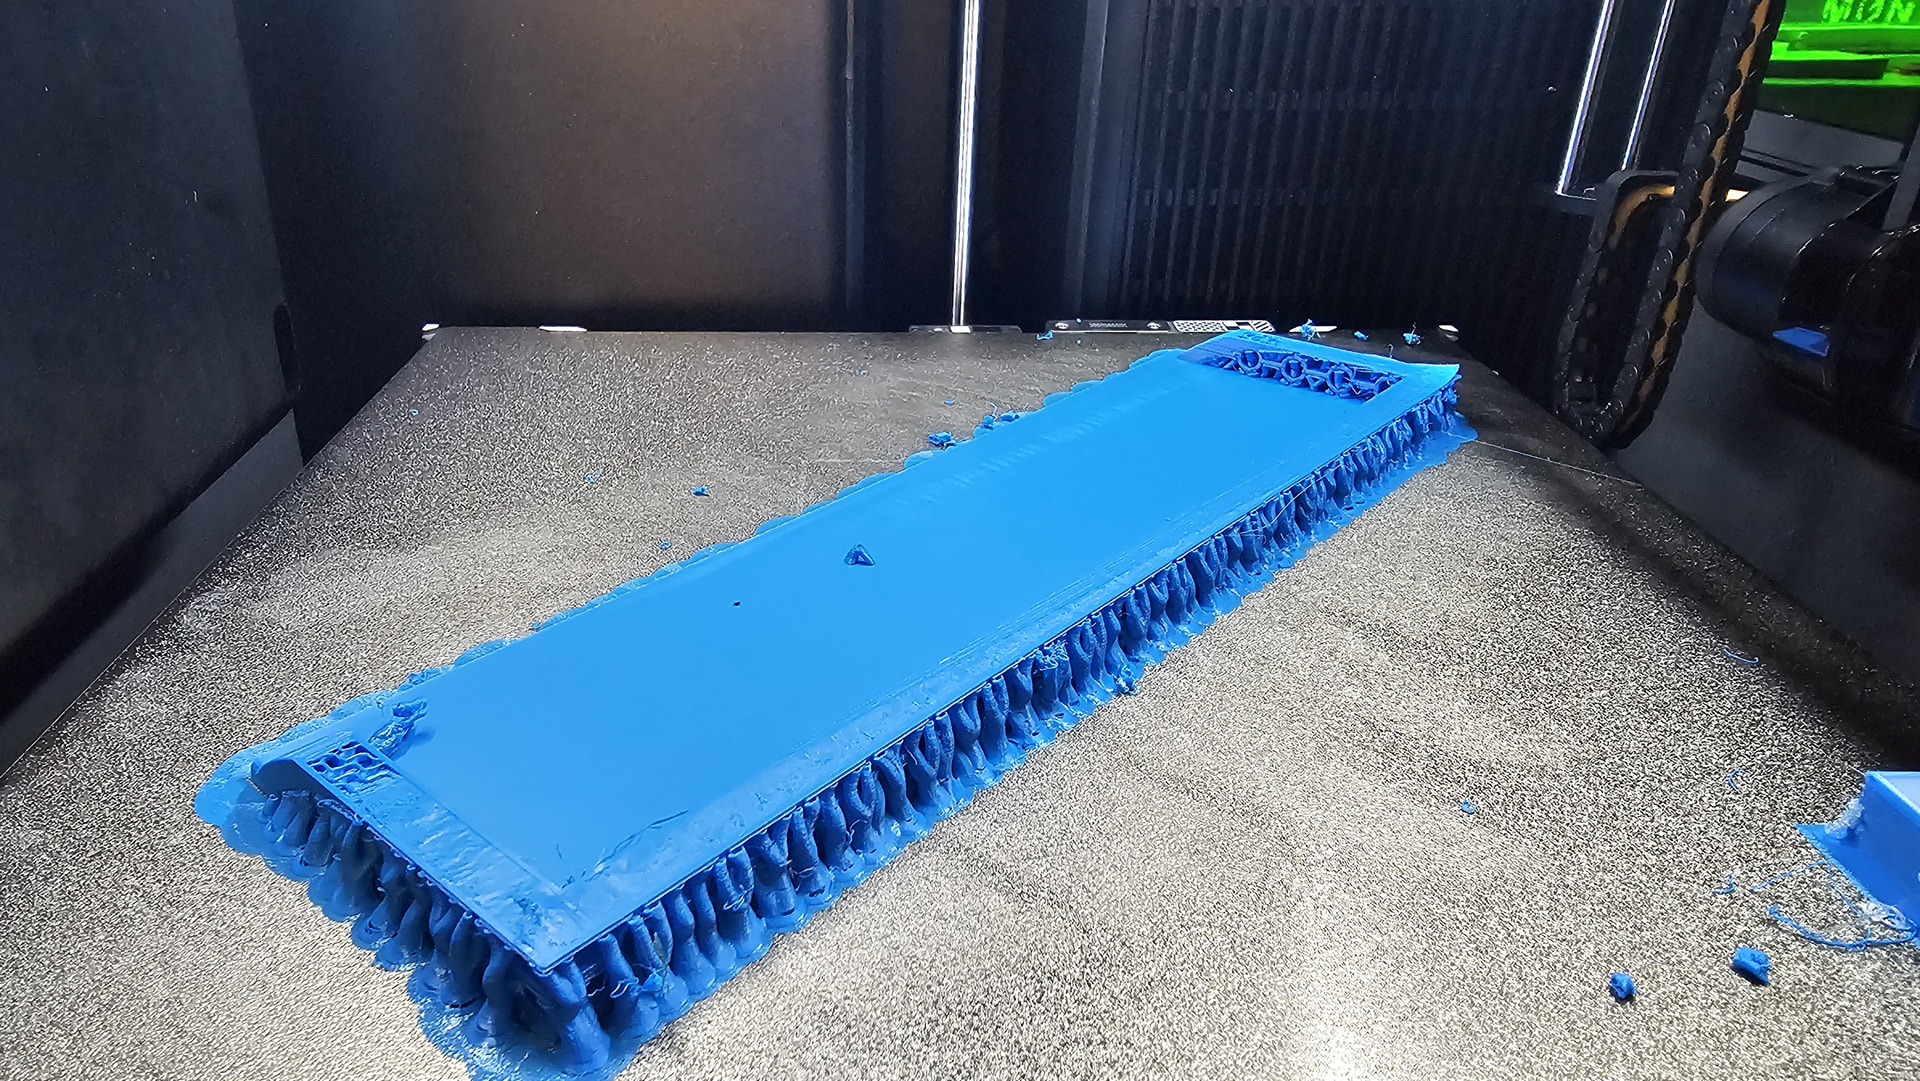
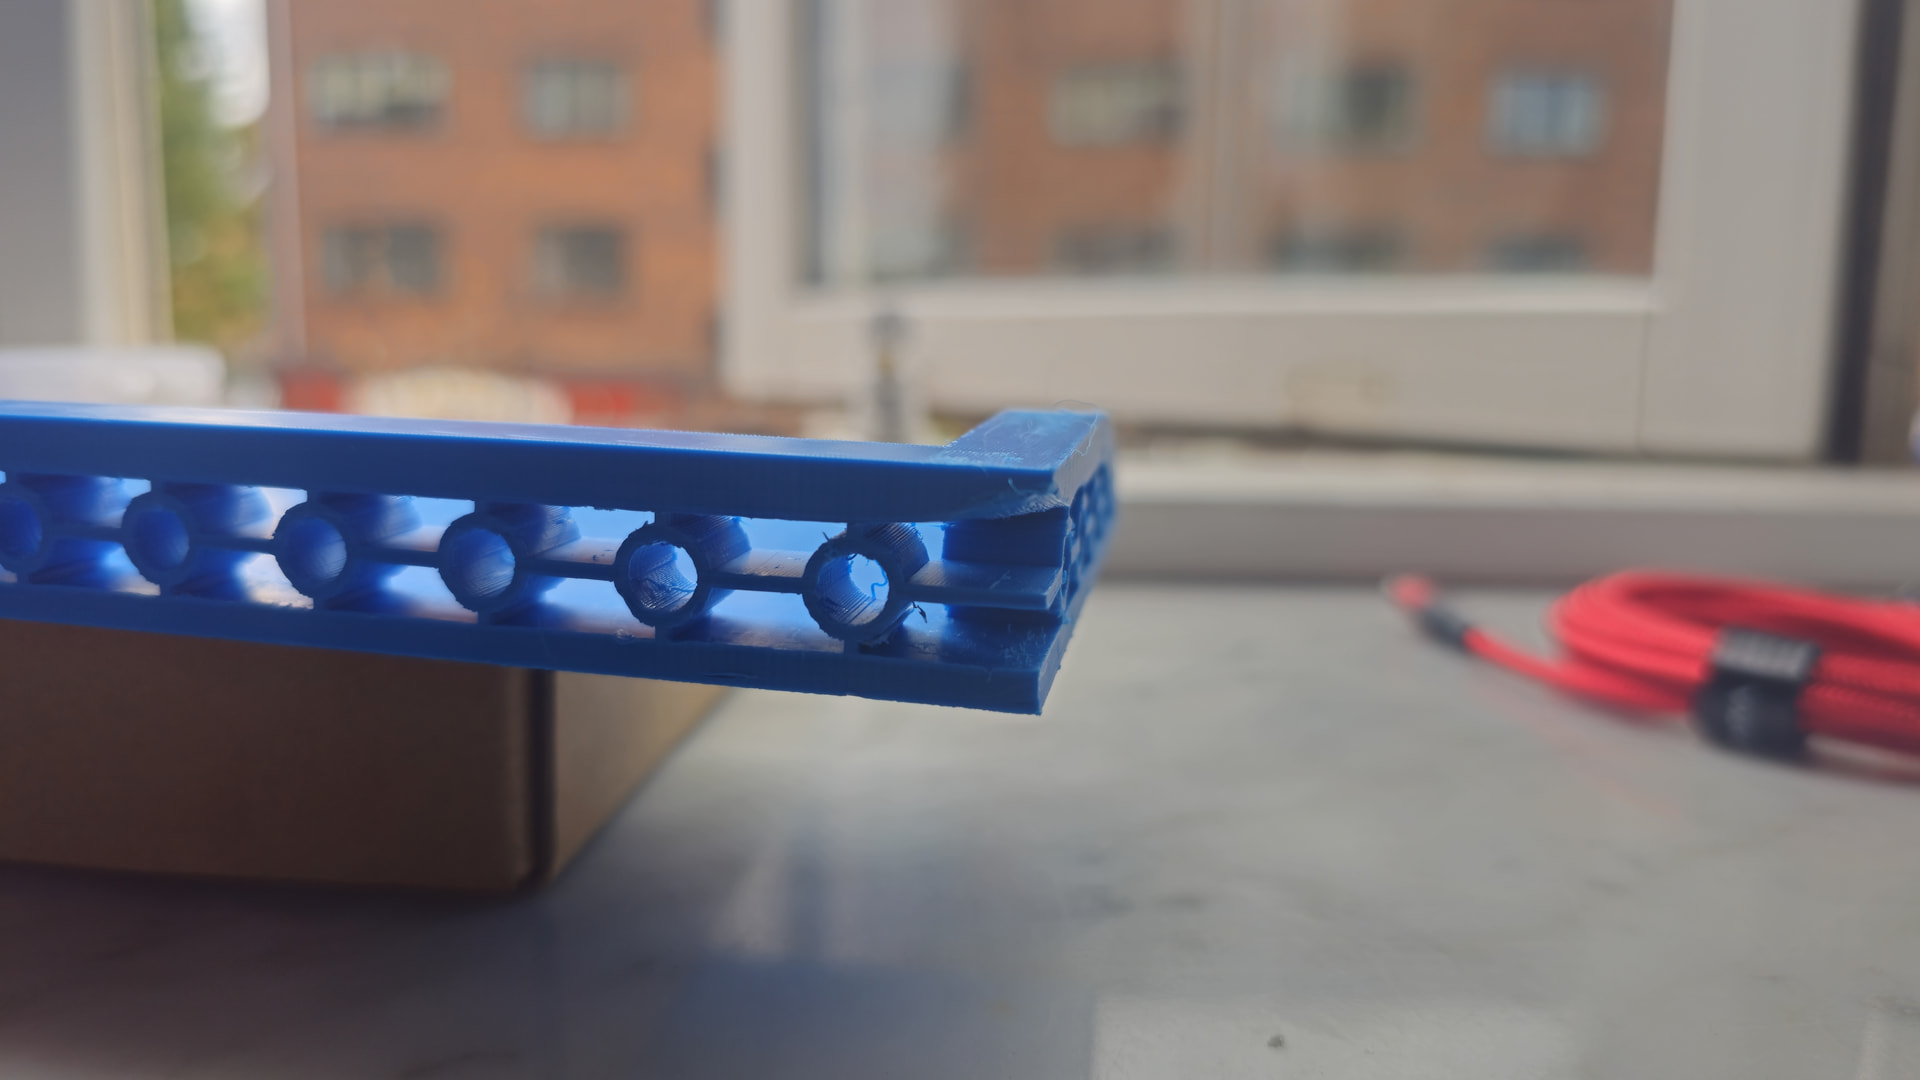
However. The print isn’t up to snuff.

Lots of debris in the chamber.

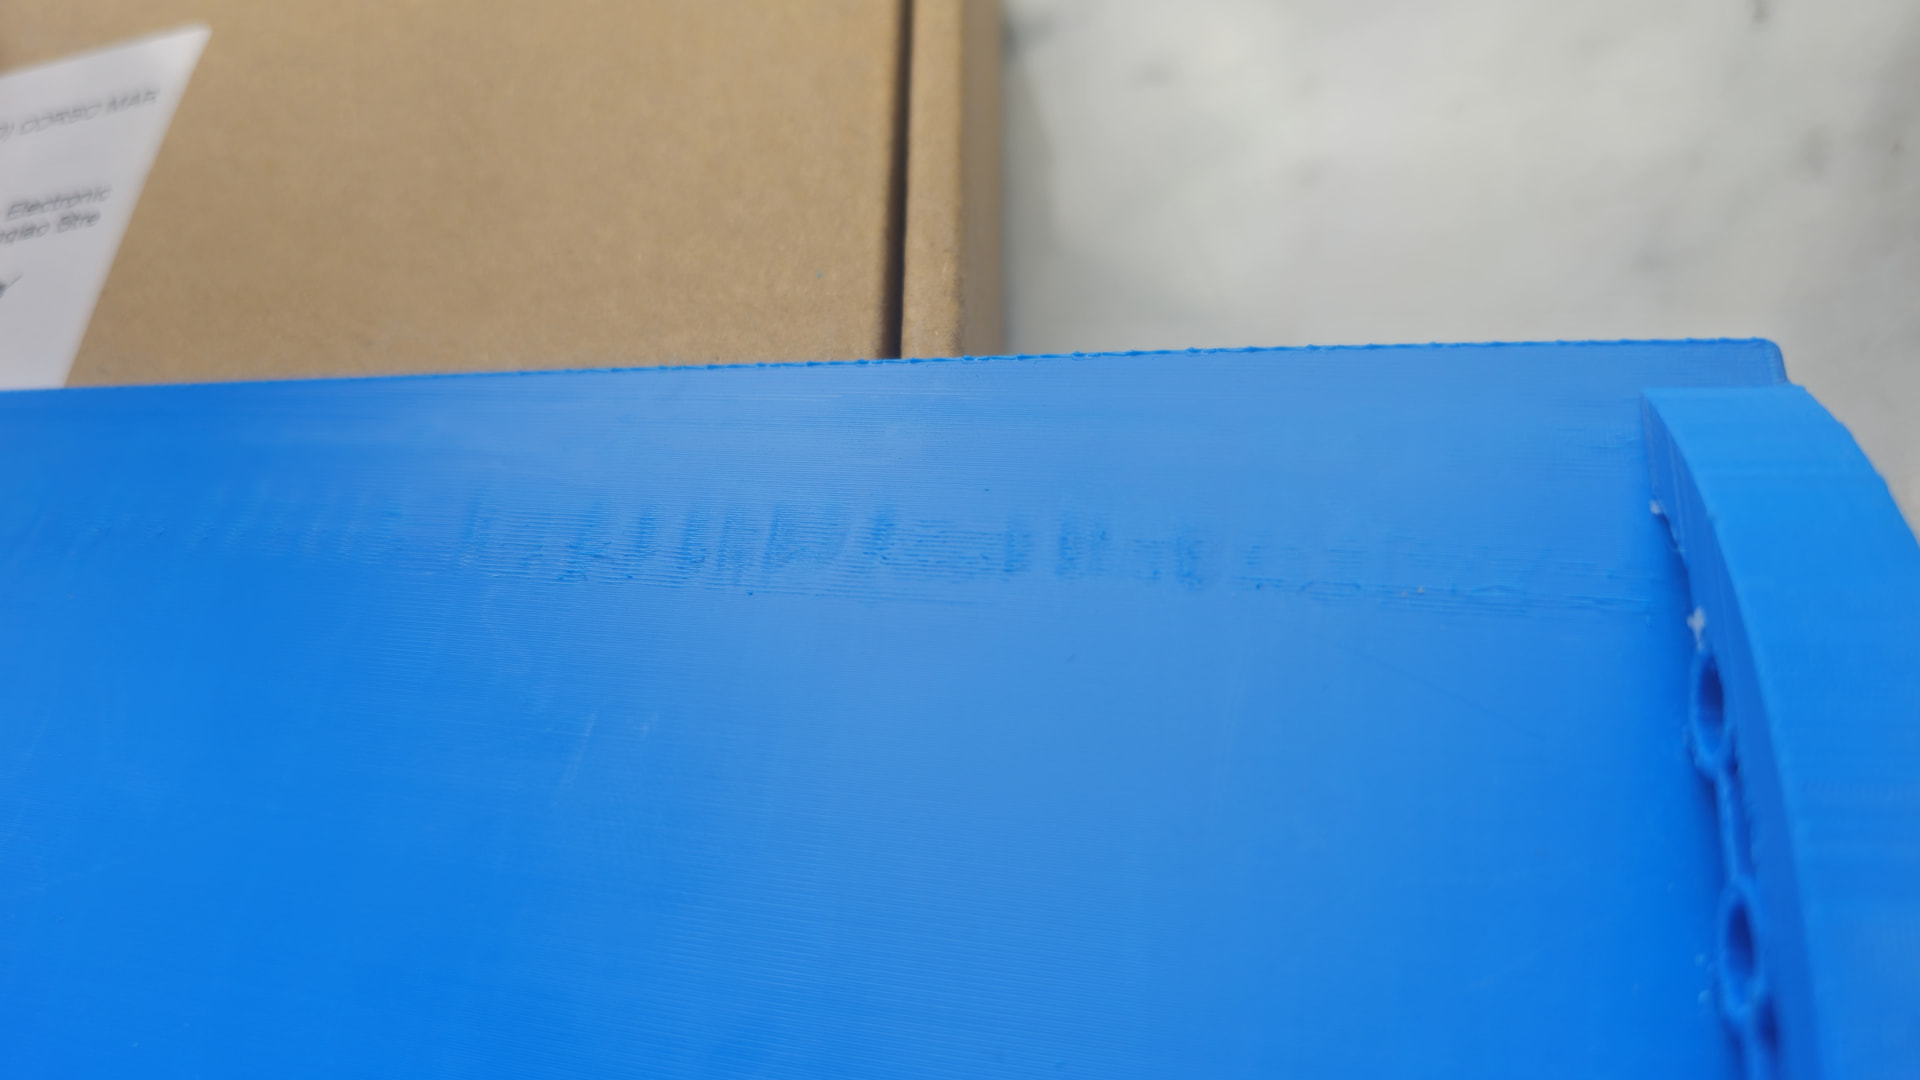
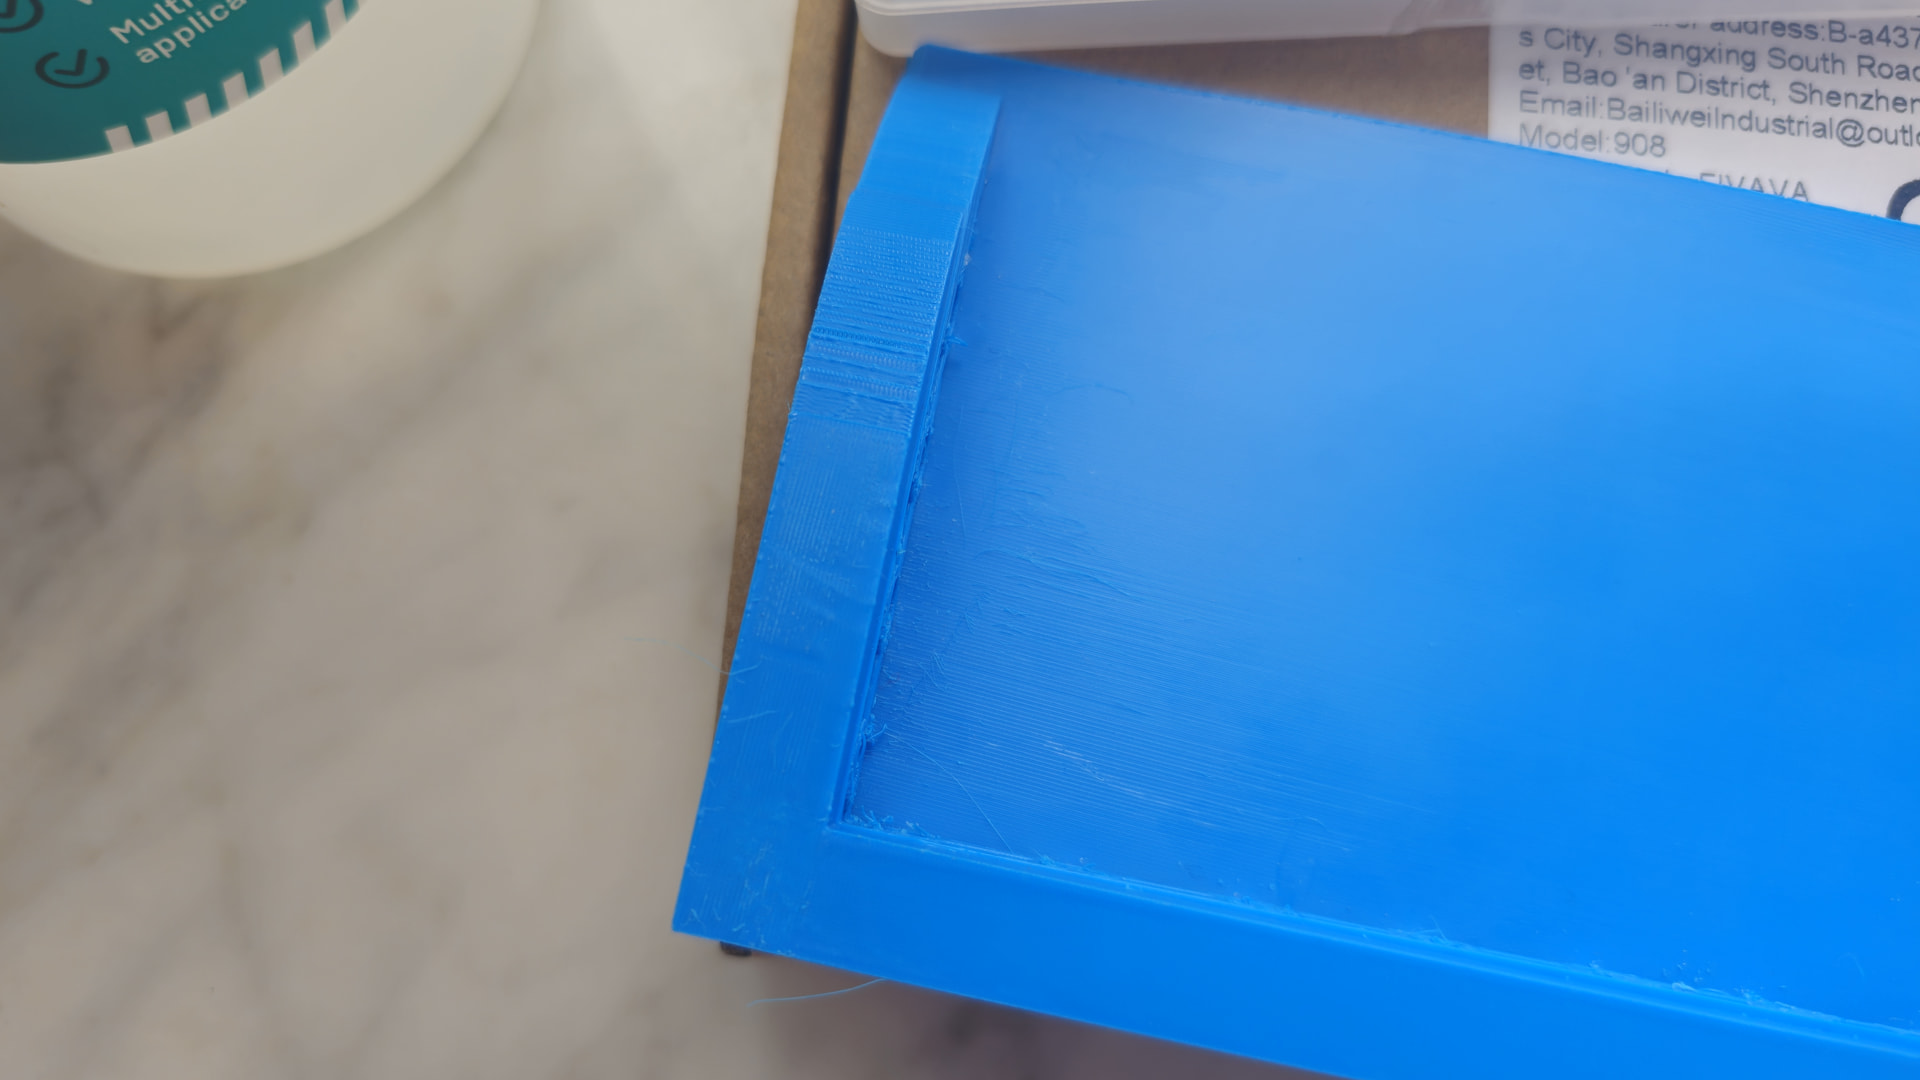
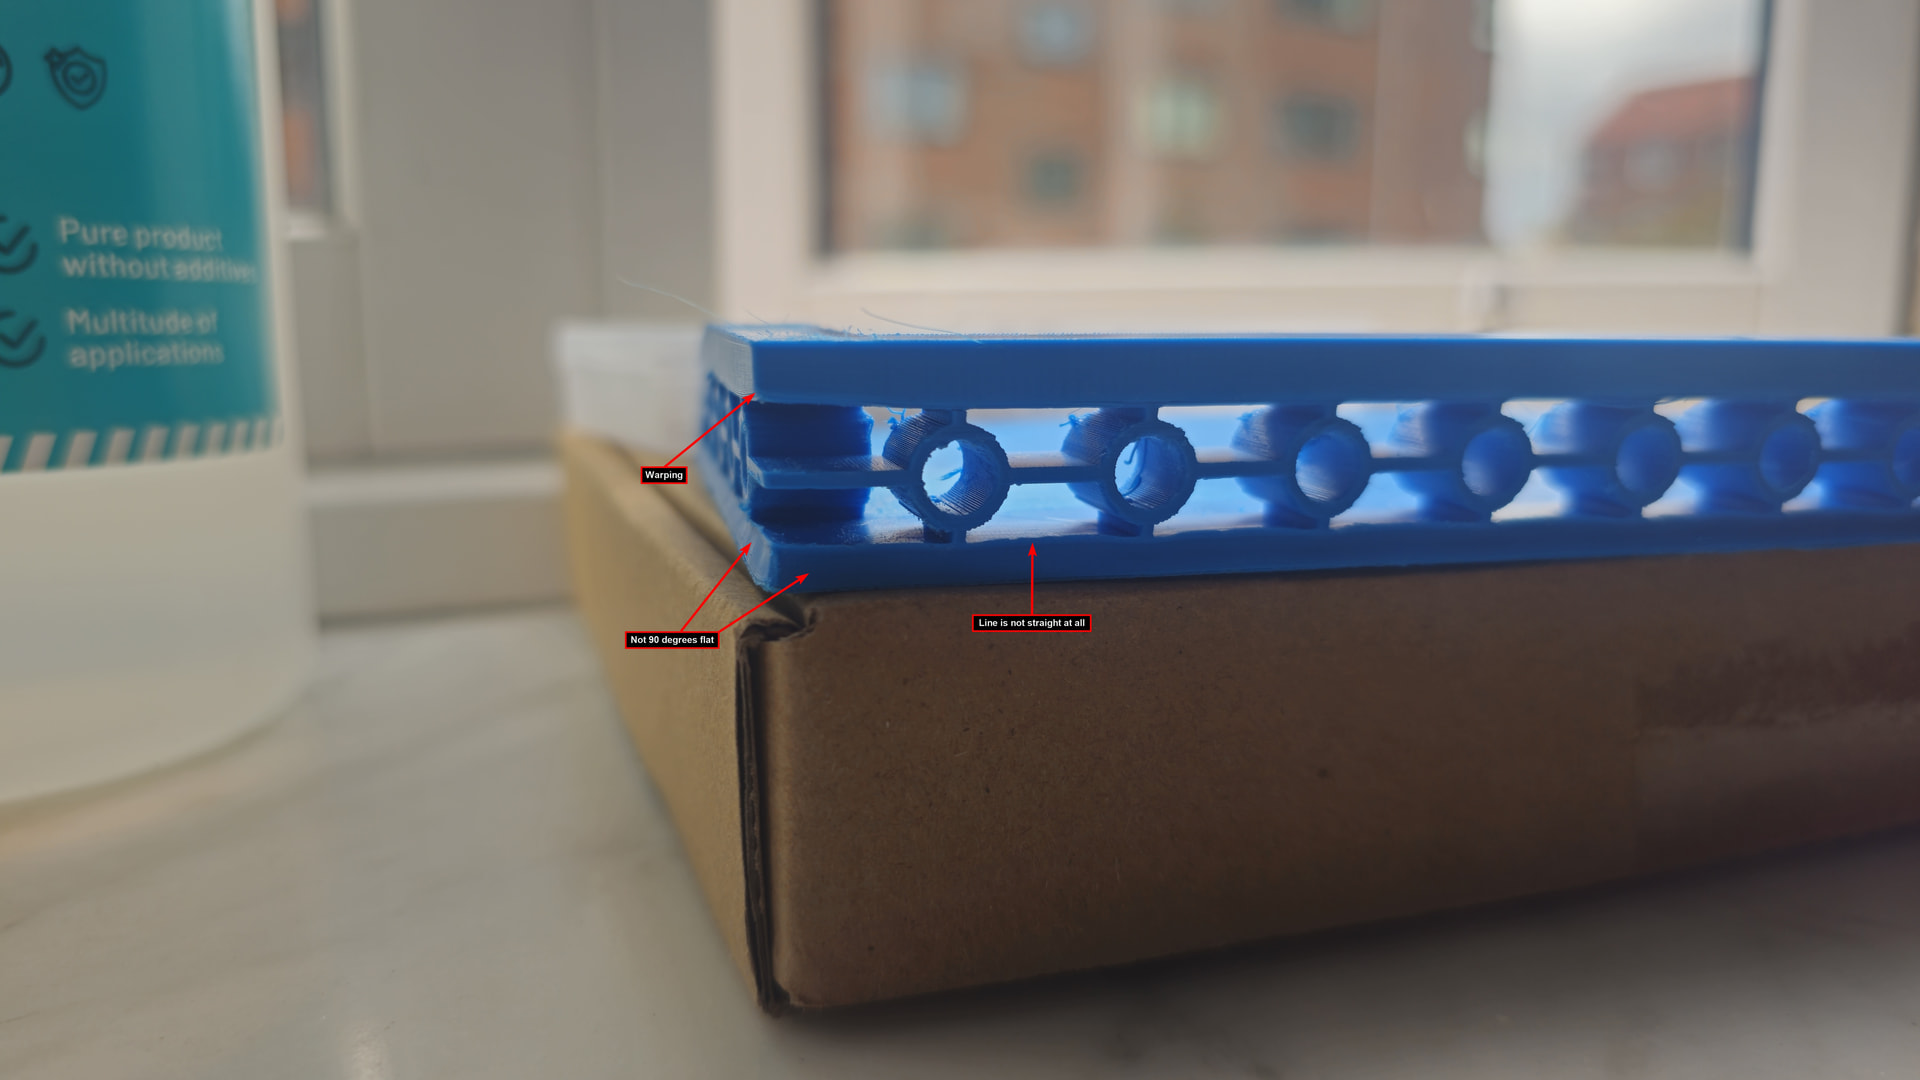
Warping several places…

Scraped surface…

Ugly final layer finish..

Lots of warping…

This is a project for a iPad holder that I need to be spotless for my specific project. I have cut most of the tablet area off, just to test print the raiser and the pattern in between.

Question now is how I can improve the print quality so it prints smoothly with no errors and restarts - and also with a much cleaner finish without warping and flawed details?

How do I get these final issues resolved. This is the first time it finished this specific print.

I wonder if cranking the bed leveling screws right down when cool is resulting in the bed being more likely to deflect when it’s heated.

You need to do this process to ensure the bed is at a good “neutral” position.

After that, you should re-run the bed leveling calibration from the printer settings menu.

Also, now that I see what you’re printing, there is absolutely no reason to use a 0.2mm nozzle on this part. You’re forcing yourself into unnecessarily thin layers and increasing the likelihood of failures - and wasting a whole lot of print time in the process

There’s also some part design issues that are likely contributing to your warping.