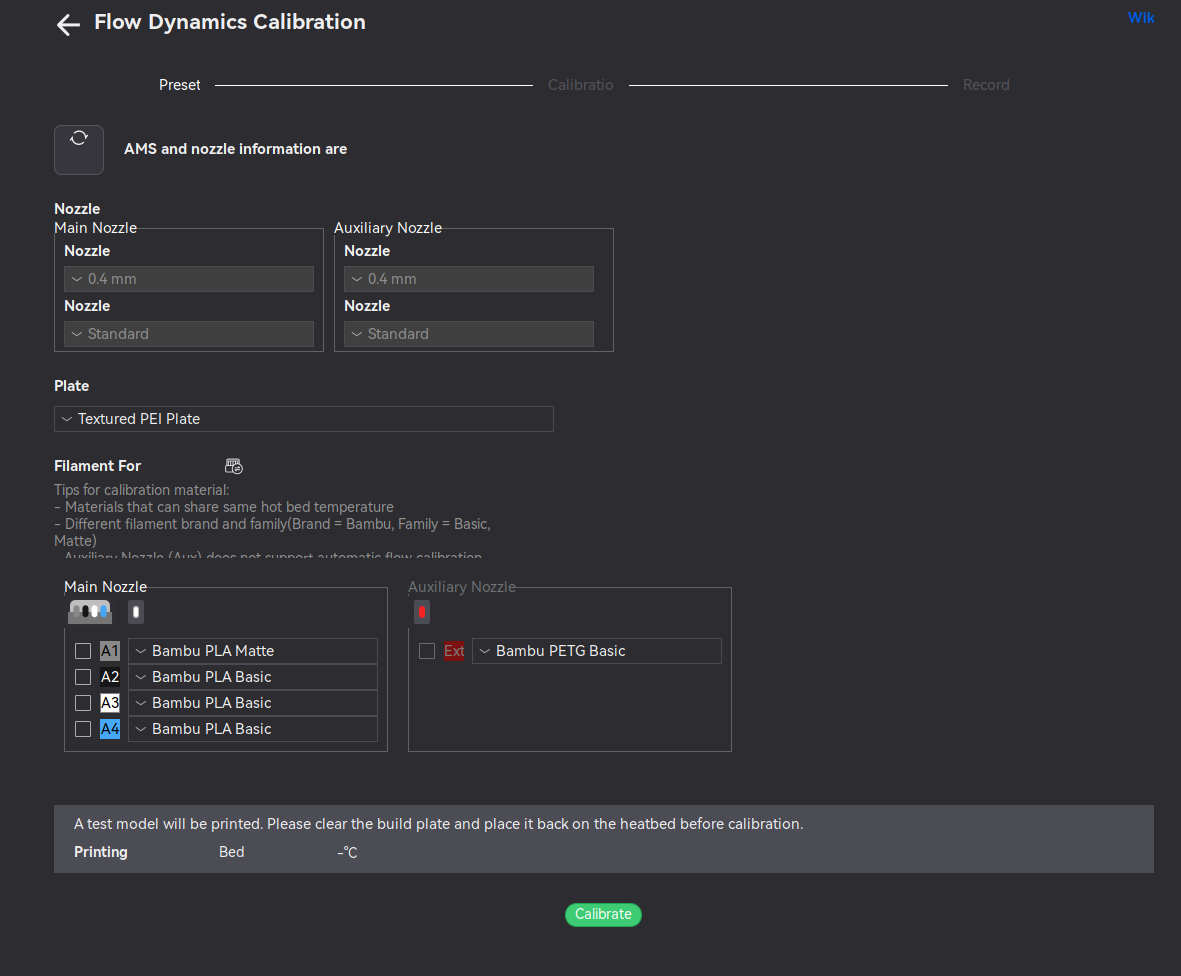
I have not tried to use the flow calibration in the slicer before and was having some minor issues with my new X2D using PETG in the auxiliary nozzle when using it for support interfaces for my prints. I have already done the other calibrations from the developer mode which yelded the current settings wen’t an issue but I wanted to try this that is in the calibration tab. when I opened it and choose automatic, the slicer will not allow me to select the loaded spool of PTEG on the right nozzle, but only allows what is loaded in the ams for the left nozzle.
Am I doing something incorrectly? the Bambu wiki doesn’t say anything about not being able to select filaments that aren’t in an ams (manual spool holder) or anything for the auxiliary nozzle that is a boden drive setup.
Have you actually loaded the EXT filament (PETG Basic) into the nozzle? You have to physically load any/all external spool[s] into the hotend/nozzle before you can make any use of it.
Yes the filament is loaded into the nozzle. I played around with it and it allowed me to do a manual calibraton, just not with the automatic. printing with the manual it printed lines with a K factor from 0 to 0.5 the 0.5 was the best of them all but there was still a buldge on the ladder part of the line.
I am re-loading the PA test from the developer calibrations to re do this with higher setting. I believe the devs may not have implimented the auto calibration for the auxillary extruder for PETG yet due to how new this printer is.
Btw. I am on linux (Kubuntu 24.04) with the latest public beta of Bambu Studio. might also have something to do with the calibrations.
The issue I am hoping to solve is when I use PETG in the auxiliary extruder (right nozzle) for support interfaces, when there is a small area like at the end of the tree support where the amount of filament that is needed is for an area maybe the size of 2mm diameter or less, very little to no PETG is extruded leaving a gap in that area. This or will sometimes leave hair strings when traveling from one surface to another. this string sometimes results in going through the actual printed part.
I have already ran flow and other calibrations and once determined what was best, looking at the default settings in the slicer, they don’t need to be adjusted. my next step is to change to another spool of PETG which I have already ran through the dry cycle. the stringing tests I have ran already only results in a random string here and there so it seems random that the extruder is over/under extruding. I have gone over the ptfe tubes and assembly verifying everything is in place and secure, so this might simply be due to the new spool I got with the printer.
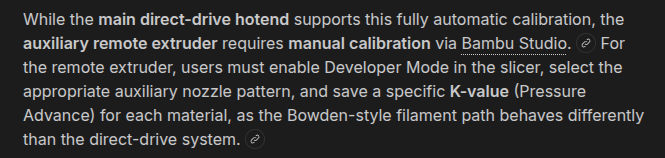
Info I found online and this is something I suspected as well. it’s not the slicer but the right nozzle (auxiliary) does not have a sensor to do the auto calibrations. I found this tidbit online and my search AI said this…
I ran the manual calibrations again for it and found that best K factor for PETG seems to be 0.46 to 0.48. seems kinda high but then again it’s a boden setup. I experienced this on my old Ender printers as well. Now that this is set I can re-calibrate retractions and others. I learned with my old Ender 3 that once you have flow and other retractions in the ball park, to get the PA (pressure advance) calibrated, then go back and re-run all the calibrations again. then again re-run the PA once more and see if it needs to be dialed in further. If the PA gets changed you have to go back and re-do all the other calibrations except for max volumetric flow. a single change will effect the others. back in the day I had my old Ender 3 printing really good quality for what it was. For this new X2D, it’s back to the basics for the right side extruder!
Hope others find this info helpful. and Hopefully this fixes my issue here as well.