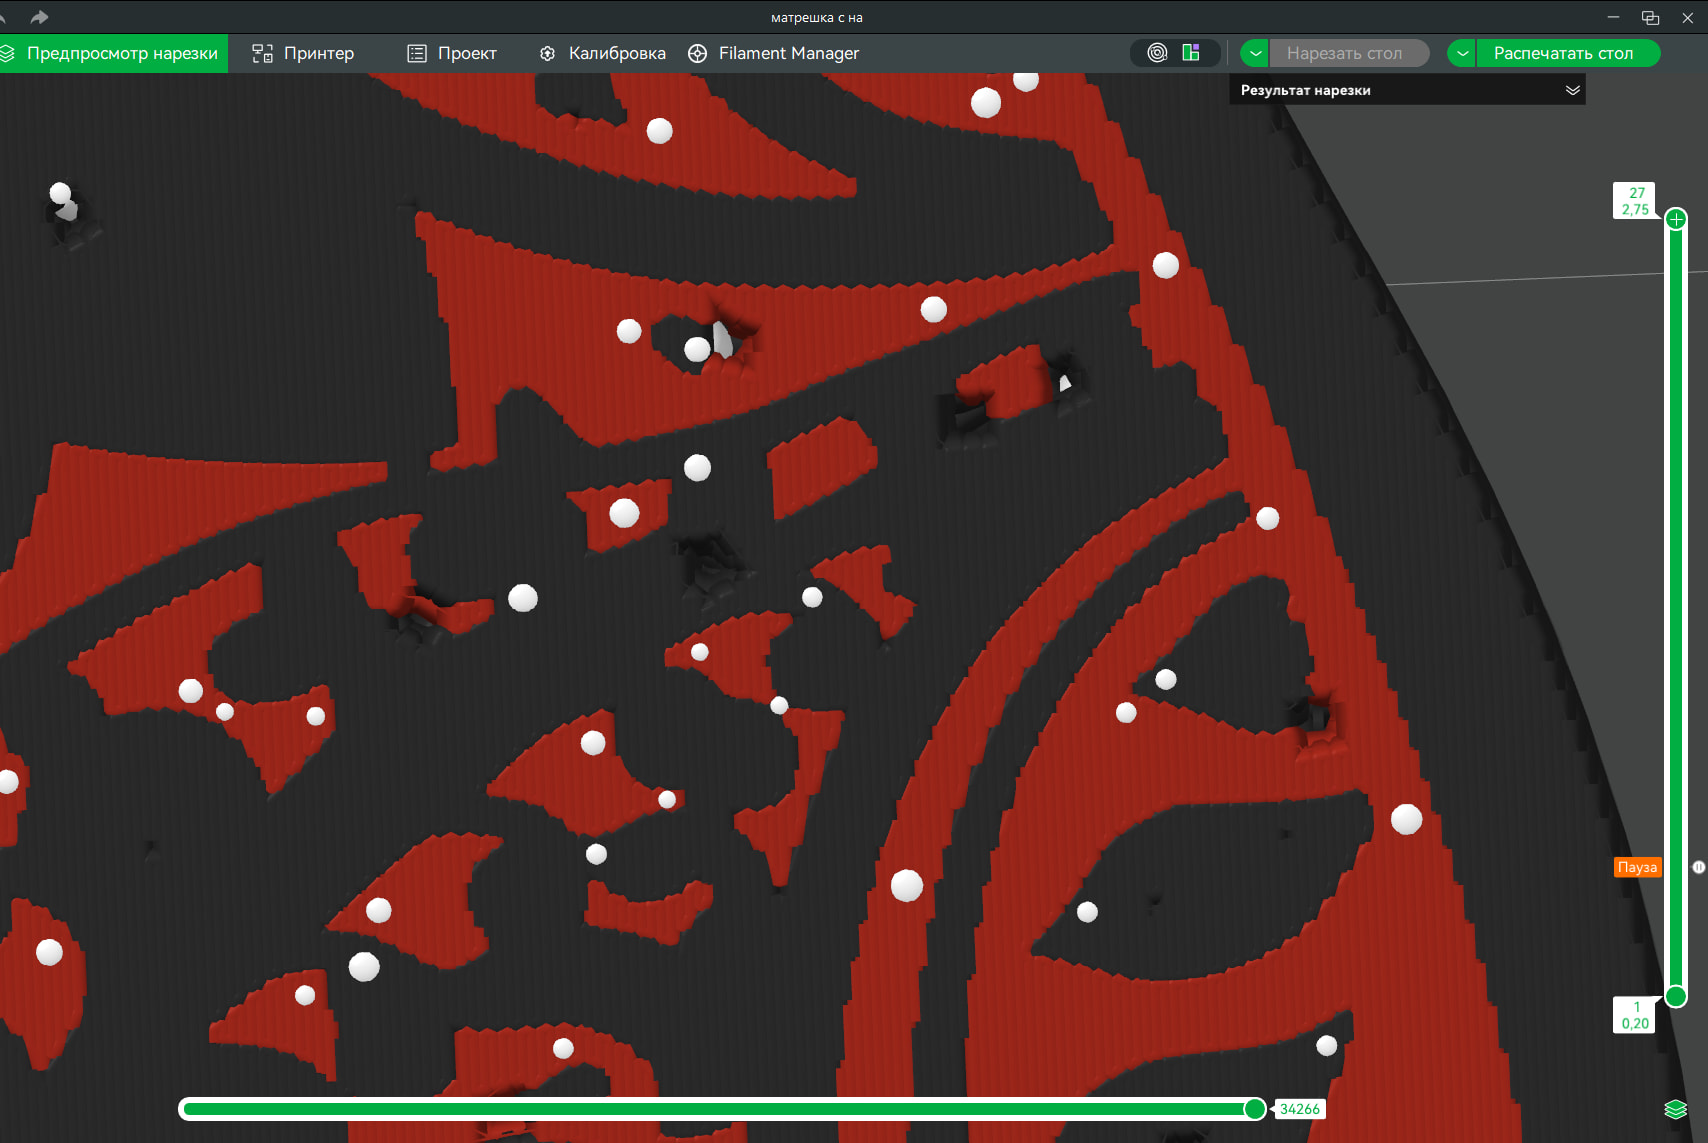
Hello! I am slicing a flat keychain model with a lot of complex multi-color patterns using a 0.4mm nozzle in Bambu Studio.As you can see in the slicer preview, there are empty gaps (holes) between the colors on the TOP LAYER. I already enabled the Arachne wall generator, set the minimum wall width to 45%, and changed the top surface pattern to Monotonic, but these slicing gaps won’t go away on the top surface.What setting should I change to force the slicer to fill these narrow spaces completely on the top layer? Thank you!
Have you actually tried printing the part to see how it comes out?
The onscreen preview is just a representation of where the toolhead moves, and is not indicative of flow at those locations, which is the whole purpose of arachne - vary the flow to better fill irregular areas.
You really need to try it to find out.
Failing that, you can change the top surface infill pattern, that will hit all the geometry differently and may not leave the same gaps, and if all else fails there’s always 0.2mm nozzles…
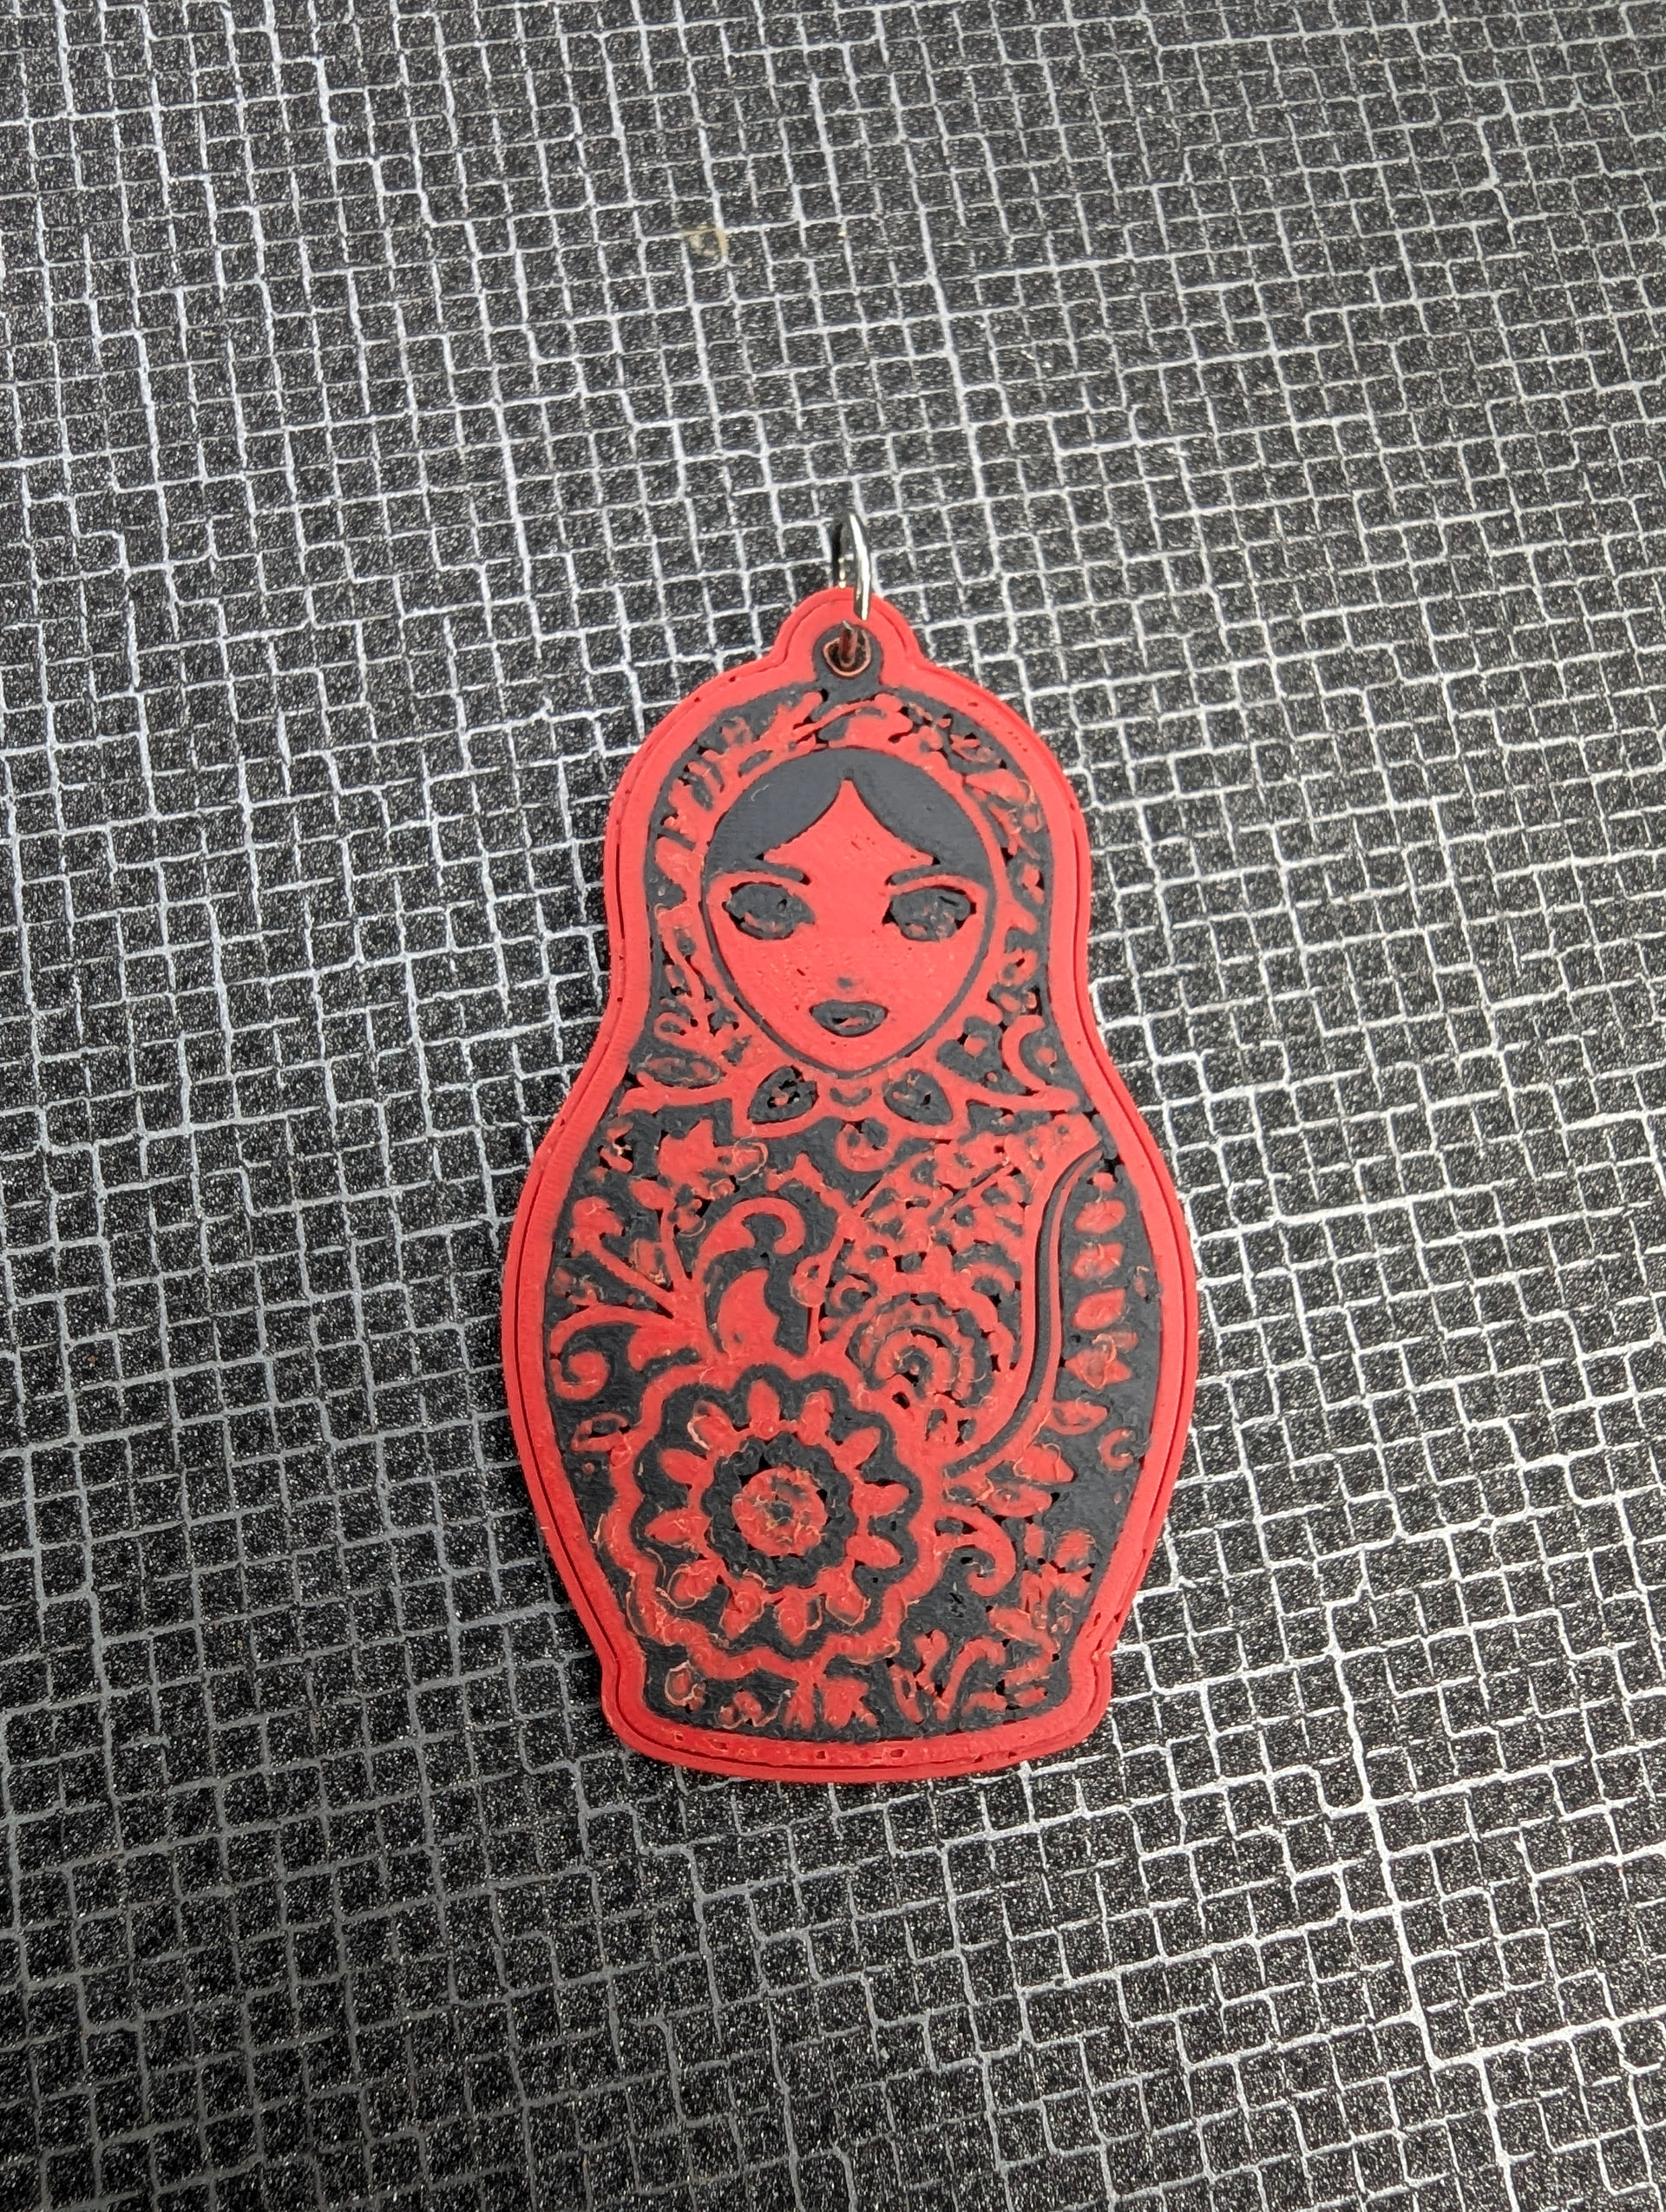
No, there are actually only two colors; they are matte, which is likely why it looks like there’s white—but the white you see when cutting is just the seam. However, aside from the seam, there are also holes.
Firstly, the details are much too small for a 0.4 nozzle. If you want to print a keychain, for example, you can only achieve fine details by using a different nozzle, such as a 0.2.
Secondly, the base model is not printer-friendly and has not been optimised. This could be due to export errors, an unclosed mesh or text / logo that’s too small, for example. There are many possible causes.
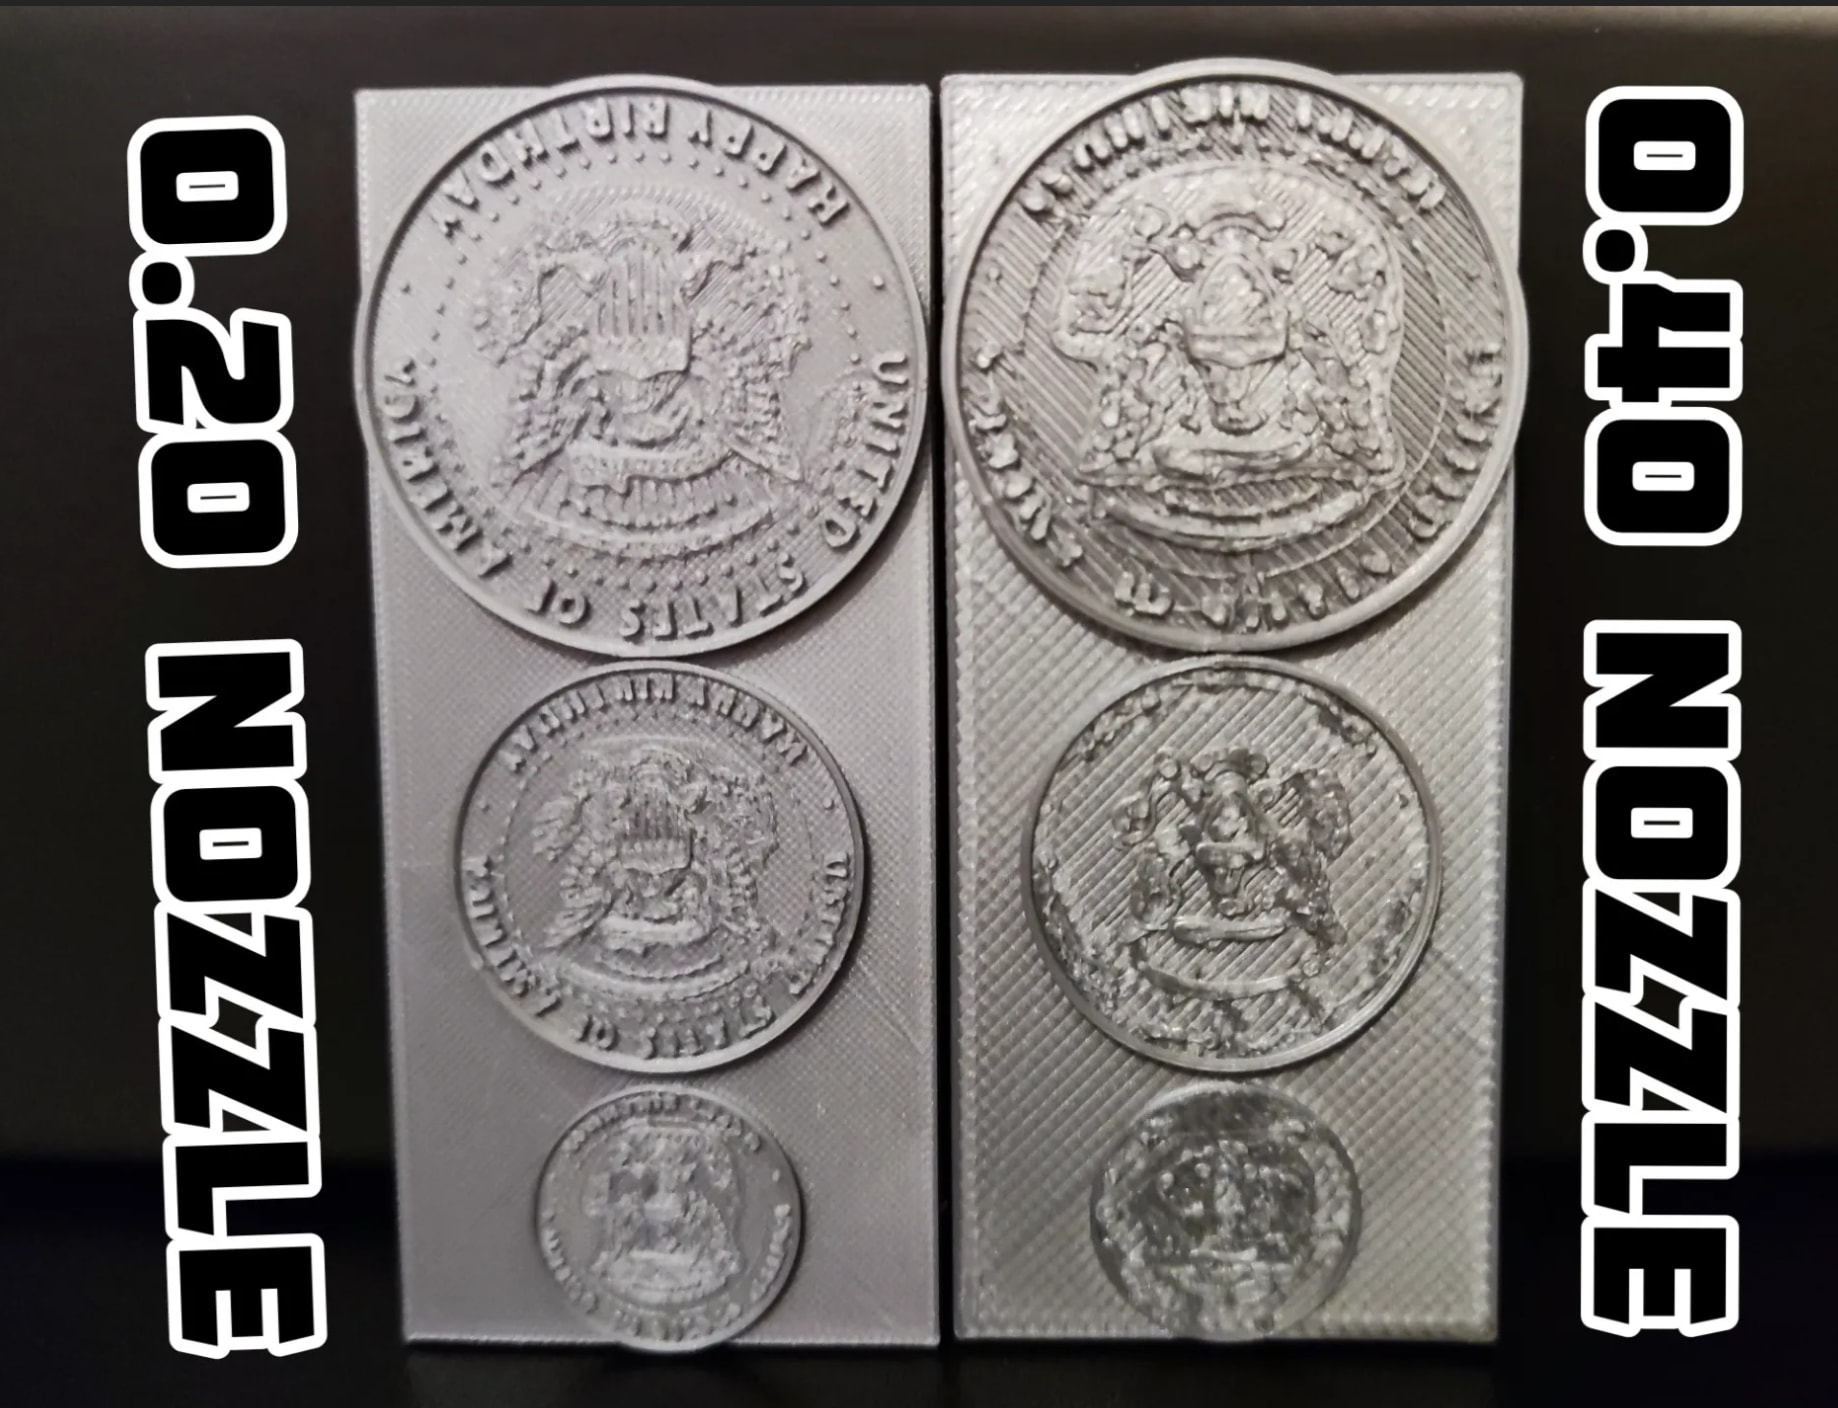
I actually did a comparison test specifically for cases like this - the 0.4 nozzle simply reaches its limits:
You could try uploading the 3MF file into this thread; then we could check whether the problem is due to the settings or if the model is defective. Either way, though, you’ll be pushing the 0.4 nozzle to its limits, since your model has an extremely high number of curved lines.
As an immediate test: Try setting the 0.2 nozzle in the slicer and see if that helps - don’t print, just slice.
Unfortunately, you have to choose between quality and saving time. You could just print several at once - then it wouldn’t be such a big deal, and you’d save a significant amount of time again.
With multi-color-print, it doesn’t make much sense to print just one item. Fill up the plate.
I’ll most likely have to install a second nozzle—much as I’d rather not. Right now, the model is being repaired in Windows; I’ll take another look at it, slice it for the fourth nozzle, and then proceed with the nozzle swap.
Repairing the model resulted in the complete removal of the paint job, and now it is impossible to paint it as before because everything has merged together.
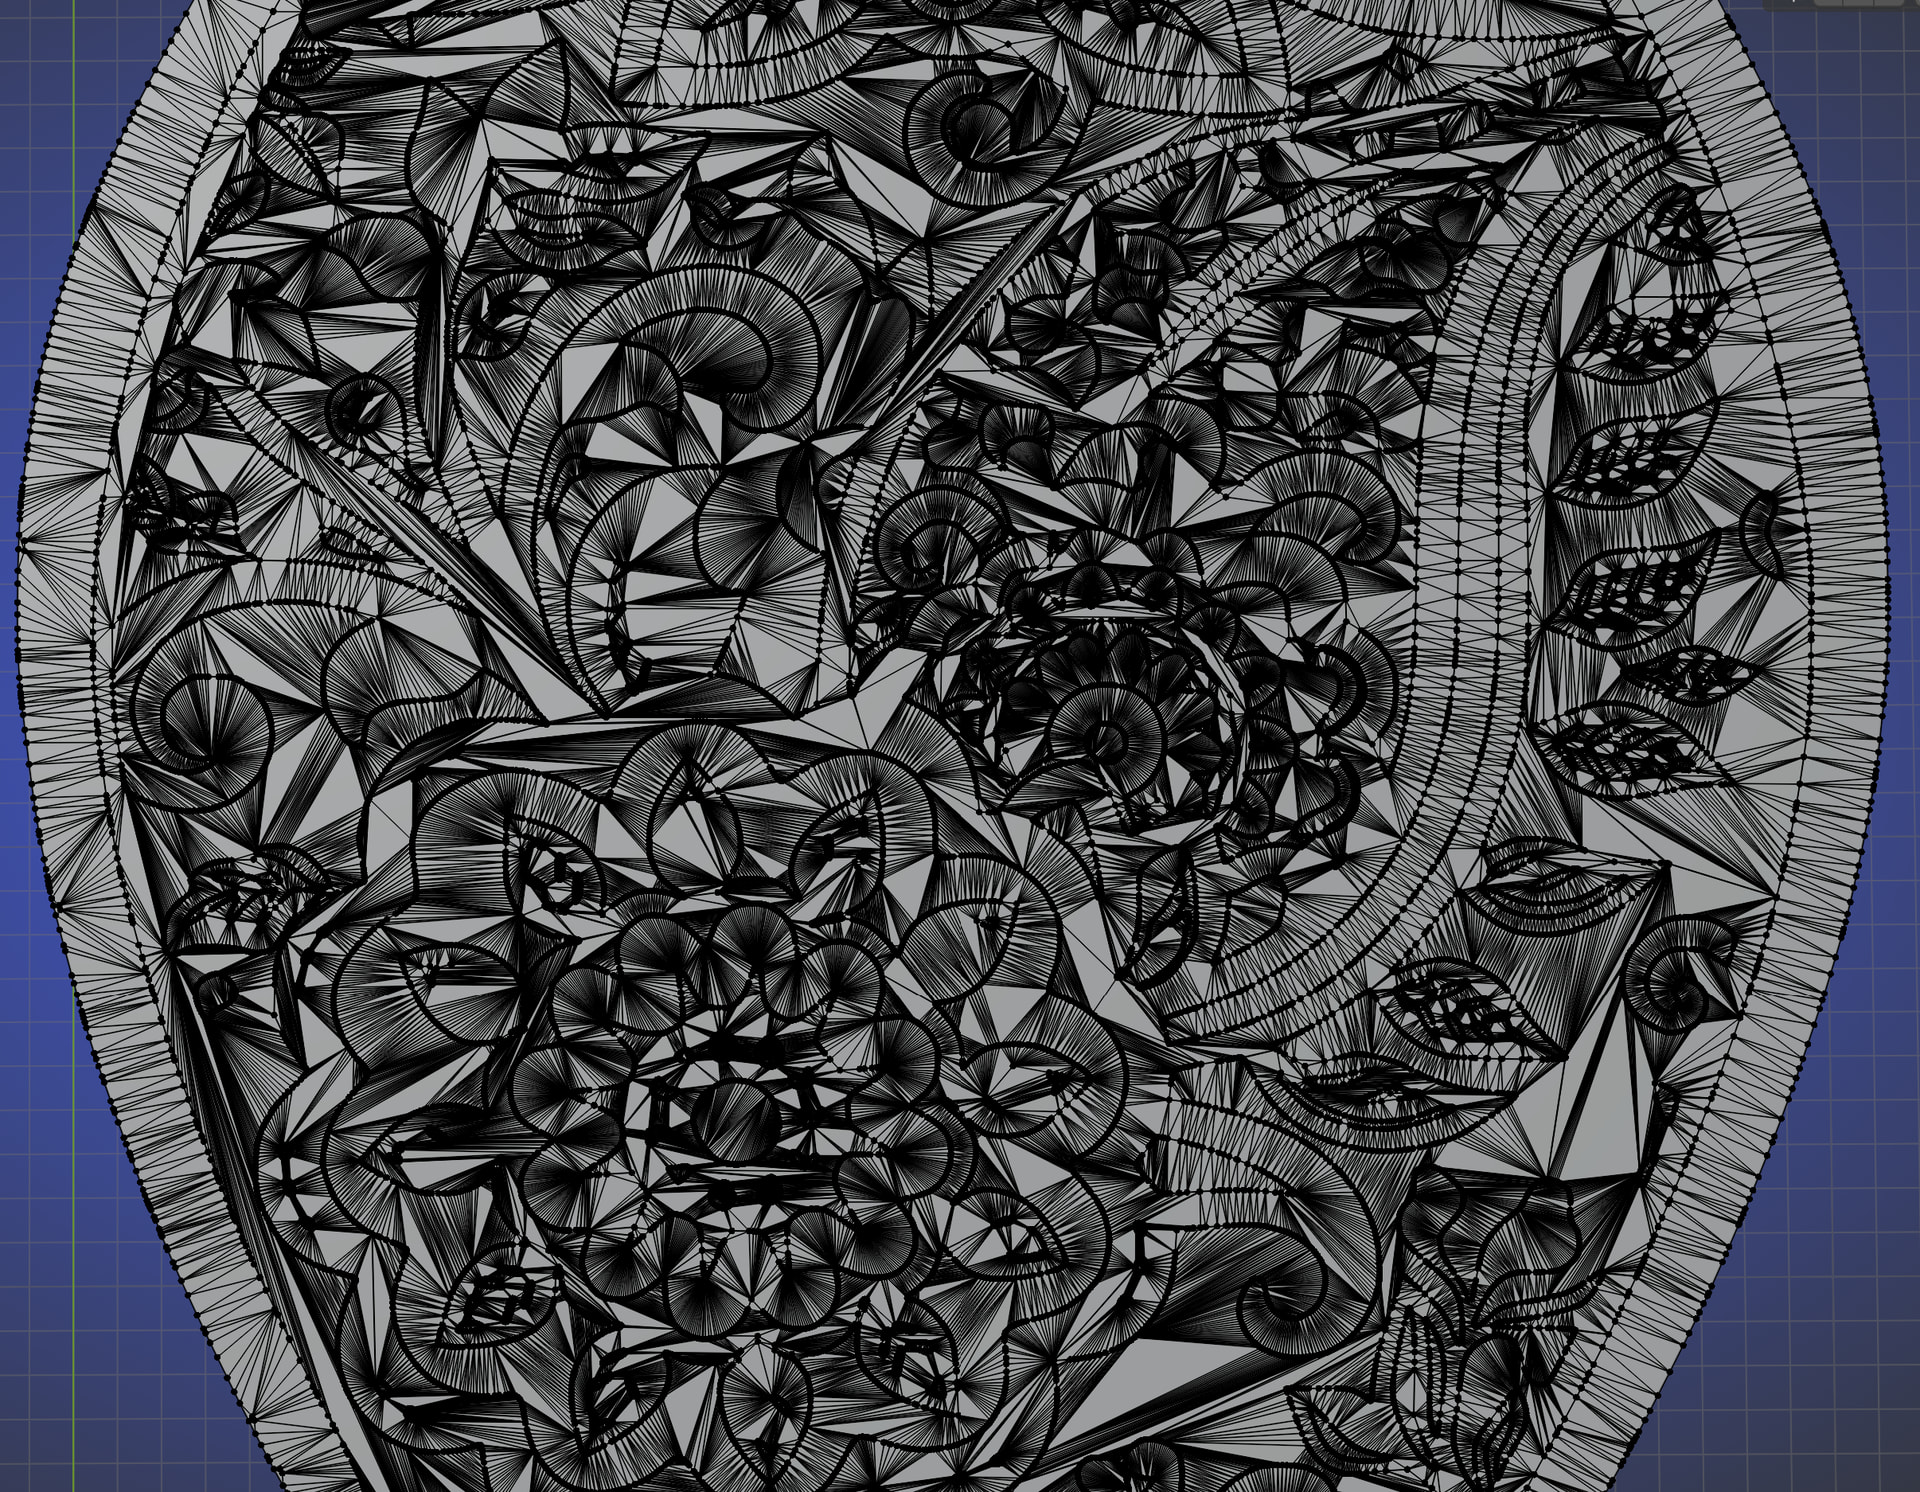
I’m almost certain it’s a modelling issue. Probably has so many intricate details and geometries that the slicer doesn’t know what to do with it. This is what it looks like in Blender:
Your object has 330,000 geometric details (to put it simply). For comparison, a keychain usually has fewer than 100,000. Your object is even making my high-performance computer struggle.
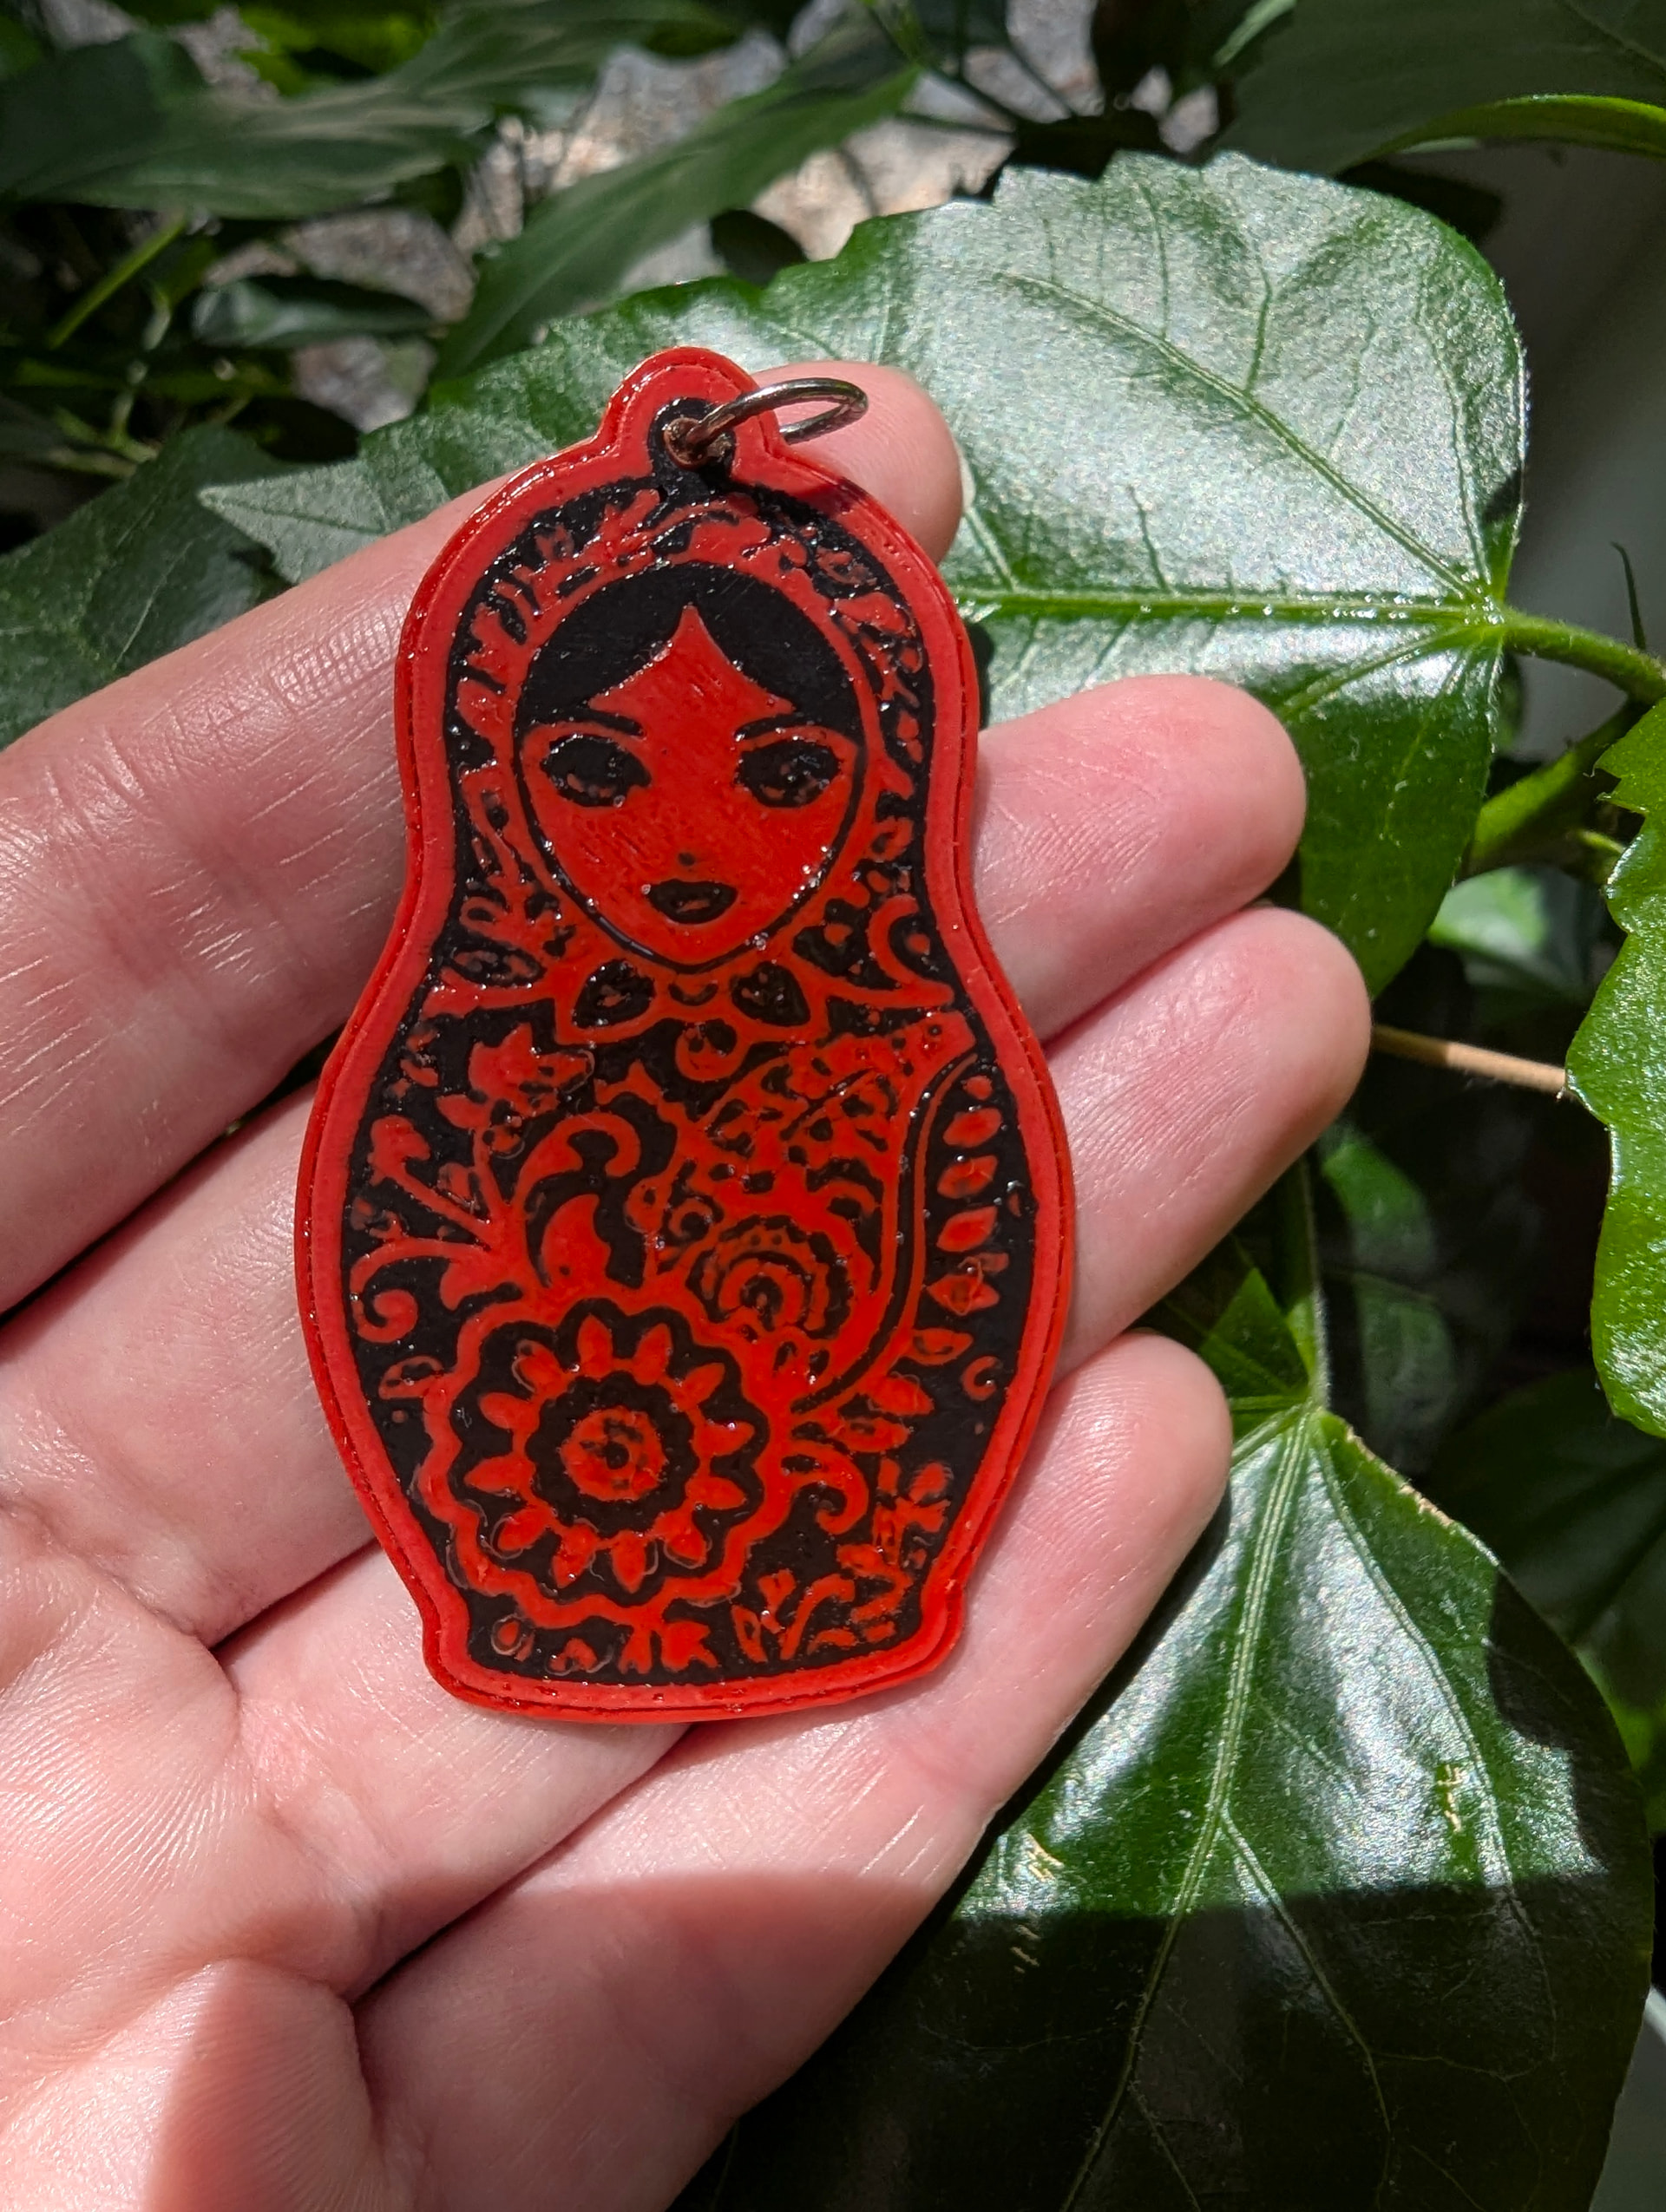
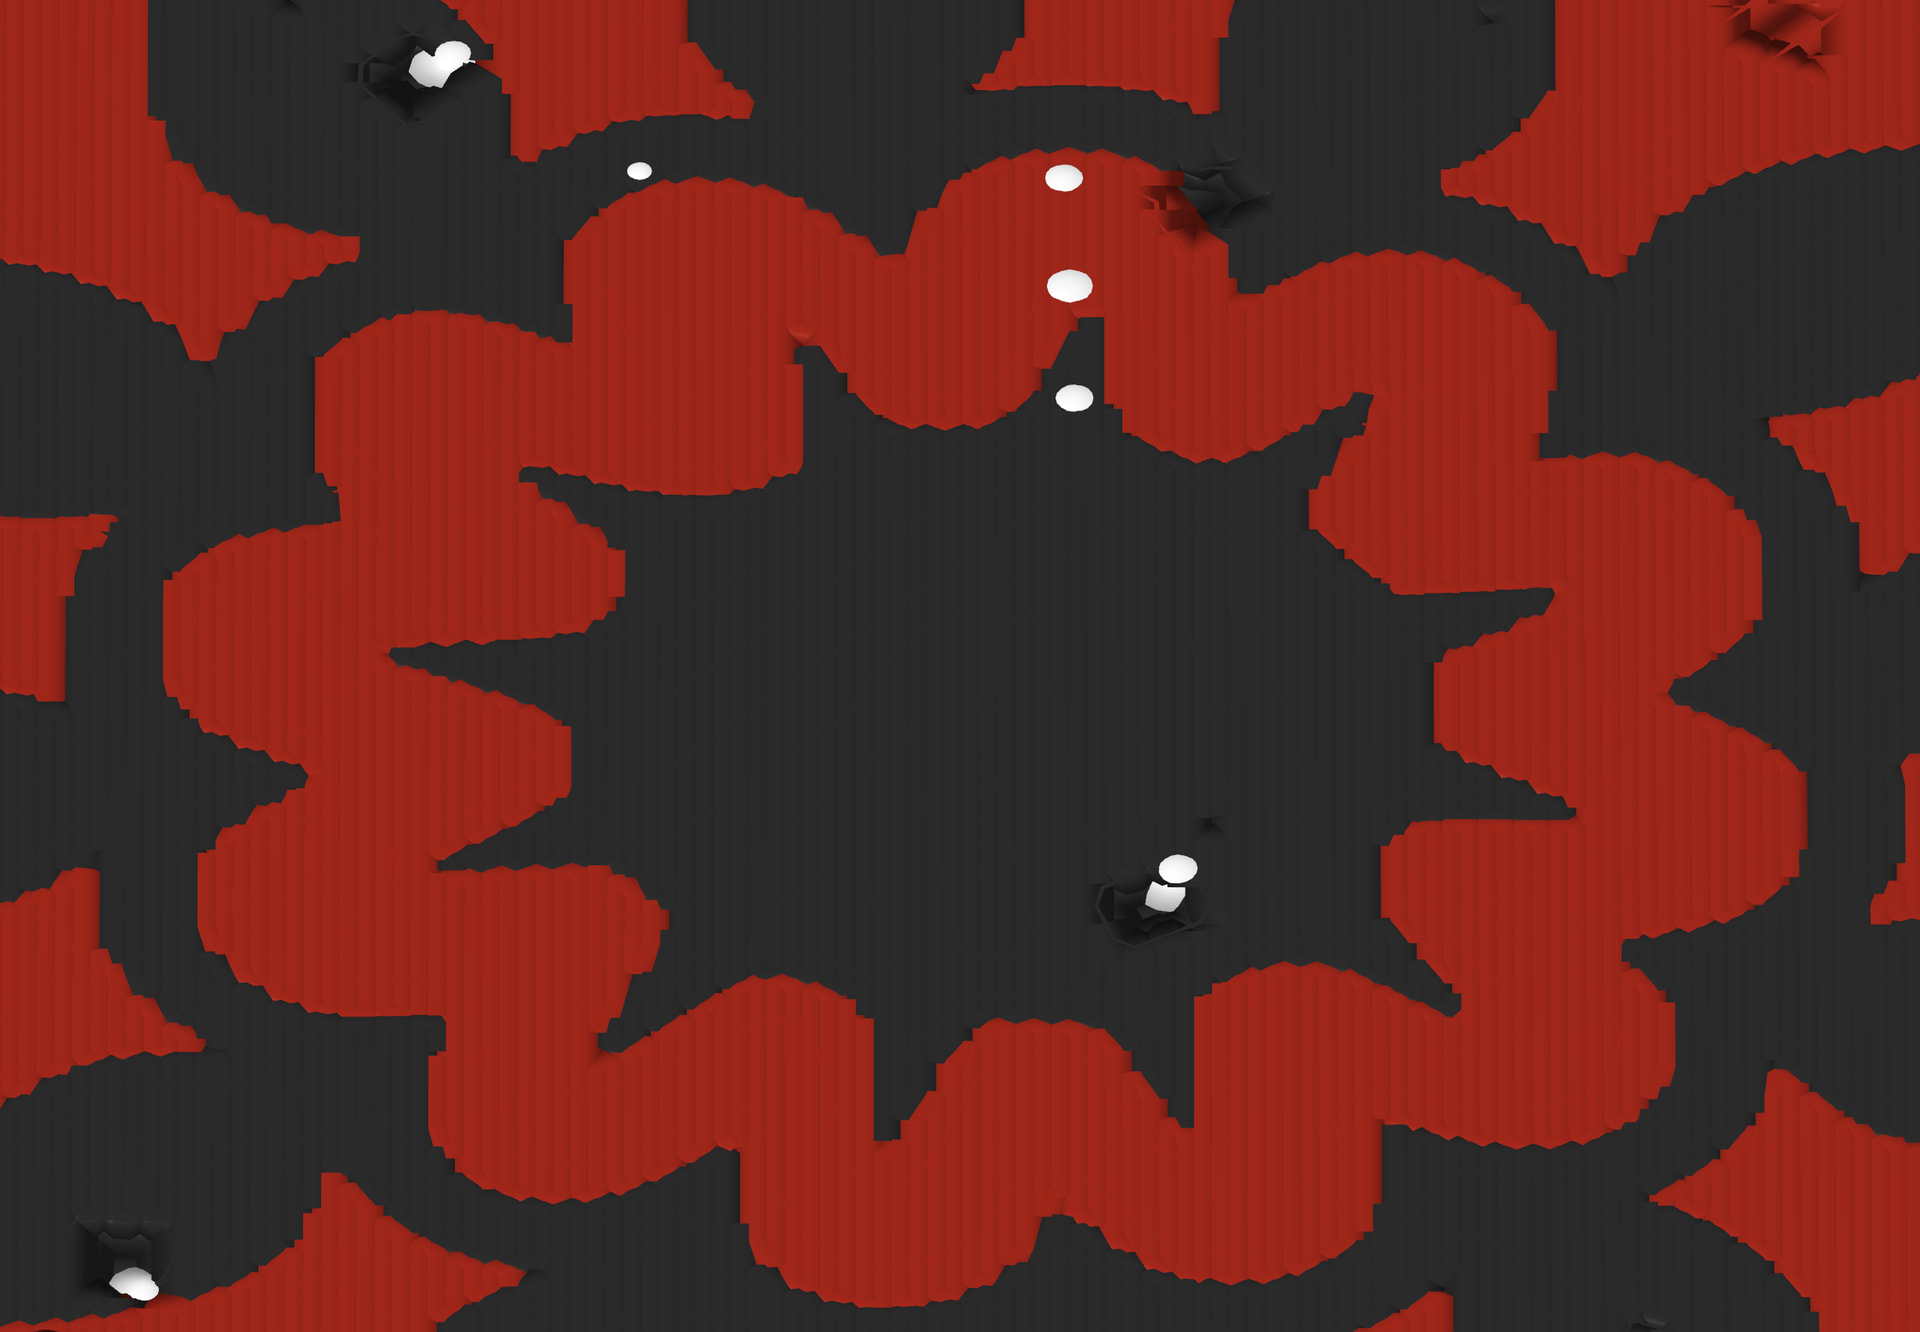
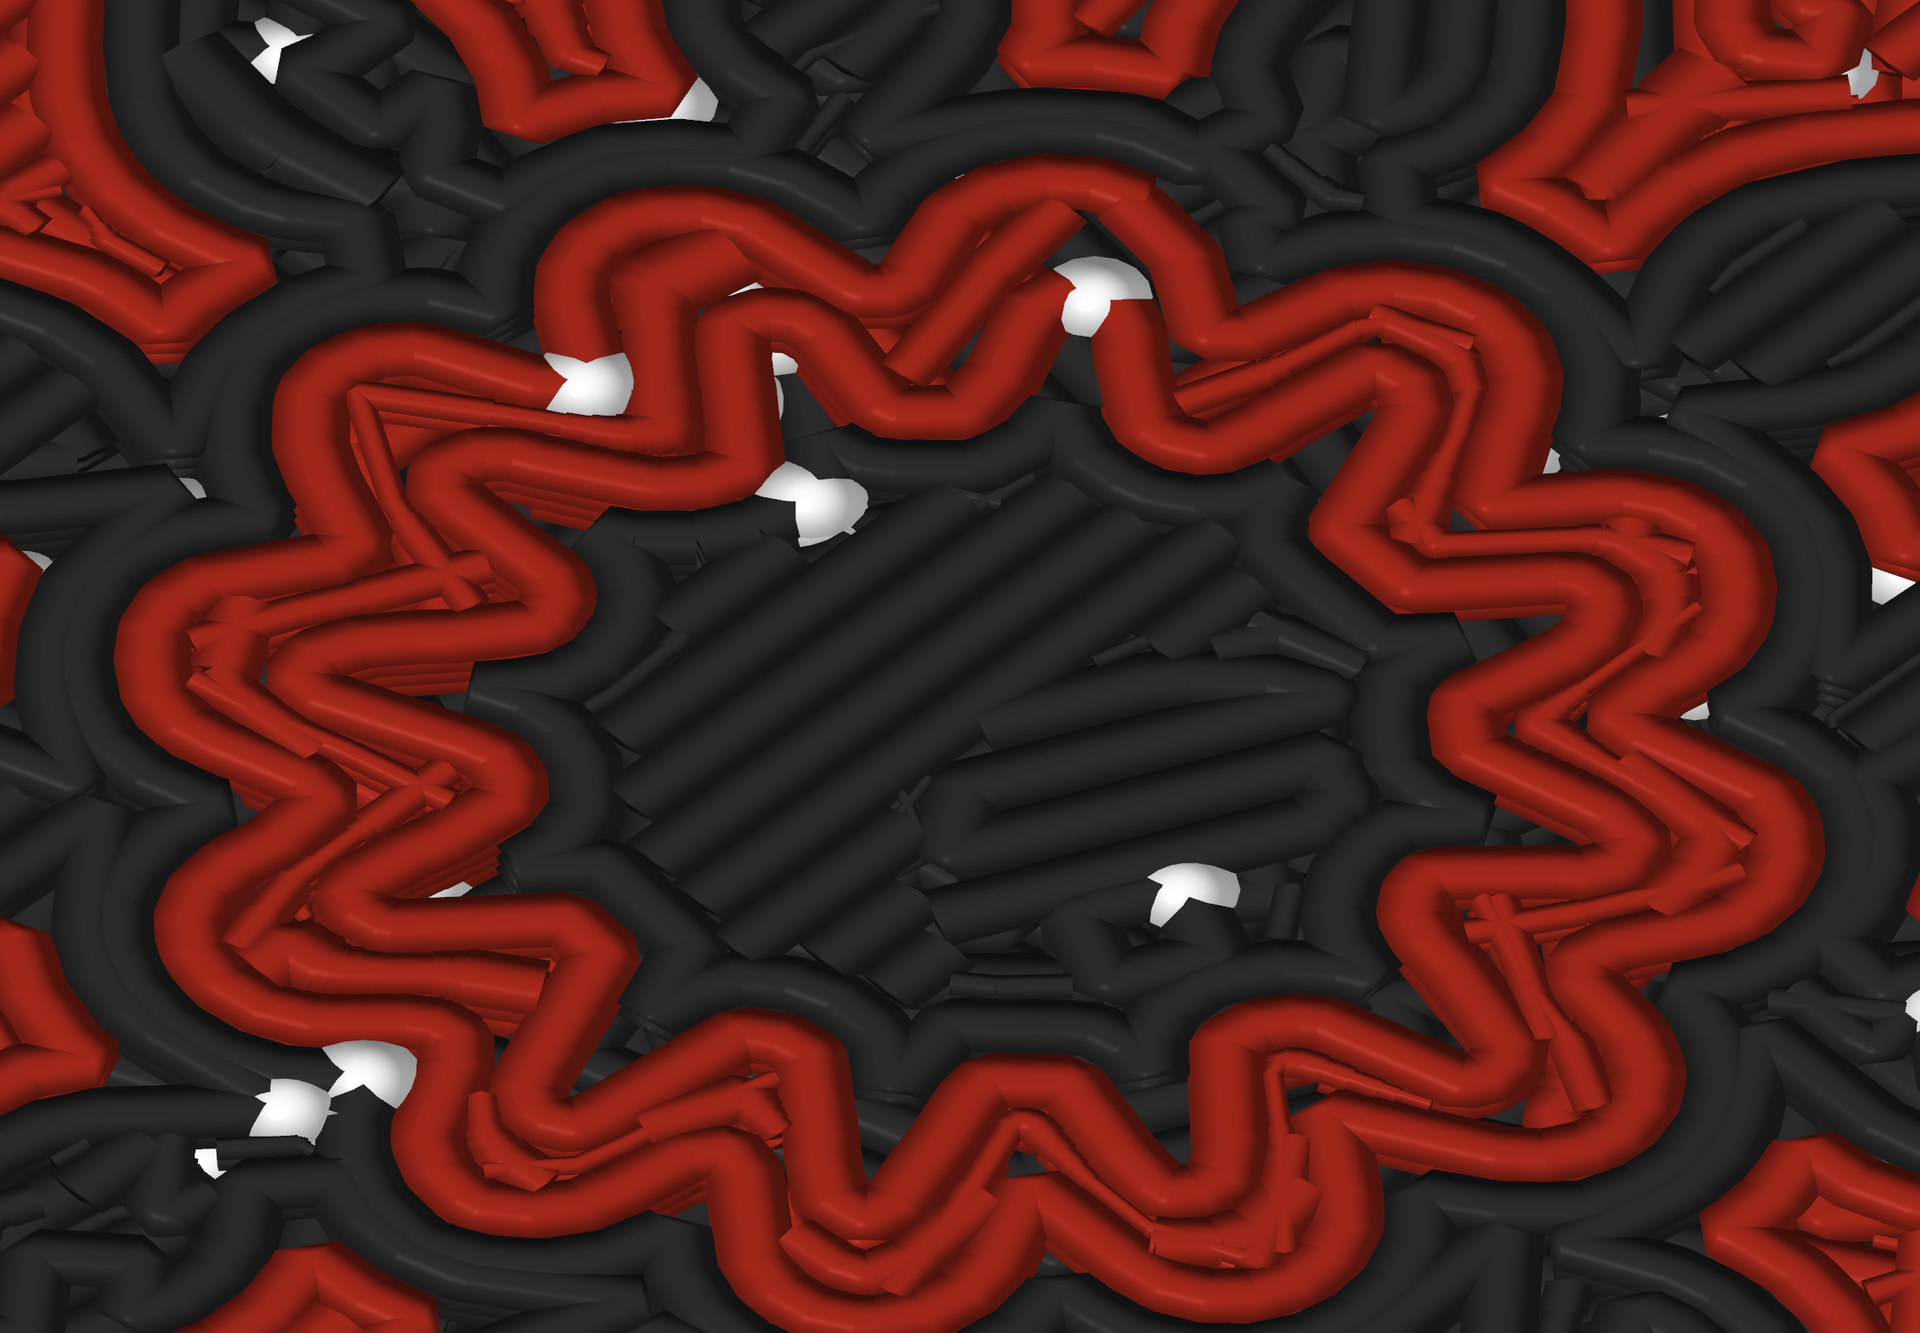
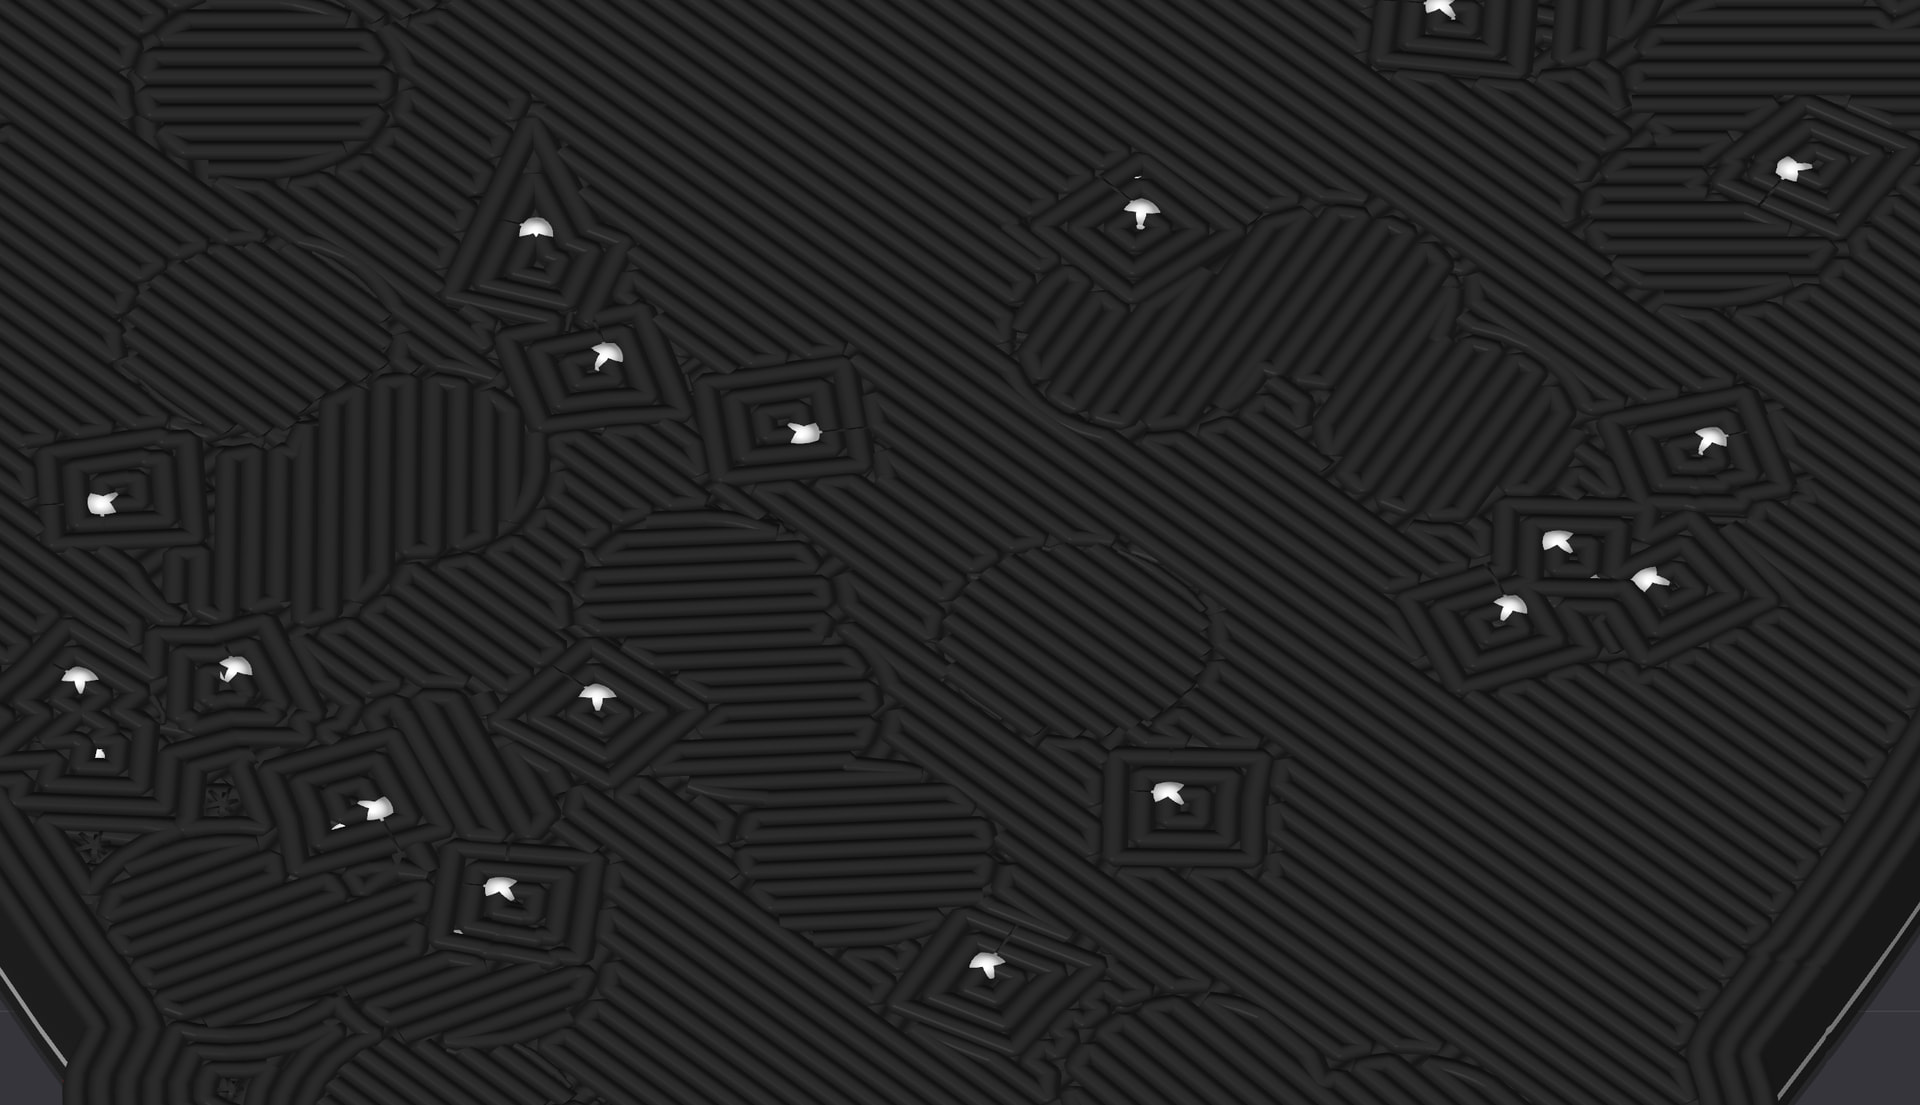
First of all, I reset your profile and saw what had happened. It’s much better now:
And now we come to the crucial question: why is that the case? This takes us back to point one: the object’s geometry is completely strange. Take a look inside the object - it’s not solid, but made up of all these strange shapes. As you can see from this cross-section, they crisscross in all directions.
There’s a lot of information here, and now you’re probably wondering: What now? Well, something in your workflow for creating the object isn’t working. This has nothing to do with the settings in Bambu Studio; your object is simply defective.
You’ll have to go back much further to fix the problem: How you created the object.
Not mistakes! You’ve encountered new learning opportunities!
I agree with all of Sharky’s assessments.
The instinct when exporting something into an STL/3MF is to turn the detail up as high as possible - that’s rarely necessary and in this case likely detrimental. The trick is turning the detail as low as possible while preserving the necessary detail.
Although already nicely resolved by @RetroSharky , I’d just like to add that surface holes are more prominent with “Monotonic” than with “Monotonic line” due to the path logic (90° for Monotonic, parallel to wall for Monotonic line) when changing direction.
“Circumferential” leaves the fewest holes, but those may quite large due to sharp corners in the tool paths.



 &
