I’m hoping someone in the community can help me solve a persistent print-quality issue that I have been unable to eliminate despite extensive testing.
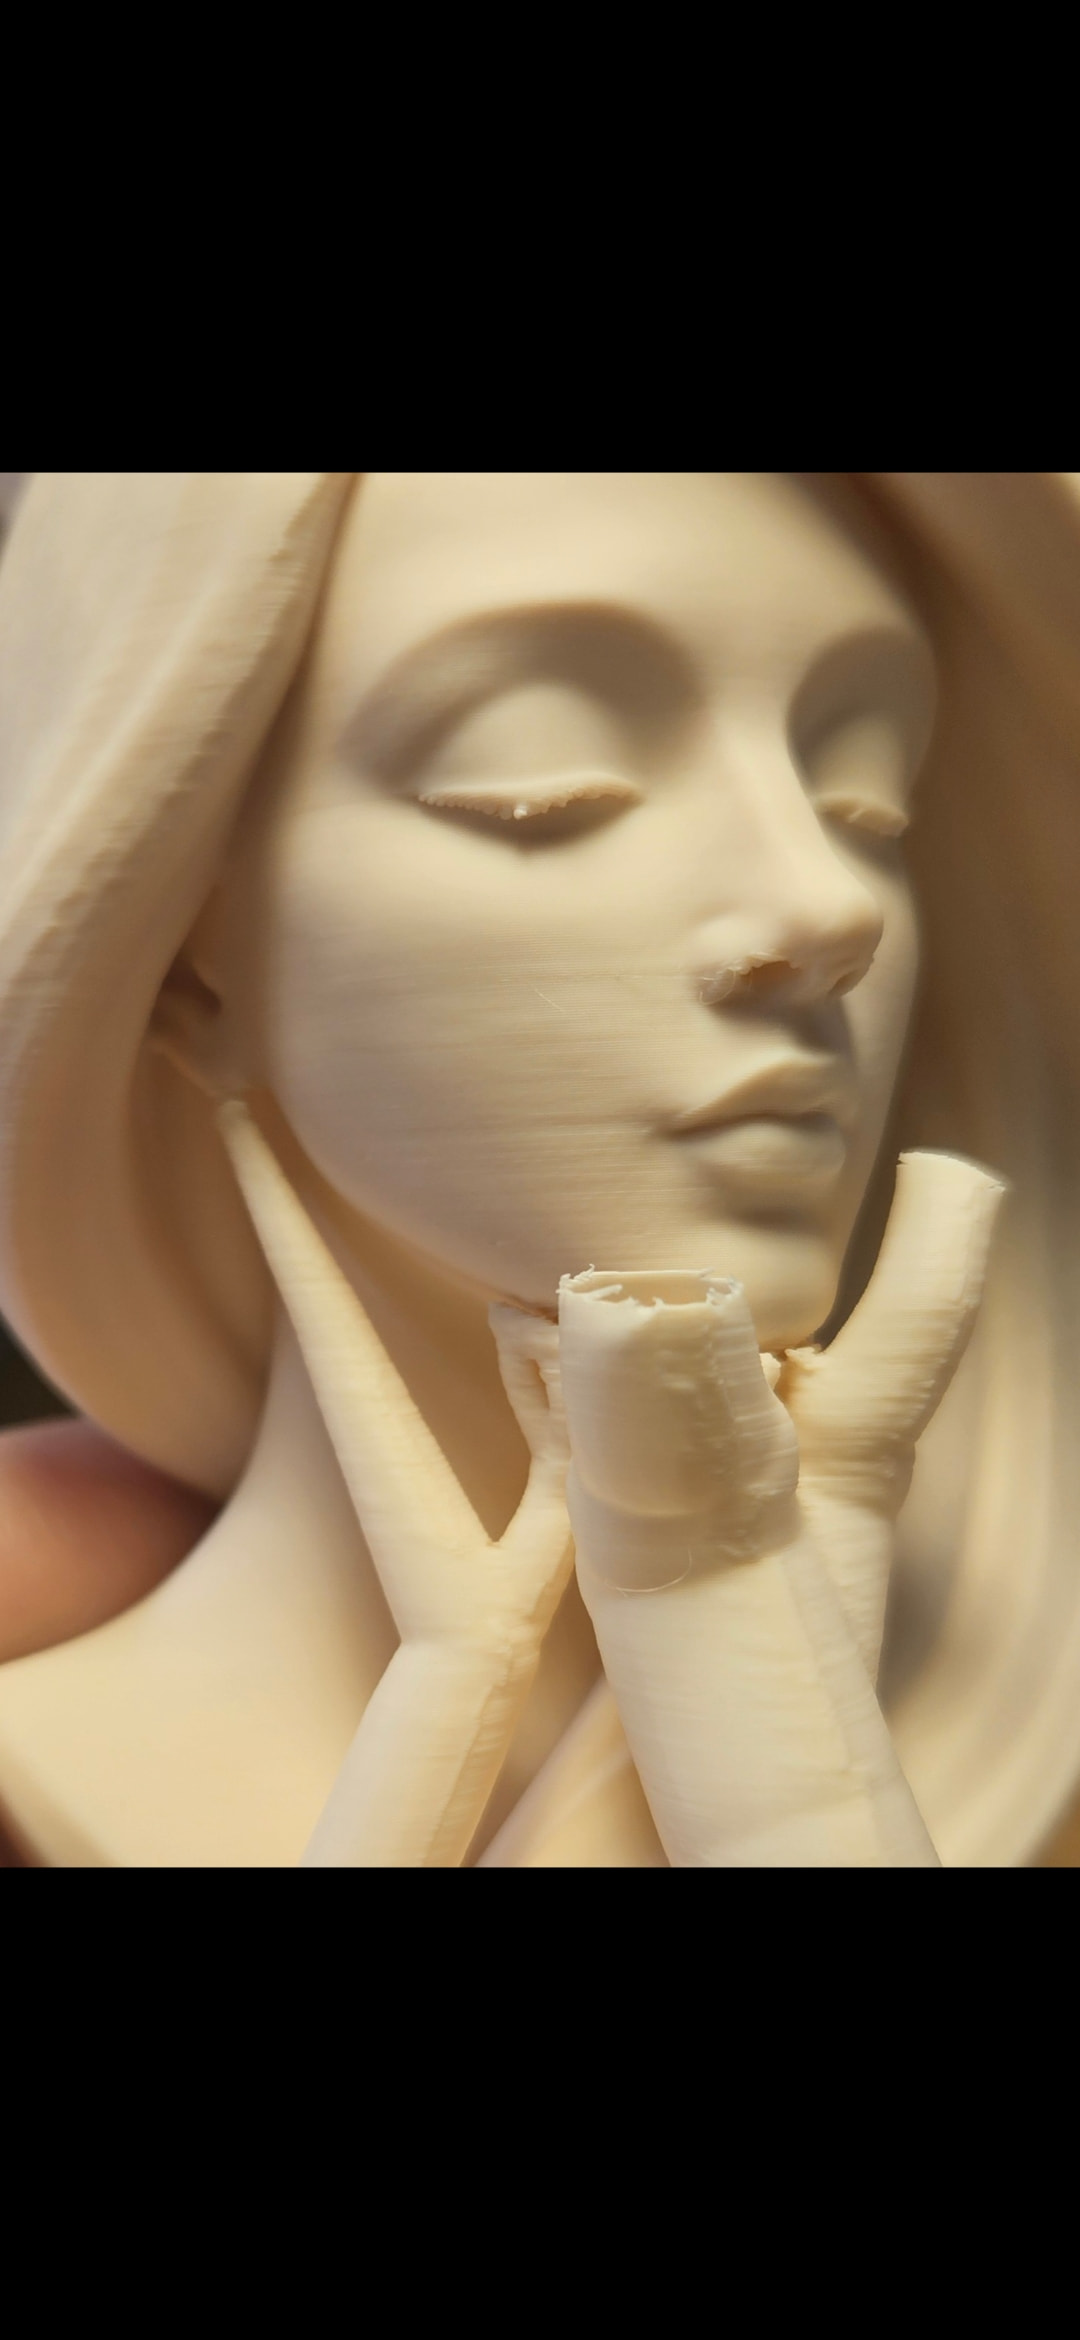
I print AI-generated figures approximately 150 mm tall using two separate Bambu Lab P2S printers. On nearly every figure, a very sharp horizontal line appears on the outer surface at approximately the height of the corner of the mouth or the bottom of the nose. This seems to be the point at which the model’s cross-sectional geometry changes significantly because of the lips, mouth and nose.
The line is not simply a change in gloss. It appears to be a visible physical surface irregularity that catches the light.
Here is everything I have already tested:
Testing on two separate Bambu Lab P2S printers
The same issue occurs on two independent P2S printers at the corresponding height of each model. The Z-axis lead screws on both printers have been cleaned and freshly lubricated.
The position of the line also scales with the model: it appears higher when the figure is enlarged and lower when the figure is reduced. For this reason, a mechanical Z-axis issue or fixed-height lead-screw defect seems very unlikely.
Uniform speeds and layer times
To eliminate sudden changes in cooling, flow or printing speed, I set all relevant speeds to a constant 60 mm/s, including:
Outer walls
Inner walls
Infill
Solid infill
Top surfaces
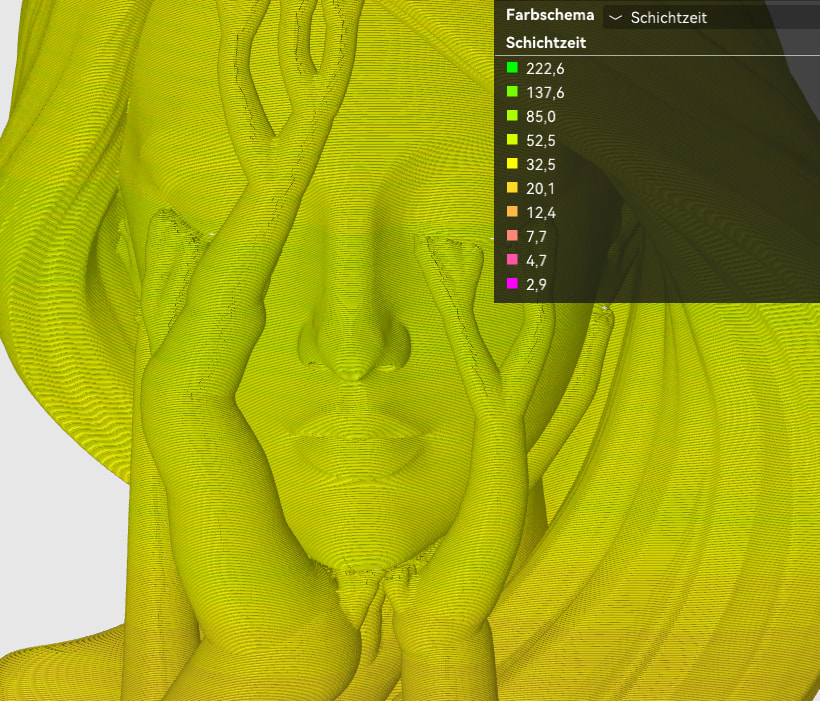
In the Bambu Studio preview, the model appears completely uniform in the Layer Time view, with no visible changes around the affected layers. Nevertheless, the line still appears.
Wall and geometry settings
I also tested the following settings:
Wall printing order: Inner/Outer/Inner
Wall loops: 4
Wall generator: Classic
Ensure vertical shell thickness: Disabled
Infill/wall overlap: 0%
None of these changes eliminated the line.
Different filament
I originally printed the figures using Bambu PLA Basic. I then changed to Bambu PLA Matte, hoping the matte surface would reduce or conceal the visible line.
Unfortunately, the line remained clearly visible and appeared physically unchanged.
STL mesh checked
Windows 3D Builder reports the STL files as healthy, with no detected non-manifold geometry or other repair errors.
The strangest and perhaps most important observation is this:
If I use the cutting tool and print only the head or face, without the neck and body underneath it, the cheeks, mouth and lips print perfectly smooth. However, when I print the complete figure from the base upward, the horizontal line returns.
Current modifier test
I am currently testing a modifier cube over the affected facial area. Inside that region, I have reduced the number of wall loops from four to two and set the infill to 0%. The idea is to isolate the facial geometry and create a thin eggshell-like structure, in case the defect is being caused by internal geometry, infill or accumulated shrinkage from the body below.
Has anyone experienced something similar, particularly with AI-generated meshes?
Could this be caused by a sudden change in layer cross-section, internal stress, wall thickness, polygon density, vertex normals or another mesh-related issue that is not detected as an STL error? The fact that the isolated head prints perfectly smoothly, while the same head develops the line when printed as part of the complete figure, is especially confusing.
I would be very grateful for any ideas or settings I could test next. I will attach photographs showing the defect, along with screenshots of my Bambu Studio settings and preview.
Can you color code by layer time? I wonder if that section is taking longer to print so cools and shrinks more?
Not sure how to compensate on this kind of model. On boxy things adding chamfers can help to reduce step changes in layer time but no idea on curvy stuff.
If it is a layer time / cooling issue, maybe a warmer printing chamber?
Thank you for your suggestion! I already checked the model in the Layer Time preview in Bambu Studio. After setting all relevant speeds to a constant 60 mm/s, the entire model is displayed in a uniform yellow color, including the affected area around the mouth and nose. There is no visible jump in layer time at the exact height of the line.
I have attached a close-up screenshot of the Layer Time preview for reference. A warmer chamber might still be worth testing, although it remains strange that the isolated head prints perfectly smoothly while the exact same area develops the line when the complete figure is printed.
For the isolated head, the oddness will be sooner in the print and closer to the build plate for whatever influence that may have.
On the full figure it would print much later. I’m not sure what part of that is triggering the line though.
Maybe others will chime in? There’s a number of threads here though about those kinds of surface anomalies but generally with boxes where chamfers can help. But they do talk about chamber temps, bed temps, and such too.
Vielen Dank! Der unterschiedliche Abstand zum Druckbett ist ein interessanter Punkt, an den ich bisher noch nicht gedacht hatte. Ich werde mir auch die Bauraum- und Druckbetttemperaturen genauer ansehen. Nochmals vielen Dank für deine Hilfe!
Use the layer bar on the right of preview to scroll down to the affected area. Is there anything in the geometry that stands out?
Provide a photo with the support still in place from your current test print, in case the support is causing or otherwise what you experience.
As you have printed on two different printers (albeit, the same models), it is less likely to be hardware issues, although it doesn’t rule out a hardware problem, but one that doesn’t jump out.
Its unpopular to say but I think you should manually calibrate your pressure advance. Thats the thing that really hammers home how crisp your overhangs transition back into regular printing. Turn the automatic stuff OFF, print a test down to 0.005 resolution, input the value, save, and go. Use the EXACT same profile you use to print this thing to print the test [speed/accel/filament settings]
One thing nobody’s checked yet, takes about thirty seconds. Right-click the object in Bambu Studio and use Split → to Objects. If it comes apart into more than one, there are nested shells inside the mesh. Image-to-3D generators leave them around the mouth and nostrils in particular, because the reconstruction reads those as cavities and closes them off as separate volumes. 3D Builder will still call that healthy. It checks that edges are closed, and two closed surfaces sitting one inside the other pass that test fine.
Though I’ll argue against myself here, because your own observation doesn’t fit. If an inner shell were the whole story, the isolated head would show the line too, same place relative to the chin. It doesn’t. So more likely the geometry decides where and the cooling decides whether. Something changes in the cross section at lip height, and on the full figure that layer lands somewhere thermally different, while low down on the head it doesn’t. Which lines up with the point made above about how much earlier the head prints and how close to the plate.
So before touching pressure advance, scroll the preview to that layer and compare it with the ten below it. Wall count, estimated layer time. If the cross section narrows sharply right there, layer time drops with it and cooling changes, and then it’s a minimum layer time or a slower outer wall rather than PA. Calibrating PA by hand is good advice in general, I just wouldn’t expect a PA error to show up once at one height on two machines. It’d be on every corner and overhang on the figure.
If you’re reprinting anyway, cheapest test I know: scale the figure to 115 or 120%. Line stays at the lips, it’s the model. Line stays at the same height above the plate, the file is innocent and it’s the profile. Two printers with the same file and profile rules out one printer, not the other two.
(Disclosure: I work on PHORM, a repair and validation tool for generated meshes. Everything above is just Bambu Studio.)
 &
