How do I stop black from bleeding into white on multi-color sign?

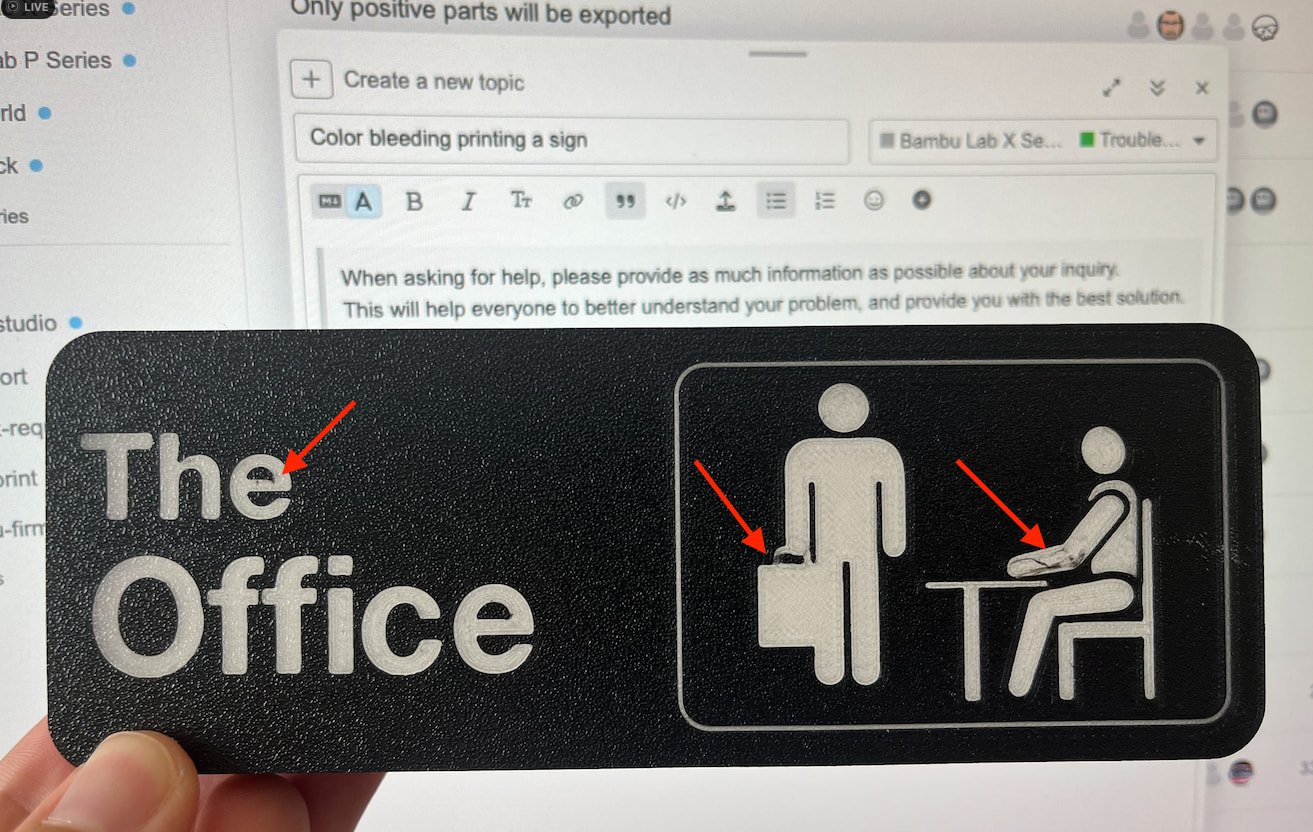
I have a sign that I print in black and white, but I’m almost always getting some black in random spots of the white part:

I’ve tried purging more filament, changing the prime tower settings, etc., but it always ends up happening.

Is there anything I’m missing? Any other way to make sure this doesn’t happen, or at least to reduce the chances as much as possible?

The white filament is a translucent glow in the dark filament, so any black bleeding into it kinda ruins the sign :frowning:

If you are talking about an X1. Steinwipe is great for this. It has Gcode to wipe after color changes. And tuning your purge amounts will help.

Couple things I have found to help.

  • Clean the tip of your nozzle before you print making sure to remove any crusty bits stuck on it.
  • Make sure your filament is dry as moisture can cause stringing.
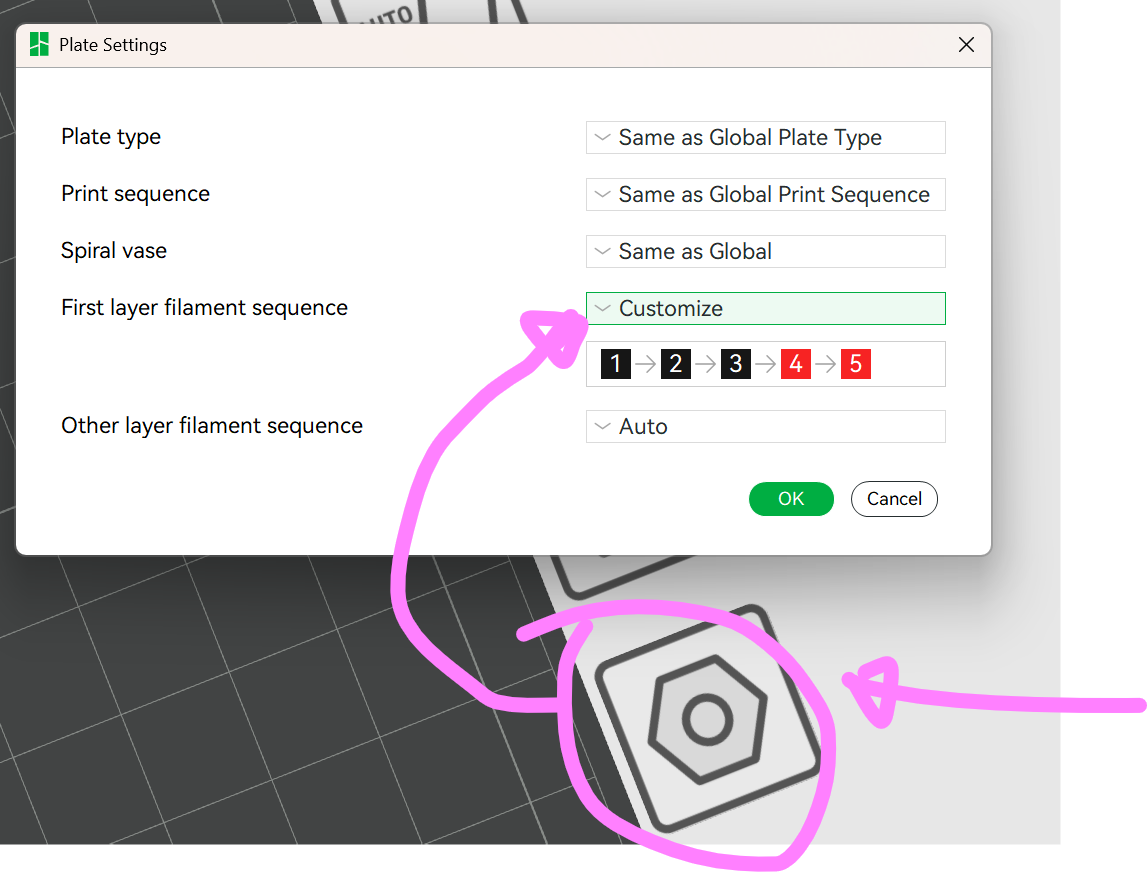
  • Set your filament print order so that that white filament prints first.
  • Put a pause at the beginning of the second layer so you can manually brush off the first layer of the print.

I have the X1C yeah.
That’s cool, I didn’t know about it. I’ll definitely give this a try.
Thanks a lot!

Great advice, I haven’t thought about putting a pause and cleaning the layer and even the nozzle tip after printing the consecutive white layers.

I’ll give it a try and see, thanks a lot.

This is the one that helps me most. It’s this control:

Your first layer is often slower than regular printing, so it can show wet filament extra extrusions/wispys a little more severely than the rest of the print too. Maybe consider a dry on the black just in case too

The white has been printing first always. The problem is that because it is translucent, if the second layer bleeds some black it shows :frowning:

Do you know if it’s possible to add a pause after a color change? so after changing to the other color’s filament and purging, pause there so I can clean the nozzle and then continue.

To my knowledge you can only insert a pause via Bambu Studio at the start of a layer. Another option is to manually edit the gcode file.

Having said that you might be able to trick the system into pausing by loading both colours into the AMS, starting the print and then removed the second colour once the first colour has started printing. This “should” cause the print to stop when it gets to the second colour and wait for you to (re)insert the second colour filament.

I haven’t tried this personally so I can’t say for sure that it will work.

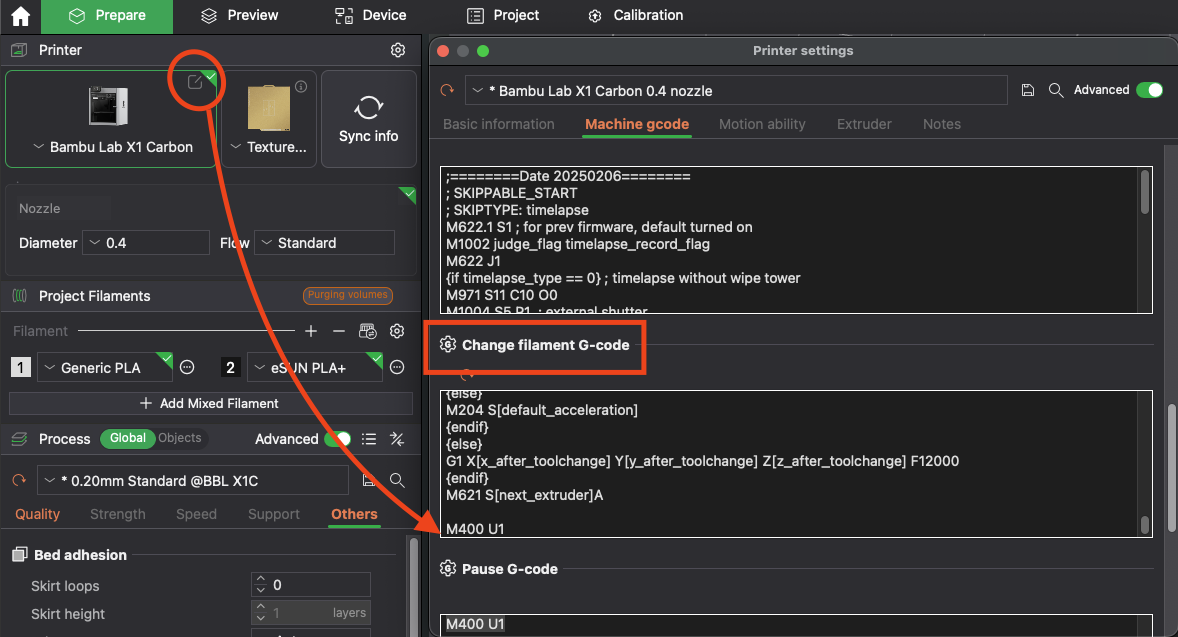
So I was able to add the pause command right after changing color and purging.
If you open the printer settings there is a section called “Machine gcode”. And there you can modify or add extra things.

I just added the M400 U1 pause command at the end of the Change Filament g-code section:

I did a test print, cleaning the nozzle every color change and looks like I got better results. I’ll keep testing this.

Thanks everyone!

I’d forgotten adding it to the colour change gcode. Well done!

There may or may not be another problem. If your printer inside surfaces haven’t been wiped down occasionally, wisps can accumulate in the printer. Use a can of air to blow away wisps from your print and you can stir up more wisps to fall into the print.

I use masking tape (tack rag should also work) to wipe down the inside of my printer like using a lint roller. It can help.

Also, during filament changes, a low angle flashlight beam can reveal bits to remove with masking tape.

How do you change the color print order? I didn’t know that was a thing.