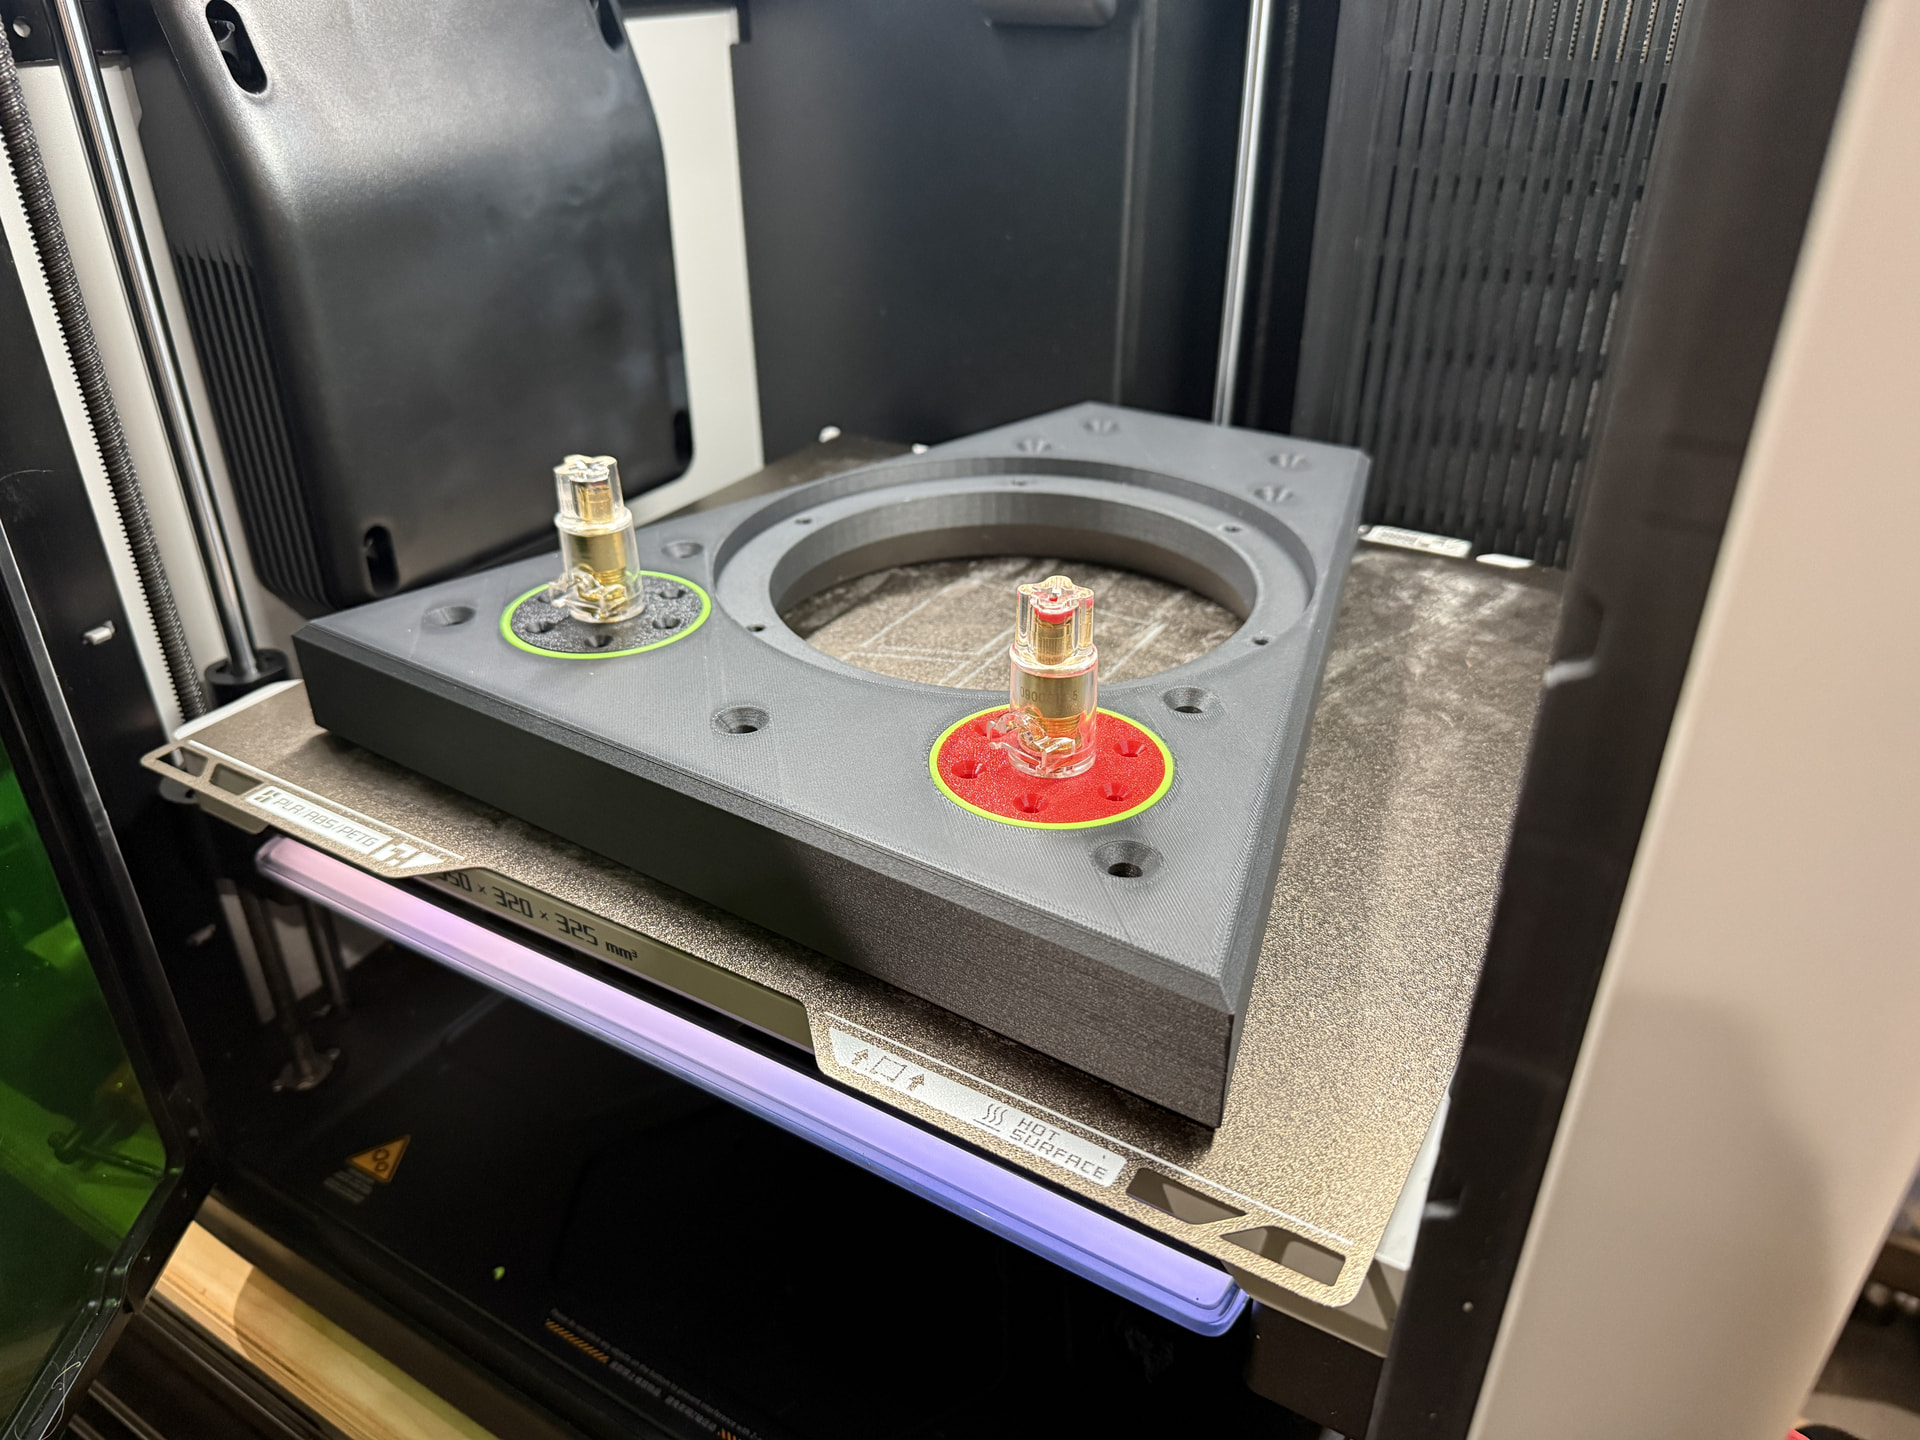
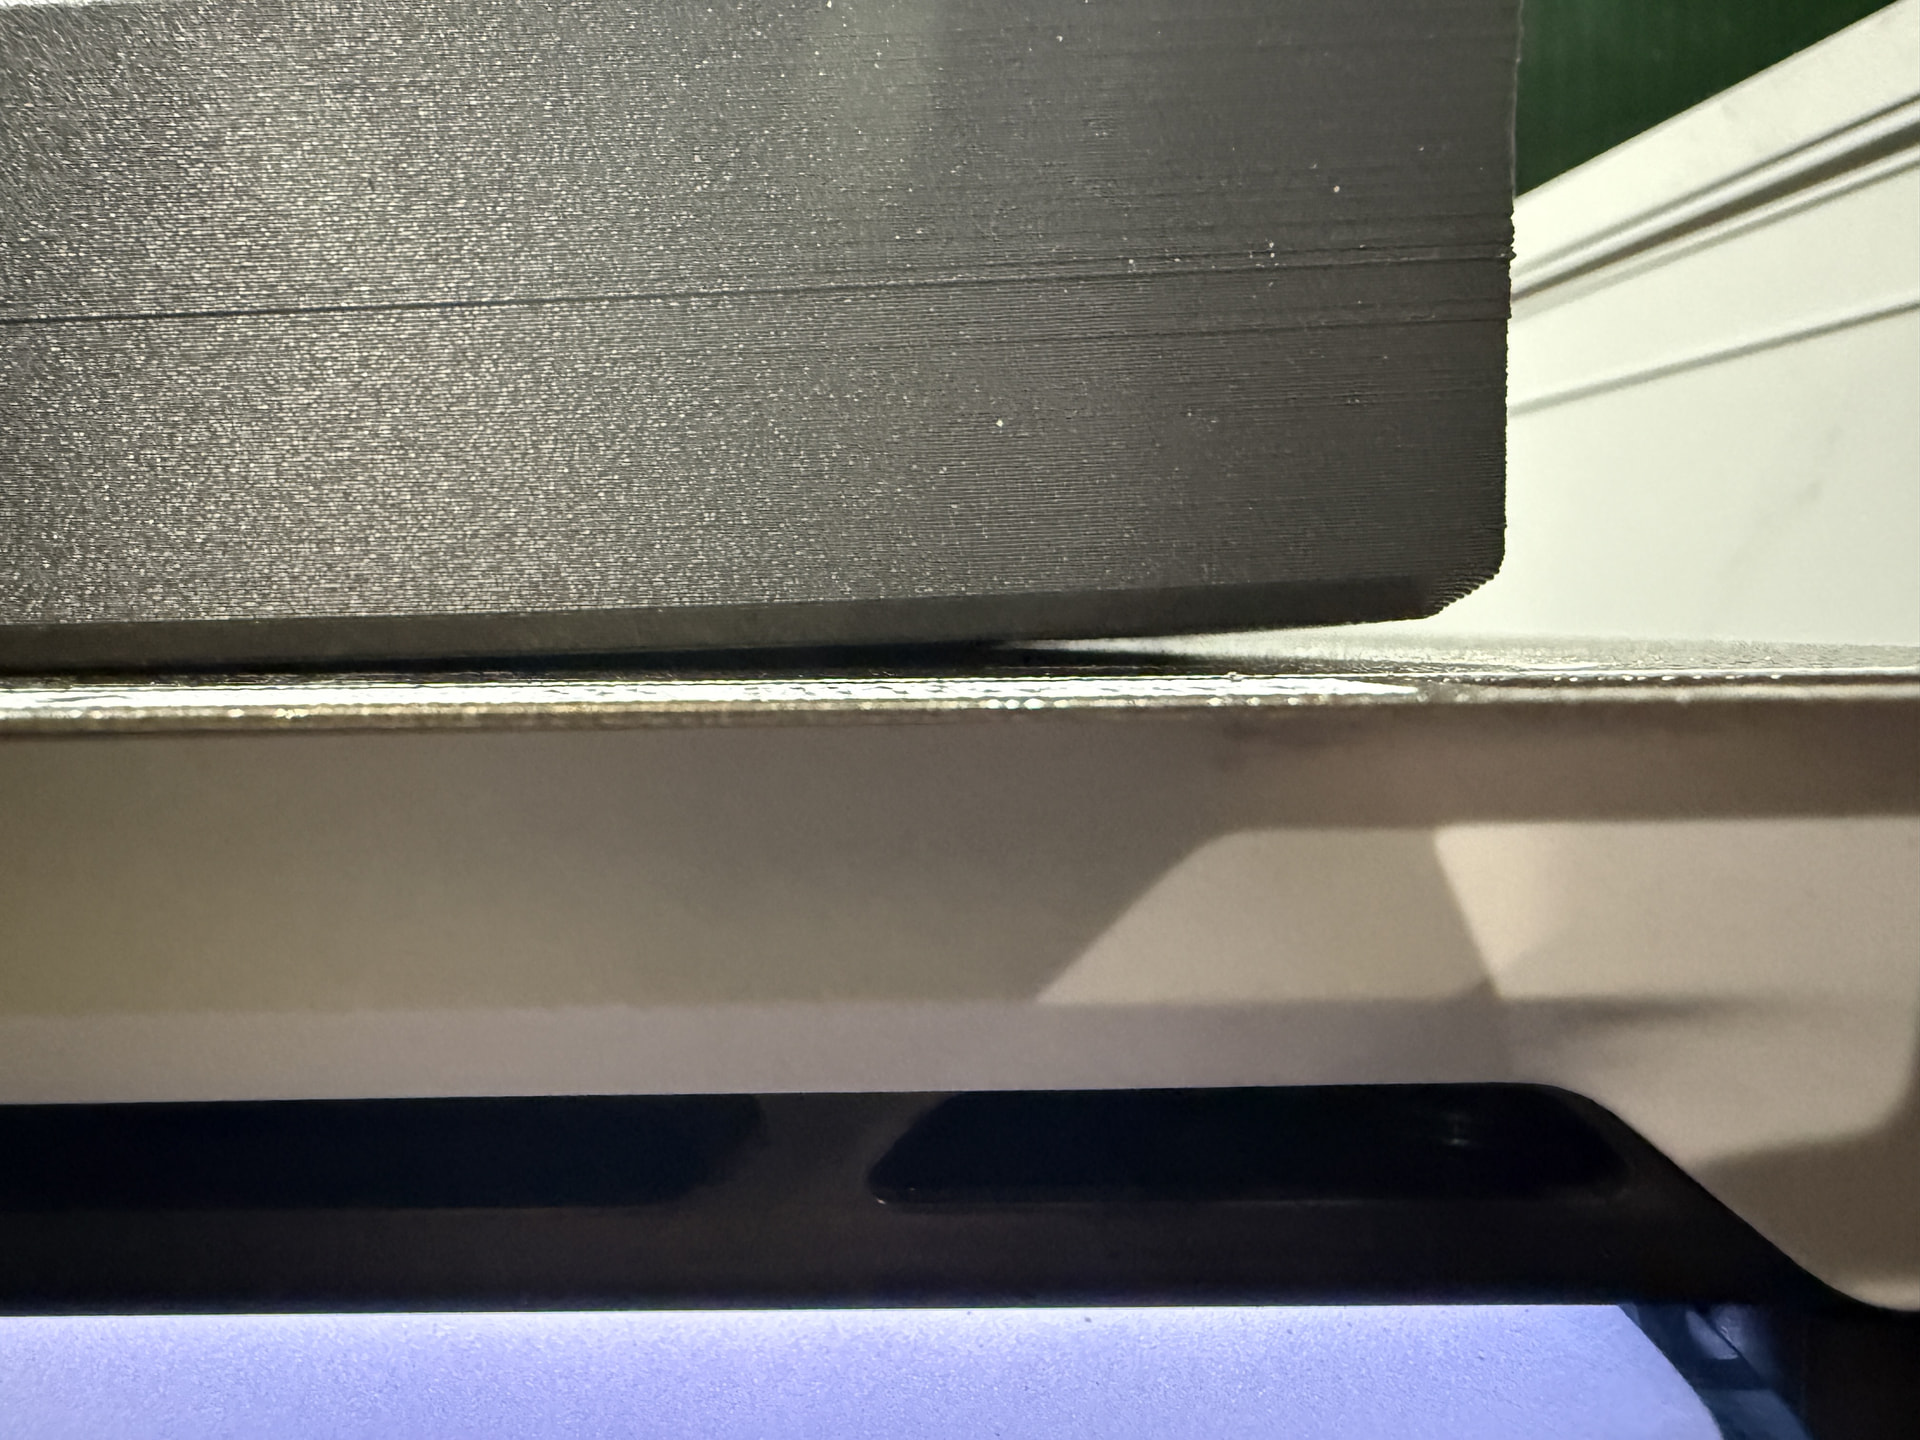
Greetings! I have a pair of H2Ds that have been working very well for me over the past ~18 months or so for smaller projects, but I’ve ‘graduated’ to a larger project of my own design and have hit a snag. Namely, on long and large prints (>1 day print time @ nearly the full bed width) I’m seeing notable retraction of parts from the bed at the corners of the print. This is important because these parts need to seal against each other using a thin TPU gasket.
Apologies if this has been posted before - I did attempt to use the search feature.
Materials I’ve tried include PLA, PETG, and PETG-CF. PLA is not preferred for this project but shows the least retraction (but it does retract). PETG and PETG-CF unsurprisingly show about the same retraction. The CF variant is the filament of choice for this particular project but I also need PETG and PLA to work.
Thing I’ve tried include beveling the underside edges slightly and manually increasing be temperature by a few degrees. I’m wondering if I should go further on the temperature, but I have little experience in that since the printers have always been pretty flawless on other prints. Could use some input there. I typically just use glue sticks by the way, but I don’t see any adhesive solving this problem as it’ll often just bring the bed with it if it’s really stuck down.
Photo ‘reenactment’ of the issue shown below. (the other parts were printed separately from the gray PETG-CF, except the binding posts of course, which were purchased).
All printed plastic shrinks - it’s a % of the original length, so the longer your uninterrupted length, the greater the shrink length, and very thick walls make that force greater until the ends are able to break loose from the plate. As printers get bigger this becomes more of a problem.
Alright, so in summary (between your comment and several others you reference in that thread) :
The 6 walls I’m using probably contributes, if I could reduce that it may help. Note that infill is at 25% for this particular part but would only be 15% (while maintaining the 6 walls) for much taller prints of the same overall shape (but not nearly as ‘solid’).
Increasing bed temperature AND chamber temperature may help, though the specifics on what temperature to use are currently not known.
Specifically drying the PETG-CF in the AMS2 would likely be helpful. Due to the volume of filament being used (and the fact these are second gen prototypes) I had been skipping that step to just load a bunch of new rolls into the AMS2. This is the one very obvious area to improve upon for the (hopefully) final prints for this project.
Adding relief lines in the model may also help. Need to watch some videos on how to implement those to see what, if any, could be done.
Re relief lines, this is a pretty good (starts at about the 2min 15sec mark) discussion of the technique:
You may want to try a high-grip bed such as Bambu’s Cool Plate Super Tack. It comes to mind because I just gave one a try myself and holy !@#$% was it a challenge to remove my part. But, I think this would be more of a hack than an actual solution to your problem – I think a design tweak would be more reliable.
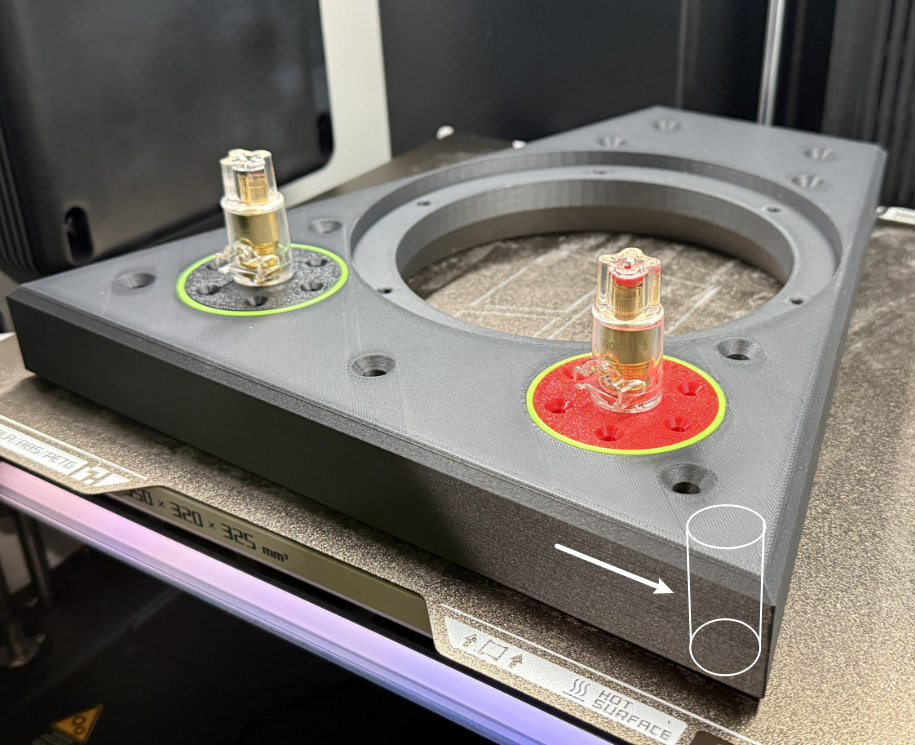
I’ve found adding an inner empty cylinder at near the sharp corner really helps, For such large piece, you would want to have multiple inner cylinders along the edges. You don’t need go from edge to edge, I typically go 1/3 of the length on each end.
With PLA & PETG, wipe textured PEI plate with 99% IPA works like glue. It does leave a tiny bit of white stain on the bottom layer.
I might repeat some of the things already mentioned by others, but here is what works for me for large warp free PLA/PETG prints:
Use a Supertack or Frostbite plate - the adhesion is much stronger
Use gyroid infill - it wont pull as much on the side walls when it shrinks during cooling
Reduce or turn off the cooling fan speed - will prevent overcooling and warping on large PETG items
Turn off the AUX fan if its on
Reduce or turn off the chamber fan speed if the printer is in a cool room
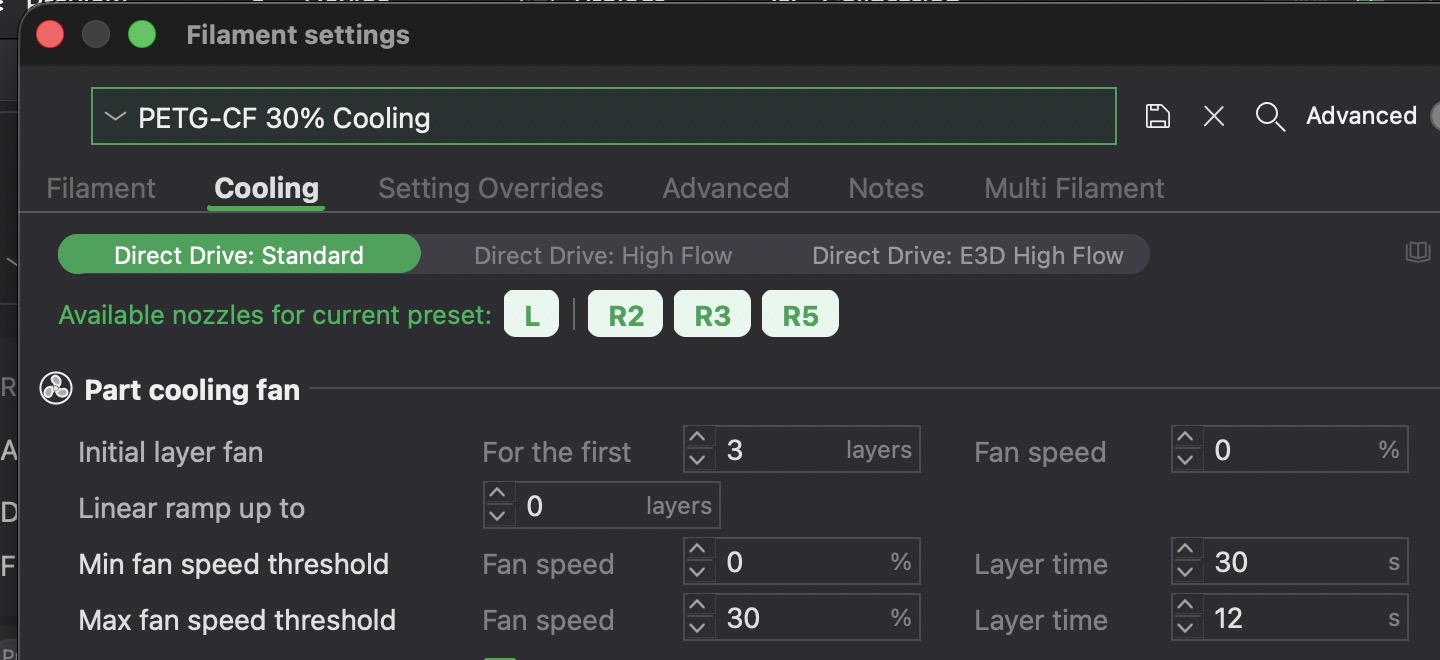
For me with large PETG items the biggest help to prevent warping was custom profiles with cooling turned way down. Here is a screenshot of my profile for large PETG-CF items
cold plate (supertack, frostbyte kdeavi) run at nornal bed temperatures will increase adhesion)
for large prints on an h2d even for pla i like to run the chamber temperature at 41 degrees. no issues with heat creep and much less warping, even with “just” the standard pei sheet.
Assuming geometry wont be changed –
The way the stresses line up from walls is inherent and unavoidable, you want walls, walls are your strength. A key part of controlling this bottom edge curl is the cool plate. If you hold the material under the glass transition temp, it cannot curl. It will break free suddenly, or pull the plate off the magnetic backing, etc, but it can’t just deform. PLA typically glasses at 55C, so a plate that lets you go under that is pretty key. @designrama’s mockup is a good start for making the geometry changes. I’ve also found that just slapping a gridfinity template on the bottom [42mm square outline cutouts] is a quick and dirty way of deleting this frustration, but it isnt always a viable option