When asking for help, please provide as much information as possible about your inquiry.
This will help everyone to better understand your problem, and provide you with the best solution.
- Detailed description of the problem
- Printer model used
- Slicer settings used
- Type of filament used
- Photos that clearly show the problem
- .3mf file (if the file can be shared)
- Any potentially useful information that is related to the problem
Currently I’m working on a print that has imbedded magnets. Sometimes the layers right above the magnets are not adhering correctly. I have added ironing to the top most layer and that seems to have helped but I was wondering if anyone had some other recommendations to try.
I’m using a P2S
my settings are pretty much unchanged from the initial. Just some changes to infill density, infill pattern, added supports, added brim, and topmost layer ironing.
I’m using PETG Basic
Here is some pictures of what is happening
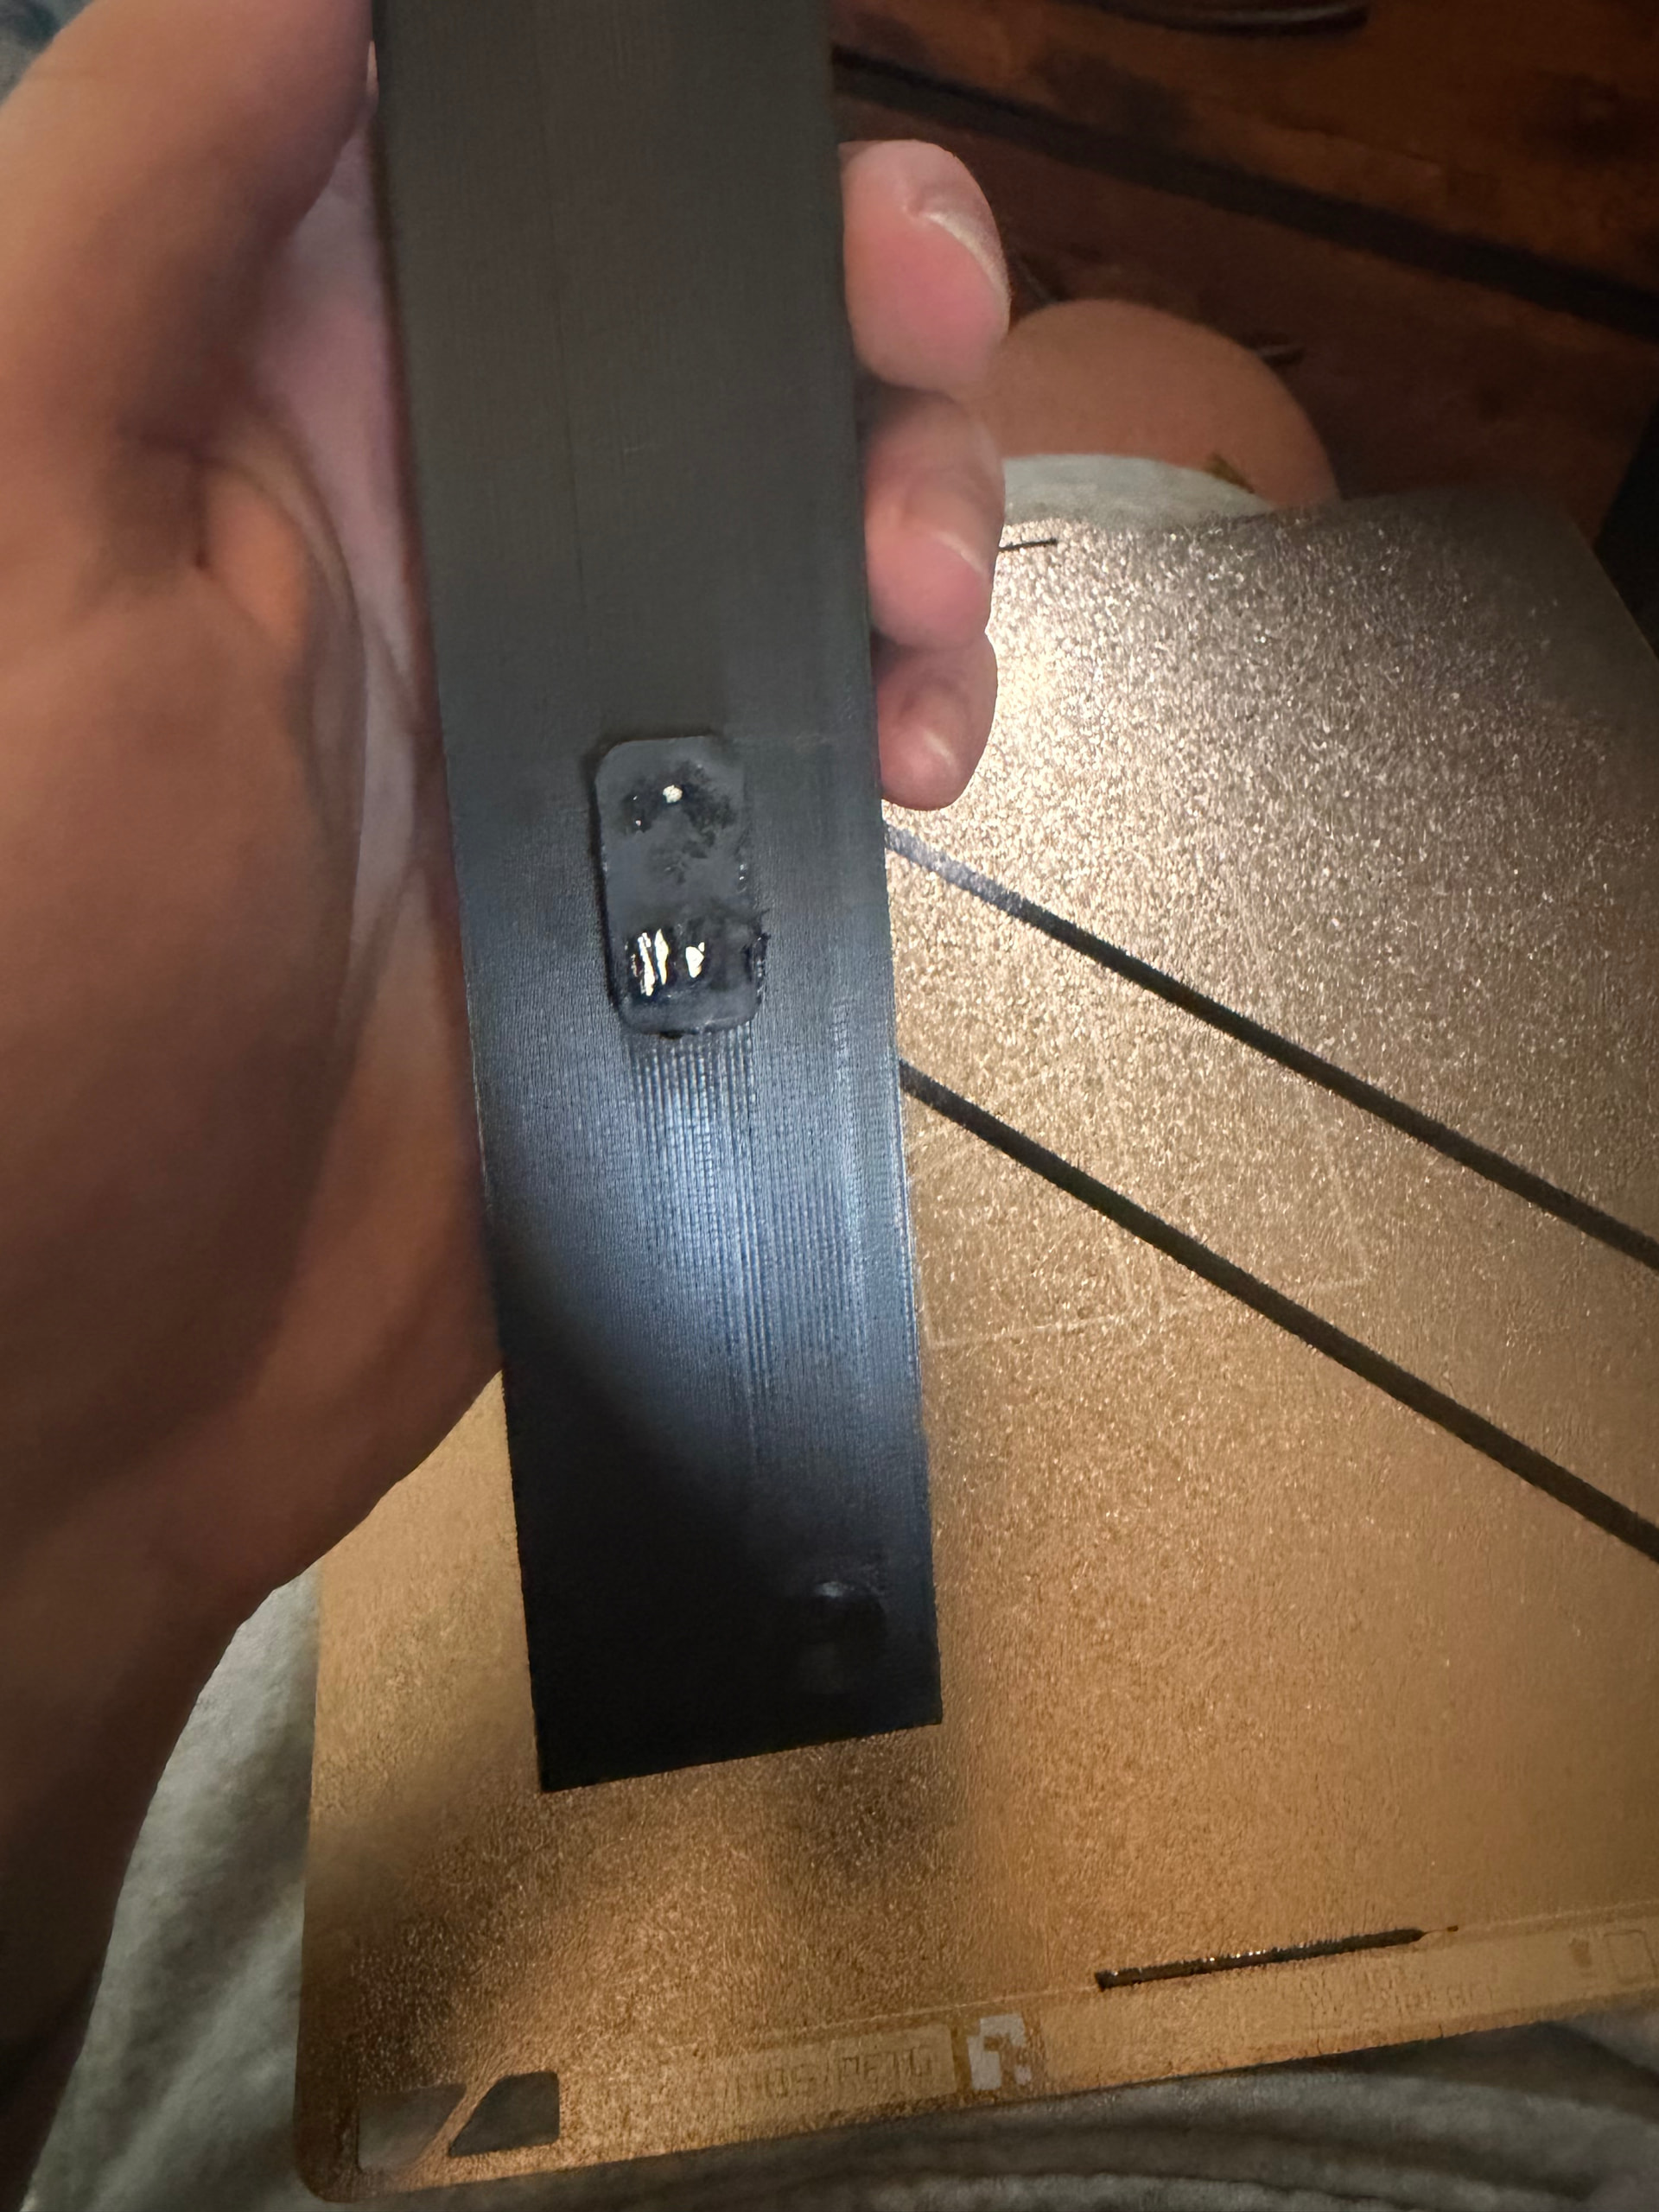
The magnets are snug and there is not an excessive area above the magnet and the next layer. It just seems to not adhere and then creates spaghetti for the first layer then the second layer and the ironing seems to be fine