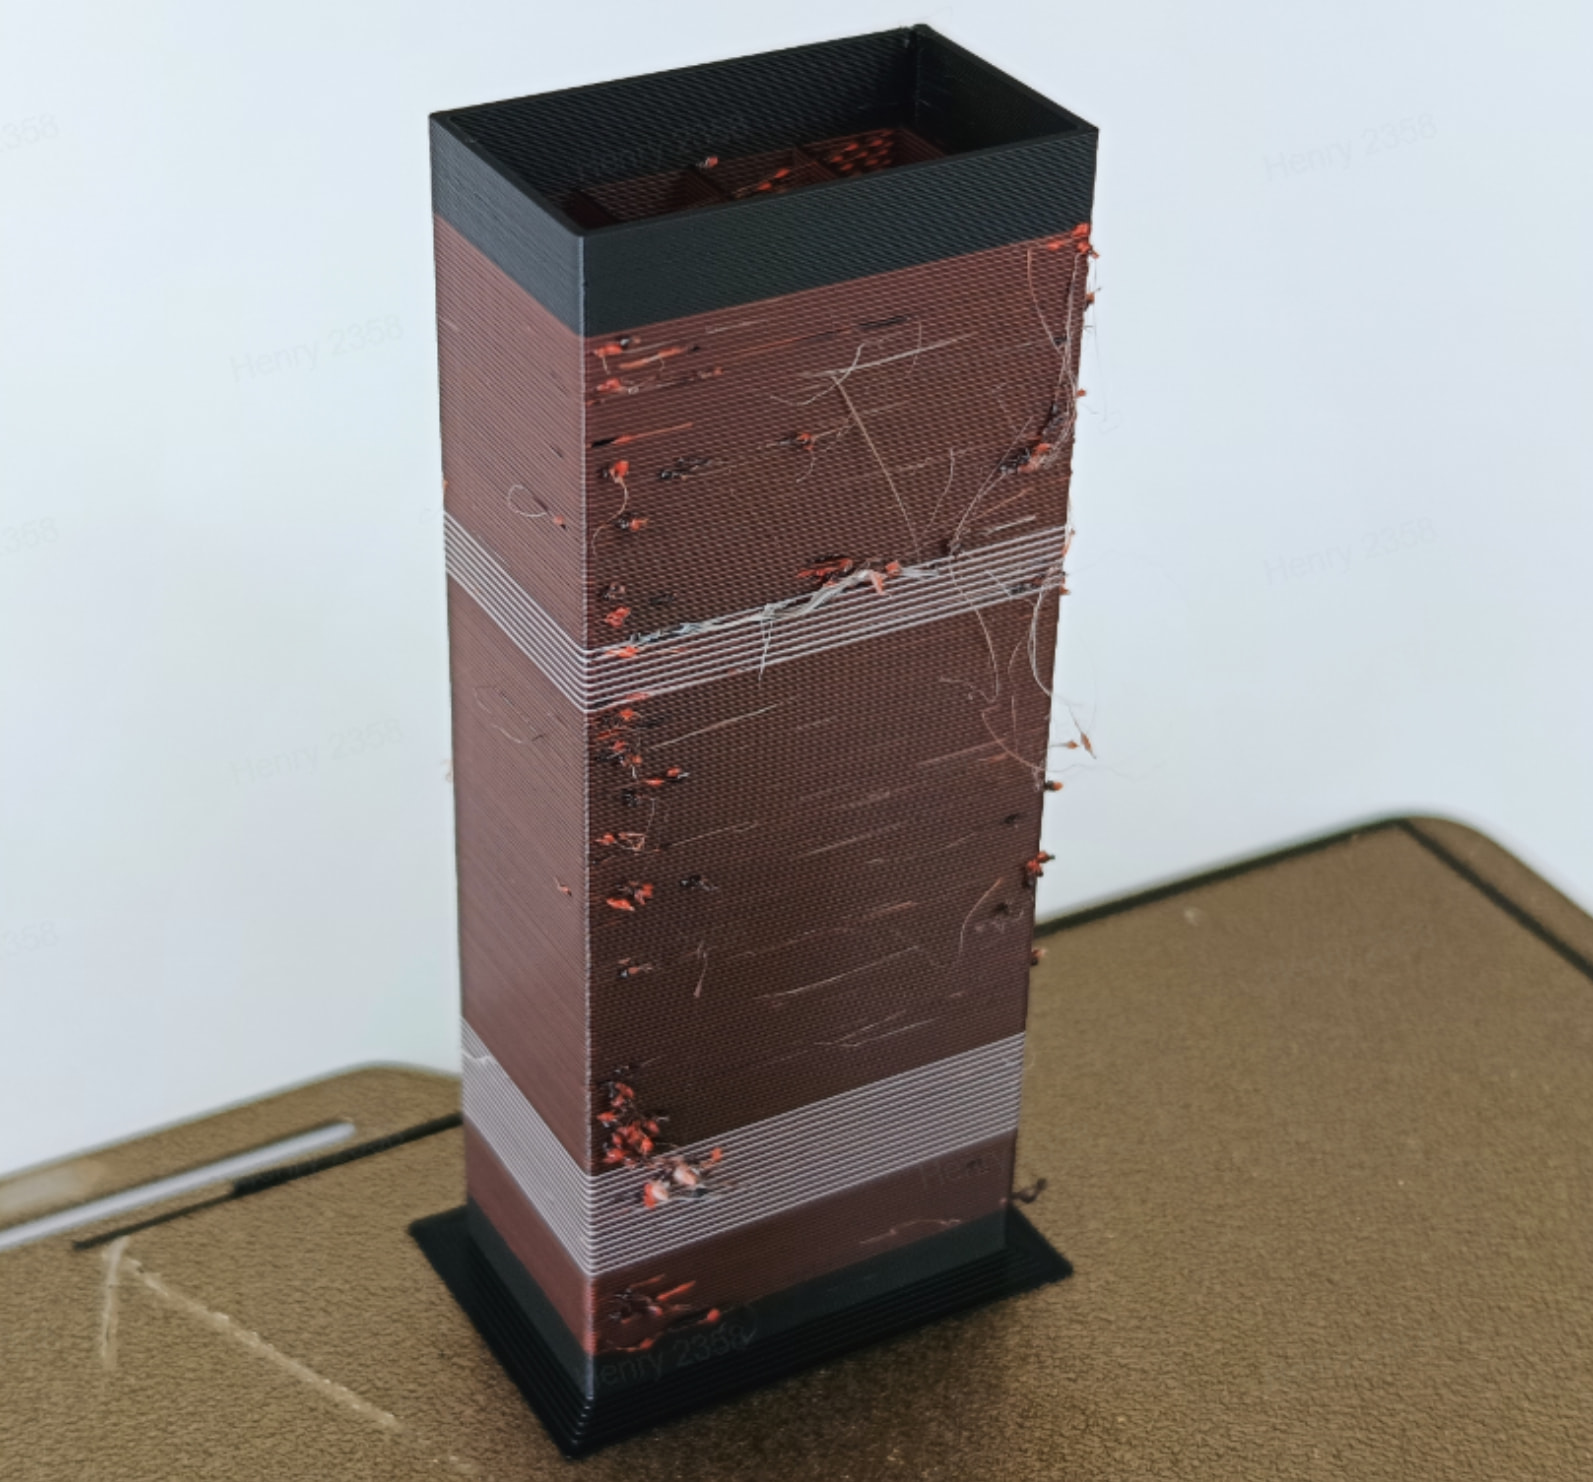
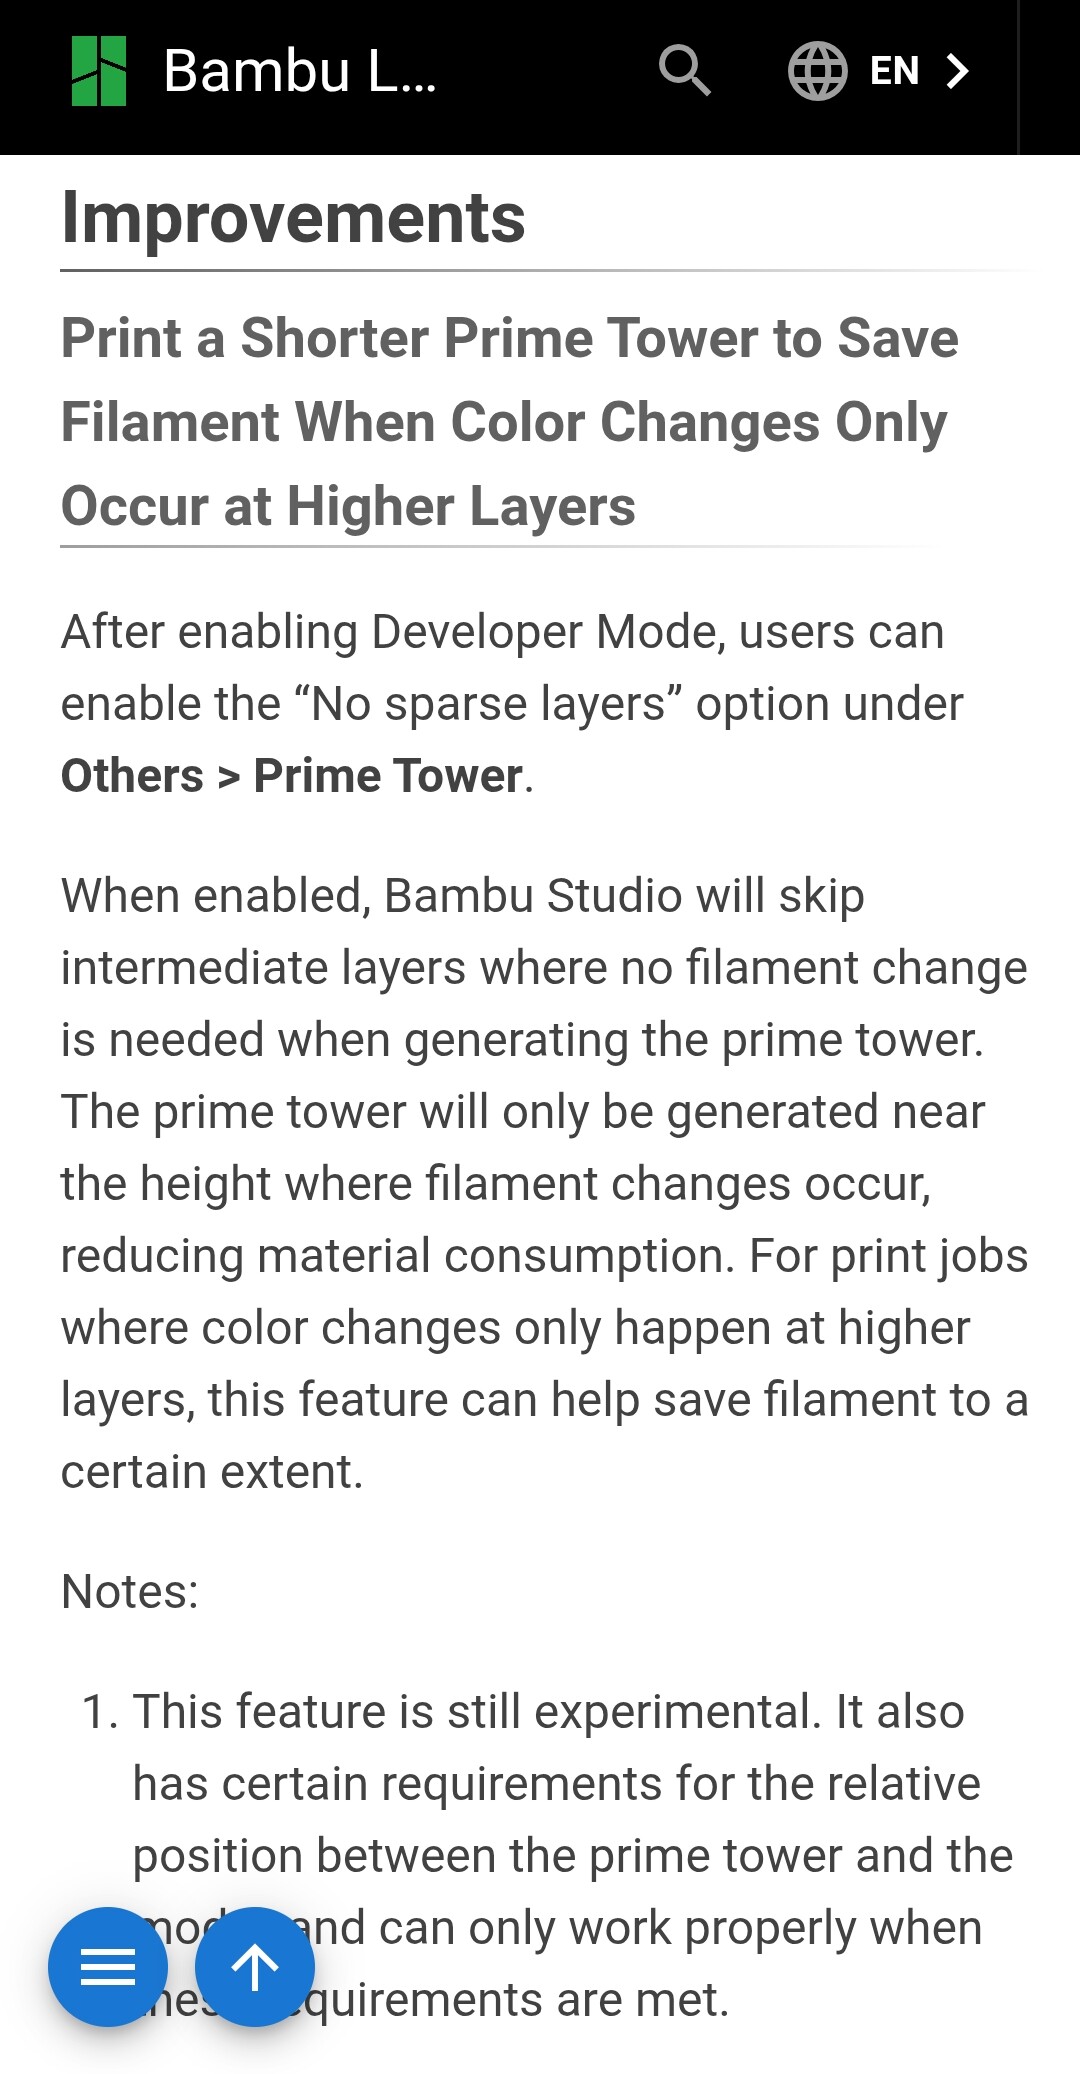
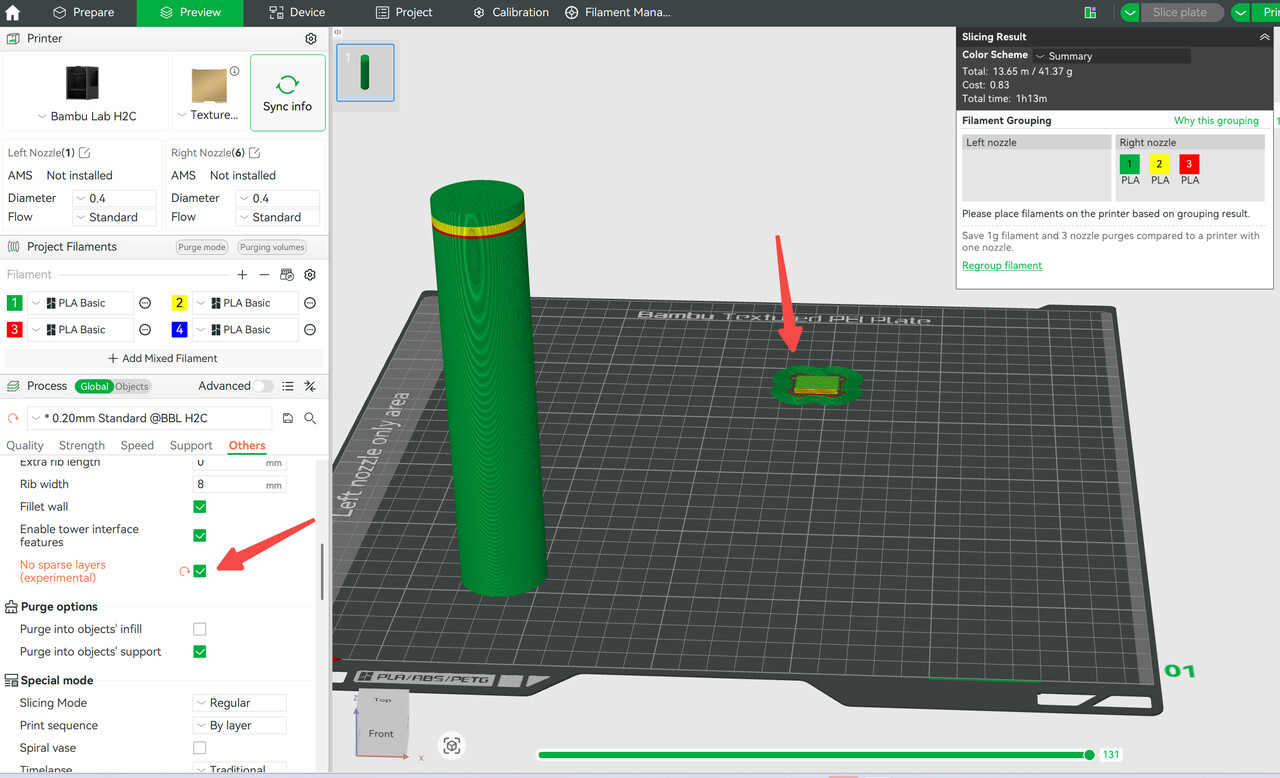
Stringing on prime towers introduces unnecessary risk in the print area. So many prints have failed due to the prime tower getting knocked over, It’s giving me Ender 3 vibes! Maybe it’s something else, yet I’d be OK with a little more extra purge waste if on every nozzle swap, the first few mm of filament is dumped out the poop chute before hitting the prime tower. It doesn’t have to be a lot.
Is there a G-Code instruction I could add to my prints to have it do that?
The prime tower is actually designed specifically to absorb problems with printing, which is why it doesn’t exactly look pretty. To put it very simply: If the tower looks bad, you know it’s doing its job - as I said, that’s a huge oversimplification.
I ended up utilizing the replacement plan for my H2D and swapped it out for a new one. Prime tower looking much better on the newer one. And I guess I am wrong about the purpose of prime towers and are a necessary evil. I guess something else is knocking the prime tower over
This totally checks out! Would that explain why the hairs get longer as the print progresses? Small prints are no problem. Anything over 400 layers at .2mm was at risk. Replacement unit is playing nice for now. Any recommendations on compensating for that over extrusion build-up? I’ll see what I can find in the mean-time
If you mean the nozzle starting to extrude in the air before hitting the tower, you can visualize the path in the slicing preview. I don’t know why they decided to make it doing that, I have no issues on the models
Where I am located there’s a really nasty heat wave happening upper 90’s to lower 100’s. The unit is in a garage with no air conditioning and no means to cool it down. Can’t have it inside the house either. Despite replacing the unit I began to have the same type of failure on the same model. I’m thinking that it’s just too dang hot.