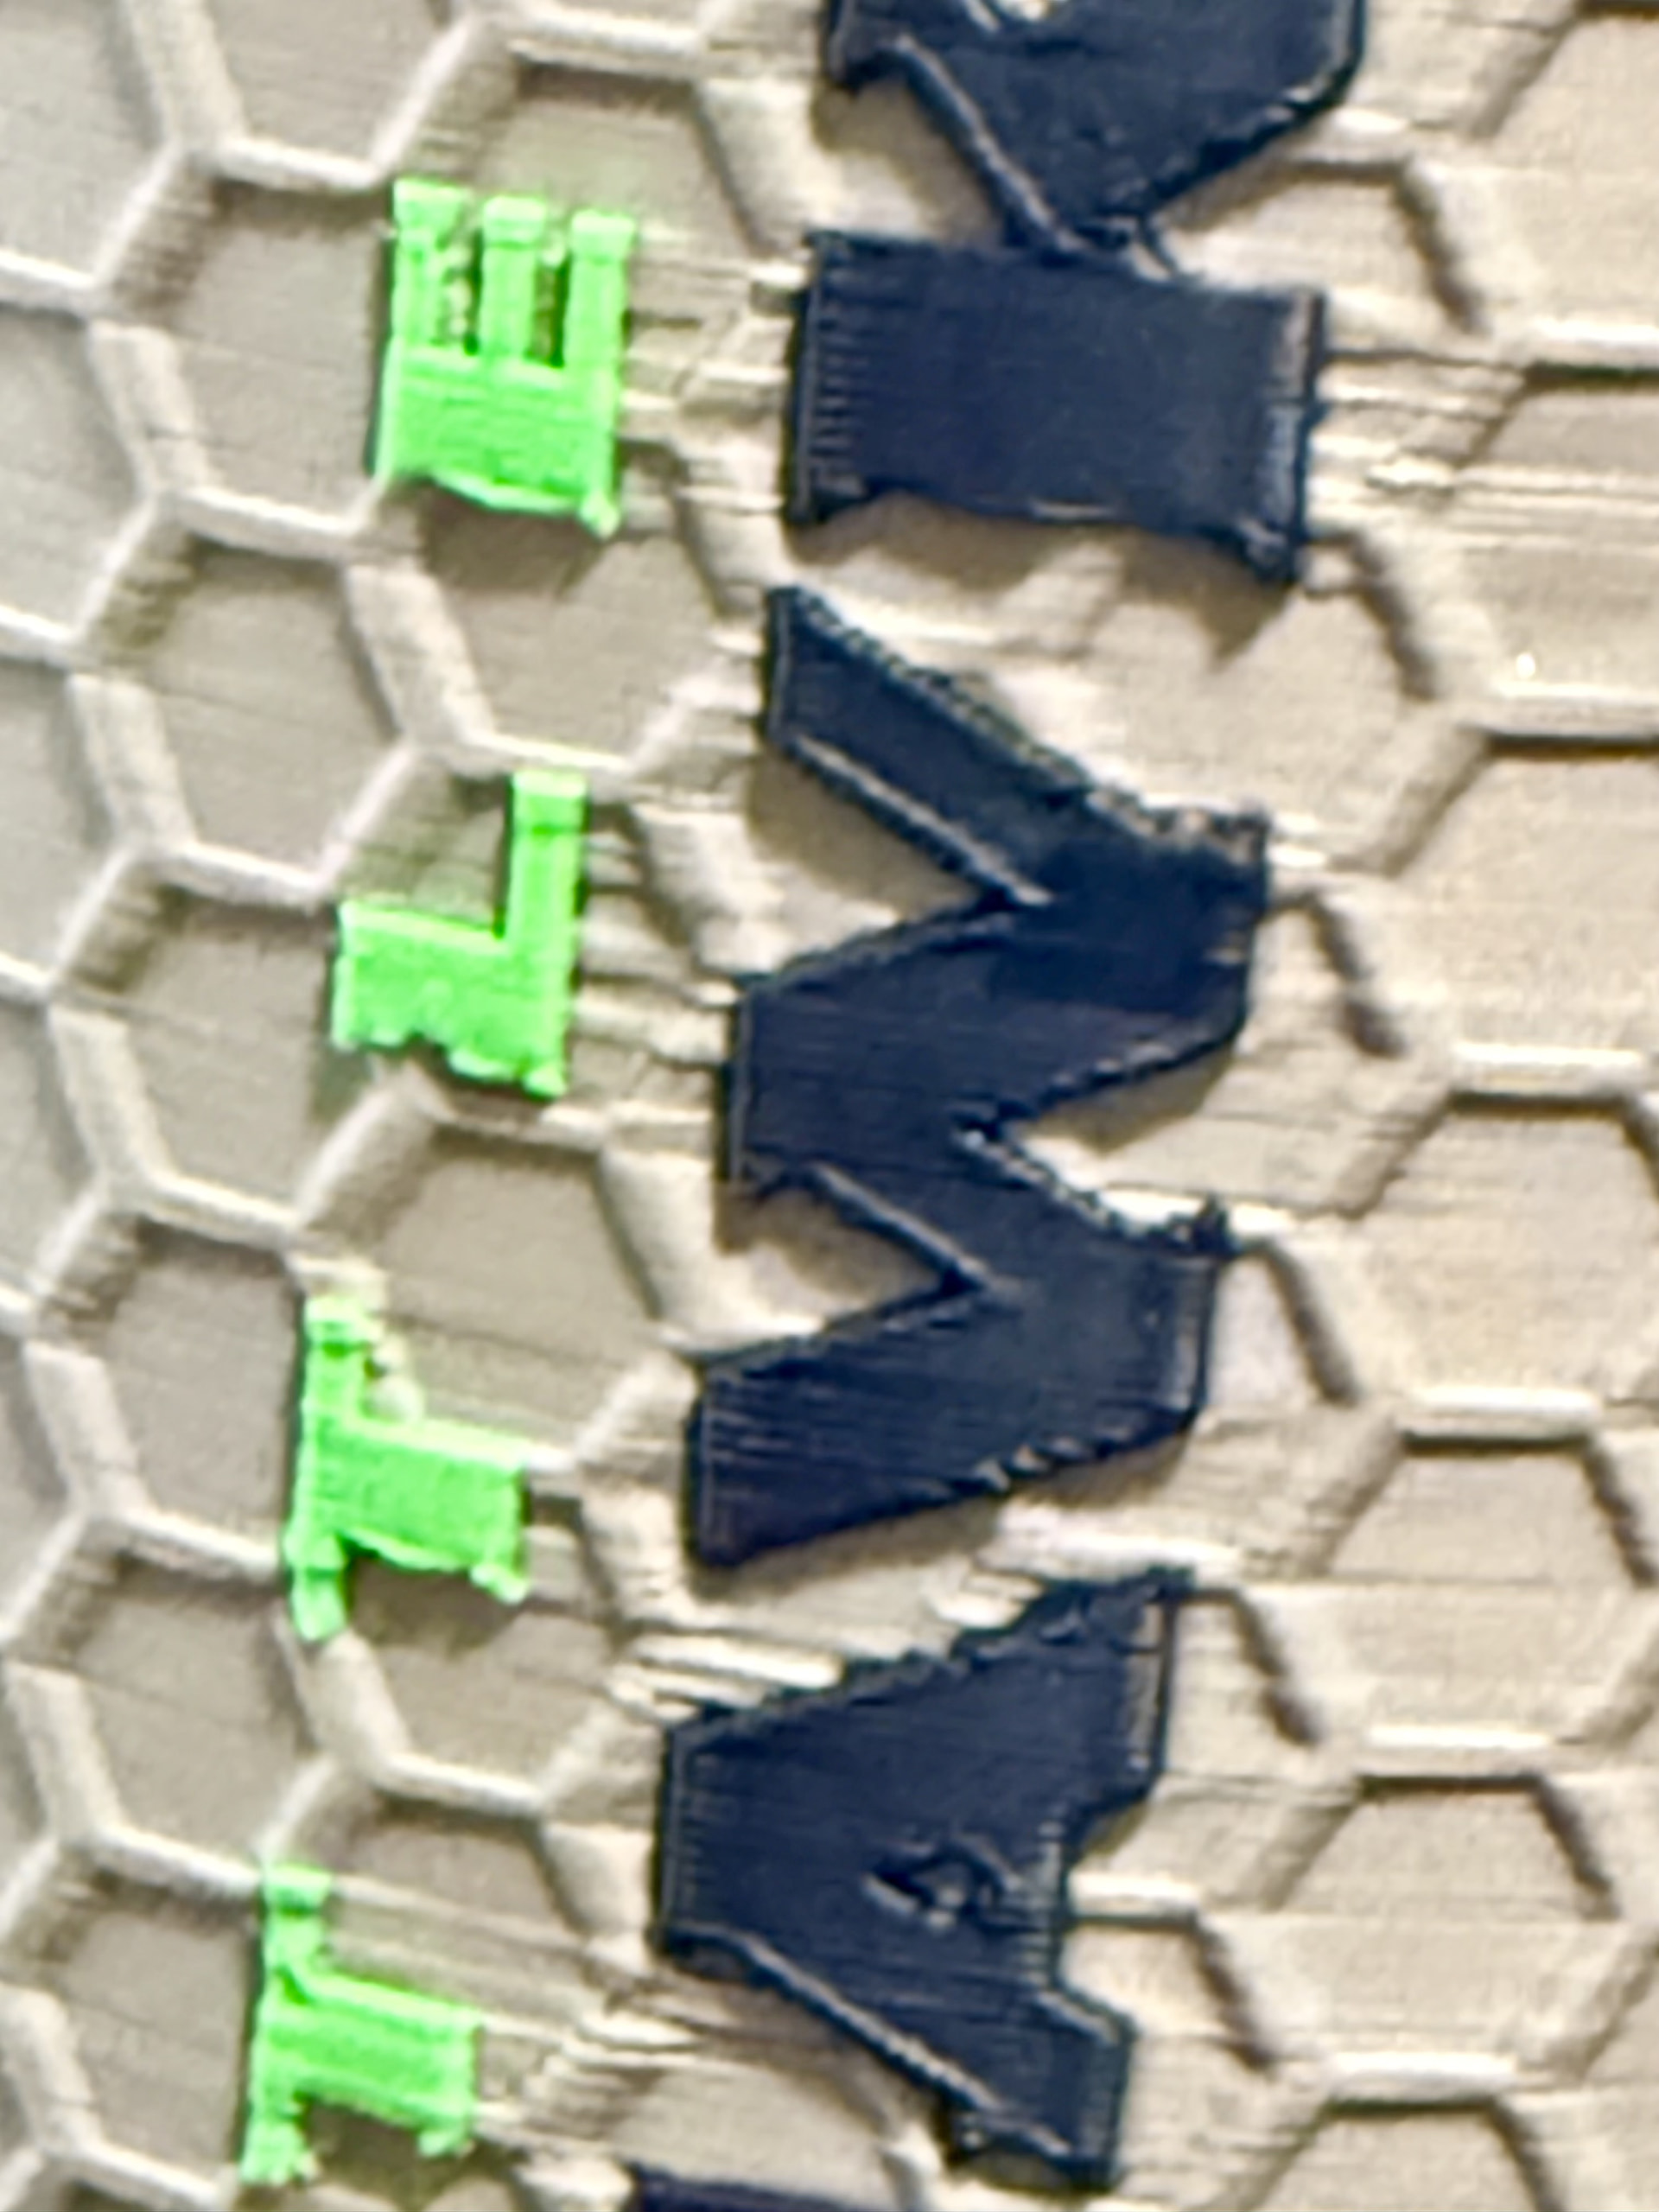
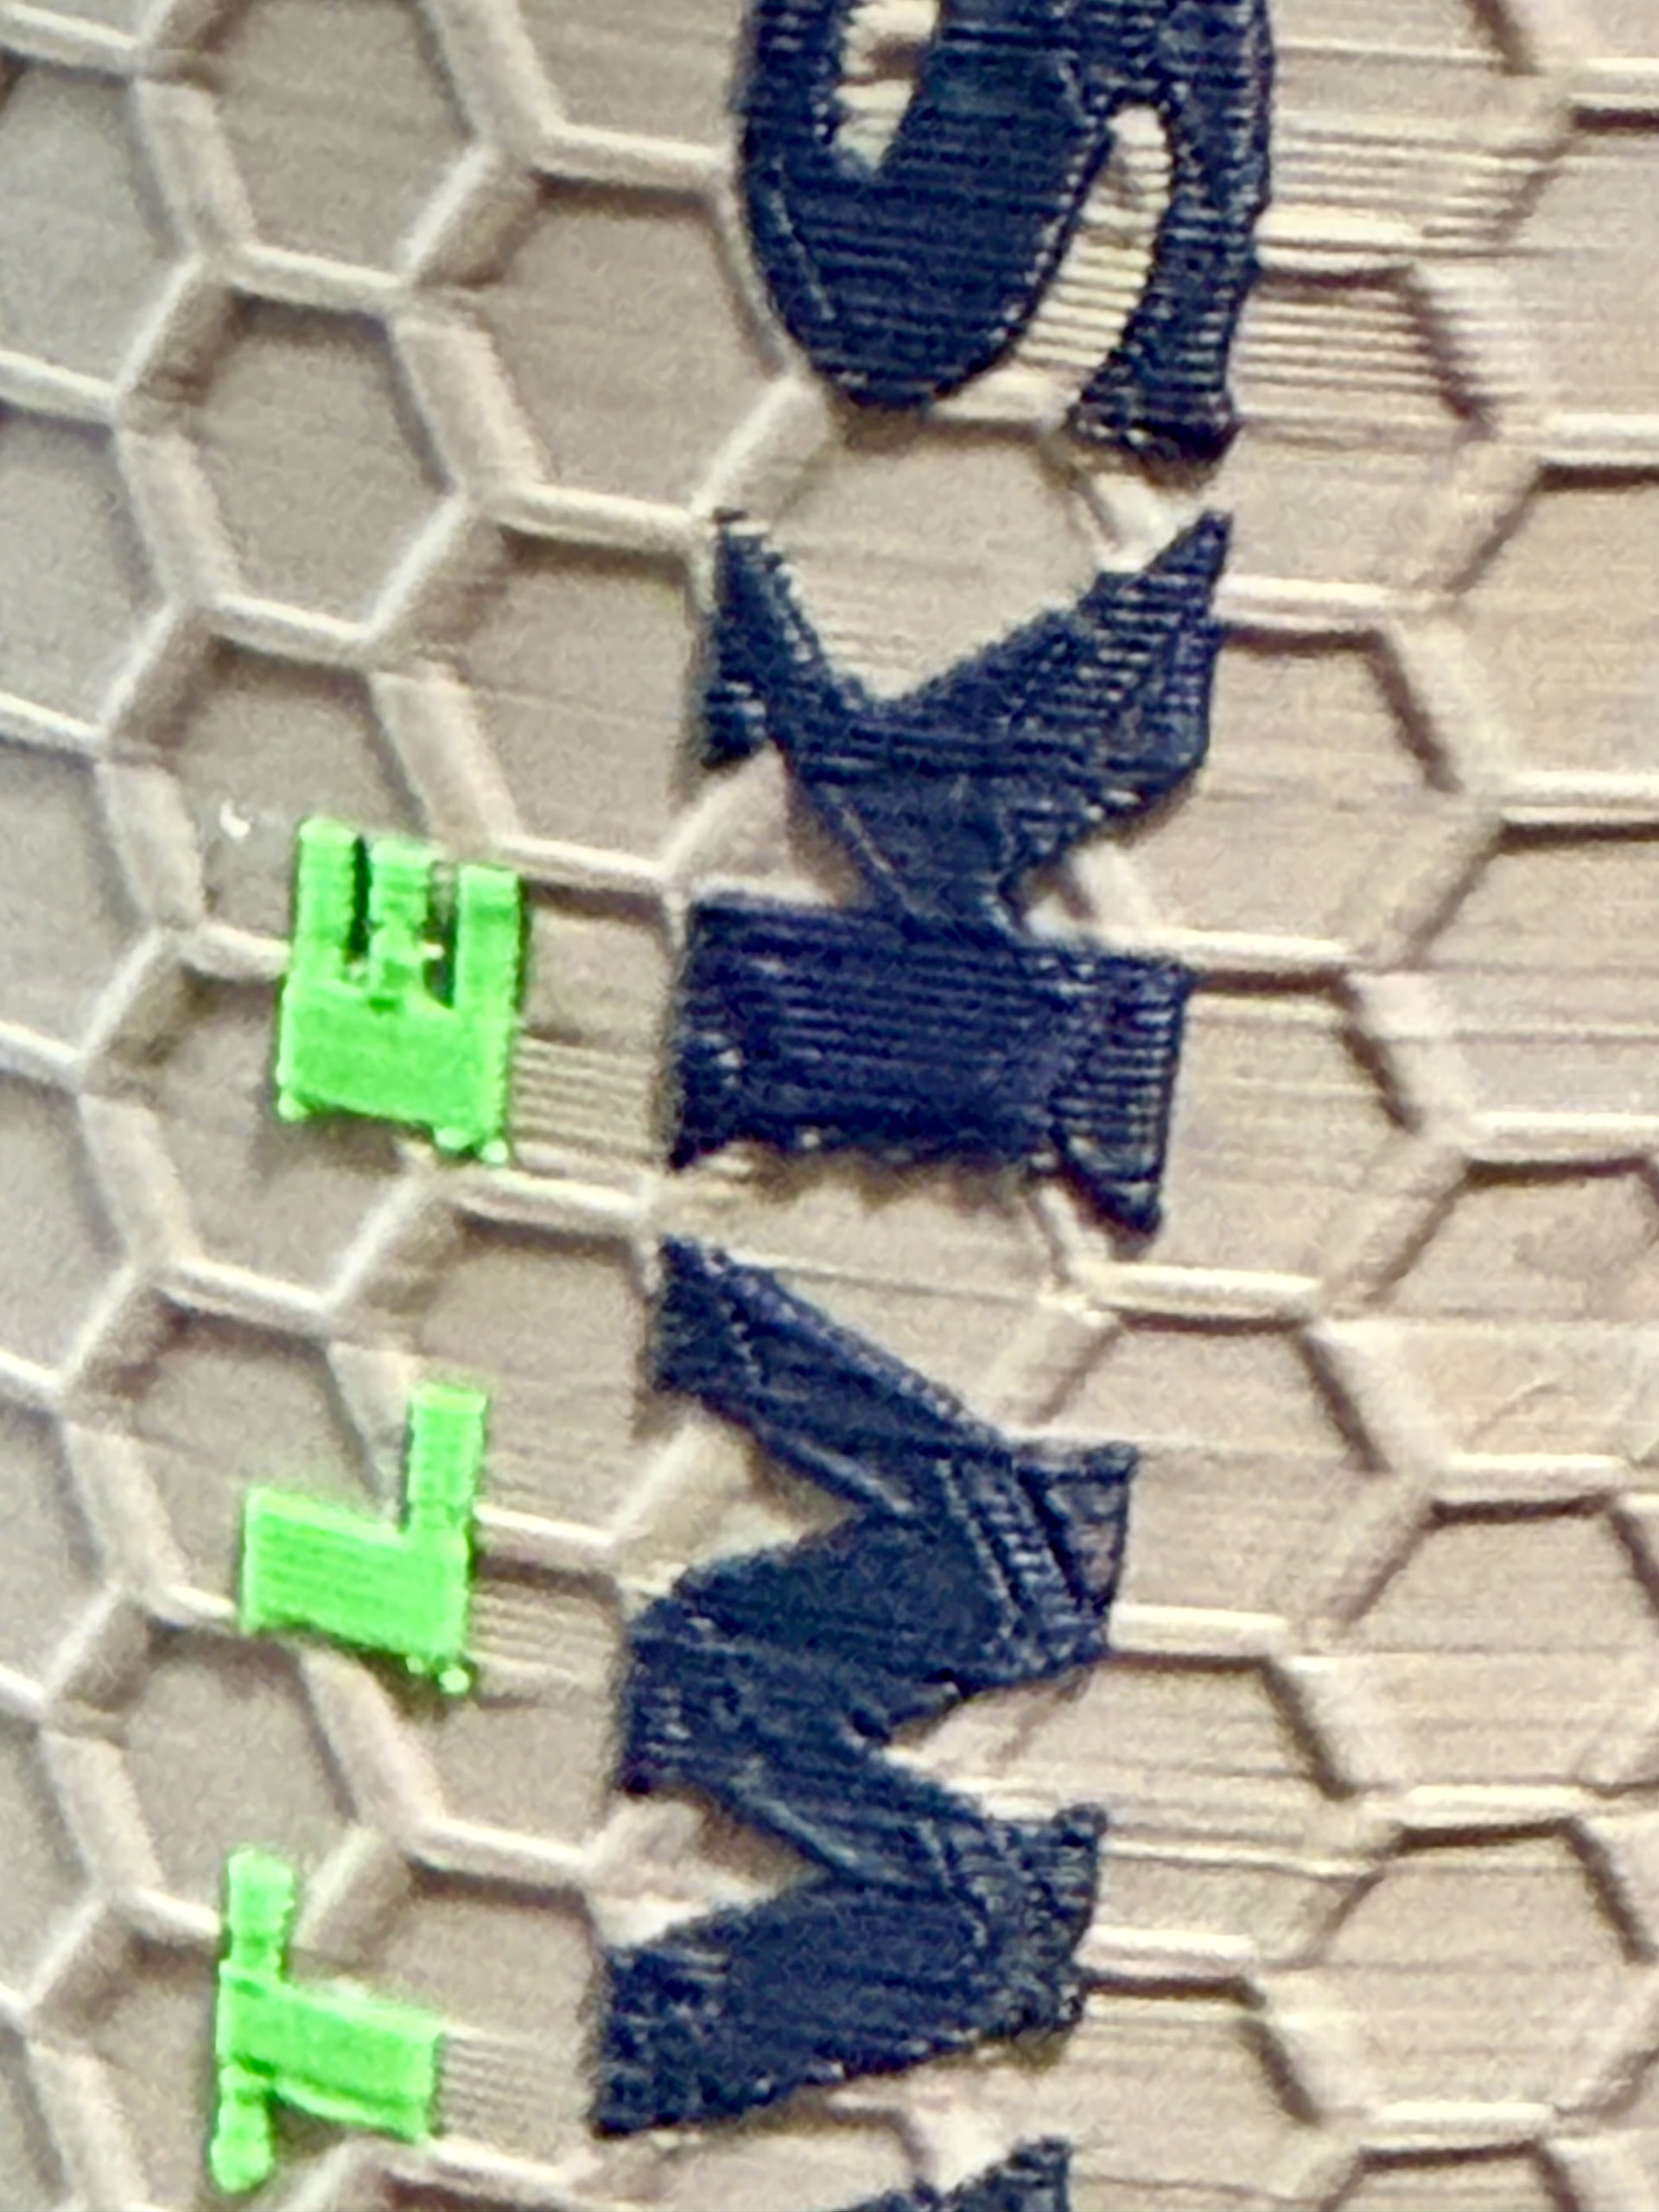
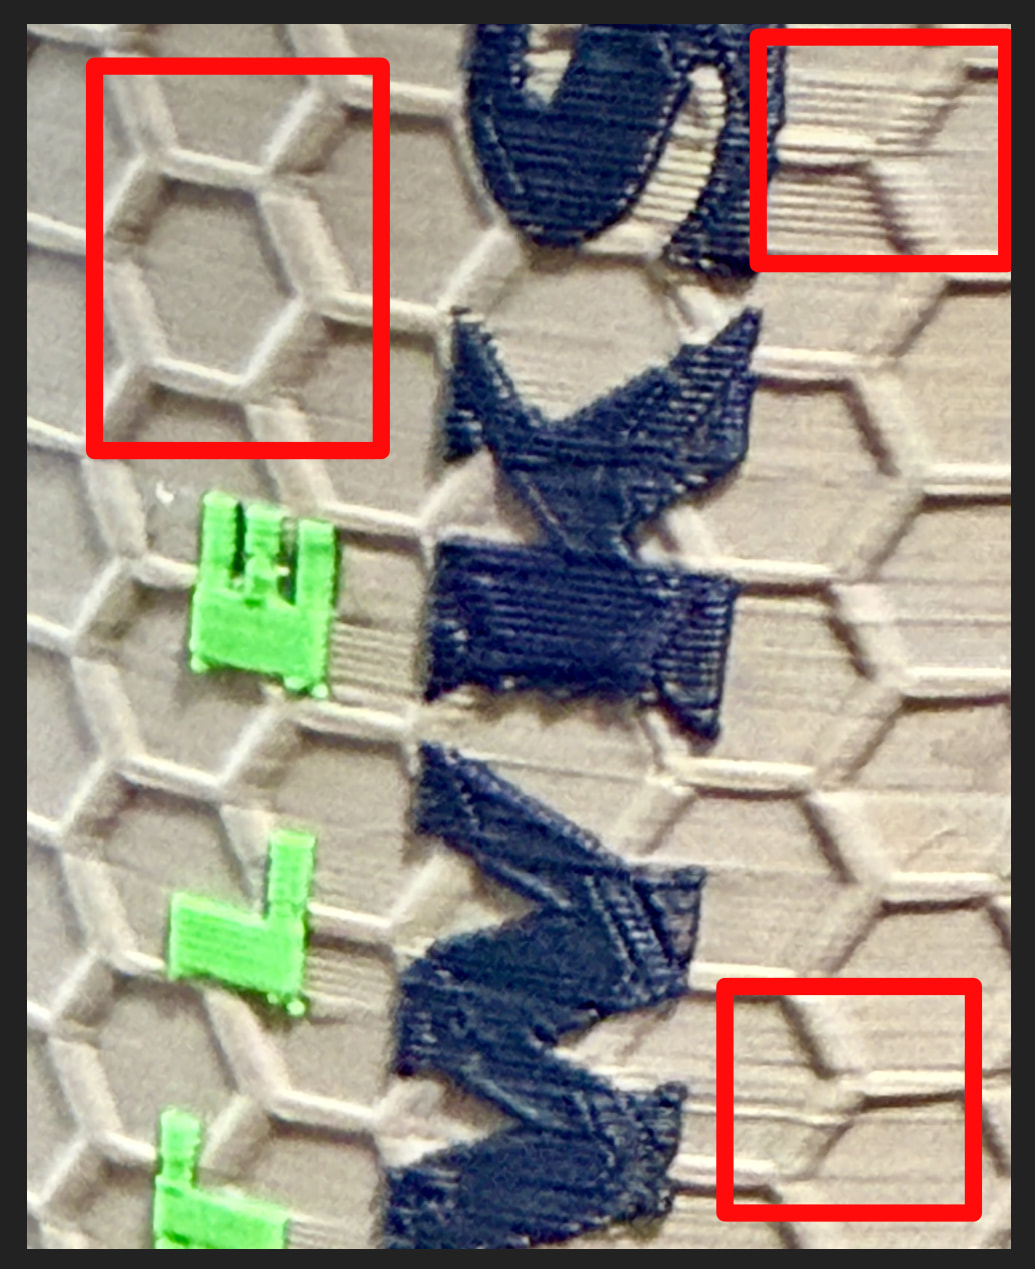
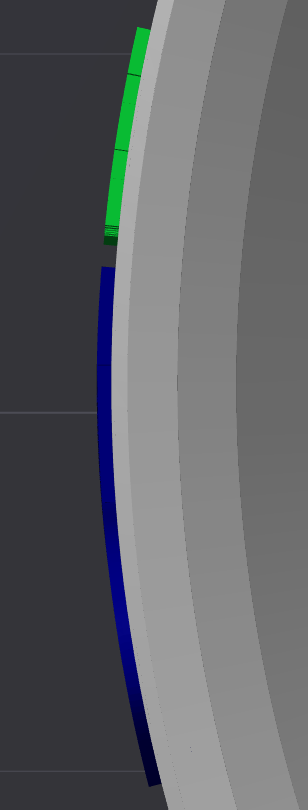
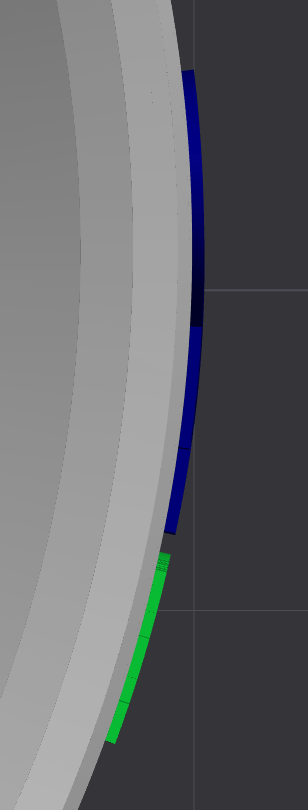
Hi all, I have an issue that is more of a frustration than a show-stopper for me. I’m trying to print a can Koozie with text embedded vertically on either side of the shell. The shell has a raised hex pattern that the text is “embedded” in. Here is how I set it up in Studio:
Created the text in Fusion (embossed on a cylinder, then used a negative extrude to remove the cylinder leaving the embossed text with the proper curve. Saved as STL.
Added the koozie shell and embossed text STLs to a new project in Bambu Studio.
Created a clone of the embossed text STL and flipped it vertically so that it’s curved side would fit against the opposite side of the shell.
Painted the text objects (green “Seattle” and navy blue “Seahawks”)
Centered both text STLs with the shell and then made an assembly with the shell and both text objects.
Positioned both text components vertically.
Moved each text component into the outside wall of the shell until the outside surface of the text was .01mm above the surface (no grey from the shell showing through the green and blue of the text) then moved them out another .3mm so the text would be raised on the outside of the shell. Both text components were positioned the same way. I can’t confirm that they were both precisely positioned the same on either side, but they looked very close. Unfortunately, I couldn’t get the measure tool to find good points or lines to measure.
So, then I sliced them and they both looked fine in Preview. When I printed them, the one on the near side (initially I positioned them with text facing front and back) looked as expected BUT the one on the far side printed almost flush with the shell, even printing the underlaying hex pattern in the blue and green letters. The surface of the text was raised above the surface of the hex pattern on both sides in Prepare and Preview, but when printed, the near one was fine but the back one was flush with the hex pattern and had the hex pattern in the text color.
I’ve been able to make this work by exporting the assembly as an STL, then printing that STL after re-coloring the letters. It’s a hassle, but it seems to work.
Any ideas why this is happening? What don’t I know?
When I look at your photo, it seems that there are several fundamental issues with your printer. There are quite a few errors and defects visible. To address this, it would be important to first ensure that your printer is functioning correctly.
Please consider servicing the printer, checking the screws and belt tension, cleaning the nozzle and extruder gear
Making sure the filament is dry
Calibrating both the printer and the filament.
From the photo, the entire print appears to be affected, so resolving these technical points should help significantly.
In a nutshell: I doubt your printer is even capable of printing anything properly in its current condition. The problem you’re describing is just a side effect, not the cause.
lol. Yeah, it prints really well. Those photos are of hex cells that are about 5mm wide, so you’re looking pretty closely at it. Also, it was a .2mm layer height using the normal settings and printing in Sport mode. Not the best quality, but I’ve been chasing this issue for a while.
I appreciate you pointing out the flaws in the print. Any suggestions that address the problem I asked about?
I’m using an H2C. Should have mentioned it in the original post. Also, I’m using Elegoo (navy blue) and Isanmate (grey and green) matte PLA. Filament is dry and the profiles are reasonably well calibrated. The issue is really about the external lines being flush on one side and proud (as desired) on the other side of the model. Very weird.
Even weirder is that the blue and green are showing the hex pattern, but that pattern isn’t under the blue and green I could understand it if the colors were being printed around the pattern, but they aren’t The blue and green are following the pattern of the surrounding grey. SO weird!
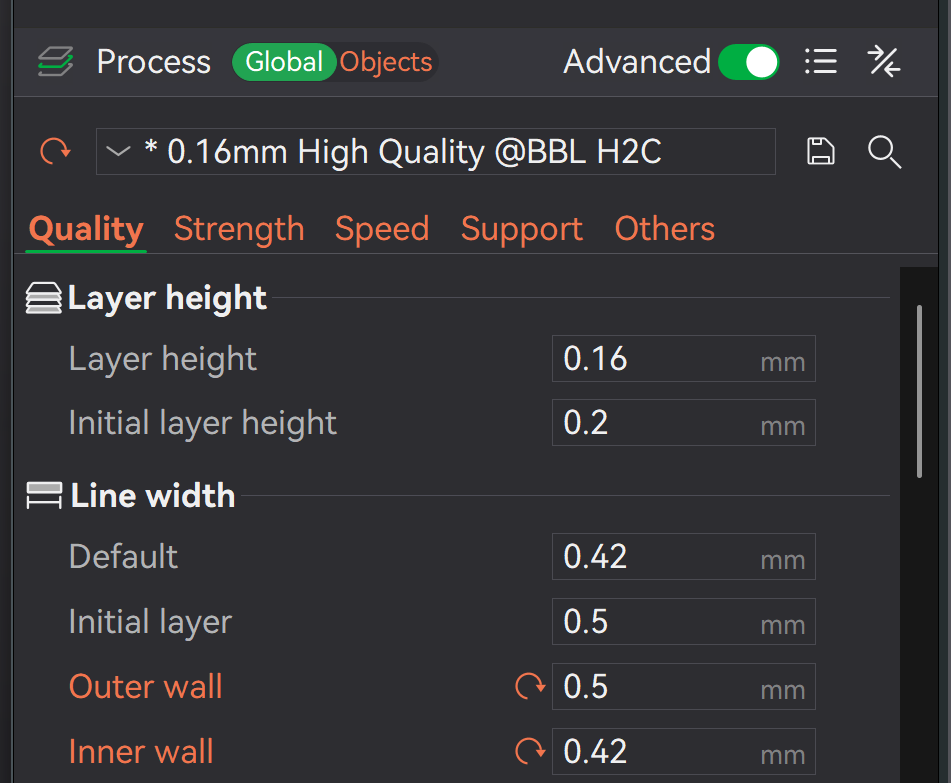
I’m wondering if it is a tricky math kind of issue? My external wall line is set to .5mm to help with overhangs while other walls are set to .42mm. I set the strength to 3 walls, could the software compensating because the line widths don’t allow for three walls within the geometry of the model?
I’ll post the file in a few minutes if anyone cares to take a look.
Here’s the .3MF file I’m printing. My sample that I took pics of was done at .2mm layer height, but the model is intended to be printed at .16mm. In case anyone wonders…
So, first of all: the text isn’t aligned on the left and right. It sticks out from the cup by different amounts, and the spacing around the curve isn’t consistent either.
In other words, we’re dealing with the problem that the two sides simply aren’t the same. I don’t mean the text is mirrored - the spacing and rotation are just different.
How exactly did you position the text?
On top of that, you changed a huge number of parameters - both global and object‑specific - and some of them even contradict each other.
Then you mixed different filaments from different manufacturers, which is something you really shouldn’t do at all.
And finally, I’m getting a G‑code warning saying that something was modified.
To put it simply: I’m sorry, but for the first time in a long while I have to say no. There are far too many variables changed for me to make any sense of this 3mf file.
OK, I’d really like to know what you’re seeing, so I can fix the issue, but you aren’t providing any specific information.
Not sure why it isn’t lined up right when you open it. I’ve attached a screen shots showing what I’m looking at. If they aren’t lined up correctly, then it is off by hundredths of a mm, if that. I can’t use the measure tool because the tool won’t catch edges close enough to provide a reliable measure, so I can’t provide precise offsets, but they are very close.
When you say I changed a huge number of parameters, and that the object settings contradict the global settings, can you tell me what the issues are. Essentially I modified the stock Bambu profile, I just didn’t create a custom one. Is there a parameter that might affect how the print turns out? The issue I’m having is that one side of the print is not matching what I see after slicing in Preview. The print doesn’t seem to match the software. What is it that you saw that could be an issue?
As far as contradicting… AFAIK, object settings will take priority over global settings if there is a difference. There shouldn’t be a contradiction. The slicer goes with global settings unless there’s a difference in the object settings, and then it uses those settings. Is that not how it works?
I don’t agree about using filament from different manufacturers, but that has nothing to do with my issue.
What is the gcode warning you get about something modified? I’ve never seen anything like that. You opened it in your slicer which is set up for your machine I presume. What is the message?
Look, I’d really want to help you - but this goes far beyond basic troubleshooting. You’re not starting at step one - or even step ten. Instead, you’re focusing on a single issue that only appears around step one hundred: the logo.
Right now, you’re trying to build a skyscraper on sand. The foundation isn’t stable, the structure is already sinking, and you’re wondering why the logo at the top isn’t straight.
Alright, let’s put that topic aside for now. However, when I look at the filament profiles, they don’t match the manufacturer’s specifications. You need to set up the filament profiles correctly first so you can rule out this possibility during troubleshooting.
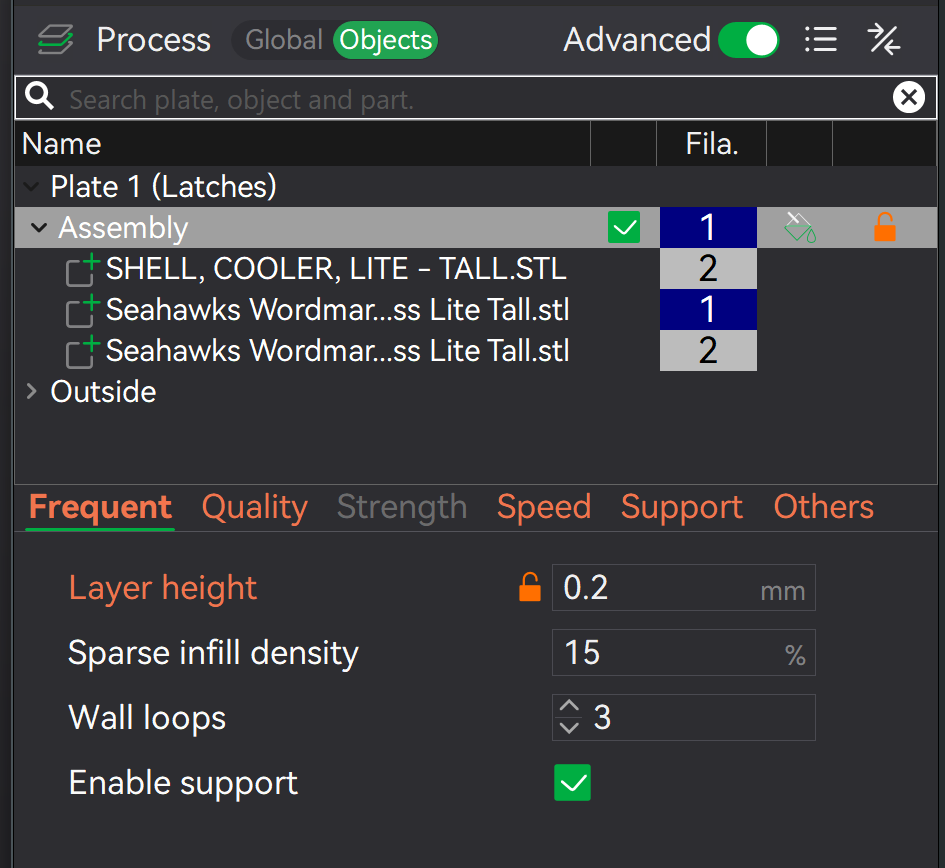
Here you’ve changed global variables - in the first image - and in the second image you’ve changed object variables as well. Why? That doesn’t make any sense at all.
You’re asking the community to tell you which checkboxes you need to click to fix the error. Maybe there’s actually a way to do that - in which case, you’ve been lucky enough to find a needle in a haystack.
However, instead of looking for a needle in a haystack, you can simply avoid the haystack altogether.
Here’s my suggestion:
Dry the filament, calibrate it, and create the correct filament profile.
I know you don’t do that anyway, but use filament from a single manufacturer - filaments from different manufacturers have different flow rates.
Reset print profile to default and use any a high-quality profile. You may also want to adjust the support settings, but leave most settings at their defaults.
Rotate the object, for example, by 90°, then print it out and see if the fault moves or stays in the same place. Does the flaw move along with the text, or does it stay on one side?
Then at least you’d know whether it’s a settings issue or a problem with the printer itself - like a fan blowing like crazy from one side. Theoretically, it could be a fan radiating precisely onto that side. Maybe it’s the needle you’re looking for.
@RetroSharky Ok, I’m going to let this one go. You’ve comments are vague and the issues you point out aren’t really issues… The global and object settings don’t match because the original file I use has about 30 pieces on it, with different layer heights, support settings, etc. because I want all of the project in one file. I print them individually as needed. I extracted the single cup for simplicity when I sent it to the group, so it retained the global settings from the original project plus the object settings for the cup. The differences you see don’t matter anyway as I said before, there is NO conflict between settings. When there’s a difference between global and object settings, the slicer prioritizes object settings. Those are the settings that matter in this case. Not an issue. The reason I asked about this is because I observed something in the final print that was not shown in the Preview of the slicer and I was hoping someone had some insight into the issue I mentioned. It is a difference between one side of a print and the other when both sides are pretty much identical. If your comments had pointed me toward things I could try to get different results, then that would be great. But, you seem to have gotten tripped up on a bunch of settings and instead of asking why, you assume I’ve screwed up the model from the start and there’s no point in helping trouble-shoot the issue I actually asked about. So, I’m going to move on. I’ll figure it out eventually.
No problem at all - I only offered to help because I genuinely wanted to support you. You’re never obligated to accept it; it’s always completely optional. I just saw that your post hadn’t received many replies, and I tried to guide your complex issue in a direction that might lead to a solution.
I do all of this in my free time, and your problem actually kept me busy for a few hours. I’m not a Bambu employee, I’m not paid for this, and I don’t earn any points or rewards. I simply enjoy helping when I can. Analyzing your 3mf is just a bit more complex than telling someone to clean their print plate.
I truly wish you the best of luck in solving your issue, and it would be great if you could share the solution here afterward so others can benefit from it too.