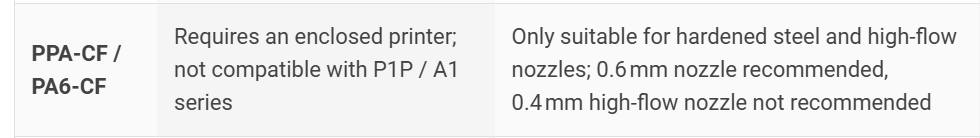
Greetings! I’m fairly new to the forum and this is my first post. I’m looking for some help with selecting a nozzle for some very small, complex geometry. This will be a part nest used in a piece of production equipment and was considering using PA6-CF. According to the Wiki (image below) it does not say specifically that a 0.4 Hardened or even 0.2 hardened nozzle will not work, only that a 0.6 is recommended. Will the carbon fiber fill plug up a smaller nozzle and give me more headache than it’s worth? I’ve had the PA6-CF for months but have not yet even opened and dried it in preparation to test. Thanks for any advice!
Depends on the brand. Some have more fiber and really need the larger nozzle. I am assuming you are talking about the Bambu stuff.
A 0.4 hardened is fine. Some brands like fiberon perform better with a 0.6.
0.2 nozzles will get clogged right away.
Never use a high flow nozzle. They clog very easily because of the passages meant to heat filament faster.
Nylon needs to be dried real good. So do that before anything. About 8 hours at 85c should do it.
A 0.2mm nozzle? I would say almost certainly.
I run all my CF filaments with 0.4mm nozzles regularly (PETG, PLA, PA, PET, PPA) and the only clog I ever had was self inflicted - I didn’t immediately purge the PPA-CF out of my 0.4 ObXidian and it annealed itself in the nozzle.
You should only use 0.6 or 0.8 non-HF hardened nozzles with PA6-CF. You can use 0.4 but you risk the chance of a clog. Also, PA6-CF is used for functional parts where the increased detail you get from 0.4 vs 0.6 is negligible.
What printer are you using?
Also, not sure if you know this but PA6 is very hygroscopic. You need to dry it at 80°+ for 6-8hrs and print it while it is drying if the print is longer than a couple of hours. When done the filament needs to be stored in a dry box.
Thank you all for your input and help!
@CincinnatiDesigns I have Bambulab filament, and an AMS HT so drying should be adequate.
@CarbonForge I’m happy to hear that you’ve had success with 0.4 nozzles and CF material. The assembly that I need to locate is only about 1" x 3/4" x 3/4", and we need to have it accurate enough to slid in pins with about .012" clearance to the bores. My test with 0.2 mm nozzle and PETG-HF made a reasonable nest but we know it will not stand up to insertion/removal every 30 seconds over an 8 hour shift.
@hyiger I’ve got an H2D. I will heed your warning about the 0.4 mm nozzle but feel like I should give it a go. Or maybe, print with the 0.6 mm and see if it’s accurate enough? I do like avoiding problems…
Do not use a 0.2mm nozzle IMO for any filament with “stuff in it”, its asking for trouble. Over the past couple years as the industry has circled around 0.4mm as standard, filament mfrs have been targeting that as the particulate size they grind the stuff up into so that it is more guaranteed to clear the extruder.
You may want to look at the IGUS brand of filaments, they make some very tough formulations for high wear applications including some that are self lubricating.
Then again, depending on the speed, loading, surface finish of the pin, and environmental conditions nylon may be fine.
Best of luck!
Thank you @Bullocks, that is helpful insight. And @CarbonForge I am a big fan of Igus products and have been designing with them for literally decades. I knew that they had offered custom parts but didn’t realize that their filaments could be purchased and used in my own printer! That opens up a world of design possibilities.
Awesome! Talk to your rep, they have little sample packs of their filaments, I’m sure they’d send you a bunch if you ask!