Hi there!
Fairly new user here, around 200 hours in printing (a few hours of printing other things with success, as well printing with PLA with success).
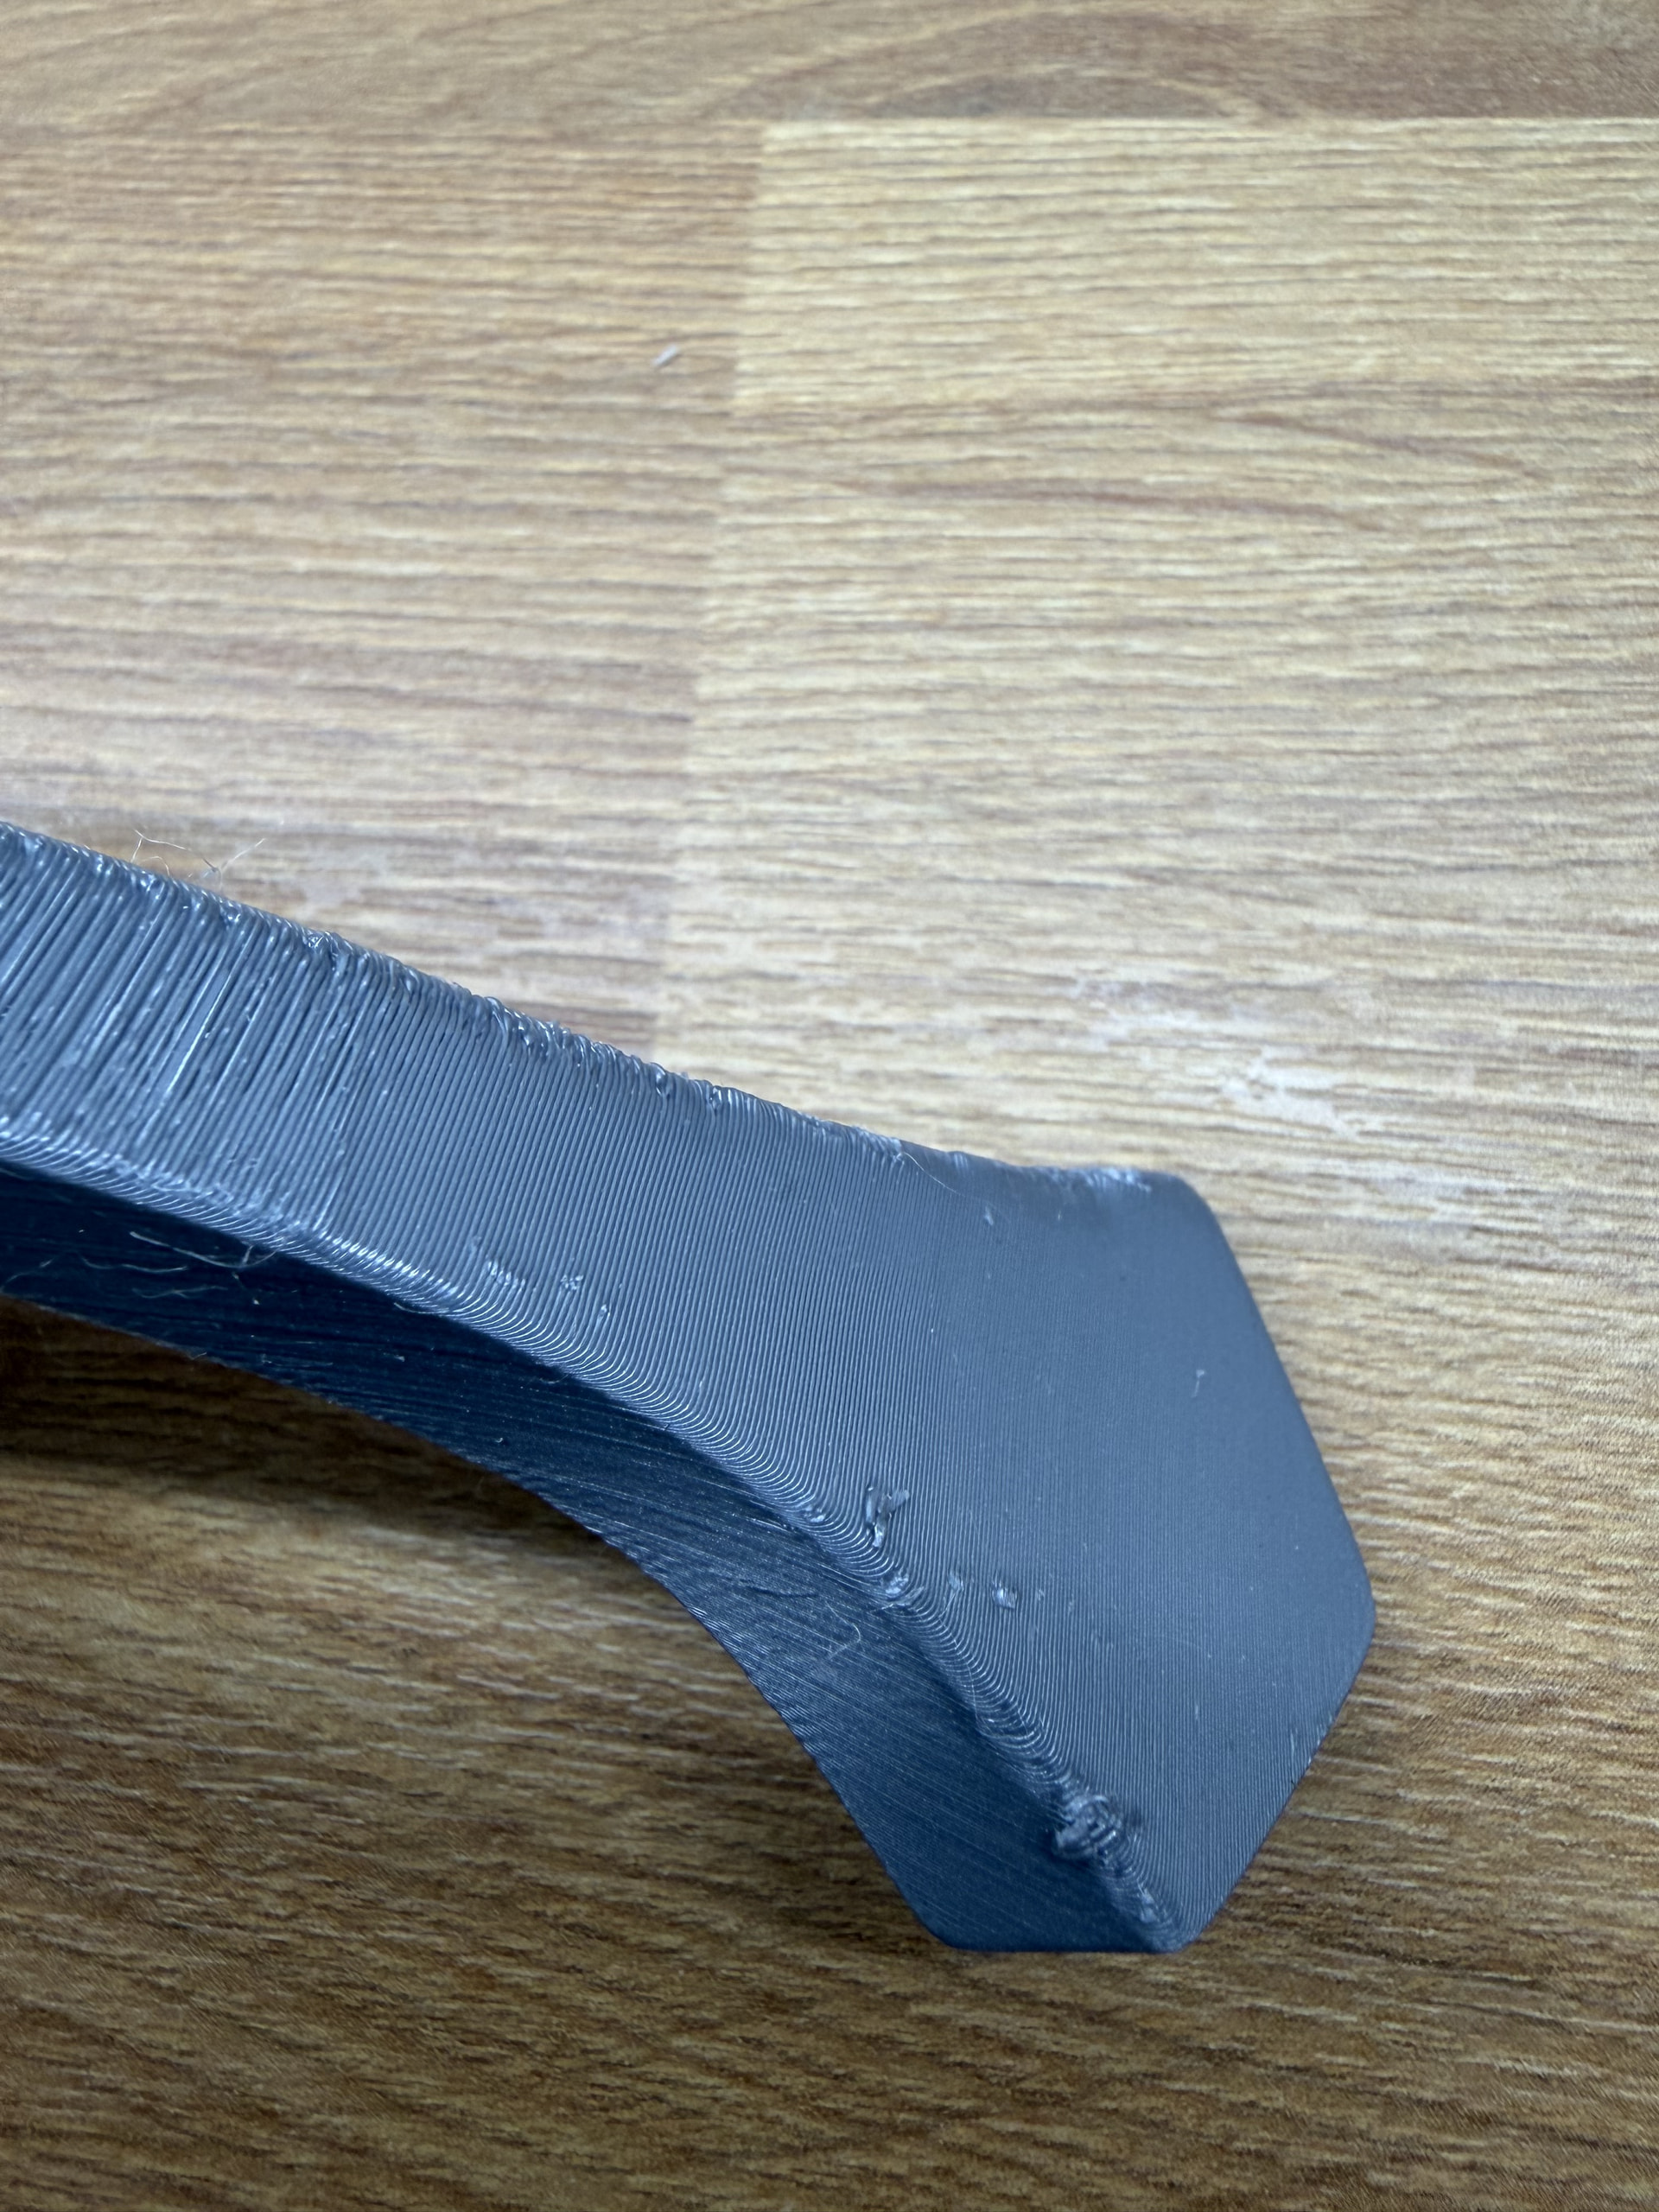
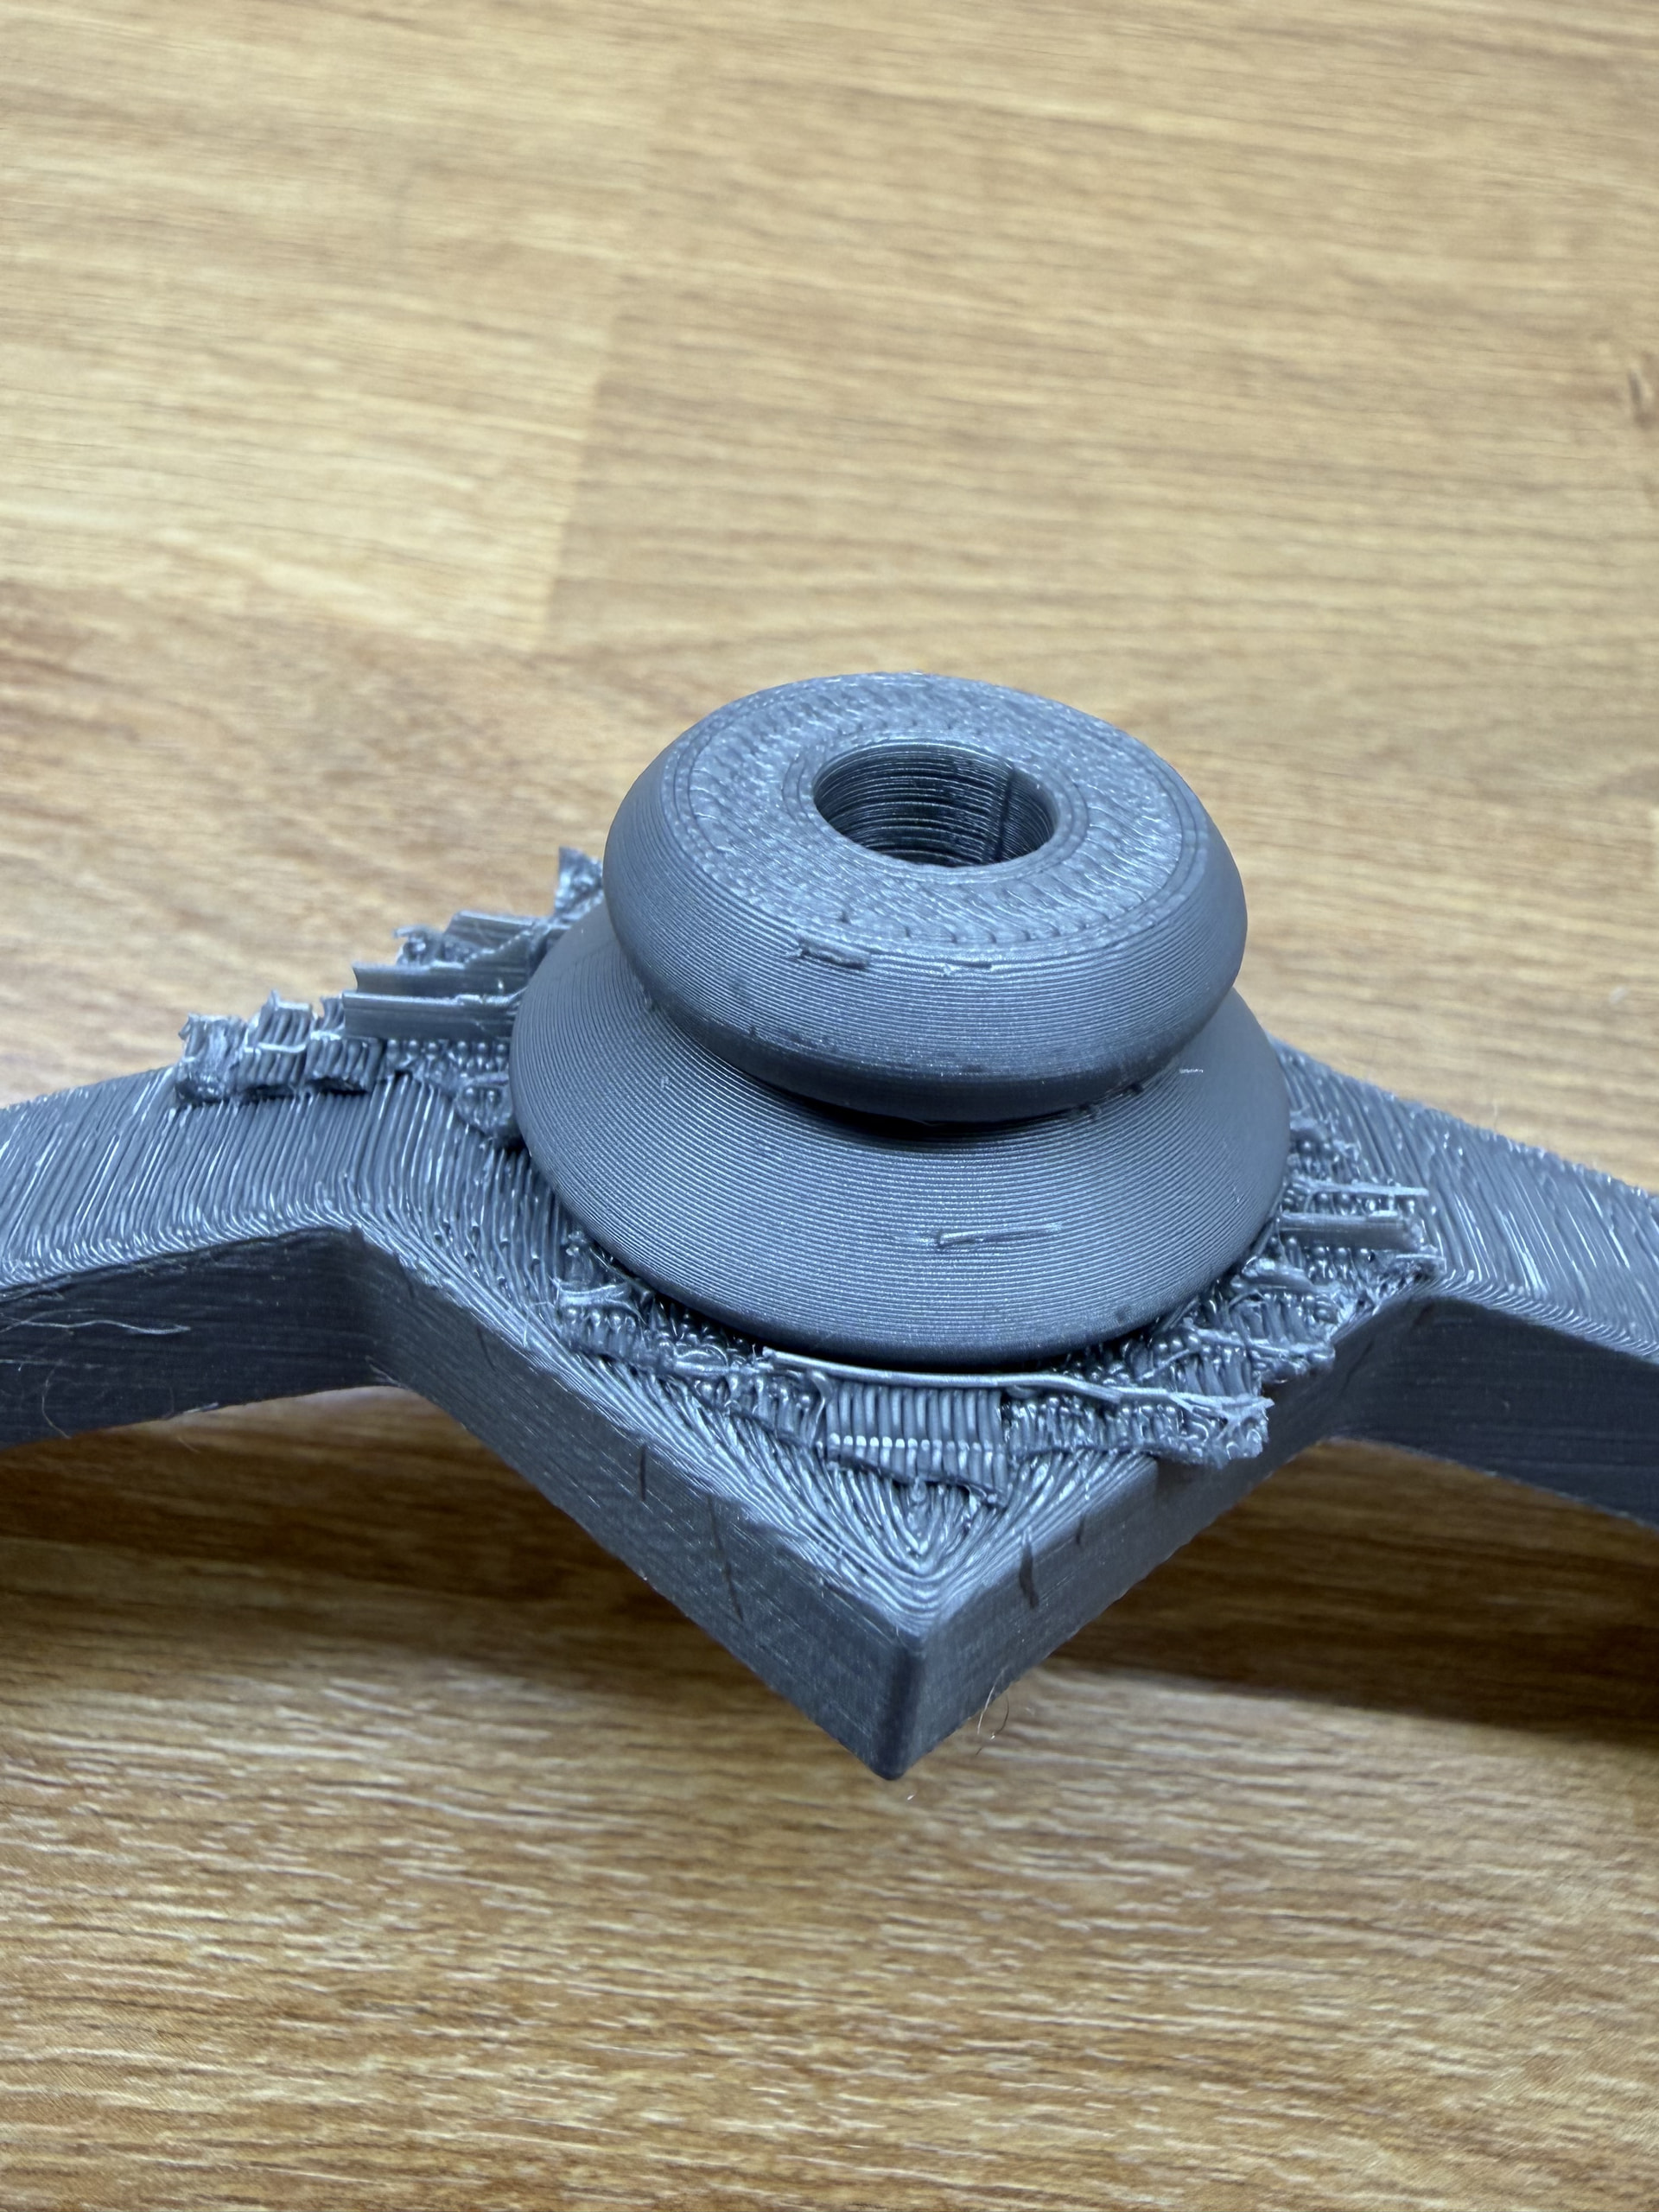
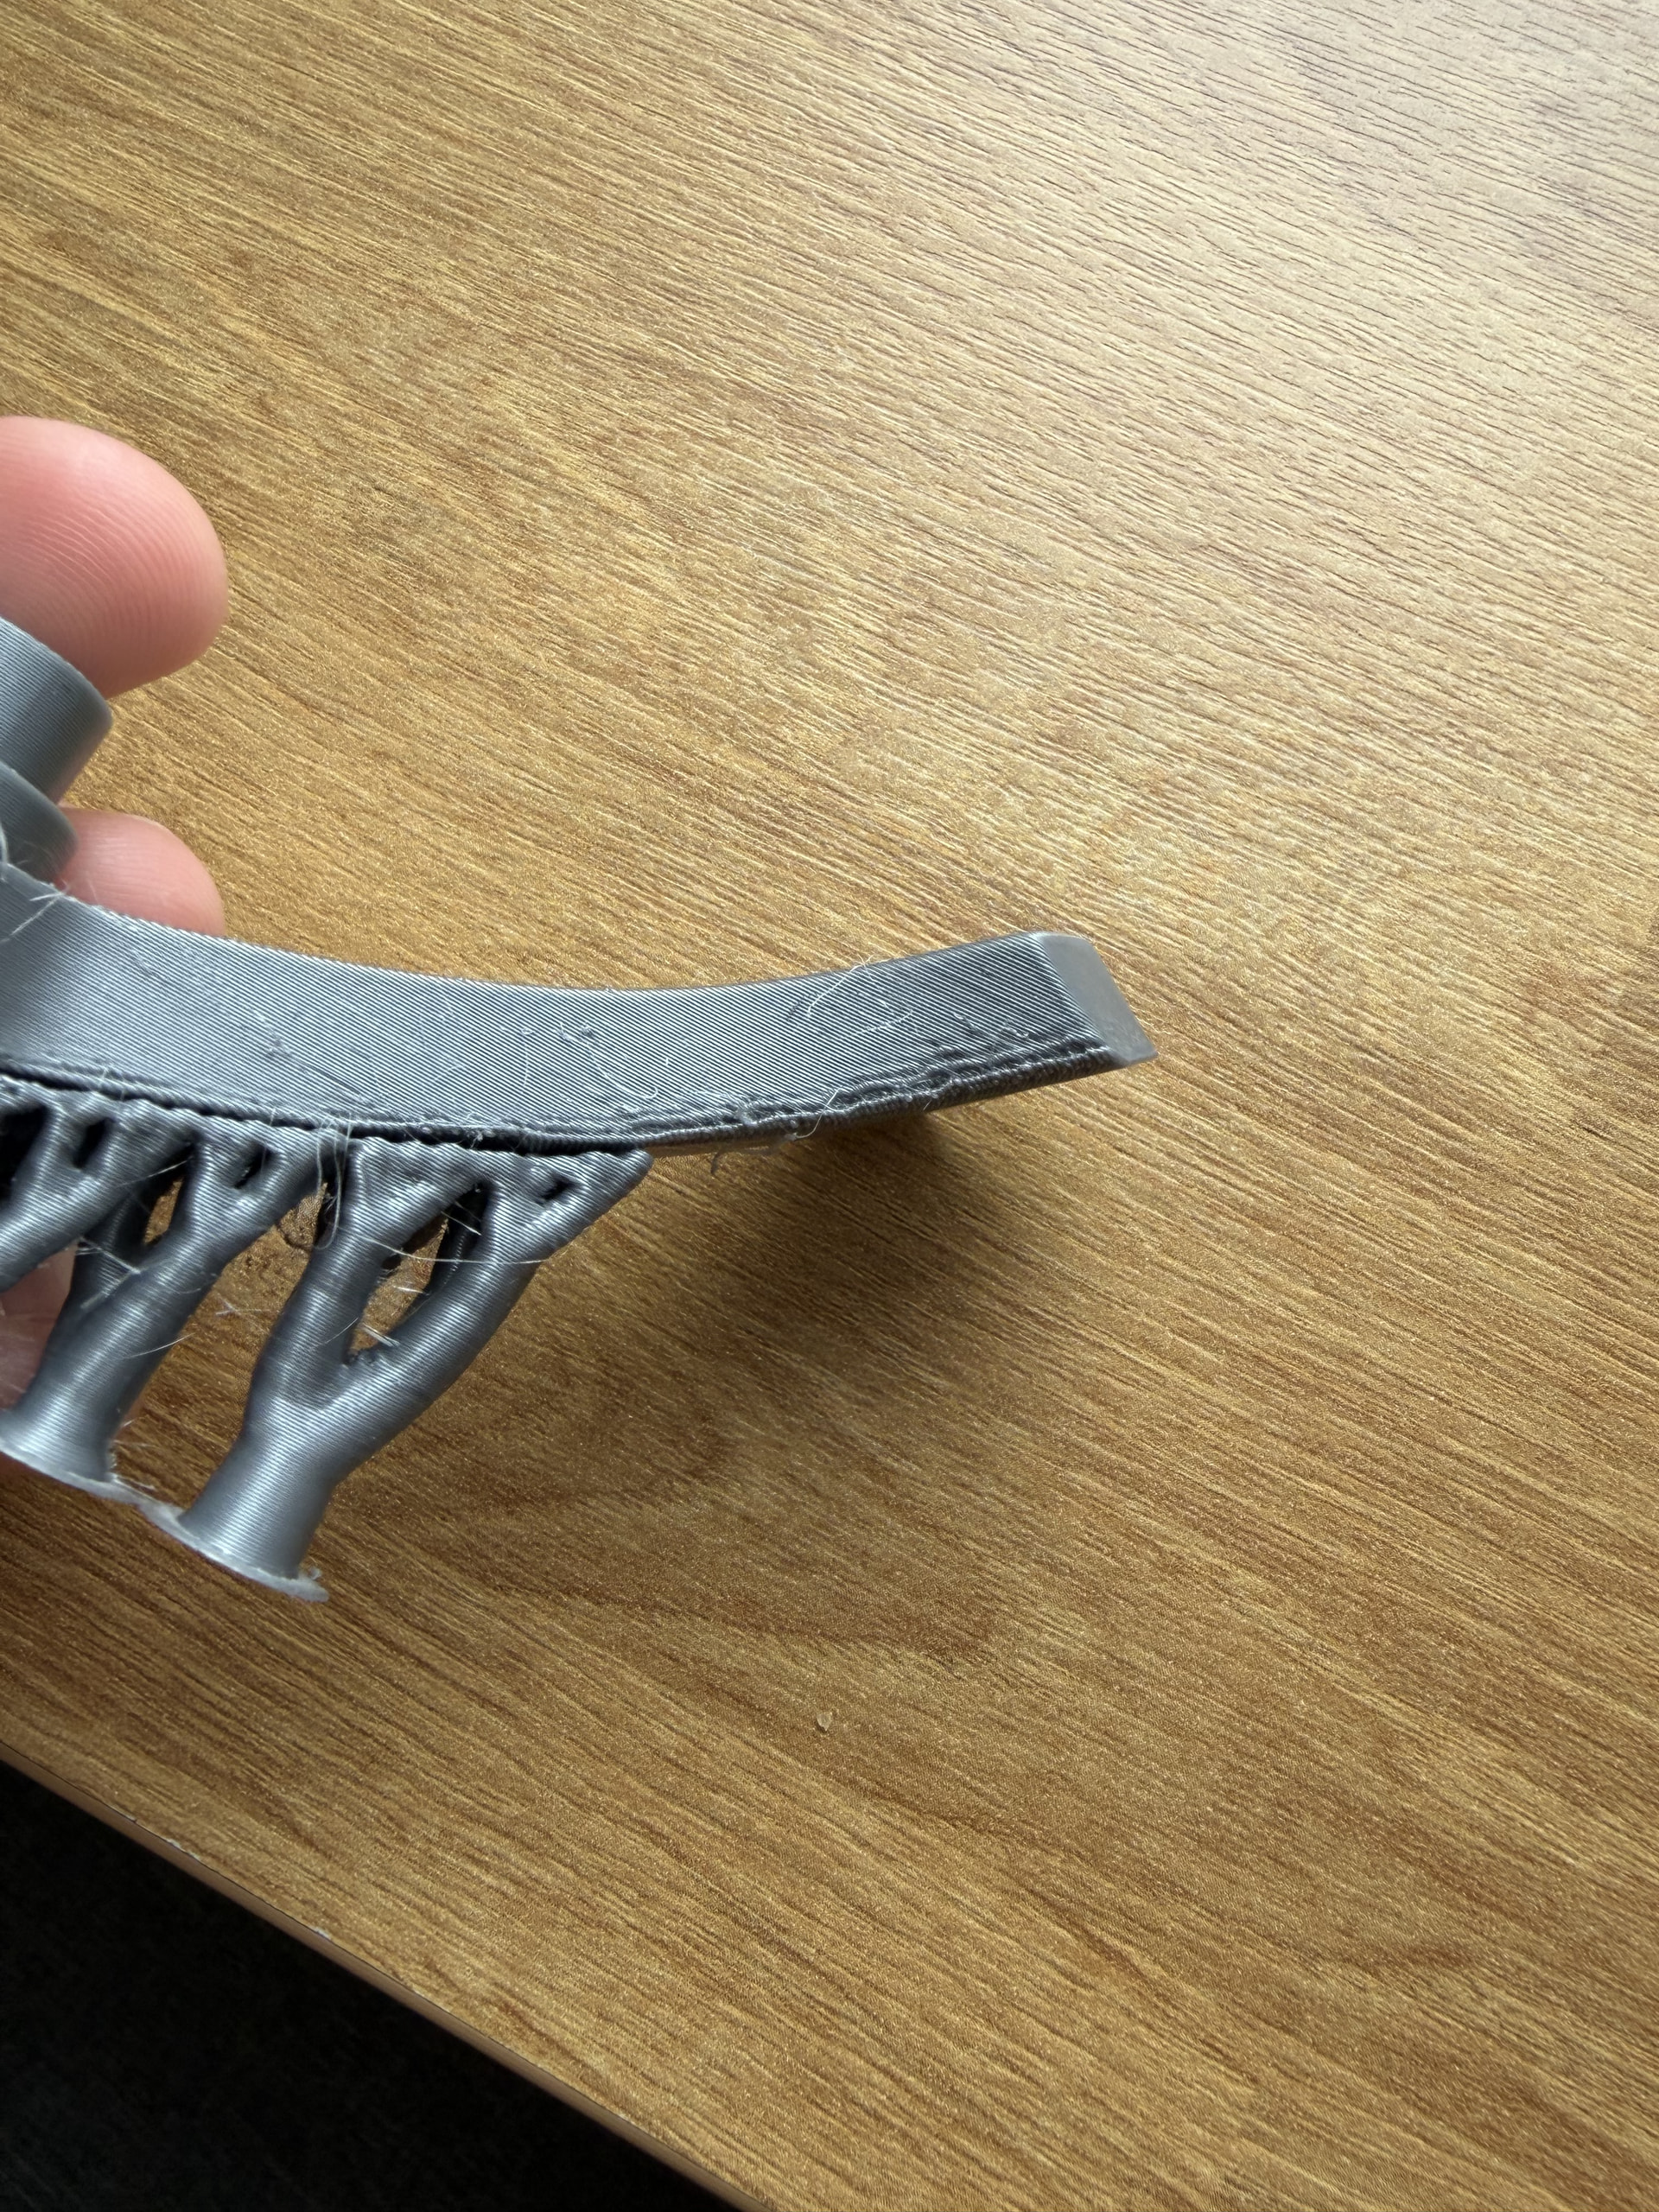
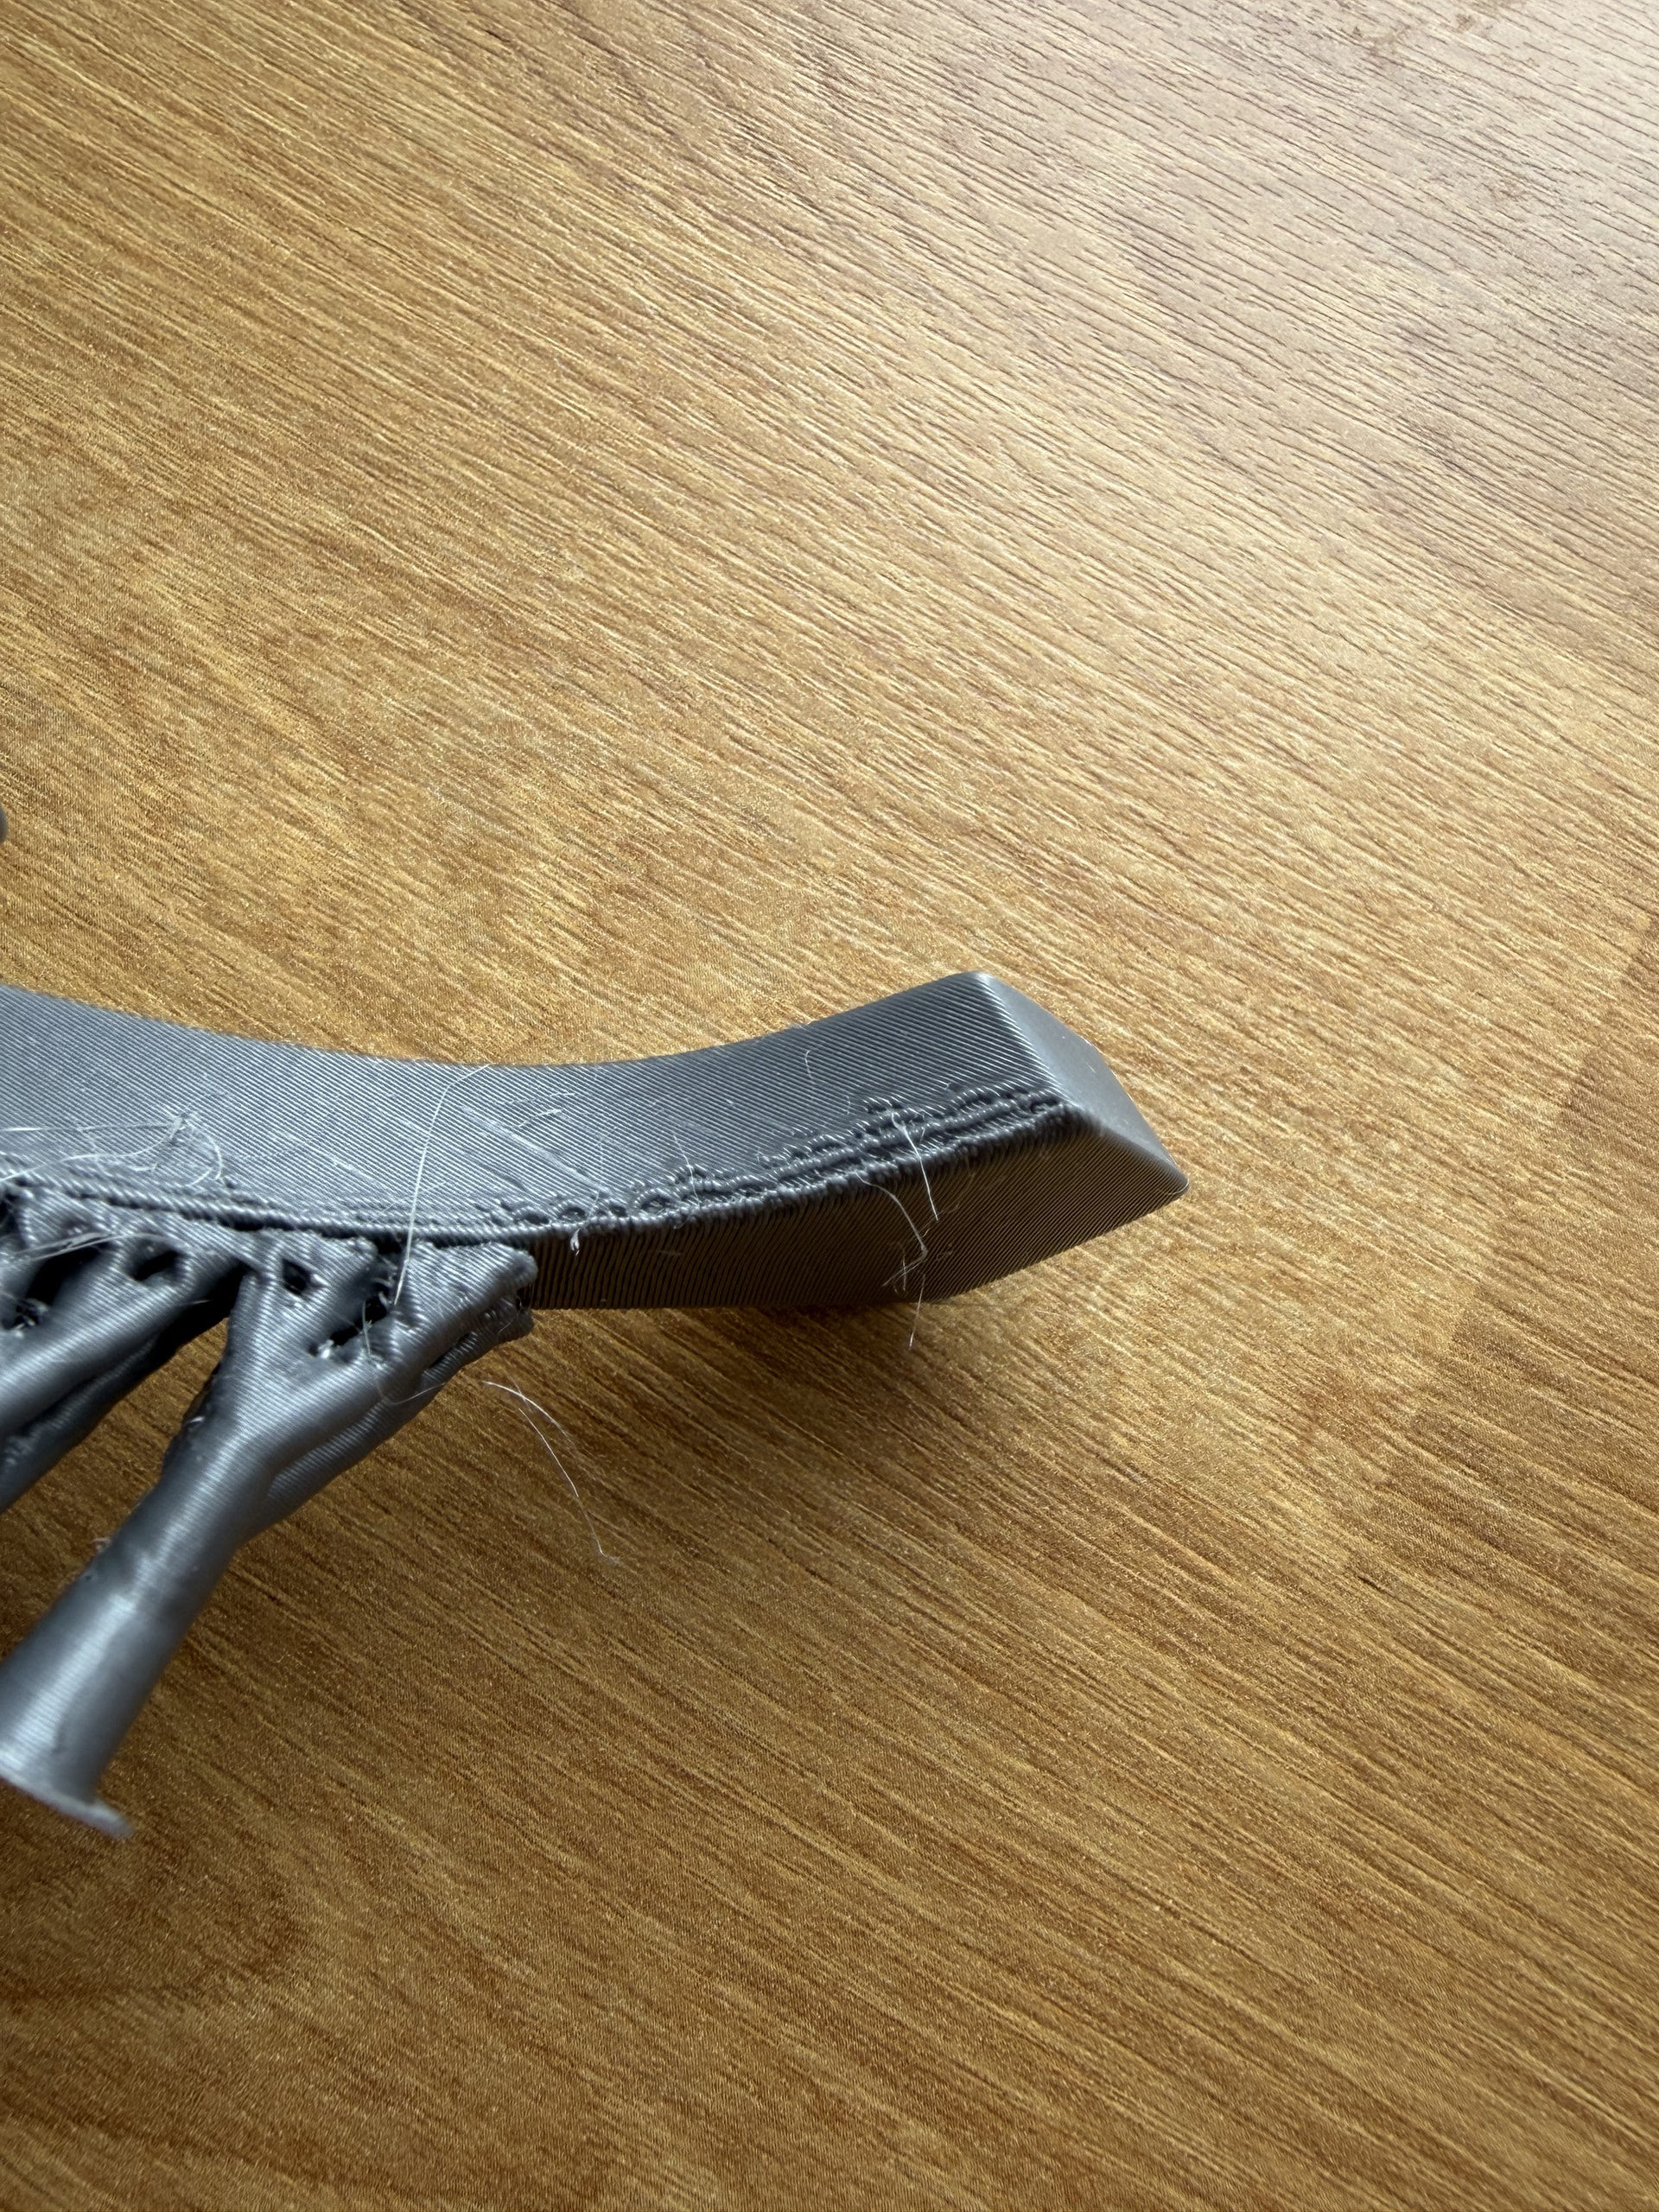
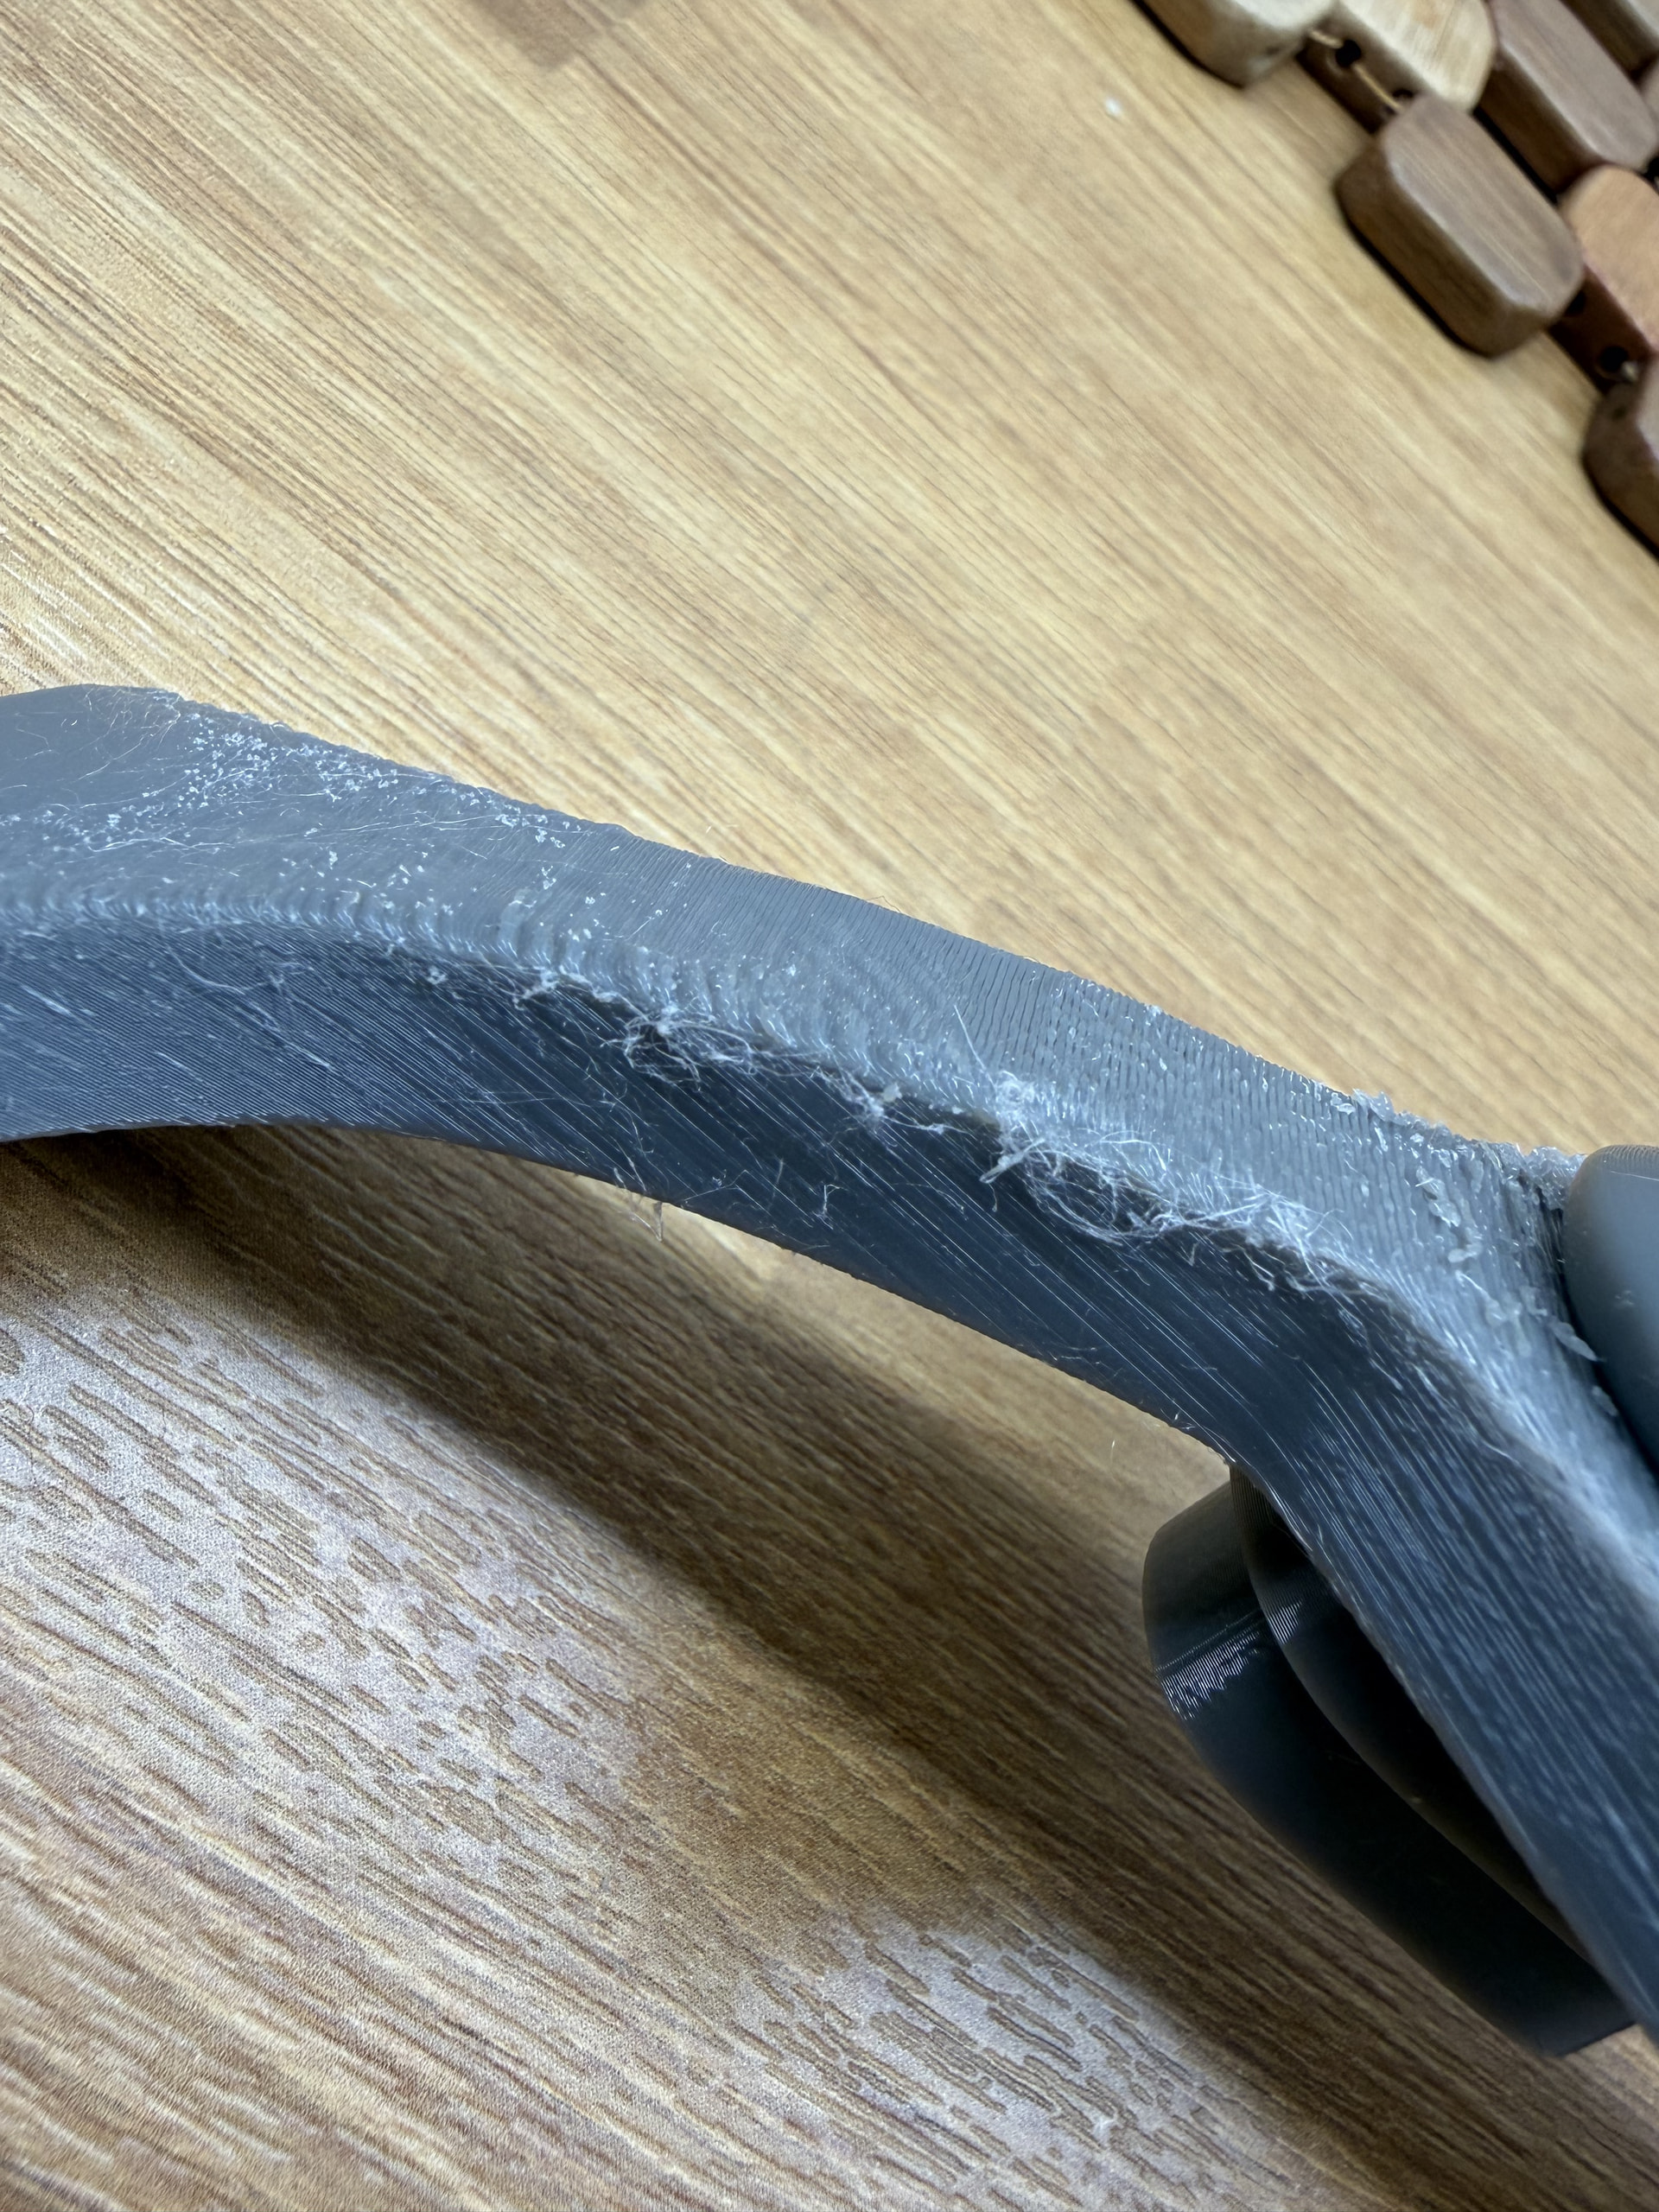
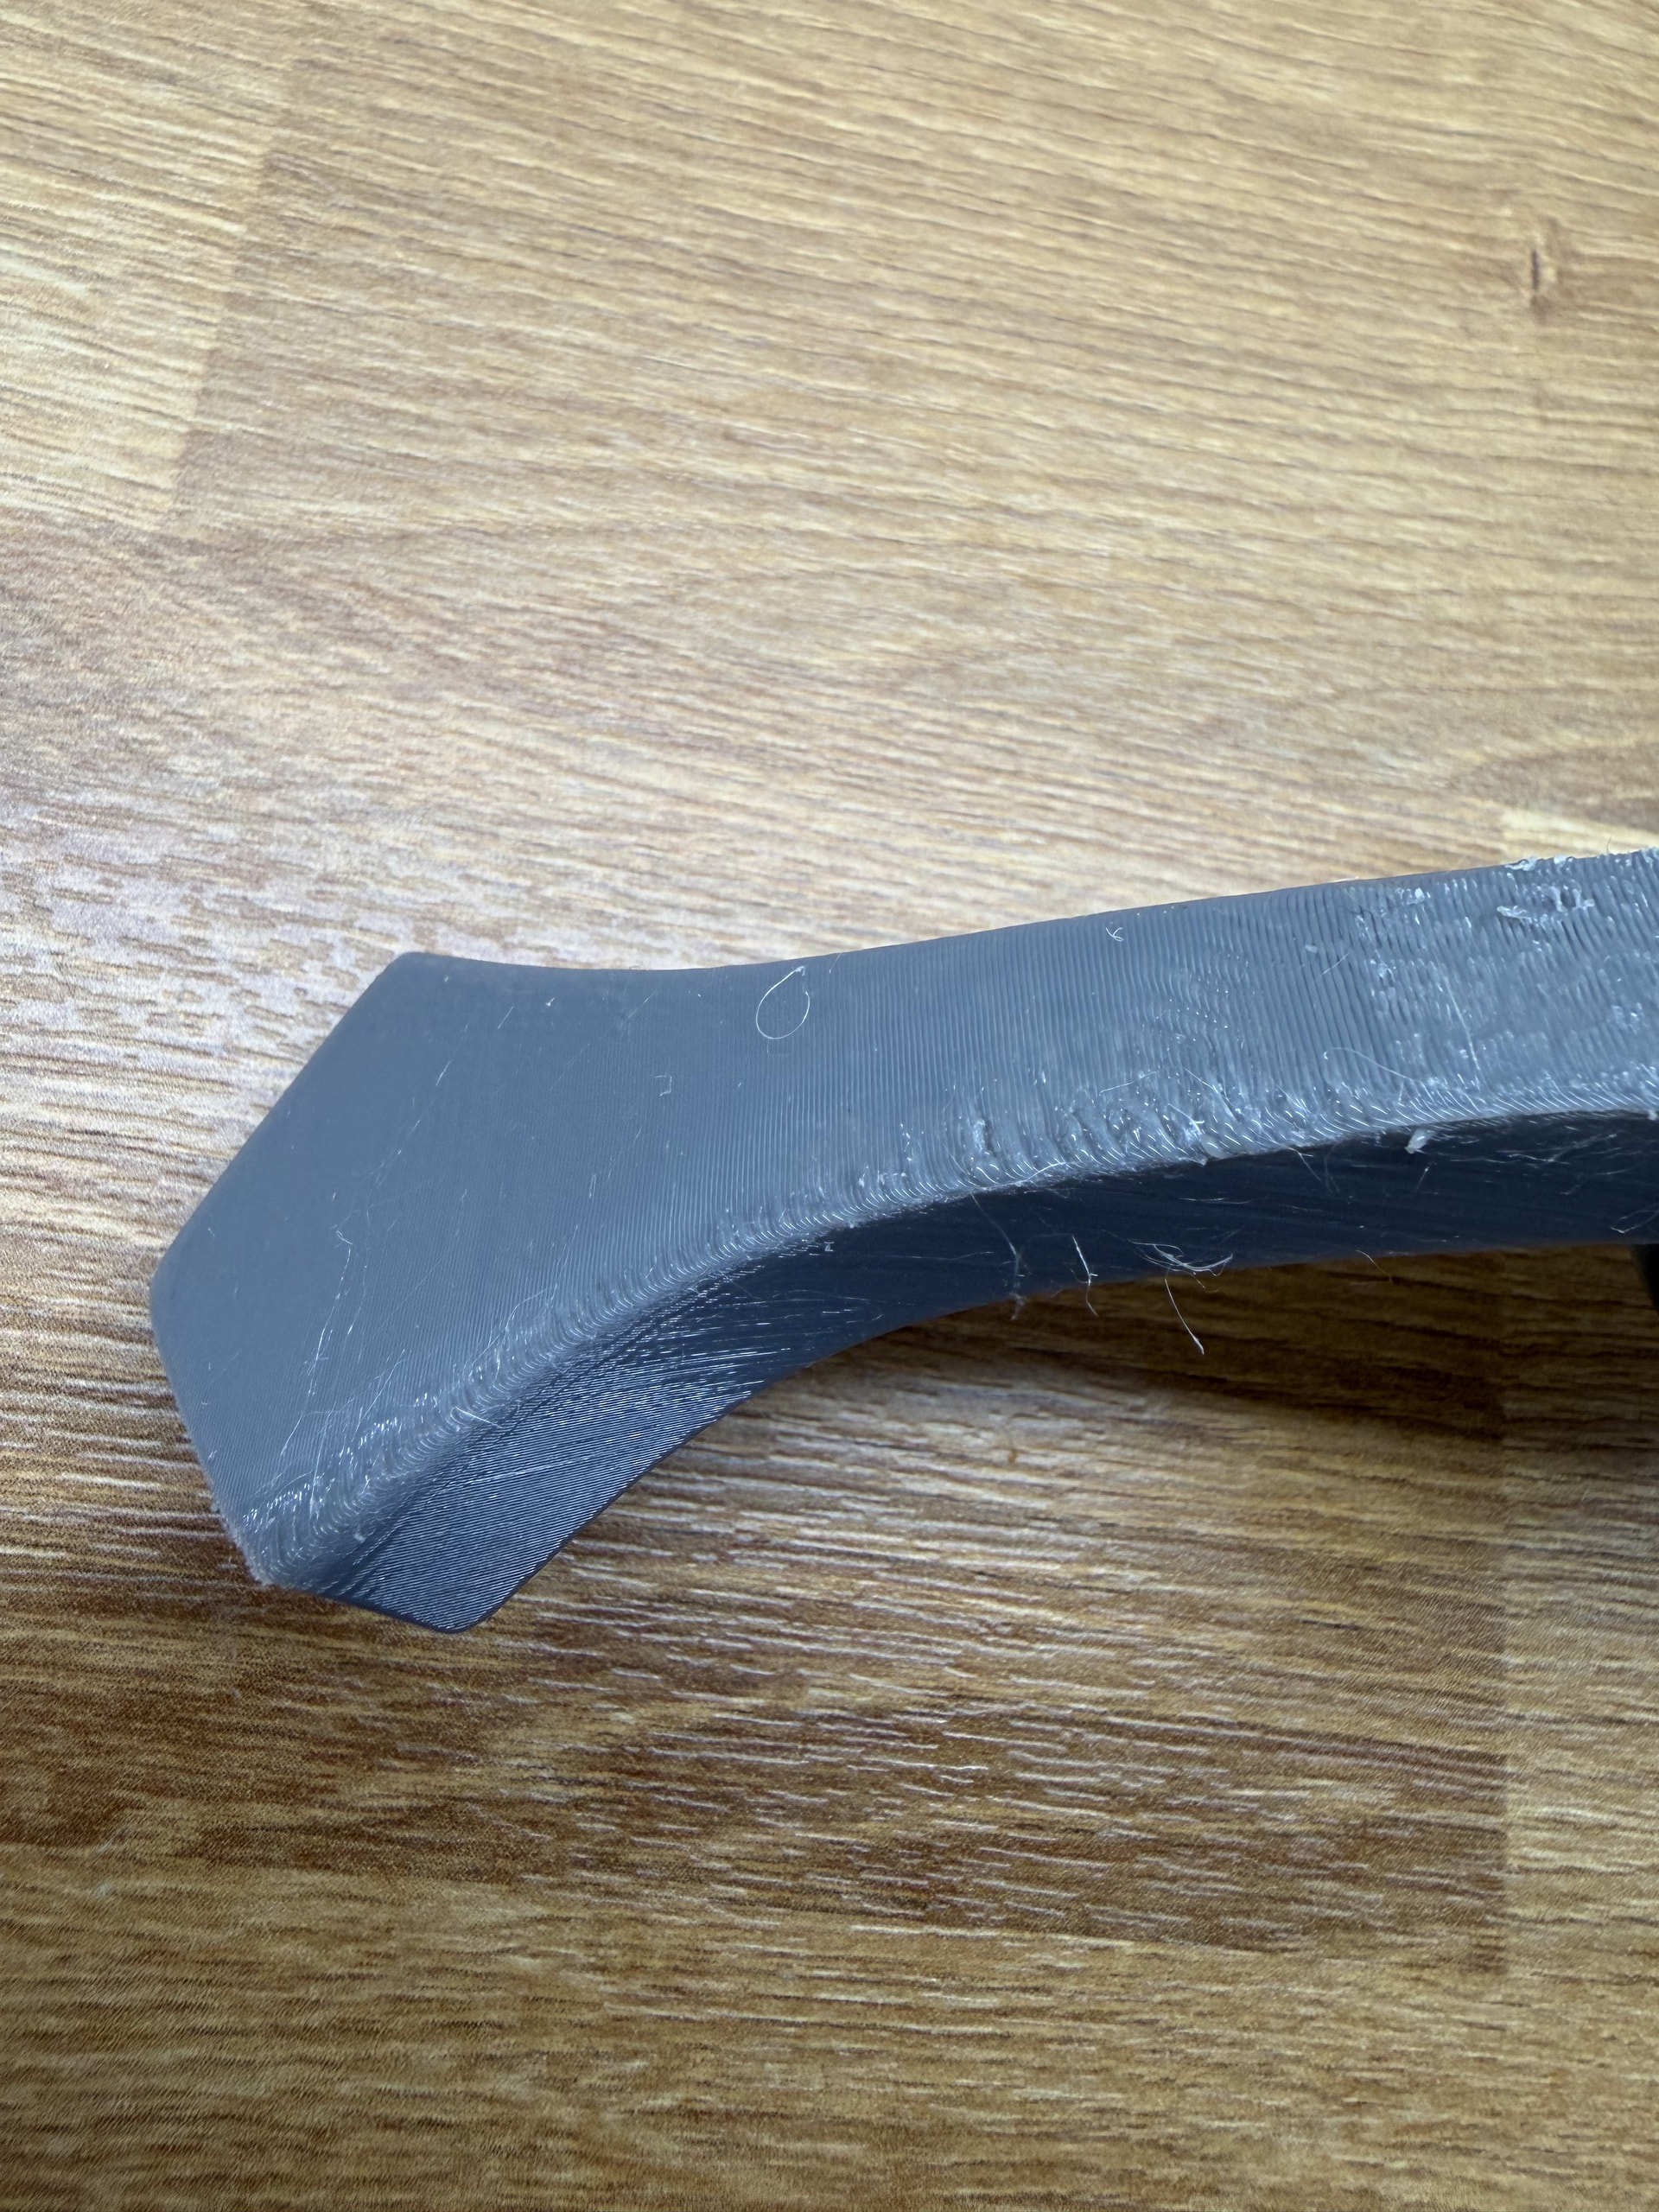
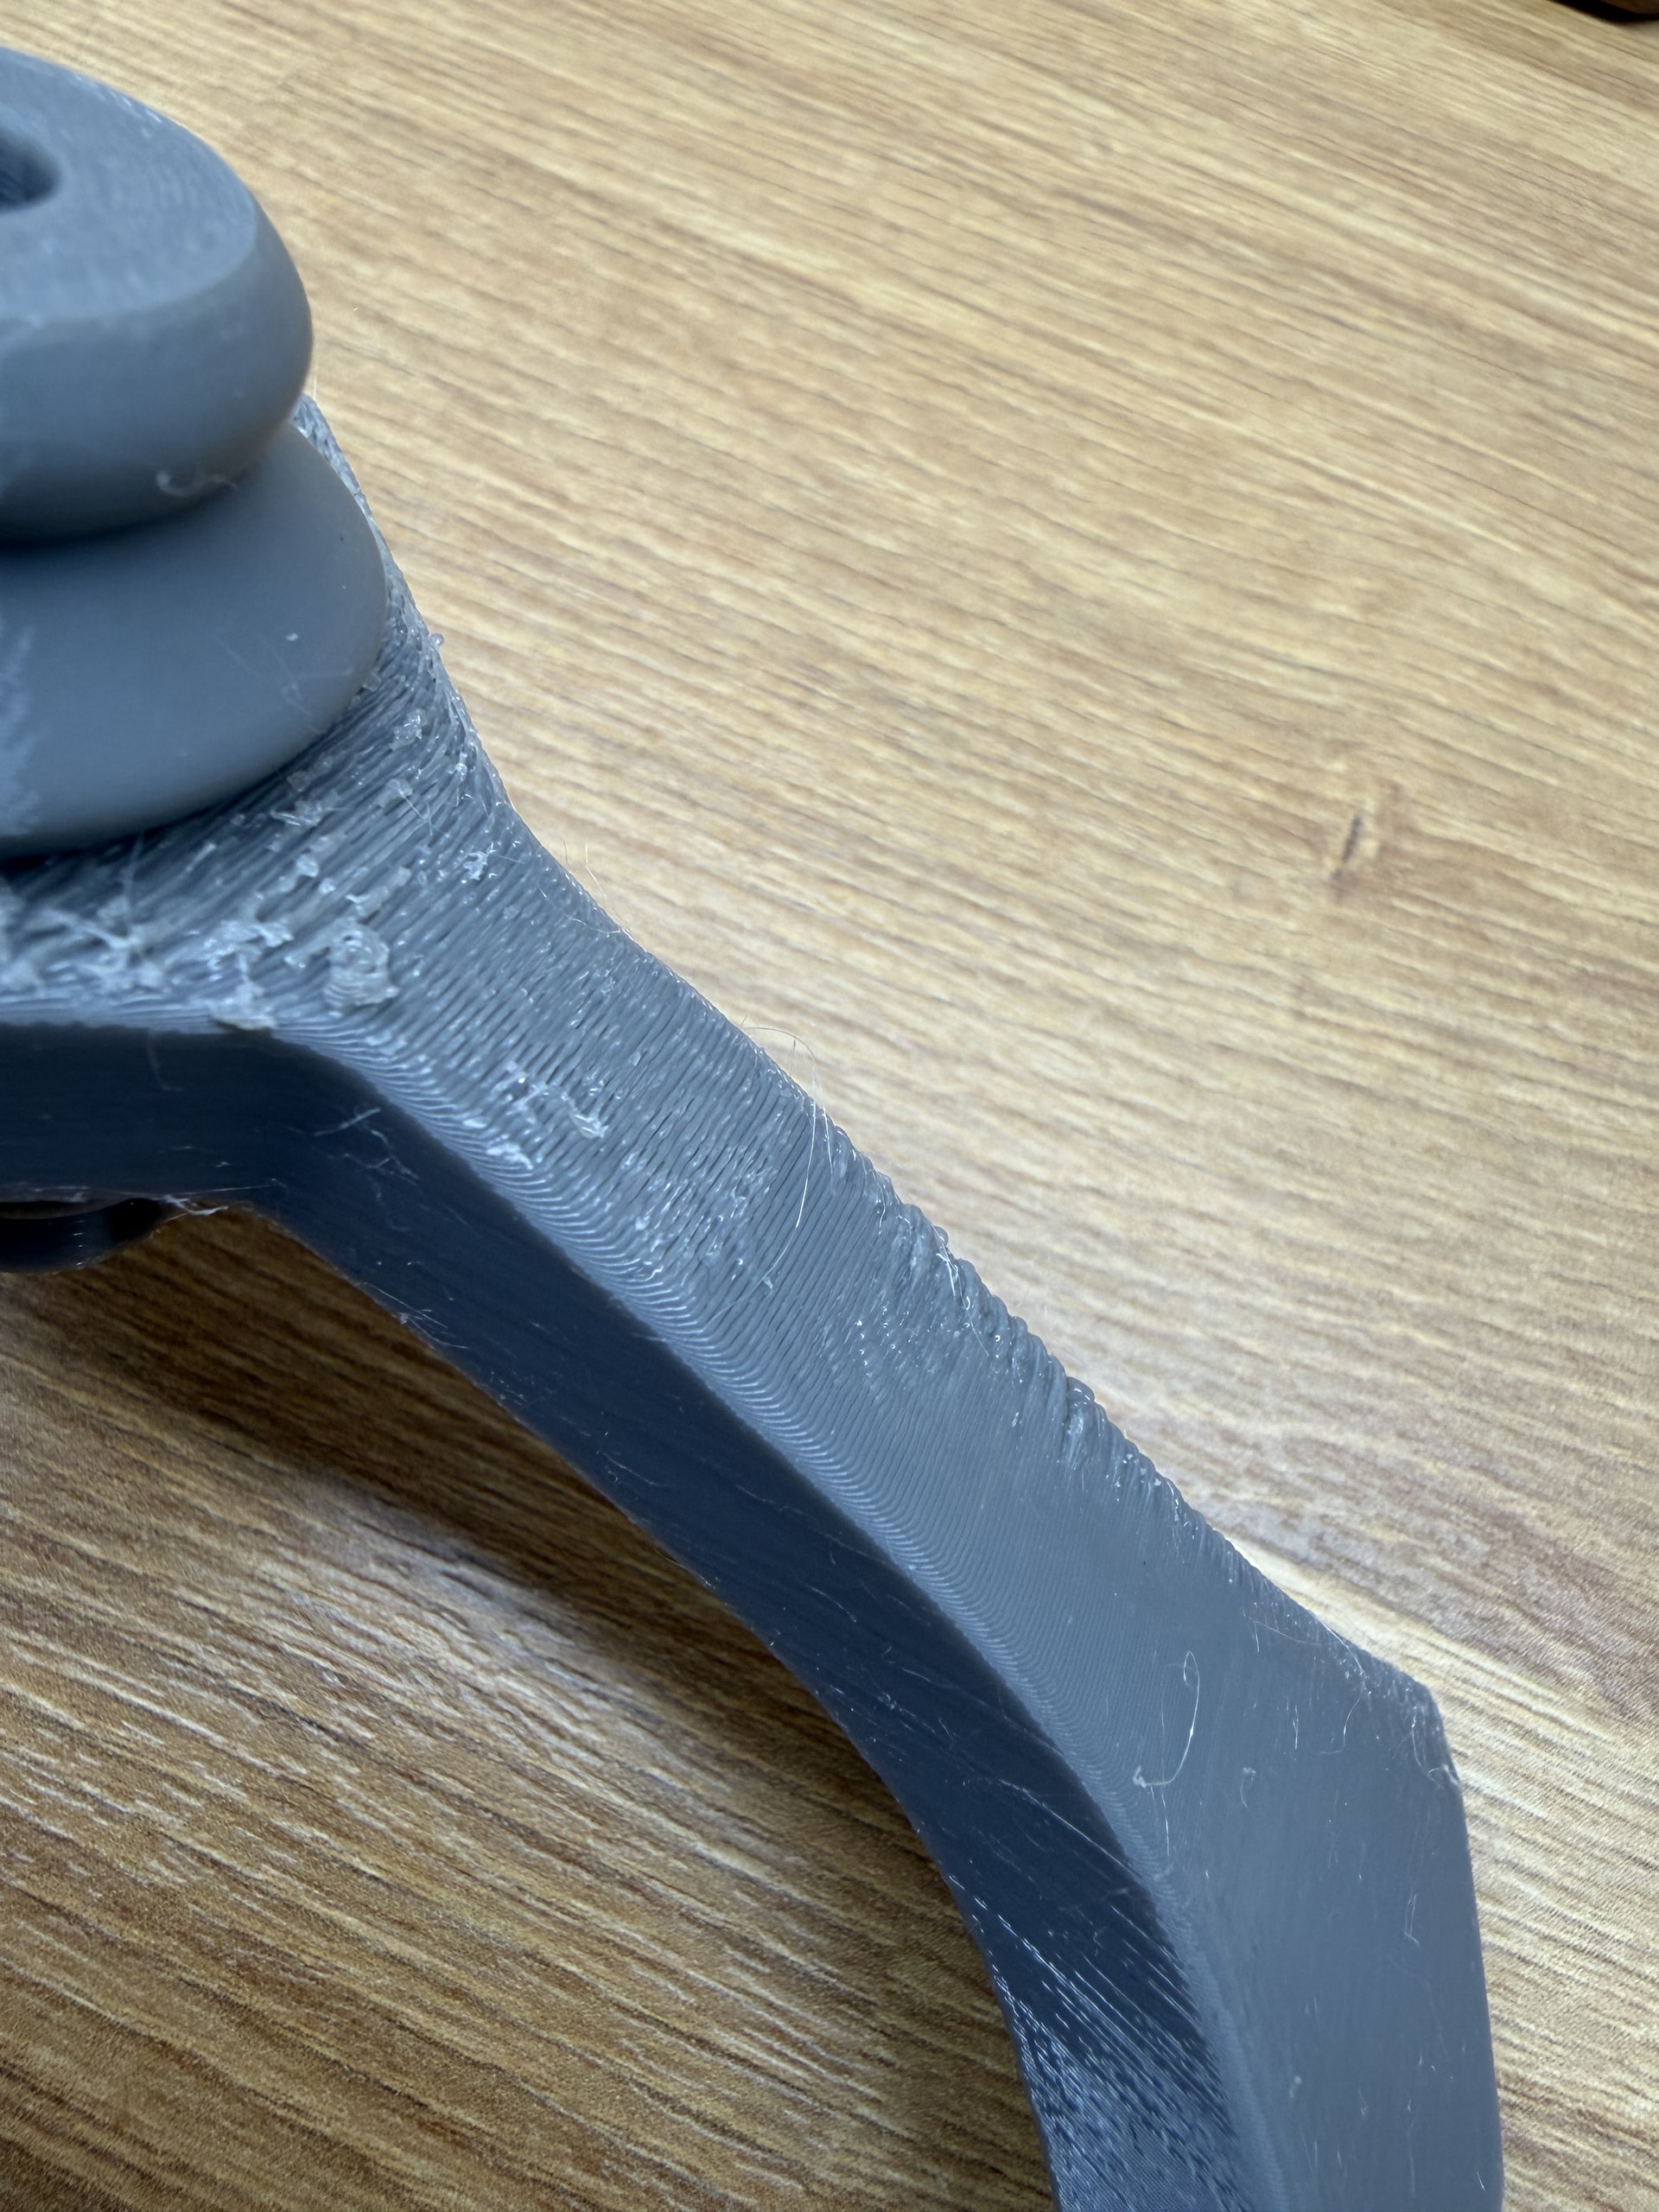
I have been trying to print this sword guard with Elegoo Rapid PETG on my P2S, but most of the time I have these rough edges and overhang walls.
As you can see in the pictures below, the edges are not quite sharp and smooth, while in the upper area of the picture the edges are in a great shape.
Also please don’t mind the remainings of the supports, I didn’t bother removing them completely as I saw the issue still persists.
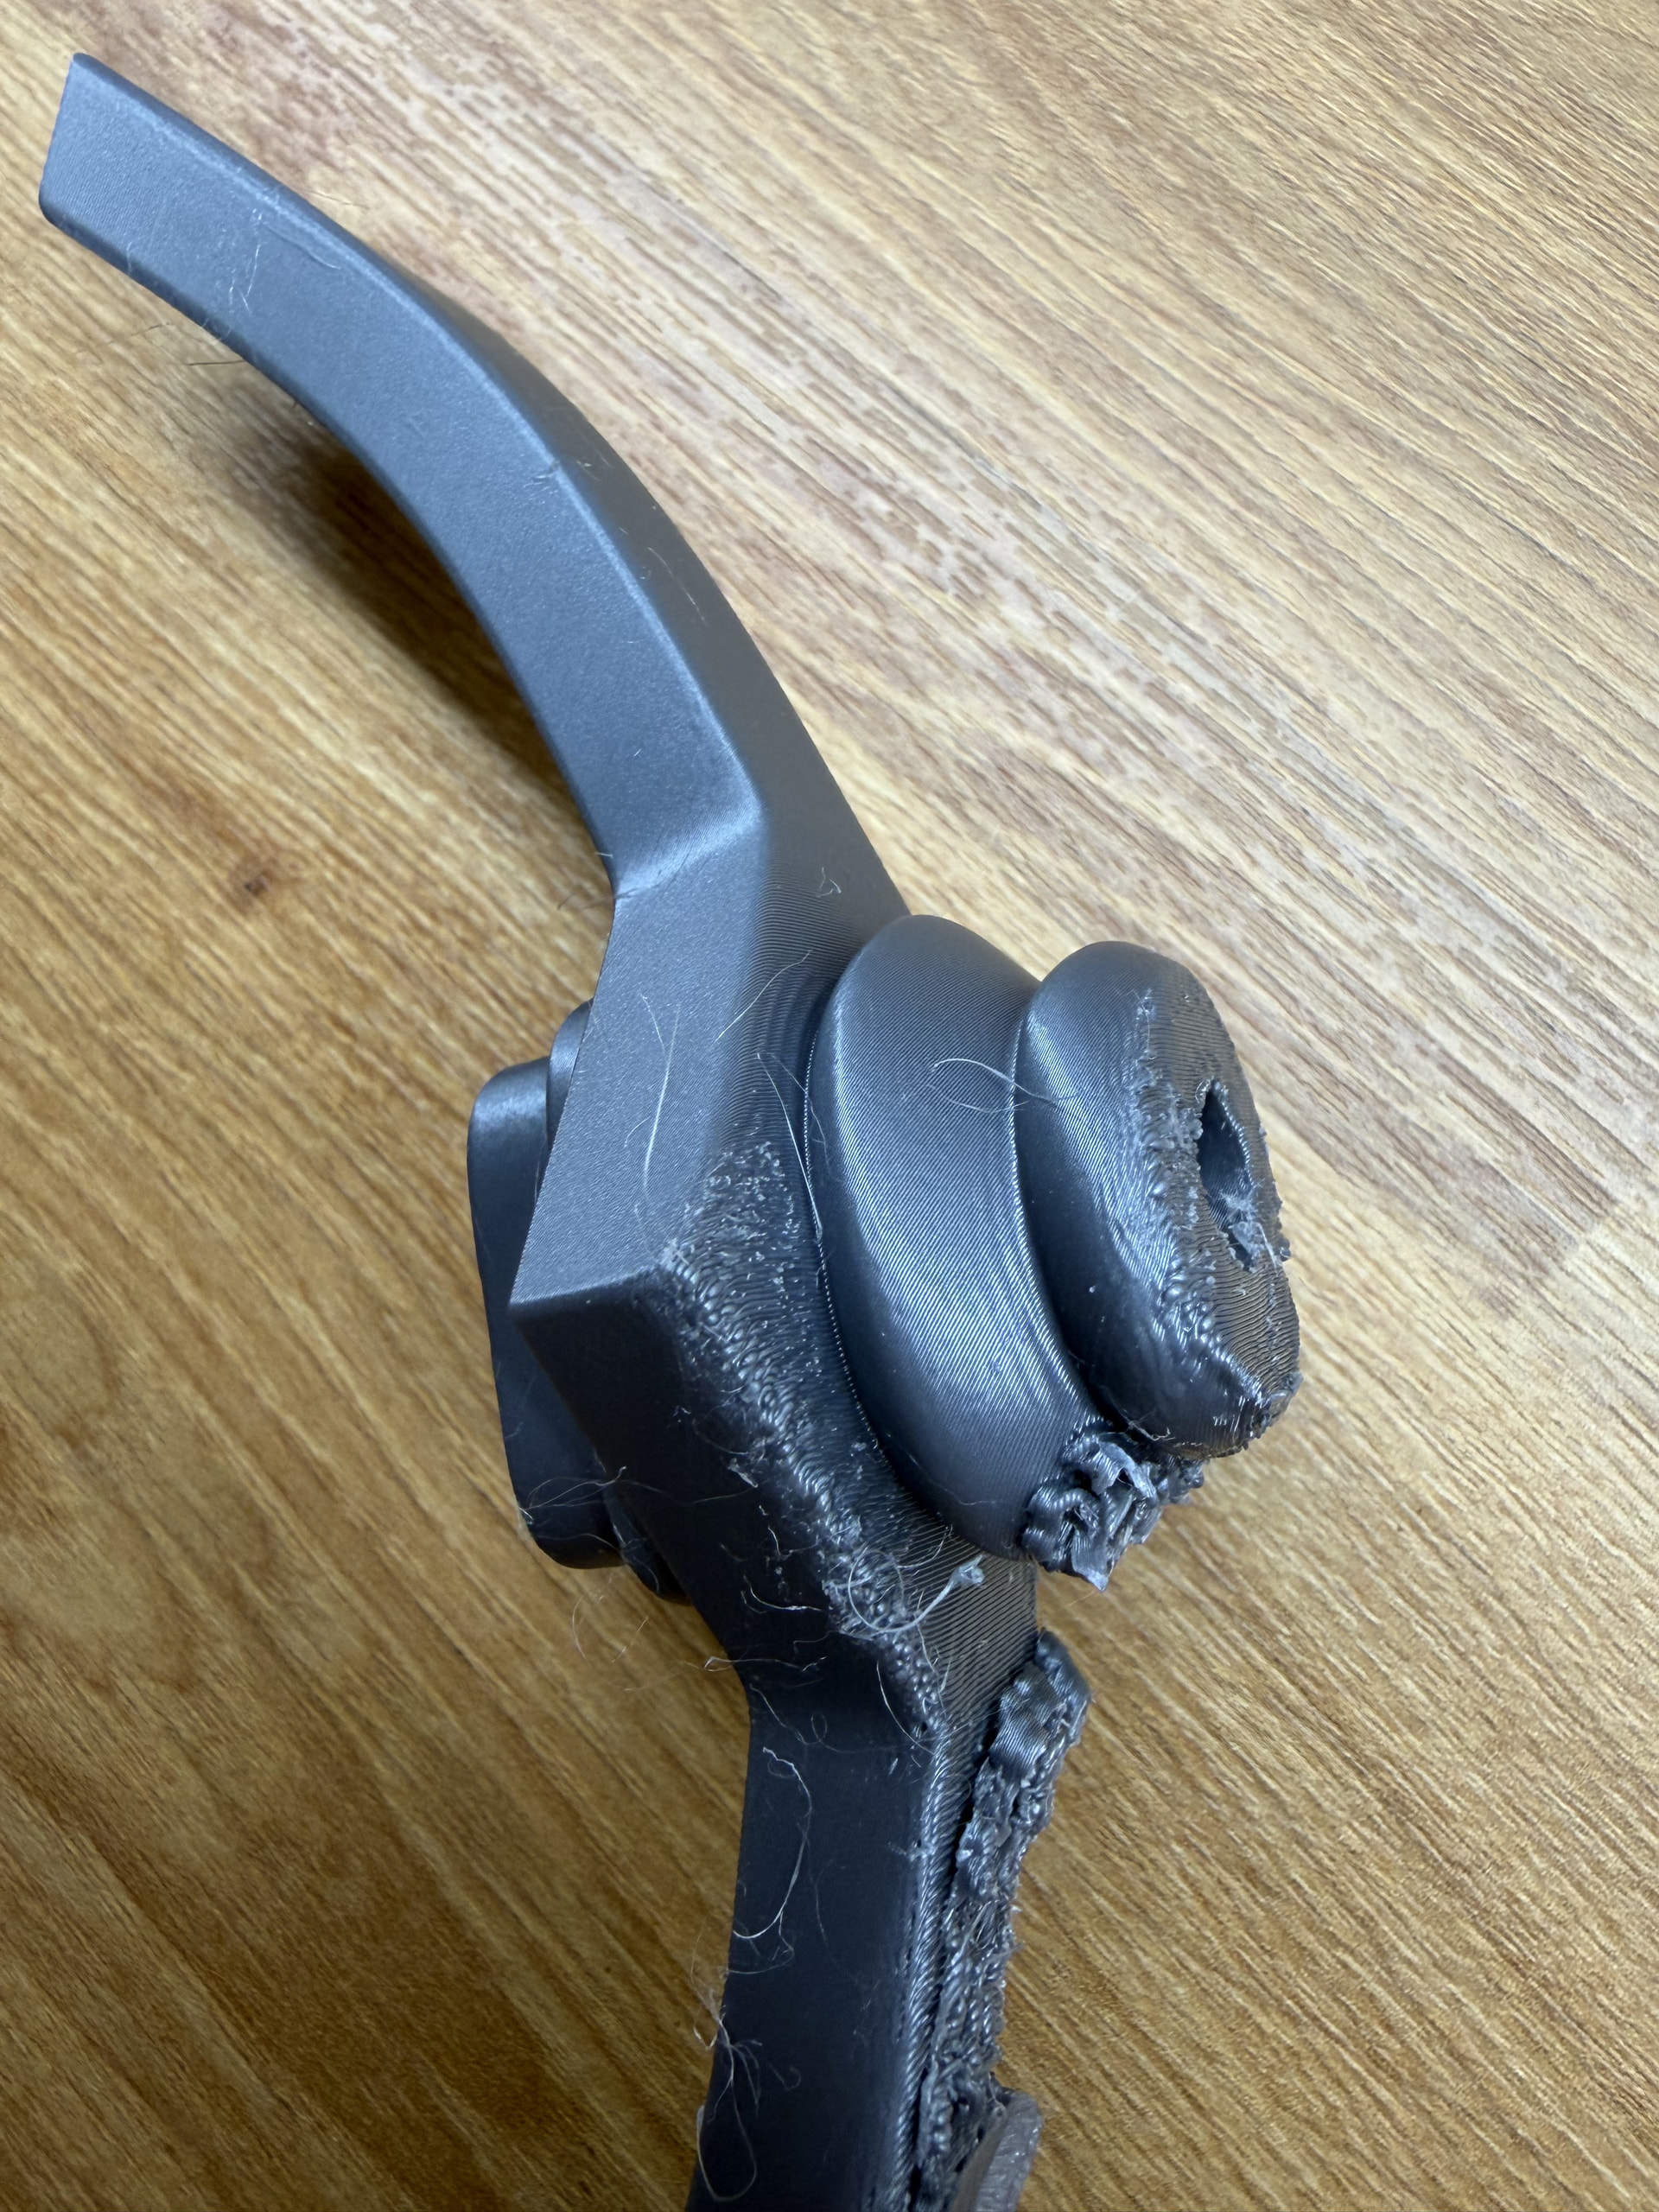
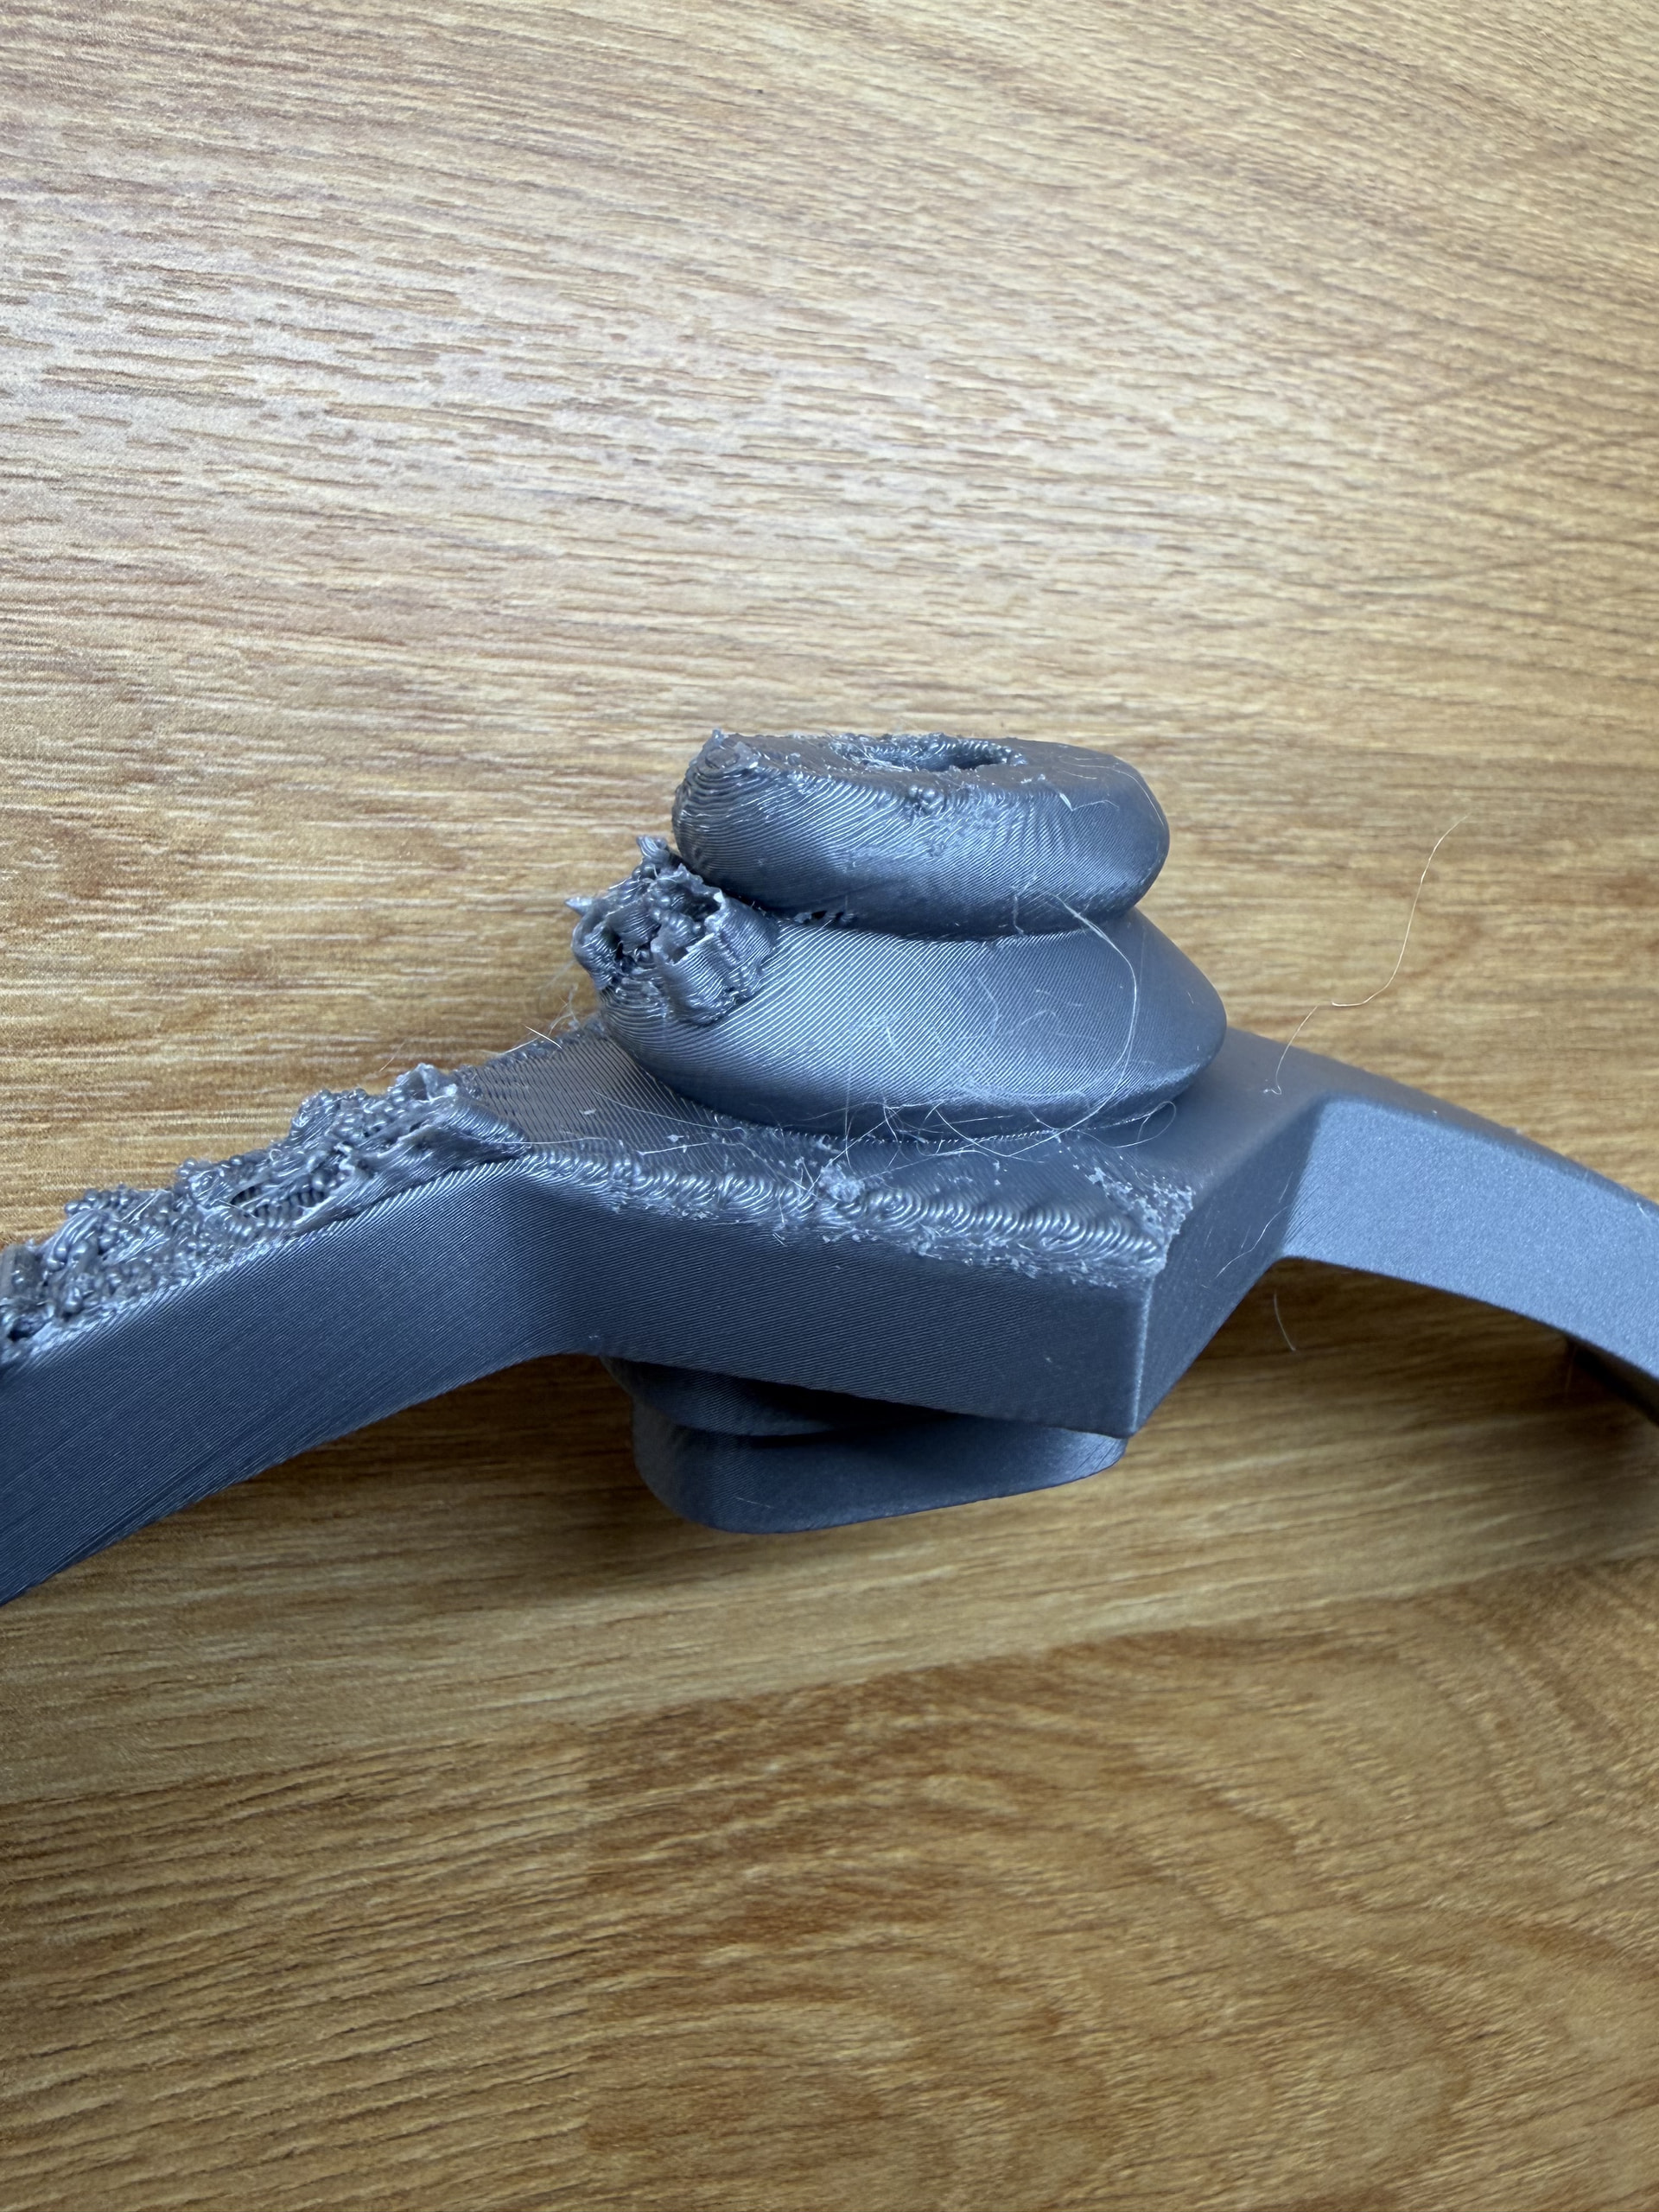
I tried SUNLU PETG for a change, and while it’s a bit better, the issue still persists at the edges and around the overhang walls. This filament has not been dried at all, been in the drawer for a week or two now. Put it into the dryer for 3 or 4 hours in the morning before printing, most likely still has moisture in it. Regardless, the result is a bit better. Also, it’s not calibrated and I used the Generic PETG preset with dynamic flow enabled.
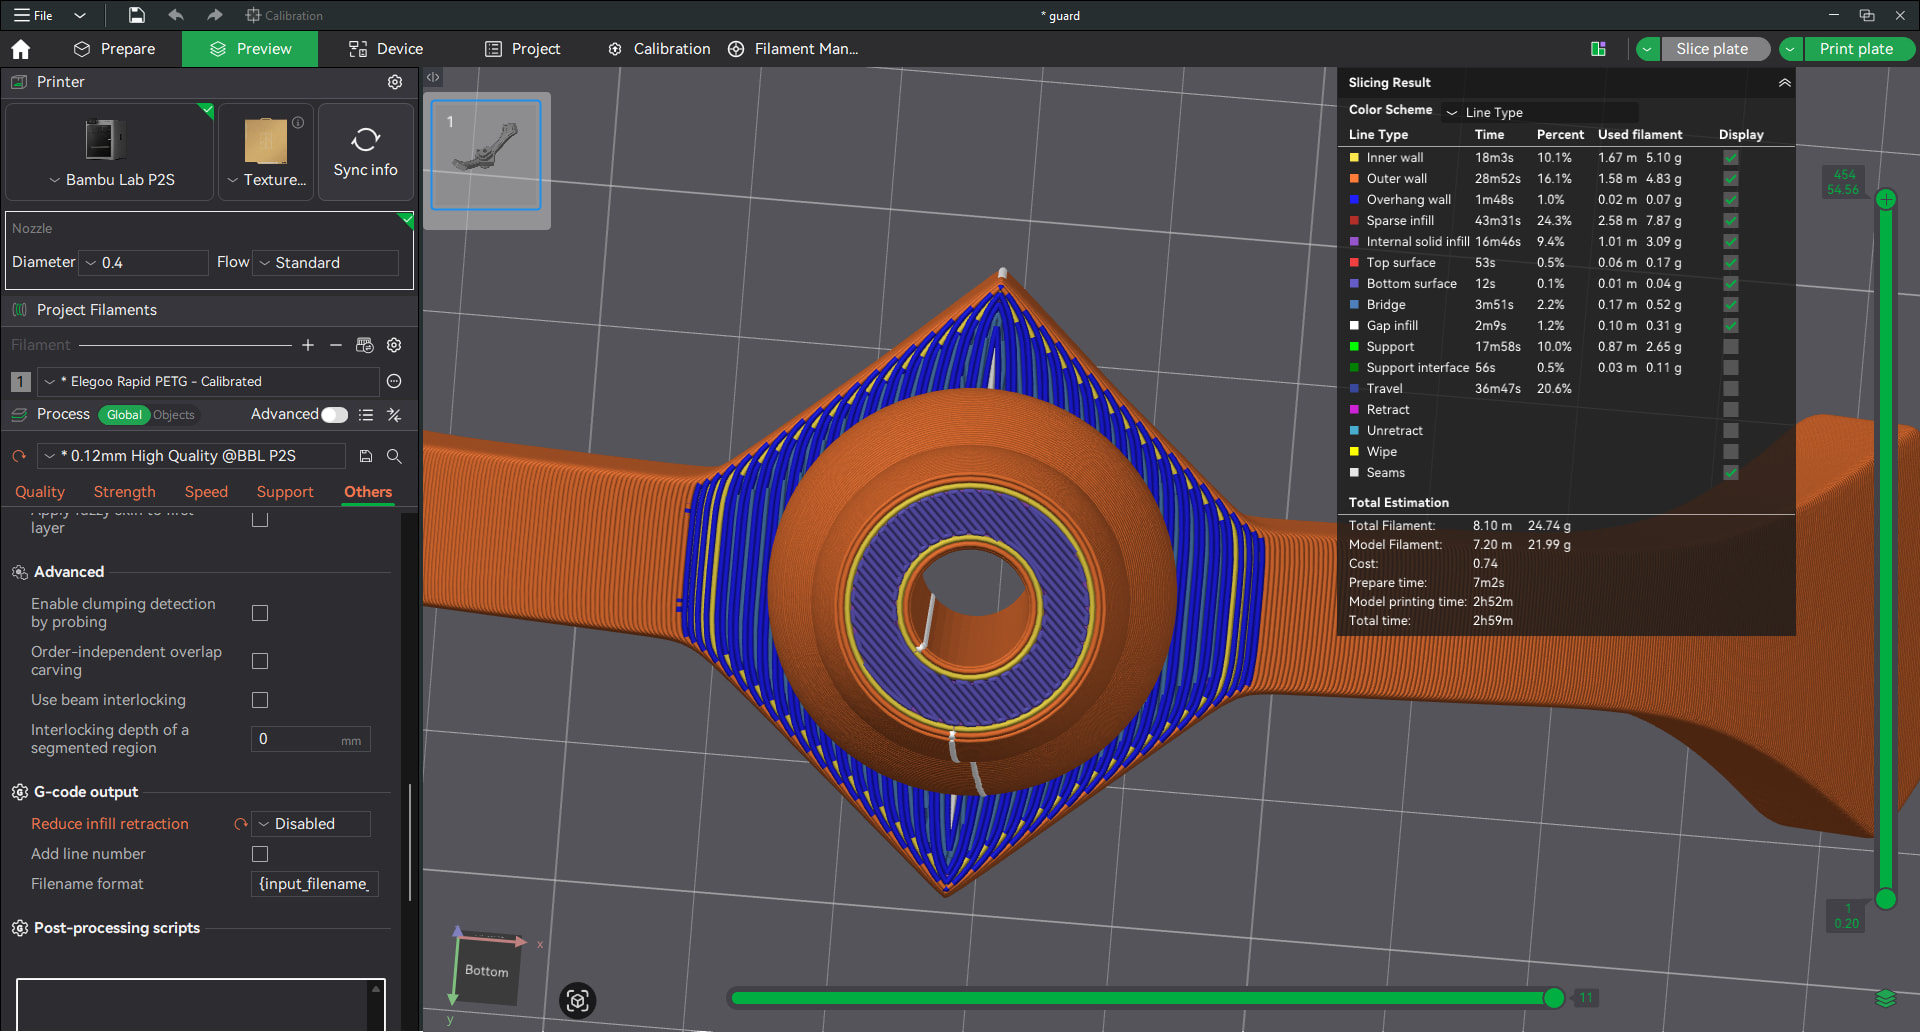
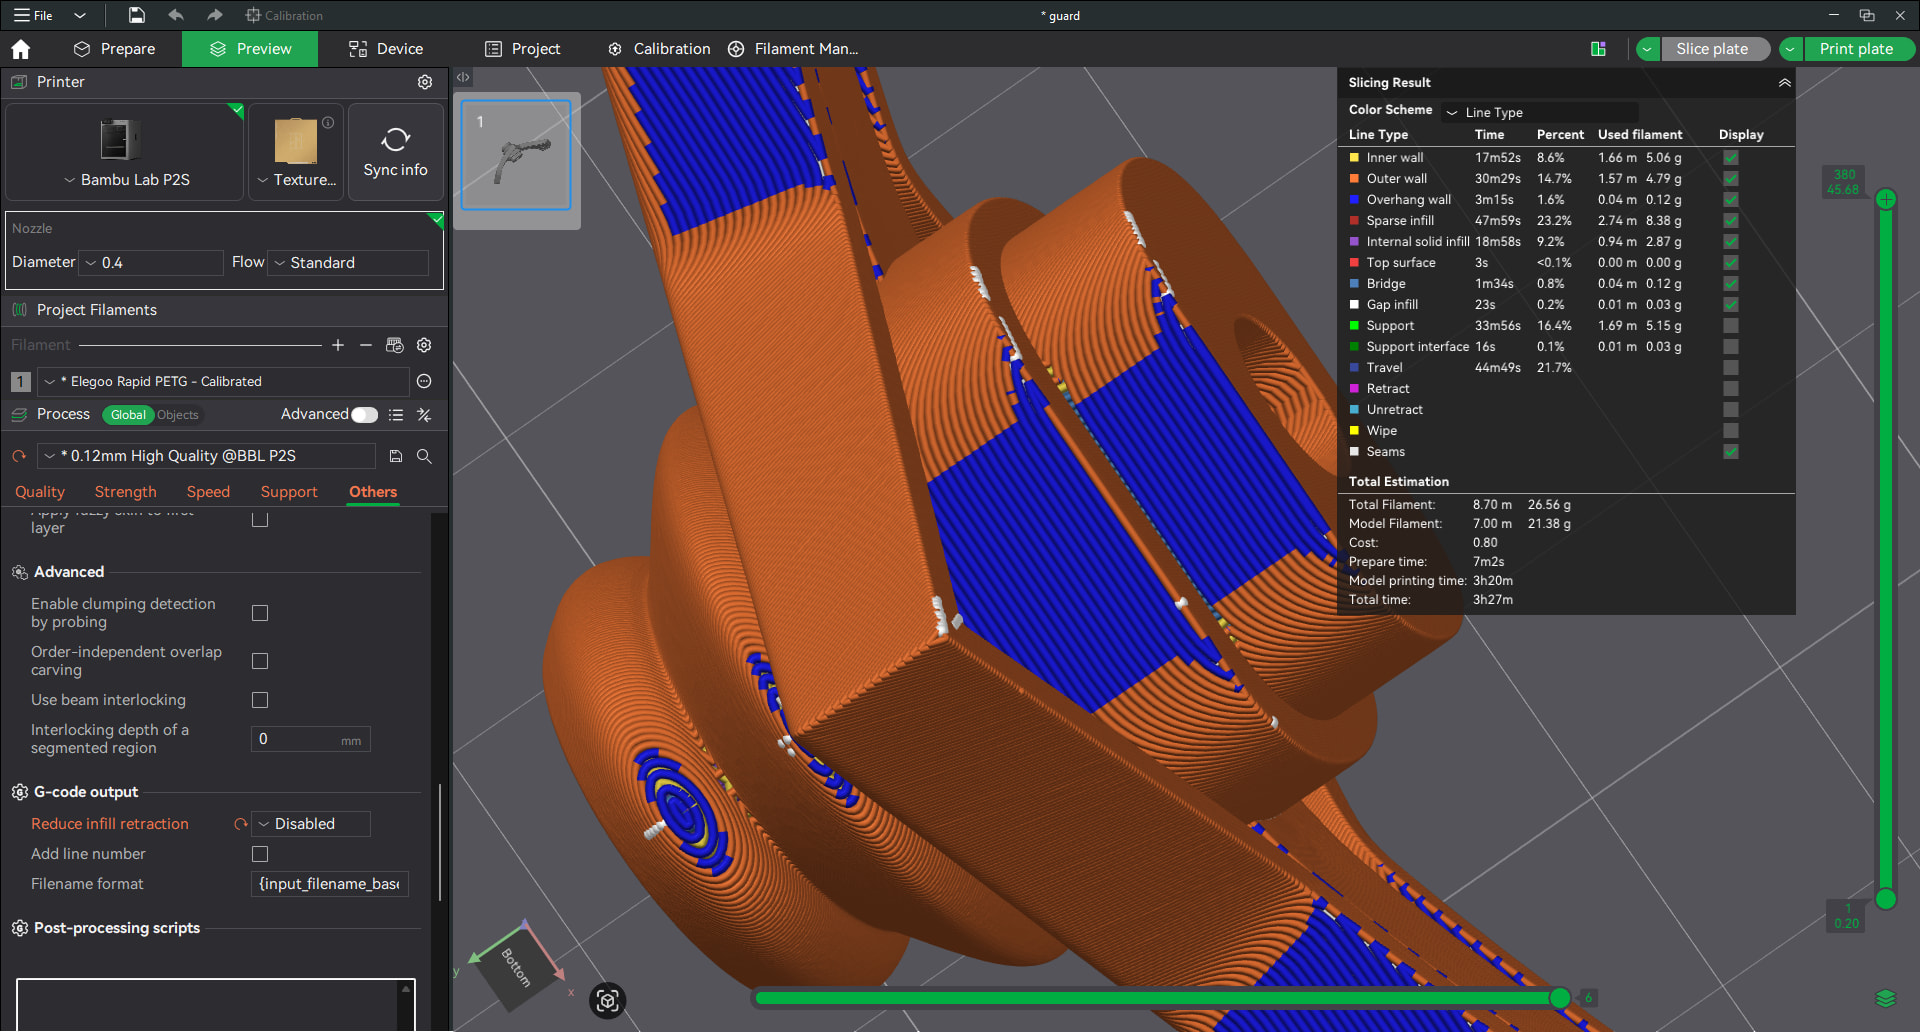
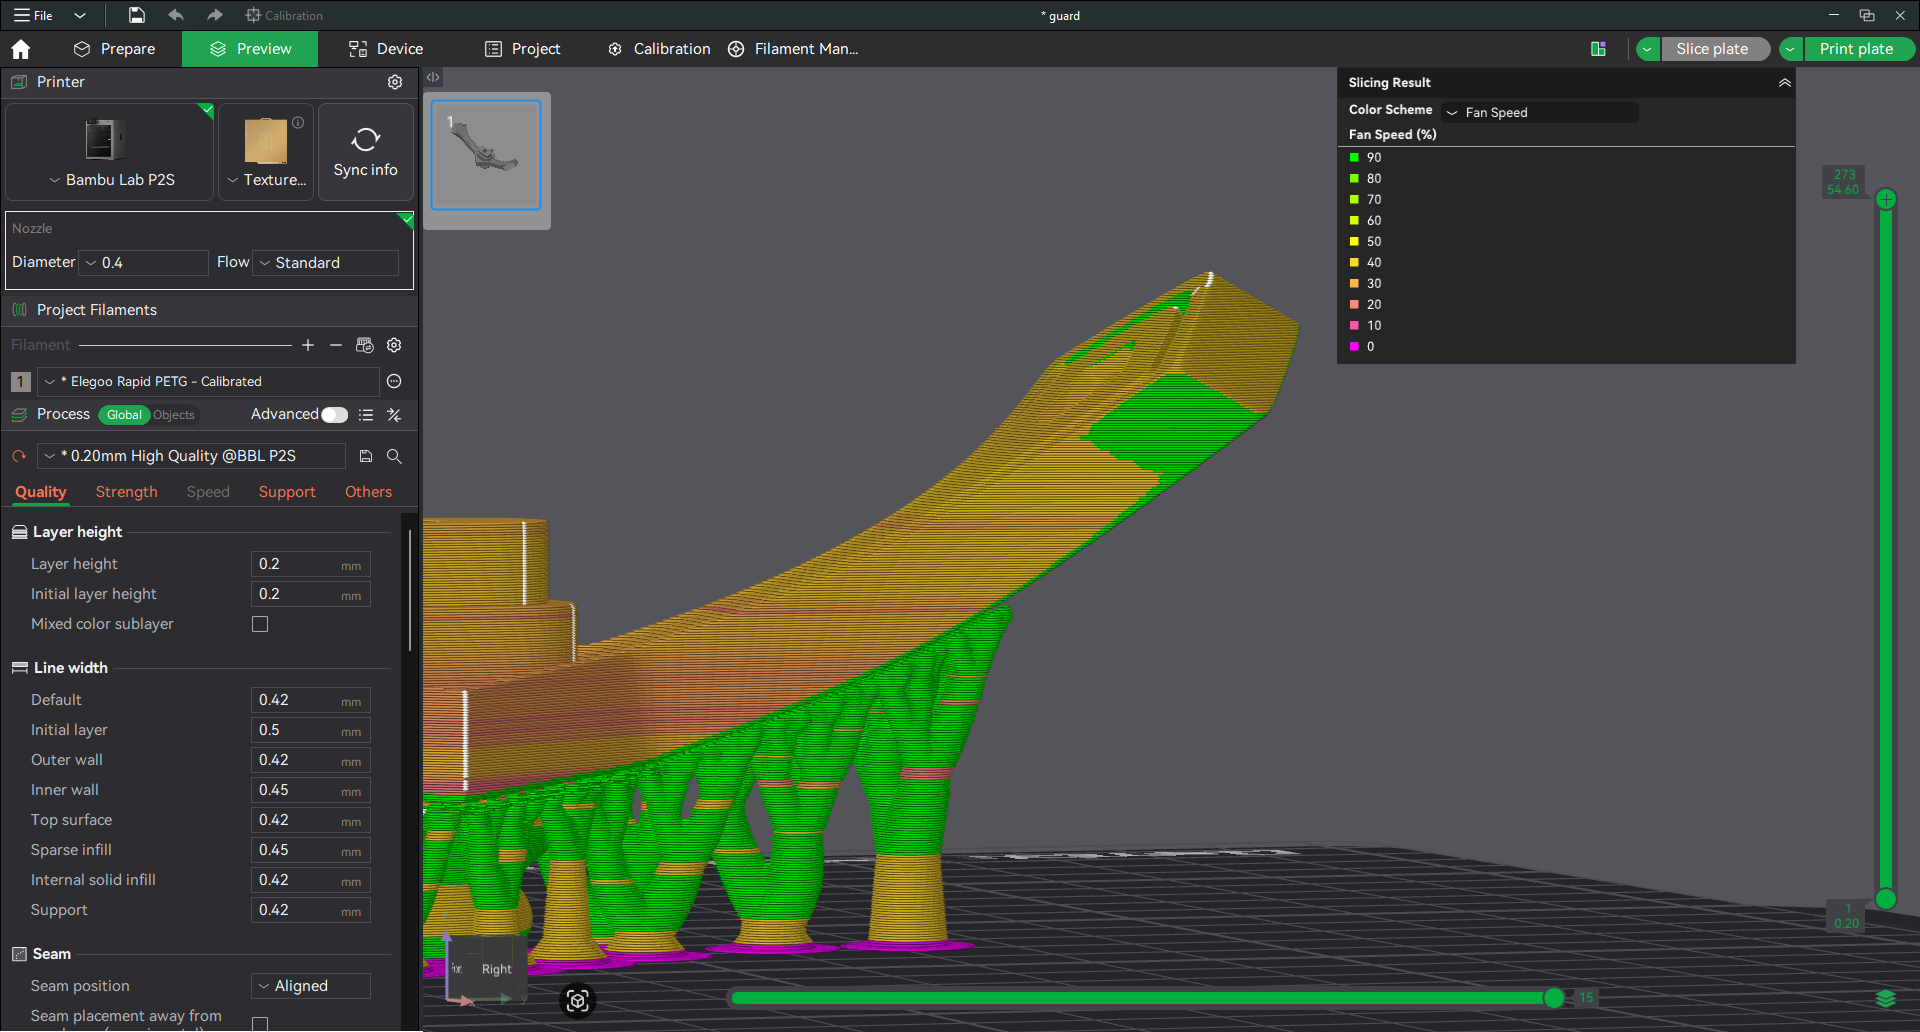
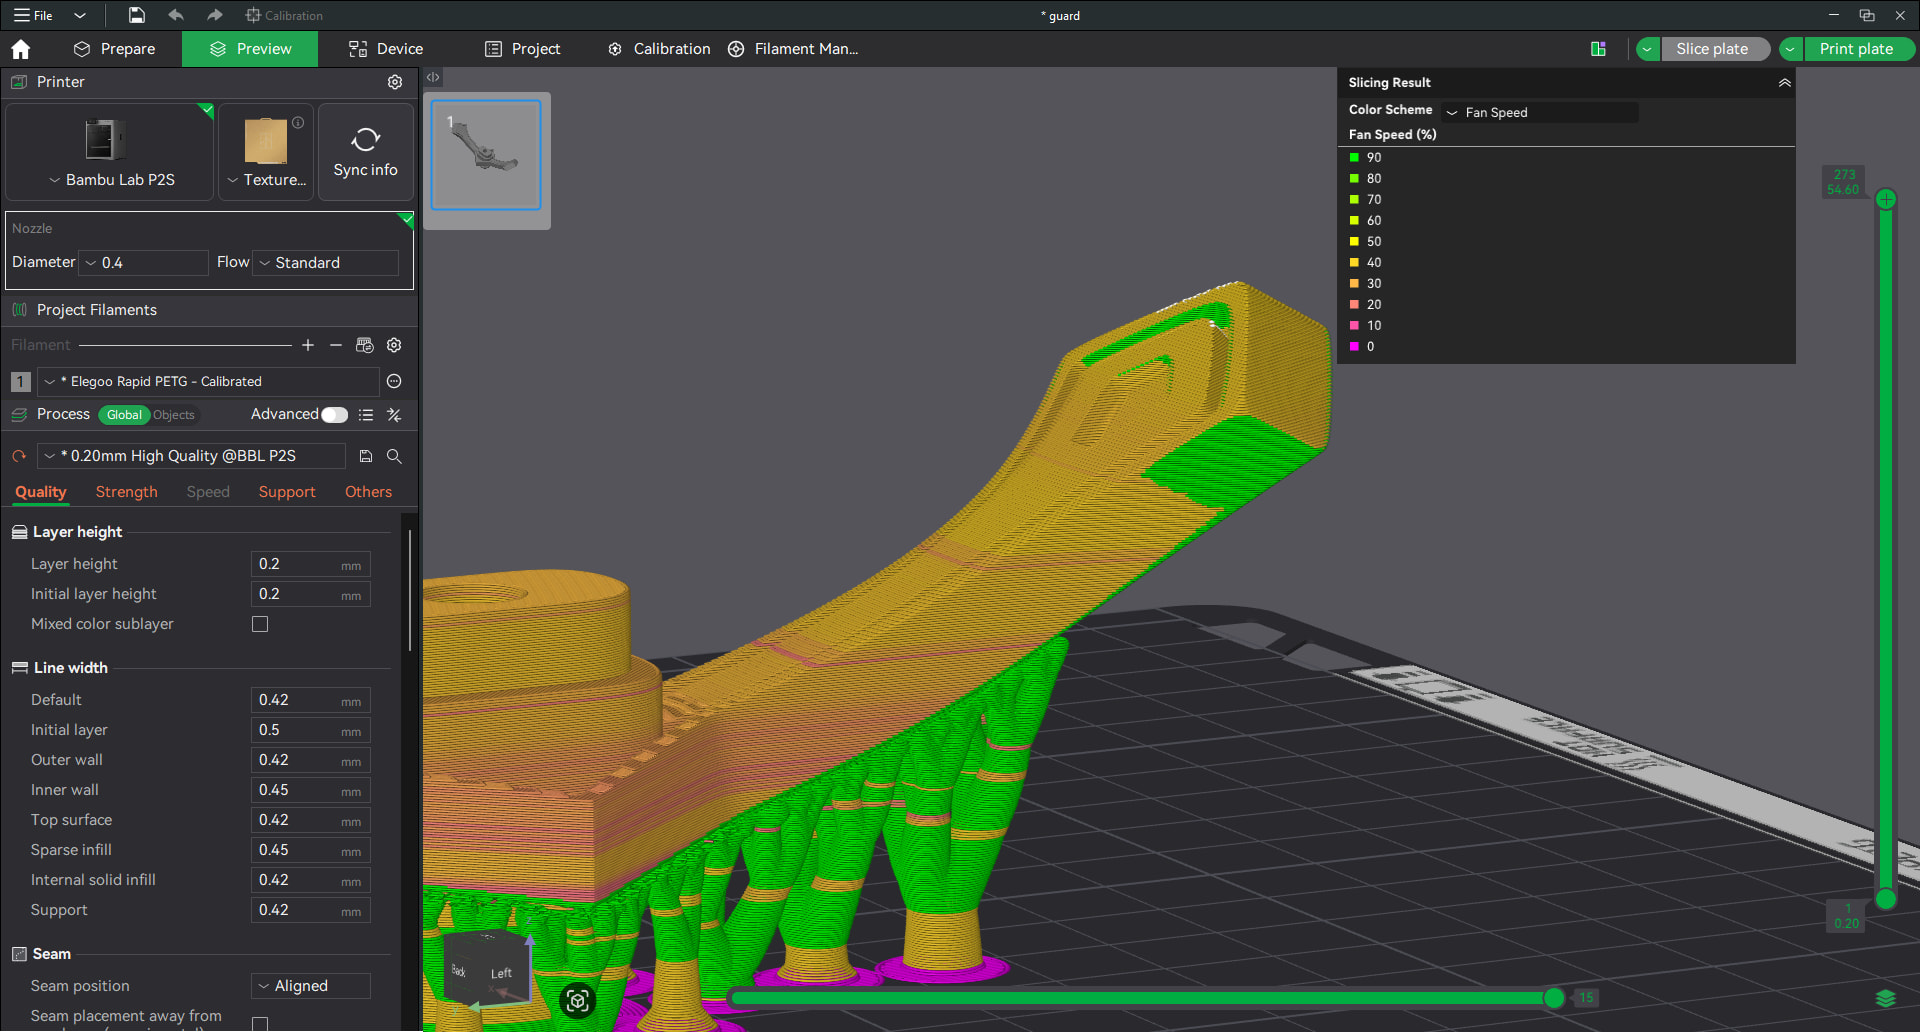
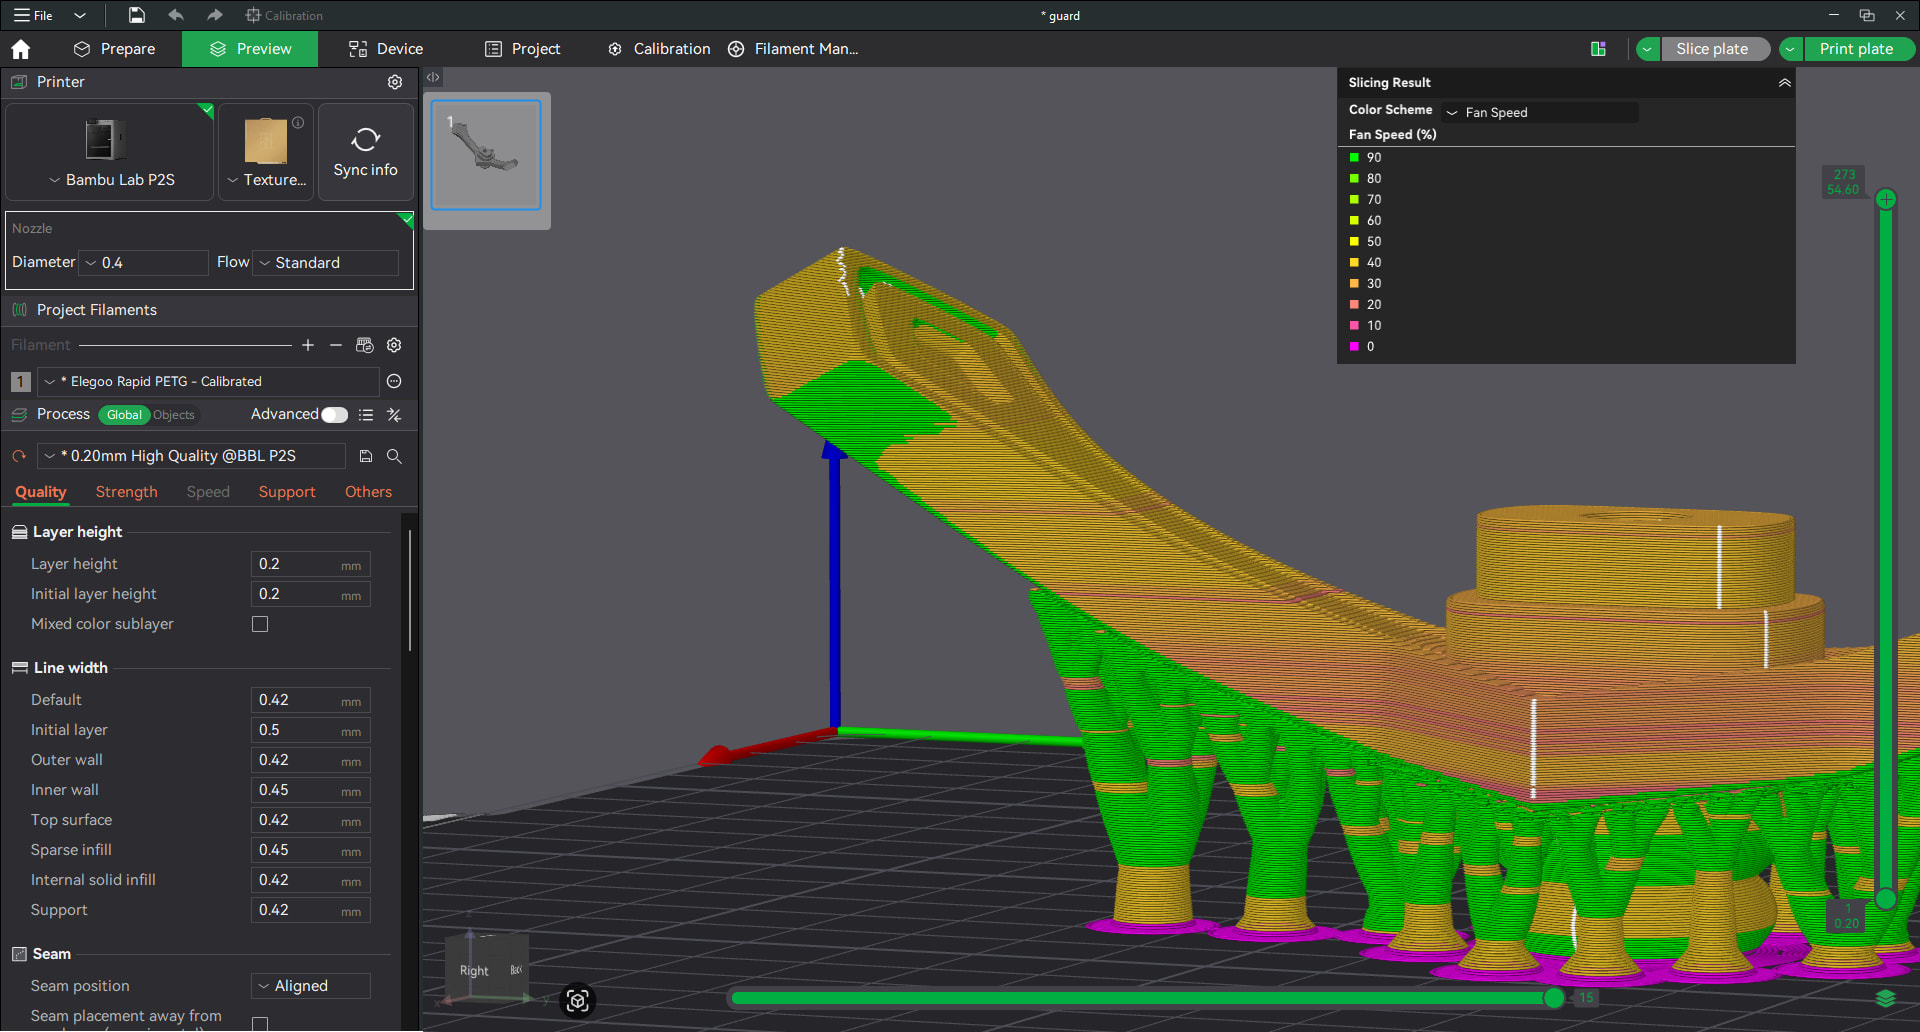
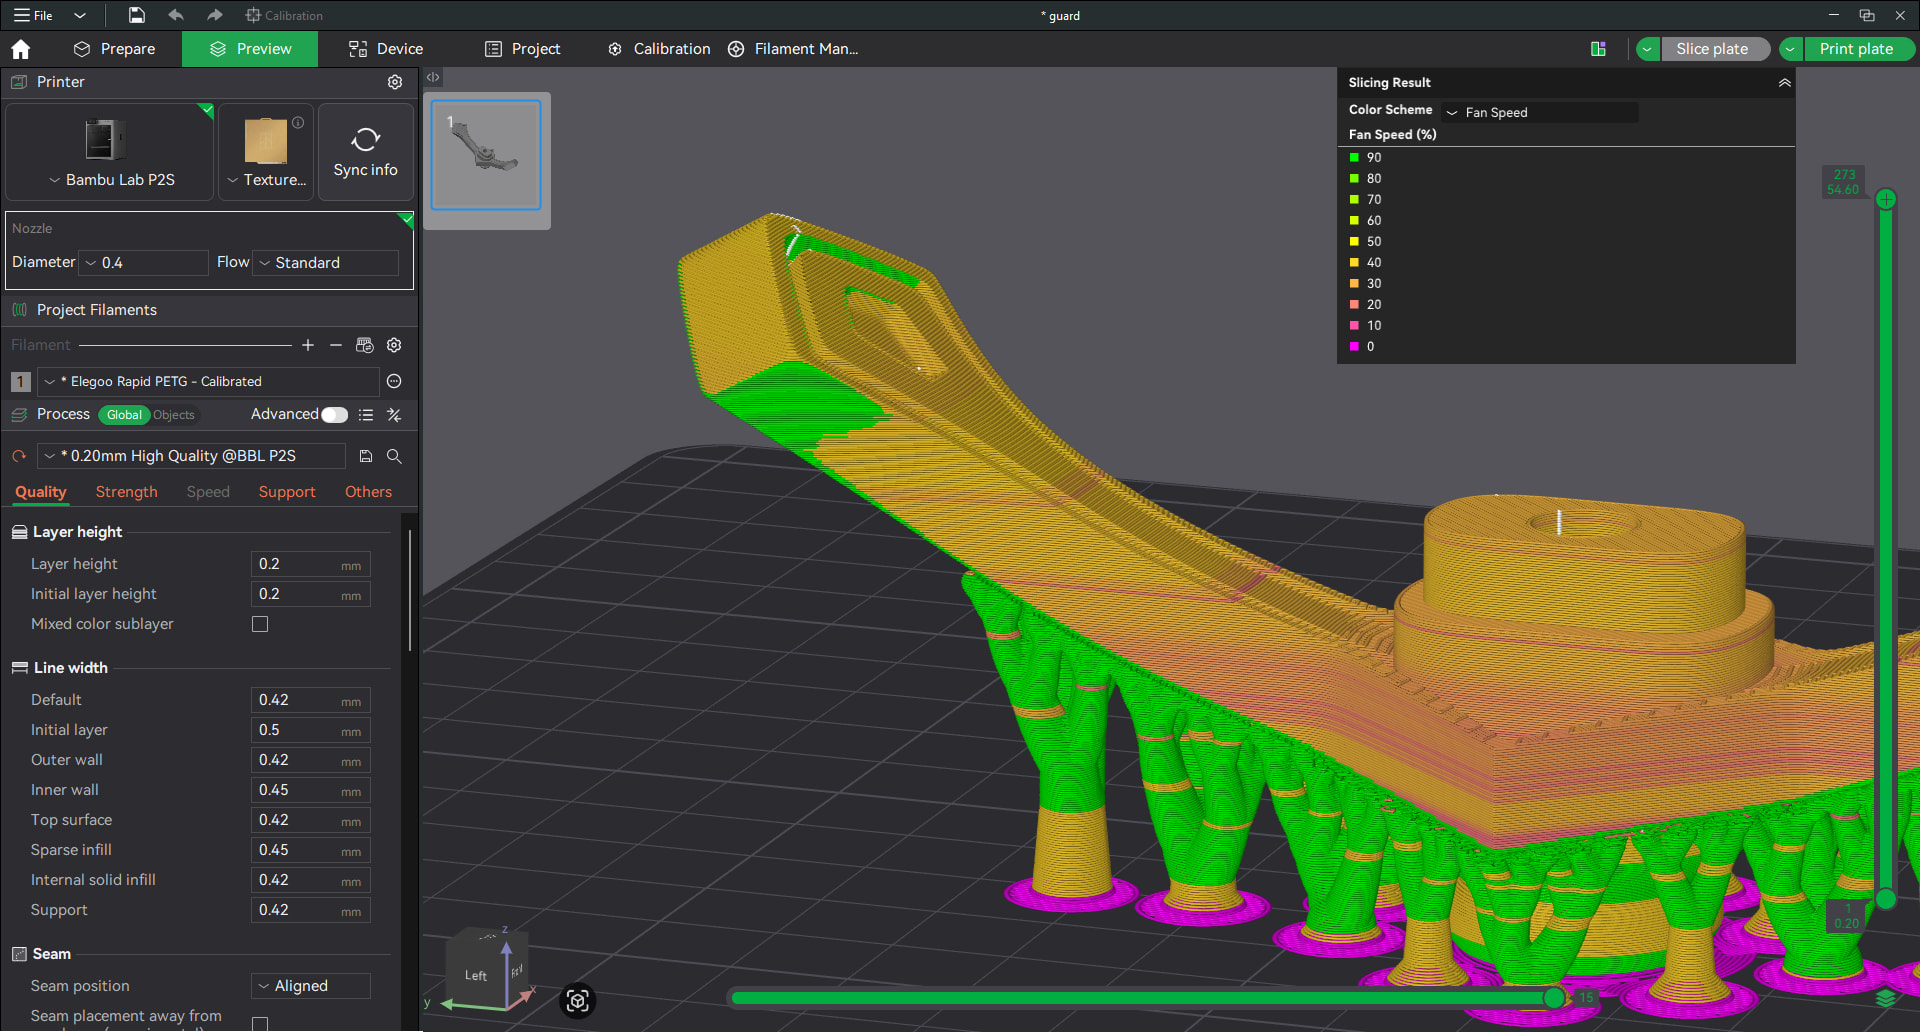
In Bambu Studio the overhang wall looks like this, and it prints the exact same plus the support, which I turned off so you can see what I mean.
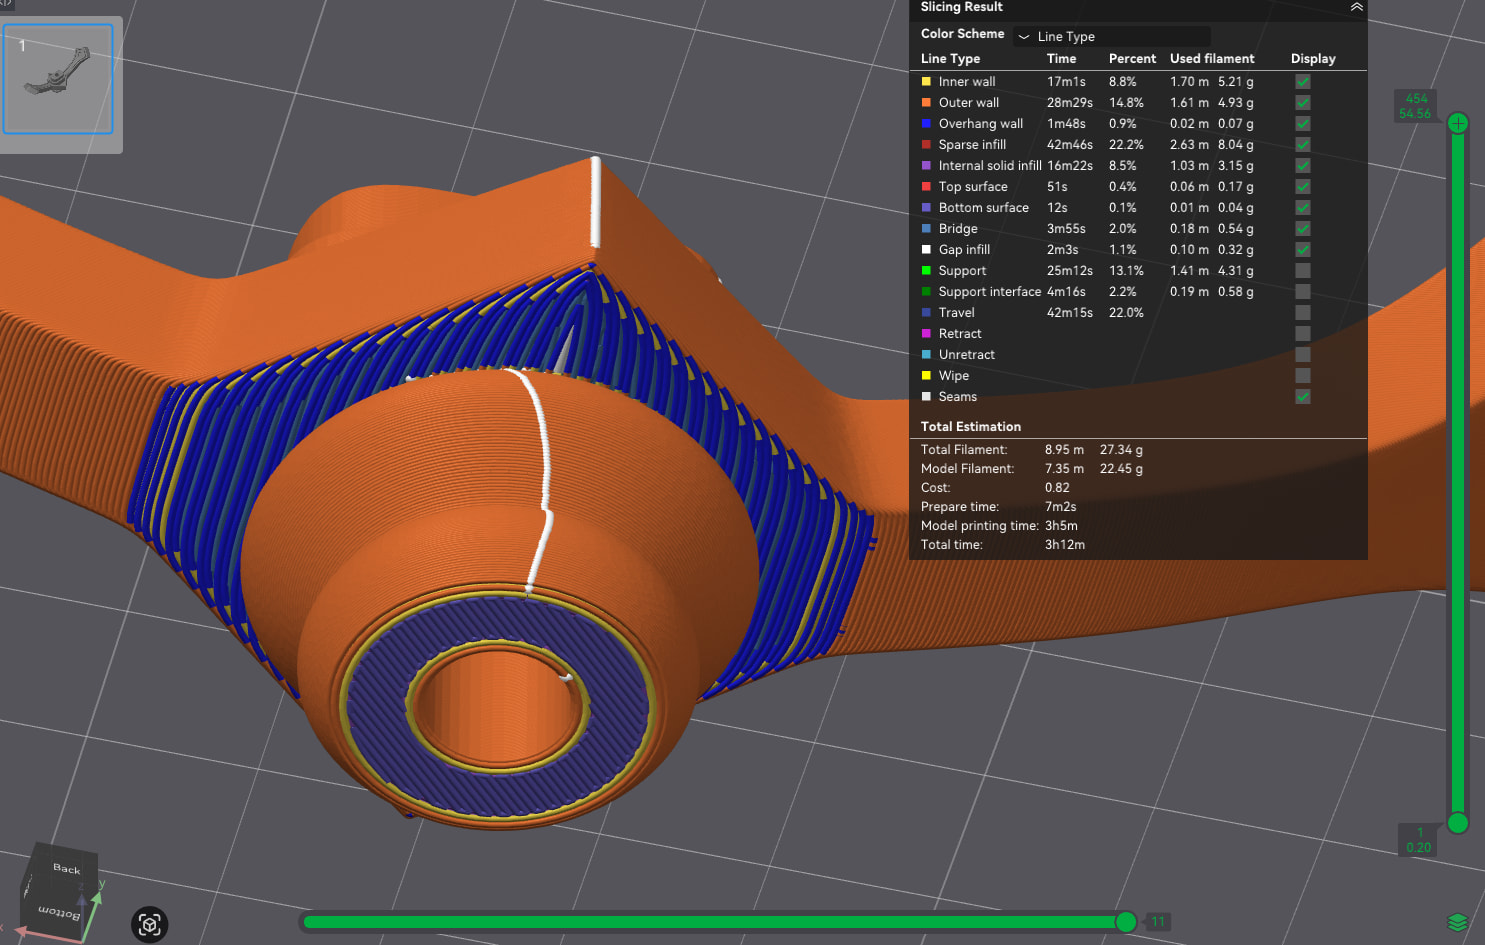
Right now I do not own an AMS, but I heard that the support can be a different interface with it thus the supported surface is better. I cannot get an AMS for the next few months, I plan to purchase one later, until then I would like to try and fix, or work around these issues if possible.
I’m using these printer settings below:
-
Bambulab P2S (without AMS)
-
0.4 Standard Nozzle
-
Textured PEI Plate
-
-
Bambu Studio
-
Elegoo Rapid PETG
-
I calibrated it through this video step by step
-
Flow ratio: 0.95
-
Plate temp: 70 C
-
Nozzle:
-
Initial layer: 240 C
-
Other layers: 240 C
-
-
Max volumetric speed: 8 mm/s (I started with 12 mm/s, then turned down to 8 mm/s)
-
Cooling min fan speed threshold: 20% (Layer time is 30s)
-
Cooling max fan speed threshold: 40% (Layer time is 12s)
-
Aux fan is completely turned off
-
Retraction length: 0.4mm
-
Z Hop when retract: 0.4mm
-
Z Hop Type: Spiral
-
-
0.12mm High Quality BBL P2S preset
-
Turned on Avoid crossing wall
-
Adjusted Sparse infill density to 25% from 15% (for the extra strength so it’s not brittle)
-
Turned down Bridge speed from 50mm/s to 20mm/s
-
Turned on Support
-
Changed Reduce infill retraction to Disabled
-
The filament has been in the dryer for over 40 hours now at 65 C, and it’s turned on even while printing. The dryer is a Creality Space Pi.
I prefer to print this in PETG because of the better heat resistance (it is for a cosplay), so I’m ready to cry and pray in the corner if that’s the best solution out there.