Hi everyone,
Looking for some more advice. I have been using Inland Brand Petg+ tranlucent and clear varieties and running into similar issues. When printing things that need a large amount of smaller supports for intricate details I’m running into issues where the supports are adhering to the bed fine and for many layers into the print the supports are fine. But eventually the supports get broke off from the part or bed by the nozzle due to some possible blobbing and the supports begging to get sloppy. Has anyone else had this experience and what did you do to over come it. My petg experience is limited and I’m still learning this filament. I’m using the stock bambu translucent petg profile with a custom adjusted temp range for 255 for the initial layer but 250 for others. This is based off the temp tower test I did with the bambu settings to adjust for best print. I am drying at 55c in my AMS heater from Sunlu and print while drying.
The nature of PETG is low viscosity when melting but sticky (to nozzle inside and outside) so that retract does not completerly suck up cleanly the plastic before next movement. To reduce blob built up ouside of nozzle, I suggest doing a few things:
- Underextrude a little bit, like flow rate 0.94 is perfect, then you should go with 0.92 or 0.90
- Increase retract length a bit more, like 0.8mm to 1.2mm or 2mm
- Increase cooling and lower a bit of nozzle temp
- Wipe nozzle frequently
But beware that, PETG has the highest layer to layer bonding thanks to its lower vicosity compare to PLA or ABS. So that, increase cooling and lower nozzle temp can help it keep shape and form a bit but it also can reduce layer to layer bonding drastically.
With underextrusion a bit, there is less excess material that the nozzle can pickup to form blobs outside of nozzle, but it could lead to voids or gaps on top surface.
The dye they put in PETG could change viscosity a little bit so that there would be less blobs and you might need to slightly change of flow rate.
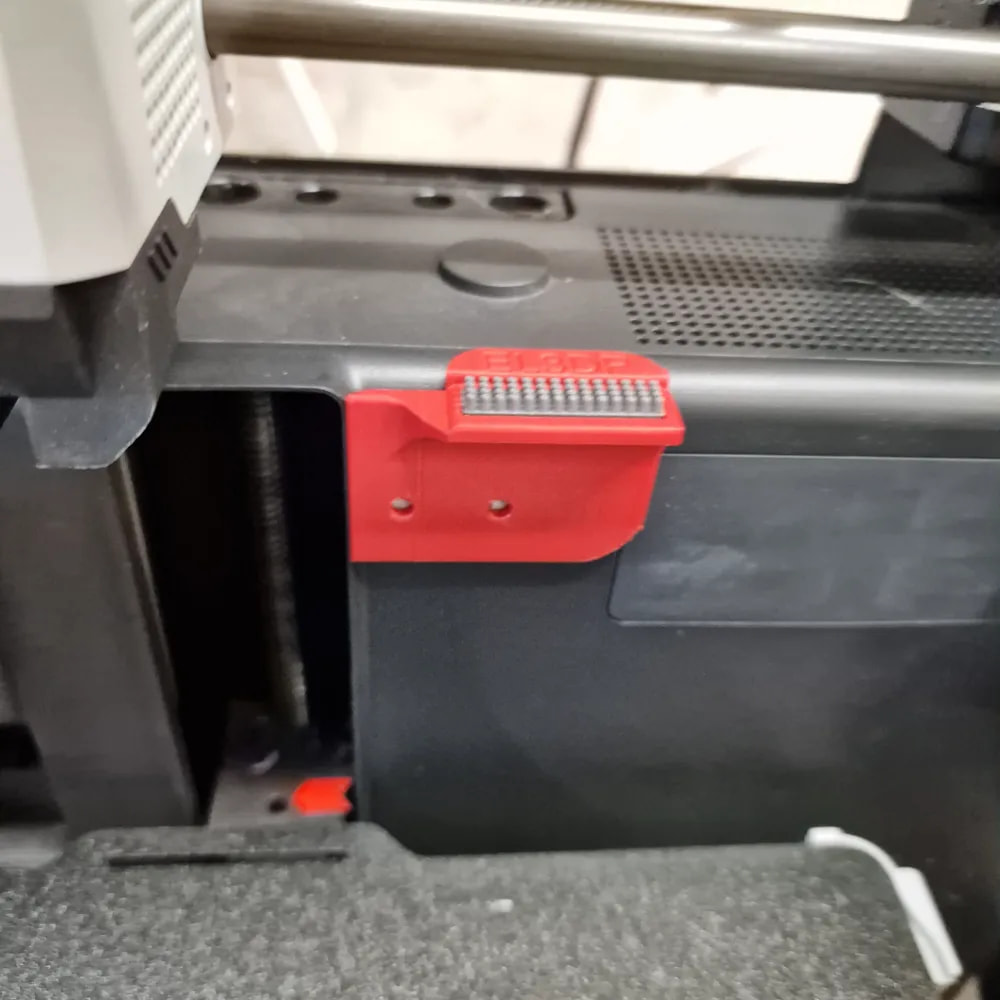
You might need to add extra gcode for nozzle wiping for every layer and use some 3rd party solution like this community solution
Edit: add link
https://makerworld.com/en/models/1025501-steinwipe-nozzle-wiper-for-x1-and-p1-series#profileId-1050795