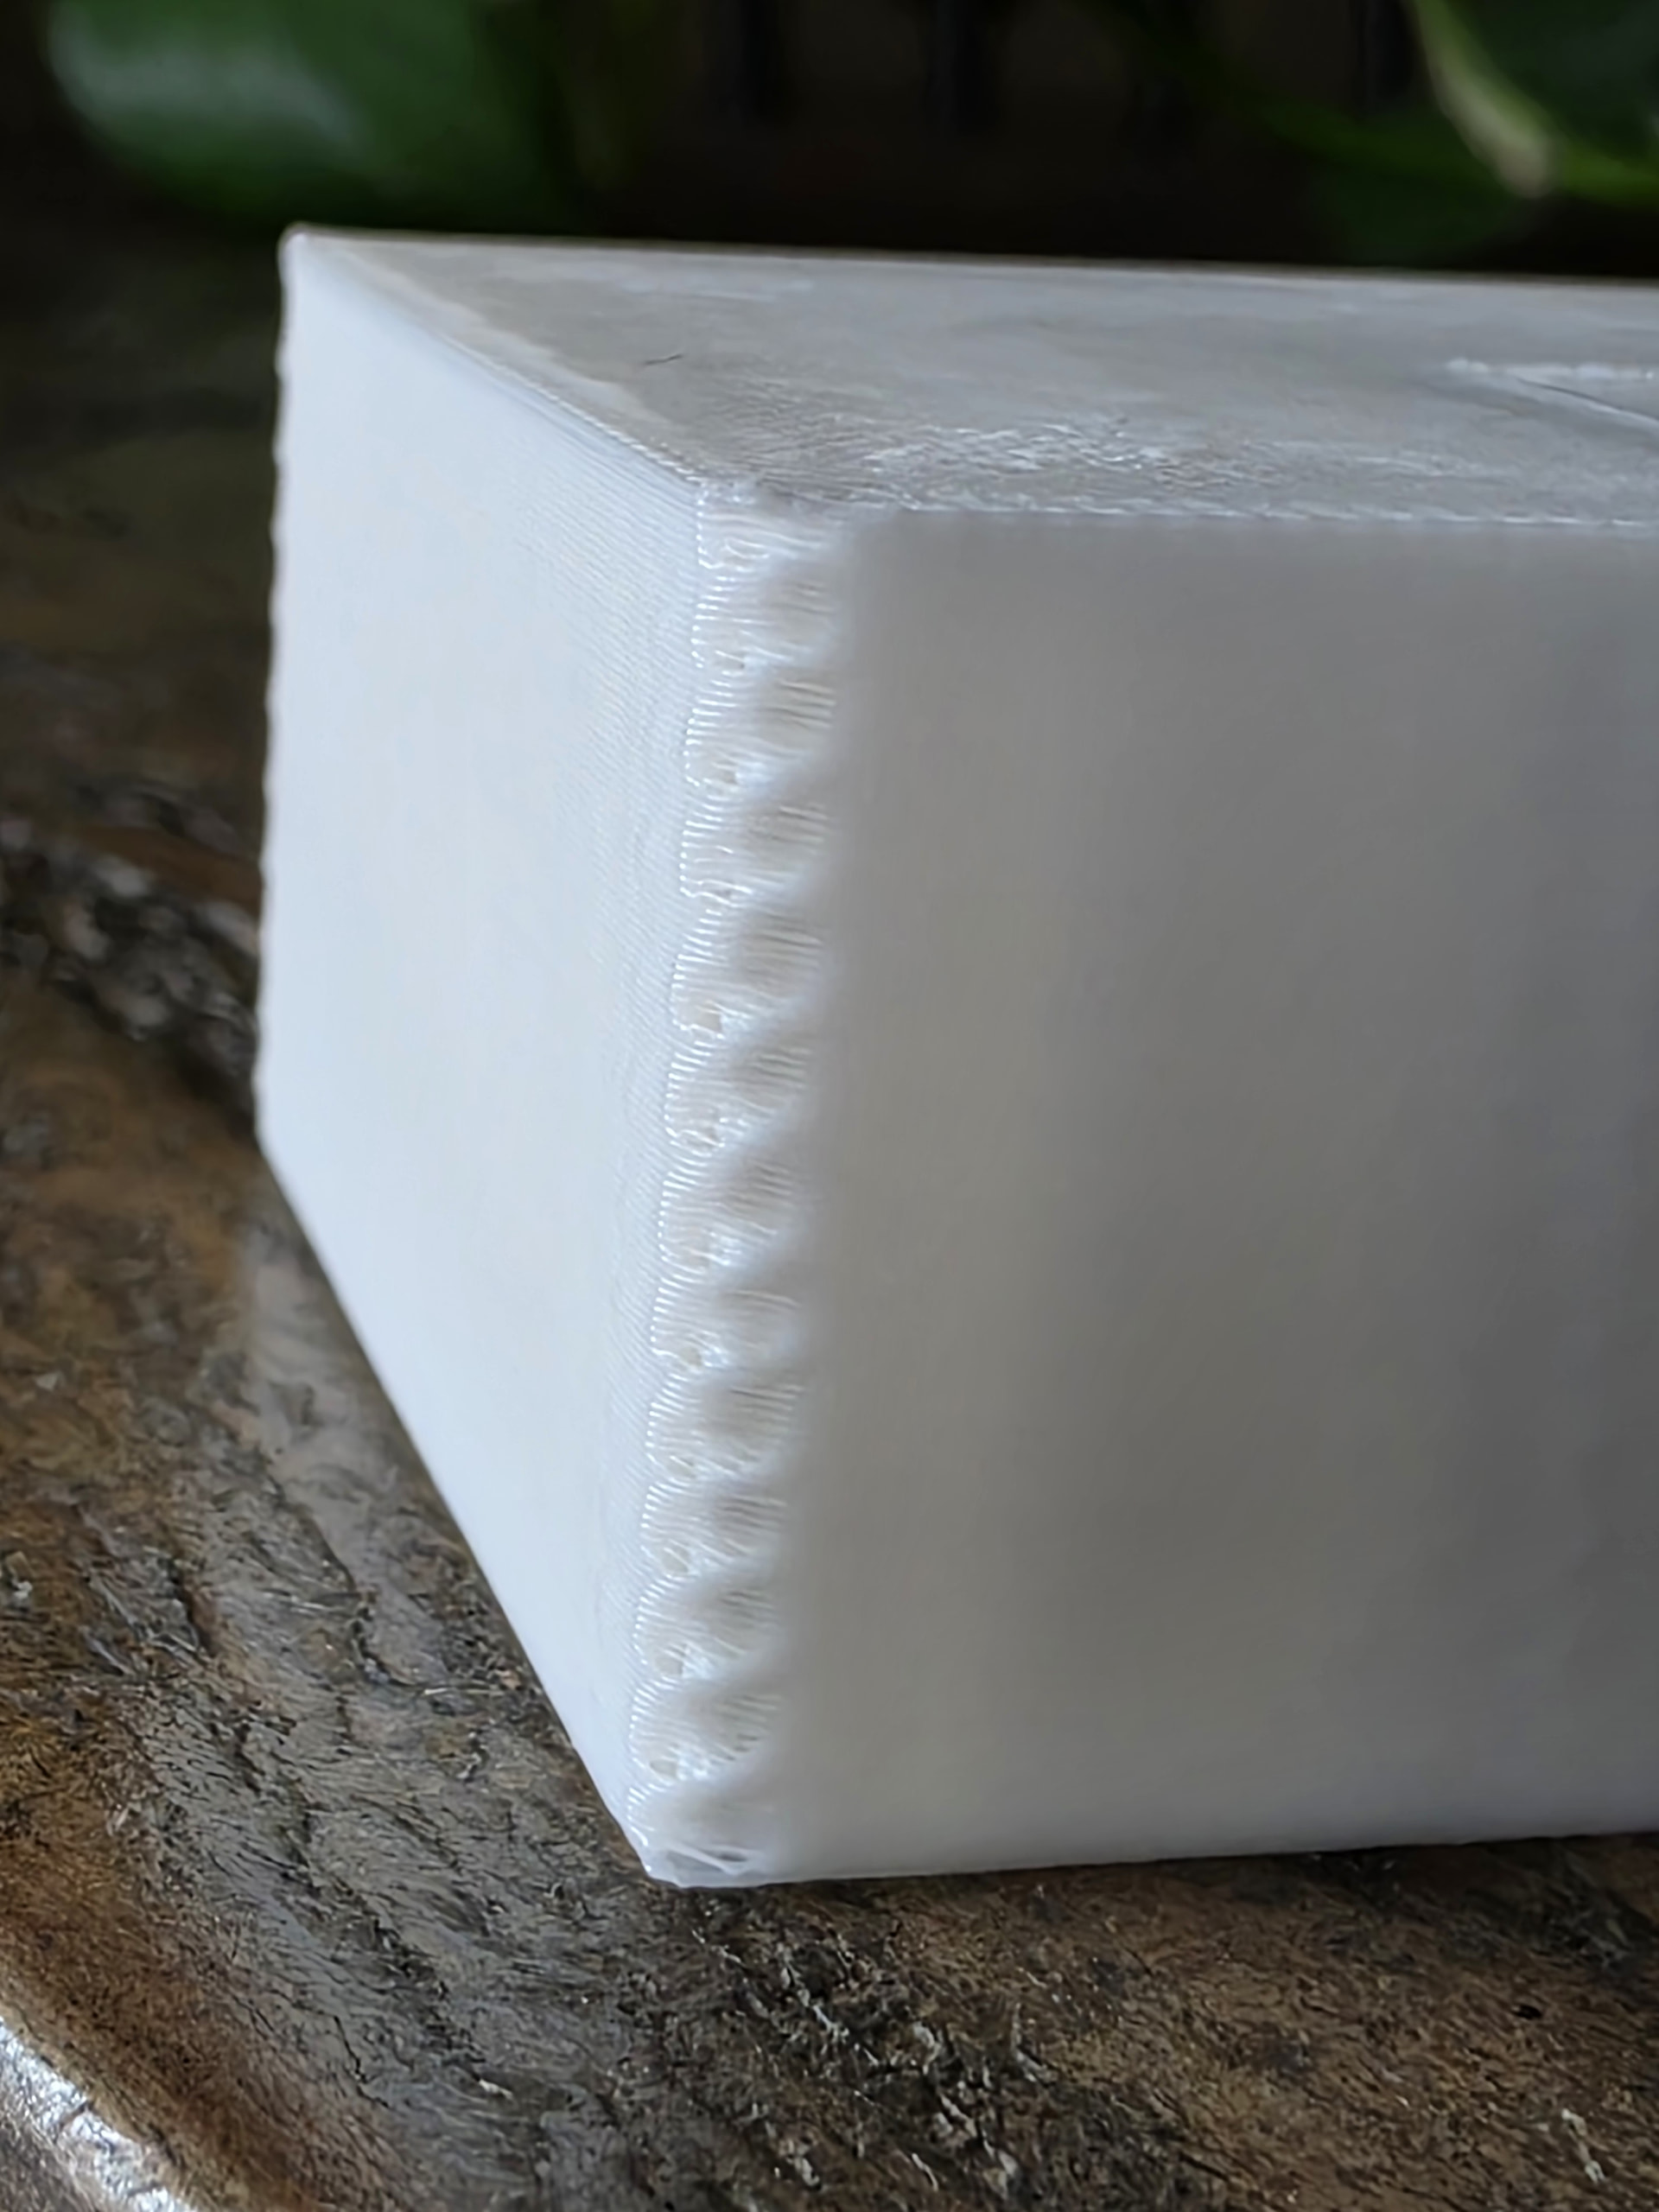
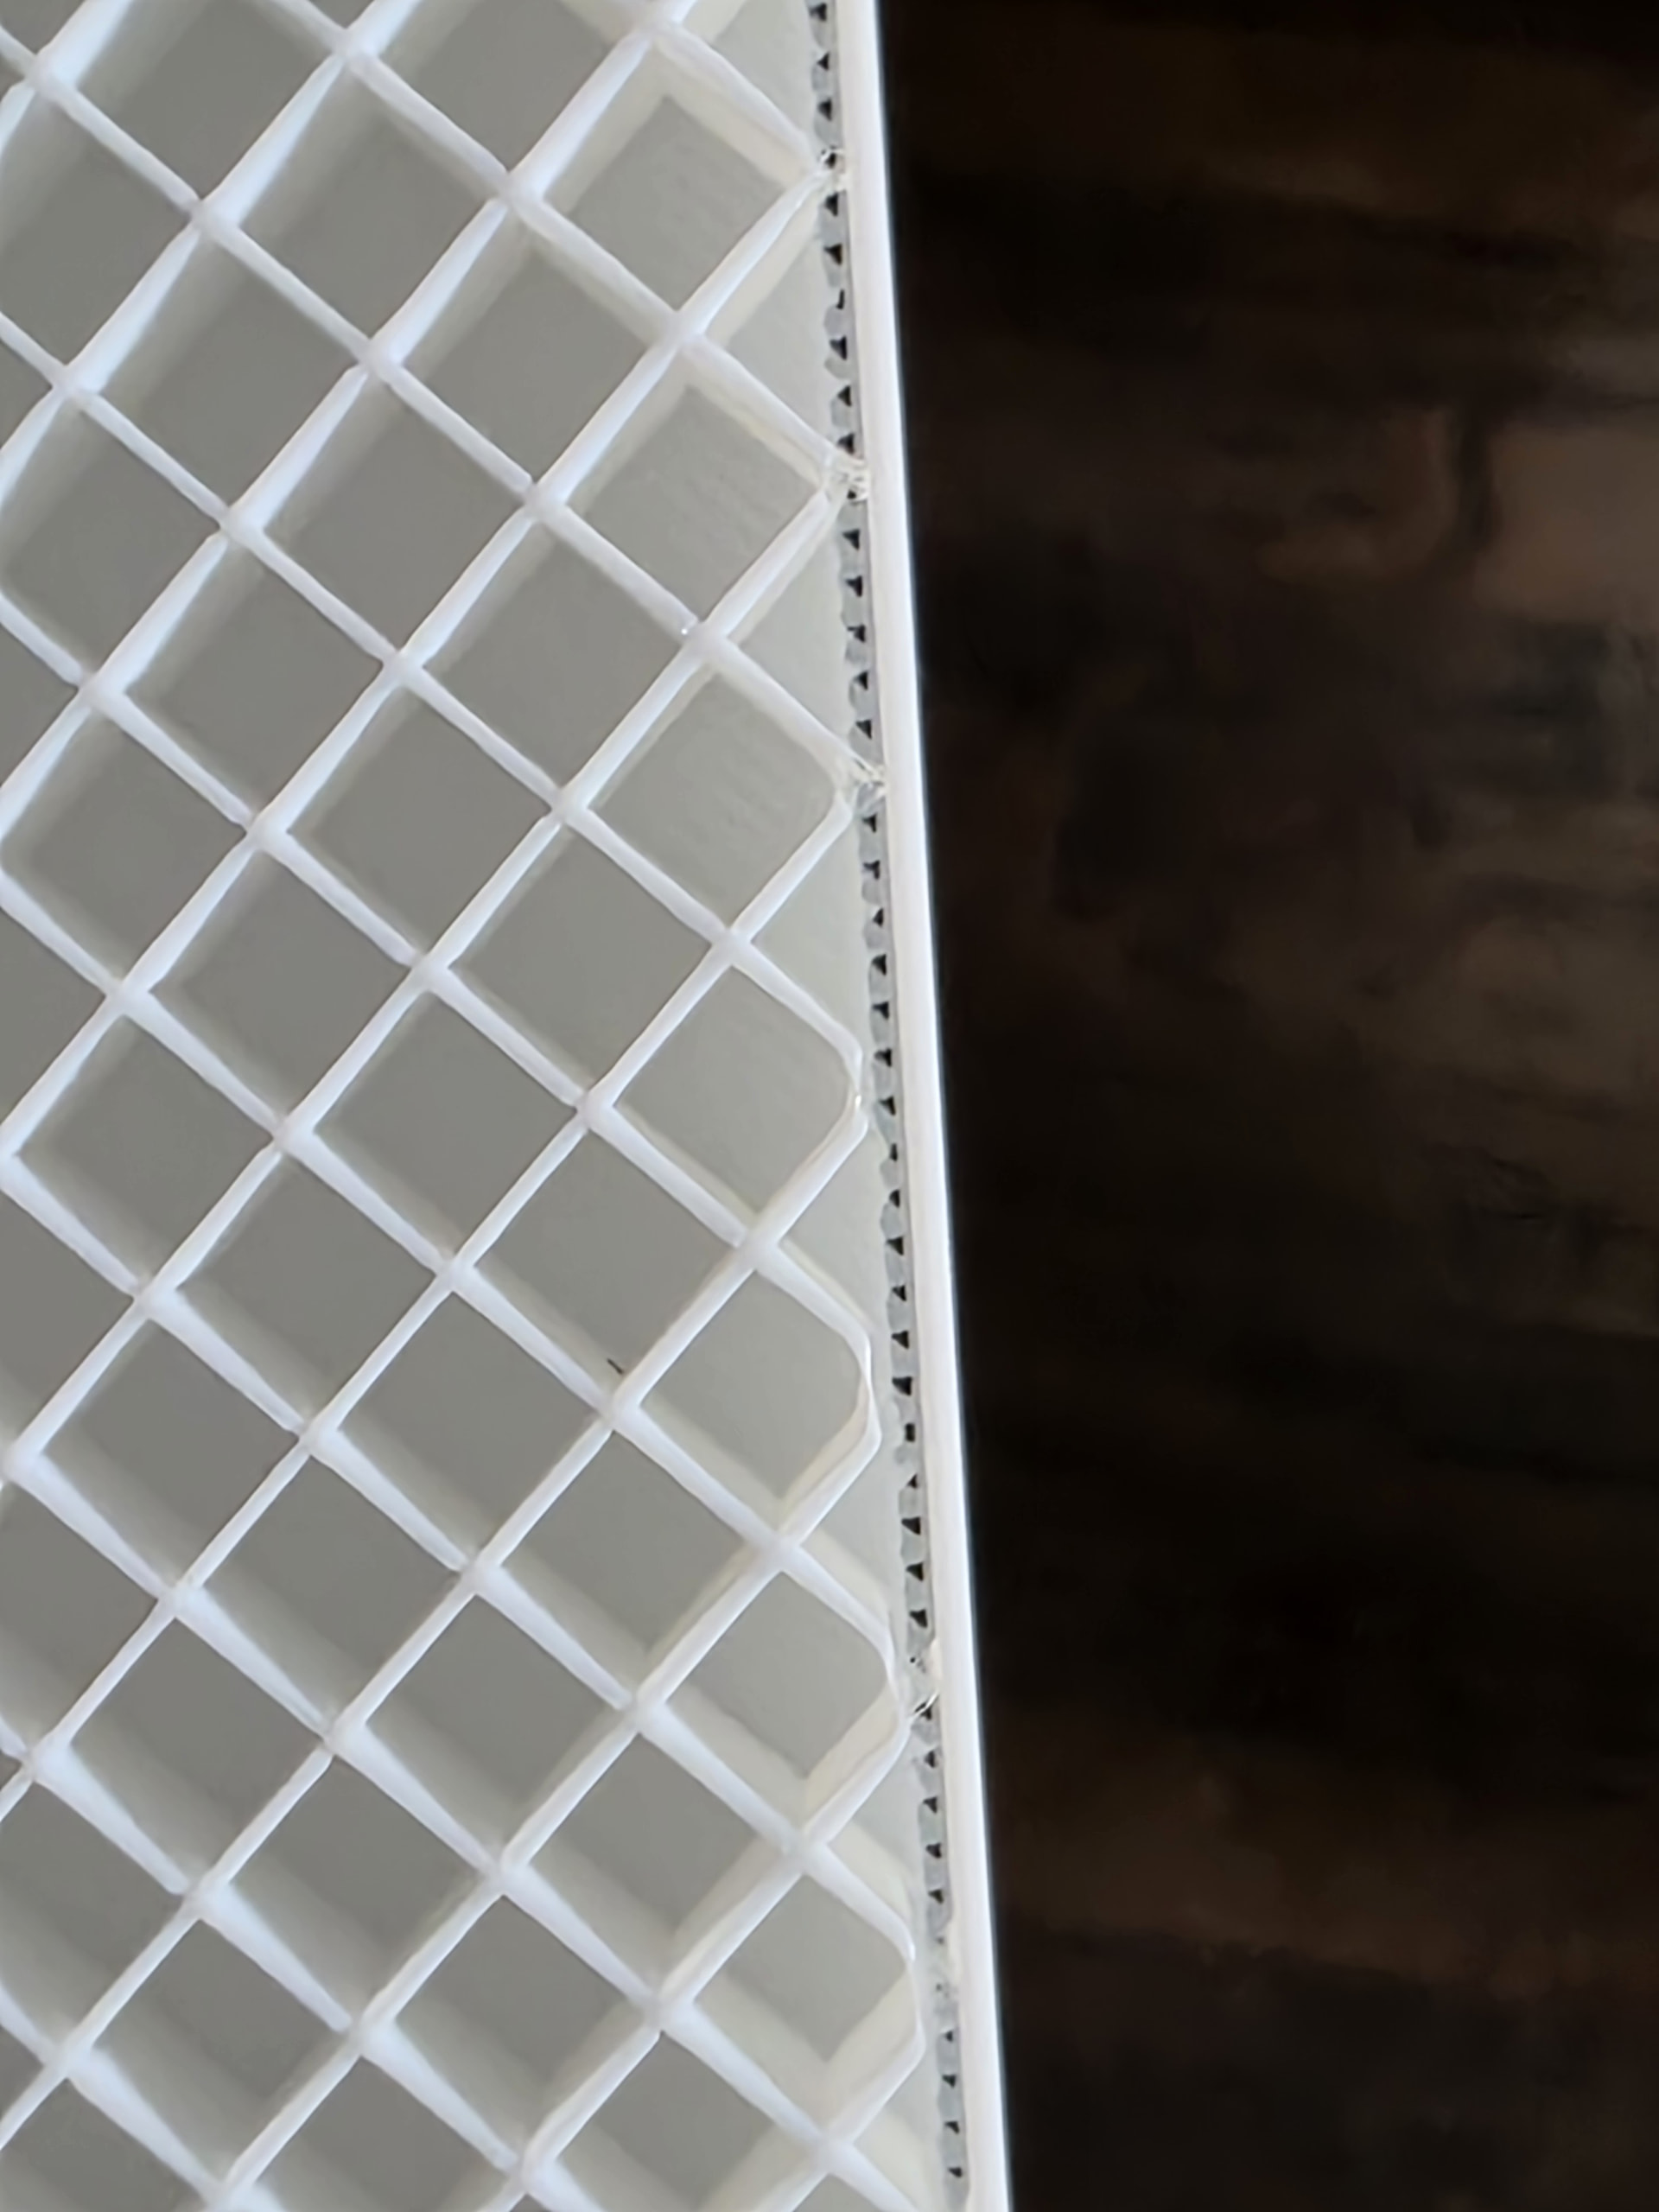
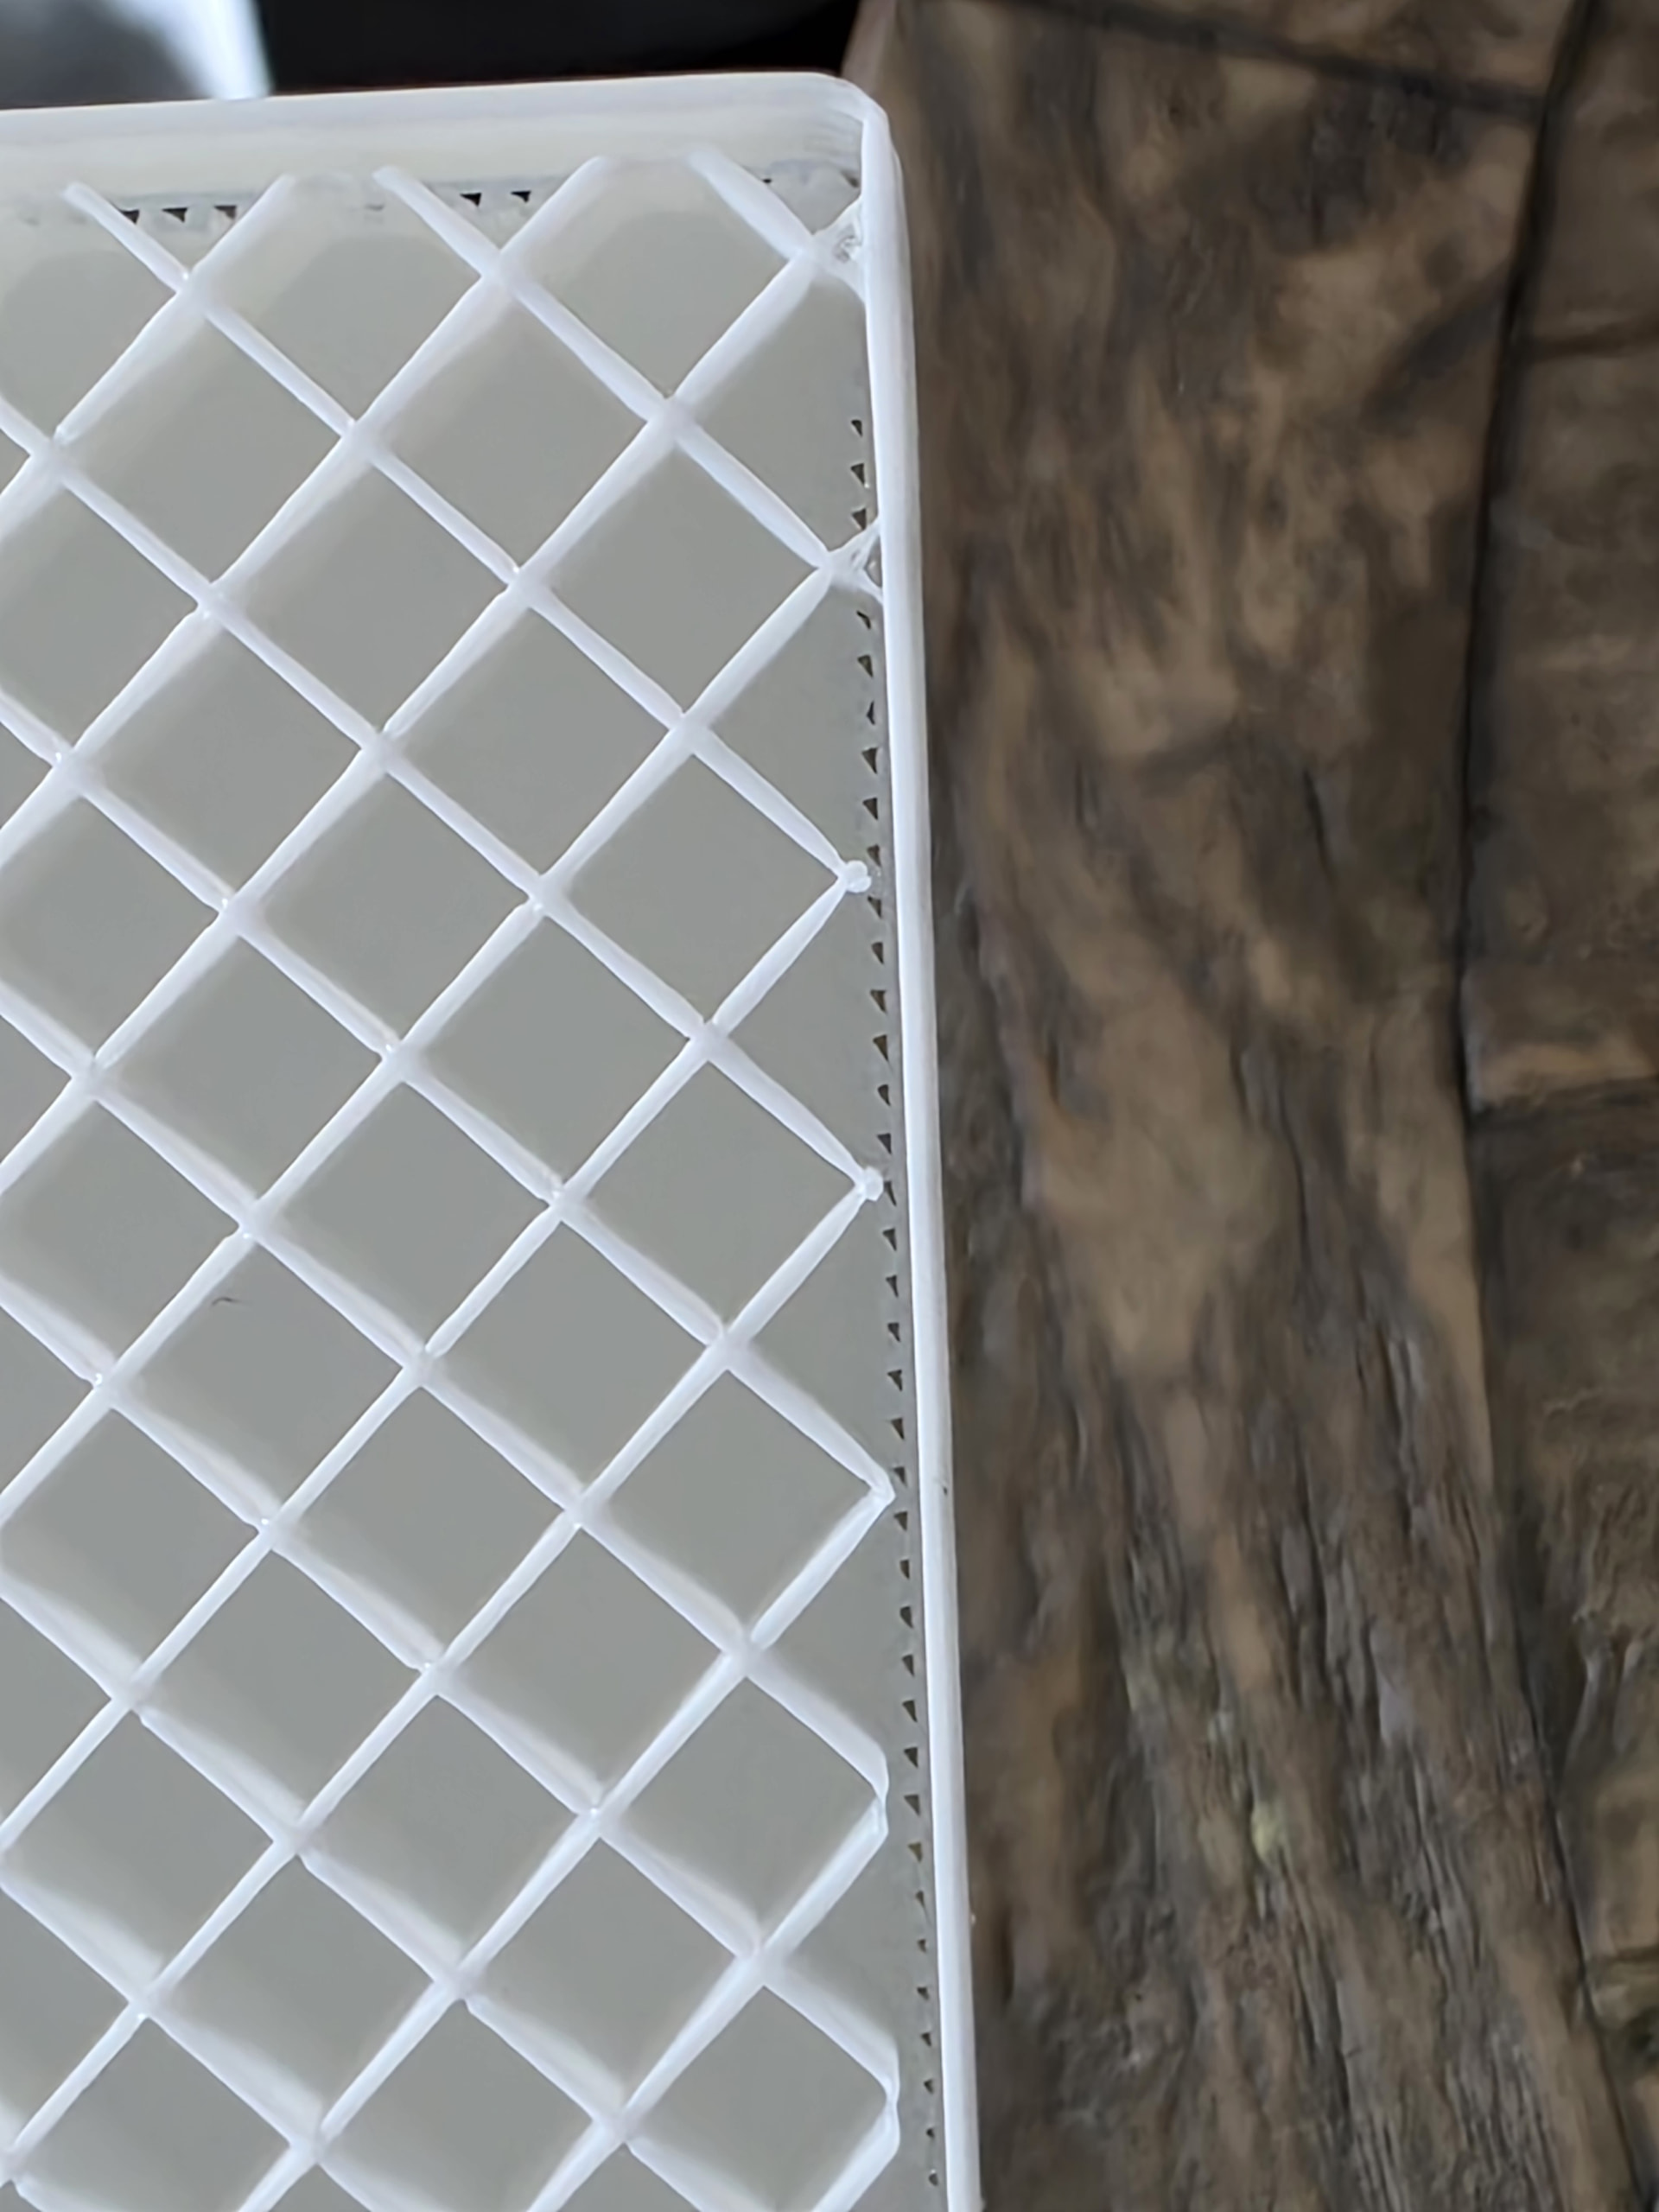
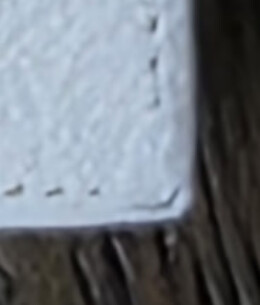
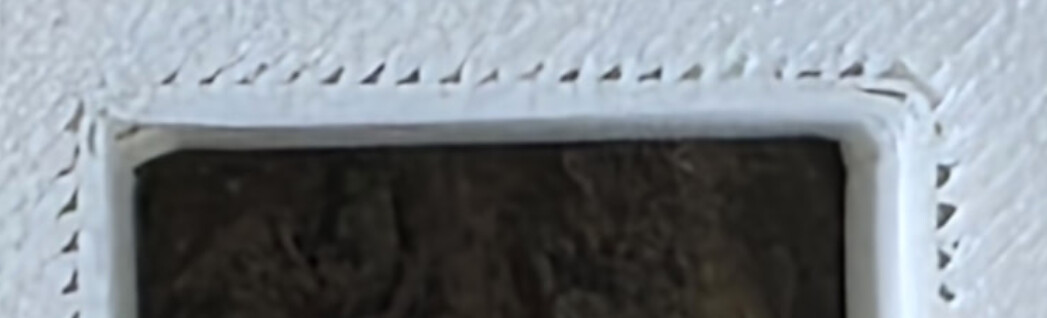
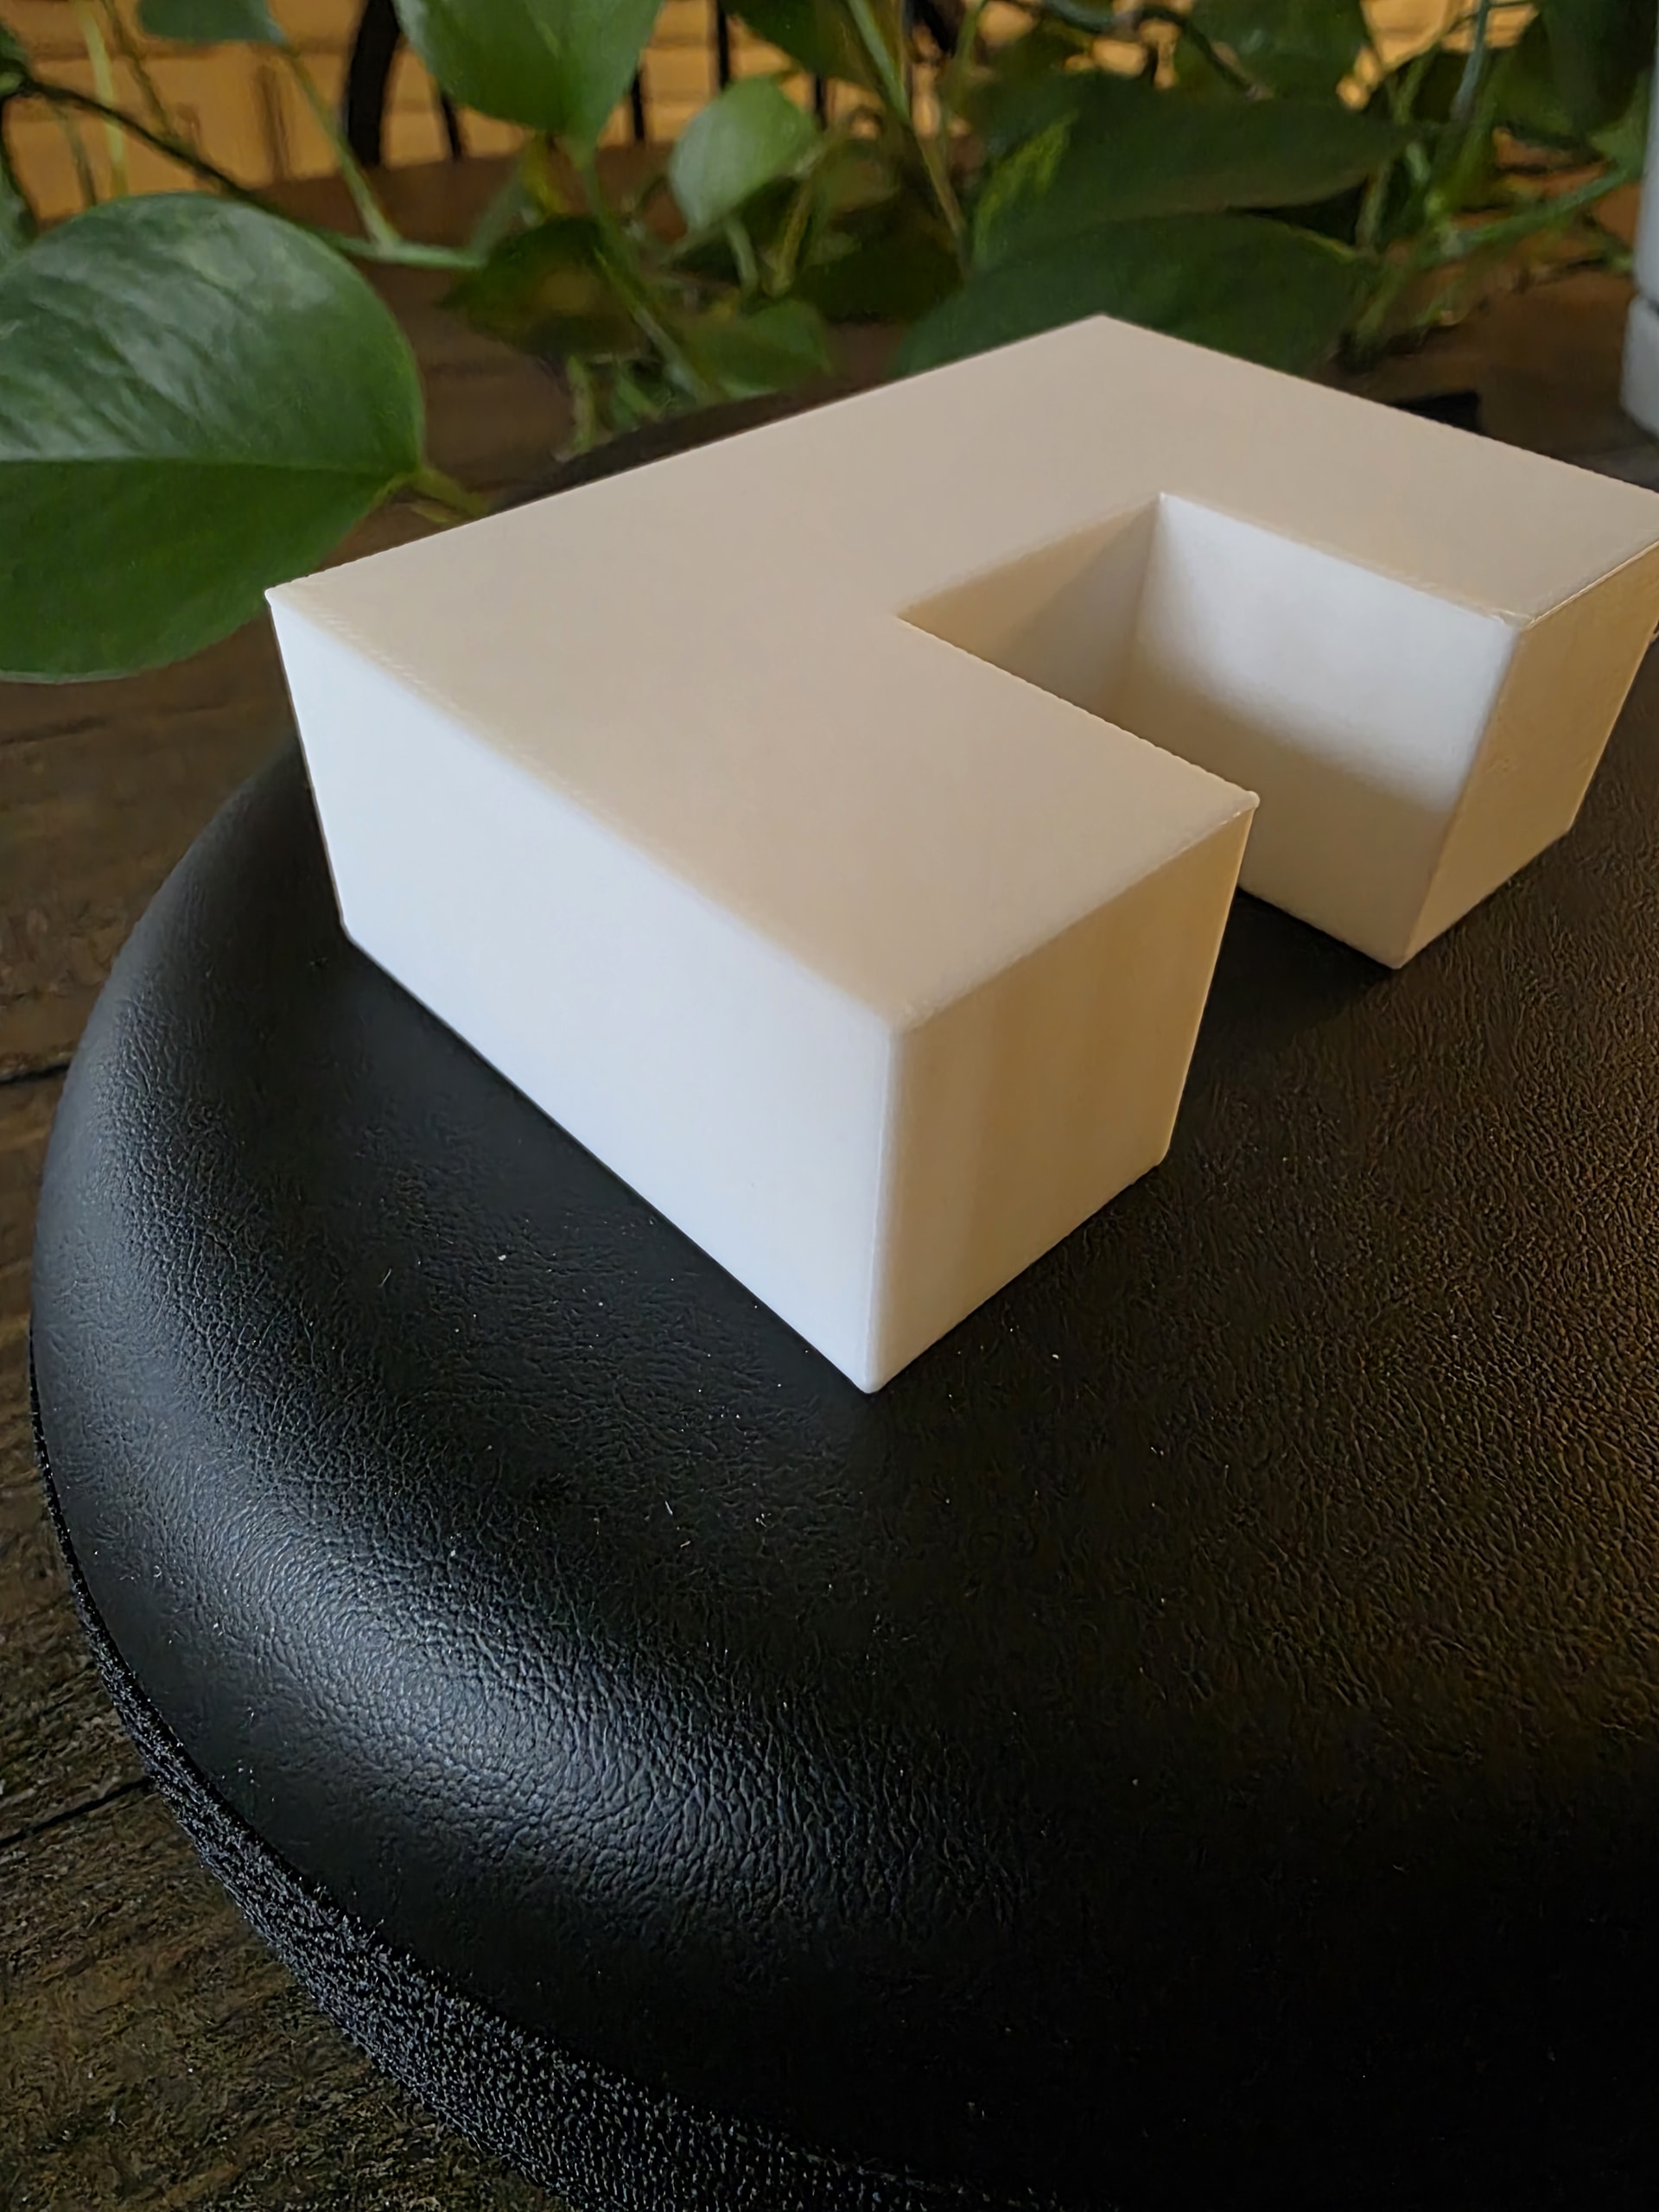
Pretty new to printing so I appreciate any information that would help…I have a P2s that initially printed without any issue. After a few months every print started to fail due to extreme stringing. I swapped the nozzle and that fixed the stringing, but now I am getting a consistent print error around corners (see pictures)…also it appears that the infill isn’t going all the way to the outer wall of the print (See pictures).
I was able to print this file prior to swapping the nozzle without the infill or corner error. Any input on how to fix this would be appreciated.
When the stringing started I read that it could be moisture so I bought new PLA and had the same issue…the issue resolved itself after I swapped the nozzle. The print error I have now is with corners and infill not going all the way to the walls (see pictures above)…those errors have been since nozzle replacement.
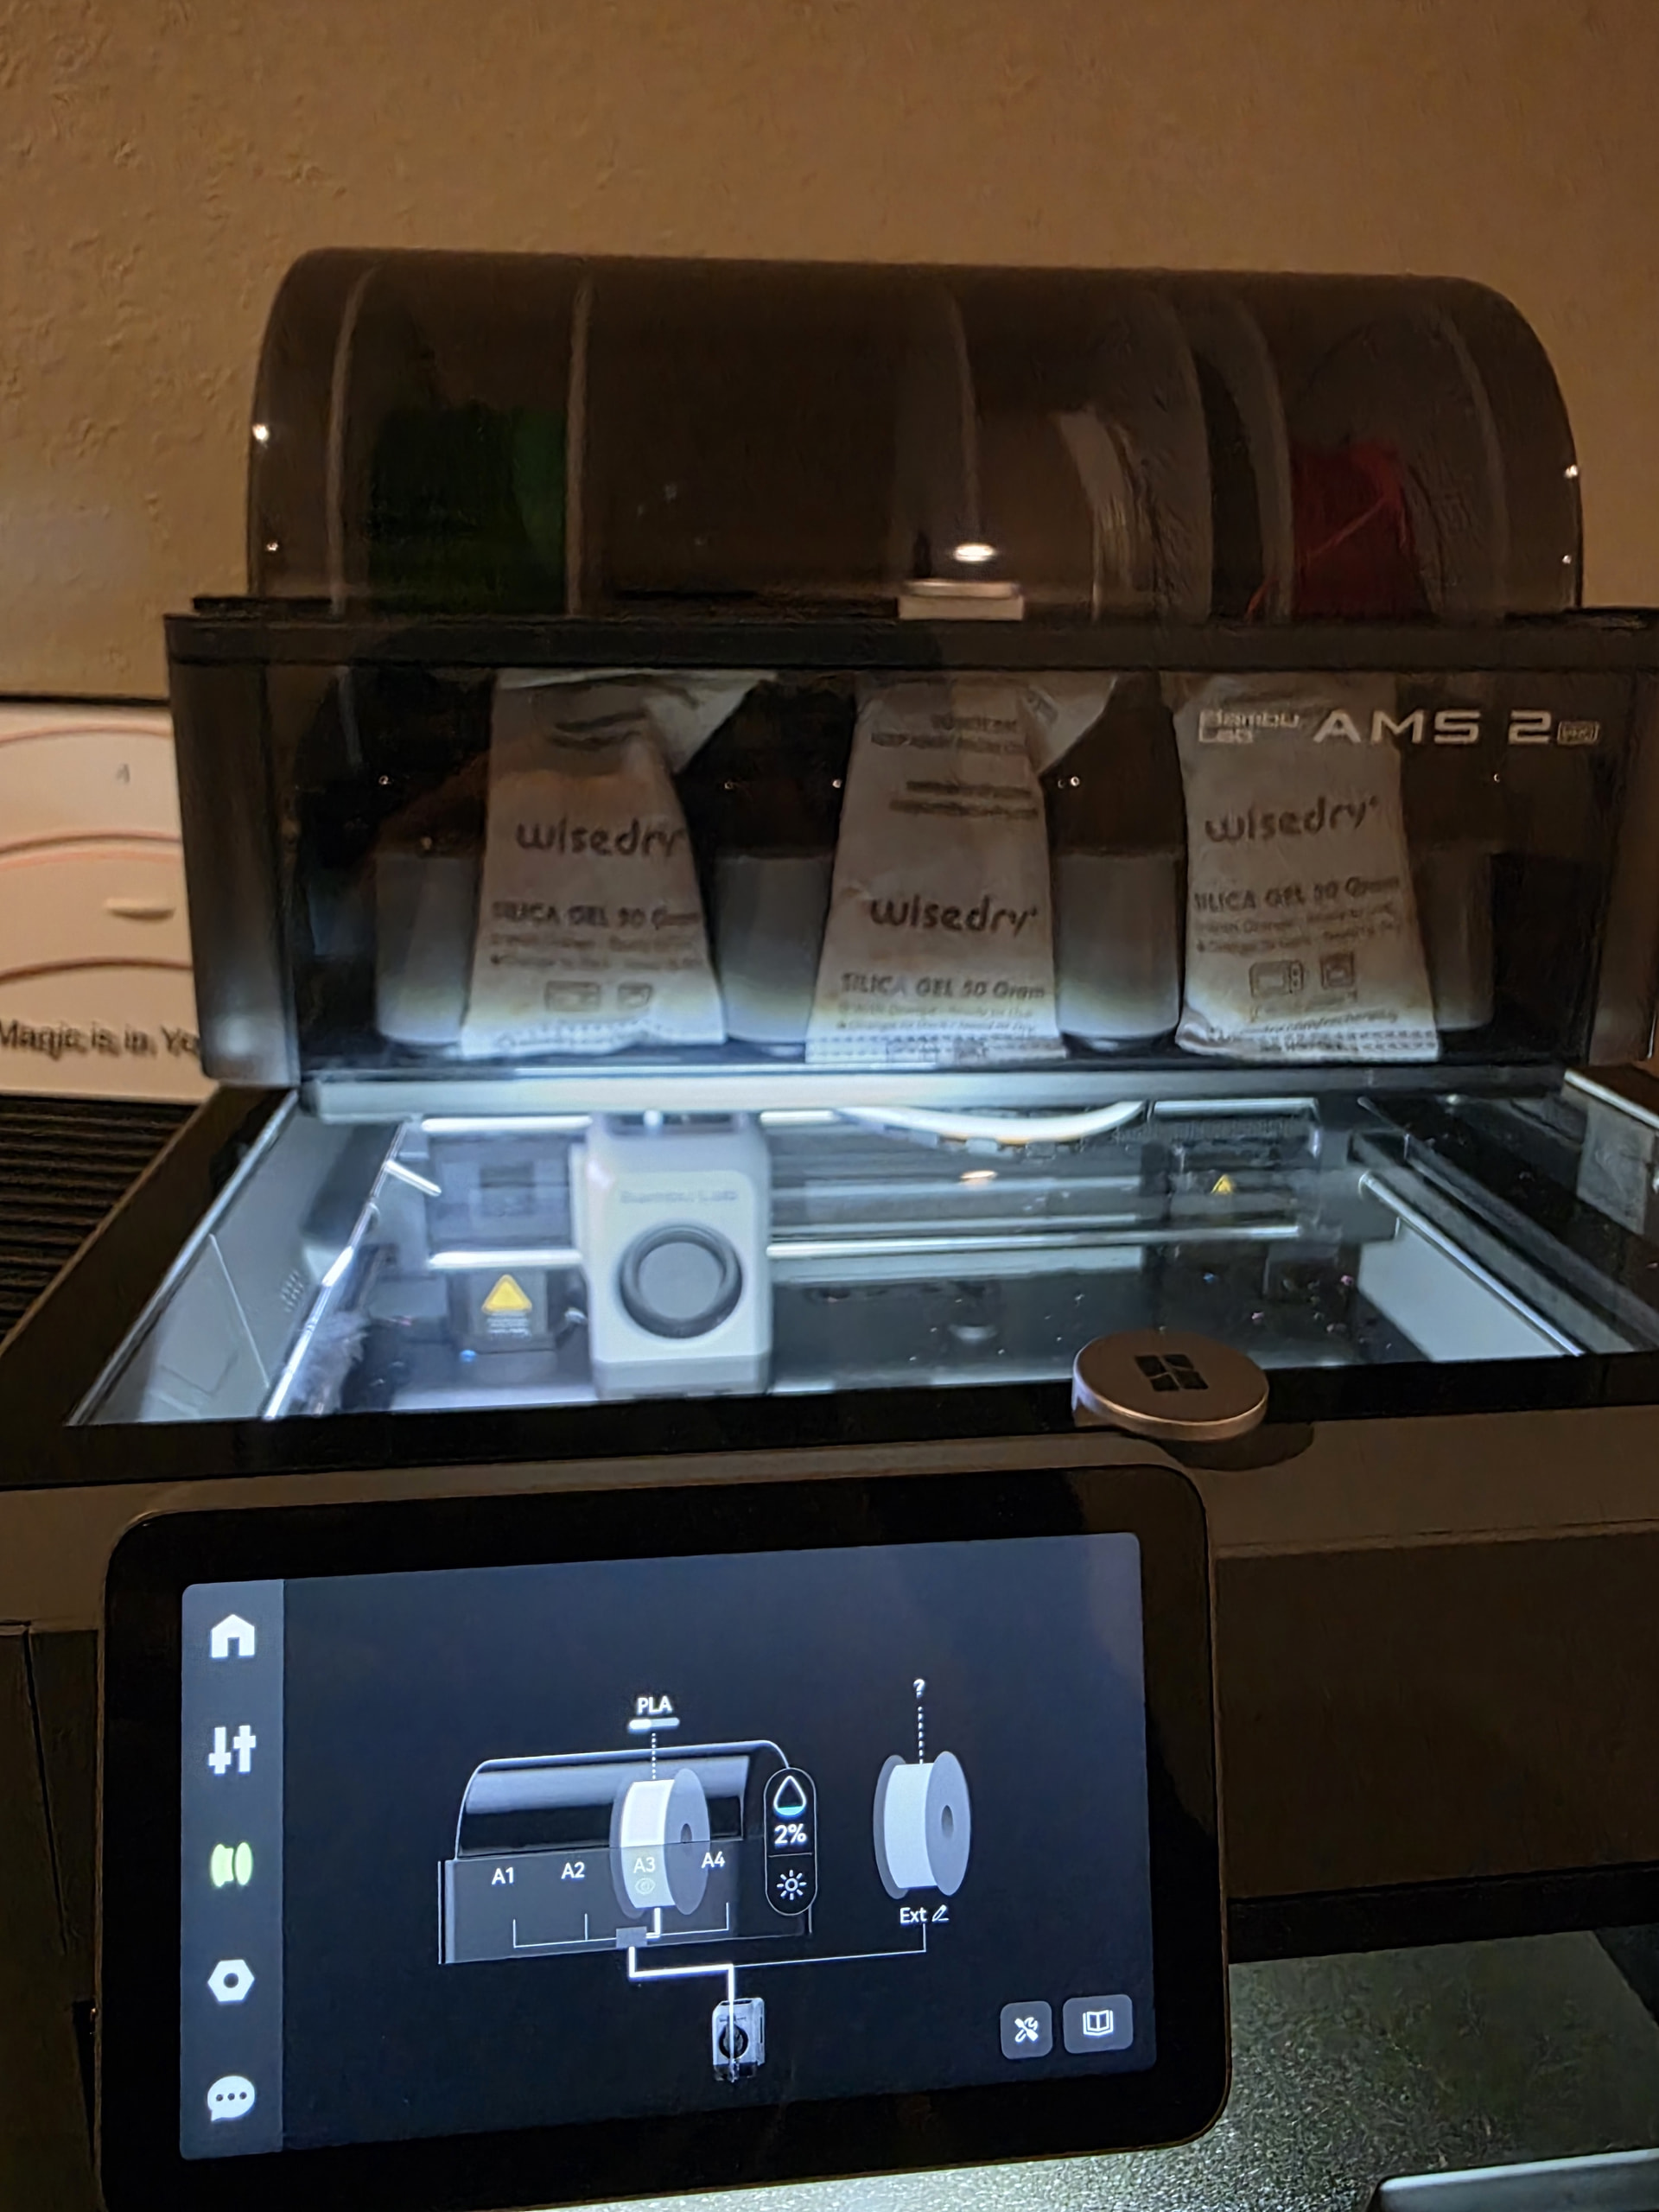
An AMS2 with silica gel packs is a huge double-edge sword.
If you don’t monitor humidity carefully they can go from water scavenger to water source especially when the AMS2 is in drying mode.
What you want to do is take the silica gel and filament out of the AMS2 and see what humidity it can dry to empty. Read the AMS2 humidity value.
Put the silica gel back in and read the AMS2 humidity again once the beads have had a chance to warm up. If the humidity is now higher, it’s past time to regenerate the beads.
If the humidity goes up when you put the beads back in (no filament), the beads are actually crippling the performance of the AMS2. If the humidity drops from the no-bead and empty AMS2 when the beads are at drying temperature, then they are helping.
As to the print issues, I’m not familiar with water doing what you’re seeing but it’s hard to say. Thing is, my own water issues also grew in over time when spring raised humidity. I had a number of good months of good prints over the winter (ours are very dry) but spring brought humidity and I had steadily decreasing print quality right into failures until I got drying sorted. If your humidity has recently been increasing, that would possibly point to water but I can’t really say from your photos. Stringing can be a sign of water though.
Thanks for the info I did assume they were dry when new. Do you think the current issue is am having is due to moisture?..It only happens on corners and I am not having stringing issues.
Hard to say but I’ve seen people discuss these kinds of things when the extruder is loose. Is it possible when you changed the nozzle that somehow during that the extruder or nozzle wasn’t tightened properly?
Only on corners with a change in direction could also point to something loose? Not sure though. It just seems kind of like the symptoms others have discussed.
It doesn’t look like anything I’ve seen from water though. I just brought up the beads in the AMS2 thing since they can be a problem if people don’t keep them dry. Silica gel holds far more water than filament or air and if it gets too much water content built up can wreck performance of any active dryer.
But some symptoms you mentioned before changing the nozzle sounded like minor water symptoms but since changing the nozzle fixed that, it’s hard to say one way or the other about water.
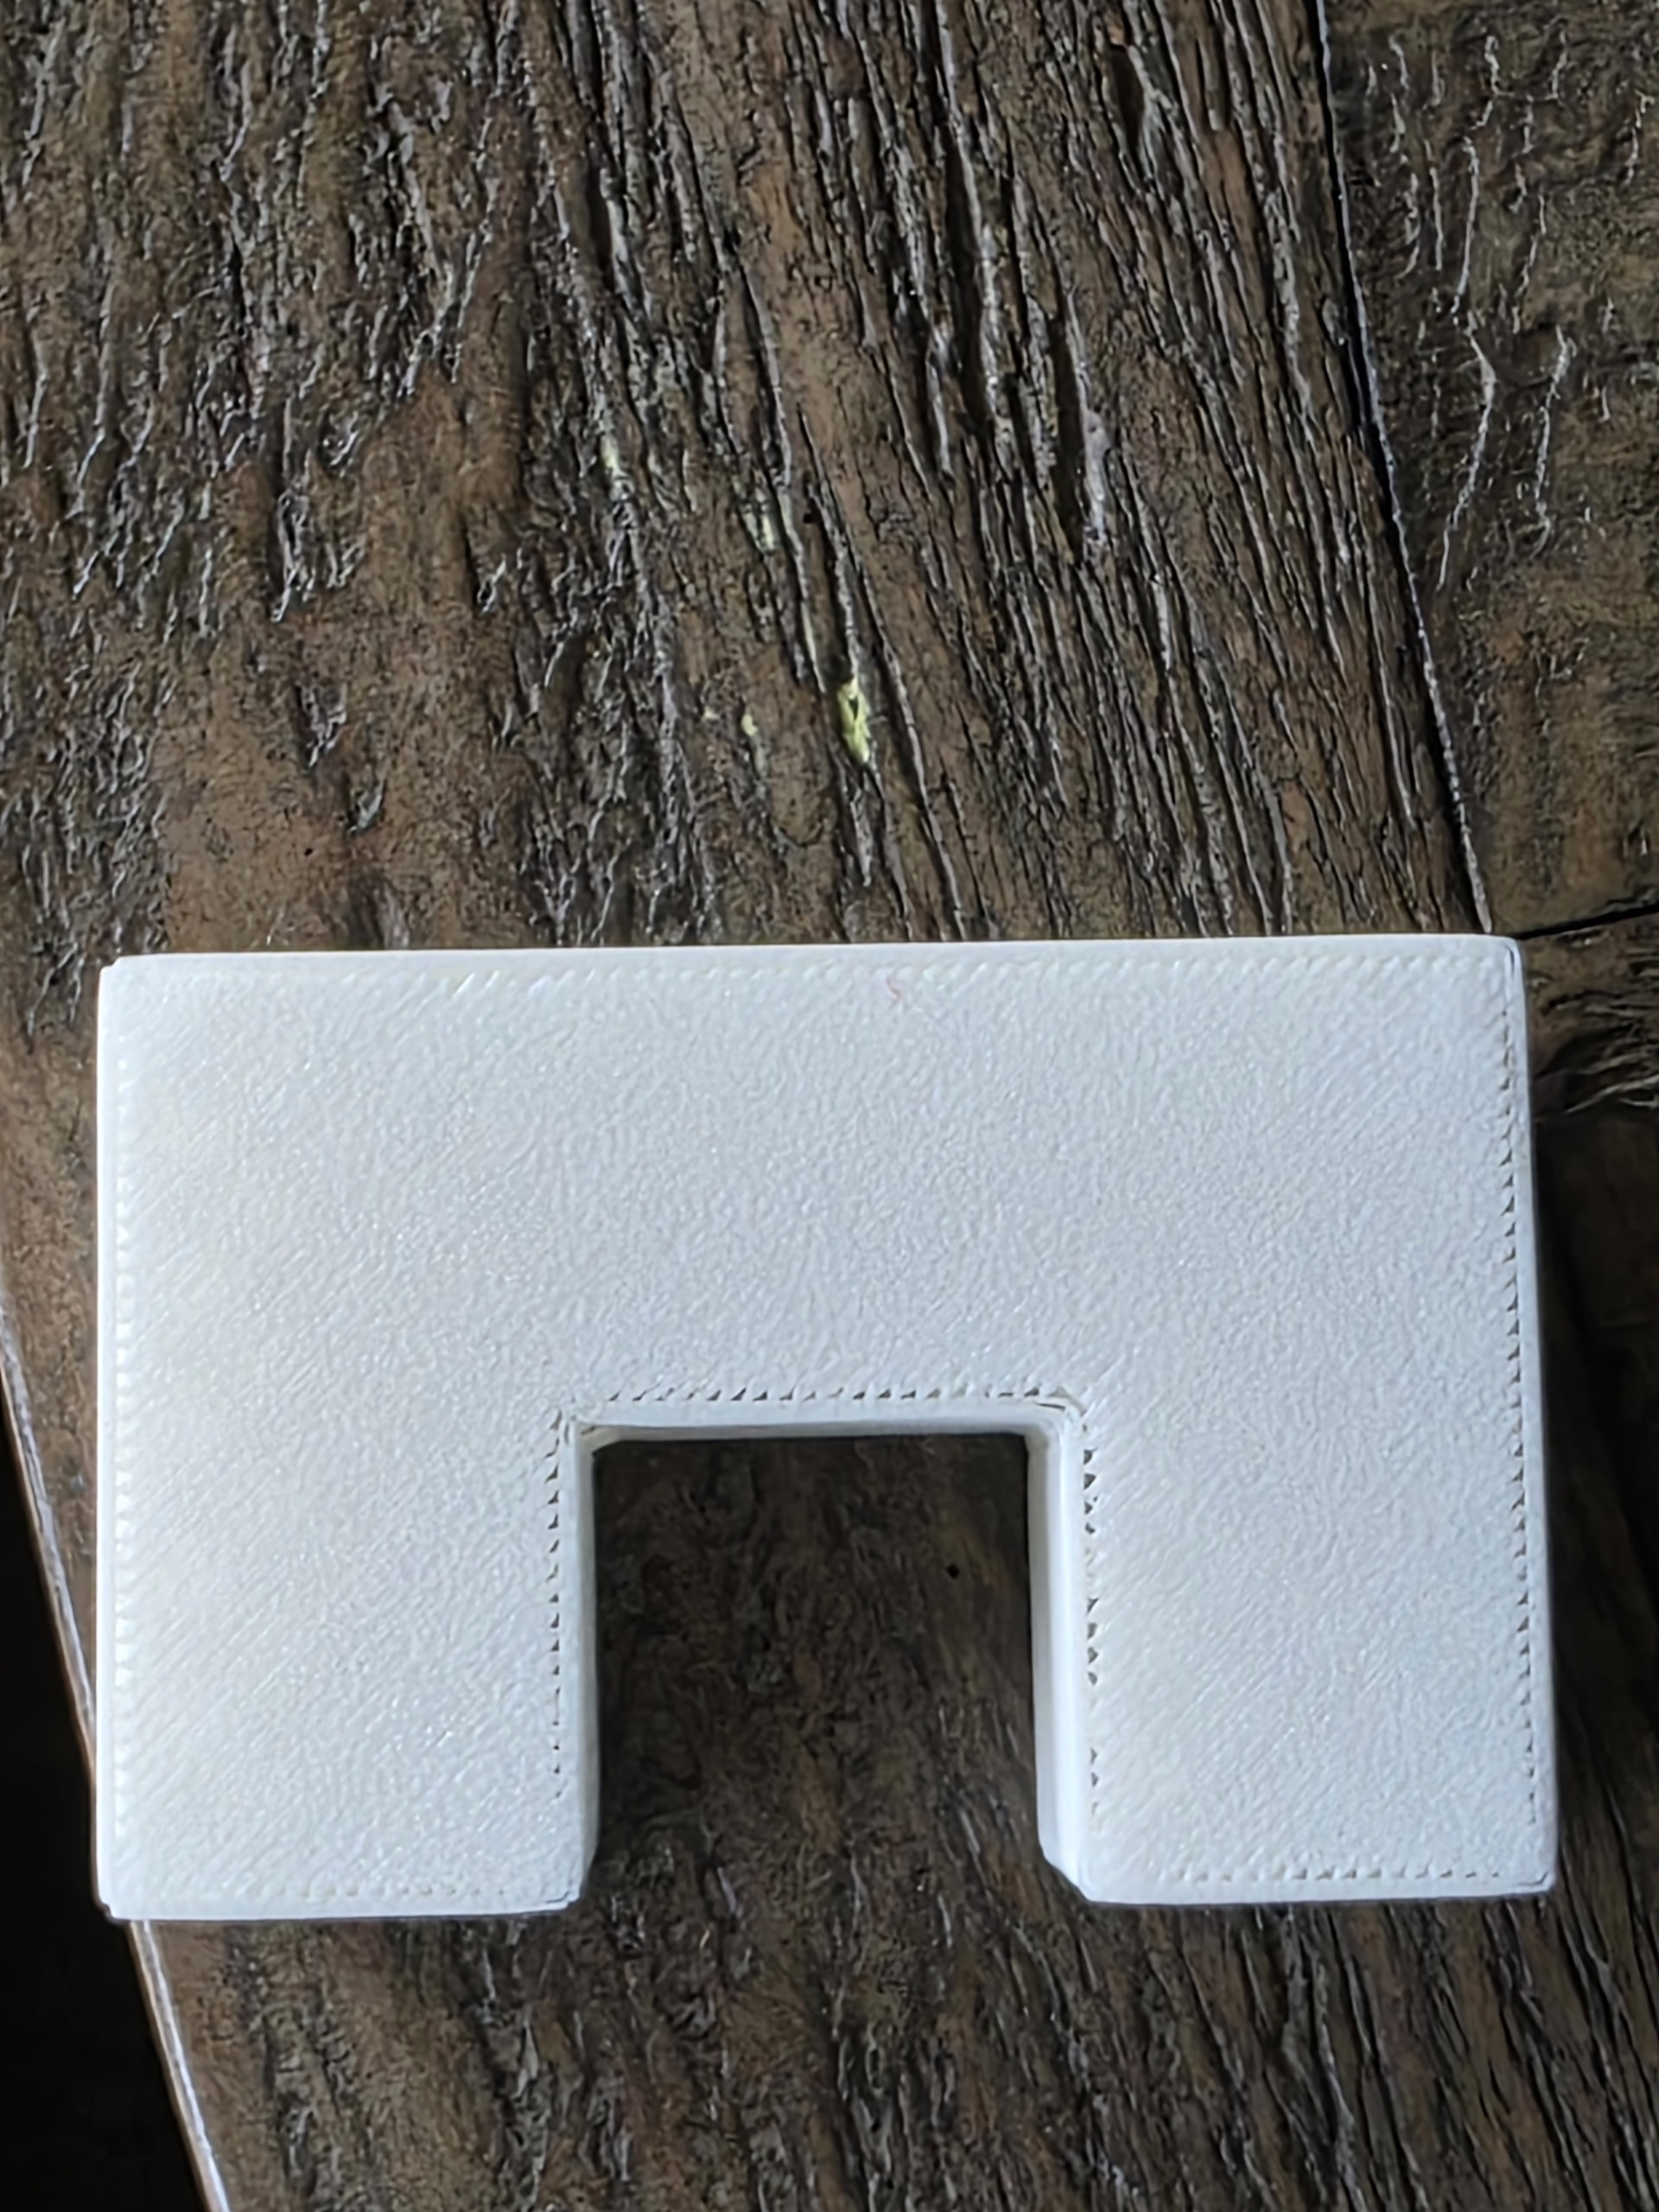
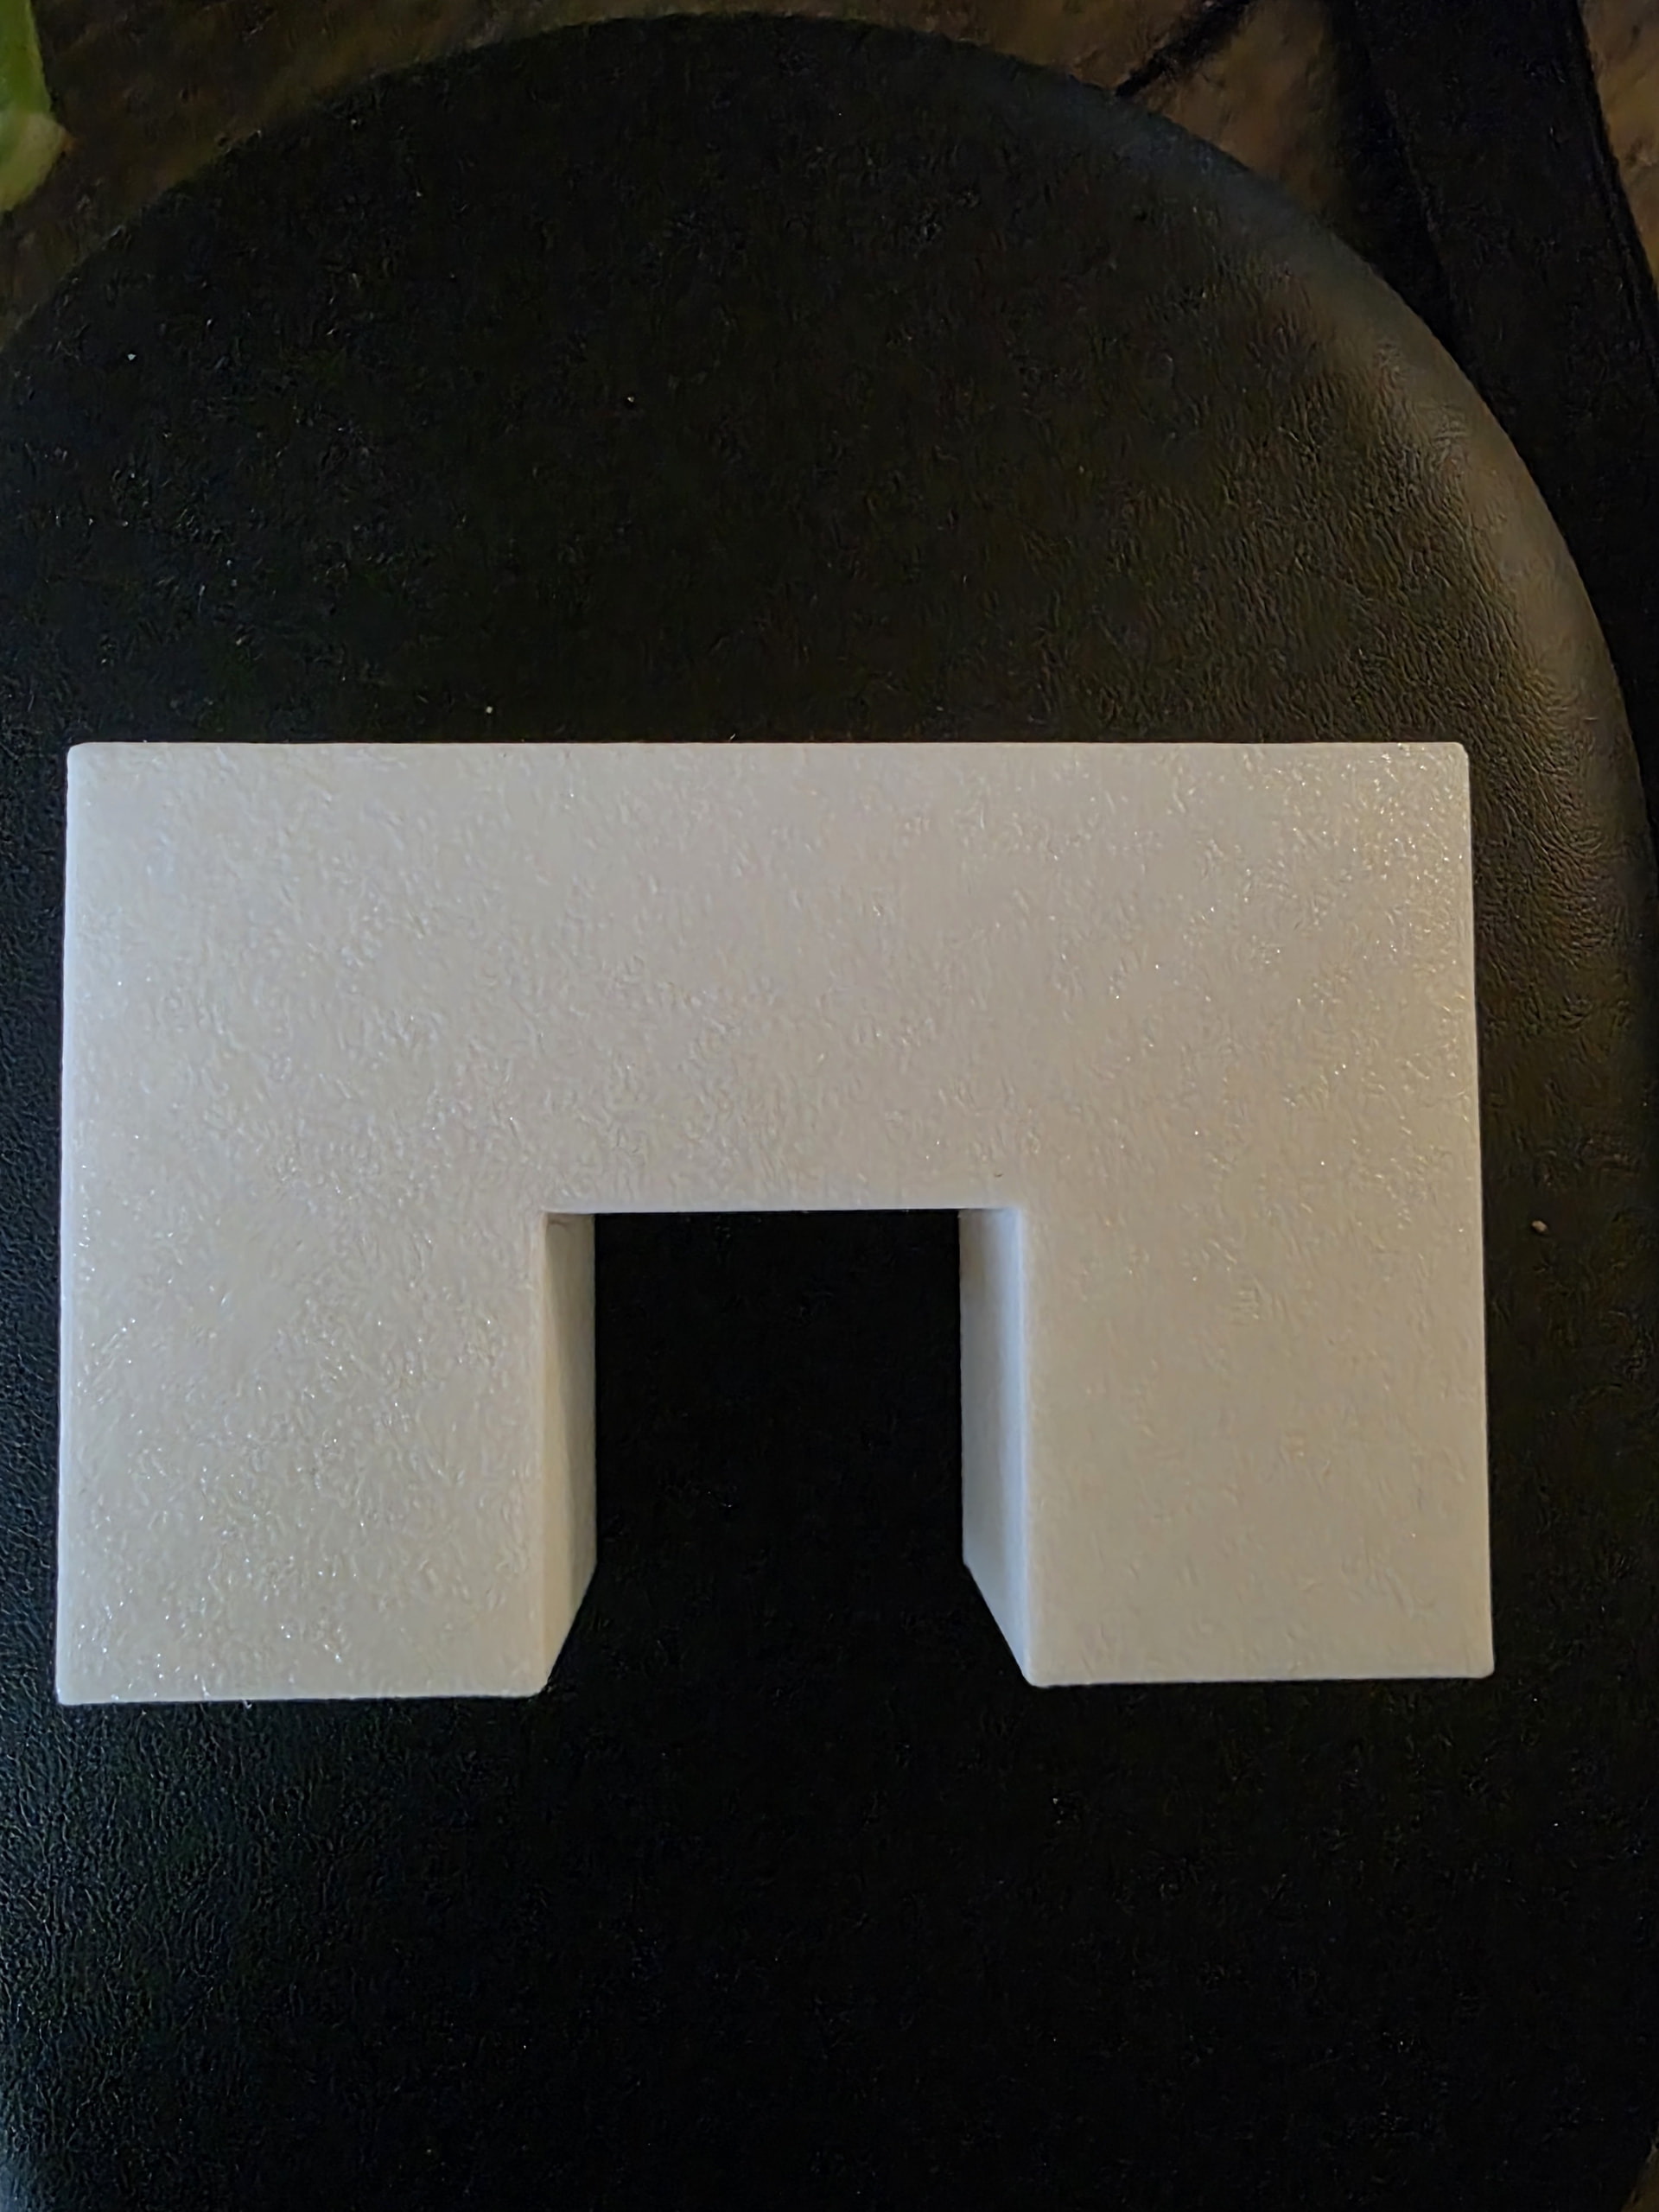
I adjusted the K value using a calibration test and it fixed the issue (see pictures)…Thank you for the help!
Just a quick question: What causes the K value to be off? I only use Bambu PLSA basic and have never had to manually adjust K value? Just curious if it’s something I did?
I do not know why your previous PA value stopped working. It could be due to a combination of factors. The new nozzle, a different filament batch, different ambient temperatures— who knows?
The default presets usually work fairly well for most printers, but I’ve always found at least a small improvement by calibrating filaments manually on my printer.