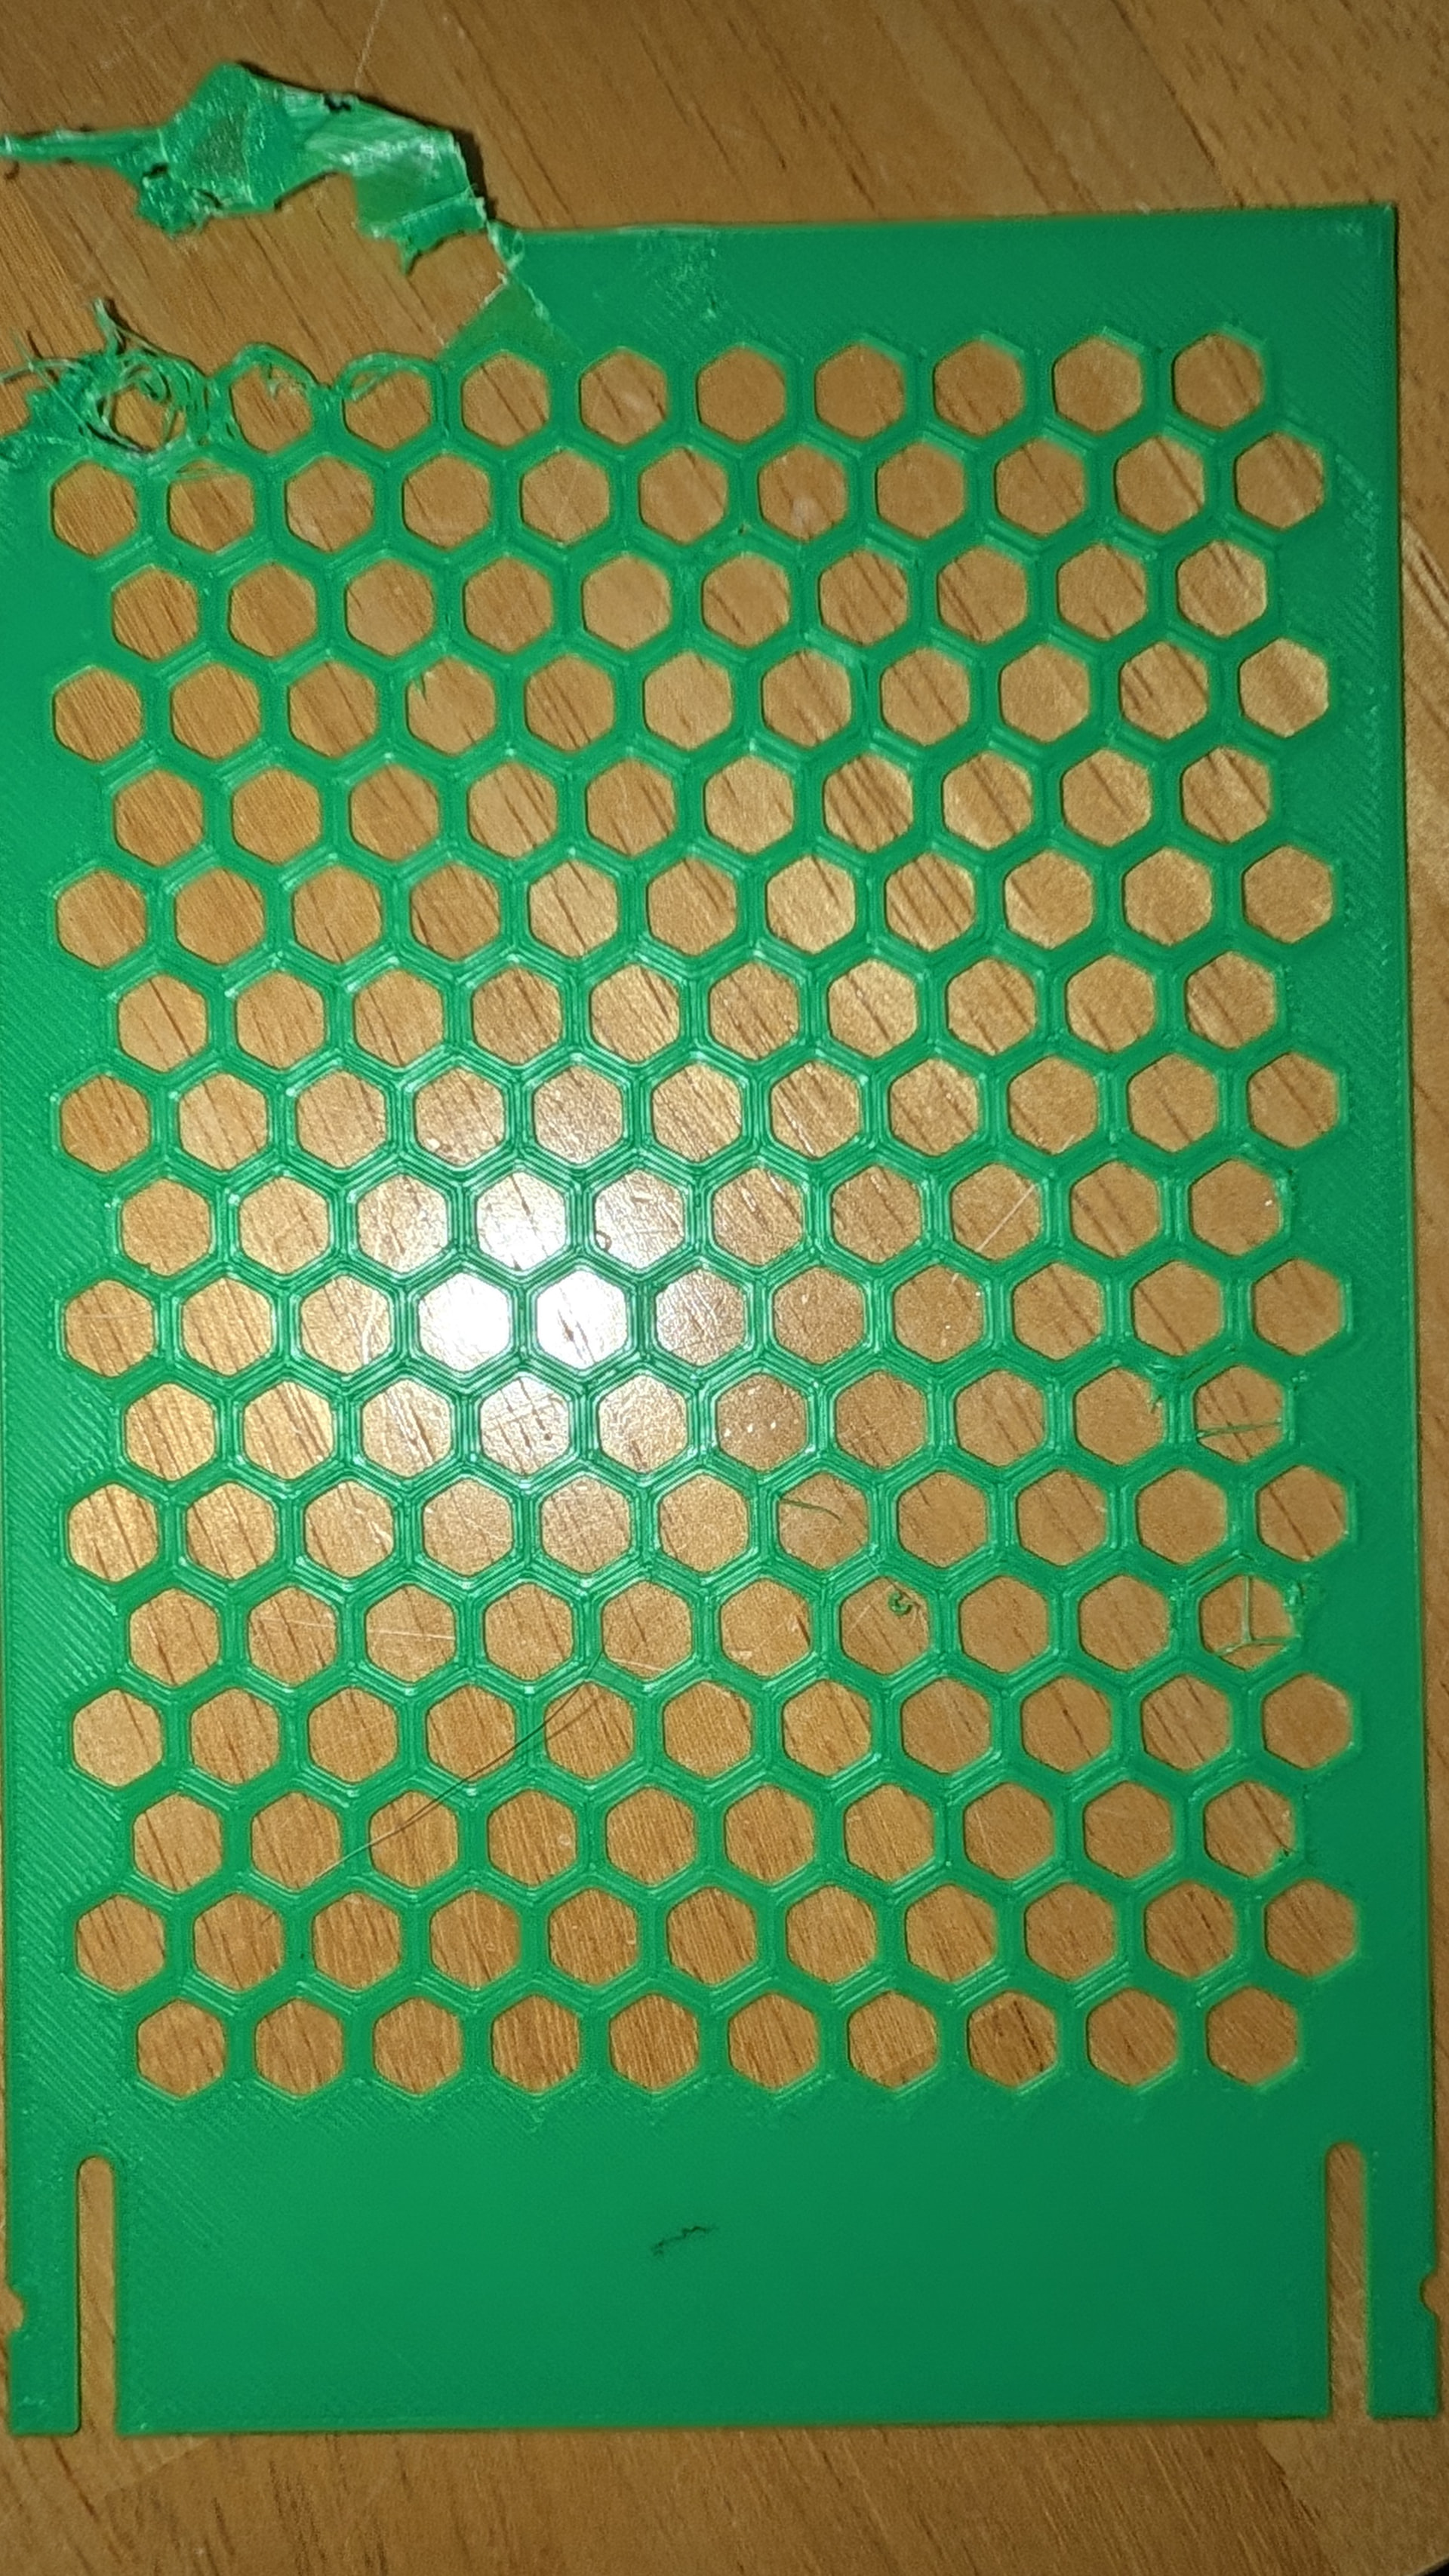
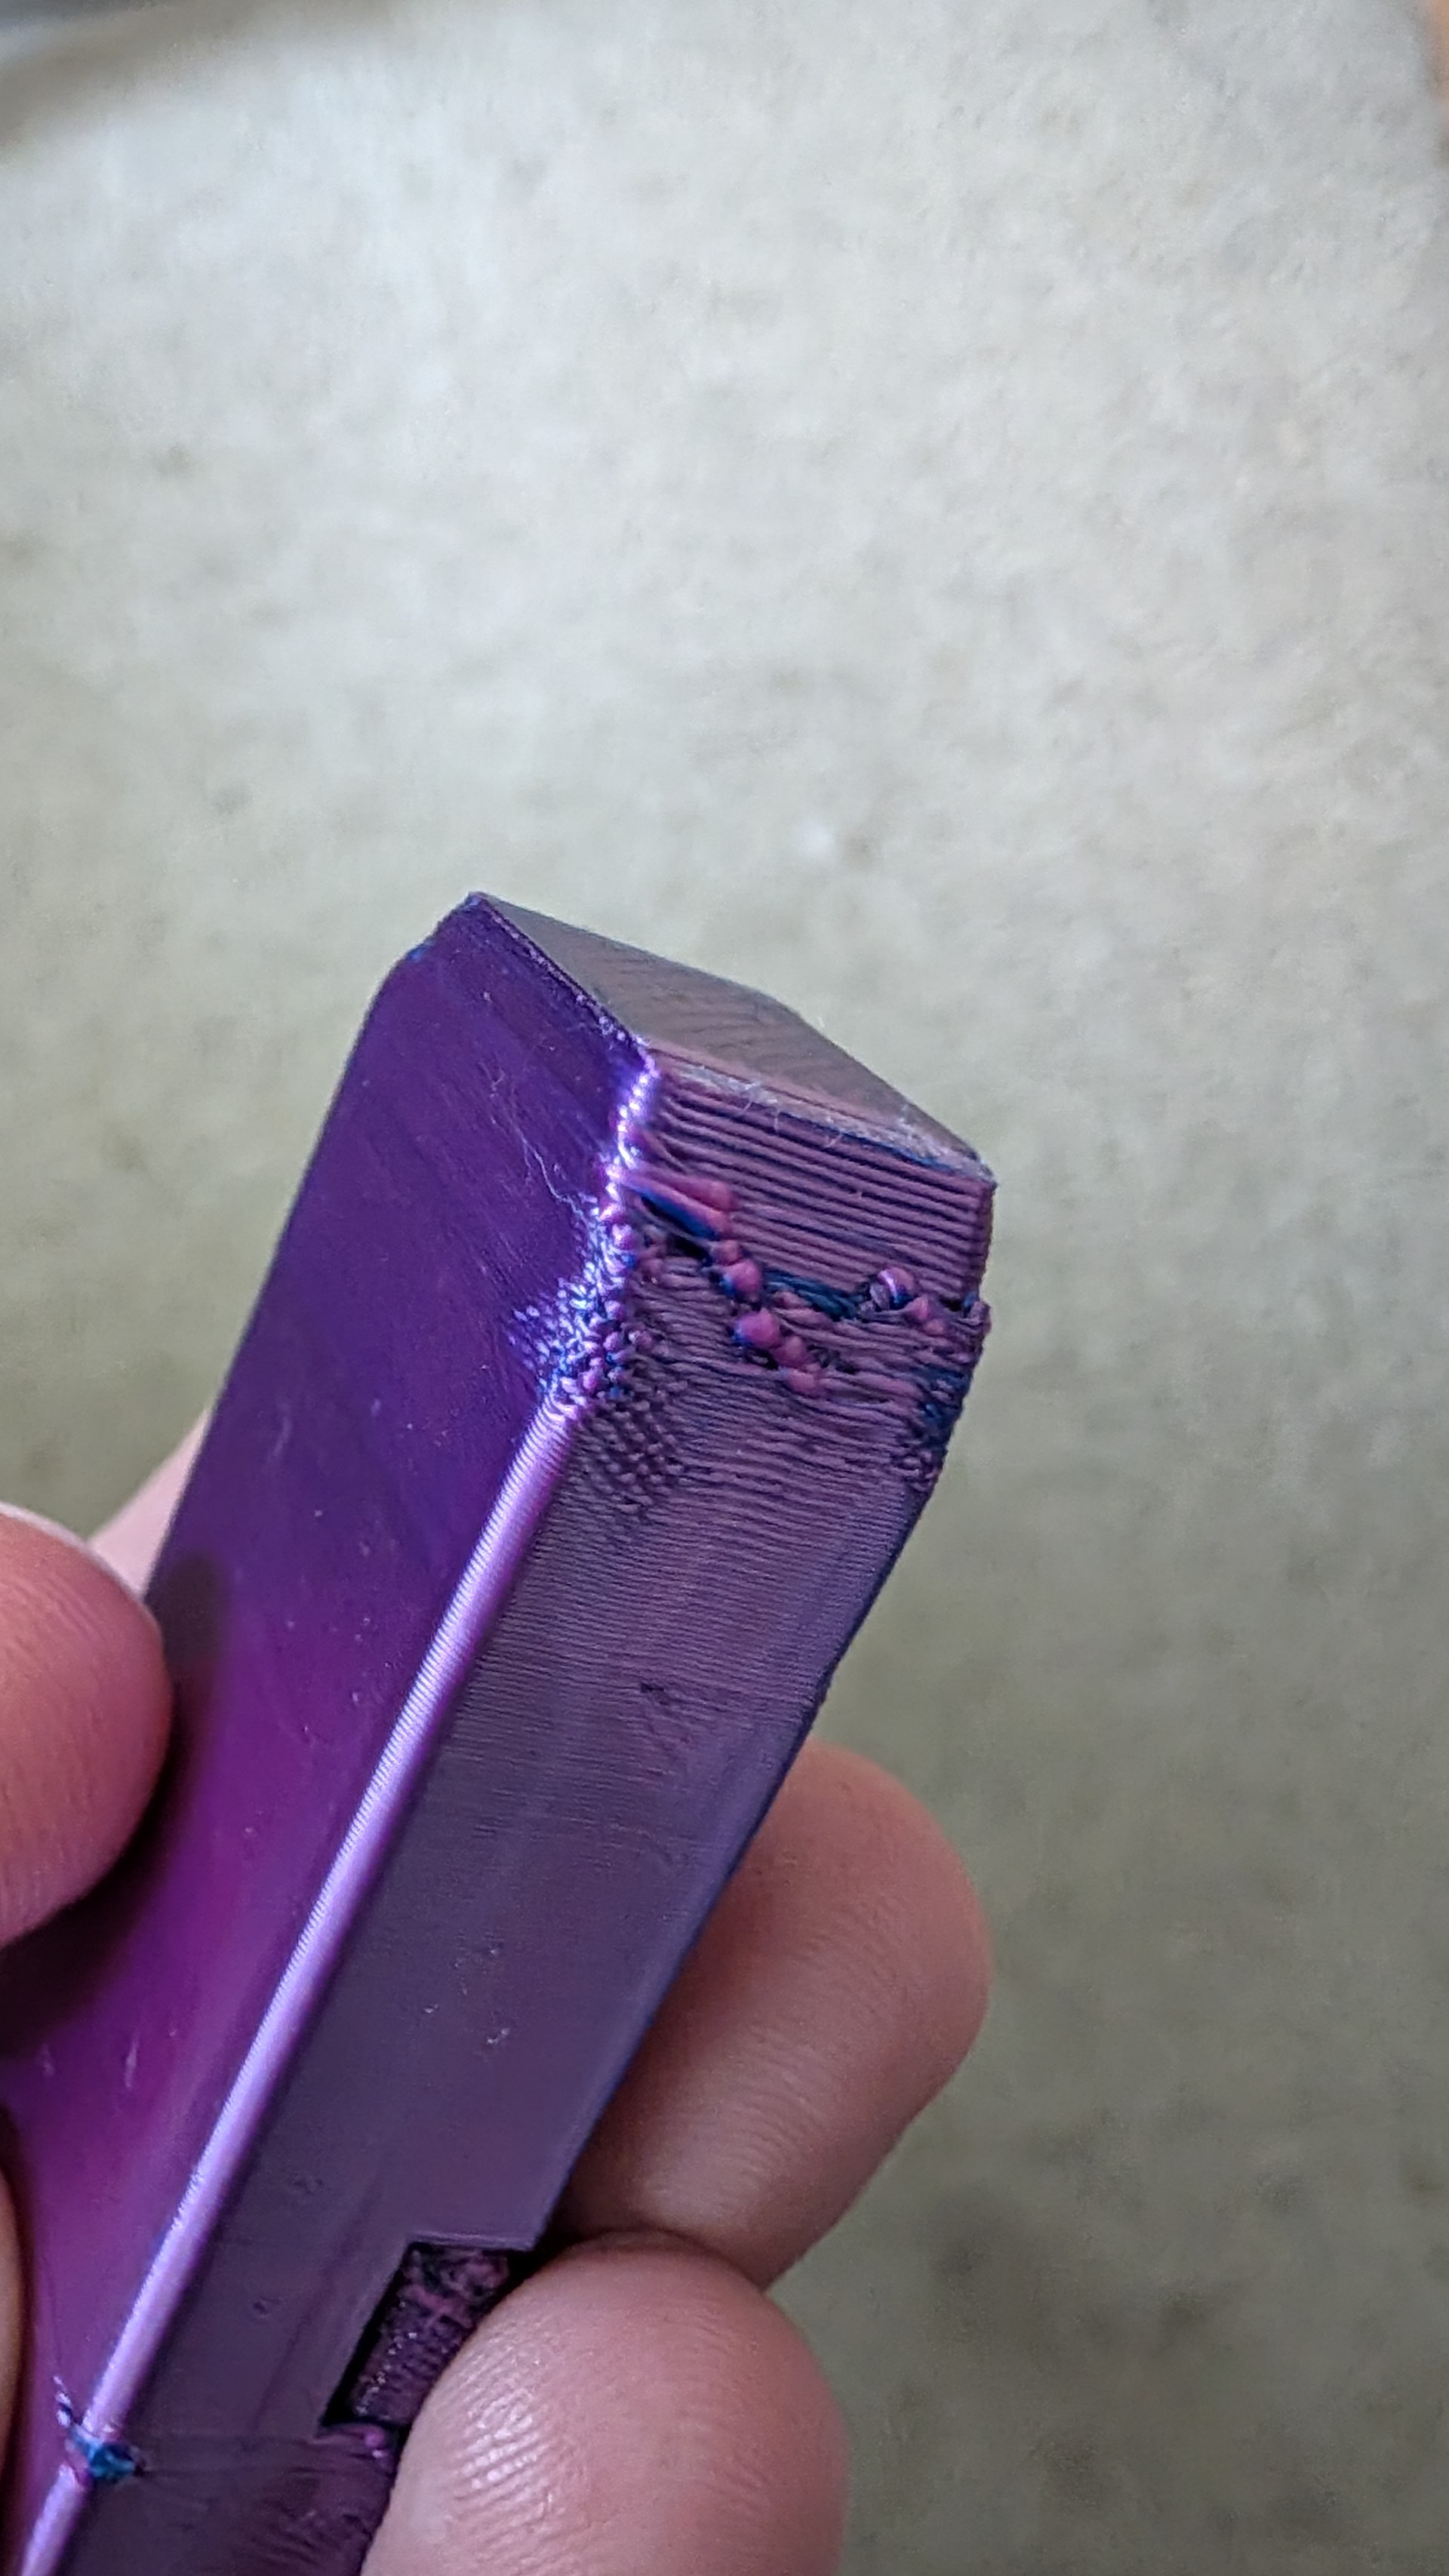
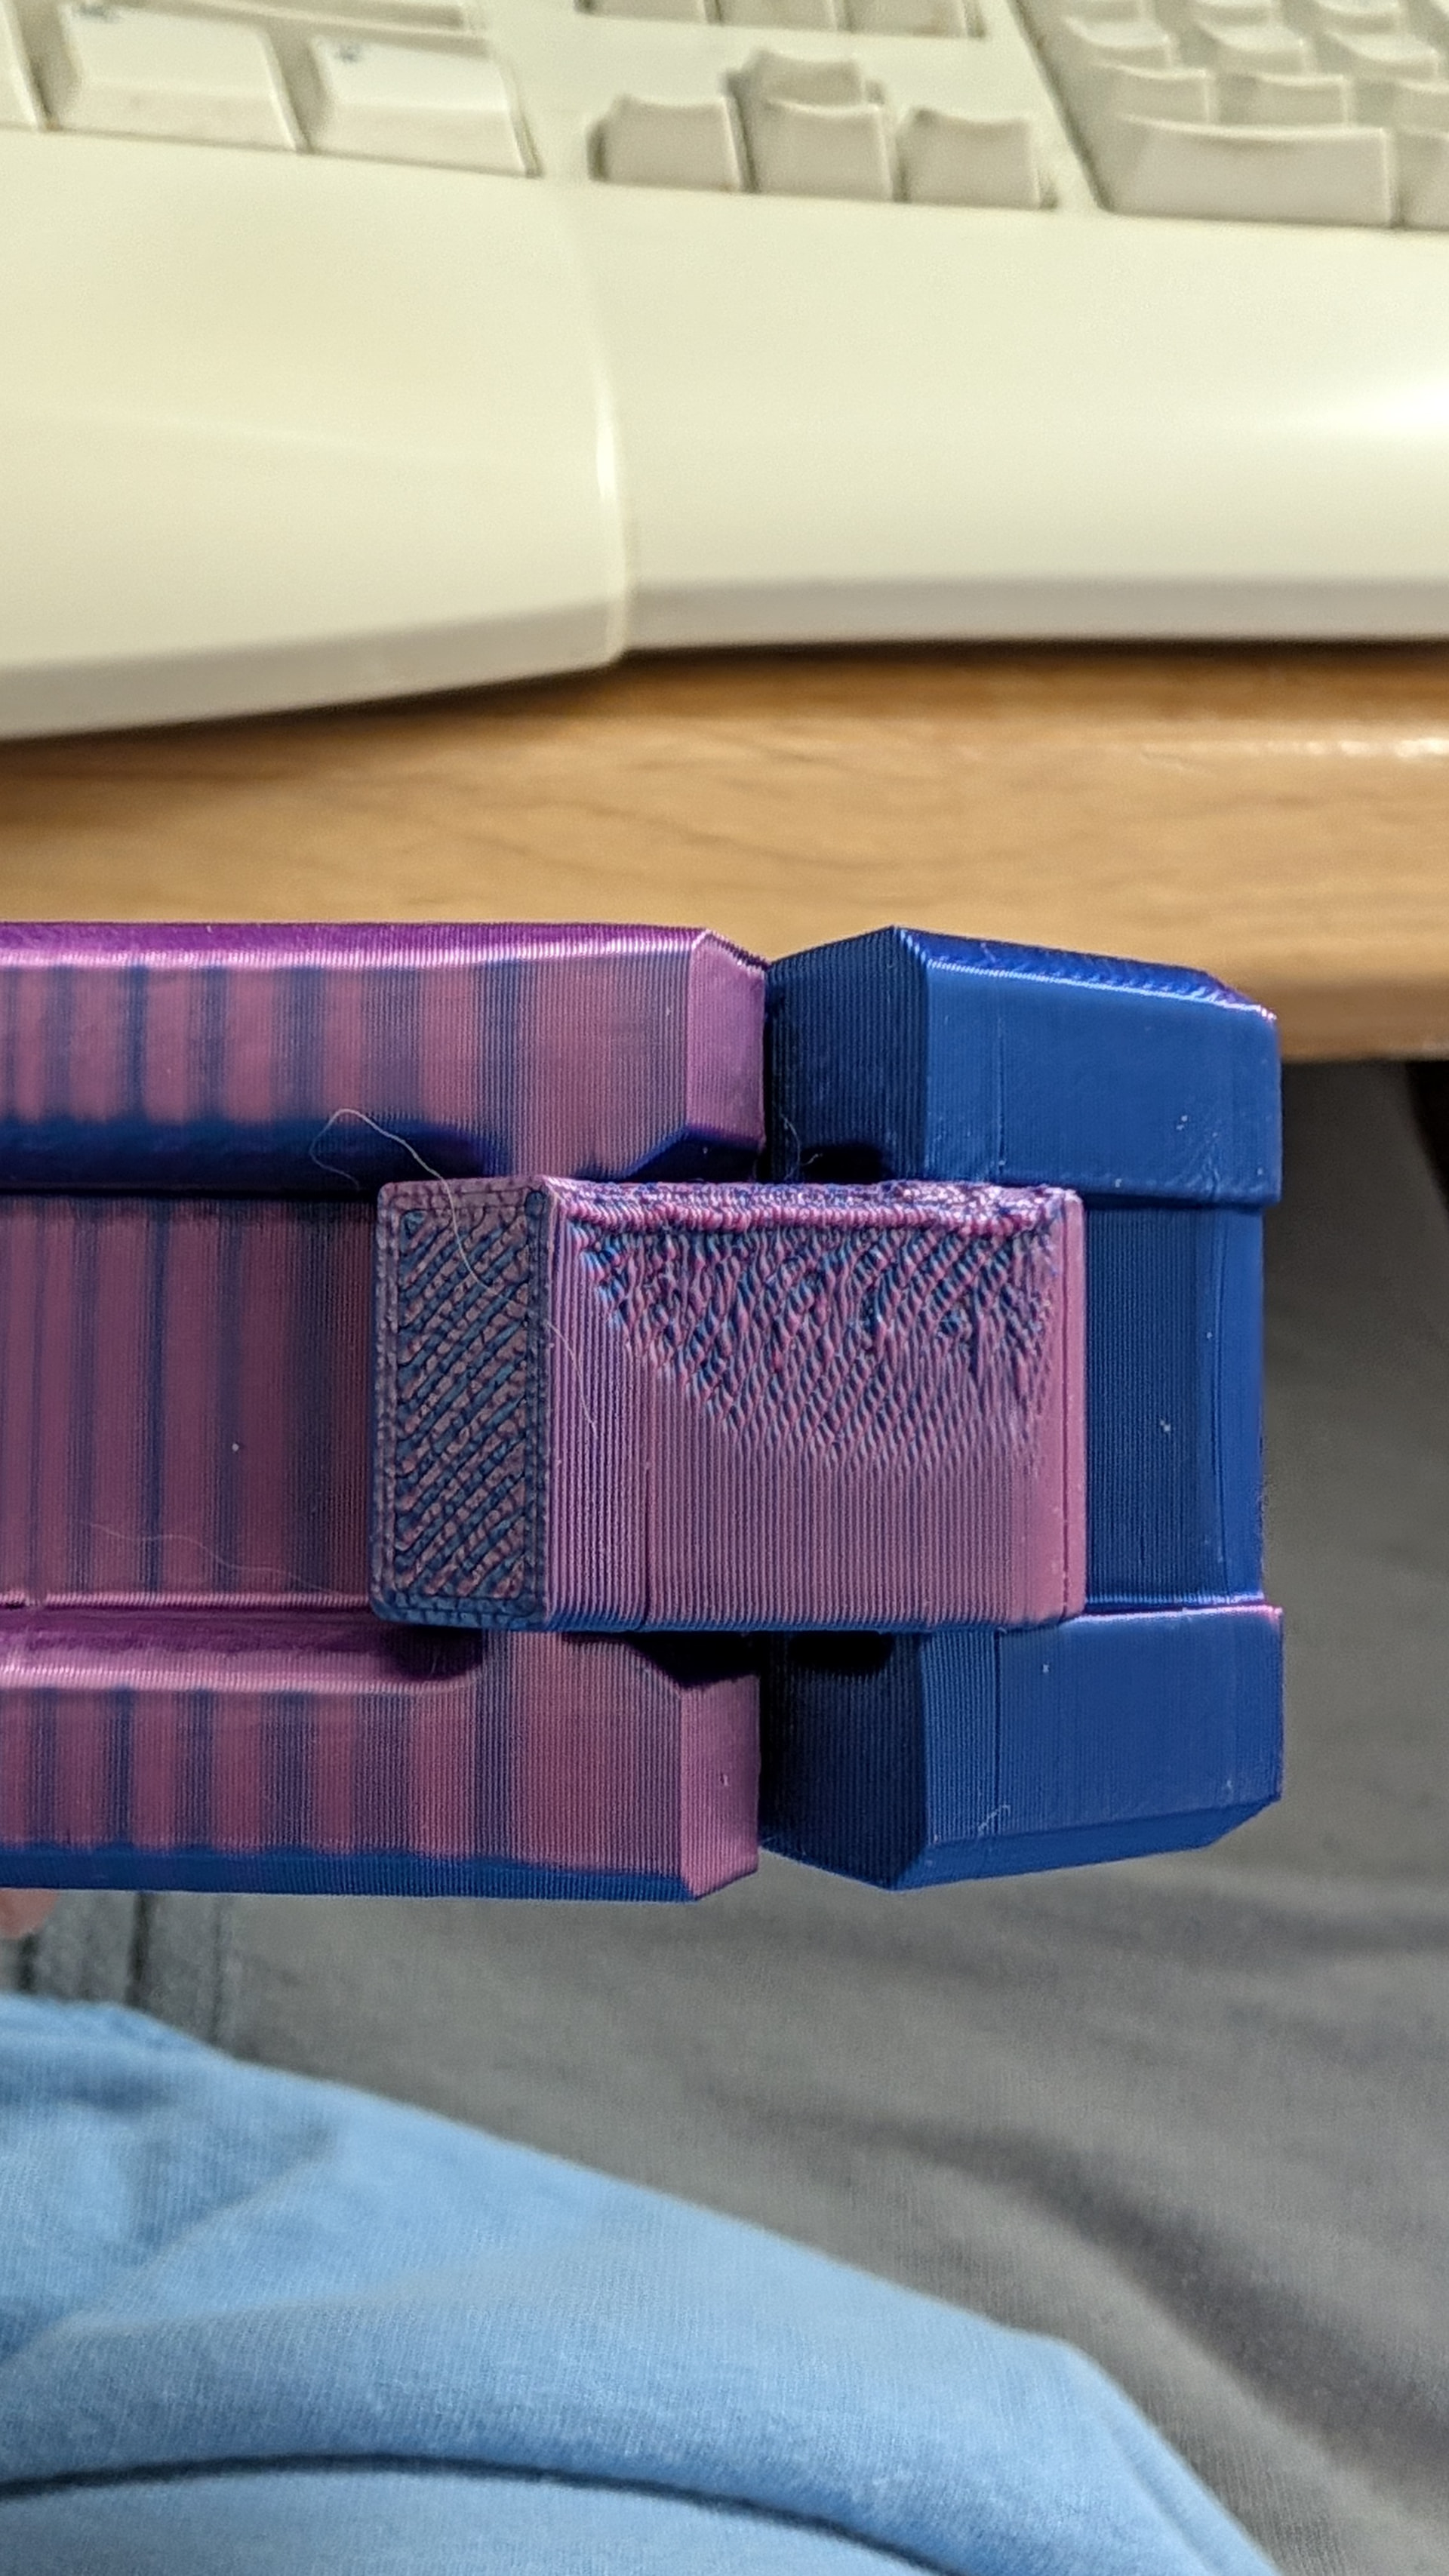
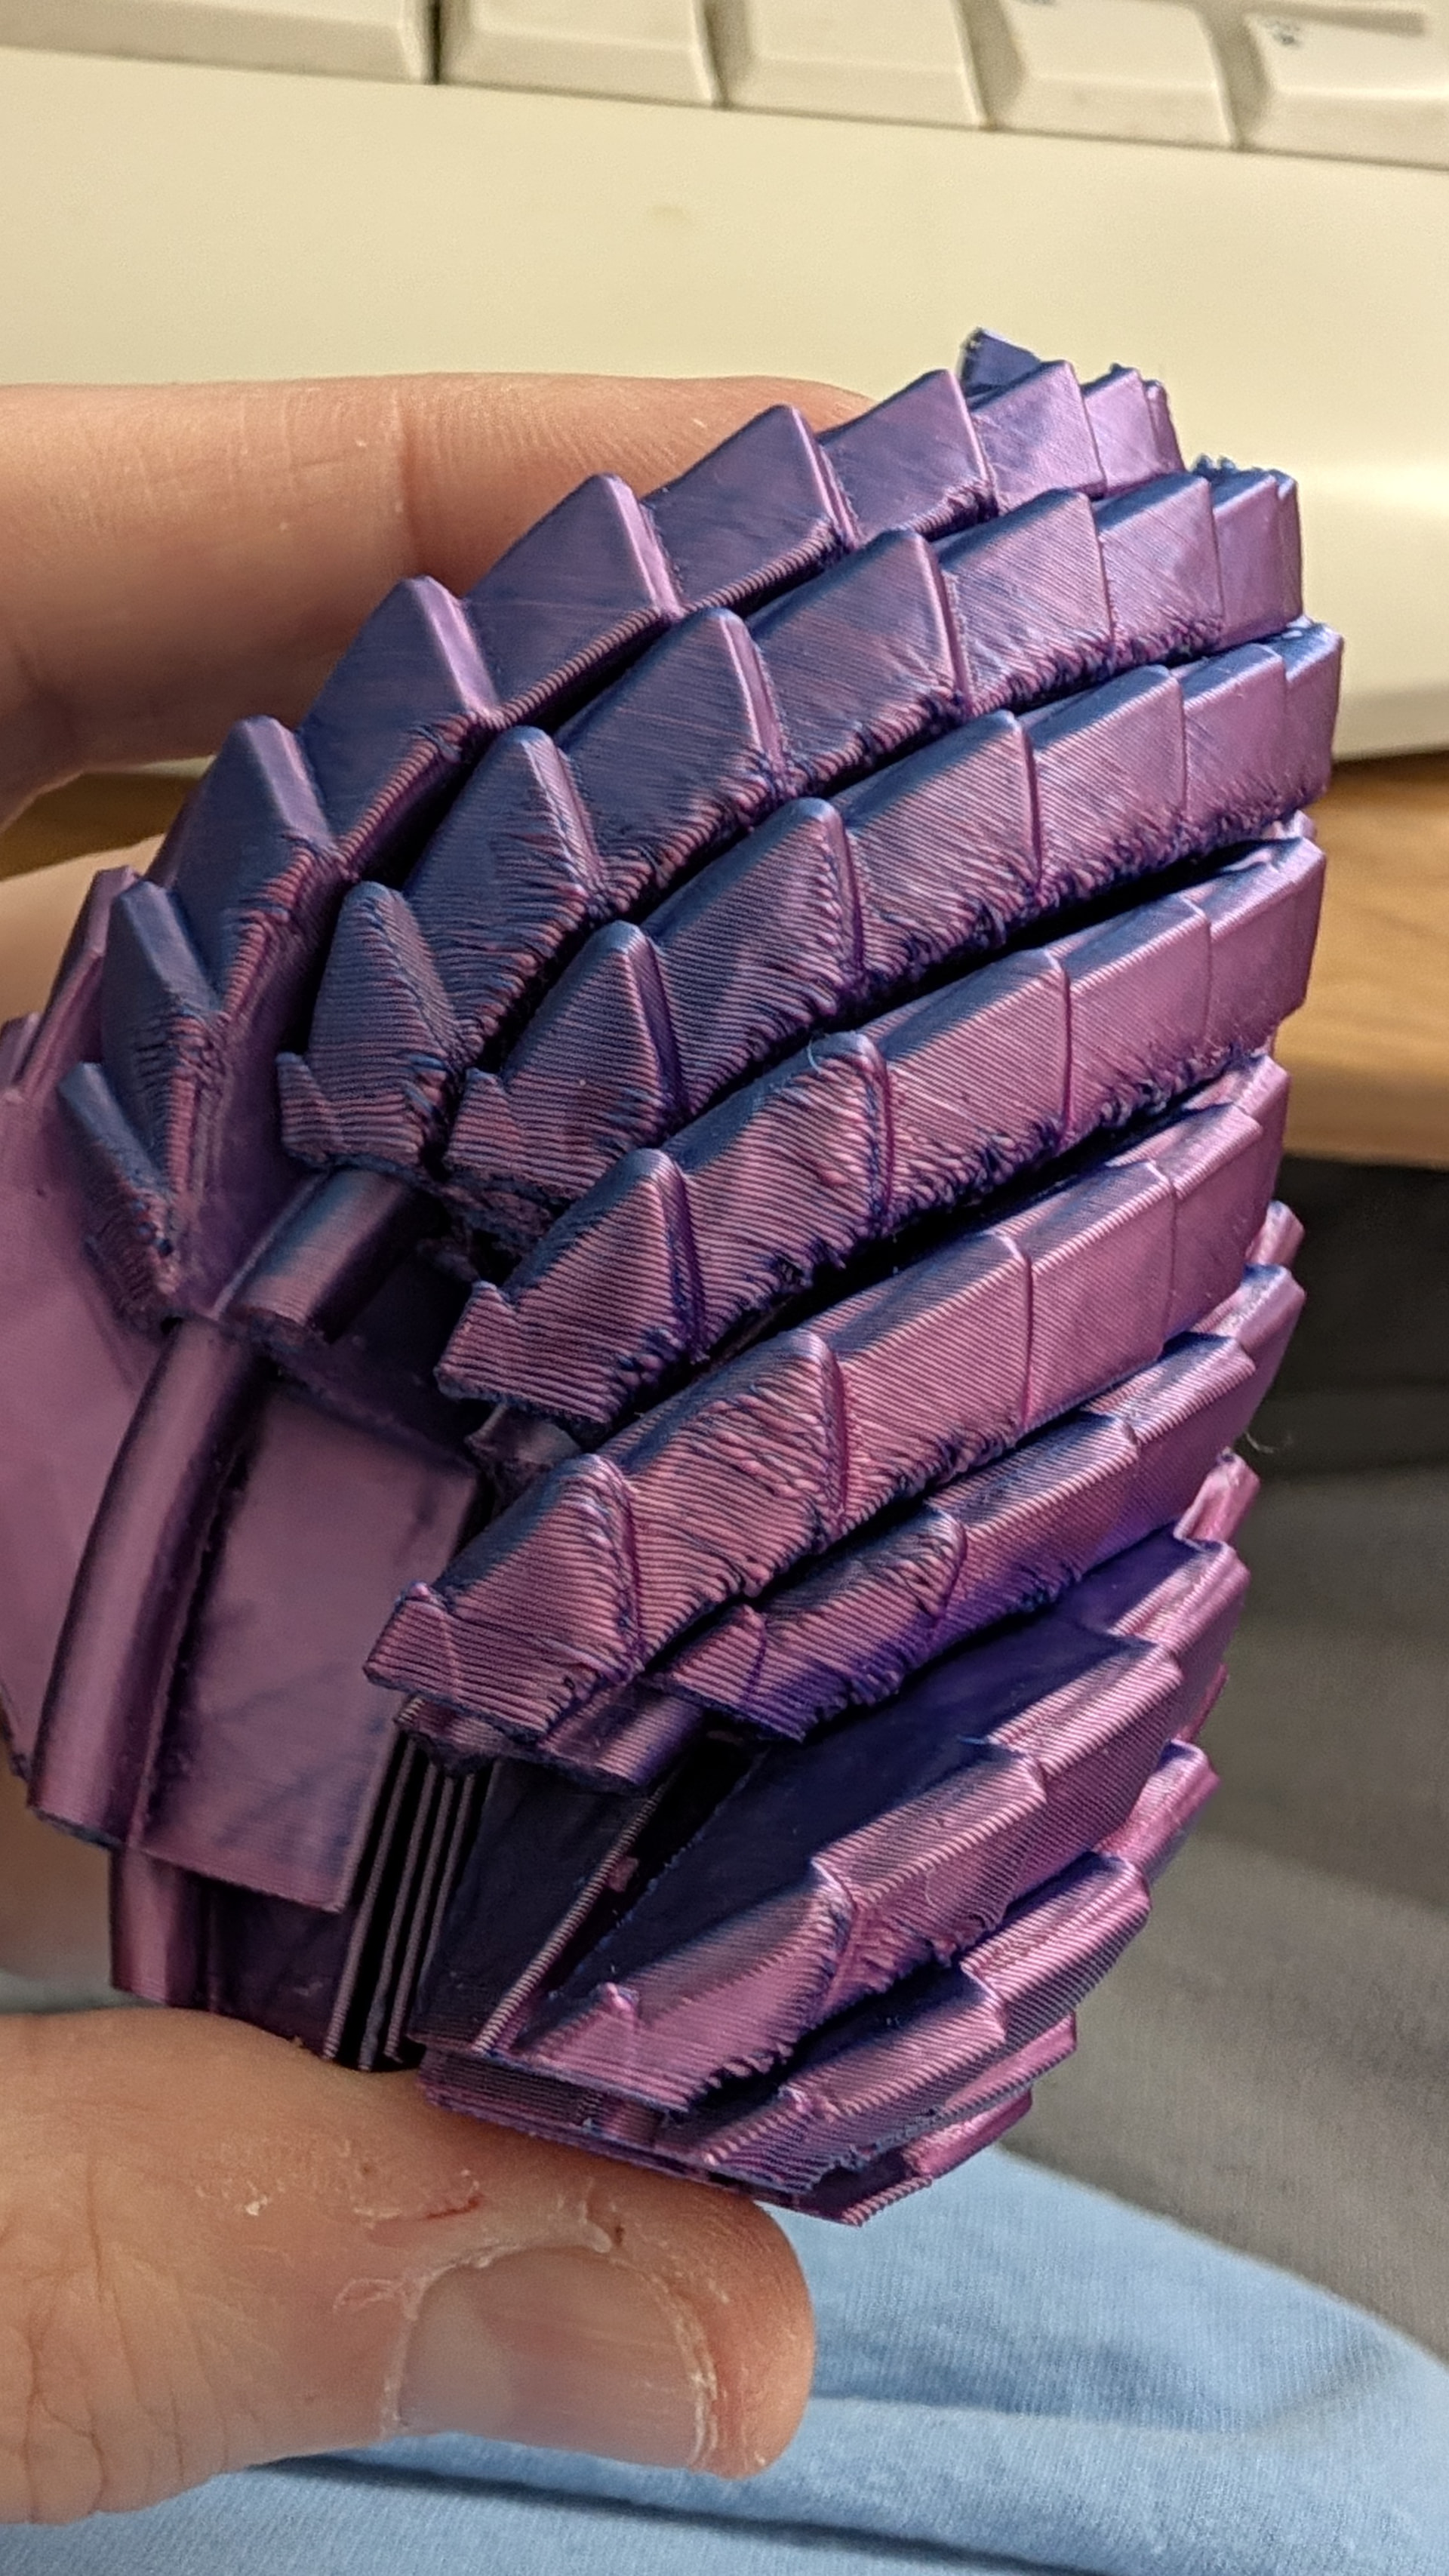
I’ve been printing on my P1S for about a year and a half and am now running into print issues. The attached photo shows what happens when it messes up enough to catch on the print, but also you can see some stringing in the hexagons lower.
I’ve been using PLA and have had this issue with both old but also freshly opened bambu PLA. Everything about the printer is stock and unchanged.
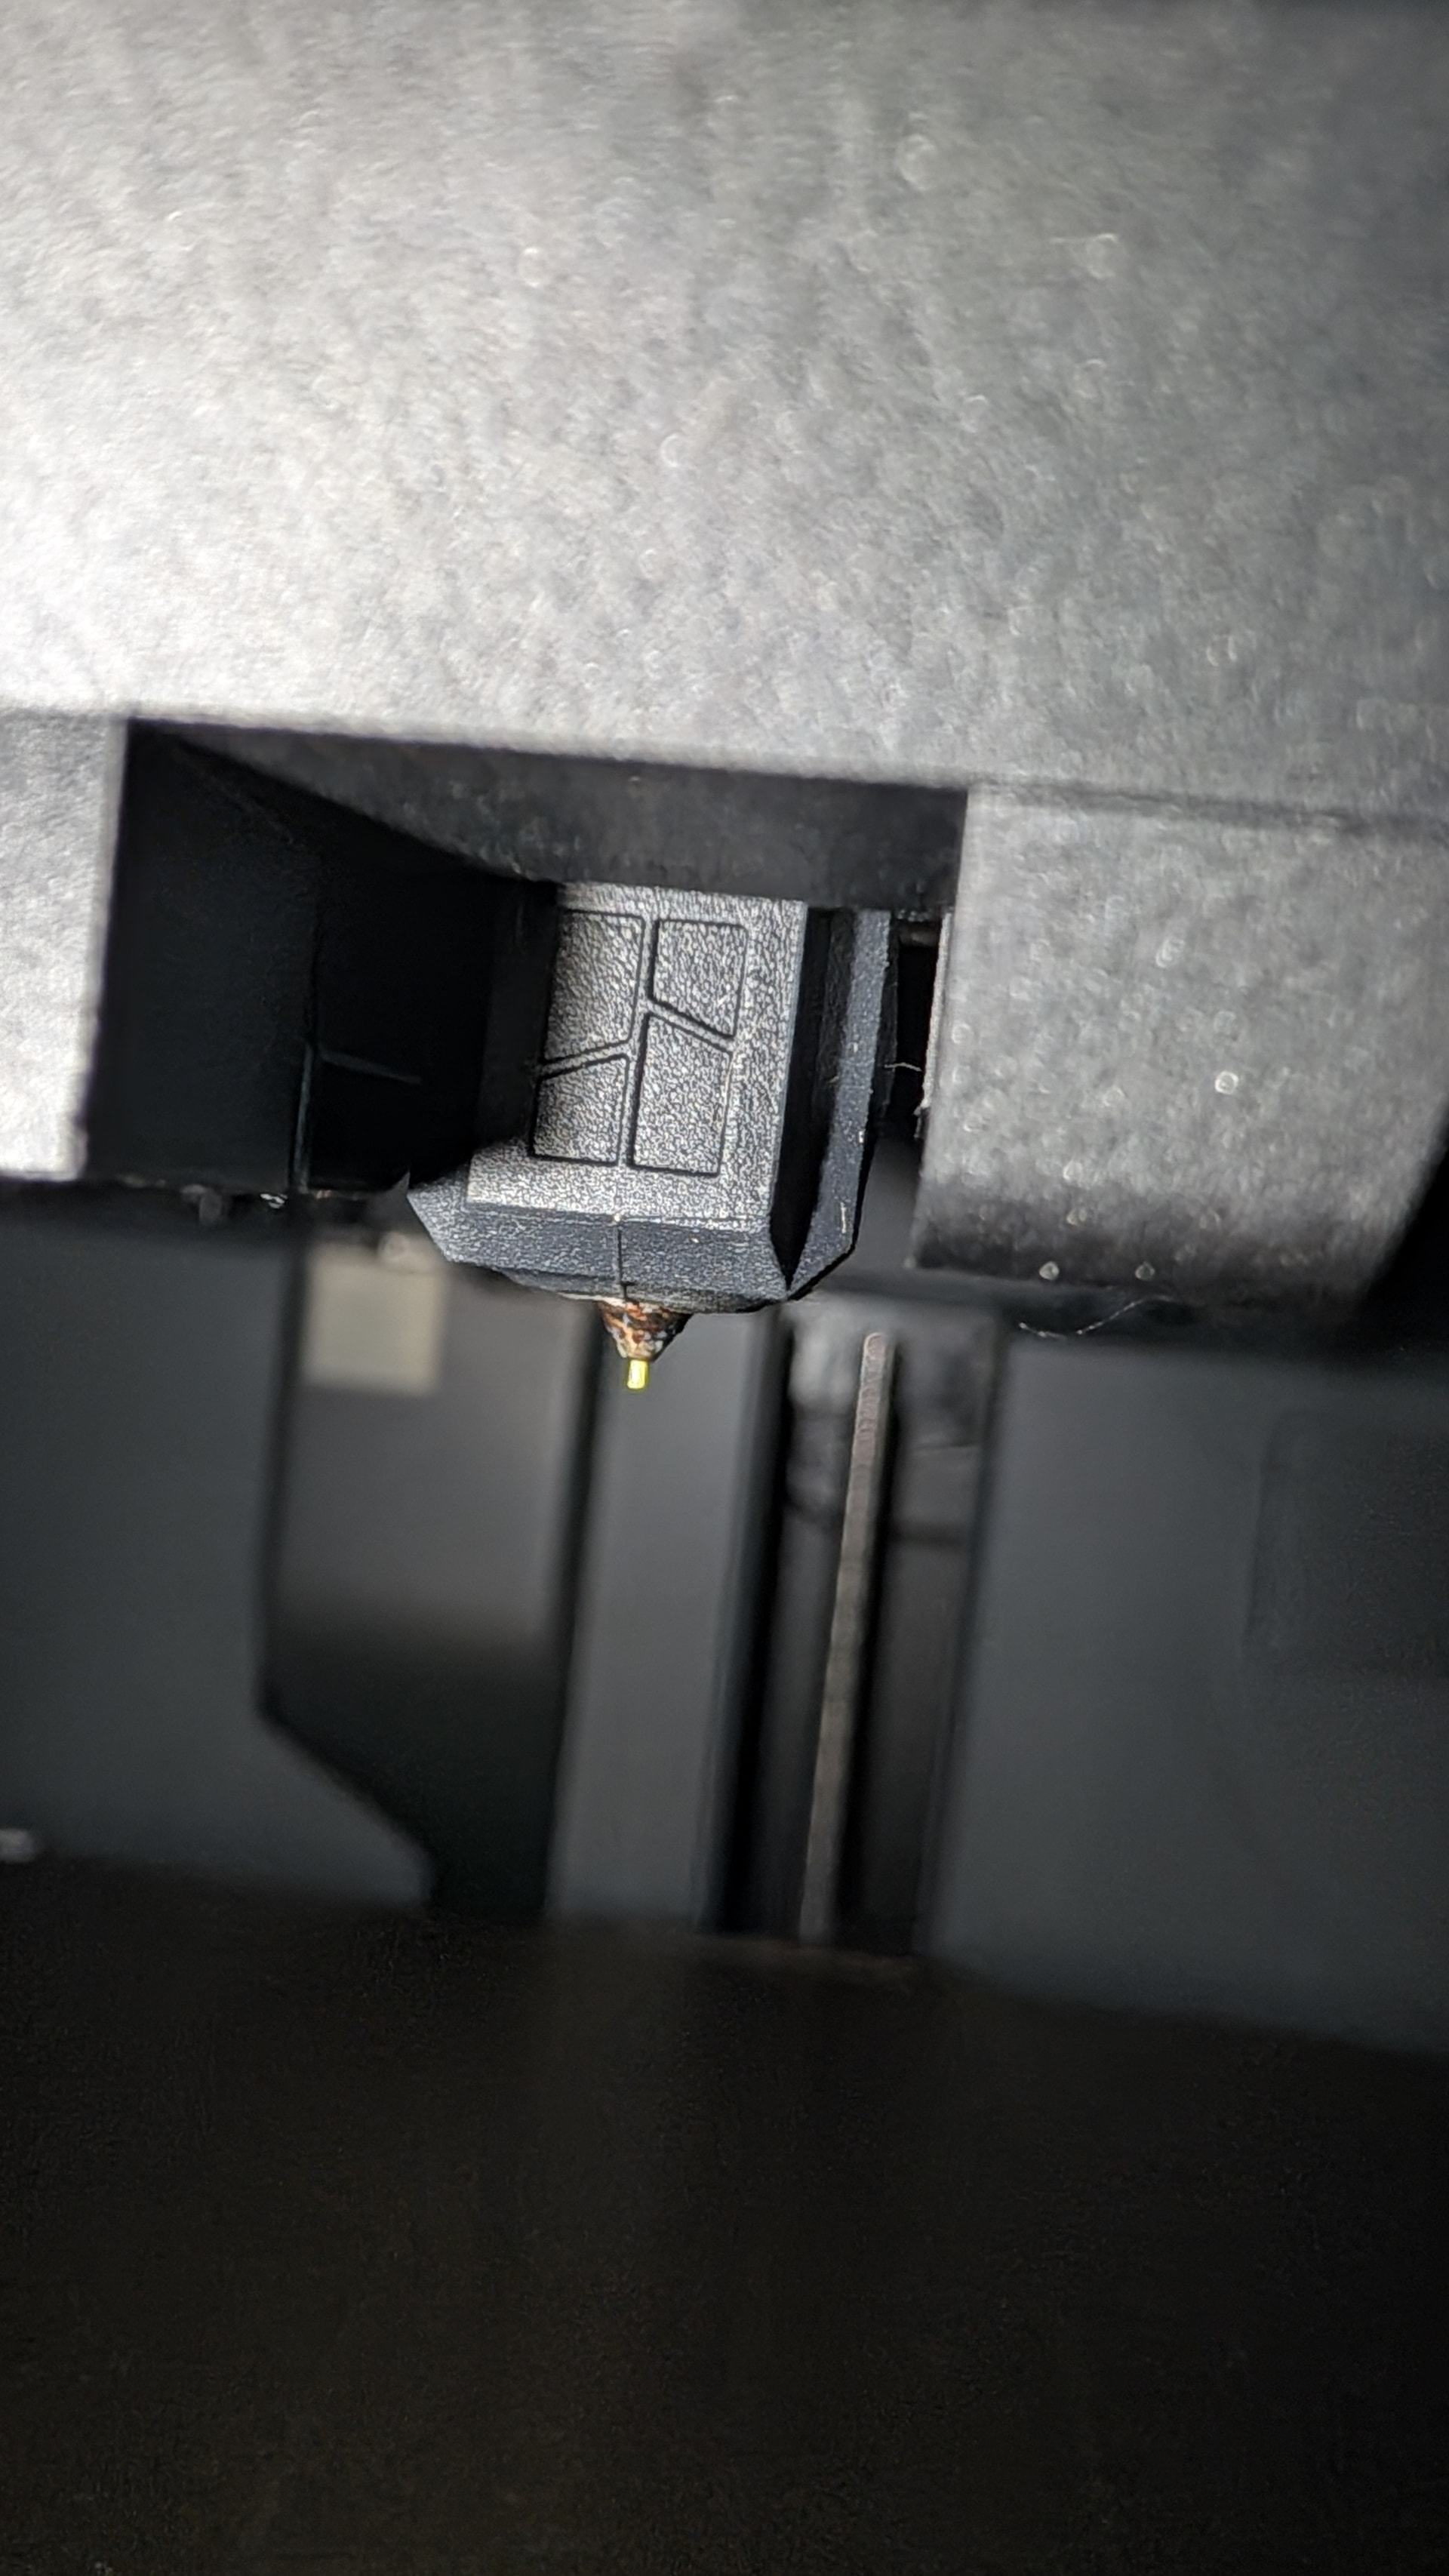
I’ve also included a close up of the nozzle. Does this need to be replaced, or does it just need a cleaning? I have replacement pieces that came with the printer, but am not sure which ones should be replaced first.
My guess is cleaning the build plate will be the best place to start.
You could rotate the print 90° so it doesn’t sit in that location when you try again.
Build plate cleaning is an often missed regular maintenance task.
Remember, build plates are consumables, they do not last forever, less if not cleaned when needed.
You can reduce the interval by only touching the build plates on the edges and using a microfibre cloth to wipe it down (dry is fine) between prints. This will remove residue that isn’t burnt in, which subsequent prints can cause. Cleaning usually gets rid of those.
The only other thing I’ll mention is stringing and adhesion issues can also be related to filament that’s too wet; if you live in a place with excessive humidity - pretty much everywhere, really, and you aren’t actively drying and mitigating against moisture when storing your filament, this needs to be looked at.
In space, look at the avatar!
That is what I thought, too, but it also is happening with freshly opened PLA that has just been put into the AMS.
Thanks, I’ll give cleaning it a try. I actually have two, so I could try swapping it out to see while cleaning the other.
Freshly opened means absolutely nothing, being in a plastic bag slows moisture absorption, but humidity still moves through plastic.
Think about it - filament is plastic. We all understand that filament absorbs moisture - meaning moisture passes into it - but we think the plastic bag we put the filament in doesn’t have the exact same problem?
It is two-sided, you can flip it as well.
I finally was able to do another test print. I ended up flipping the plate, but the print still looked like it struggled a little, and at the end, there were very light “spider webs” on the interior. I was able to brush them away easily enough, but still.
That seems like it is likely, then. Thanks! Which, seems odd to me, since the environment in my house has been consistent.
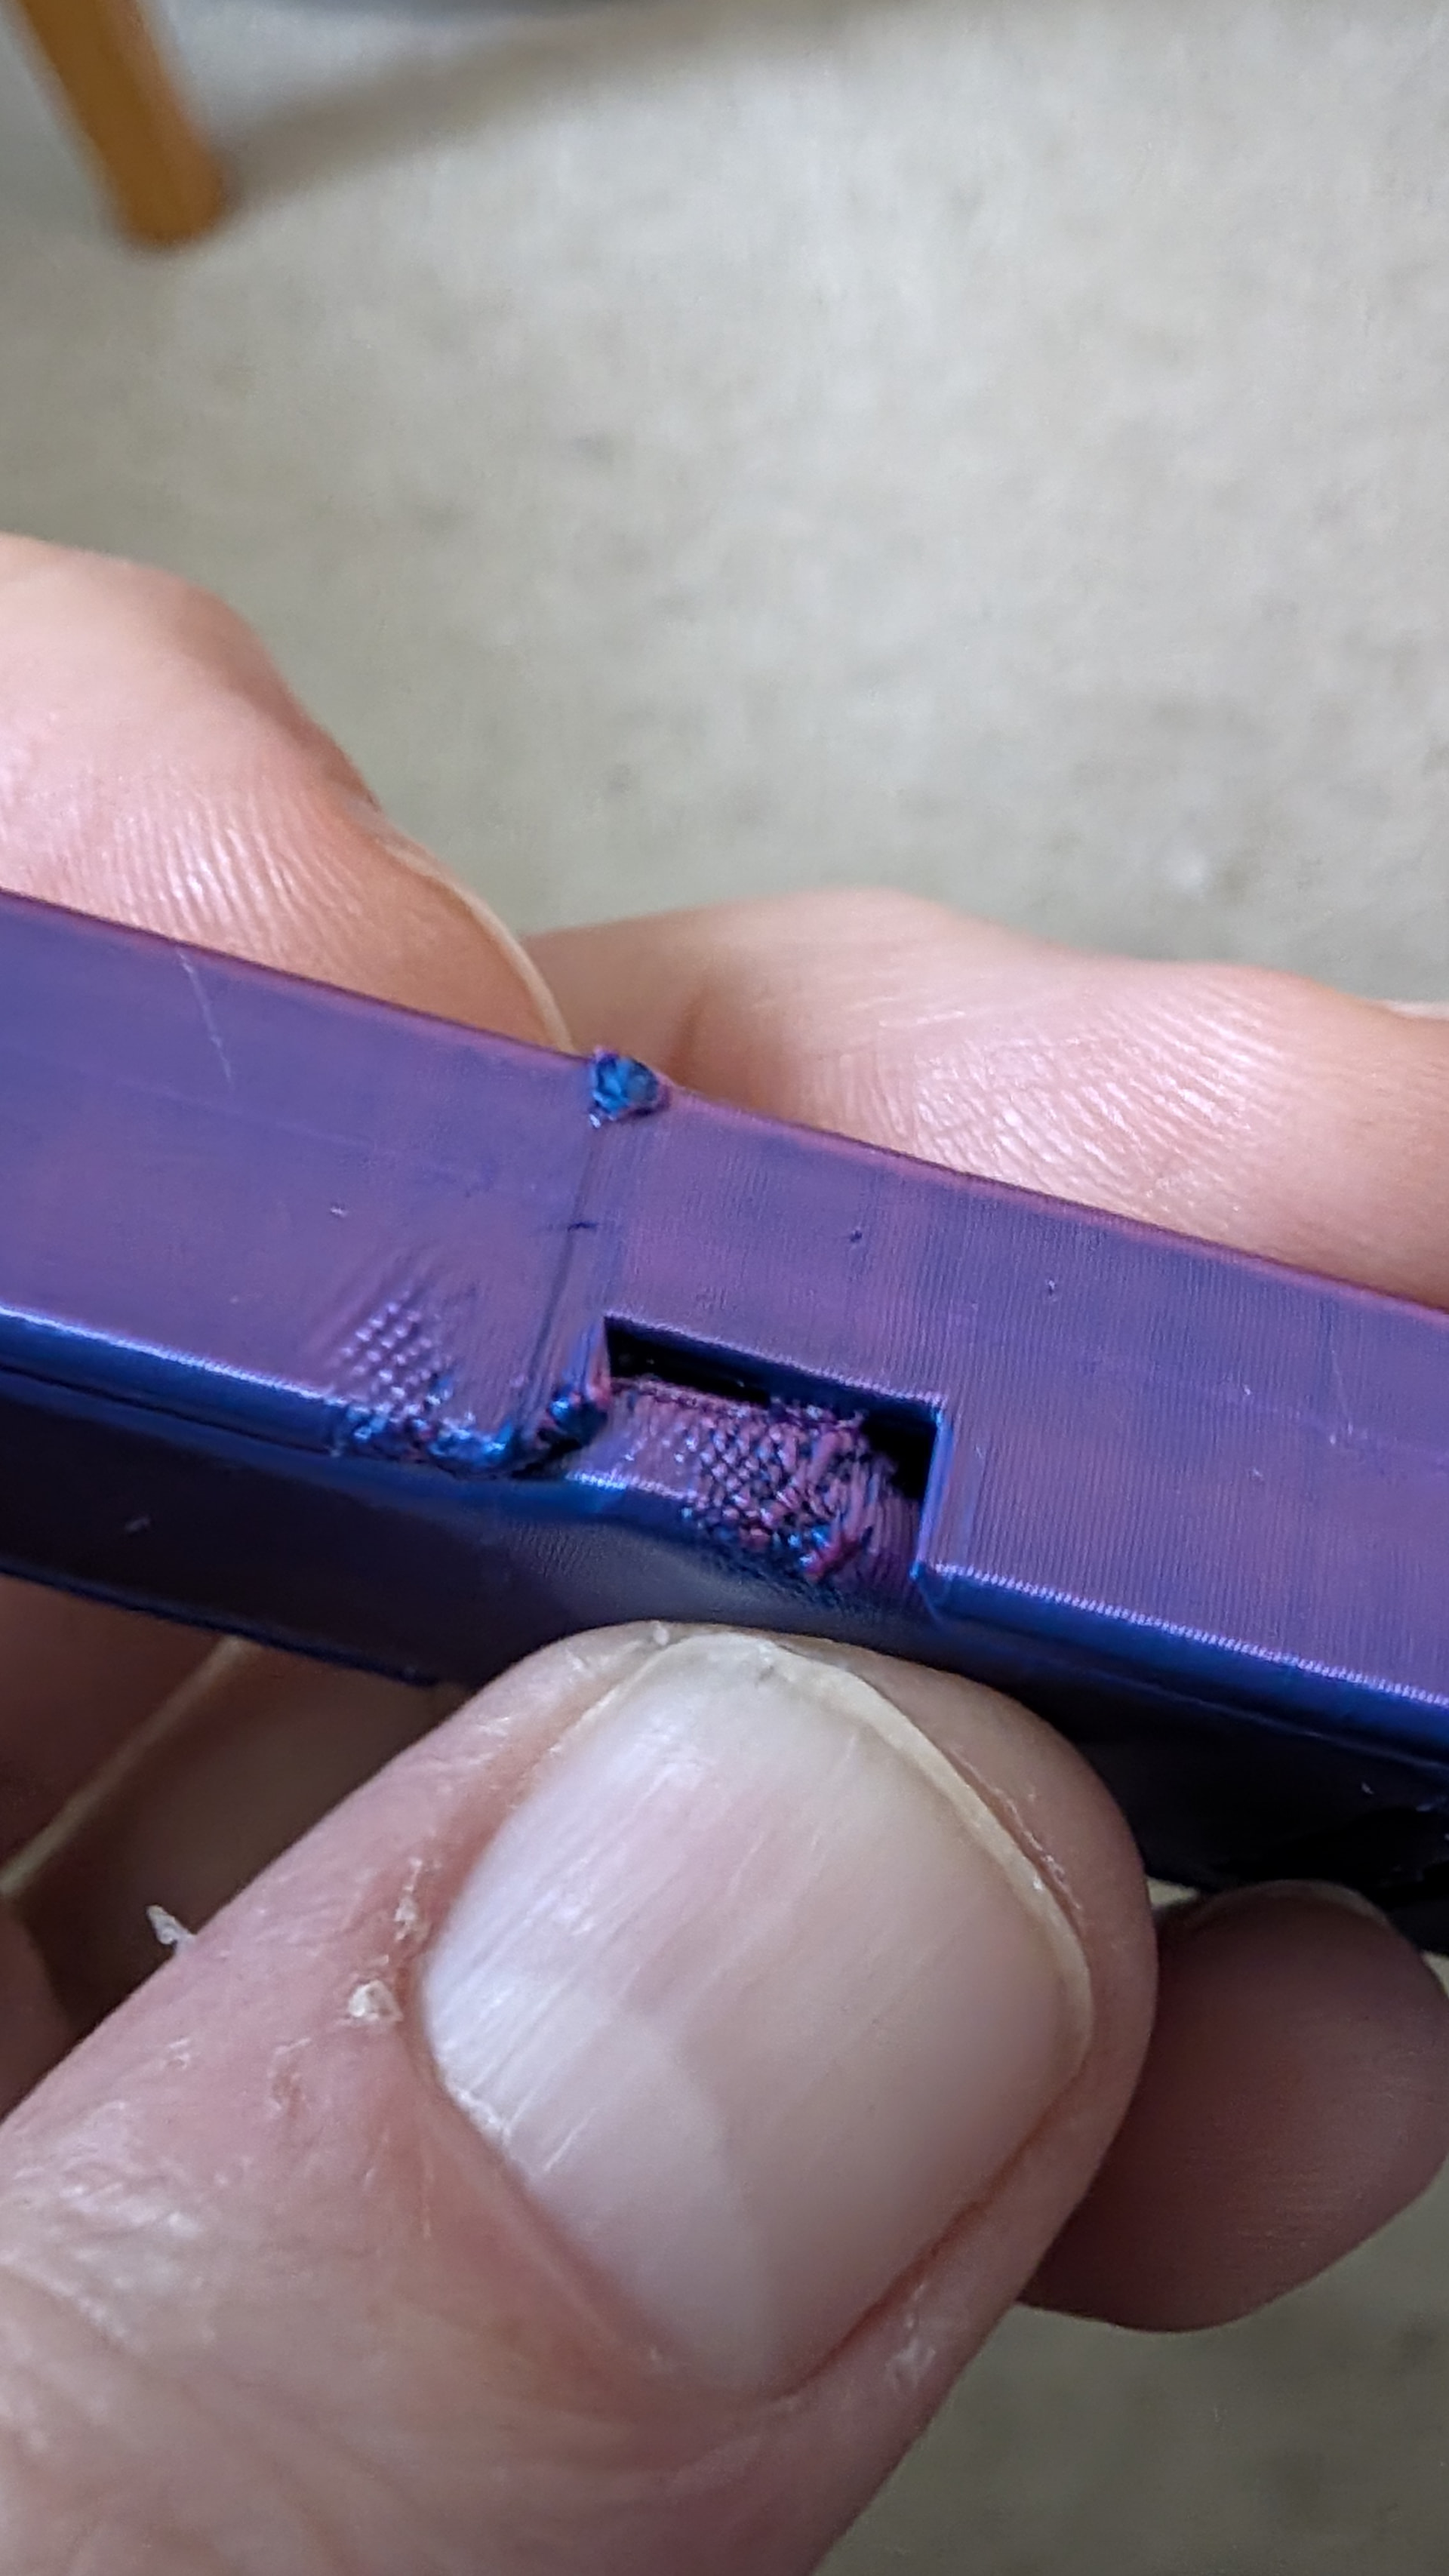
Regardless, I want to confirm that this issue would also be a moisture one. The little bit of blue was an extra little glob I cut off, and you can see the poor texture in some parts as well.
That’s a separate issue, it looks like the overhang layers aren’t getting enough time to cool you’re getting sag.
Was this printed with the door open or closed?
You may need to reduce print speed for very small cross section areas to allow more cooling time from one layer to the next.
Thanks for your help. I’ve printed a couple more items in this (PLA Silk) and had very minor cobwebs on the first, but none on the second. However, both had the same issue above.
I always print with the door closed, and because of the cats, wouldn’t be comfortable trying with the door open. I adjusted some of the settings, mostly made the nozzle temperature more on the lower range for silk: 200 C. I also tweaked some speed settings for the outer wall. Do you have some specific values you would suggest I change?
This looks very much like insufficient cooling combined with a wet filament.
Silk PLAs are far more hygroscopic than standard PLA, and are therefore much more sensitive to moisture. Definitely spend some time drying that silk PLA.
Since you don’t feel comfortable opening the door because of the cats (understandable), you can print out a small part that will prop the top lid open slightly (there are many available on Makerworld, and any of them will be sufficient, while still keeping it on the printer. If your AMS is sitting on top of your printer, than what you will want to look for is an AMS riser with either 1) ventilation holes, or 2) the ability to open the top glass without removing it. This will help keep the overall chamber temperature cooler.
From there, you can 1) increase the part cooling fan speeds in your filament profile in ~10% increments, or 2) slow the print speed down, until you get a better surface.
I have just recently used the printer to dry the silk filament, but maybe I didn’t let it go long enough. It is certainly easy enough to do it again.
I’ll look at the parts you suggested, thanks.
The odd thing is that most of the print is fine, it is only in this one section that it is poor. The rest looks great.
Cats gonna cat I guess.
You could also open the top lid partways as well. I know some of the AMS risers also give a “prop guide” that allows users to open the glass a few inches only.
There might also be a standalone solution for this.