I’m trying to understand why this model is printing the way it is. Please read everything before commenting, as I’ve done quite a bit of troubleshooting already and have ruled out many of the obvious causes.
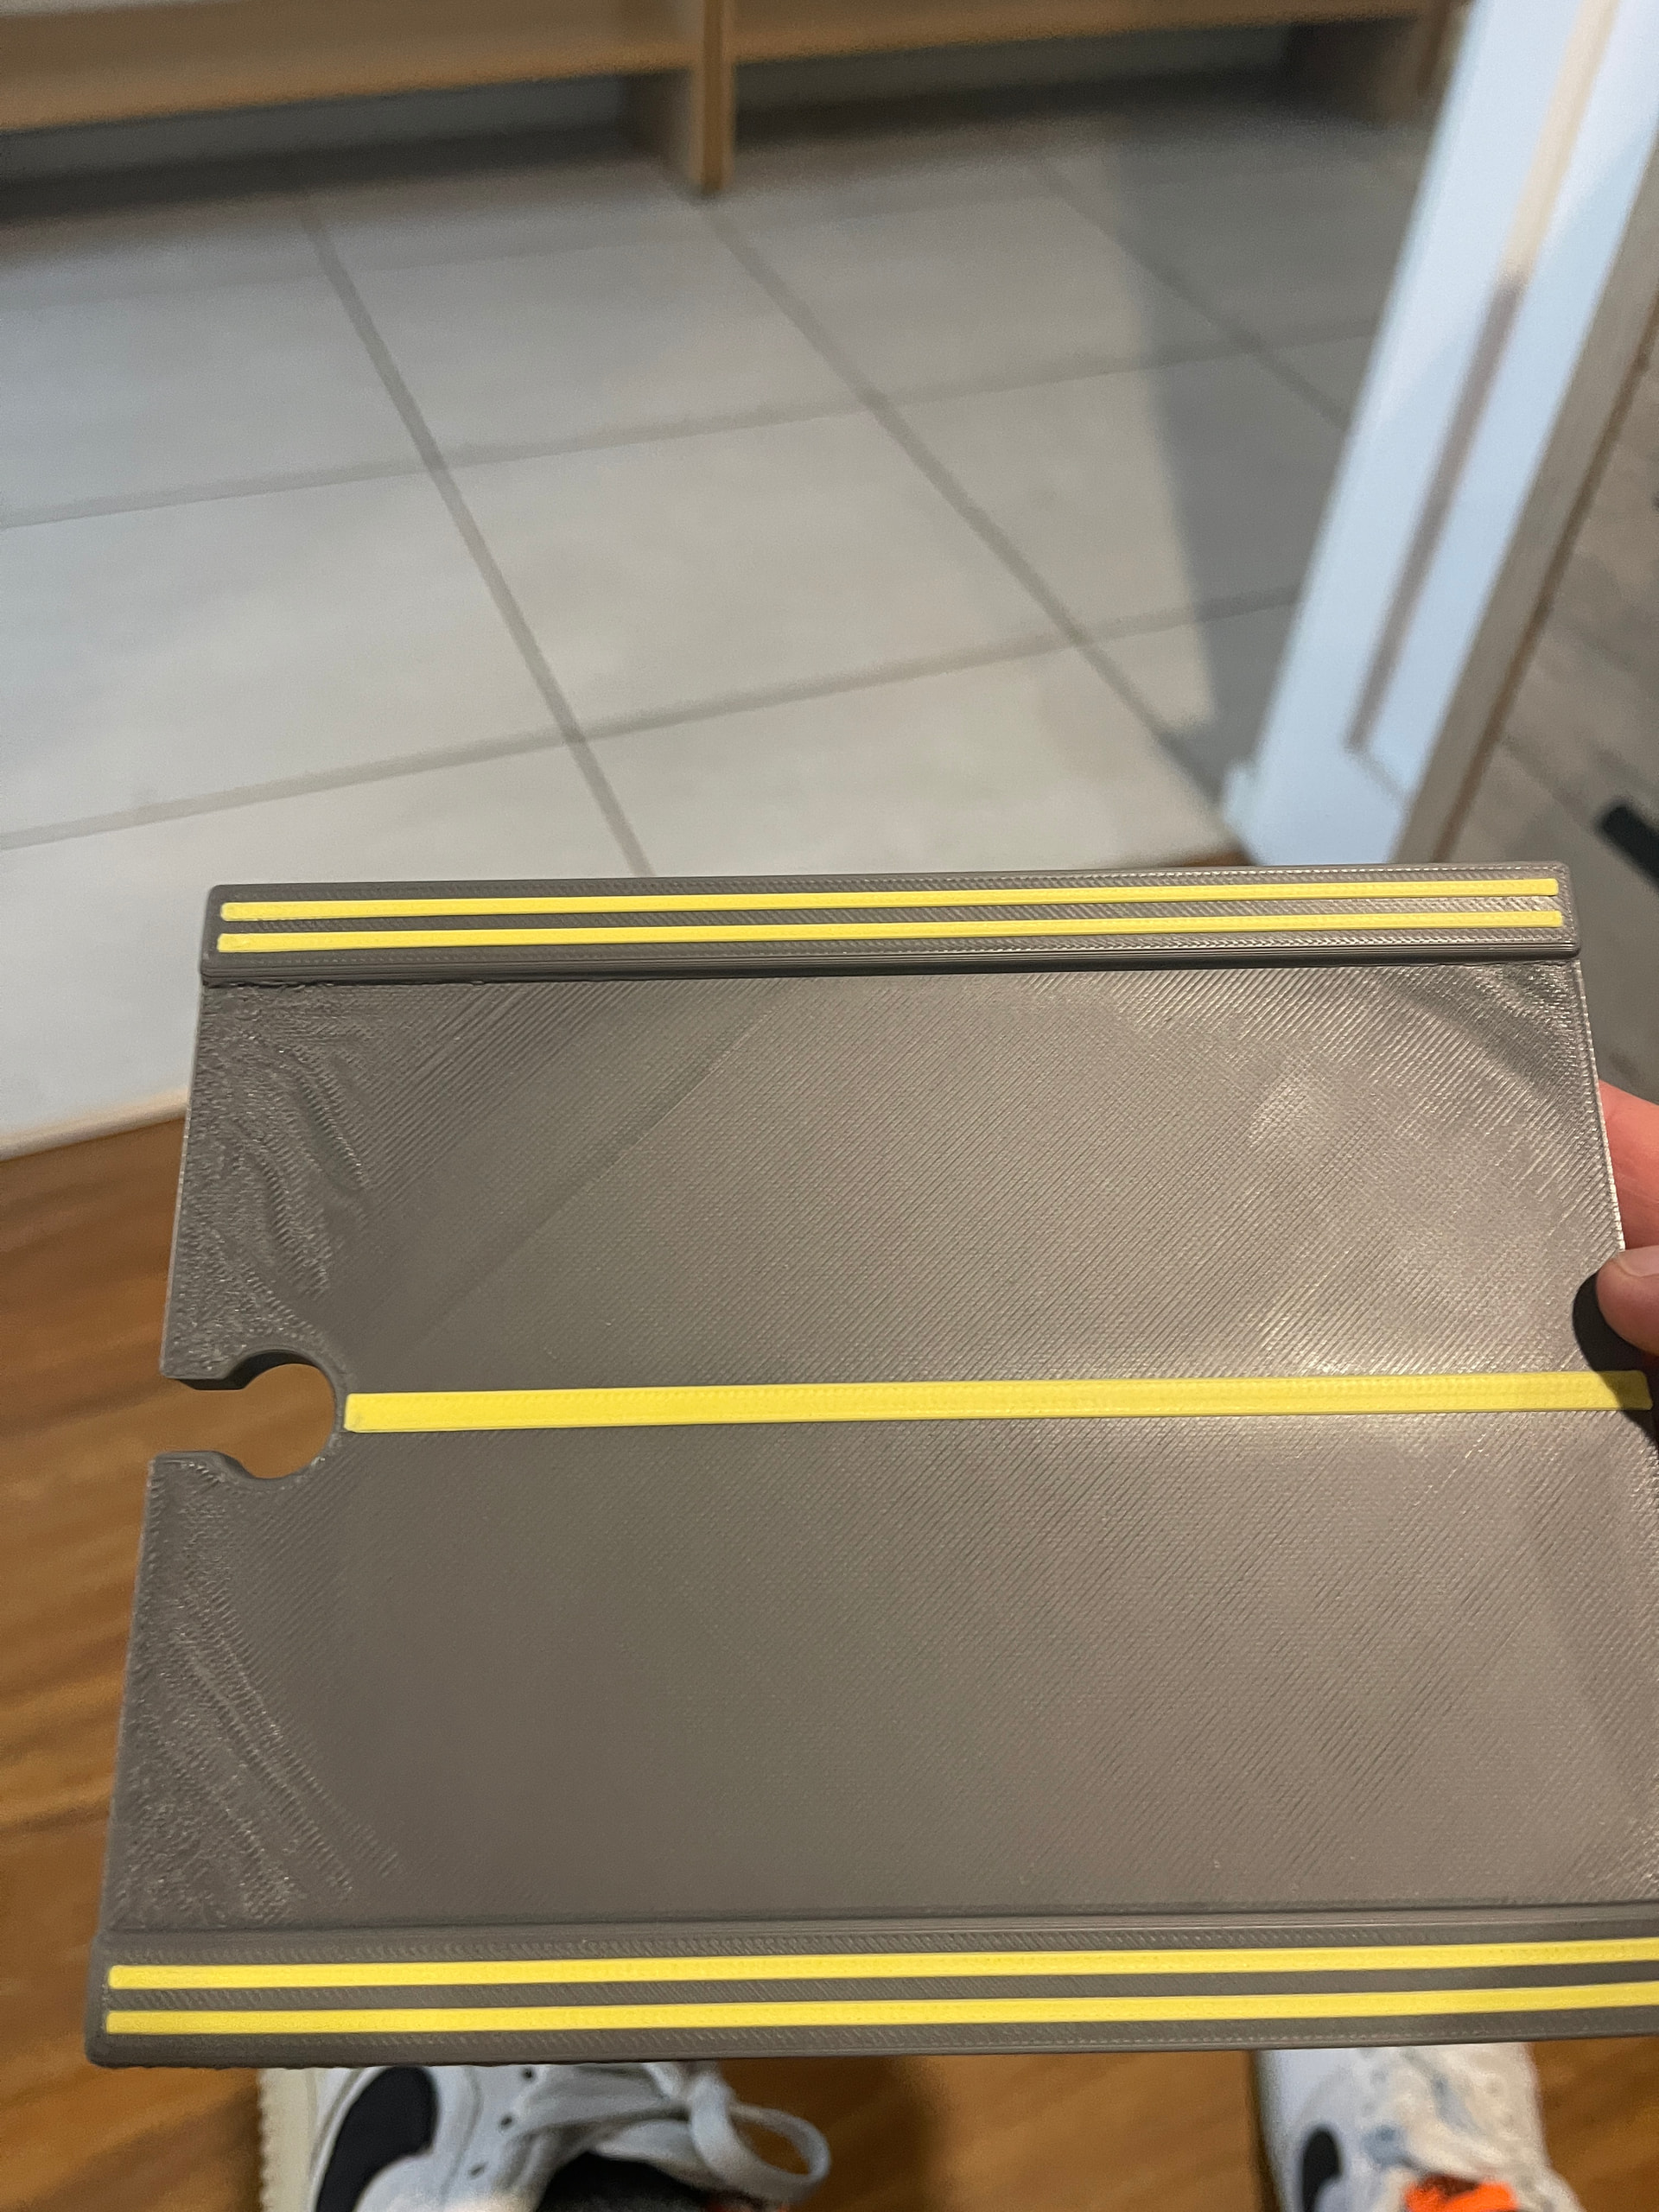
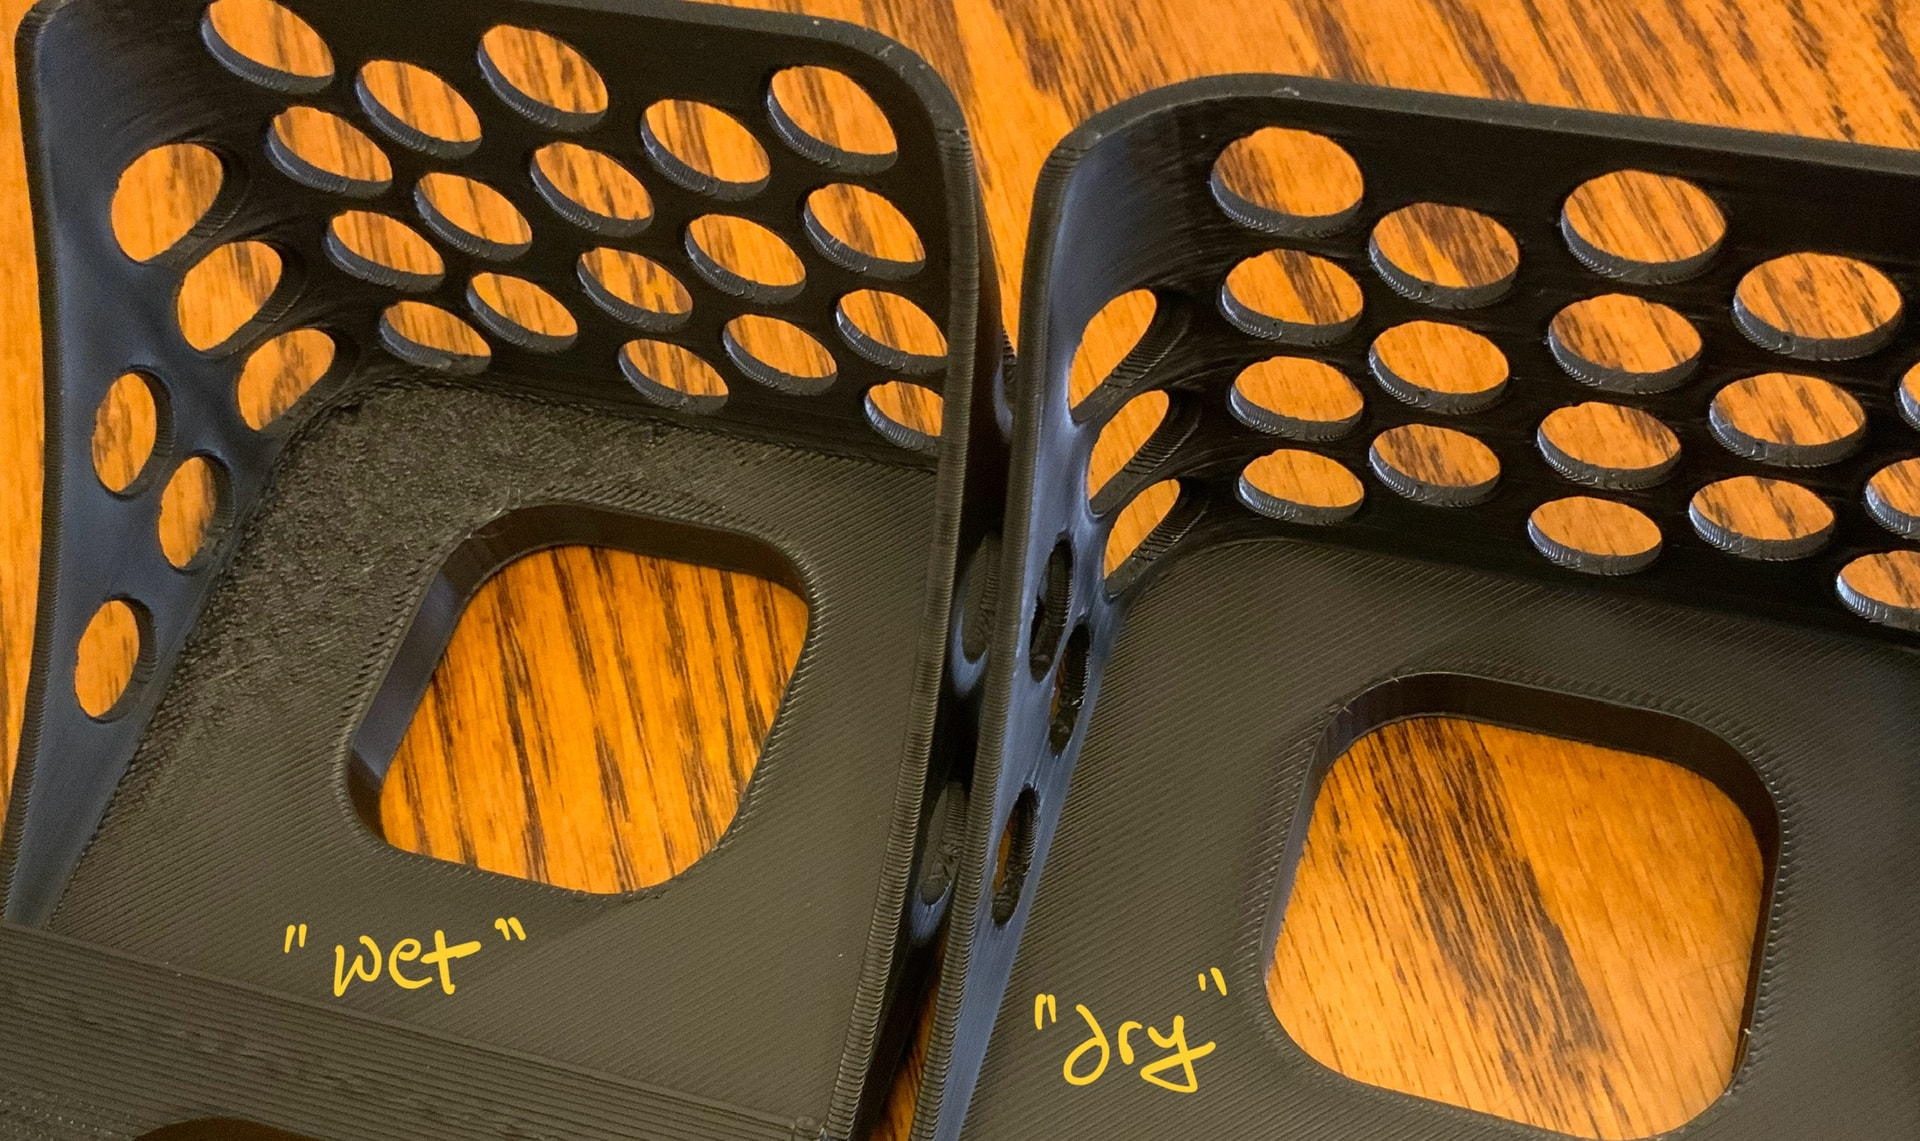
In the first image, you can see what appears to be over-extrusion around the edges. I’ve done a lot of prints and have noticed a pattern: this only seems to happen when the printer is moving back and forth over short distances. My theory is that, as the print head approaches the corners and the travel distance becomes much shorter, the extrusion rate is too high for those small movements compared to the longer runs across the middle.
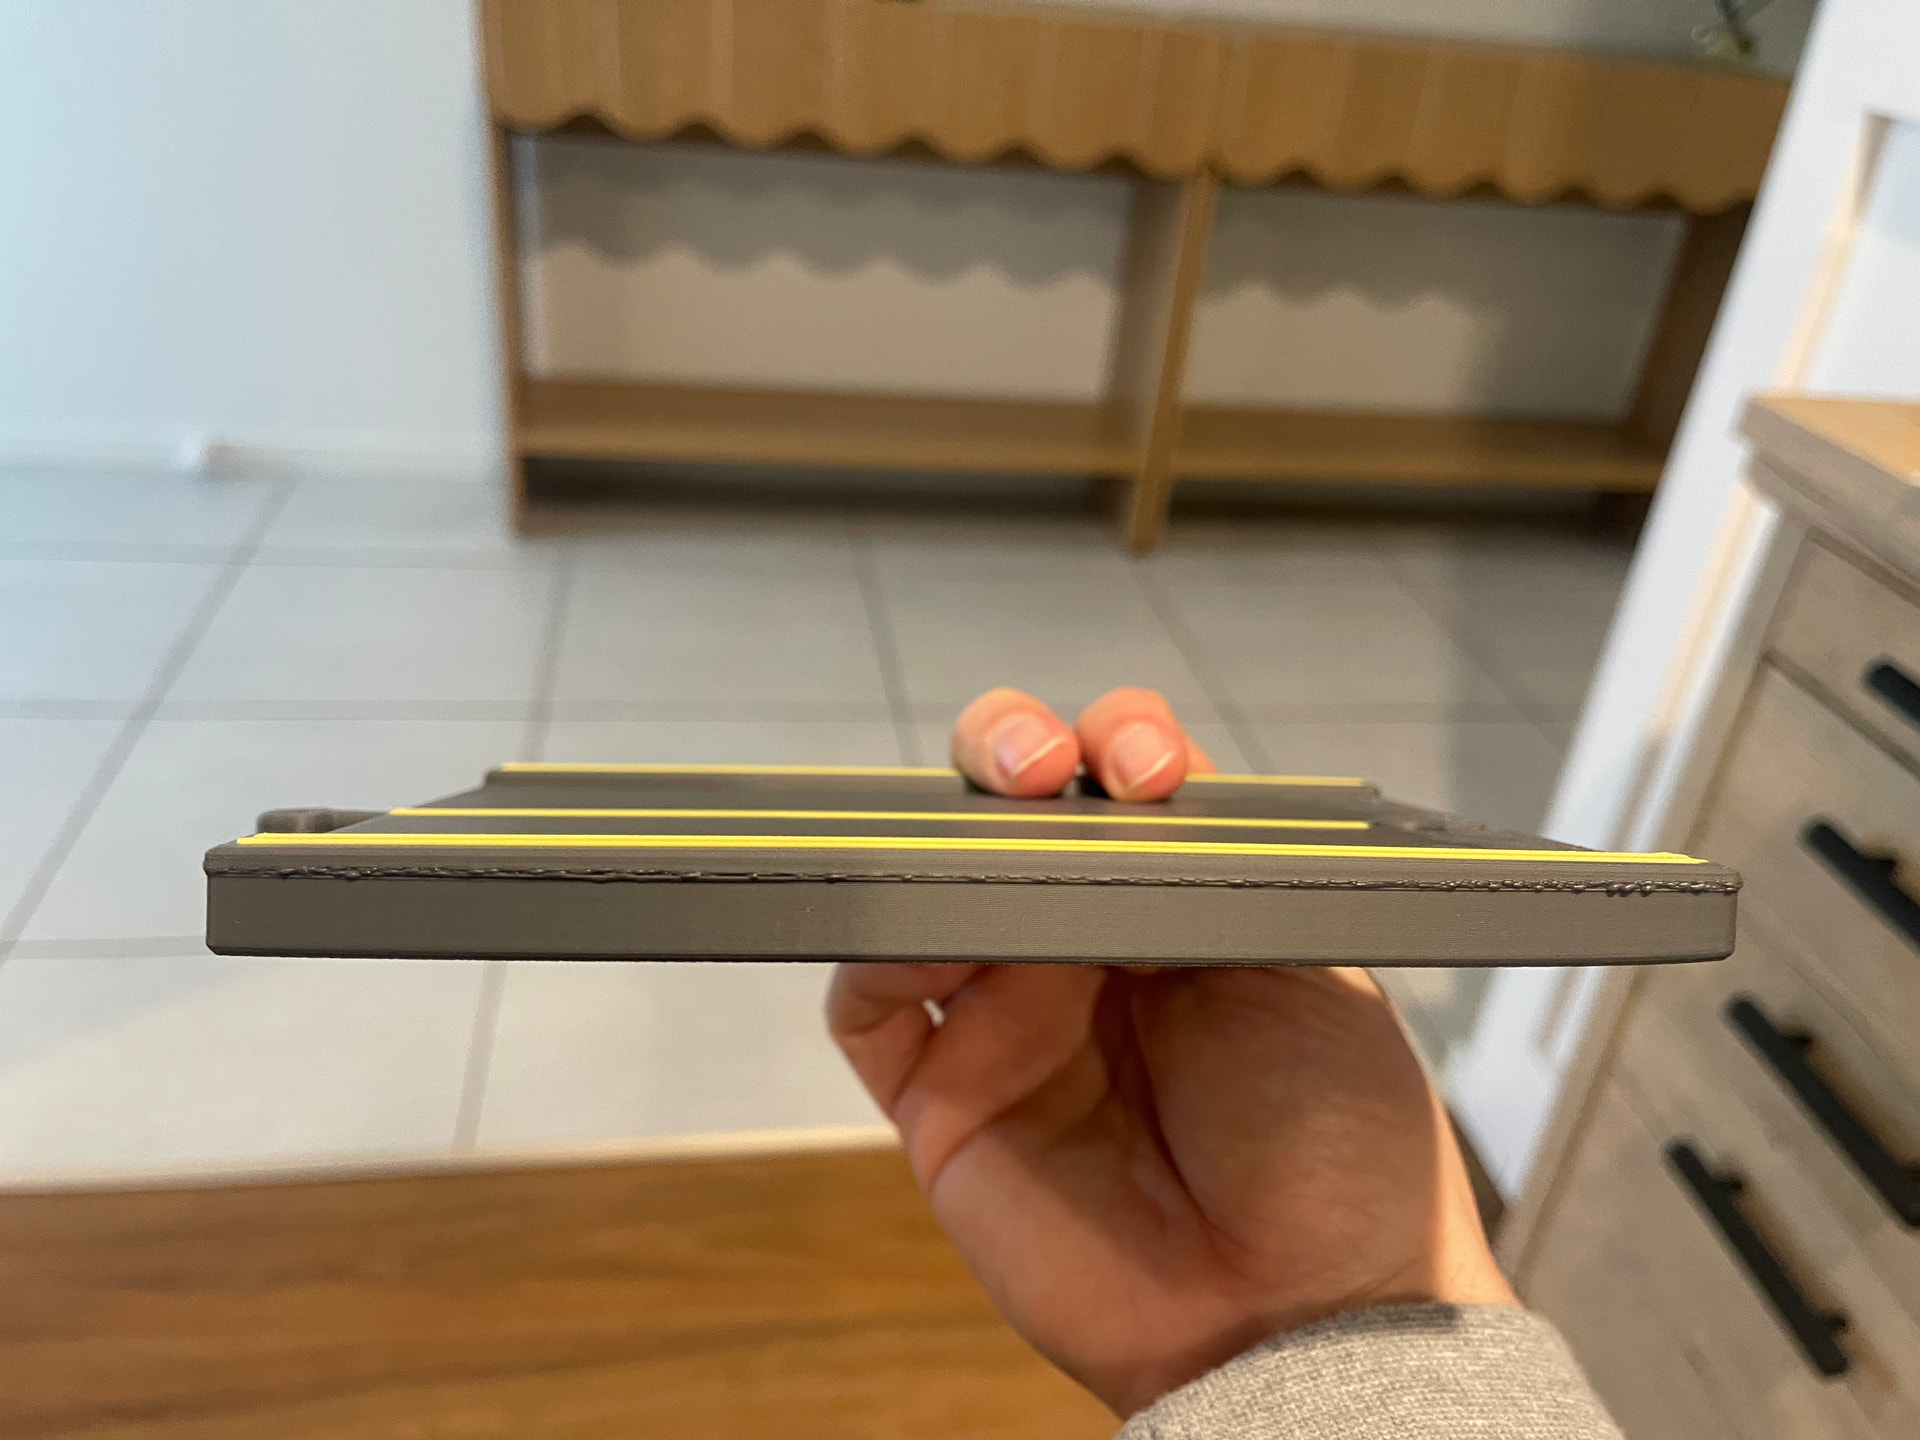
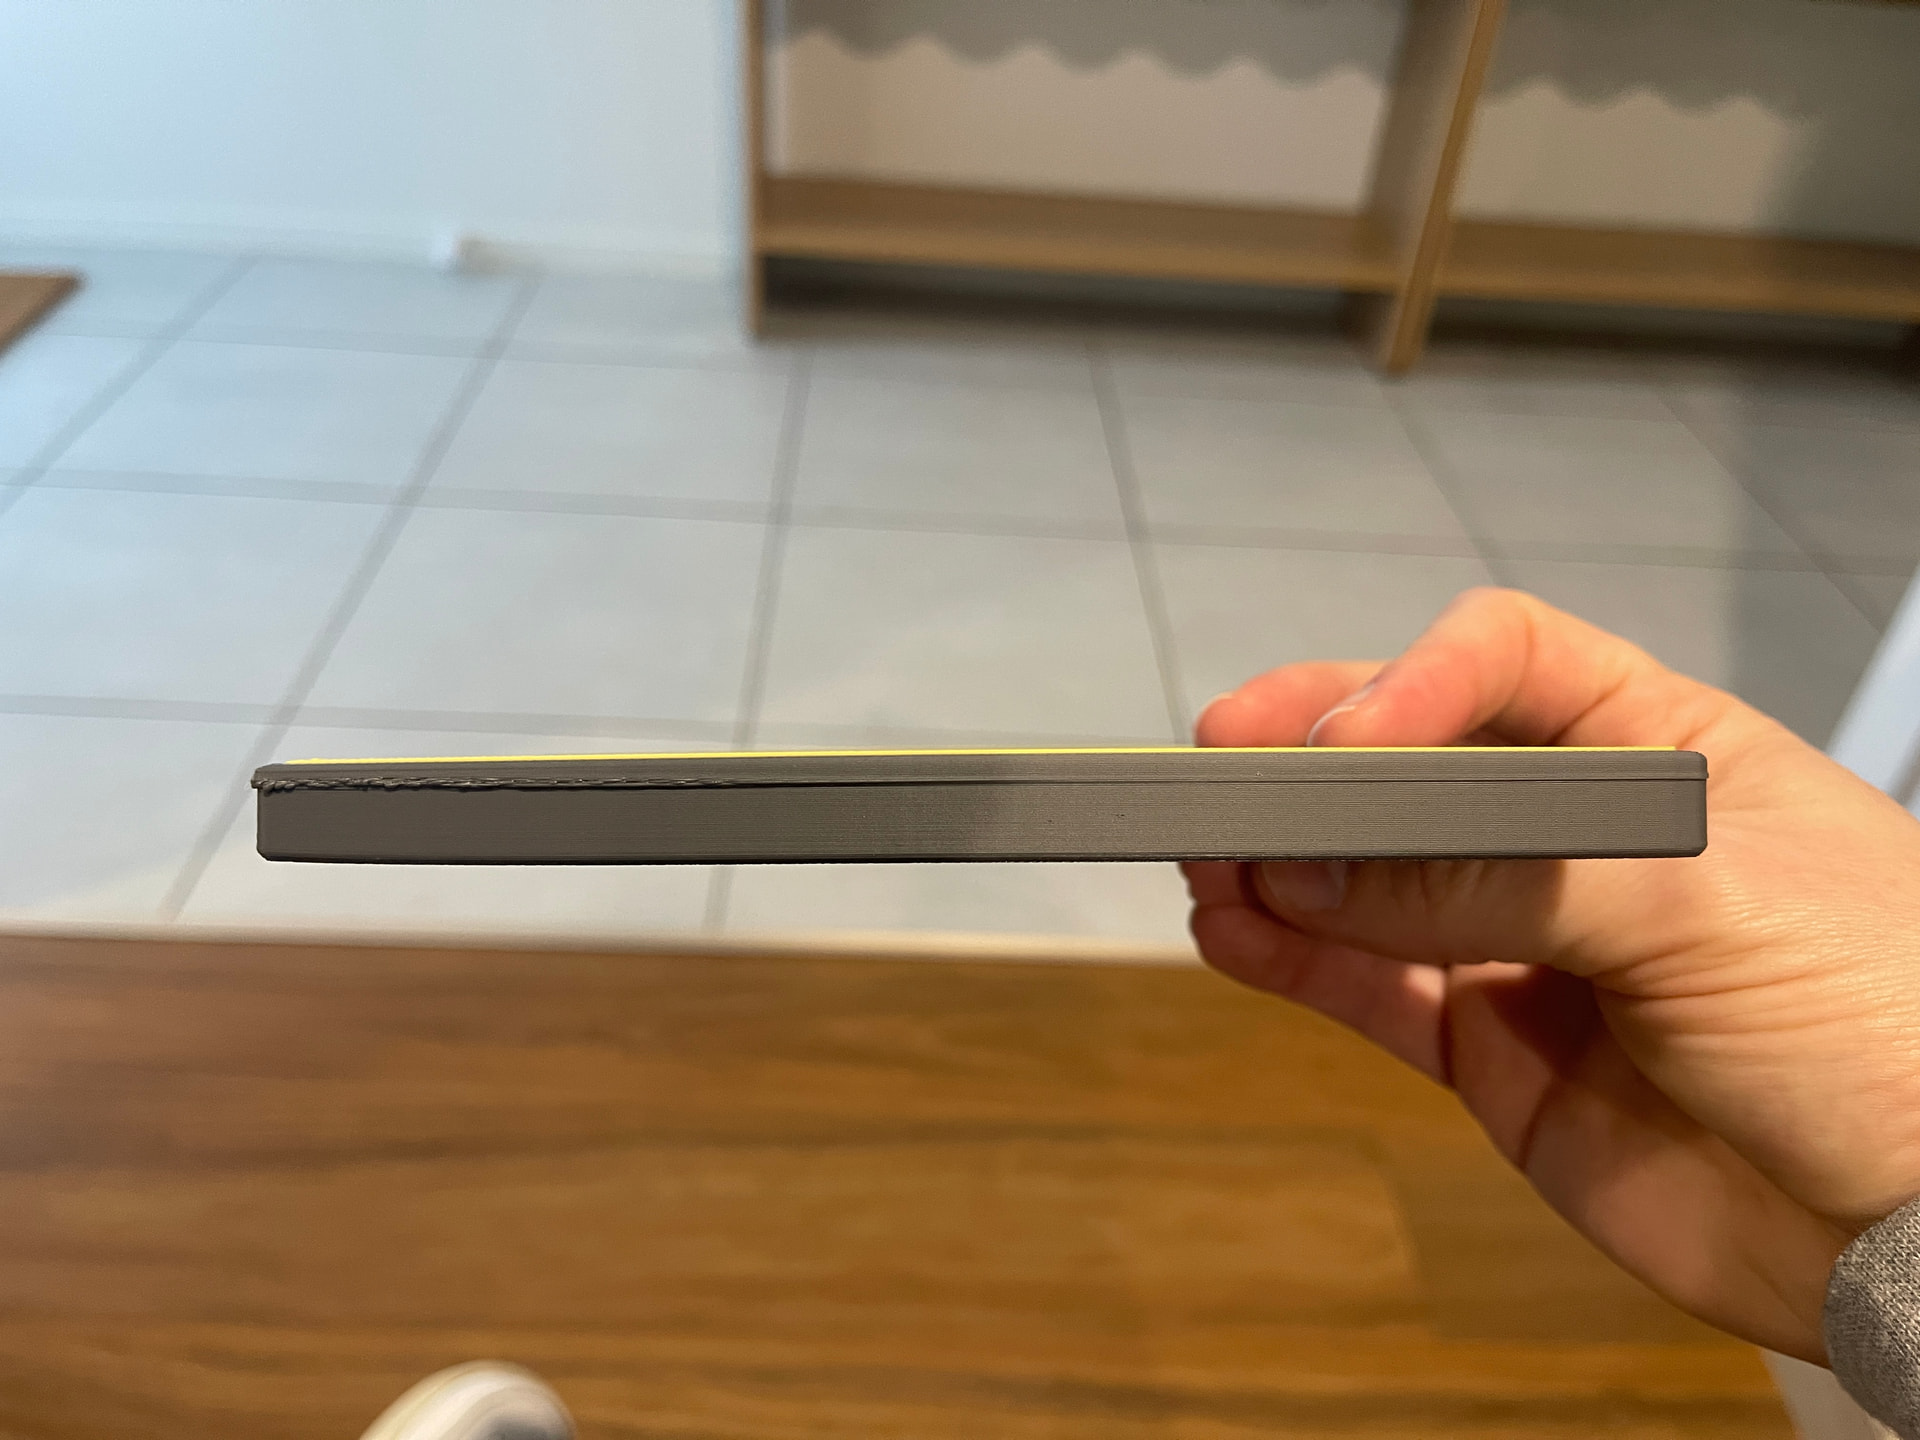
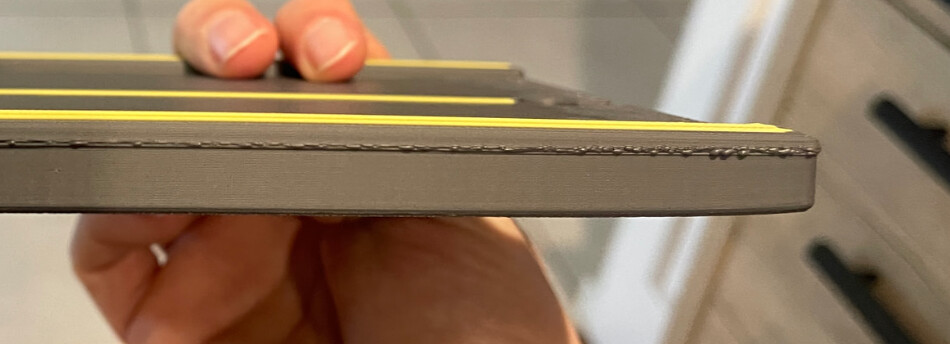
In the second and third images it’s a little harder to see, but one side of the top surface appears thicker than the other. This seems to be because the top layer is sagging or overhanging slightly on that side.
Here’s everything I’ve tested and confirmed so far:
It’s not a filament issue. Initially I suspected the cheap eSUN filament I was using. To rule that out, I opened a brand-new spool of Bambu Lab filament and printed the model immediately after unsealing it. The results were virtually identical, so I’m confident the filament isn’t the problem.
It doesn’t appear to be a nozzle or printer issue. I’ve cleaned the nozzle, checked the cooling fans, and inspected the printer. More importantly, it prints other models perfectly. For example, I printed two Bambu Lab spools yesterday, and they came out immaculate.
Because of this, I feel I’ve effectively ruled out both the filament and the printer, leaving either the slicer settings or the model itself. However, the model has excellent ratings, and I can’t find any obvious issues with it. Many other users have posted photos of successful prints. I’ve also synchronised my printer and filament settings in Bambu Studio, so I’m using the correct profiles.
At this point I’m genuinely baffled. Through a process of elimination, I feel like I’ve ruled out everything obvious. Has anyone experienced something similar or can suggest something I may have overlooked? The issue seems to occur only with this specific model, yet everyone else appears to be printing it successfully.
This is easier said than done but if you have a decent thermal device to visualize the heat bed temperature across the entire 250 × 250 build plate that might be worth doing. I would suggest that if you have access to hardware it is worth doing regardless of whether you are or are not having build plate adhesion issues or not. I have a FLIR thermal imageing adapter that plugs into my Samsung Android phone and it was enlightening and dictates my model placement. Ive checked the heat bed multiple times, the temperature profile the same whenever I check it and FLIR is a recognized leader in that technology.
I absolutely did not buy it for 3D printing. I bought it as a troubleshooting tool for work.
The bed is vital to 3d printing and that is information everyone should have. The profile of my P1S was not what I expected but it definitely factors into model positioning
That’s the whole point of pressure advance - it ramps pressure up and down in advance of a nozzle movement change.
That said, it isn’t your issue. If it was, it would be causing other strange over/under extrusion issues elsewhere, too.
I’m almost certain the issue is caused by part warping - as it lifted on that edge, the 0.2mm of new height for the new layer to be printed in disappeared due to the upward curl, so the only place the filament being extruded for the outer wall loops could go was outward.
Dry your filament before printing, and clean your build plate very well with dish soap, hot water, and a nylon scrub brush. Dry with clean paper towel afterward.
If the warping persists, you may need to use glue, add a brim to the part, or both.
If the model bends upwards due to warping it gets closer to the printhead and that will look exactly like it does on your print. There’s too little space between the print and the hotend and it will look like massive overextrusion. At my case it even lifted the plate from the magnetic bed. Depending on the material you use you might have to play with temperatures and cooling to get warping under control or reduce strength of the model.
Some good answers here. The curling/lifting off the build plate is what is causing the surface scarring. The change in layer print time between the large flat area and the smaller border region that sticks up around the flat area is why the squish out the sides. The Bambu wiki discusses this and ways to get around it with chamfers or fillets to smooth the layer times transitions.
And about the filament being dry, I saw very similar lifting/scarring issues with wet filament that simply disappeared with dry filament. It was even the same spool of filament. Only difference was drying.
For the people posting about the filament potentially being wet though, I said in the OP that for my second attempt I used a brand new BAMBU spool - it was still sealed, and the moment I unwrapped it, I popped it into the AMS and printed it, so it can’t be a moisture issue.
@MZip any chance you can direct me to that wiki link please? Thanks
Sorry, I had a busy week right after I posted this and only looking at the replies now.
P1S and I have the door open and lid off. Material is Bambu Labs PLA.
Did not dry it, but its not the filament as I had the exact same issue with two differnt filaments and the most recent filament was from Bambu and sealed.
I also used to believe this, but the fact that the factory sealed the filament in plastic with a desiccant pack doesn’t mean it’s impossible for the filament to be wet.
Humor us and do a good drying cycle and see if it helps.
Also as others have said, clean the build plate properly and (if ABS anyway) crank the build plate temperature up to 100C, that solved a lot of peeling issues for me like you are experiencing.
Several things I am mentioning are in the comments above.
Looks to me like it is warping of the parts. This more challanging from long continuous walls.
The filament is put down at the same temperature for all the layers. The ones closest to the bed harden at the full size. Then as it goes taller it is relaying on the layers below to hold its size. When they cool and shrink it pulls the ends up off the bed. It is obviously a bed adhesion problem.
How to solve it depends mainly on what material.
Make sure you have a clean bed. Don’t touch it after you clean it.
Make sure you are using the best bed for the material.
Try a glue or something to help bed adhesion
Try a brim
Adjust some of the temperatures. Settings that might work for others might not work for your CURRENT temperature and humitity.
Try closing the chamber. It reduces the shrinkage that causes the warping. Can cause its own problems. Depends on your current temperature and humitity.
Even though that looks like a simple model, it is a challenging one to print.
To show it is a bed adhesion problem. Right after the print finishes, try pushing a piece of paper between the bed and the part. The paper will go under at the corners, and not in the middle of a side. If you wait till it cools, the paper might go in everywhere.
Others have had models curl up the build plate during printing. There are certain design features you can add to a model to make warping/curling less likely as well as controlling chamber temperature and print settings to minimize that. It’s not always an adhesion issue as illustrated in the link @simon14 posted — but frequently is.
yes that is the same warping problem it is pulling the bed up not just breaking the bond to the bed.
My best suggetion for that problem is a different bed.
ABS has a higher shrinking rate (hot to cold). this makes the problem worse.
I assume you are printing with a closed chamber. If you somehow raise the chamber temperature it will improve this problem.
is that raising that bed during the print? I am guessing most of that print was with the bed down. and it came up after cooling.
I am printing with PLA and an open chamber as per Bambu labs guide. I used to leave it all closed, but I read on Bambu labs that they recommended having it open so have been doing that ever since (about 2 years) and never had an issue until now.
I have run out of filament for now for this model but more will arrive tomorrow. I will try some of the suggestions you have all provided and post back with an update soon. Thanks all
In general it is a good idea to leave open. Depending on your current temperature and humitity.
One of the issues is for high speed they have upped the temperature. To get the plastic to flow at that rate. But the higher temperature plastic shrinks more. So many of the settings depend on other settings.
A full bed print, with a wall on one side is a challenge to print.
Others said it better but even if its new, a plastic wrapped spool is not confirmed dry, its only dry when you dry it. Mylar bags can have a hope of it being dry from the factory, and even then its not always.
IMO your edges are warping up off the plate. If its not curling off the plate, its bringing the plate with it, but that is warp imo. Huge full plate contact patches can and will warp so strongly it brings the plate with it. When we used to print on glass, it shattered the glass.
So, if your plate is staying down, try a brim first, glue second.
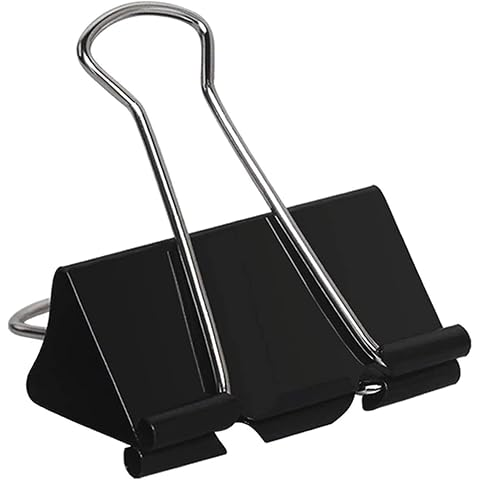
If your plate is raising up, you need to consider some more wild things. People use bed clips to physically restrain the plate, which might work.
After filament is made they run it trough a water bath to cool it down. Sometimes this water overwhelms the desiccant. Places that use the aluminized bags are more expensive and are more likely to dry, but not guaranteed. I have not seen warping from moist filament. Bad surface quality, but not warping. Very hard to argue drying is not helping. But maybe not for the problem described.