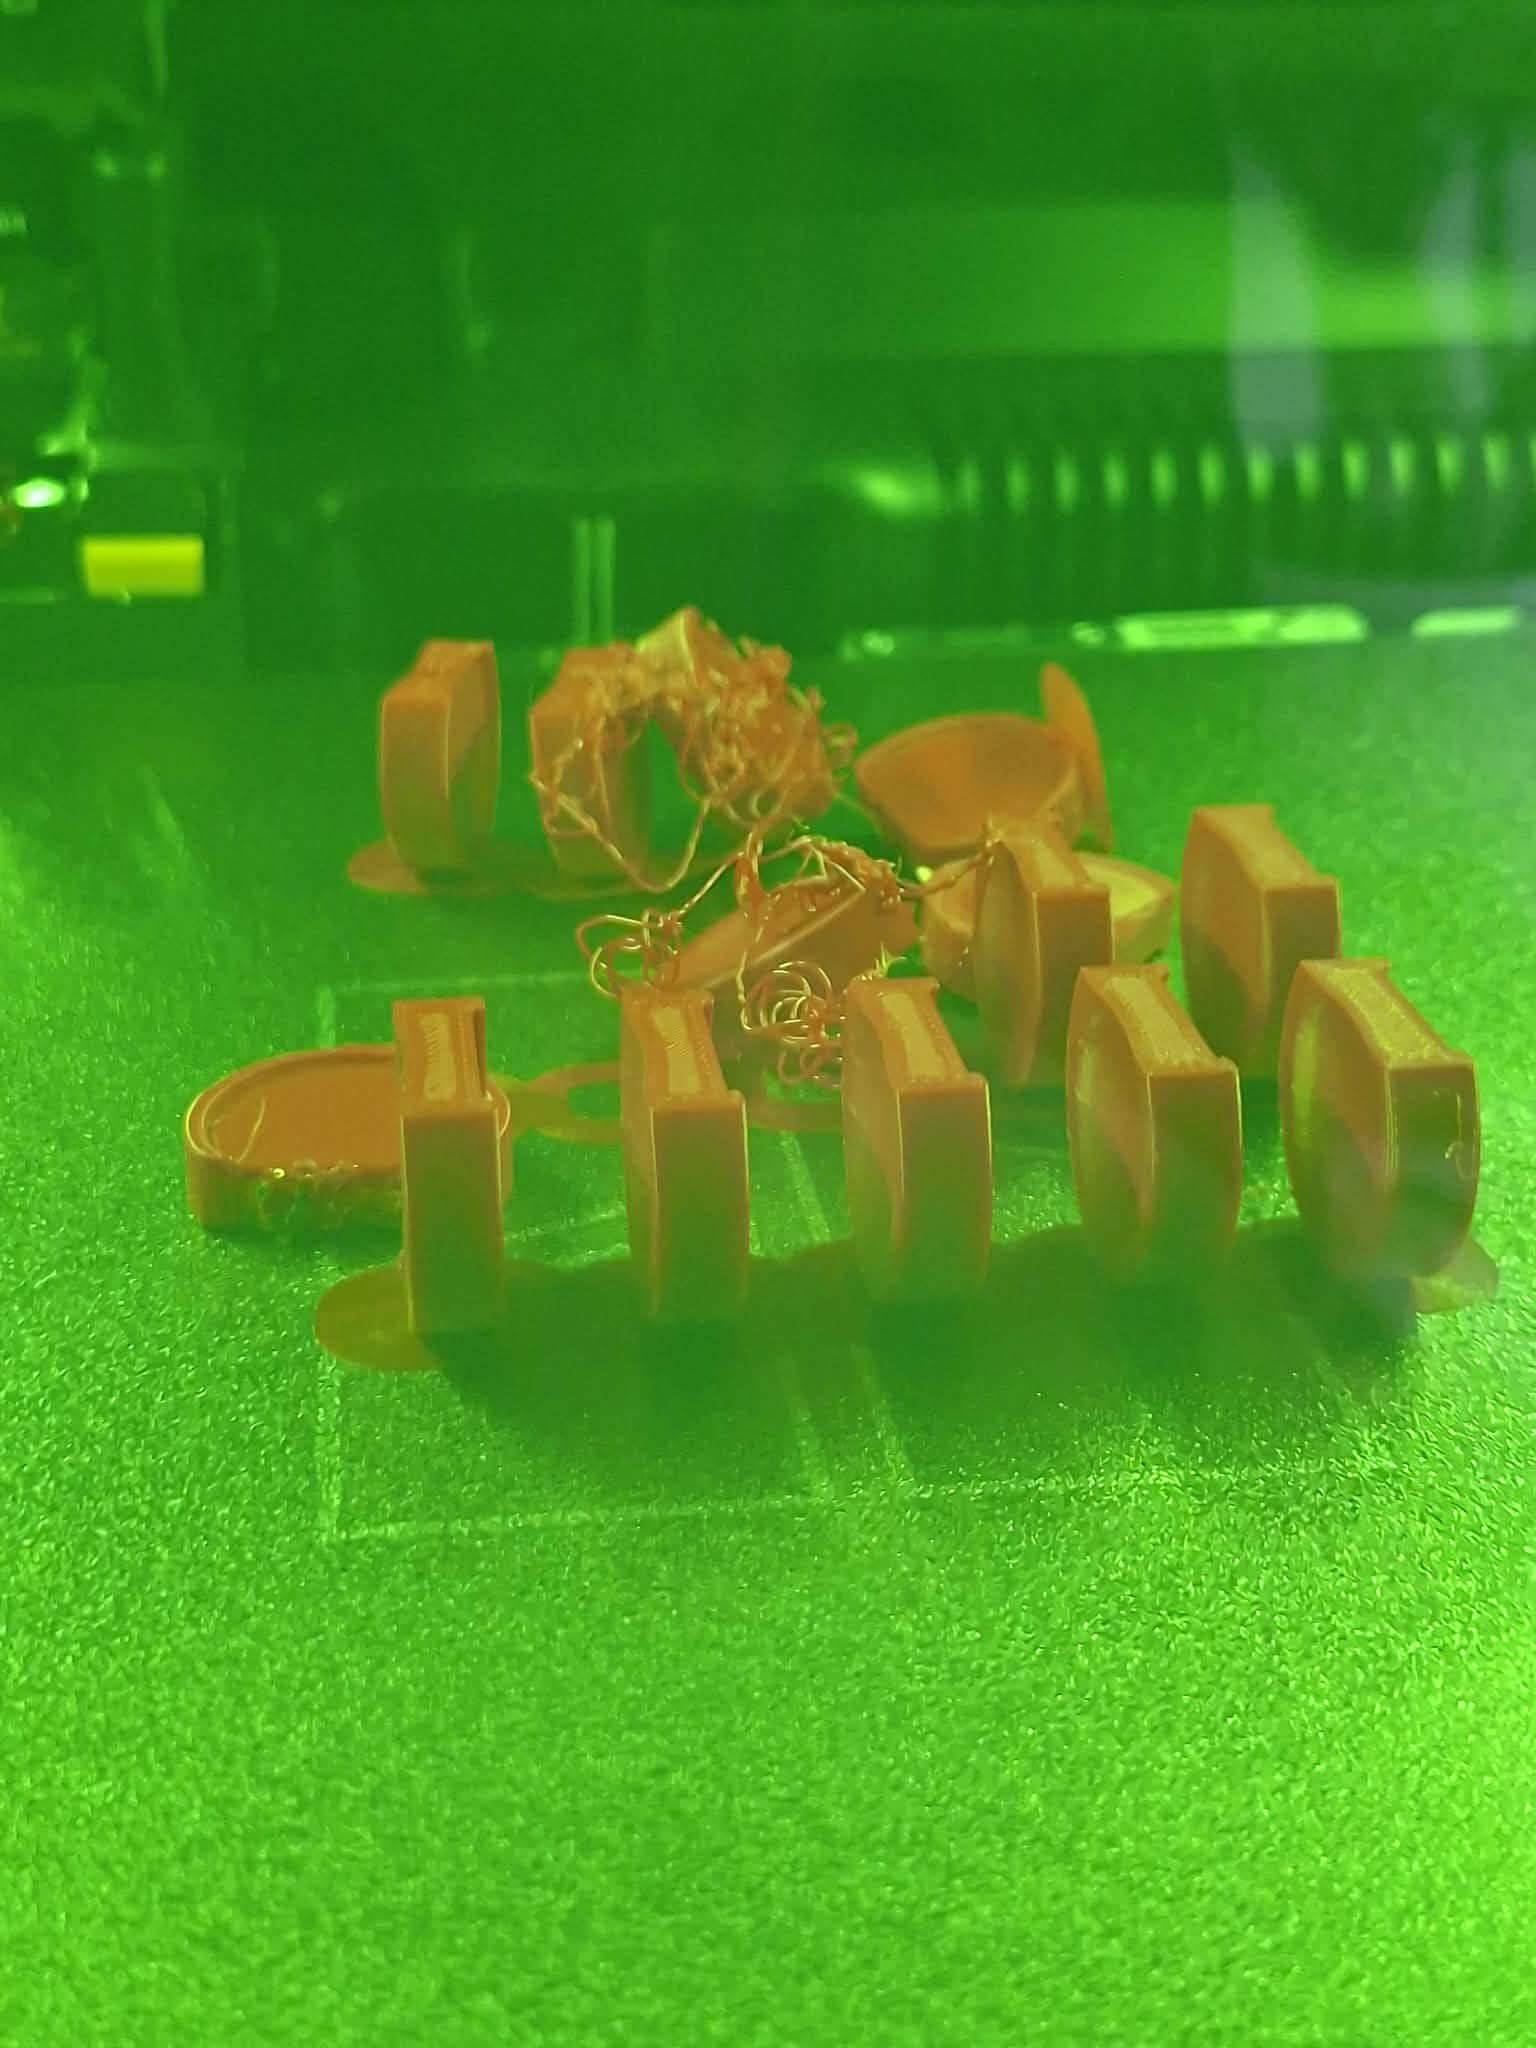
The pieces print very well for most of the print, but when they reach approximately 80–90% completion, the top layers start to become messy and the nozzle eventually hits the piece, knocks it over, and the print fails.
I have tried:
printing several pieces together;
printing a single piece at a time;
changing various print settings;
adjusting speed, temperature and cooling.
Has anyone experienced a similar problem when printing small, relatively flat objects such as checkers pieces?
First, make sure your bed is clean for best adhesion. Dish soap, hot water, nylon scrub brush, and dry with clean paper towel afterward.
It’s likely that you’re getting a bit of nozzle oozing as it jumps from part to part and those are what’s getting caught.
To avoid this, make sure your filament is fully dried following the mfg’s directions, and do both a flow and pressure advance calibration with this filament.
You can also try putting the pieces much closer together - the smaller the jumps, the less it relies on pressure advance and the less time for noodles to happen.
Oh, and go back to all the default settings before doing any this - there’s no way to know what the impact is of all the things you changed trying to diagnose it.
One other thing I do sometimes for very tall models - set them on the slicer so the edges are juuuuust touching each other. The parts then support each other and reduce the potential for getting knocked over. So you could align them into a square pattern or a + shaped pattern. You may need to do a little cleanup at the touchpoints after, but you’re already doing that for the brim anyhow.
Looks like you’re doing good with mouse ears or brims, but you still have a small contact area with the build plate.
You could try glue or redraw those checkers to be hexagons or octagons so you get more contact.
Another approach would be to paint supports on in Studio to help hold the pieces vertical. Support may leave a little scarring and you’d want the support in place before the print gets where it fails.
And plate cleanliness can also matter. Any fingerprints or oils may be causing reduced adhesion.
You can also add 5-10C to the build plate temperature. That also helps adhesion.
There are small but the contact surface is only 1 small line and I bet your brim is only 1 layer so it only brims that 1 line. Do one of the 3 below in that order
Try to increase the number of layers of that brim
Force support on the bottom circonference up to some layers (you may have the change the threshold angle for the support to generate)
Change the design to have one side flat rather than curved and print flat on that side
Hi @user_1335105300 , welcome to the forum. Here are a few tips that have worked for me:
-I would recommend like @CarbonForge said to clean the plate REALLY WELL.
-In models that I’ve had adhesion problems, i have set the elephant foot compensation to 0 and added a 20-25mm brim.
-I would try printing it more “low poly” and not trying to do a circle printing it on its side (or printing it flat and using support material).
If you see the problem still continues, try increasing the bed temp 10°C, doing flow rate calibration and pressure advance (over extrusion can cause the model to be slightly bigger and cause the nozzle to push it away), and making the first layer wider, so it has more grip area.
-(I’m not sure, but it seems as if you use the laser cutter so make sure there isn’t any soot or ashes or dust that could cause the plate to get dirty again)
If you want 2 concave surfaces, glue them together (put a 2mm hole in each part so you can stick a piece of filament in there to align the 2 parts, or print a jig)
edit if you don’t want to learn cad, take the model of 1 peice, and cut it in half with the slicer, and put the halves flat on the plate
If you cut them into two semi-circles you you could consider two different shades of colour for each half to make them look like you went fancy on purpose!
Also, you could also consider making them a polygon with enough sides to present “round” but at least offer enough extra surface area to print from.
Another possible solution would be to add support enforcers to the bases. That might help overall. And maybe reduce the overall travel speed/ acceleration around 20/30% ish.
Also, I’ve seen several prints being knocked out of the plates with gyroid.
Try one model with one infill and another with a different infill to troubleshoot