Can anyone suggest how to fix what is going horribly wrong here. Printing with a H2D in Fillamentum ASA Extrafil using a printer profile constructed from Filamentum’s printing recommendations and generally the ASA generic one but slowing down the Max volumetric speed to 4 mm3/s. I did dry this beyond the manufacturers recommendations at a temp of 80C. I’d like to get this one nailed for outdoor use around our house as it’s a close enough color match for some of our trim. Unfortunately neither BL nor Polymaker has a close color match.
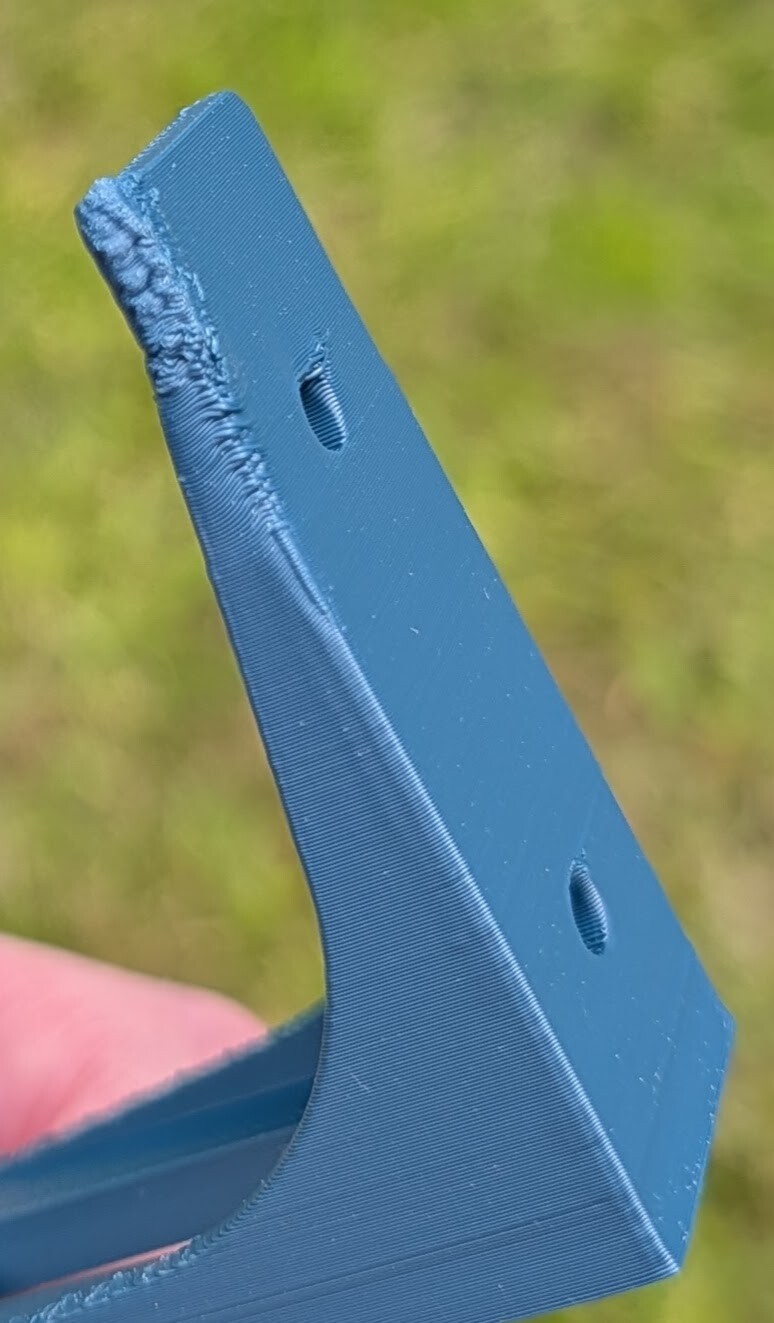
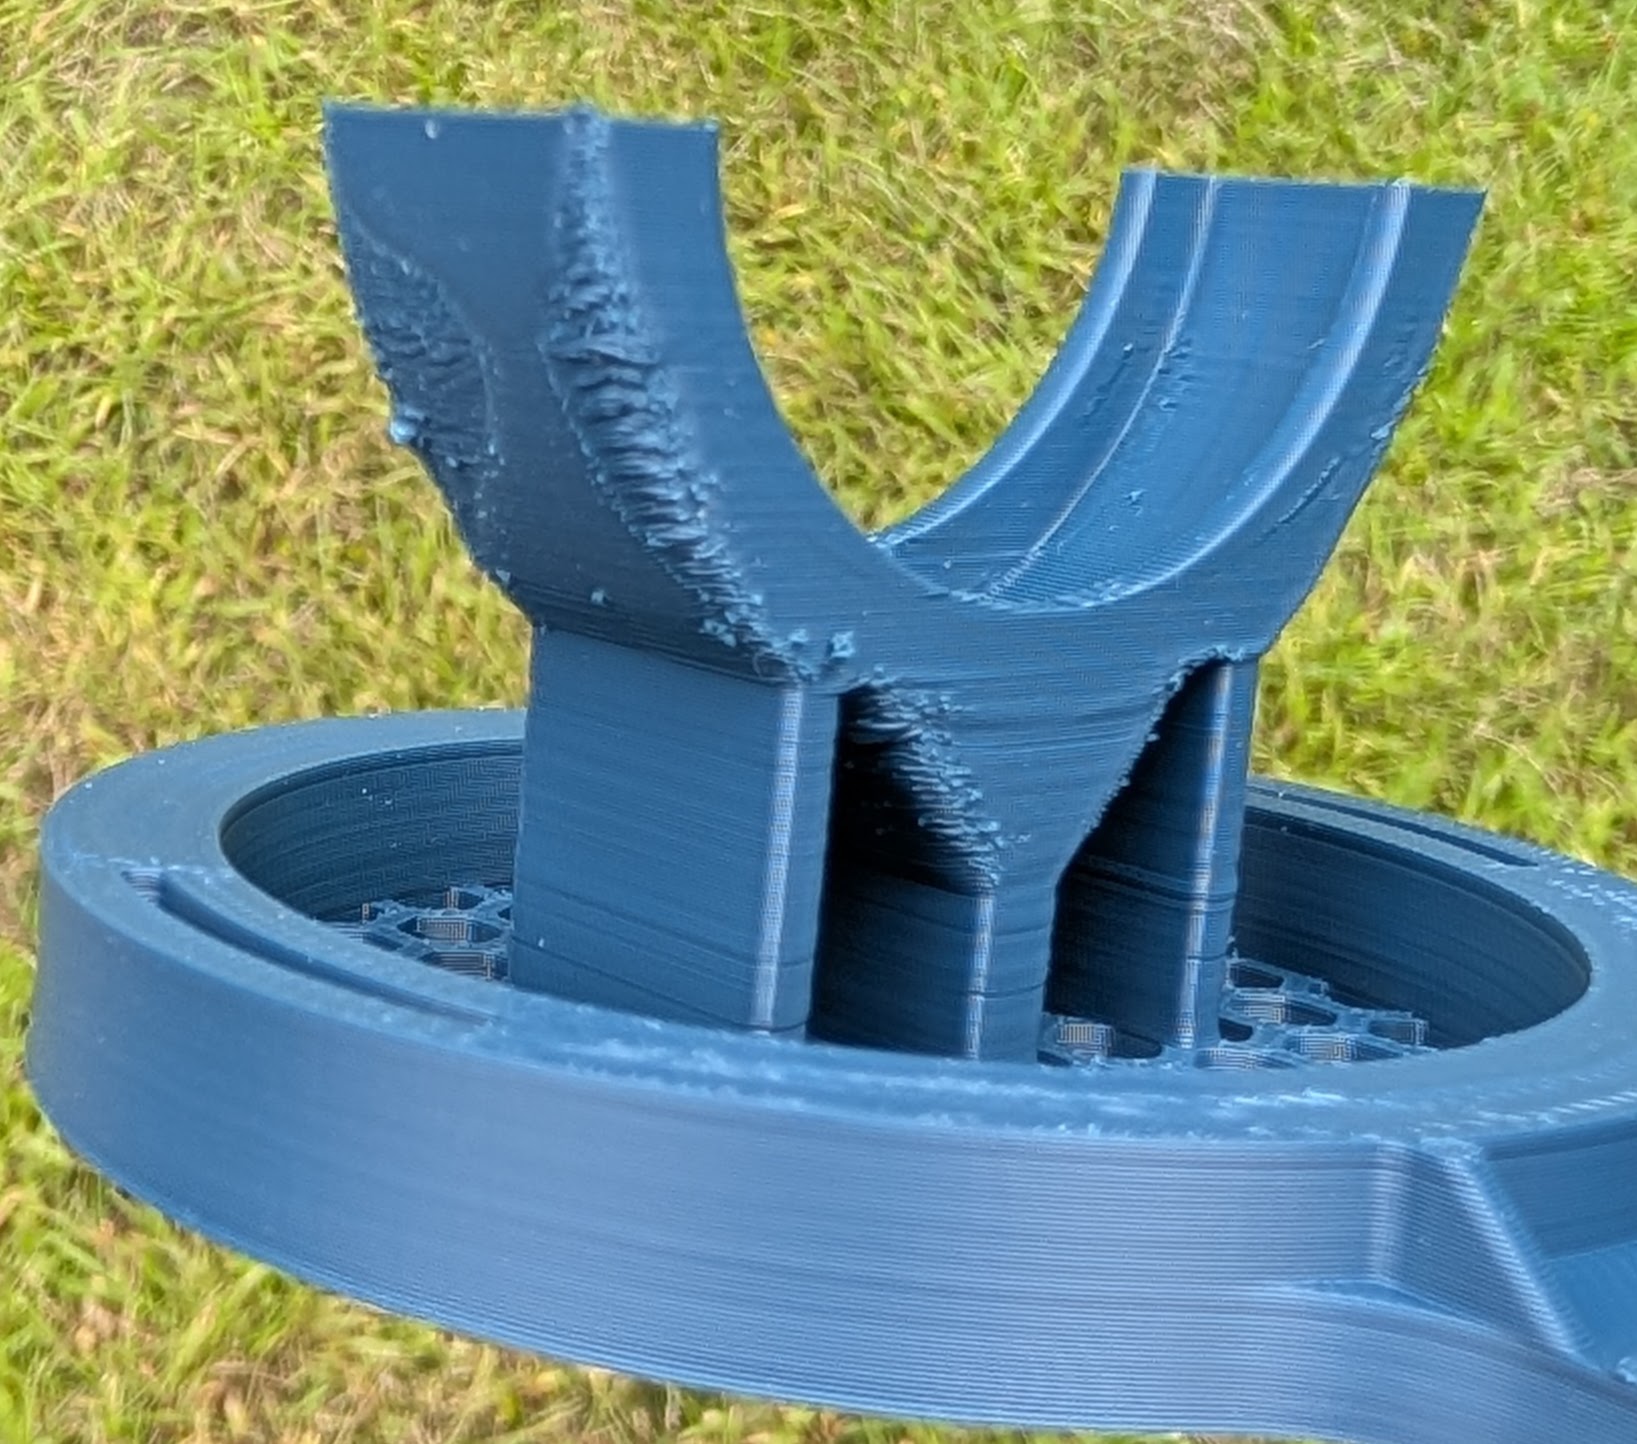
Slowing the max volumetric speed is one thing, but it looks like there could be a cooling issue where some areas aren’t getting a chance to cool sufficiently before the next layer goes on over top.
On your slicing results, select “layer time” and see if the areas that are sagging corresponds to layers with low layer time.
Too much can cause damage to the filament.
They give information for a reason. This isn’t a pet or baby, you have to take of this!
ASA needs a warmer temperature when printing. The recommendation is to set the bed temperature manually and leave the printer closed up for a while before you start the print.
This could be related.
Overview
To print successfully with ASA filament, **use an enclosed printer, set your nozzle to 240–260°C, and keep your bed at 90–110°C.
Essential Printer Settings
- Nozzle Temperature: 240°C to 260°C (start around 250°C).
- Bed Temperature: 90°C to 110°C.
- Cooling Fan: Off or very low (0% to 15%) to avoid interlayer cracking.
- Print Speed: Slow down to 30–50 mm/s, especially for the first layer. [1, 2]
Environment and Adhesion Tips
- Enclosure: Highly recommended to trap heat, prevent drafts, and stop warping. Preheat the chamber for 10–15 minutes before starting.
- Bed Adhesion: Use a brim and apply an adhesive like glue stick or specialised bed liquid if needed on PEI sheets.
- Dry Your Filament: Dry ASA at 60°C to 70°C for 4–6 hours if you notice popping or poor layer adhesion.
- Ventilation: ASA releases styrene fumes and strong odours when heated, so print in a well-ventilated garage or workshop rather than a living space.
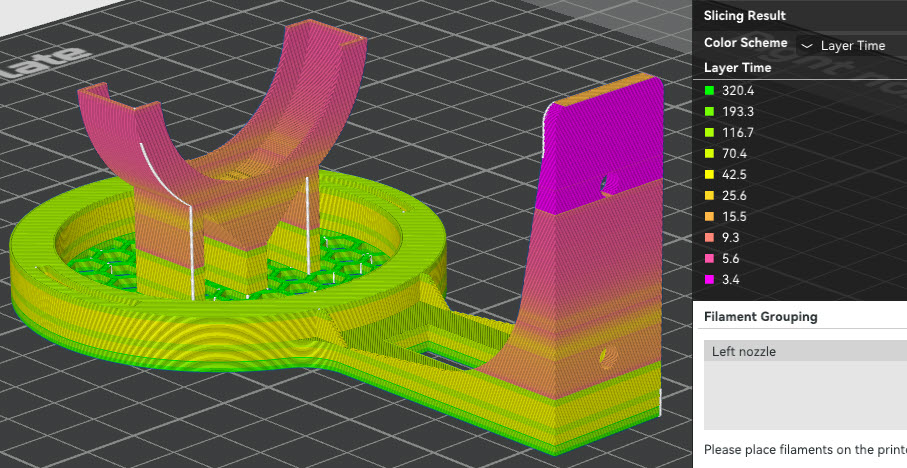
I see this when printing ASA as well. I’ve found some manufacturer part fan speeds are set too low.
As long as your chamber is maintaining a stable temperature of atleast above 45C, increasing your part fan speed can help.
I’ve had good luck increasing from say 30% max fan speed, to 50% or 60% max fan speed, without reducing my max flow rate.
I just took the generic ASA profile and adjusted the fan speed to 55% for layer times of 16 seconds or less. Left the max volumetric speed at 12. What a difference. Wouldn’t rate it a 10 but at least a 9.5. Thanks for the suggestions.