My first print attempt on new 0.2 nozzles errored out with extrusion motor overload after a couple hours. The filament was at 37% humidity, but I wanted to get a print out and was thinking about all the hobbyists out there with open frame printers and filament reels ‘hanging in the breeze’ and I went for it. Currently, I have to stop prints due to adhesion issues. Essentially new PEI textured plate, detergent washed, then Bambu Lab (BL) 3D Printing Adhesive added when washing didn’t help, very slight improvement. 20% RH in AMS-2 after 12 hr drying cycle. BL 0.08mm Extra Fine 0.2mm Nozzle process settings. All equipment has very low hours. Switched to 0.2mm 1st layer thickness from 0.1mm that lifted very fast. Longer runs lay down best, but fine detailed short movements get ‘ruffled’ and aren’t clean. All observations are watching first layer being put down. Glad to share more detail but need to get this started and move on for now. Thanks.
If you want to share your file I’d be happy to give it a spin on my H2C.
Just really simply though, stop messing with your first layer height. There is a very narrow band of height for a given nozzle size that will allow the extrusion to properly wet out onto the build plate on a first layer. A thinner first layer doesn’t help, and neither does a thicker one - your first layer should be half the nozzle diameter.
Please post pictures of your adhesion failure and we’ll be happy to have a look.
For more precise troubleshooting, you’ll need the details CarbonForge already pointed out - but I can share a bit from my own experience.
A 0.08 mm layer height and a textured plate are not an ideal combination. The textured plate is a bit of a jack‑of‑all‑trades: it can handle many materials reasonably well, but it doesn’t truly excel at anything. At such a low layer height, the surface structure of the textured plate becomes one big uneven landscape, which makes consistent adhesion much harder.
For 0.08 mm printing, a smooth plate with noticeably stronger adhesion is usually the better choice. It gives the nozzle a clean, even surface to work with and helps maintain the adhesion you’re aiming for.
I’m not saying you have to buy a smooth plate, but if you plan to print with the 0.2 nozzle frequently, that could at least be an option for more hassle-free printing.
The textured plate can be a pain to clean once it has lost adhesion. But don’t give up after a single attempt.
Clean it a few more times but add a stiff, clean brush to your routine to get down into the grooves. A fingernail brush works great. But if the grime is baked in, it takes several rounds of vigorous brushing.
As for that heat creep issue with the .2 nozzles, that is unfortunately quite common for long prints with the H2. You may need to try to keep the chamber cooler (open door) and/or try to give the nozzle some time to cool of.
An example could be applying a color/nozzle change just below the troublesome layer but have the same filament loaded in the second nozzle.
Failing that, I am aware that individual users considered adding some extra cooling to the filament path with a y-splitter. Not sure how that went other than having noted that Qidi added an extra anti-creep cooler to its latest printers.
 &

Hi CarbonForge, first off, thanks! Your offers are generous. Let’s start with the photos and take it from there. Please check my responses to other replies. The photos of ‘…Failure 2’ (F2) and ‘…Failure 3’ (F3) are montages with reduced resolution for posting. Glad to supply individuals at higher res. I messed with the first layer height once for the F3 result thinking that the first layer might be less apt to peel up. F2 was 0.1mm. After it did the prime tower base layer, the next area was already starting to peel up.
CarbonForge, currently I am blocked from uploading the photos. I am working on it.
Hi RetroSharky, thanks for your reply. Good to know about the build plates. The looks of the first layers suggests to me that something else is going on too.
Hi EnoTheThracian, thanks for your comments. I am using Support for PLA filament in an HT AMS feeding the left nozzle for interface layers. Though unrelated to the current issue(s), I am starting to question doing that. I bought some spools of it thinking that it was meant for its name sake, support material. I found out the hard way it isn’t good for that. For just interface layering it seems I’ll never run out of it.
It is frustrating to me that BL is supposed to have everything sorted out, just plug and play. Yet each time I try to do something a little uncommon I run into problems. I’ve posted about such trying to run 85A TPU, where it turns out one has to go through specialized setups for success. Now, running 0.2mm nozzles I may want to keep the door open when a controlled enclosed cabinet environment for temp control is the way to go. BTW, I am running the BL cooling fan upgrade on the extruder.
It is not clear to me how a Y-splitter can help with cooling, please elaborate.
I did get some of the original Support for PLA with my printer. I used it twice. The first and the last time 
However, the formulation has changed since then and many forum members have had good experiences and swear by it.
I did not try the new formulation though as I discovered how well PETG works as a support interface for PLA (and vice versa). It can be a bit tricky with the H2 (crank PETG up to 260°-265°C if there are adhesion issues but beware of heat creep).
In the rare cases where I need even better performance, I use BVOH. More difficult than PETG (dry, dry, dry, go slow and again, beware of heat creep) but easier than PVA in my experience.
As for the Bambu profiles, they are certainly better than what we had before. But still, I am sure that Bambu could easily provide better profiles.
PLA usually works a treat, but beyond that, there’s almost always “room for improvement”.
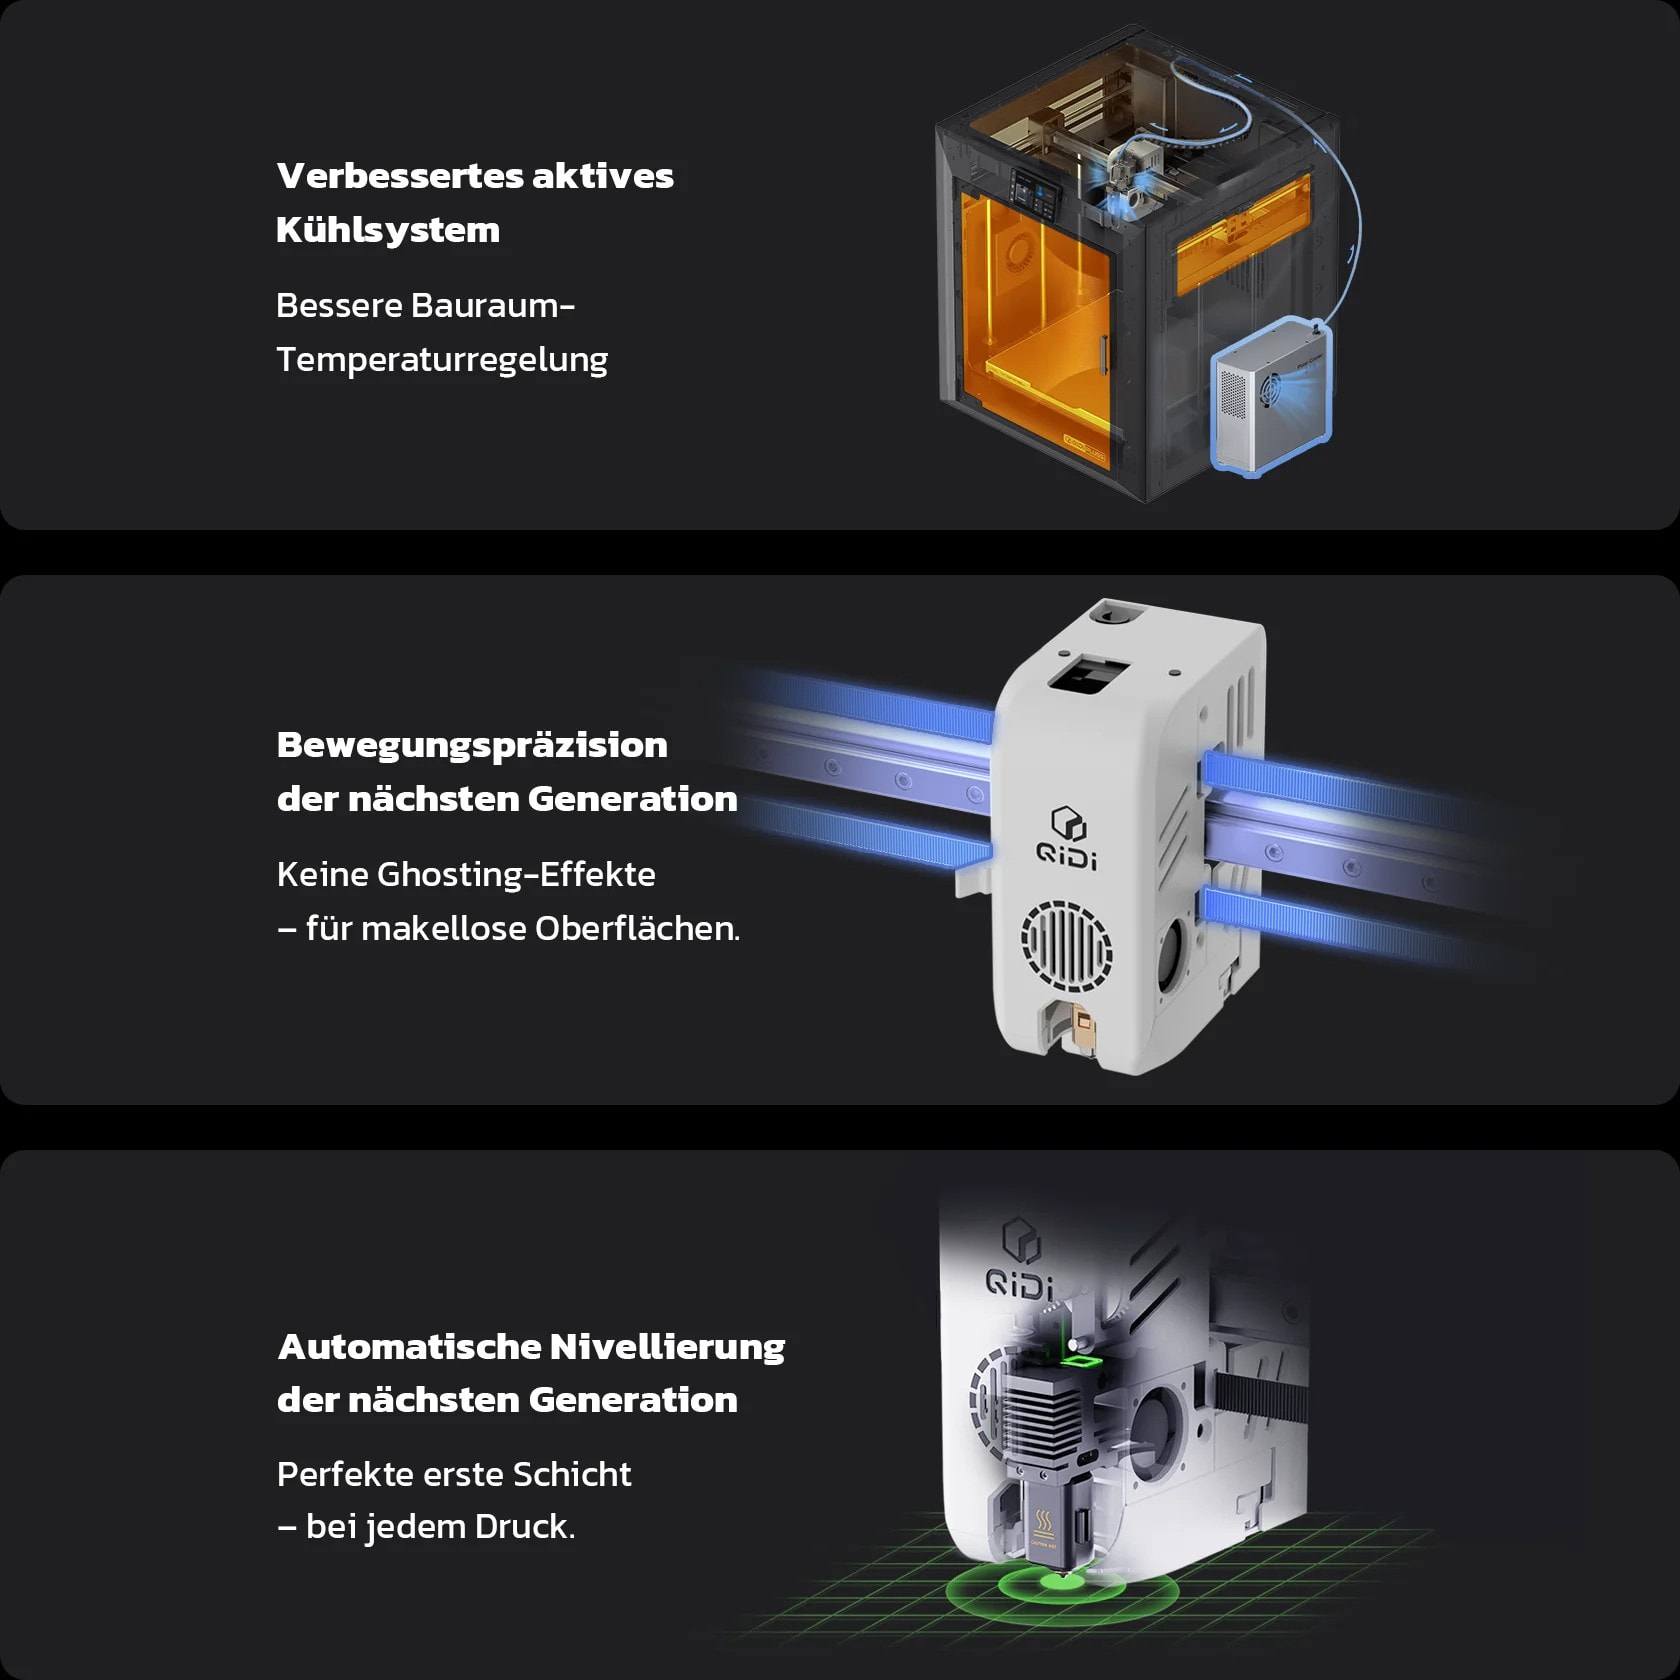
As for the Y-splitter, the idea is not the splitter, but using it to enable an additional cooling channel to provide that little bit of extra cooling for the print head. As close to the cold end of the hot end as possible.
People were considering using an aquarium air pump to feed extra air from outsides the printer through the splitter, along the filament in its PTFE all the way to the extruder.
With the relatively slow onset of heat creep with the .2mm nozzles, it may provide that extra bit of cooling to balance the heat flow at the nozzles heat break.
While do not recall any forum reports of this having been tried and being the difference between success and failure to, Qidi’s Plus 5 is advertised as using this approach (top pic). It kinda makes sense to take outside air for cooling with high chamber temps.
&
Interesting idea there…now you’ve got me wondering what could be implemented on the H2C without interfering with any of the existing sensors and hardware. Hmmmmm..
New users have limited privileges to protect the forum.
You should have a private message from @discobot, it has details on what to do in order to have your trust level raised.
Hi! To find out what I can do, say @discobot display help.
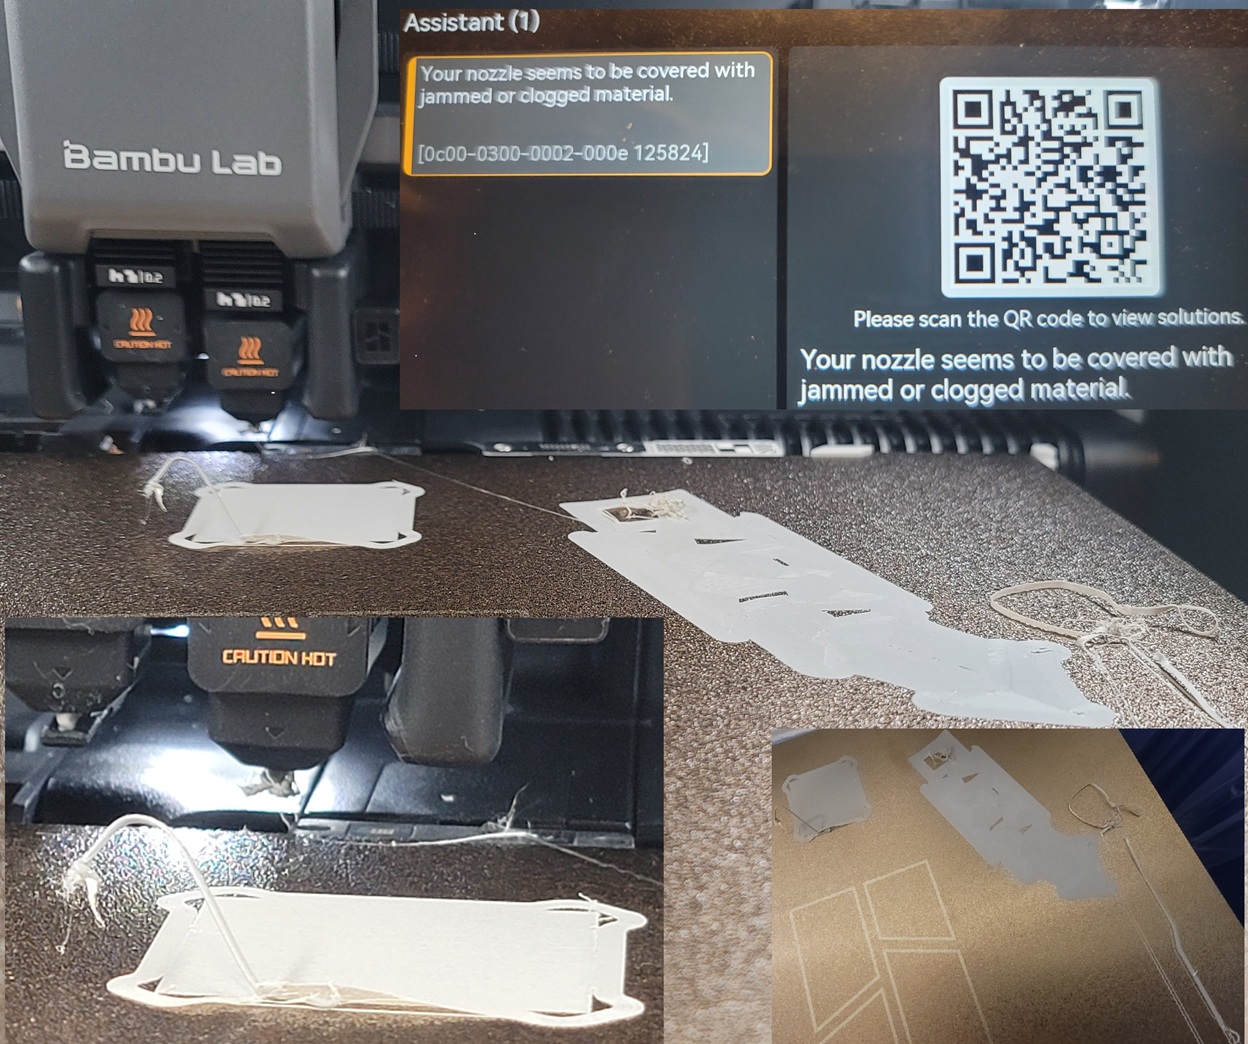
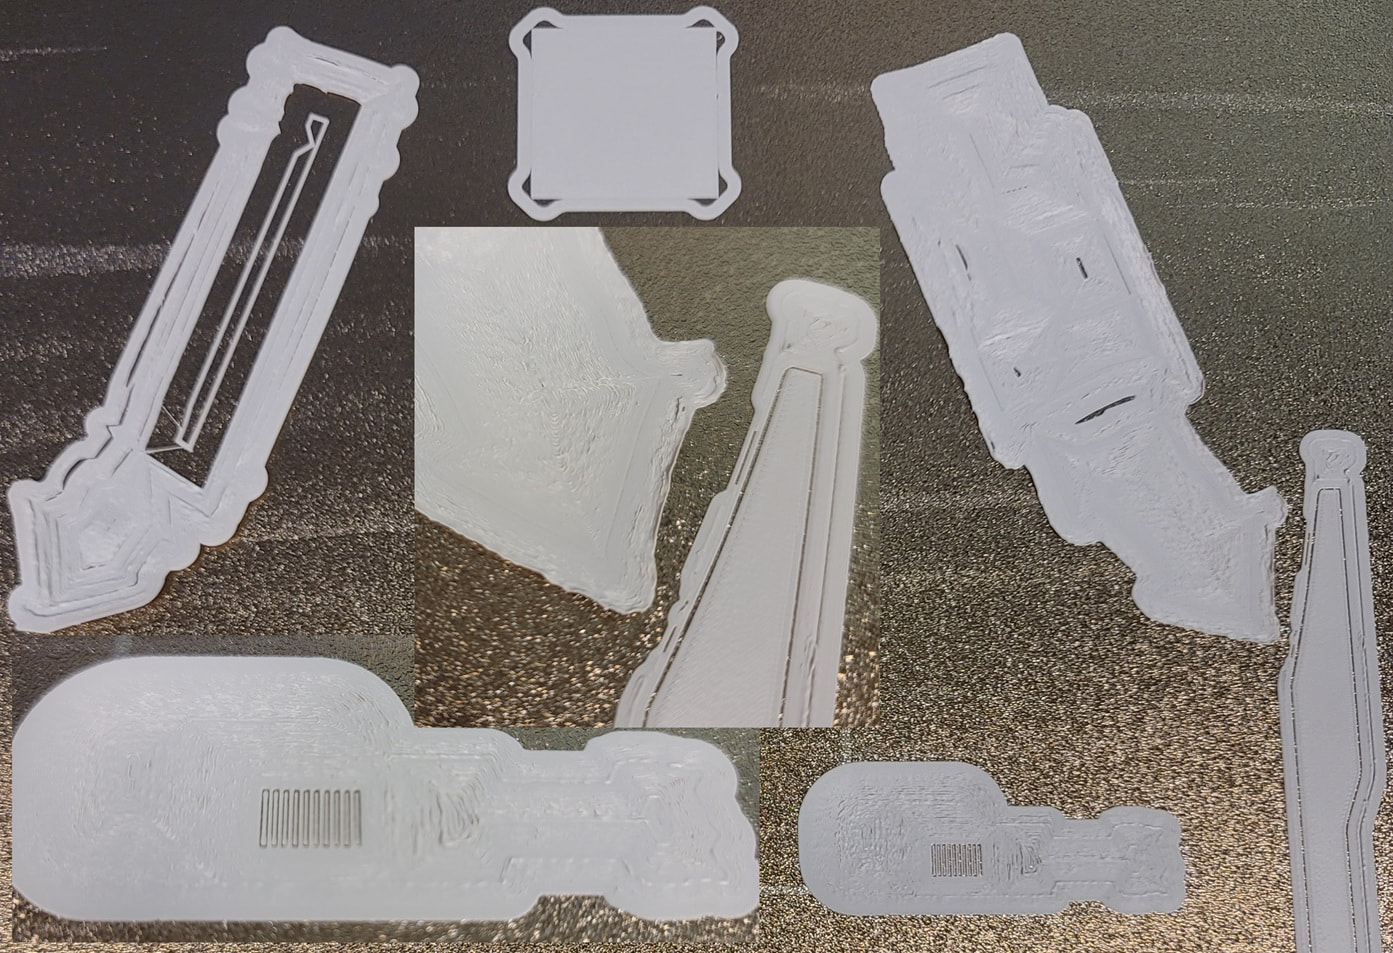
Were those pictures before or after the filament drying, and what was the first layer height?
Yeah, there is that. Although I’d expect it to be possible to easily throttle down to a workable airflow. A little fan (like that 3004 fan from MakerSupply) may already be sufficient. Heat creep does tend to become a problem with 0.2mm nozzle only after well over an hour so not much extra cooling is needed.
I’d be a bit more converned about adding another pair of couplers to an already long PTFE filament feed. Depending on the model used, it can be easier than going through an FTS, but well, there are a few issues we have to deal with with the filament feed.
&
Unless you changed first layer temps, these pics looks like plate adhesion issues and a misidentification of the error.
Do definitely check filament moisture, clean the plate thoroughly (a clean stiff brush like those for fingernails work a treat) to get the grime out of the valleys and check 1st layer temps and height as @CarbonForge recommends.
To be safe, you can up 1st layer temps (only) for the bed (5°C) and nozzle (5-10°C). But this will not compensate for filament moisture and reduced plate adhesion due to residue trapped in the plate valleys.
&
The ‘…Failure 2a’ pics are 0.1mm first layer. The ‘…Failure 3a’ pics are 0.2mm.
The Support for PLA filament I got was delivered this past July. When was the time you got yours?
I imagined that the Y-splitter idea might be intended to introduce air, but I don’t see a way for it to escape at the hot end. So, without flow of escaping air I don’t expect it would work well. BTW, I am running the BL fan kit upgrade on the head.
The pics are a montages of 2 different failures, see their file names.
Oof, I had to check my shopping history : 27 June 2023
Well, there are two observations which make me inclined to assume it’ll be enough.
- Passing along the filament path, extra cooling arrives at the extruder. So pretty close to the cold end of the got end.
- From reports I have seen on the forum and my own H2C (i.e. upgraded fan pre-installed) heat creep issues, it is not an issue for prints below an hour. So heat creep develops slowly, requiring just a little extra cooling.
There’s a caveat though: Opening the door or using temp dumping approaches (nozzle cooling pauses, nozzle swaps (multi-color)) can help in a pinch.
I am using the forum app. So filenames are not immediately apparent.
The first montage clearly shows areas of filament pulled off the textured PEI and residue on the nozzle.
The second montage has quite large areas with bad bed adhesion.
=> Best to 1st thoroughly clean the plate.
=> The 12h drying you did is usually enough but if the roll was new, it may actually require a bit more. AMS relative air humidity is unfortunately not a good indicator for filament moisture.
=> Another item we may need to consider is constrained feed (PTFE paths: I once painfully traced an extruder overload error back to a badly installed PTFE in the AMS. Also with a .2mm nozzle) and flow (residual material along the walls of the lower heat break of the hot end => cold pulls).
&