I have lurked around and tried to read some posts to see if what I am experiencing has been addressed. I have not found anything.
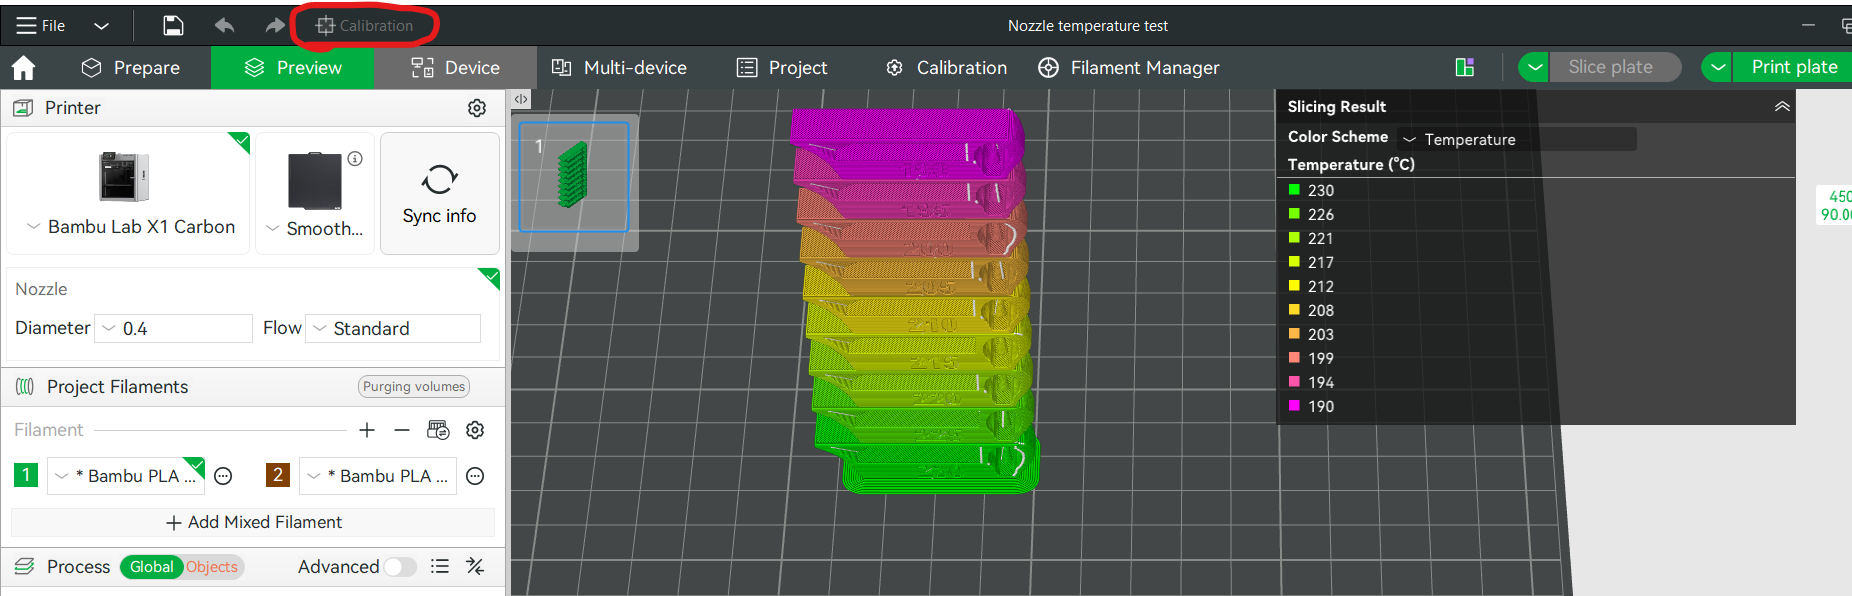
Let me present my issue. I am having issues with some filaments and I am trying to print a temp tower to dial in a little tighter tolerance. I just want that little bit more. I went to maker world, because the calibration menu on my PS1 and Bambu Studio does not have temp tower option, I found a file, downloaded it and printed it. It printed in one temperature.
I researches, learned how to change temp at layer hieght, set all my manila codes at the needed layers, resliced and checked the temperature map. All the same temperature. More research. Tried fake printer slicing, tried m104, m019, plain .STL and other formats, same result. More research. Looked for software overrides that would prevent the slicer from allowing the manual code entries. No joy.
I even went down the Orca Slicer trail, mostly knowing it won’t talk without a lot of questionable tactics that I don’t want to argue about at this point. Again, no joy.
I am quite near the point where I offer a burnt sacrifice to the printer demons in the flavor of a p1s, but really, the printer is fine. It seems more to be software related.
Any constructive thoughts or other rabbit trails to head down would be appreciated, if you please.
Thank you for your valuable consideration.
 &
