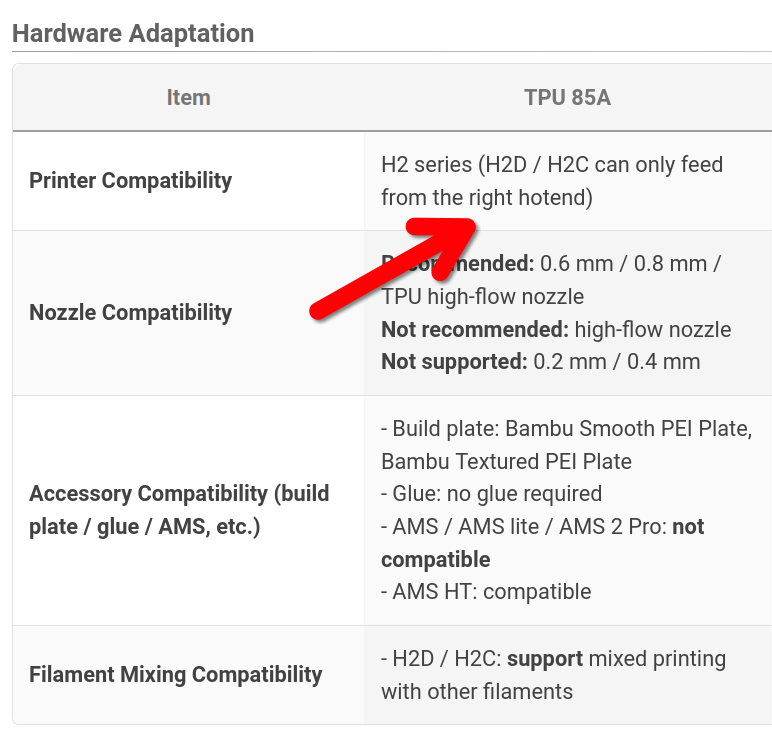
We had an Engineer who successfully printed TPU85A (non-Bambu) using the standard 0.4 nozzle. He would get a ton of stringing - but he still managed to get this to print. External Spool fished through Bowden tubes. It had no issues. This person left and I took over.
When I was tasked with running this same part again - I started getting warnings about TPU (any TPU but specifically 85A). This was new to me - but I ignored the warnings and plowed ahead since previous Eng got this print with no issue.
The print head clogged and the print failed - but it went on for a bit before failure. Keep in mind this was normal 0.4 nozzle - external spoil fed thru tube.
So I did my research and found the TPU High Flow nozzle on Bambu’s website. So we purchased this thinking it was a SLAM dunk.
So finally completed the install this morning. Open existing file and change the parameters - Nozzle 2 - TPU High Flow 0.6 and write the ,gcode file.
Had issues with feeding the TPU85 but it finally grabbed and fed through TPU HF 0.6 nozzle.
Go to print and it stops - hardly lays down two lines and gives me an error - high resistance in material feed.
So I took off some resistance to the inlet side and restarted - two lines - high resistance.
So I read you need to feed TPU85A direct into the top of the head to reduce resistance. So I unfed the material - pulled it out of the Tube and took off top cover and inserted material directly into Head 2. Pulled some slack off of spool to reduce resistance - two lines and failure - high resistance.
So I tried again - this time actually holding the material as it printed - absolutely NO resistance - two lines and failure - high resistance.
I get all the warnings - I get the issues with TPU 85A - but come on - We purchased and installed the correct nozzle and I went even with the larger orifice.
My questions to you guys - how the heck did the previous Engineer print using normal 0.4 nozzle!?!?! Why did my initial print using the same config worked until it didn’t - no high resistance errors - but the nozzle did clog? Why the heck is this problematic even with the supposed correct nozzle? I even fed the material direct into head 2.
Please help. What is going on. I guess I have seen people print TPU - of course they did.
I did dry the material before putting it on the external spool.
I selected the Bambu 85A within Bambu SW and even changed the External Spool to TPU85A. Is this an issue with temps on the nozzle? If yes how do I change these settings - is this done with Bambu SW?
You need to remember that the .6 nozzle requires double the cross sectional area of a .4 and so the extruder is pulling much harder on the filament spool.
got a photo of your setup? that might help people troubleshoot
Honestly havent tried 85 yet (so feel free to take my advice with a grain of salt) but it sounds you are running the tpu through a ptfe feed tube?
If i were to try 85 or lower hardness I would try direct feeding from above, with no or minimal ptfe tube . There should be quite a few setups on makerworld
I dont have an H2 nor any fancy TPU nozzles so this may be not great advice, but:: You didnt mention any slicer settings
I would reduce Max Volumetric Flow, by at least half of whatever your current setting is, as a test
MVF is a speed limit on the extruder, and if your extruder is pushing too hard and senses a buckle, it warns. A simple solution might be just to not make it go so fast so the physical reality of whats happening in the nozzle gets time to melt
Also, TPU is notorious for needing thorough dry, and extra ooze might be misconstrued by the servo extruder/sensors as a bad resistance, can’t hurt to dry it.
So if you read my post - I did a direct feed. Others are asking for my setup. It’s not what is recommended. I did find a setup and 3D printed parts to support the Spool directly above the system - this is not what I’m doing.
I used TPU 85A succesfully on my X1C. Some strings on the seam, but good prints nonetheless.
Key were:
Thoroughly dried
Top mounted spool holder feeding straight into the tool head
Never allow the feed to tighten! Always ensure that there’s a gently curve.
For my H2C, I just installed the TPU Feed Assist module as I have read good things about it. Or, more precisely: I’d have expected many, many more negative posts if it wasn’t doing what it is supposed to
Haven’t tried it yet myself though.
PSS: Addendum: 0.4mm Standard Nozzle
PSSS: (Hopefully final) addendum:
Allowing no tension on the filament whatsoever (like your hand held trial) and slowly.
Having double checked my profile, I slowed down to 120mm/s (default is 200mm/s) but just using silent mode may be easier. I also set the “scarf around entire wall” to try to reduce seam strings and use the Arachne “wall generator”.
I am able to print 85A TPU through a standard 0.4mm nozzle with the help of TPU feed assist module. You have to trick the printer, select the filament as 90A on printer and then 85A in slicer.
I think since the original engineer did this successfully then the slicing has to be good and it has to be a setup issue (unless they left with bad feelings and sabotaged the job…)
Are you using a full roll of TPU?
Sometimes I cut off what I need and wind onto a spare real. Logic is doubled. 1) Less weight on the real = less resistance to pull. 2) Drying time is significantly reduced.
I’m using the H2D and I have printed BBL 85A TPU with several methods, all have worked flawless.
First, standard way - feeding the filament thru the backside TPU entry, 0.4 mm Standard nozzle.
Second, feeding TPU from above directly to the print head - no visual difference but annoying noise level due to missing top lid. 0.4 Standard nozzle
Third, using the BBL TPU nozzles (TPU high flow kit), 0.4 and 0.6, feeding TPU thru backside TPU entry. Got the impression that the print with the 0.6 mm nozzle had have some ‘starved’ spots but might be possible that the TPU wasn’t really dry.
Forth and last, using BBL TPU nozzles, 0.4 and 0.6, the external TPU feed assist and AMS HT (using the TPU outlet) and PTFE tubes from start to end (using an Y-adapter inside the printer to combine standard/buffered entry and TPU entry to avoid changing inner PTFE tubing). Worked perfectly as well, best speed and consistent print quality.
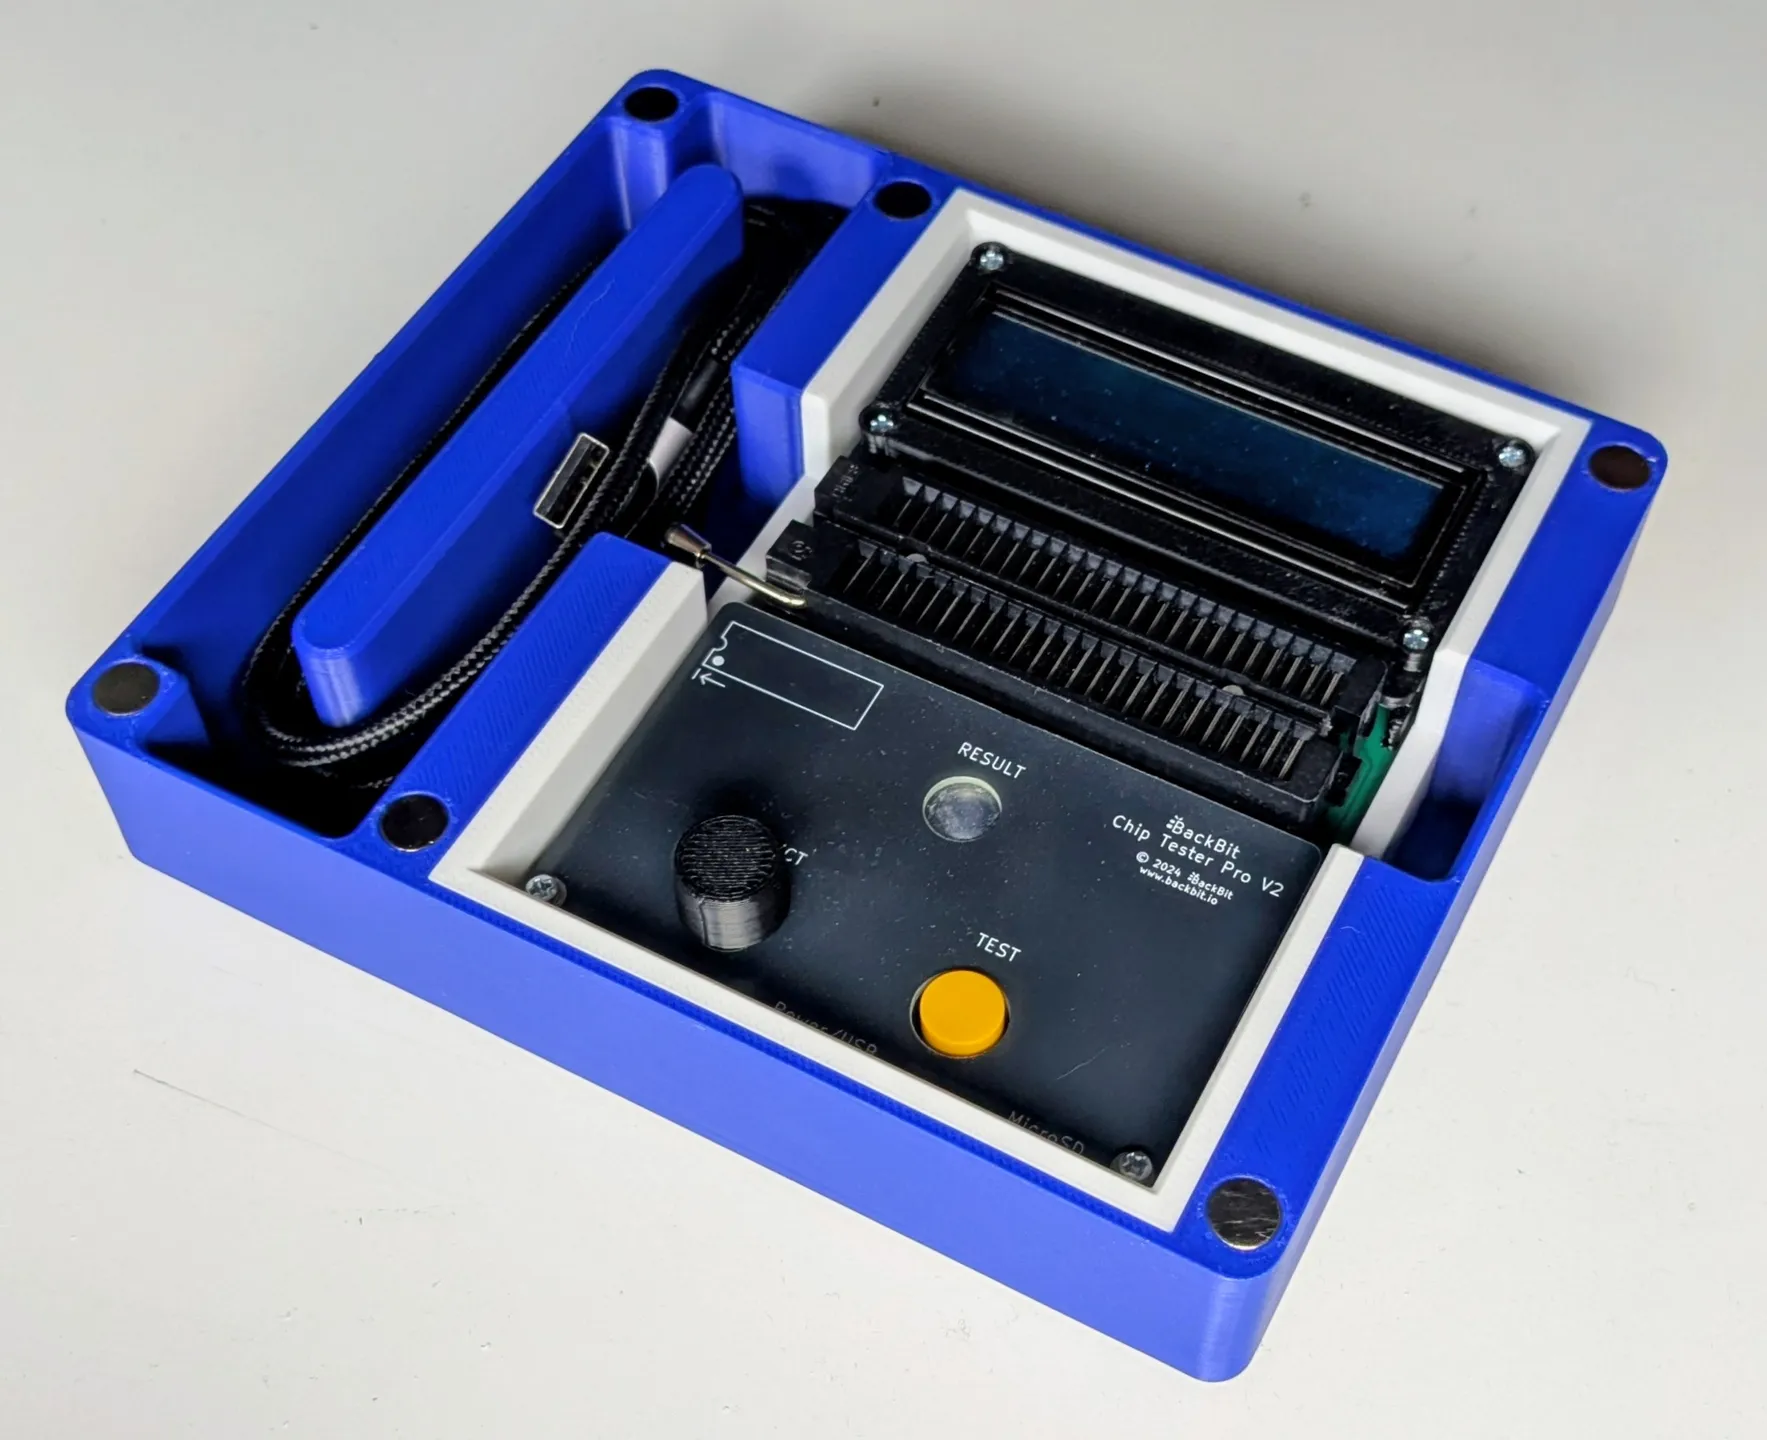
I did a combined print with PETG on left nozzle and TPU 85A on right nozzle as well, printed the TPU part (white) directly into the PETG part (blue) (initial left and right mixup corrected, as mentioned by @cyberang3l , thanks for the info!)
So you changed nothing in the Speeds section for the final gcode? Just selected generic TPU85A and went to town?
Other Nets info stated that some people bumped the hot-end temps to 250C and that solved flow issues. I also found recommendations to slow down the print significantly - 20-30 mm/s.
I guess - the file he was using got corrupted so I couldn’t interagate his settings. I found some info on settings but I don’t now where to make these changes. Any recommendations? Even Bambu’s page on TPU85A doesn’t even discuss temps or speeds - just to hang the spool above the system - direct feed the material and that’s it.

 &