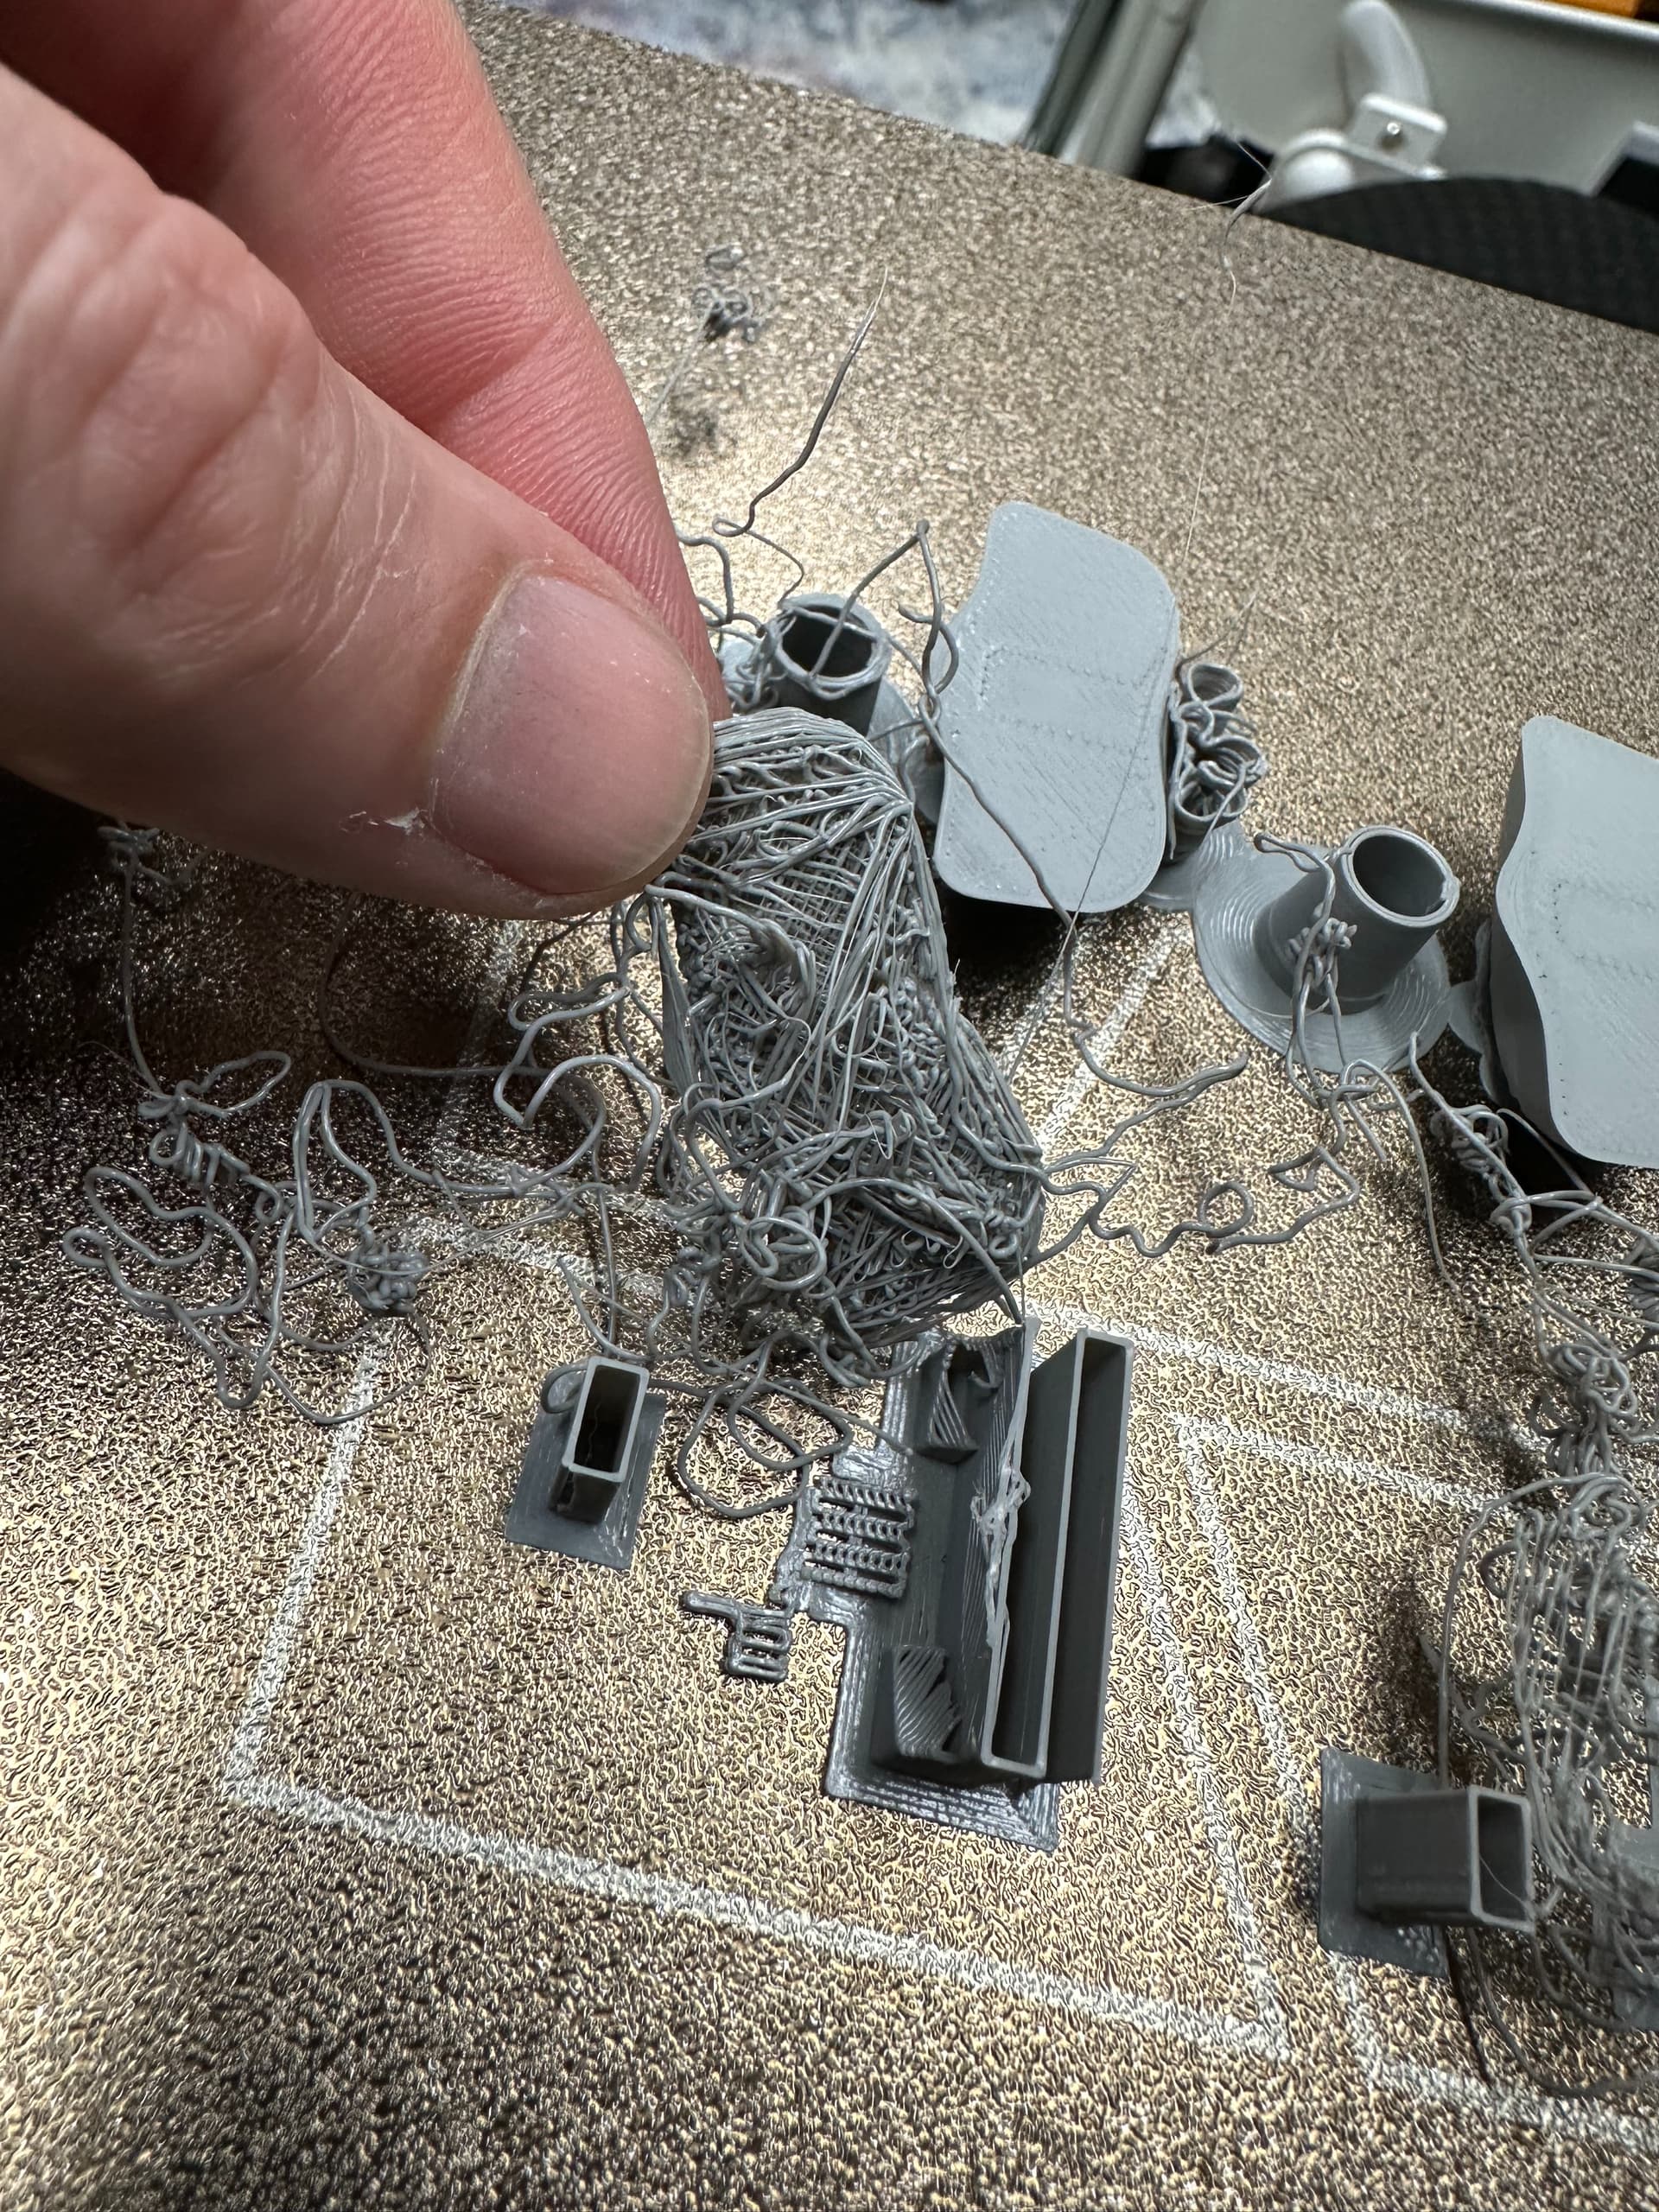
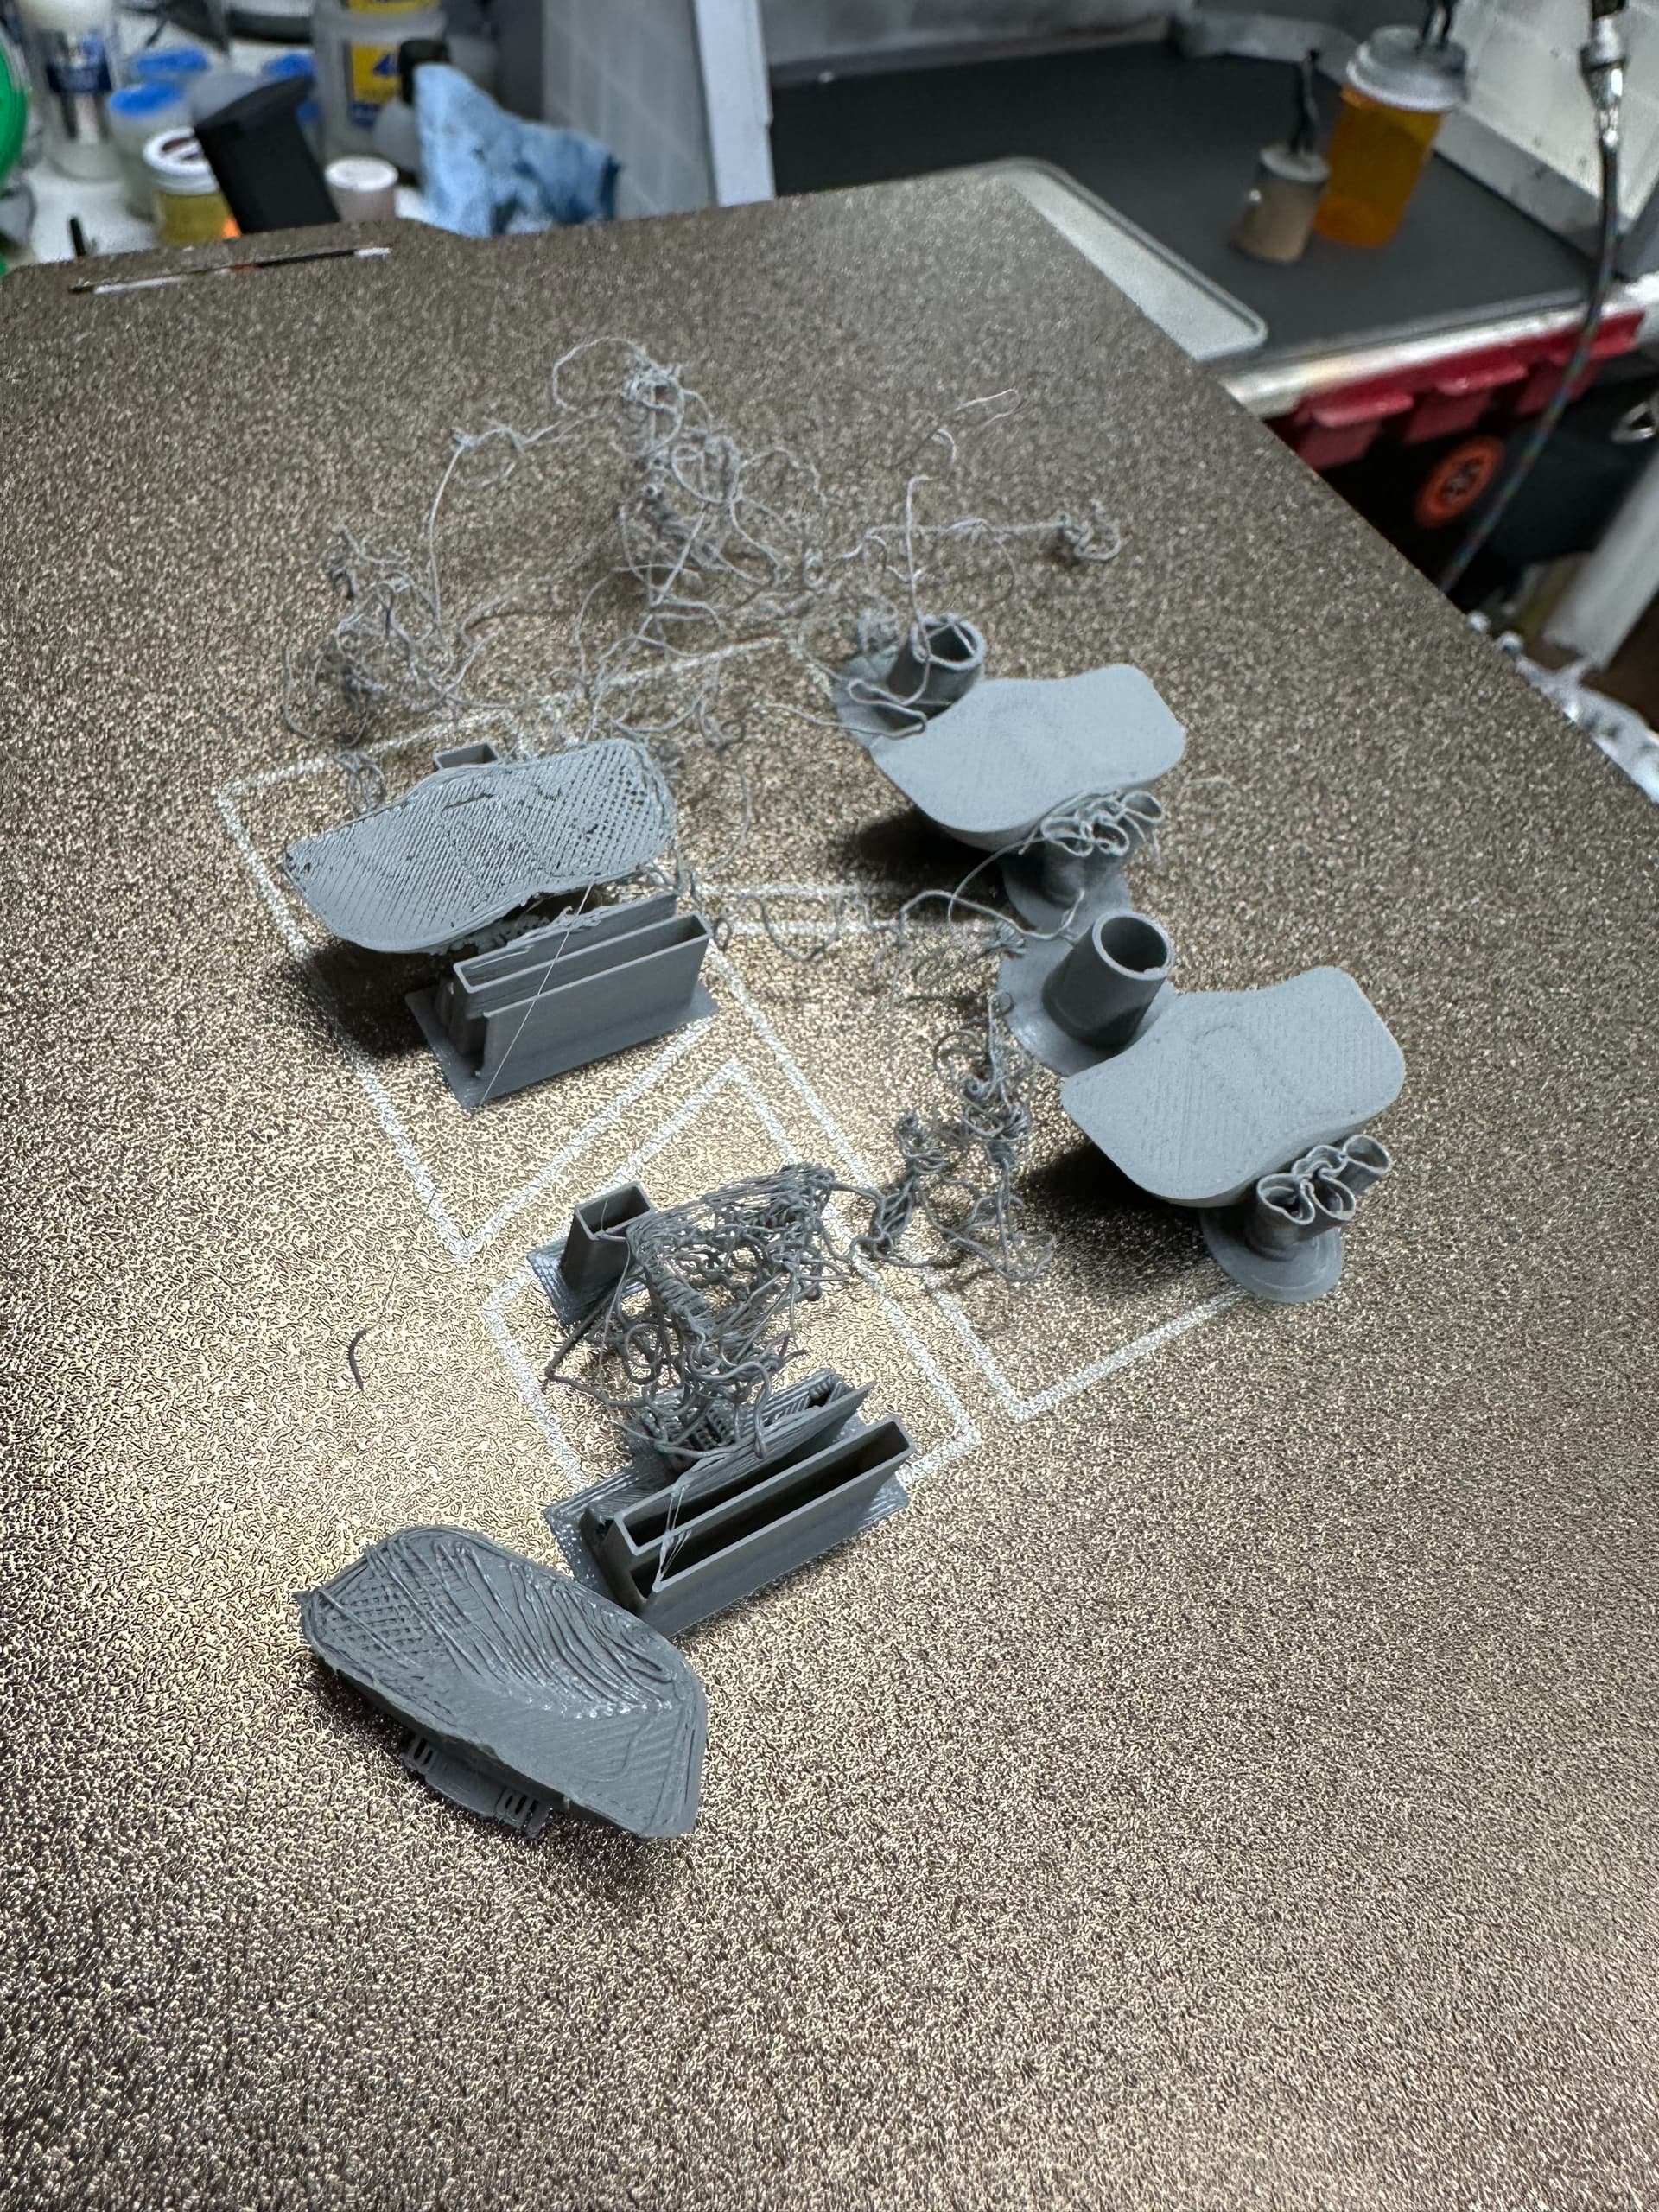
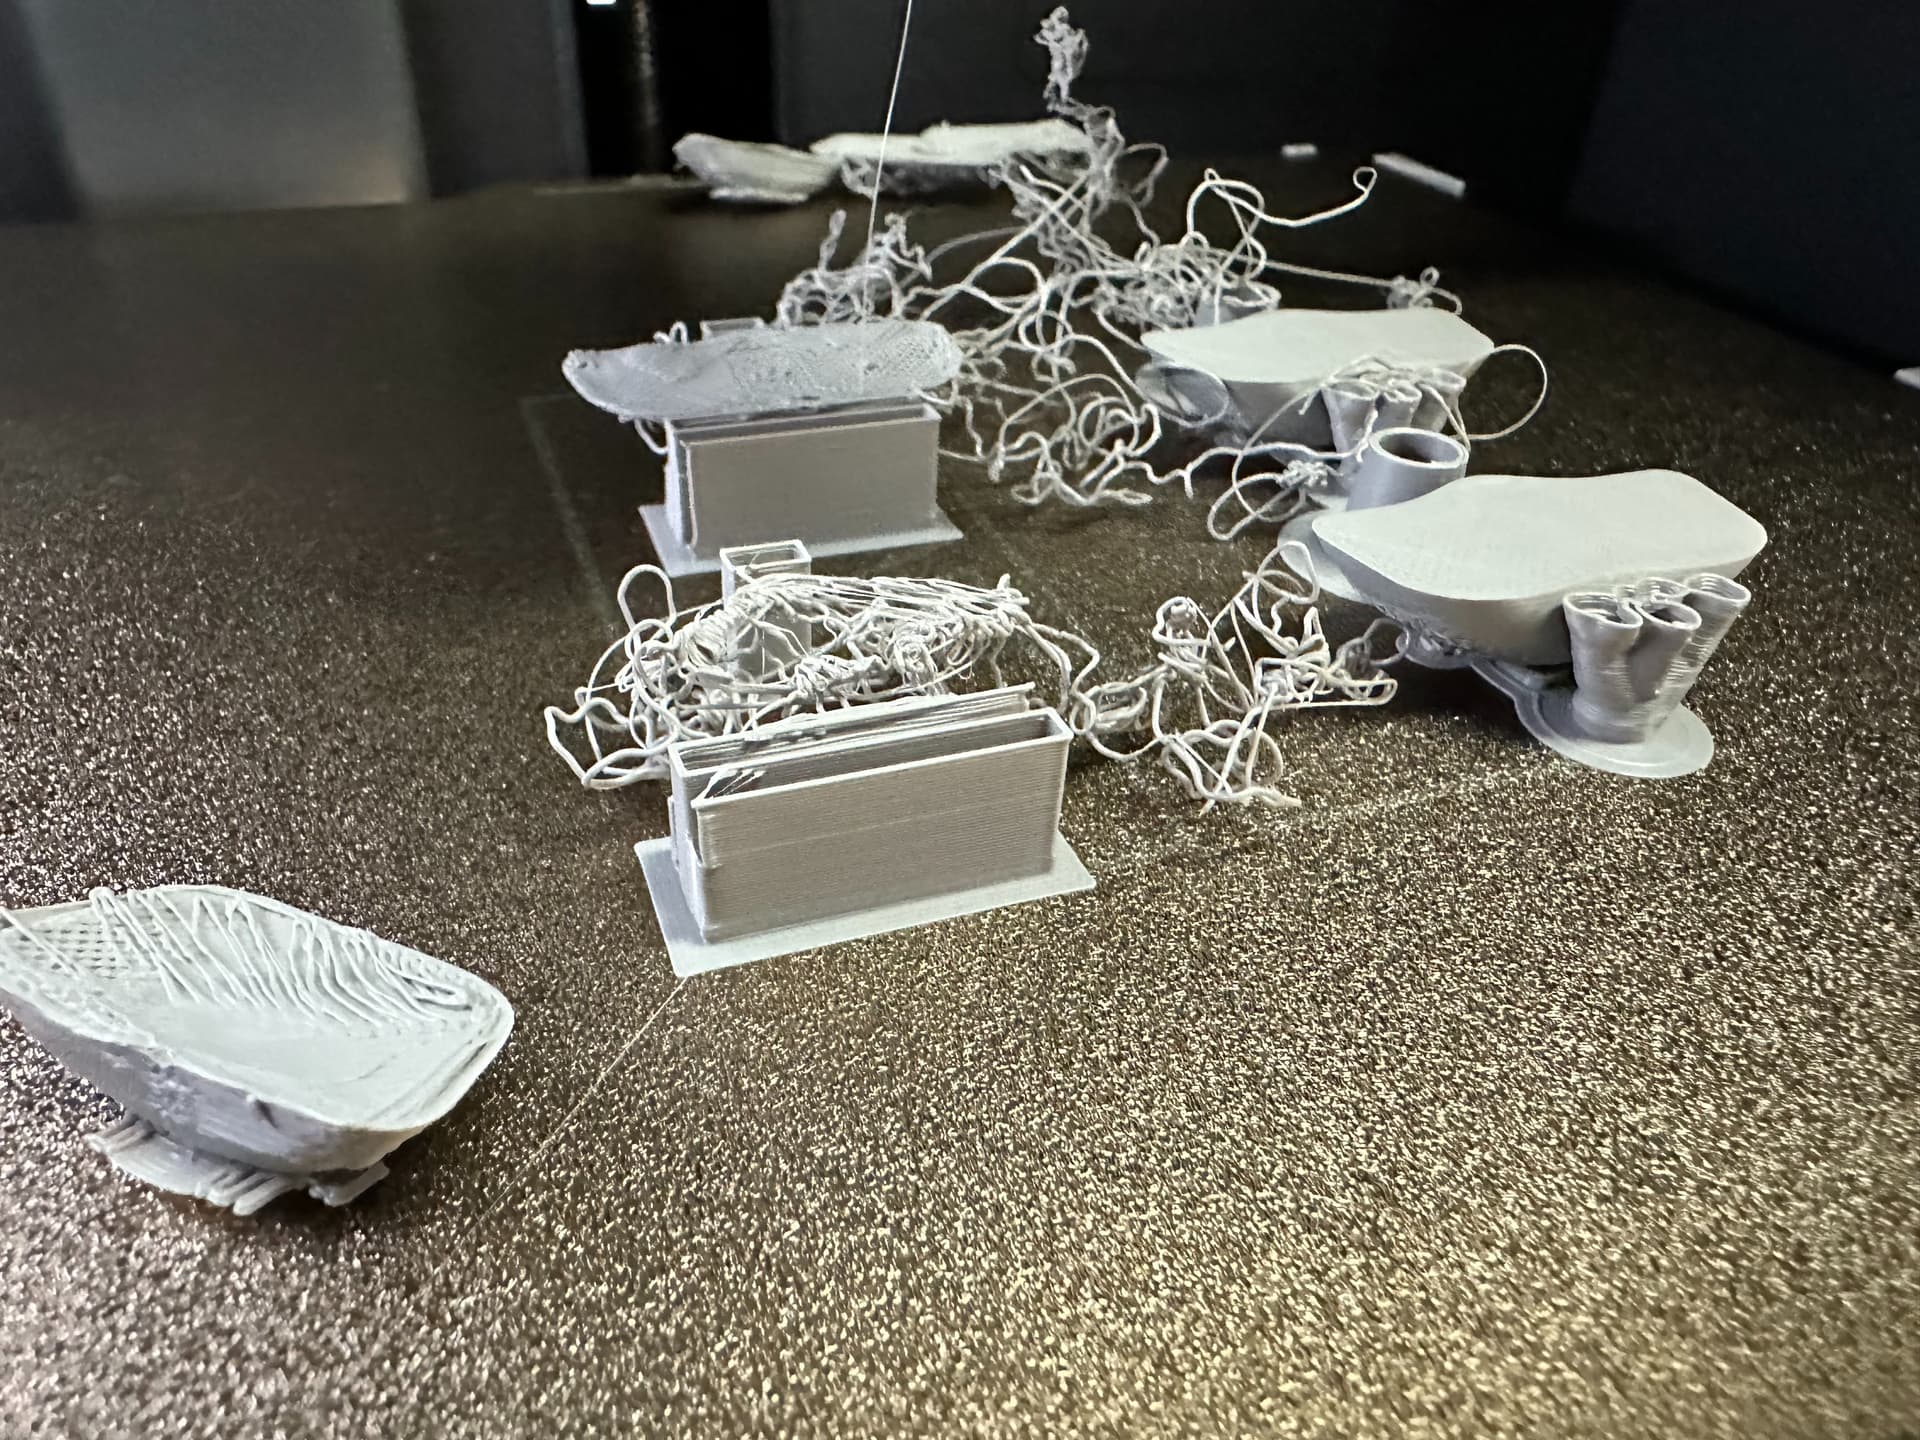
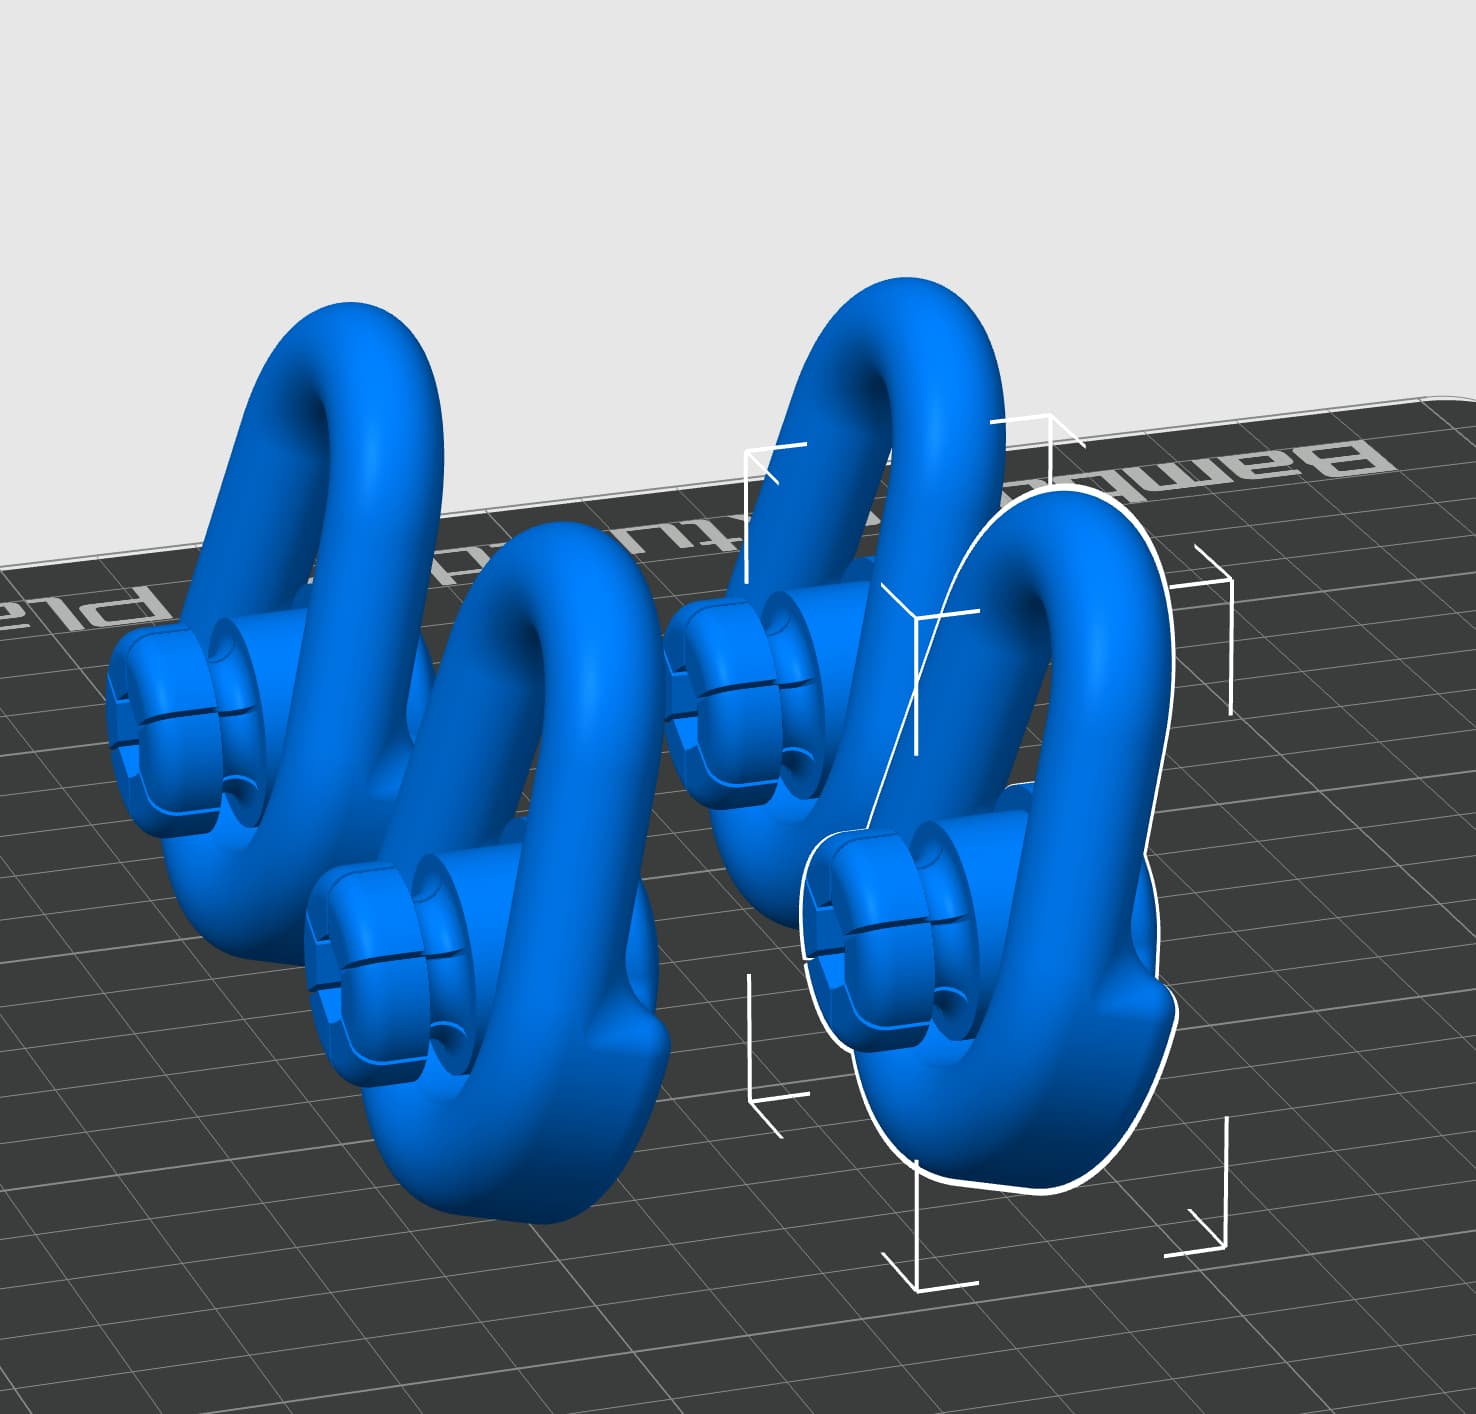
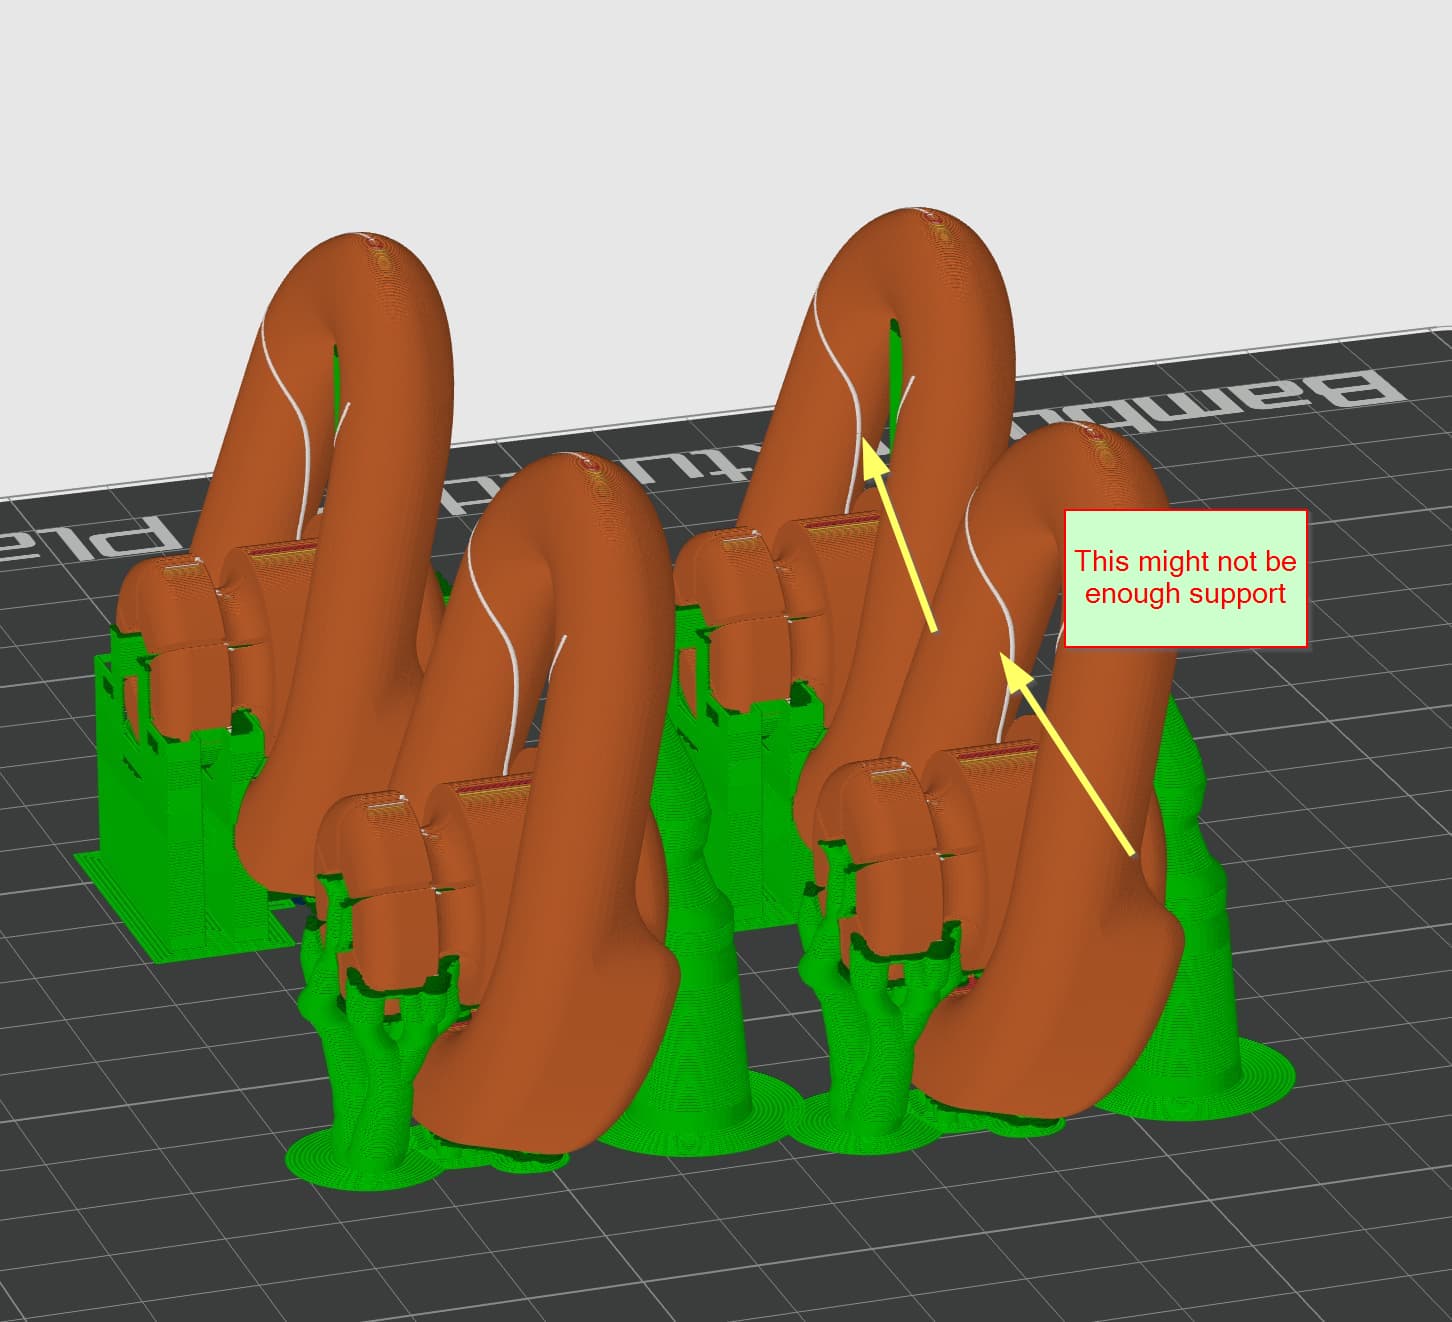
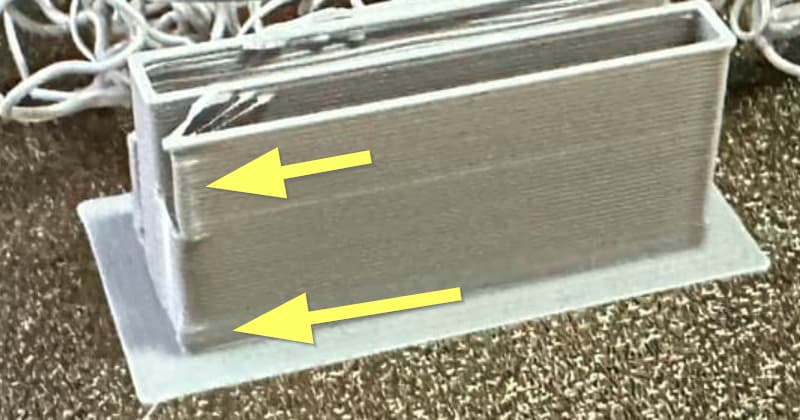
I see a number of issues.
Layer support
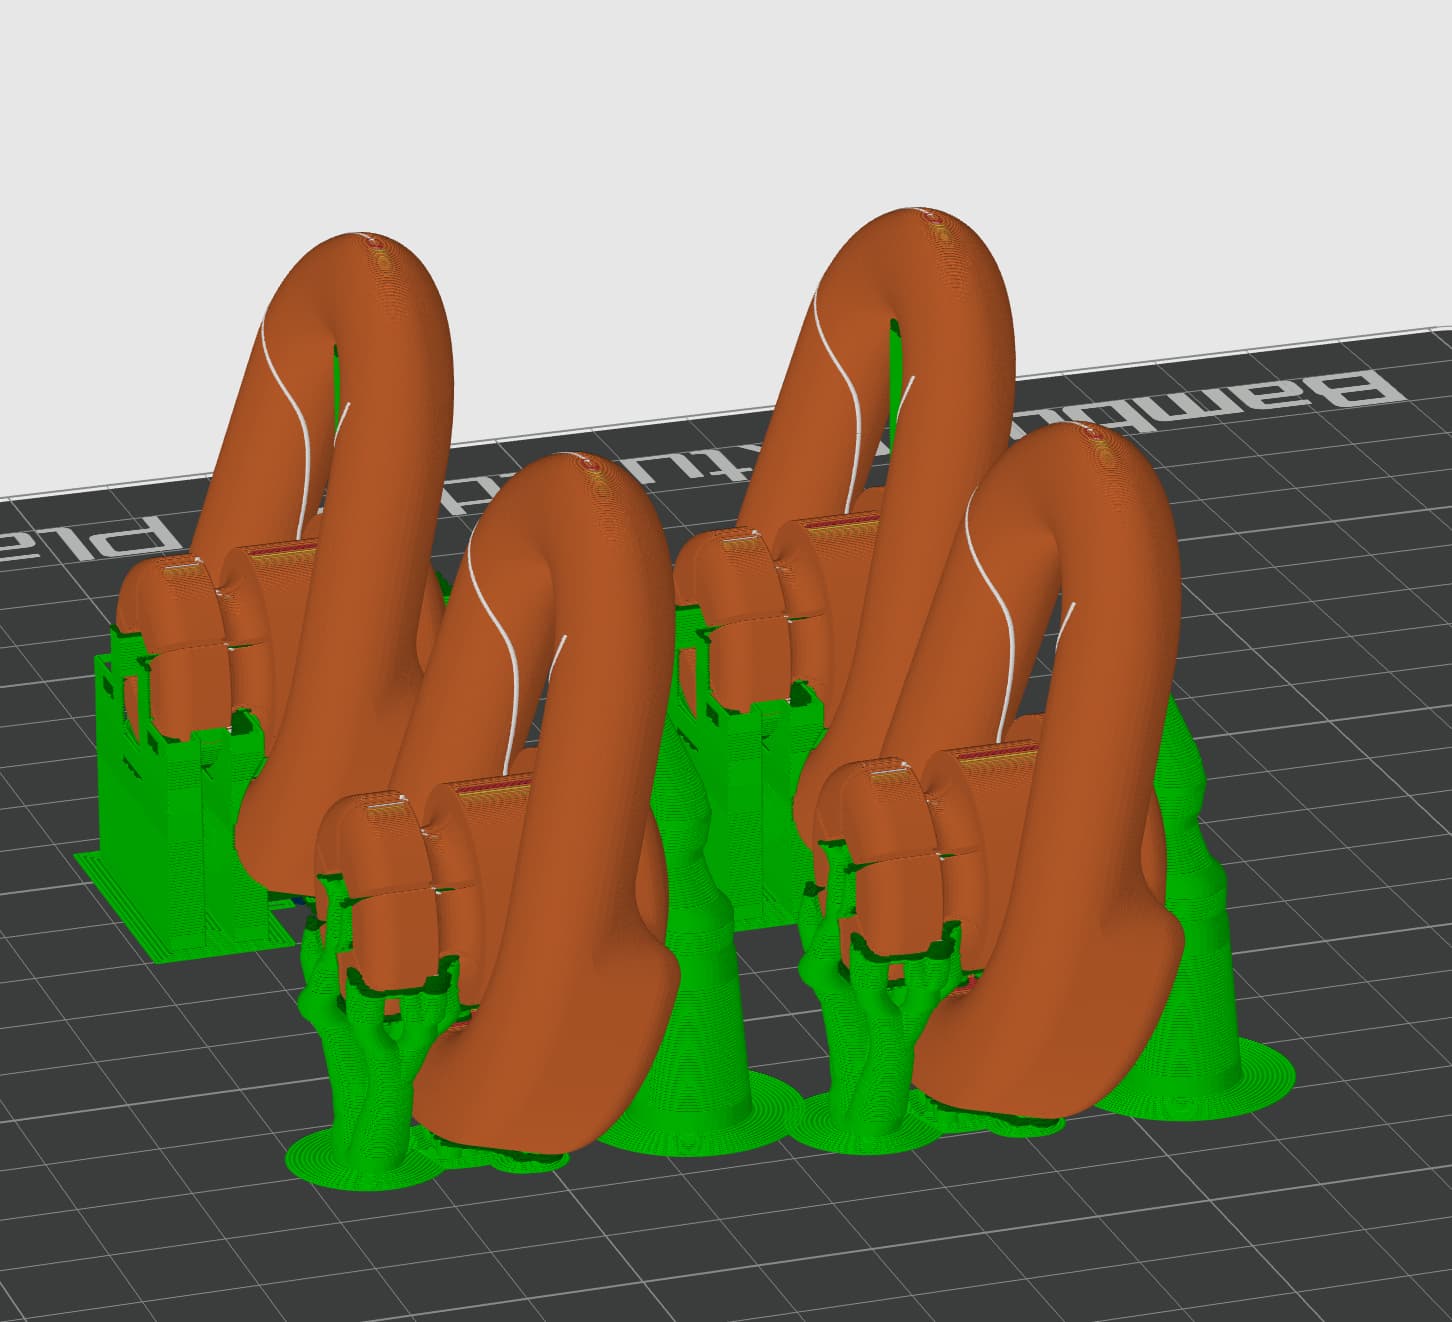
@philch is correct. You’re supports are insufficient to the task. As a result, you’re going to invite layer separation.
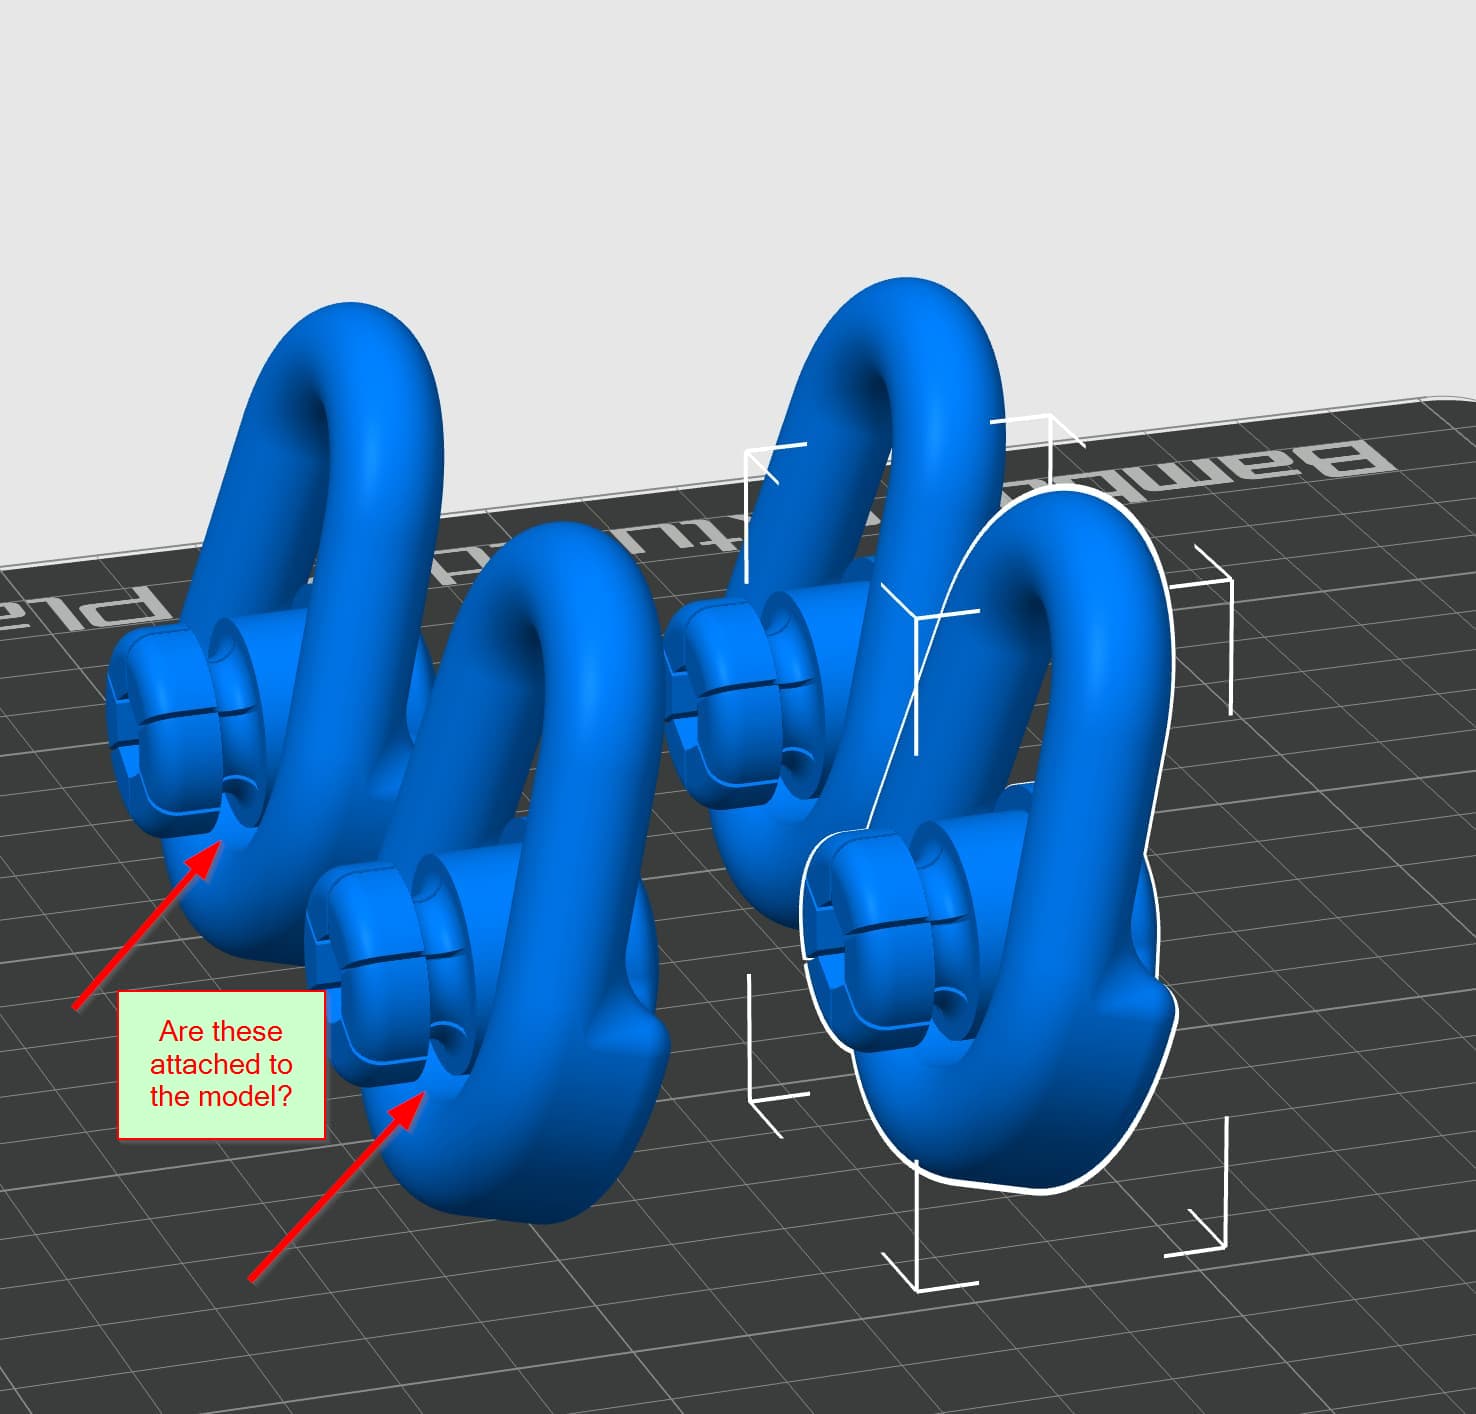
Can you provide another screengrab showing a 30-45 degree offset so that we can see the front of the object indicated by the red arrows. I can’t tell by the model but is that a floating object or is it attached. If it’s attached, it doesn’t look like there is a lot of connective material which would also induce layer separation.
Model orientation
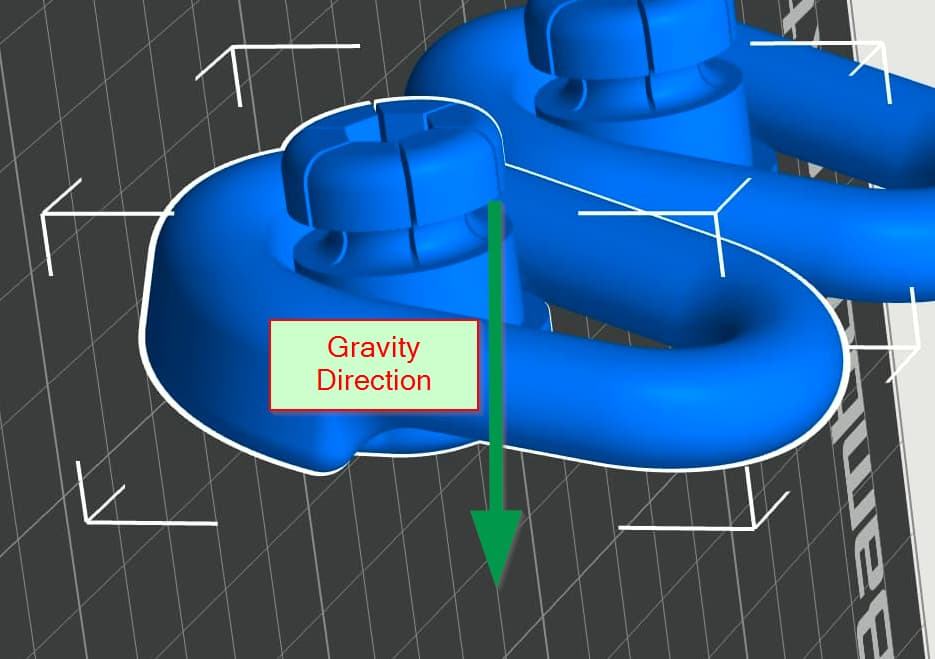
You may want to experiment with orienting your model so that the model lays down in such a way as to minimize height. Then use supports to ensure that you’ve got enough material to hold up the model.
I see that you’re experimenting with both standard and tree supports. This model if laid flat should do well with standard supports. One tip I might add is to increase the support separation from the default of 0.35mm to at least 1.25-1.5mm. This will create a greater gap between the X/Y distance of the supports making them easier to separate. You can use the same parameter for both tree and standard supports.
Filament
If it’s Matte Bambu gray PLA, that stuff is pure garbage. In fact, I’ve long abandoned all Bambu Silk and Matte filaments because they simply do not perform well. In the case of silk, they have even been shown to damage plates. Furthermore, the Matte grey filament, which I keep in my “problem child” cabinet for experiments, just doesn’t bond well even when dried and tuned. I’ve found that PolyMaker Matte filaments perform better put I still leave nothing to chance and manually tune the profiles. Also, different colors have shown to perform differently as I found out with Bambu Matte Black, Red and Gray, all are totally horrible filaments for producing parts. I think their use-case is for artistic models, not functional once.
If it’s standard Bambu PLA, have you tuned your filament? You can’t simply trust the defaults. I’ve wasted many a spool proving that theory. 
I’m seeing a lot of things I don’t like in the supports that indicate that the filament hasn’t been either dried properly(yes, even PLA) and/or not tuned properly. The flow looks wrong. Tuning would prove or disprove this theory.
Suggestion
It seems like you’re aiming to create a functional part. If you’re subjecting these parts to any stress, PLA won’t perform well. May I suggest using PC filament instead? I’ve had great success with it. While it may not produce the most aesthetically pleasing models and may require additional trimming, it machines well and can even be used in place of heated brass inserts for threads. You’ll need to set your plate temperature to 100°C. When printing with PC, it’s important to focus less on infill and more on increasing the number of wall layers. I’ve achieved the equivalent of 100% infill by increasing the wall layers to 100 and allowing the slicer to fill in using just walls. This approach eliminates the random internal surface irregularities that infill often causes, resulting in a smoother part. Additionally, the resulting structure’s strength is impressive—I’ve tested it and it appears to be even stronger than molded ABS. Also, Unlike CF filaments which indeed have uber-strength, PC is non-abrasive which is why you get that smooth almost glass-like surface texture. For best results, you will want to dry it before use, the difference is night and day. I found that out the hard way too. 
The PC filament I’ve found to be excellent is the following. I bit pricey but a lot less than Bambu or for that matter, any other PC filament I have found so far. The next one up is 20% more and Bambu is 40% higher, so all in all, I find it a well performing product. Note: The clear is better than the black.