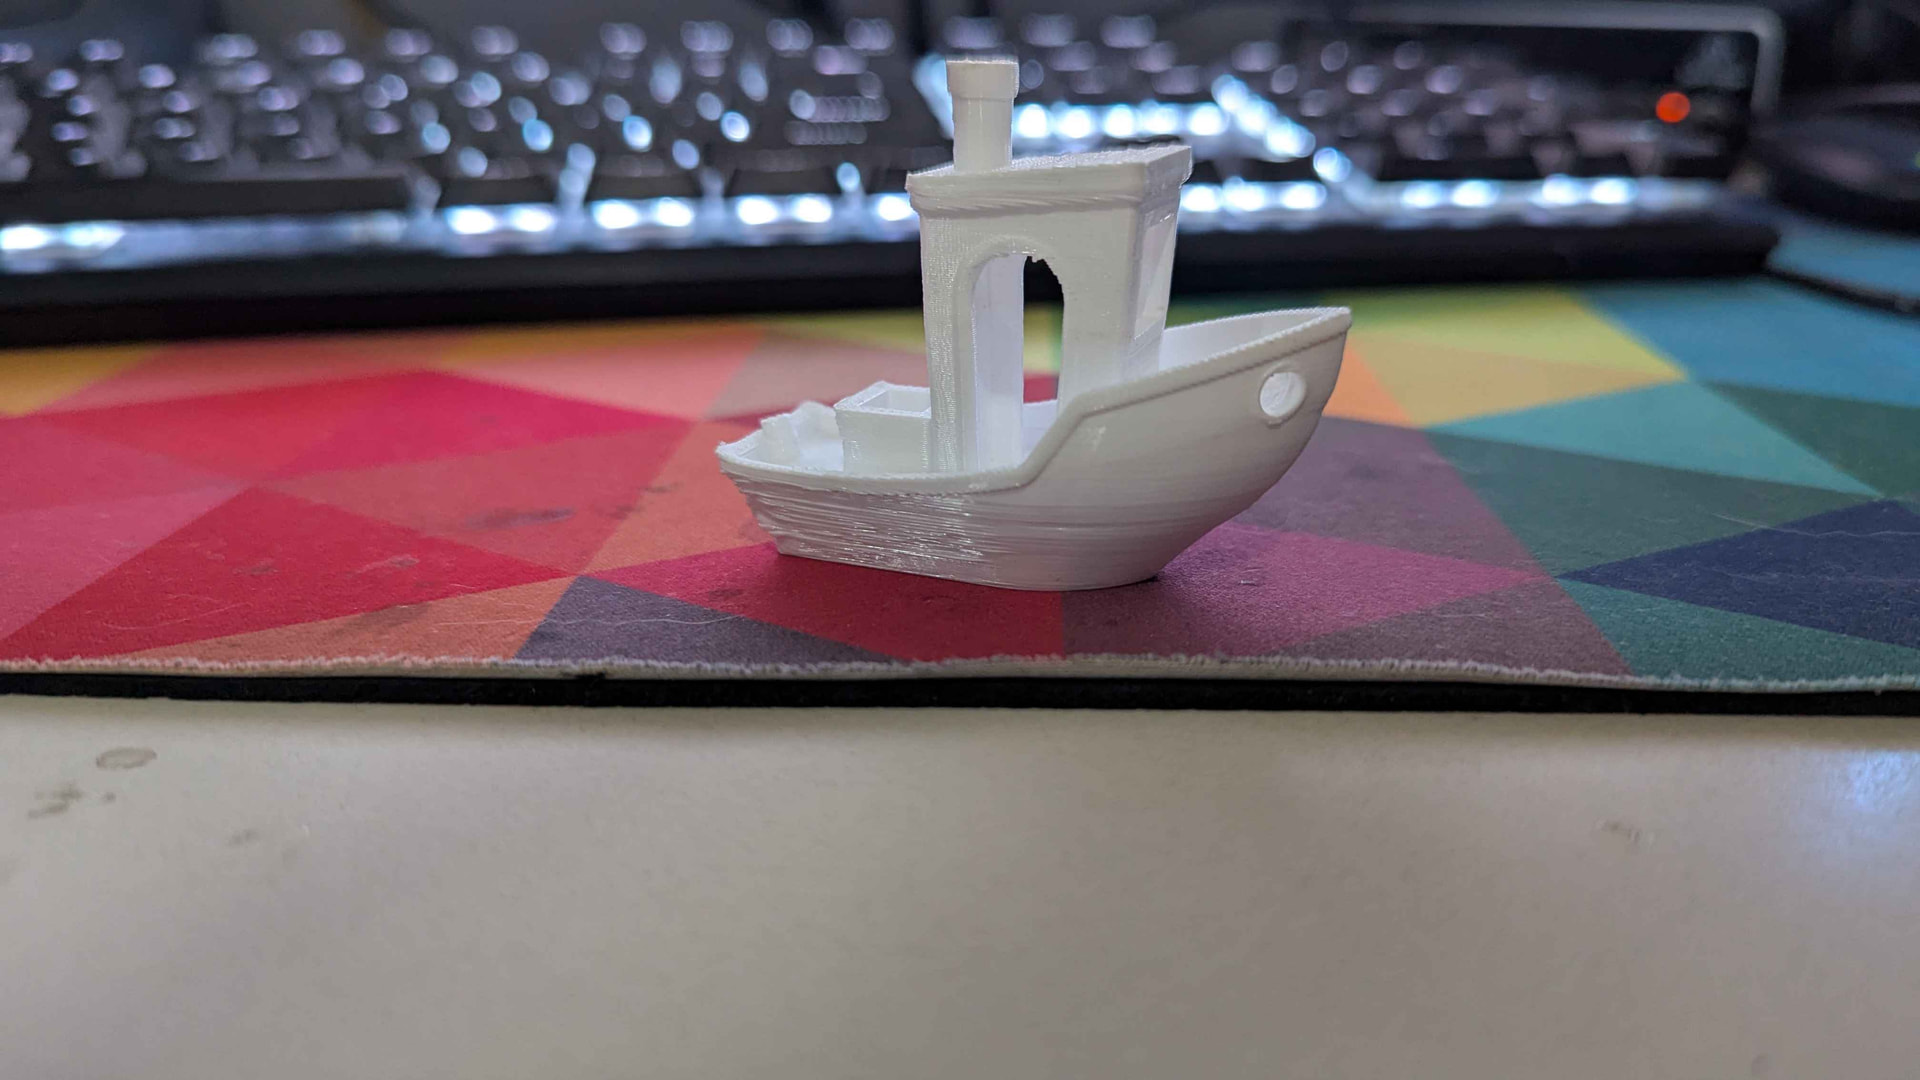
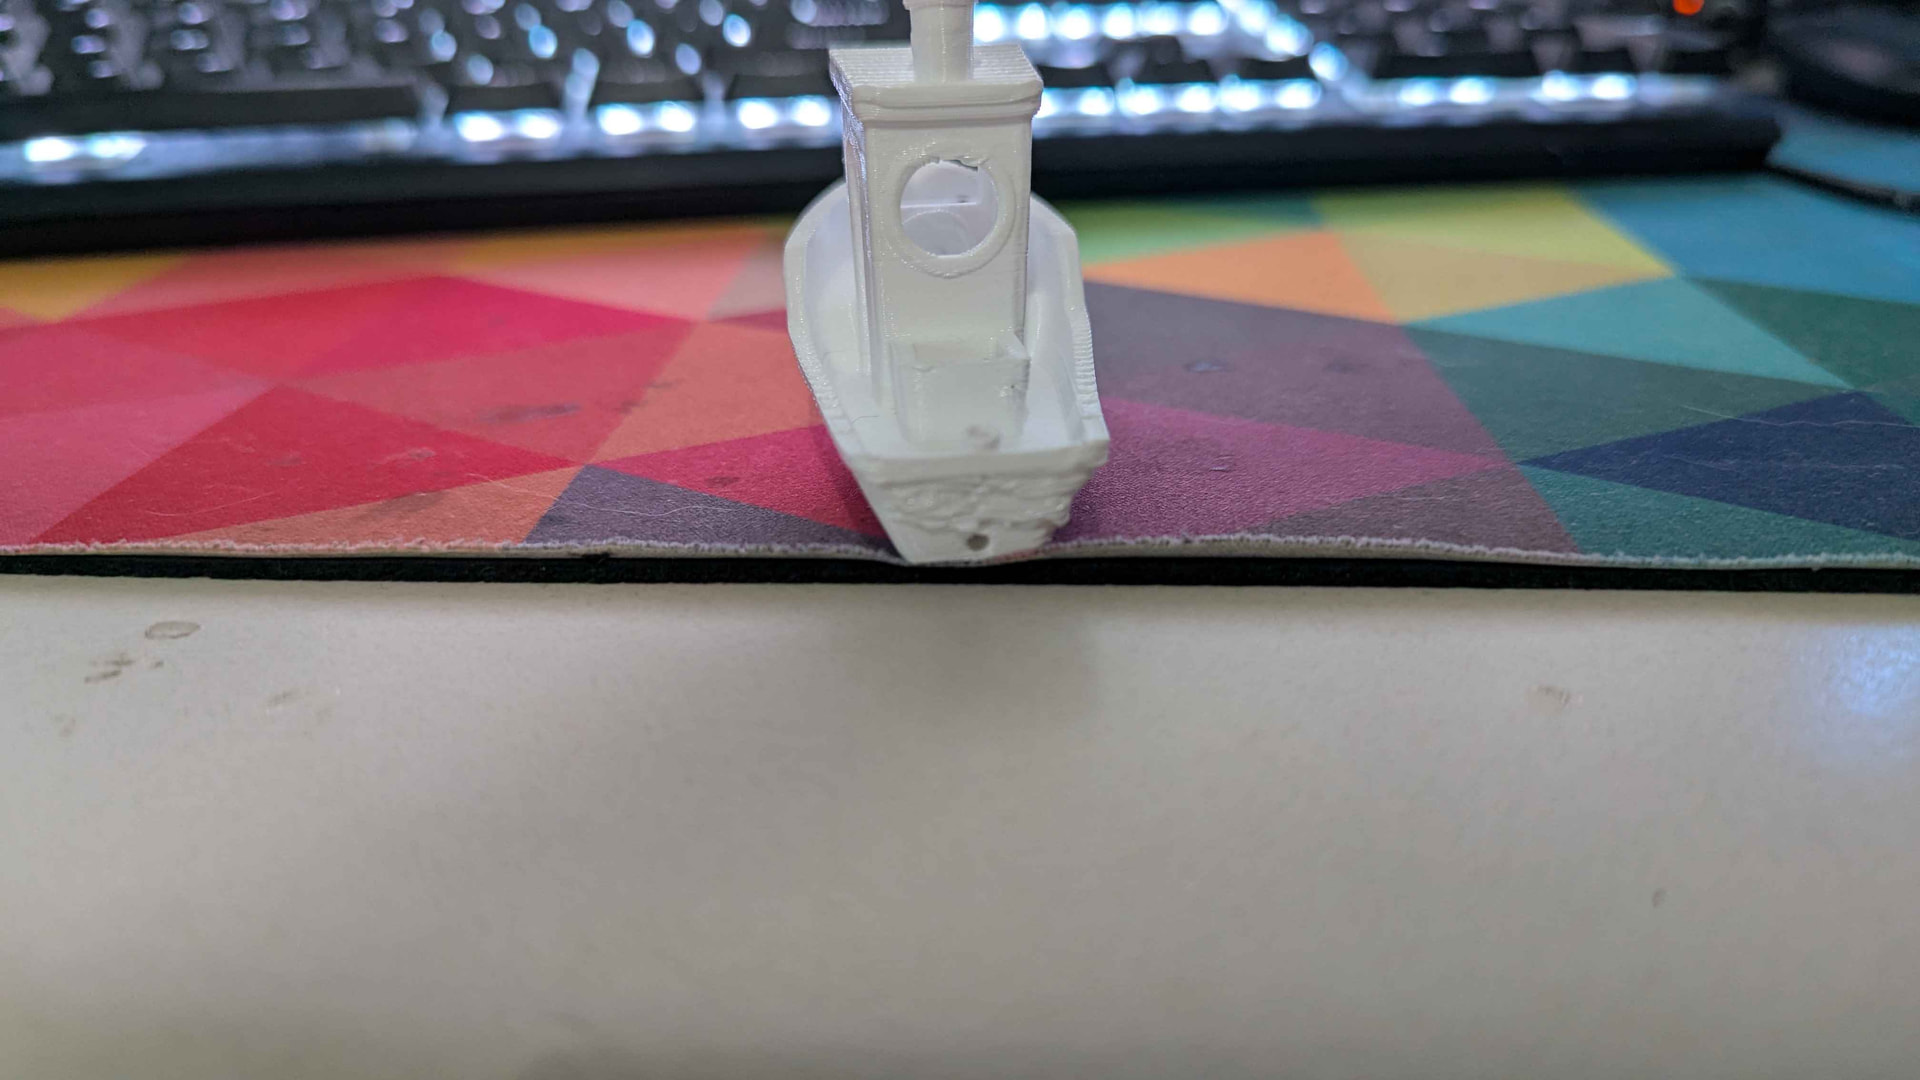
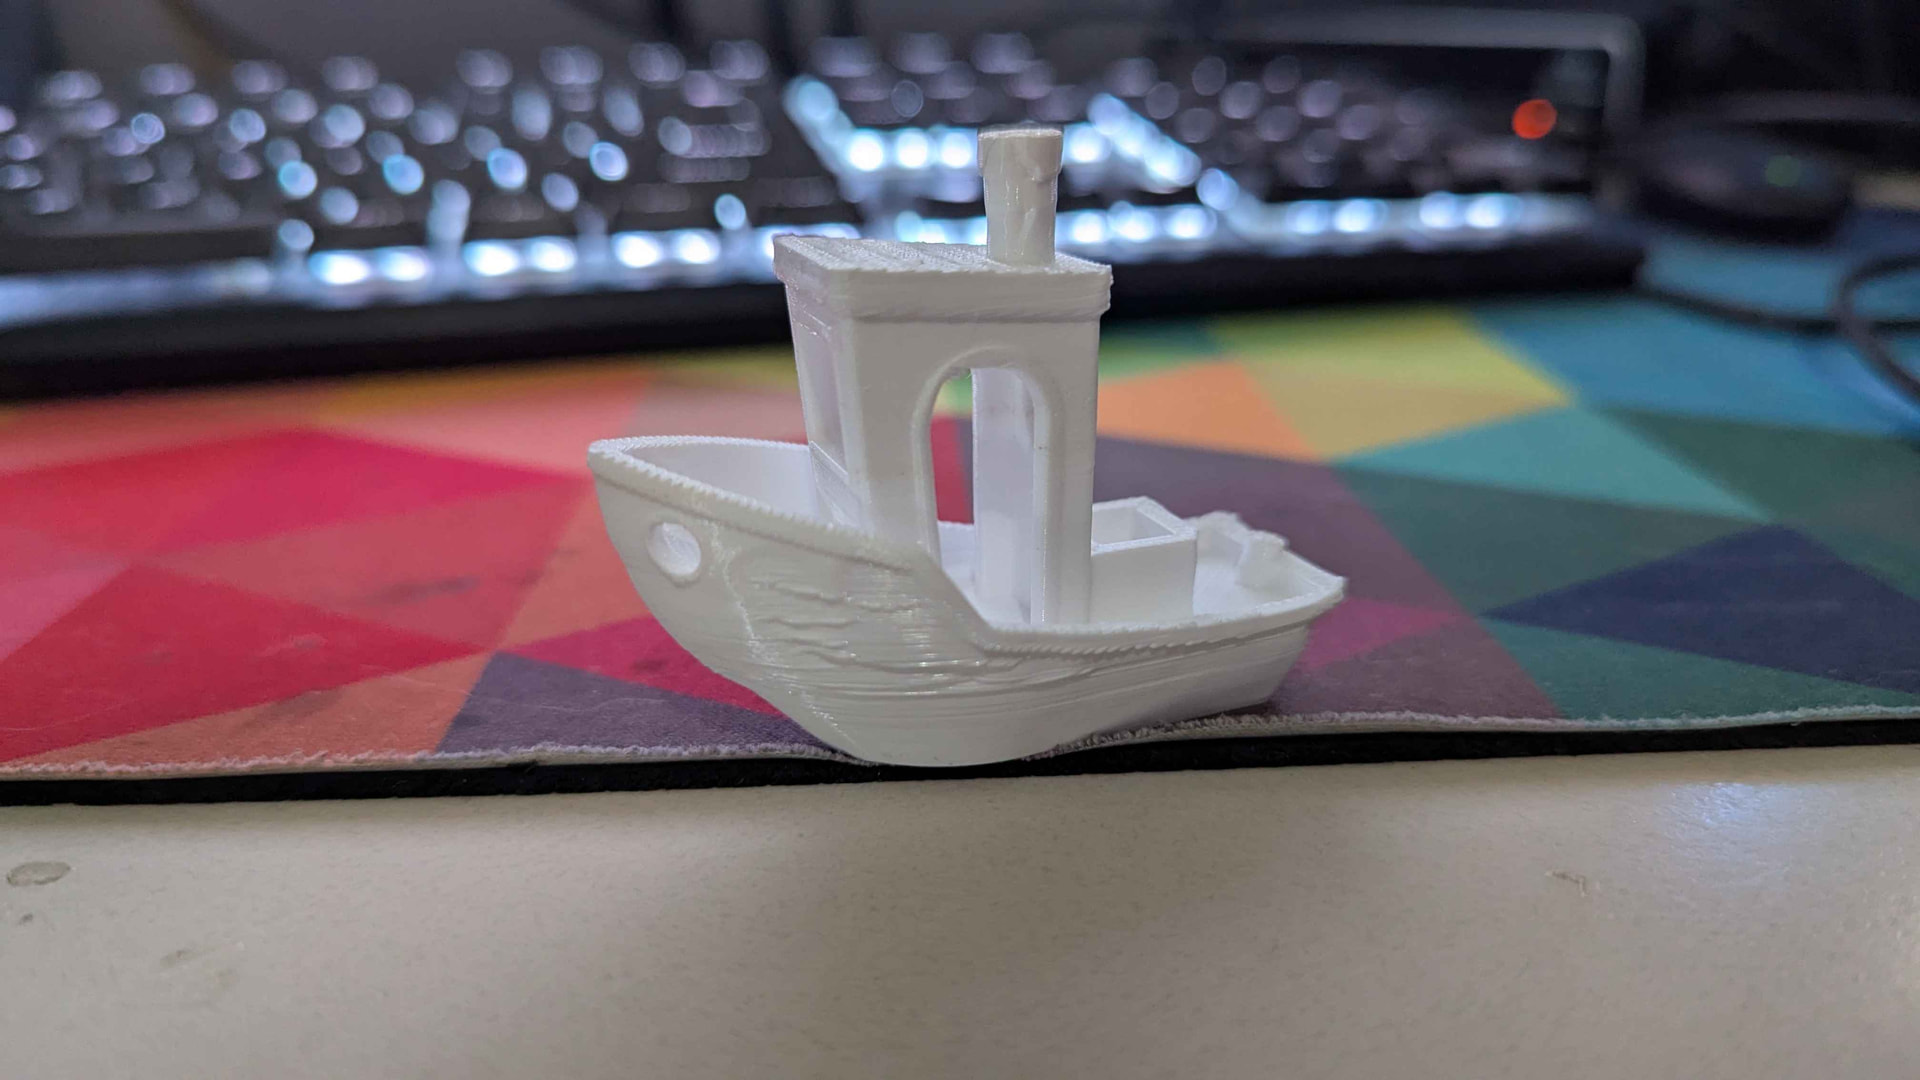
My Benchy has weird ripples in the front hull and the rear. Its probably something to do with overhang, but I don’t know what causes it. I’ve printed a couple out trying to tweak it, but have had no luck.
P1P
Petg Basic, Min 235 and Max 260
This is my first ever post on the Community Forum so if you have recommendations of what to do better please let me know.
Are you drying your filament? How? (Details) PETG is known to grab water and have that water cause problems.
First of all, the important question:
Did you use the Benchy that’s stored on the printer - which is intended solely as a speed benchmark and not for quality - or a Benchy from, say, MakerWorld, which strikes a balance between quality and print speed?
The choice of Benchy often has an extremely large impact on the print result.
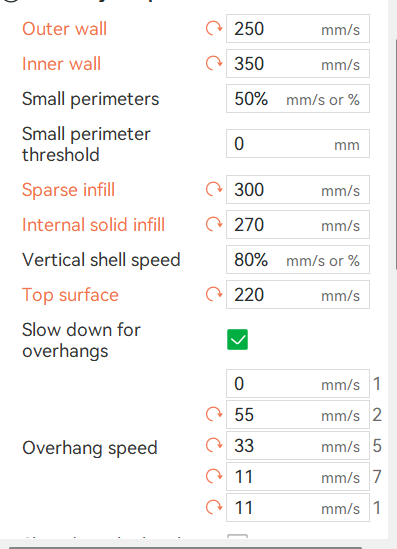
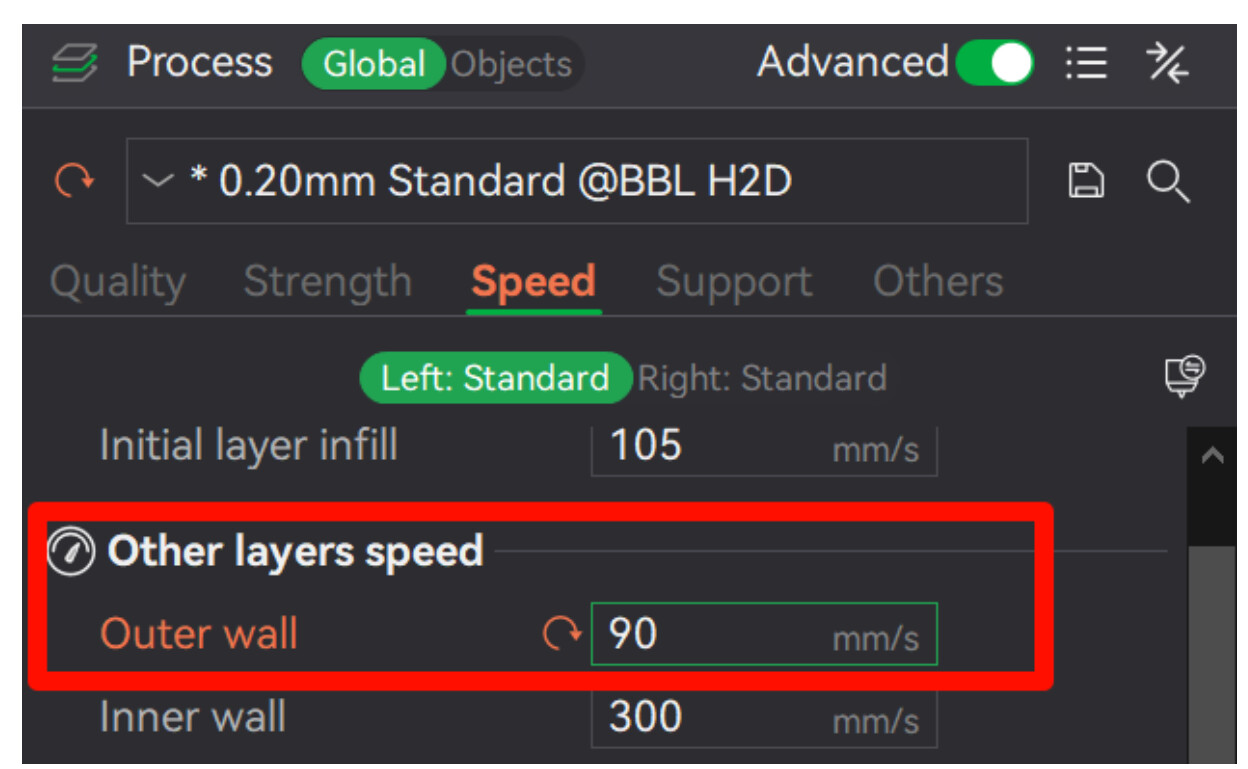
Your values seem to differ significantly from what Bambu recommended. How did you determine these values? Your outer walls: 250 mm/s. Bambu recommend 90 mm/s.
The flaw looks like “surface local under-extrusion,” as described by bambu in the wiki:
…and as MZip already mentioned: PETG almost always needs to be dried.
Yeah, I normally just put it in the dryer and print out of that, but for this specific model I forgot to start it. However, the problem still occurred when I was printing with fully dried filament. I’m using this dryer to dry my filament.
I Used the Benchy from Makerworld. I selected the P1 petg file
I don’t fully remember why I changed the speeds. I think that I thought that it was over-extrusion for some reason… But whenever I go to click the orange refresh thing it sets it to 200 so I just assumed that that was the speed that I should print at. I will go ahead and put the speed at 90 and see what it does. I also found the flow ratio which was lower than what bambu recommended.
I’ll give an update whenever it finishes printing
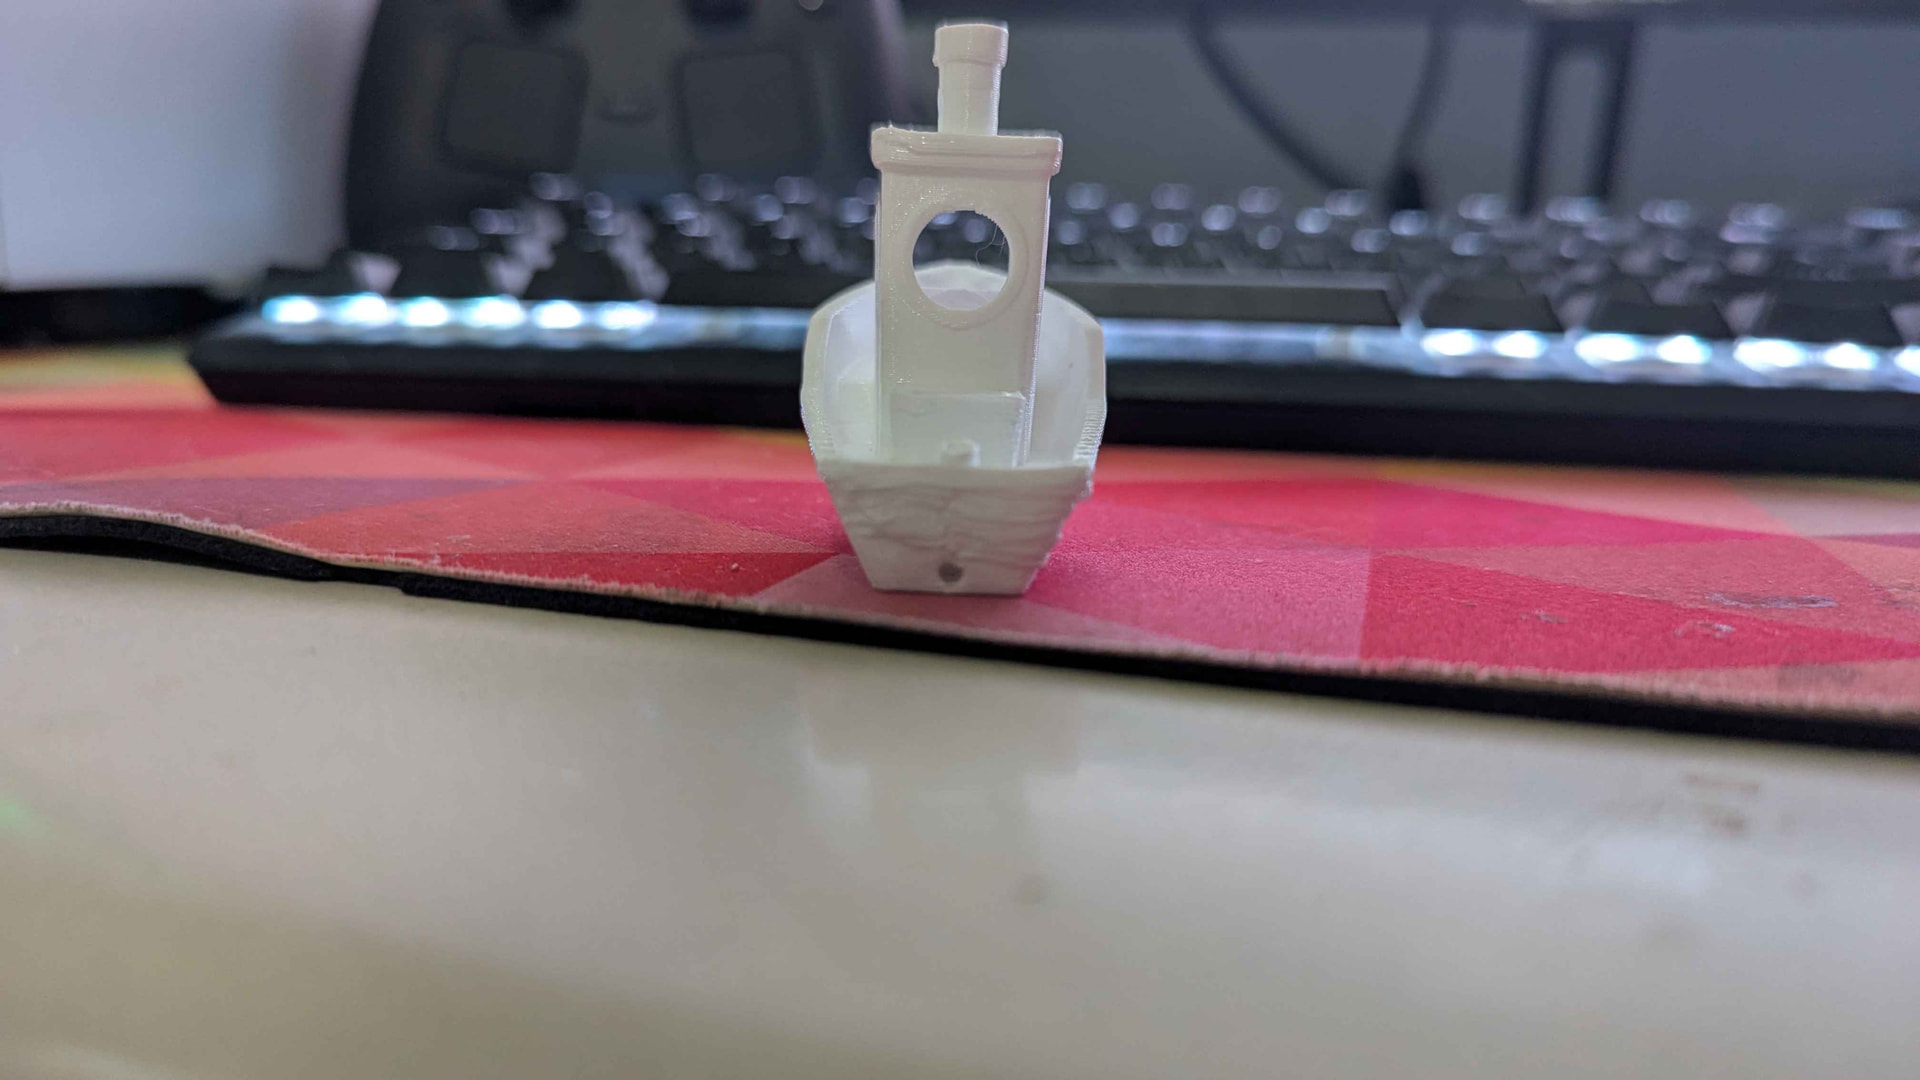
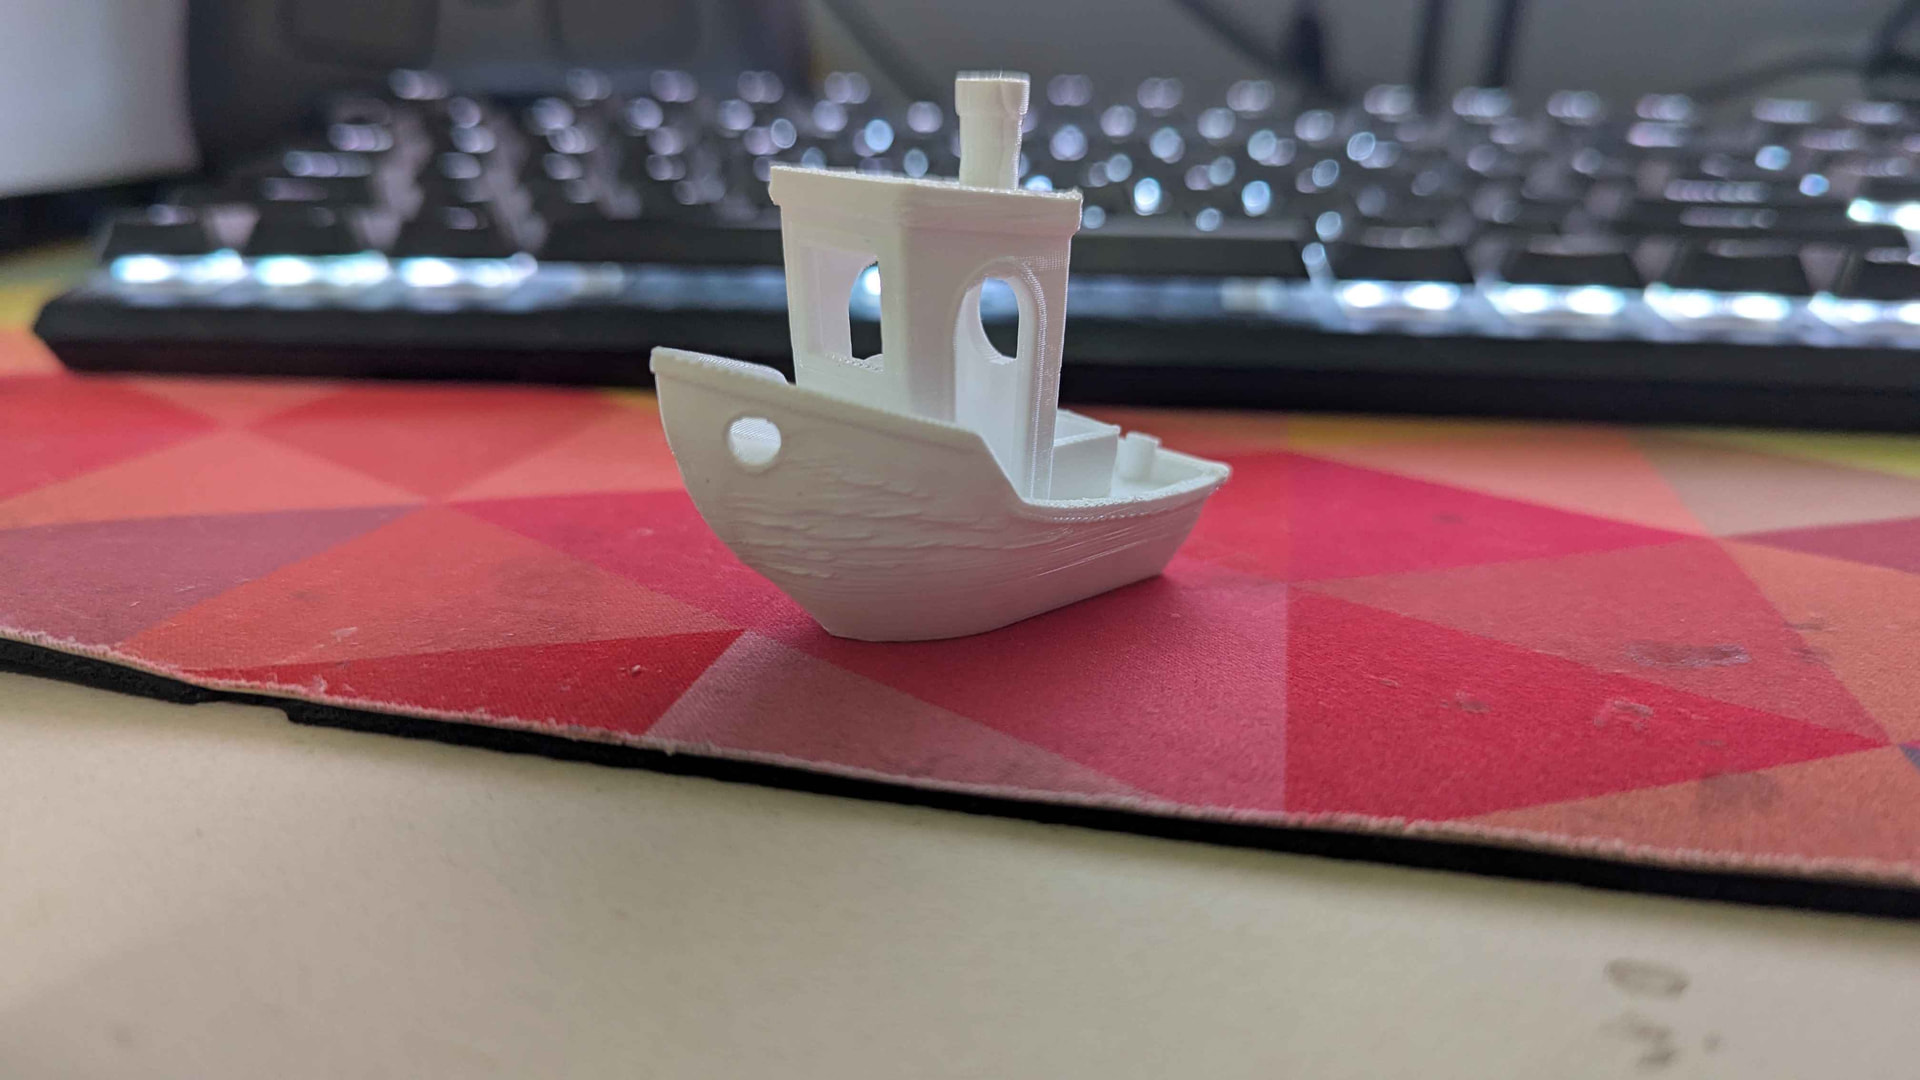
What speeds did you change? For PETG Basic (and similar) I usually set all speeds 80mm/s unless they are already below this.
I also use 12mm³/s for max flow while not opening Pandoras Box of cooling. I just change those to match the generic PETG profile.
I usually also disable z-hop and occasionally need to enable “wipe while retracting”.
But is does depend on which specific PETG you are printing. Process windows vary greatly between Basic (and equivalent), HF, GF and CF.
 &

May I ask a few basic questions to get a general sense of the problem?
- You say it’s a P1P - is that right?
- Is it new, or how long have you been using it? I ask because of wear and tear.
- Do you have problems with other models as well? For example, have you printed this model with PLA recently?
- Have you dried the filement in the meantime?
- Have you performed a calibration using exactly this filament in Bambu Studio? I mean both “Flow Dynamic” and “Flow Rate” - those are two separate tests.
Some of these questions have already been asked, but could you please summarize everything?
I changed the other layers speeds. my outer is 90 and inner 300 currently

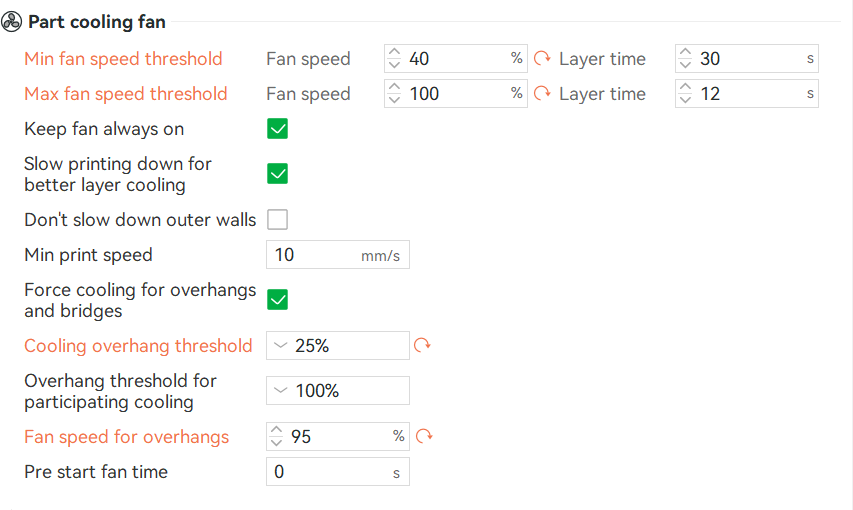
these are my fan speeds
I don’t know for sure if I have z hop on, but I think I turned it on for a previous print.
Im using petg Basic
-
yes
-
its kinda new (I got it last fall) it currently has 932 hours
-
I havent messed with pla or any other filaments very much. I know I started out with pla but I have switched to petg basic now
-
its been drying yes
-
I did do the tests, the flow rate that I thought was the smoothest (none of them were ever actually smooth) made my flow ratio .92 which the bambu wiki said could cause under extrusion. so I upped it to .95
I don’t havent really done much maintenance besides cleaning my plate. the most I have done so far is take out the hot end and get all the dust off of it. I hope answering these questions helped.
My PETG experience comes from the original release of PETG Basic rather than todays variant. But PETG does reward going slow. I’d recommend going down to 80mm/s for all speeds (except travel) that are higher. I may be a bit conservative, but I prefer a good, slow print to two bad, fast prints.
The fan settings look familiar. But I am on hol’s atm and can’t check. Not sure about the overhang fan settings though.
Also, make sure to change the default sparse infill setting from Grid to Rectilinear. The photos don’t show such defects, but PETG sticks to the nozzle like Romeo to Juliet so try to avoid crossing patterns.
&
I’ll try that and update when it finishes
IMO your speeds are way too high for regular PETG. I dont use bambu’s PETG so I dont have a good opinion on your temp or other calibrations (you say min 235 max 260, ok, but whats it set to?) but after slowing down, if its still a little loopy on the roof, drop temps slightly.
I have to assume that you are using BambuLab ‘s PETG basic filament, rather than some other manufacturer.
A lot has been mentioned already, but unless you are running a high speed variant, you aren’t likely to reach those sorts of speeds.
Otherwise, trying to use a Benchy meant for PLA could also be causing issues between print profiles, filament profiles, etc.
I’d suggest downloading this Benchy, which I’ve been using across numerous different filament types with great results: Benchy Optimised For All Filaments - Free 3D Print Model - MakerWorld
Grab the PETG Basic profile, and try that without changing any other settings.
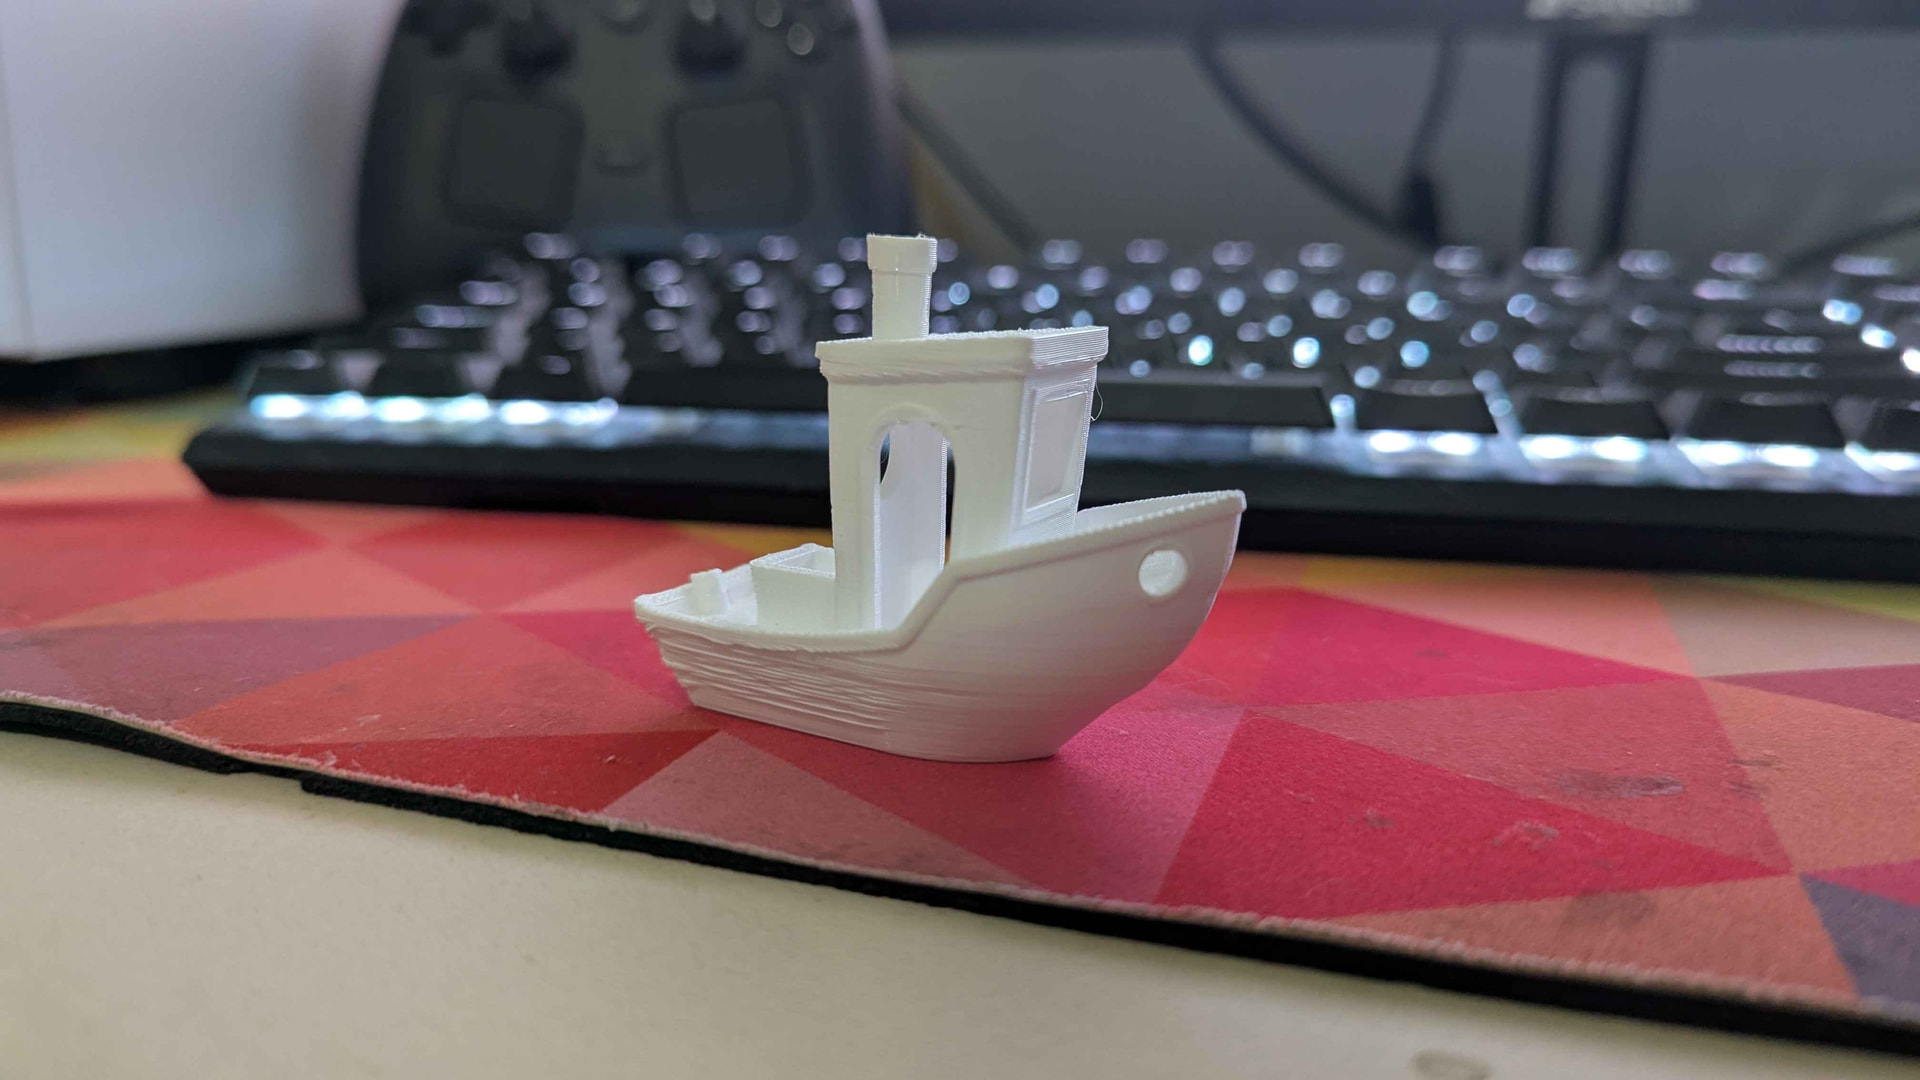
I did that and it worked. I don’t know if it is the file that you sent or if it is the fact that my part cooling fan wasn’t working for some reason. I don’t know when it stopped, but I think that that would have been a large part of the problem. But now it printed pretty good.
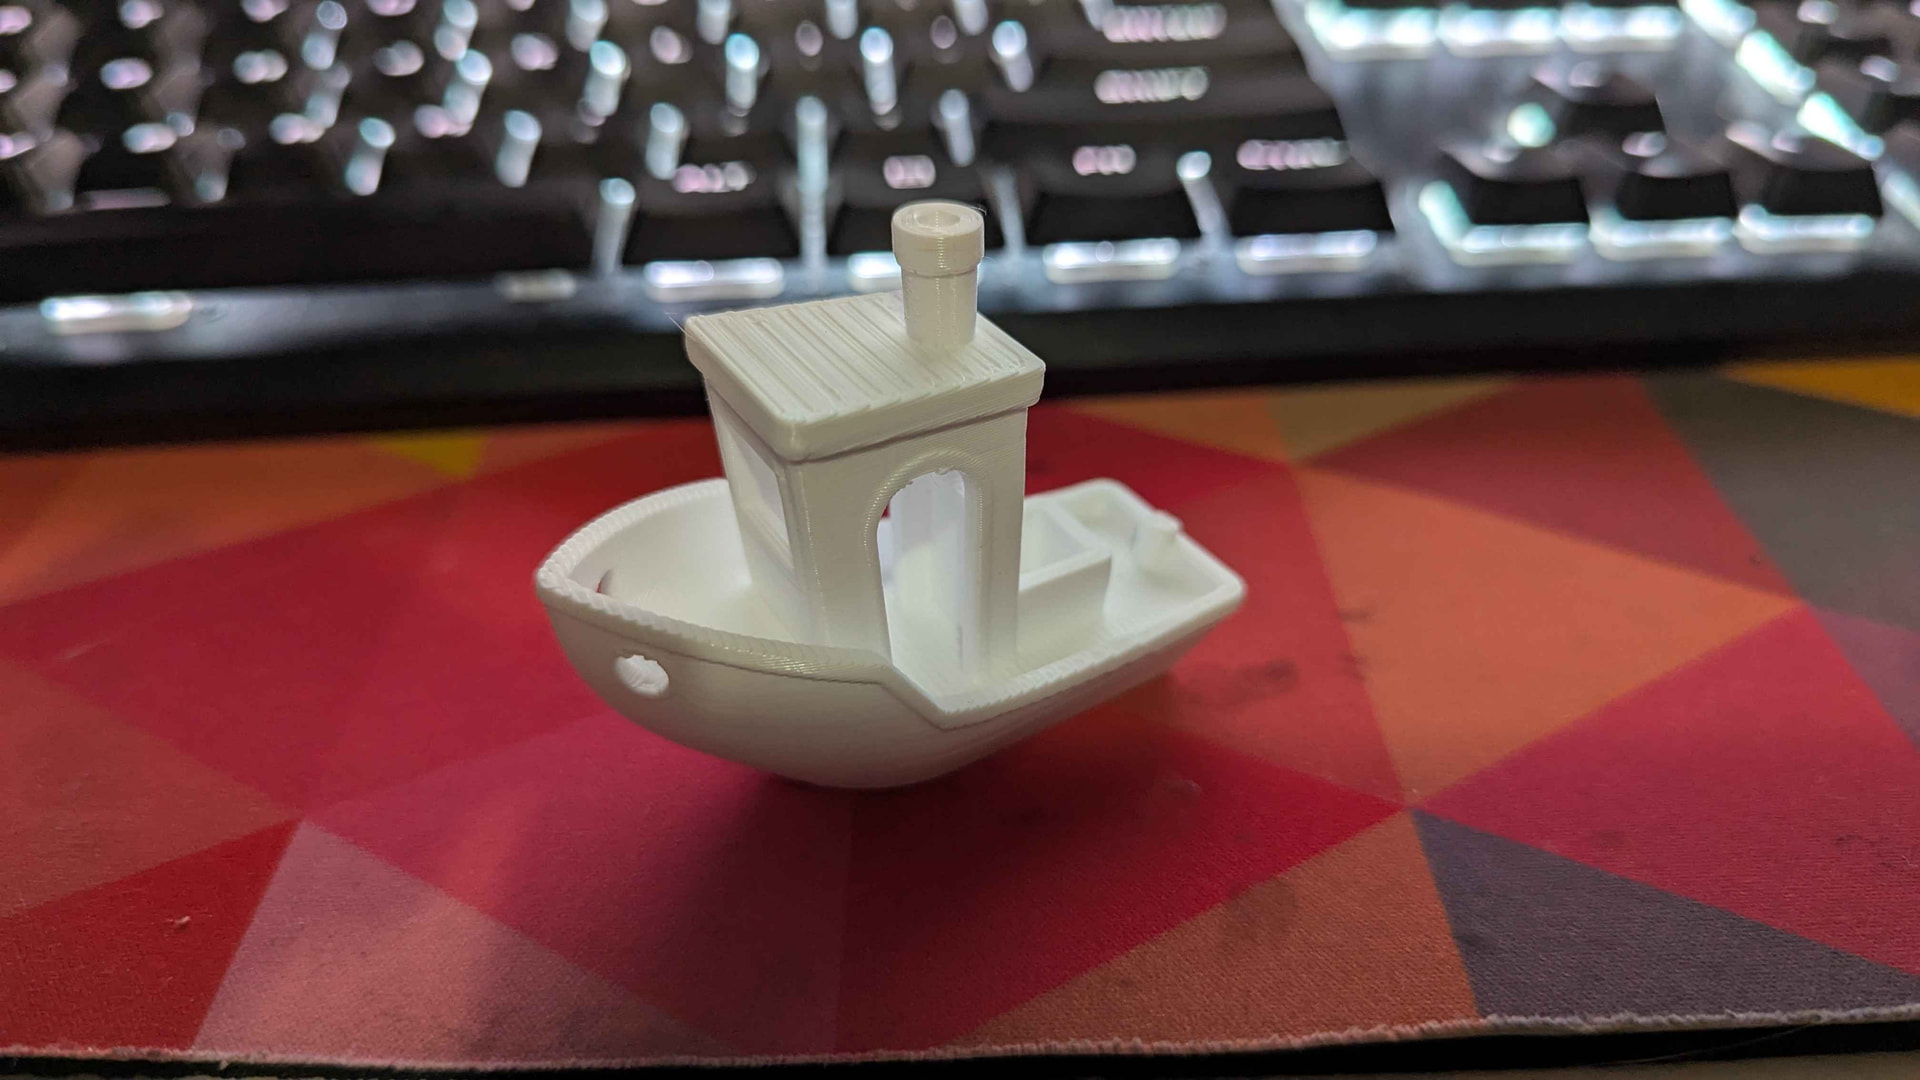
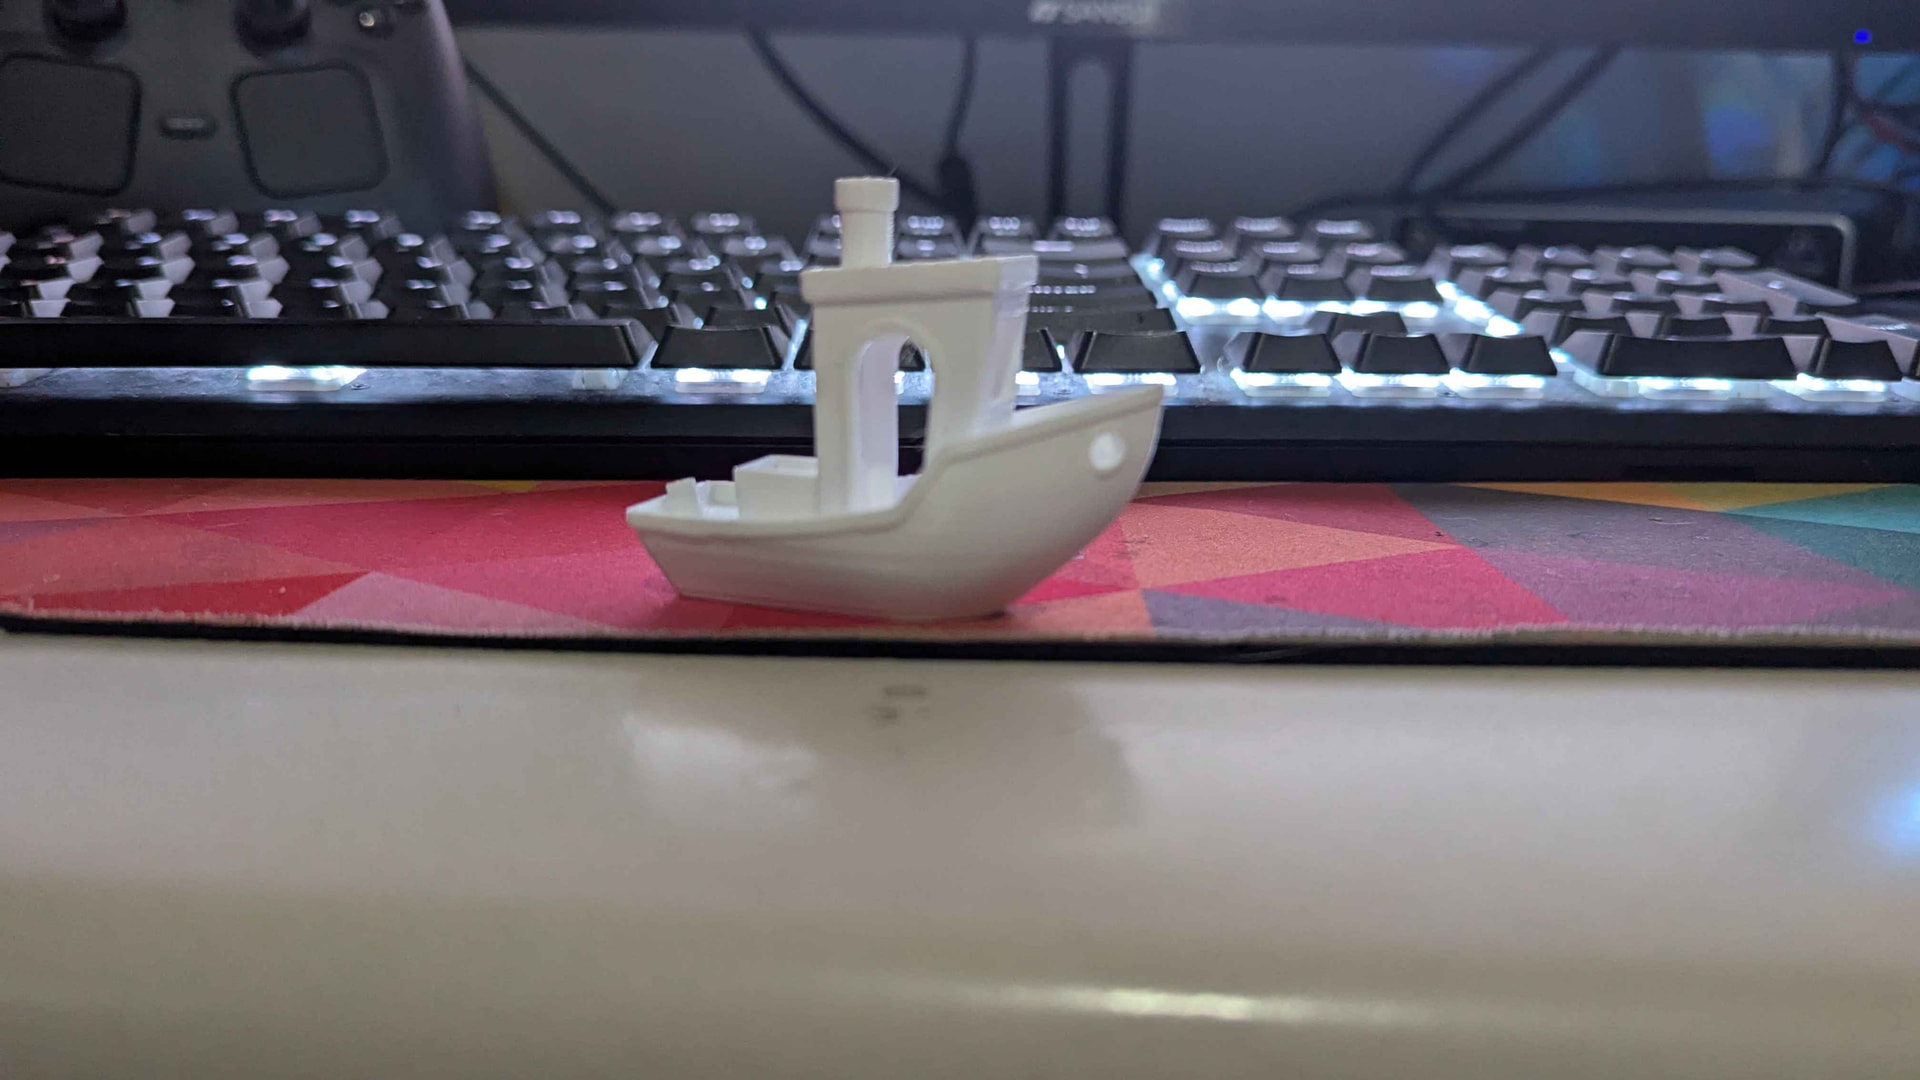
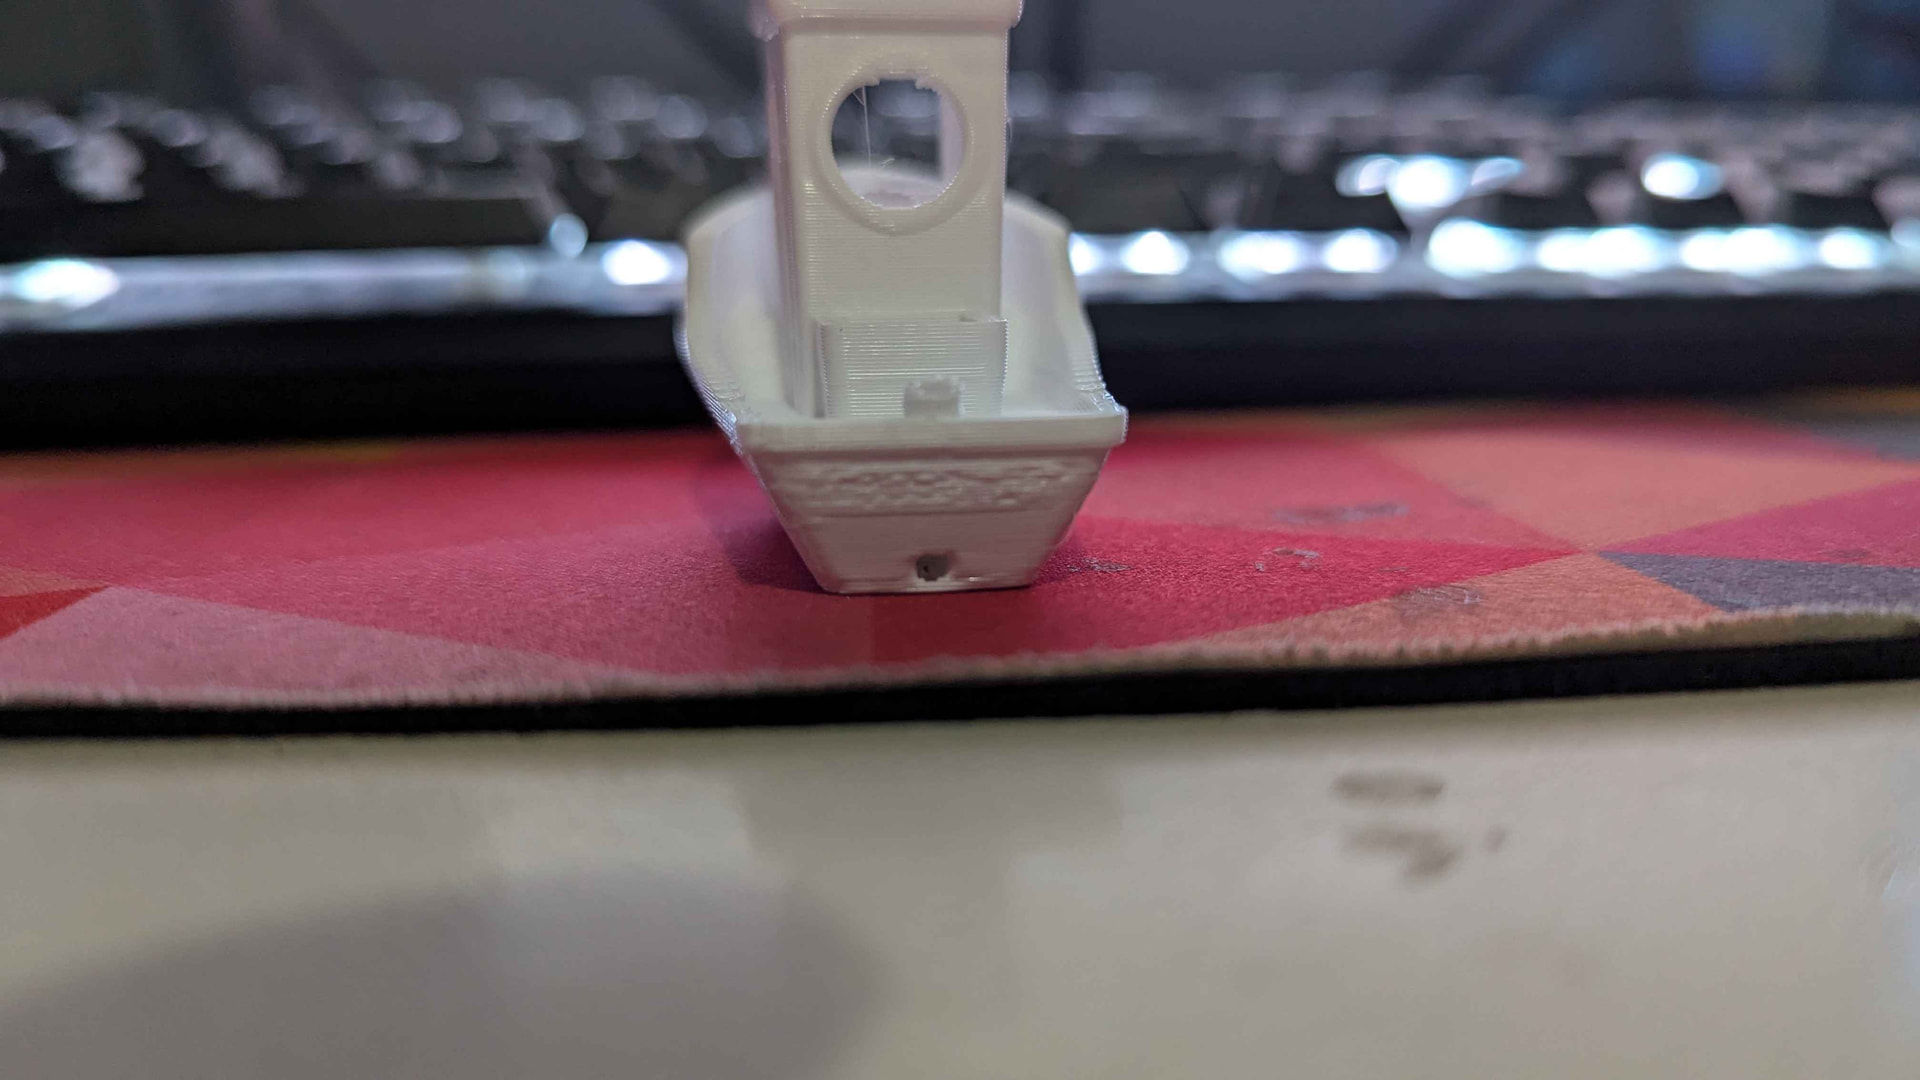
it isn’t the absolutely perfect but it is a big enough of improvement that I am fine with it. Now I have to find what to do with all of the benchy that I printed
Huge improvement! Also good to know you were having some issues with the cooling fan.
Good luck with refining and your next big prints!
For the benchies… particularly the bad ones, there’s not much you can do with them.