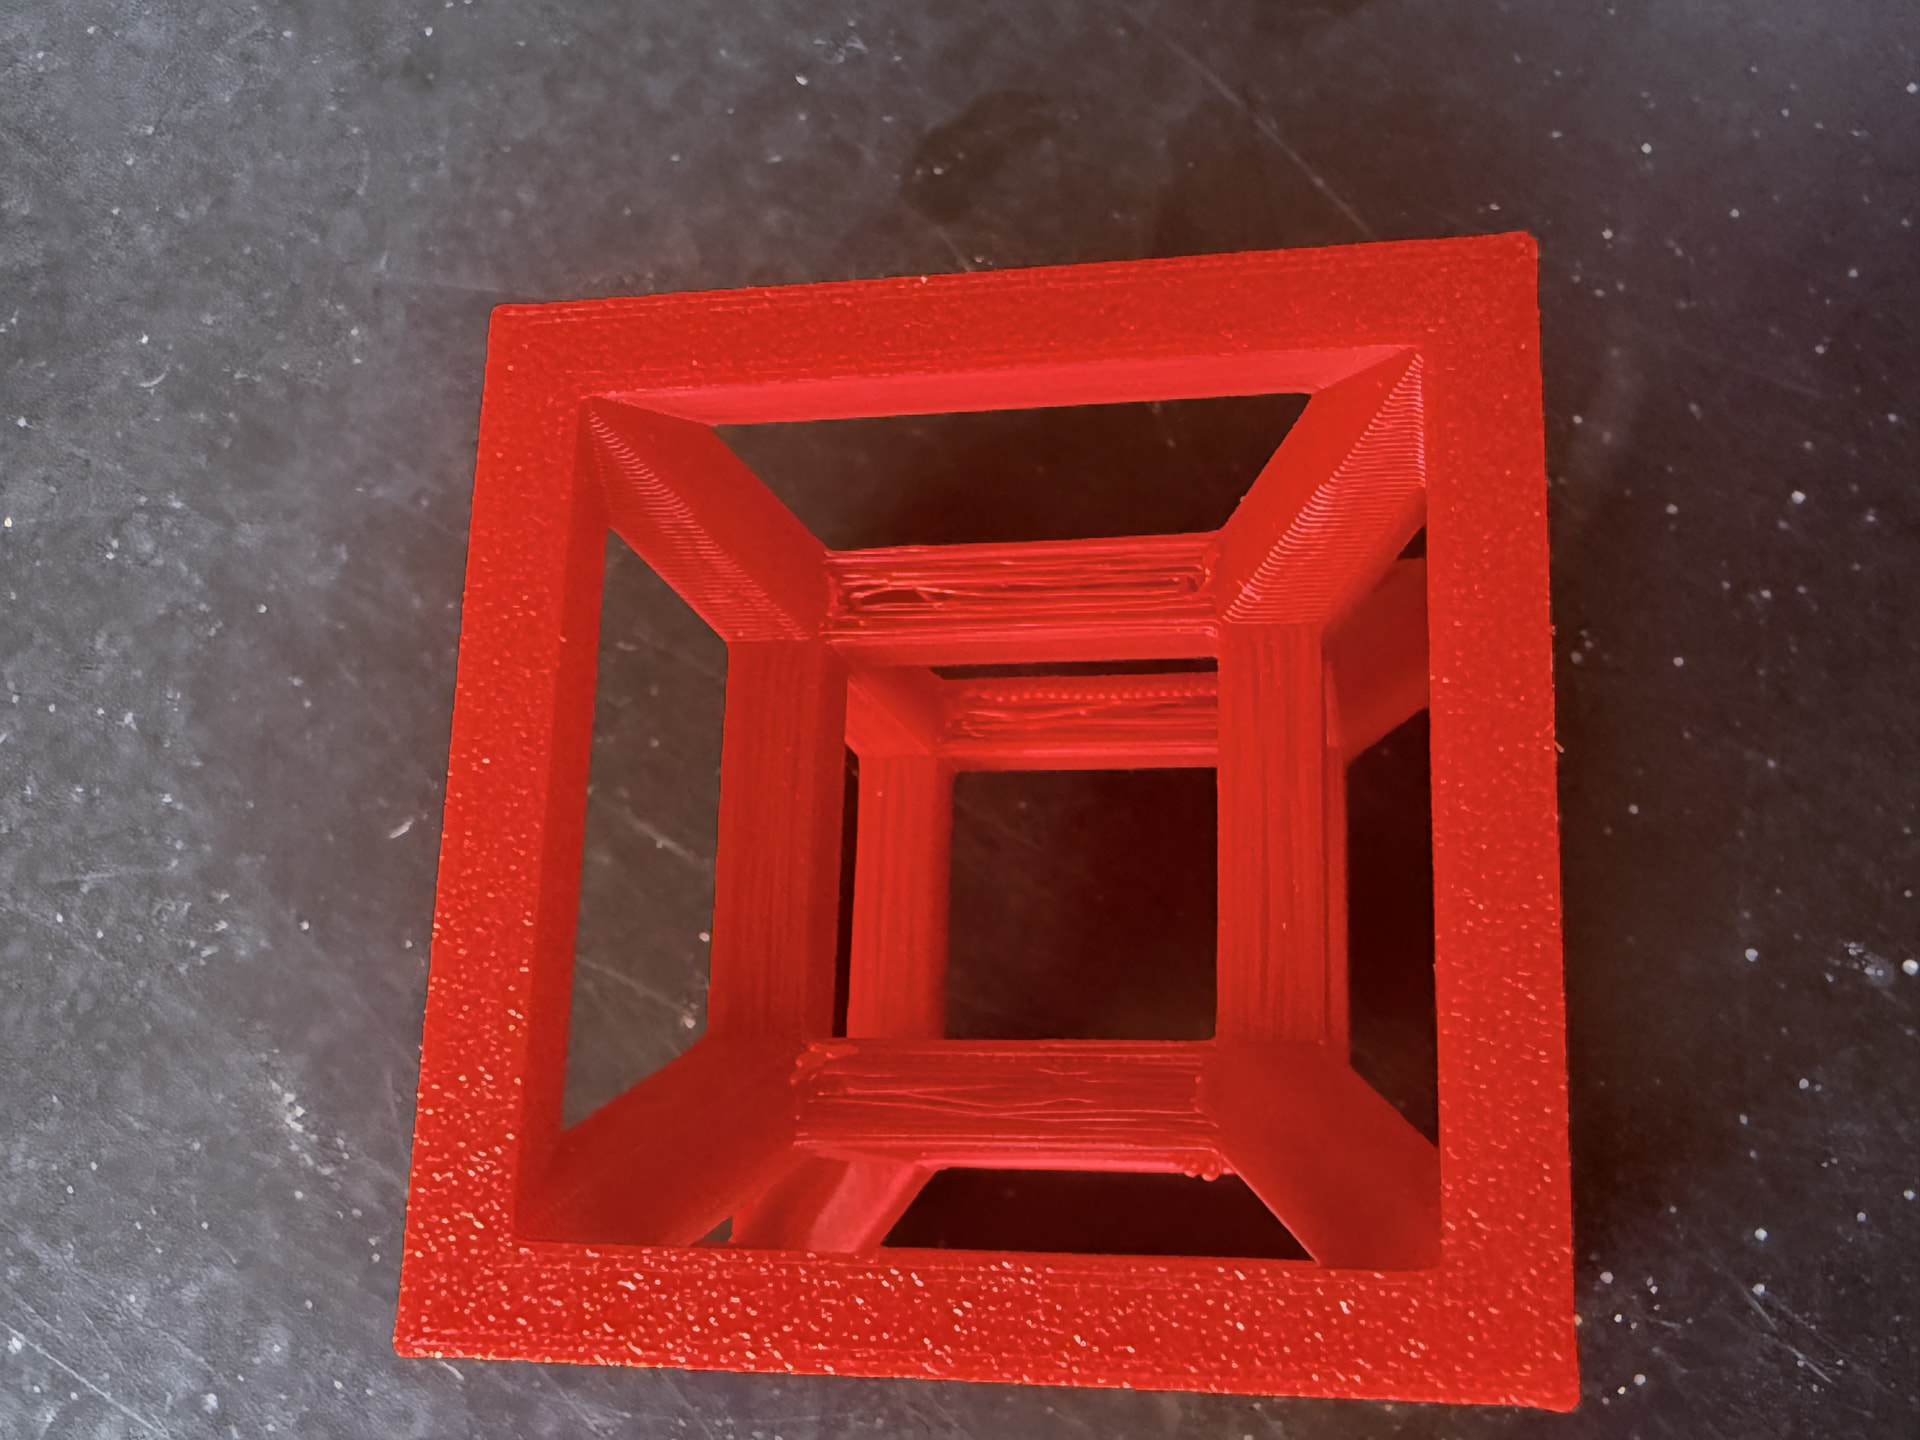
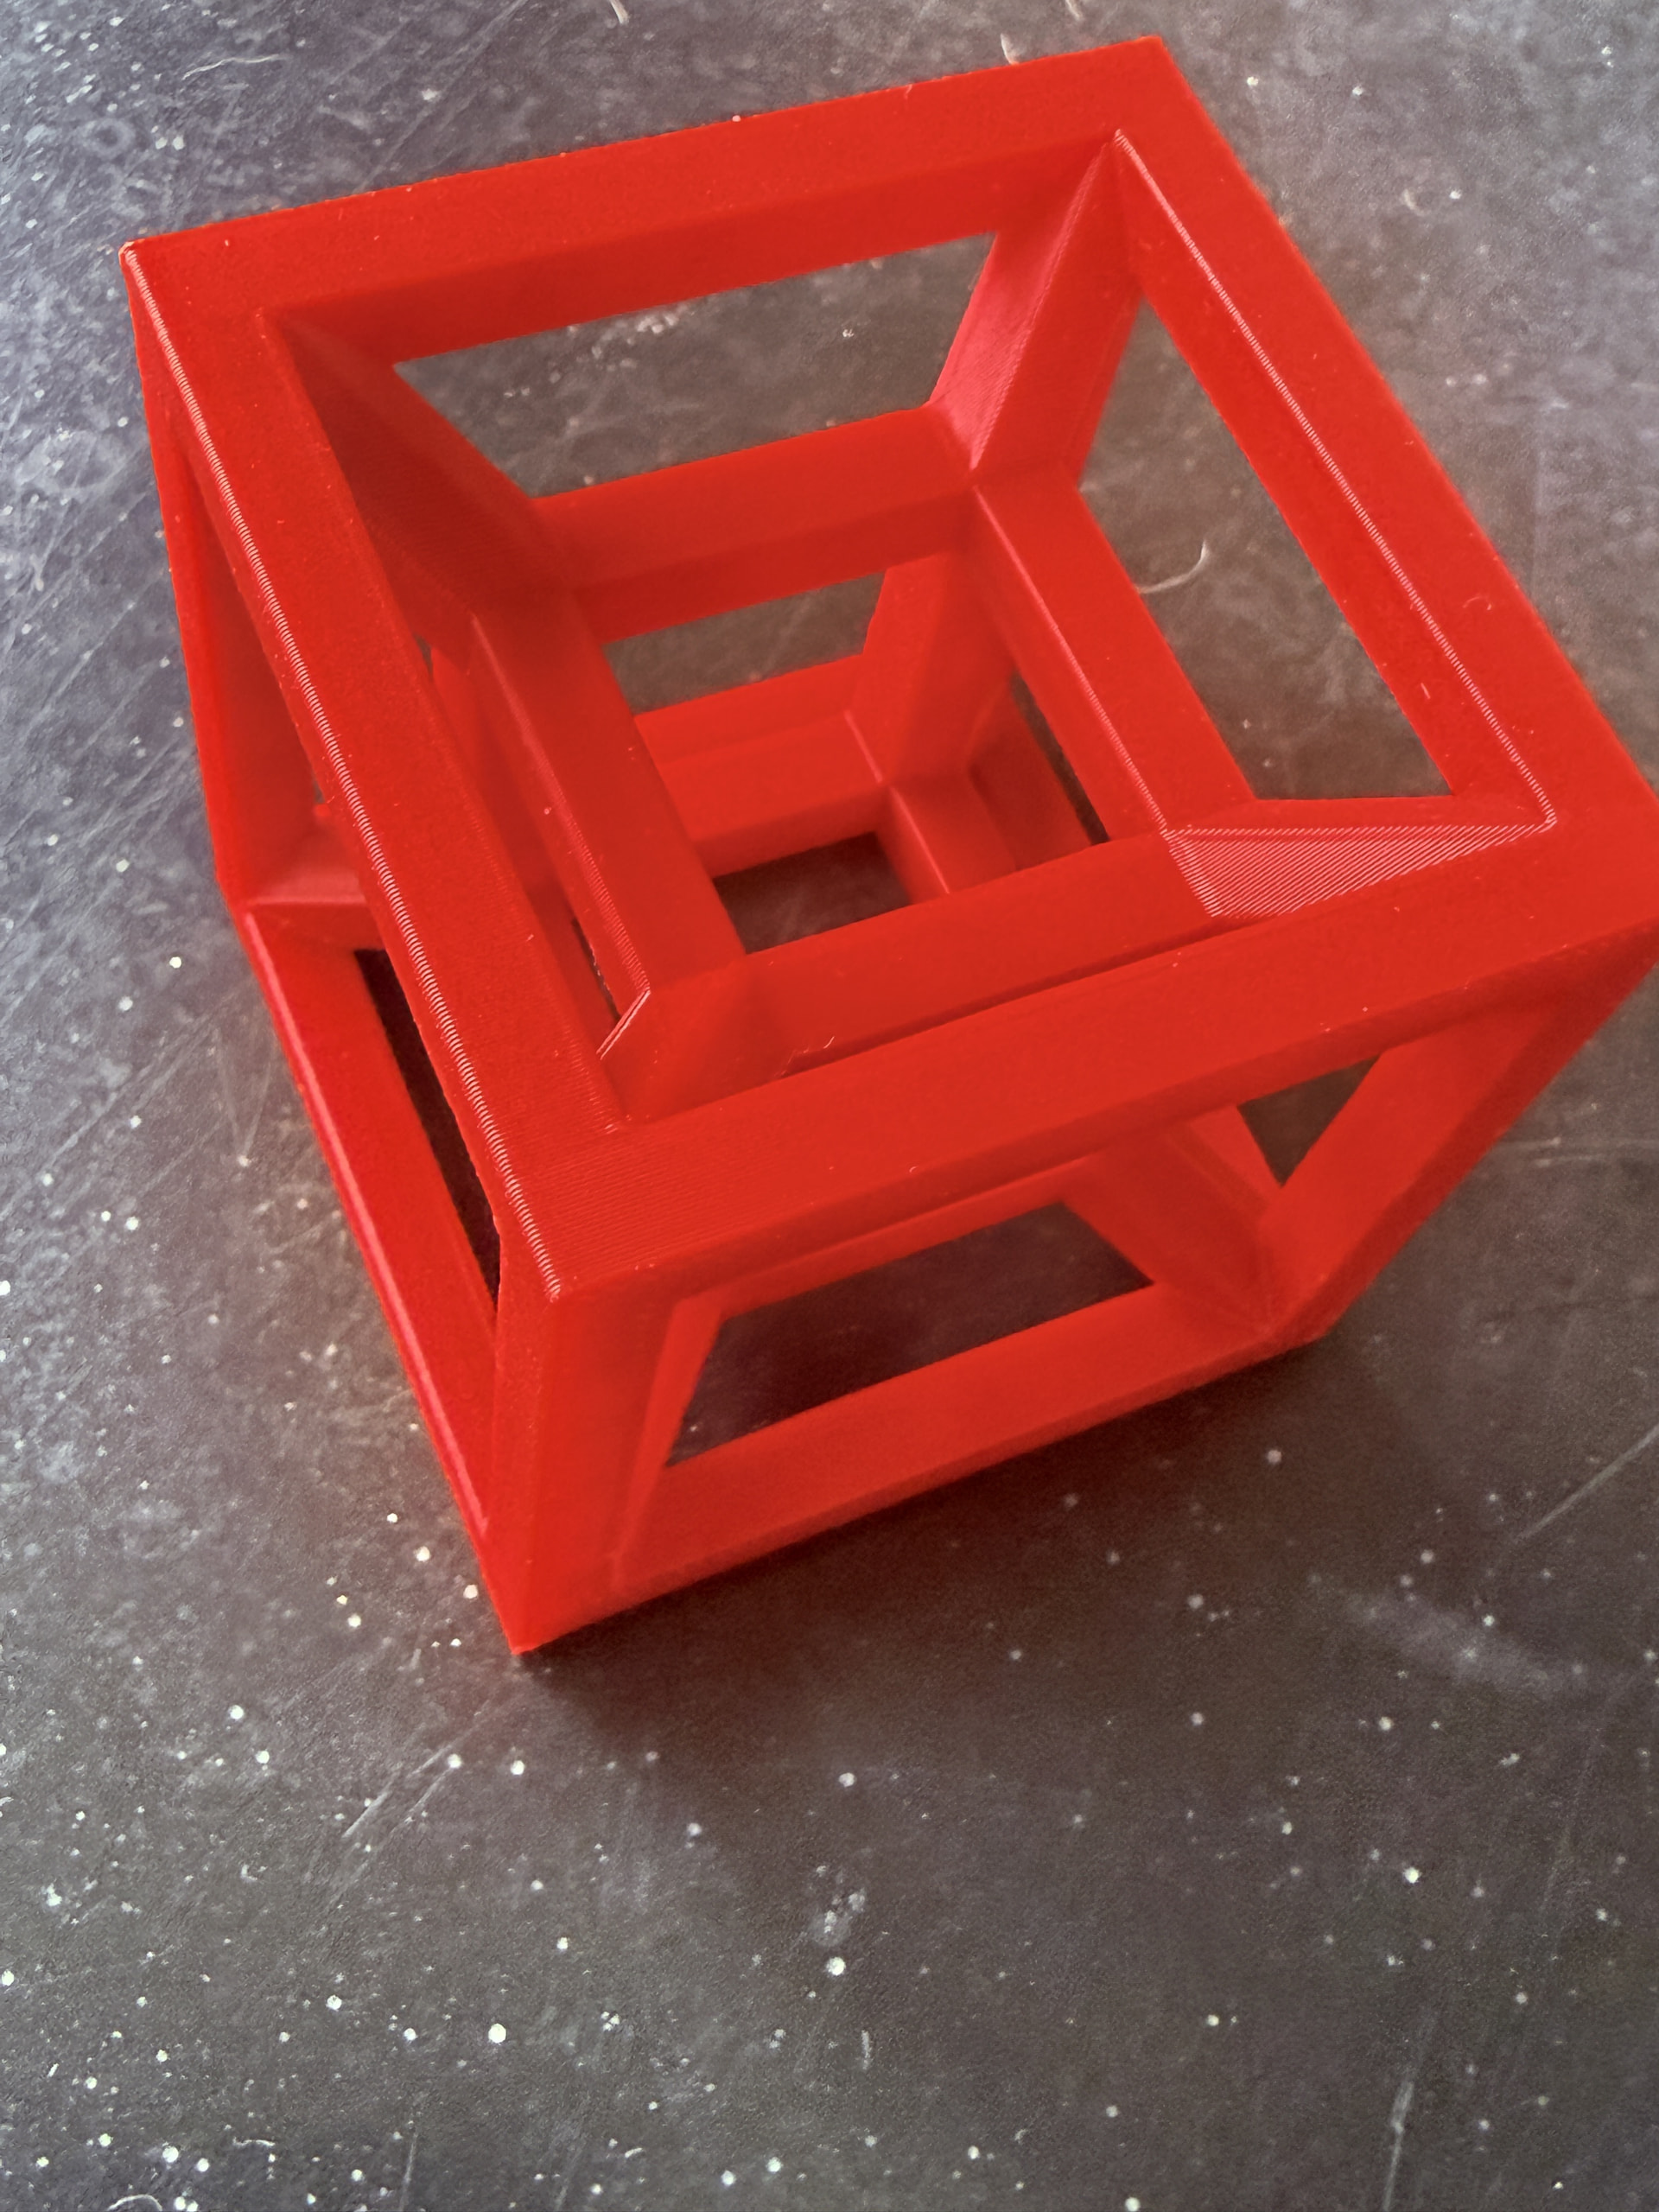
I am having a problem dealing with the underside of the bridges in my print that causes it to be stringy and droop a little. I tried supports but they only made the problem worse. You can see from the 2 photos that one shows the stringy underside while the other photo shows a satisfactory surface on the tops and sides
I tried supports using a few or a lot but it only made the problem worse, was still stringy, and it left the edges more rough.
I tried using a heat gun to melt it hoping that the strands would melt into smoothness
I tried printing it tilted at a 45 degree angle and it made it messier not just on the underside but on the whole print
Tried painting but not sure if I used the right paint also tried spray painting
I experimented with layer height and speed settings in Bambu studio, also experimented with slicing
I tried using: Pla, Pla+, cf-Pla, and even tpu
Problem generally fixed itself at super small scale like 2inch by 2inch but I want 4inch by 4inch as a minimum to bridge the gap
I’ve only tried printing so far on my Bambu labs a1 but havent tried any other printer
Does anybody know how this could be solved? I’m willing to consider methods that involve another kind of printer or production method. I’m past the prototype phase and want to find a way to begin production quality prints so that its smooth on all sides.
Bridging such a long distance will never be perfect. After all, your printer is printing in mid-air. That said, I actually think the result is good.
You can try to optimize it further: Make sure the filament is dry. Perform a flow calibration. It’s best to follow the advice from the wiki:
If you want it to be almost perfect, you’ll have to take maybe a completely different approach: Support Filament or PETG for PLA as an intermediate layer for the support.
Alternatively, a chemical solution - If you really want it to be completely smooth: The best thing to do is go to YouTube and search for “PLA smoothing.”
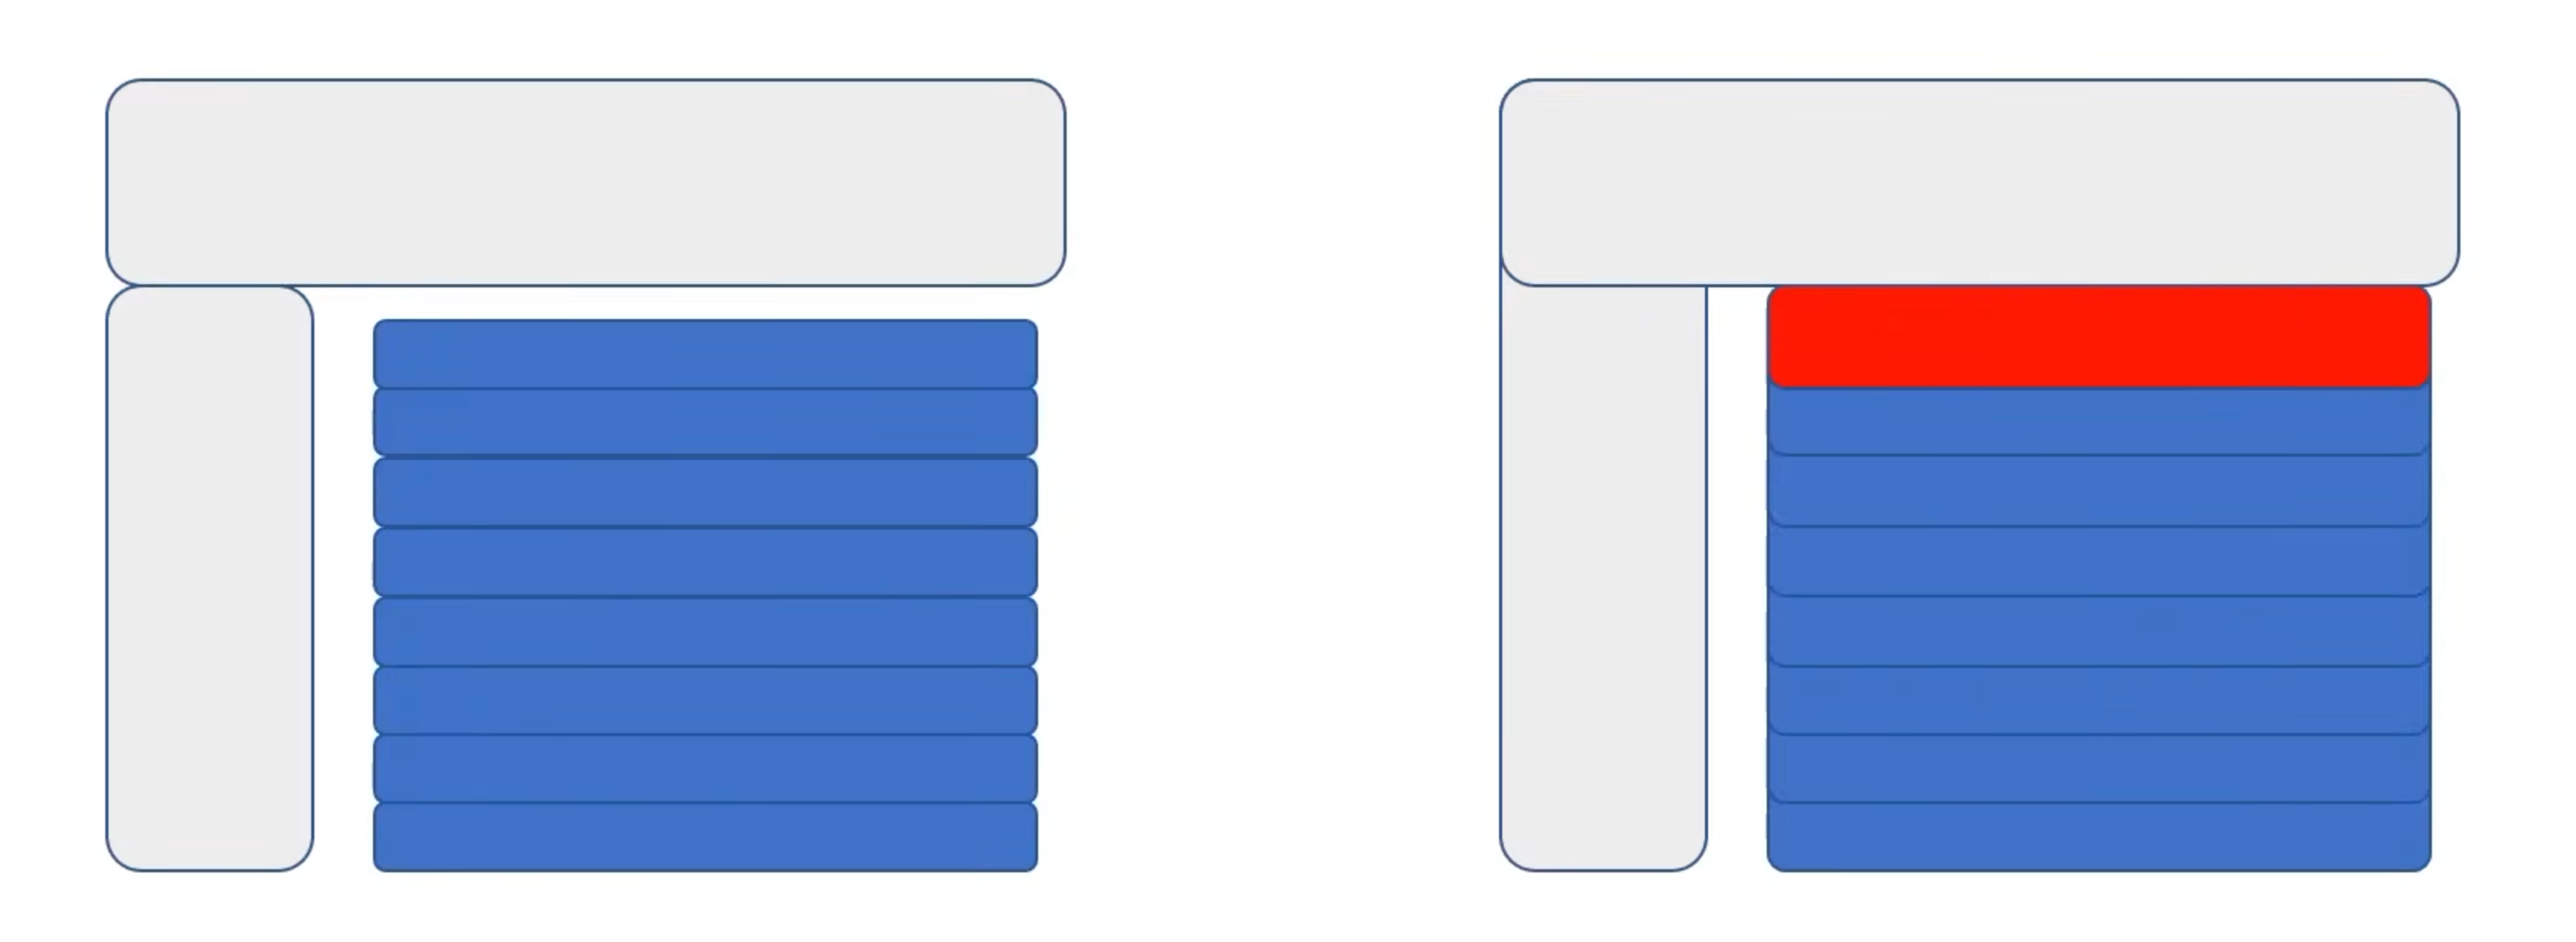
You could design a removable and reusable helper tool to support the bridges.
Say you were using PLA - you’d design a helper tool in PETG that sits directly under the bridge sections.
Configure the sliced file to pause immediately before the first bridge layer. When the printer pauses, snap the helper tool onto the print, hit resume, the bridges are no longer unsupported, so the first layer goes down clean. After the print is done, pop off the helpers and repeat.
Otherwise, if you’re willing to look at other printers, the X2D, H2D, or H2C will all allow you to use dedicated support interface material that will give you the absolute best print quality for those bridges.