Warping Issues with PA6-GF Filament

Dear Team,

I’m experiencing severe warping issues with Bambulab’s PA6-GF filament, regardless of the settings used.

Setup:

Printer: P1S with AMS, 2 weeks old, fully calibrated, factory settings.

Room temperature: 21°C.

Plates: Textured and Smooth Plate from Bambulab, using adhesive (3D-Lac spray).

Nozzle: 0.4 mm hardened steel.

Extruder gears: Currently stainless steel, with a hardened steel set available but not yet installed.

Slicer: Bambu Studio, latest version.

Settings: Using AMS system with the automatically detected filament profile for PA6-GF. Speed reduced (≤100 mm/s), bed temperature 100°C. Cooling fans set to a maximum of 10%, as defined in the profile, and I have confirmed the fans are working properly.

Infill: Tested with 10% (reduced) and 15% (default) using Gyroid and standard infill patterns.

Filament preparation: Dried in a filament dryer for 9 hours at 65°C before use.

Problem:
The model warps severely, especially at the corners and across the surface, regardless of the print size. For example, the Benchy detached from the plate mid-print and fell off, with the filament continuing to extrude into the air (see attached photo). My nearly new print plates, including an unused Smooth Plate, offered no adhesion even with glue.

Despite 4–5 attempts using different settings, the issue persists. Other materials like PLA, ABS, and ASA print flawlessly under the same conditions, leading me to suspect a problem with the filament itself.

I would appreciate your assistance.

Best regards,
Patrick


I think those 9h @65°C drying may be rather low for PA6.
https://wiki.bambulab.com/en/filament-acc/filament/dry-filament
I just did some very nice PA6-CF (which admitedly is better at warping than GF due to heat distribution during printing) prints, but dryed for 60h at 60°C.

Thanks! might be the problem and I’ll give it a dry :). The filament was new, fresh from the package right into the dryer. You think it comes “unusable” from factory?

That is at least the one safe assumption. In particular since PA6 is quite hygroscopic.

Alright, filament is back in the dryer. I’ll try my print in 3days again. Let’s see…and find out

Just for when the filament is ready:

  • I have found the smooth PEI with glue giving much better adhesion than the textured plate.
  • A brim can also help. Just like improved adhesion, it treats the symptons rather than the root cause.
  • If in dire straits, you can also try to reduce the layer height (except layer #1) for the first 2-5cm height. That will give a more even part cooling. It works through targeting the root cause.
  • Print with as warm a chamber as possible. You can use a heat soak ahead of printing and be carefully creative about printer isolation. My build chamber was at 49° for most of the print. Used my cardie for added insulation (top, front and sides only) to get to 51°C. Also helped when going for a smoke in the snow :sweat_smile:

I apologize for the delay in responding. Over the past few days, I have conducted multiple tests and tried various solutions to address the issues with PA6-GF filament adhesion and warping. Below is a summary of the steps I’ve taken. It still doesn’t work :frowning: :

  1. Filament Drying

    • I dried the PA6-GF filament in a filament dryer for 56 hours to ensure its dry.
  2. Temperature Monitoring

    • I installed a thermometer to monitor and stabilize the ambient temperature inside the print chamber.
    • It was always between 50 - 65 celcius in the chamber when printed.
    • I also preheated the chamber 1 hour before
  3. Glue

    • I used multiple 3d printing glues:
      • 3D Milk: A plant-based adhesive.
      • 3DLac: A adhesion spray
      • but no glue Stick so far (may this is the issue)
  4. Printing Tests

    • I printed a Benchy test model from Bambu support team provided with 16mm layer height and some slight improvements (lower speed, infill, etc.)
      • It took 4 attemps to achieve a successful print:
      • On the fourth attempt, the model adhered slightly better to the build plate so it could finish the print but still showed some warping.
      • The print quality was otherwise excellent.
    • I suspect the failures in the first three attempts were due to insufficient adhesion and the significant warping of PA6-GF.
  5. Build Plate Tests (always with glue applied)

    • I used the following surfaces:
      • Bambu Smooth Plate: Used for all tests; minimal adhesion.
      • BigTreeTech PET Carbon Plate: No adhesion at all.
  6. Comparison with PETG HF Filament and ABS from Bambu

    • Using PETG HF + ABS by Bambu, I encountered no adhesion issues. The prints sticked strongly with the same glue.
    • The adhesion issues are specific to the PA6-GF filament.
  7. Next Steps

    • I have ordered an additional glue stick for PA to test if it improves adhesion further.

Despite these efforts, it is still surprising how strongly the material warps and how poorly it adheres to the build plate compared to other materials.

Is this normal? Or may it has some defects in the material?

I have attached images of the test prints and setups for your reference.

Thank you for your continued support. I look forward to your recommendations.

Best regards,
Patrick


Well, I have had very good experiences with the PA6-CF. And that is probably the big difference. The Carbon helps to distribute the heat more evenly in the part during printing, greatly reducing warping.
Would CF an option for your project? Or do you need GF?

Because other than that, it looks like your only remaining options are the addition of brims with a 0mm gap, thinly distributed Dissolved PVA glue stick with a freshly cleaned plate (dishwashing liquid and water), using an even finer layer height (0.08mm) as well as printing even slower. Unfortunately, I can not give you a “this will work”. It should improve somewhat, but PA6-GF seems to be a different beast from PA6-CF.

Thanks a lot! I’ll try the other glue and let’s see.

I can also switch to the ca version. No probs. I’ve just bought the gf for convenience as it can be printed from the AMS.

I am just a bit disappointed that it doesn’t work so easy and at this price point so warping. But let’s see what the glue stick brings!

Overall the material is really nice when it stays in place.

I’ll keep you updated.

So sorry for bumping, but I also initially had warping issues with this filament. I resolved them by lowering extruder temperature gradually until the issues went away. Warping is related to the material’s thermal expansion coefficient, so the larger the delta, the more shrink and tug it’ll experience. The delta you need to close is dependent on ambient. My chamber averages ~55C, and was warping like mad printing at 285C. I lowered it to 270C, and now everything’s all fine and dandy. Yes, Z tensile strength is slightly weaker now, but that hasn’t been a problem for any of my usecases.

Magigoo PA glue works for me, a brim helps also. I find it gets stickier if the plate isn’t cleaned than if it is.

I know this is an old thread but came across it and thought I’d leave some of my experience.
I’ve printed a fair bit of in PA6-GF now on an X1C and found the following settings to help quite a bit!
On smooth PEI plate with magigoo:
Bed temp: 50 C
Extruder temp: 260 C
No cooling for the first 3 layers
Part Cooling fan:
Min Fan speed threshold: fan speed 0, layer time 5s
Max fan speed threshold: fan speed 0, layer time 20s
Aux fan 0%

Hopefully this helps!

Hello everyone. I had the same problem and it helped me a lot to reduce the default bed temperature from 100C to 80C. Paradoxically, when I set it to 110C, the problem got worse. I use 3D Lac and my settings are as follows. Nozzle 290C and Bed 80C. It works for me so I recommend you try it too.

Thanks a lot for this, seems to be working fine!

H2S Printer

Bambulab PA6-GF

Nozzle 245°C

Cabinet 60°C

Bed 70°C

Glue.

Which build plate for this settings? I Used Biqu Glacier and ir warps, 110 bed, 290 nozzle, 65 chamber and 3D Lac

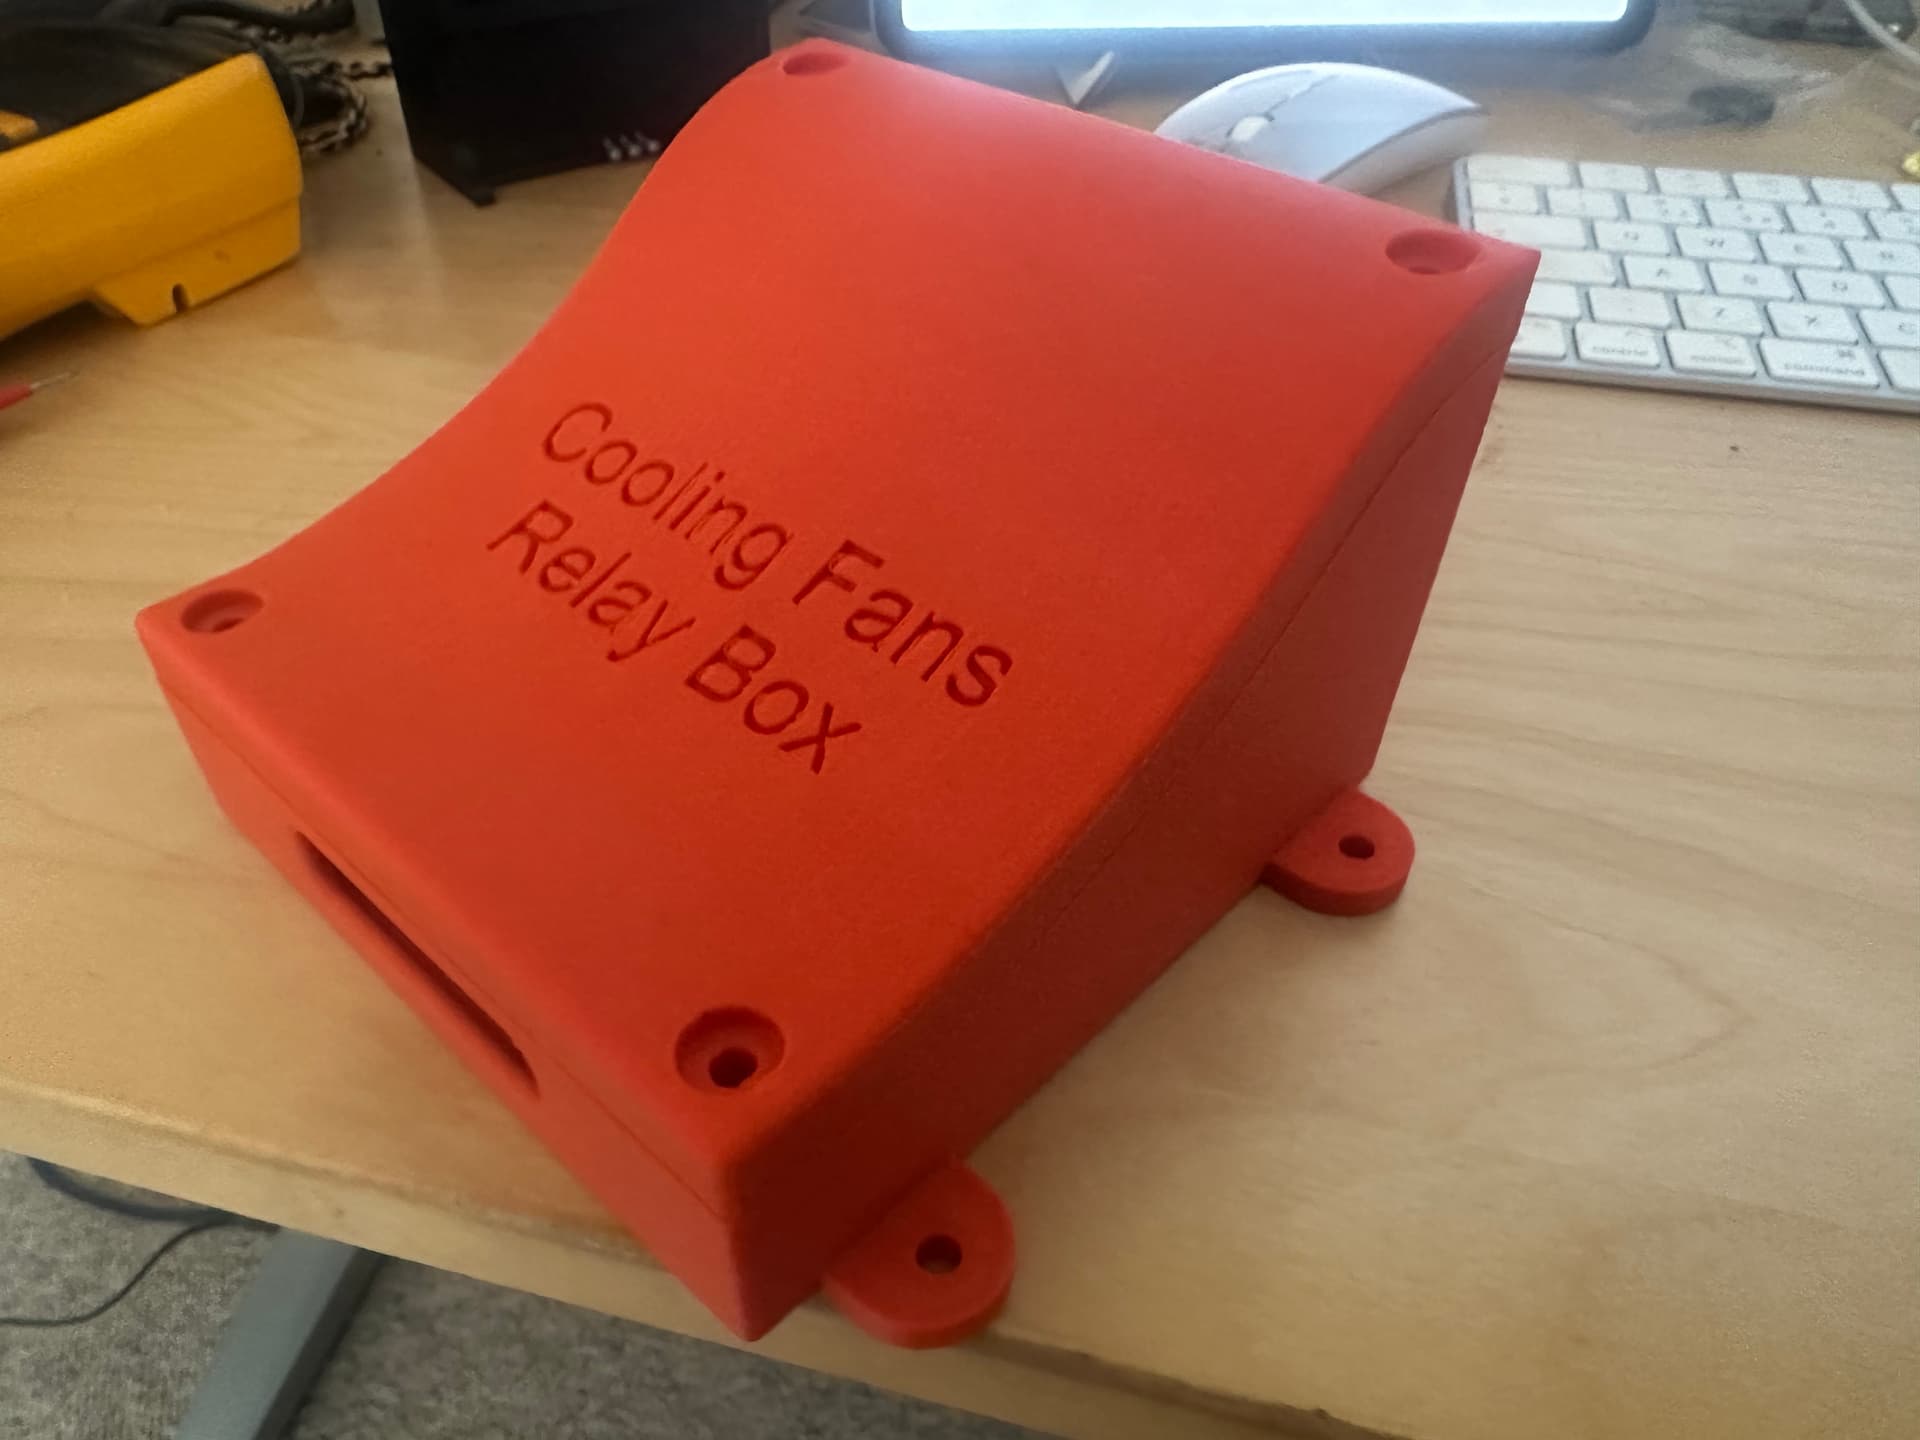
I’ll give these a go. I’m in the middle of a print right now and seeing some significant warping with Nozzle 265, Cabinate 60 and bed 100 (default profile from Bambu). This is on a textured PEI with glue stick. I’ll also switch to the smooth PEI and the liquid glue. Unfortunately I printed the lid of the box and the base in different Z orientation and I can already see they are not going to fit together…

Just to add to the comments above. PA6-CF doesn’t warp. Unfortunately the carbon fibre makes it conductive. The box I’m printing hold a PCB and I didn’t want any risks of shorts if a wire comes loose. Hence giving the -GF a go. If these settings don’t work I’ll probably go with a -CF box.

What helped a bit in my case was, increase chamber temp as much as possible. I’ve placed a heating bottle underneath the bed and covered the printer in a blanket. And slowed down print speed by setting max flow to 5-8. So that layers cool down as slow as possible. But honestly speaking it’s not fun to print the material, I would switch to the CF material nowadays.

Small parts, with small surface on the bed was much easier.

Personally I printed few Vento boxes for my friends and colleagues with PA6-GF from Polymaker and only combo which did worked for me was Bambu Smooth high temp plate + gluestick from Bambu as well. Granted it has to be re-applied at every print, otherwise I printed it on Bambu PA-GF profile and it all vent well. Worked same across my P1S, P2S and X1C. I actually love this material, the surface is so nice.

@Pera72 you settings worked great. My second attempt at my box came out without any warping. It’s not massive at 130 x 130 x 80 but very pleased to be able to get the two halves to fit perfectly. There is an interlocking rim to keep water out so the fit needs to be precise. The first attempt had enough warping that the lid wouldn’t fit the base.