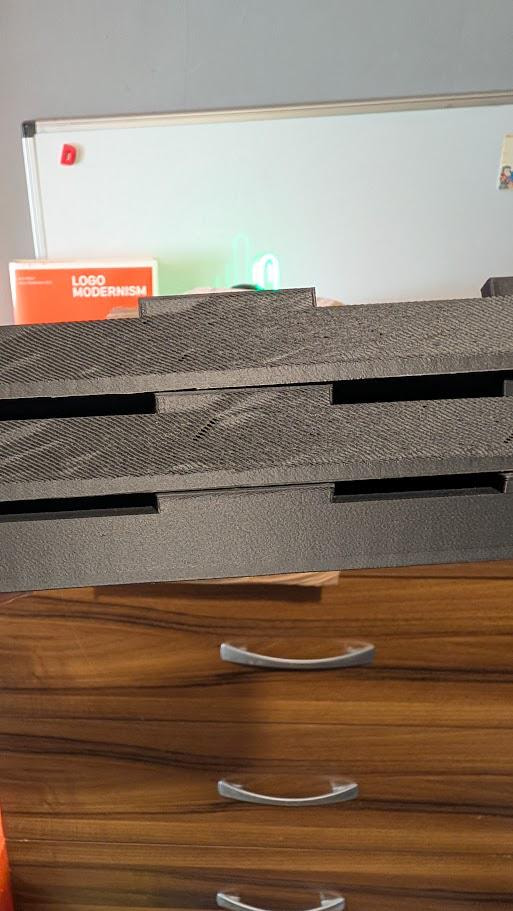
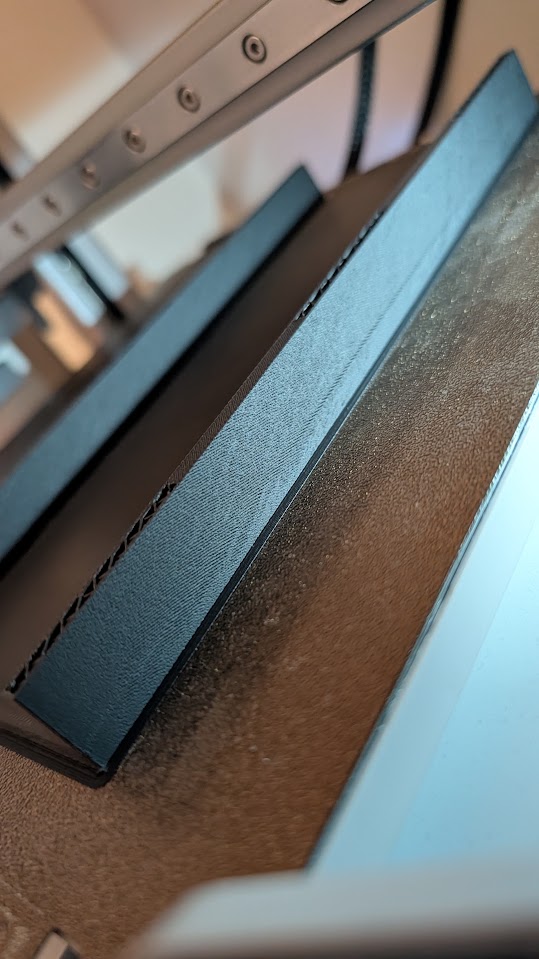
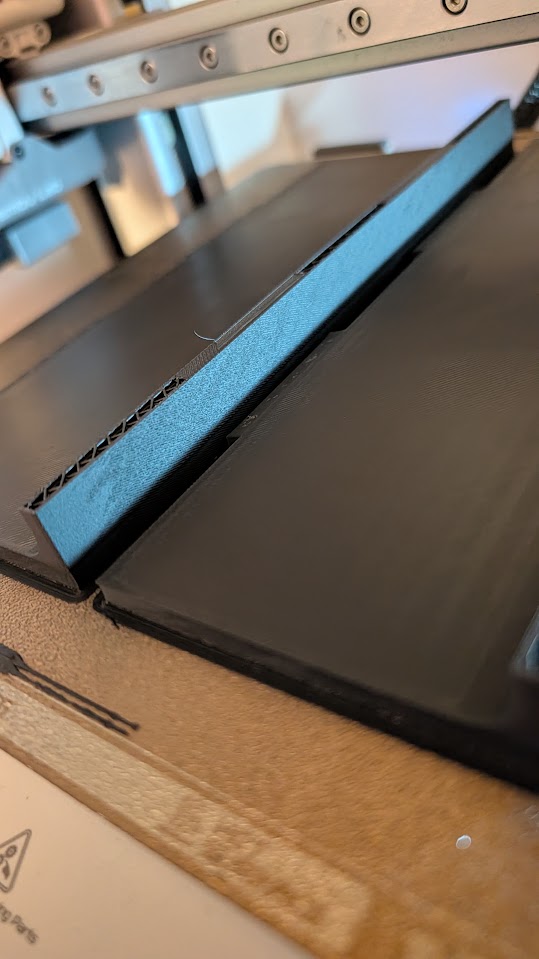
I’ve been getting some weird results on the below file, the straight back wall on both parts comes out with this weird shifting and not smooth. (Better print on the bottom vs top 2)
Using an A1 with Black PLA Matte. This is happening on two different machines, which leads me to believe it’s a settings issue, not a hardware issue.
Thank you for the suggestion.
This is happening on two different machines, which leads me to believe it’s a settings issue, not a hardware issue, however I did already tighten the 4 screws on the back and the three mounting screws are well tightened.
Are you printing with lower than .2MM layer heights?
In my experience, this is a phenomena that occurs at lower layer heights.
My research led me to pressure advance/flow dynamics issues at lower layer heights. It seems some improvement can be made by slightly increasing outer wall width from standard 0.42 or slowing down outer wall speeds but it sounds like this has not helped in your case
Nothing really stands out settings wise from your 3mf file, imo.
A1 can definitively print 0.08mm PLAs.
The defects on your photos clearly show extrusion problems, that is, the printhead struggles to maintain a smooth extrusion at targeted flow. I’ve seen this before on trickier filaments, and A1 can be more susceptible due to weaker extruder motors, but never on regular PLAs. The cause can be multiple things.
The other thing I can think of, have you checked wears or gunks on the (metal) extruder gear? Just remove the cutter’s screw and the gear can be observed from the opening without disassembly. Or anything between the filament and the nozzle that might be increasing drags. I can’t see it so, possible things like worn PTFE, worn/debris in connectors, etc.
Clarifying here, The stock settings from bambu are very fast, so did you actually try a slow run? A simple first test is to just run it again and choose the “silent mode” (reduces speeds and accels by 50% roughly) and if that helps, then save those lower speeds in your slicer profile.