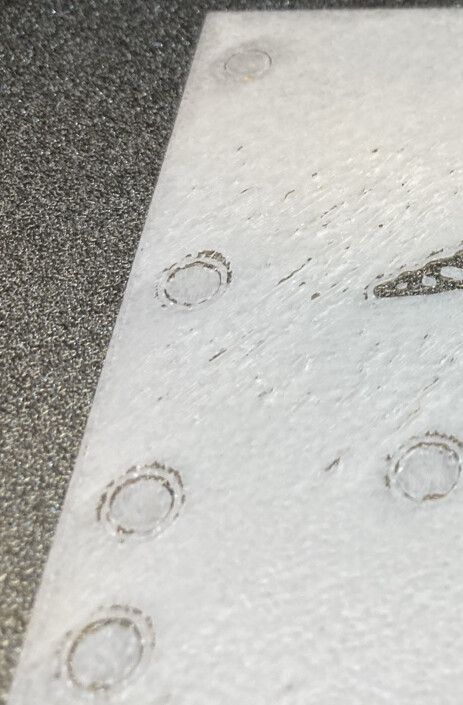
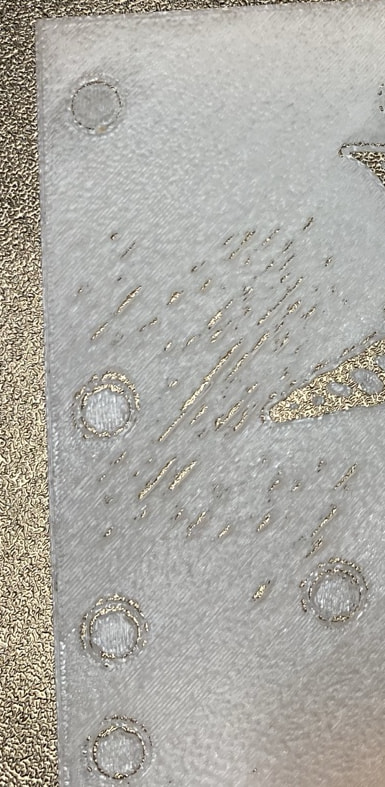
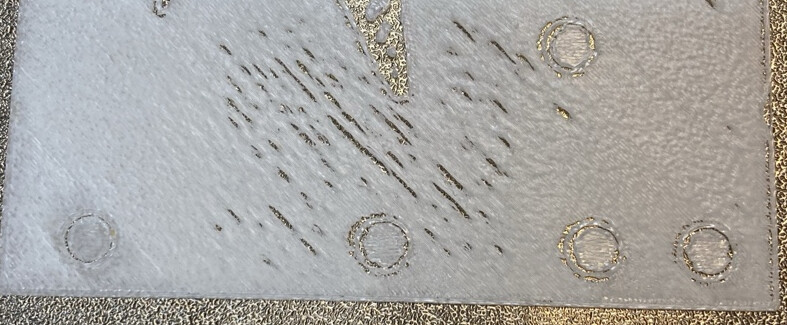
This isn’t that uncommon. Some see it on a single piece where the print quality changes across the piece and it is repeatable for them too.
What to do about it is more out of my experience but what I’ve seen mentioned is fans running that maybe shouldn’t (or maybe not running that maybe should), air currents with the chamber door open and maybe a fan nearby, or some other aspect that causes a different print environment - even fairly subtle differences across the print or build plate.
Hopefully others that know this aspect better can chime in. I think @JonRaymond and others may be familiar and hopefully not putting Jon in a hot seat.
But there may be another contribution at play here but like I said before I’m not familiar with ABS. In checking Bambu’s ABS filament page they caution specifically to use enclosed printers though I couldn’t tell you why. They mention drying but don’t emphasize it like they do with PETG.
At least with other filament types, I’ve done a fair bit of experimenting with drying and moisture issues and those seem to fade in as moisture levels rise. It could be, but I’m not saying it is, that you have just enough water in your filament that it’s starting to misbehave. You can tune out some moisture effects so it stands to reason you might be near a transition and the microclimates across your build plate are doing some tuning for you.
I know it’s hand-wavy and it could be wrong. I know you said you dried your filament too but there were no details. Thing is many standard filament dryers are less than ideal for really drying filament well. I’d be curious what your drying procedure is and if you do any checks to know your drying was effective?
I use a standard single-bay dryer that is really well built IMO but non-ideal at drying filament. Unfortunately this is not uncommon. The water doesn’t have a good way to leave so essentially stock you’re giving filament a sauna which is not a good way to dry it. On MakerWorld people have created door props for a number of dryers to fix that sauna issue and they really help. During the first half of my drys, I prop the lid to my dryer open about 3/4 inches. That lets the heat drive off water while letting the water out. It gets significantly more water out than drying with the lid closed.
But I don’t know this is the issue and unfortunately can’t advise at all on ABS. With PLA and PETG, if you put a spool of filament in a gallon ziplock bag with a hygrometer (no desiccant), after about a half hour the hygrometer will settle to a value. I don’t print PLA above 25% RH at room temperature and PETG above 20% because water effects for my setup start appearing. Typically my filament is much dryer than that - below 10% and I don’t see any water issues at all.
So for whatever all this is worth. Maybe someone else has other solutions?
“Update: WTF setting “initial layer” width to 0 seems to be the solution. But I think I tried it in the past and have got negative wall size for arachne wall generator.”
Wow. Not sure why that would fix it but good going! Seems an error to me but I don’t use arachne that much to really say. Congrats!