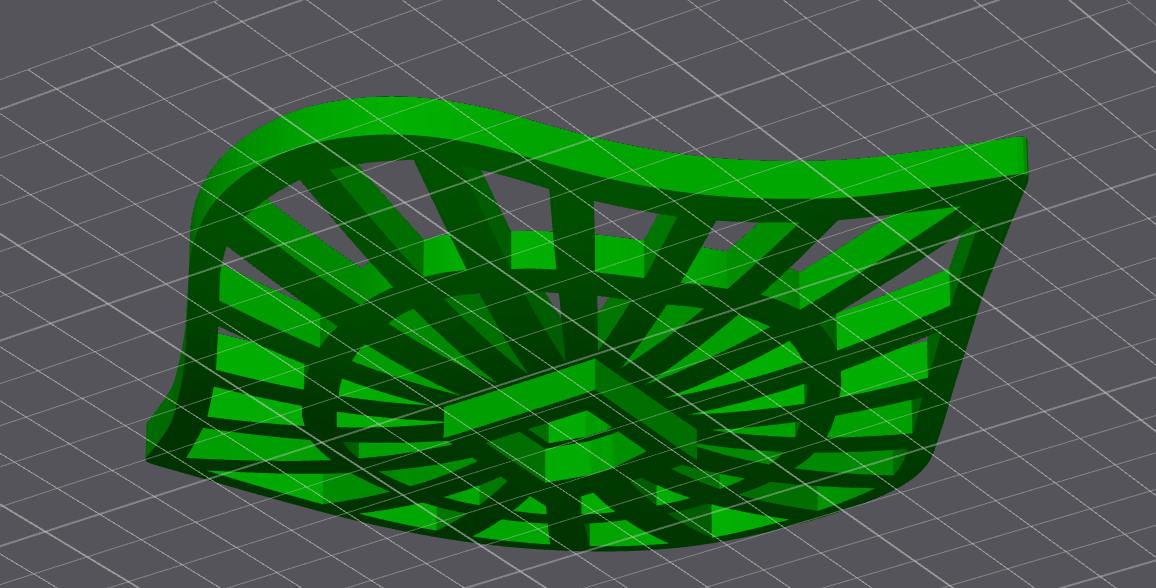
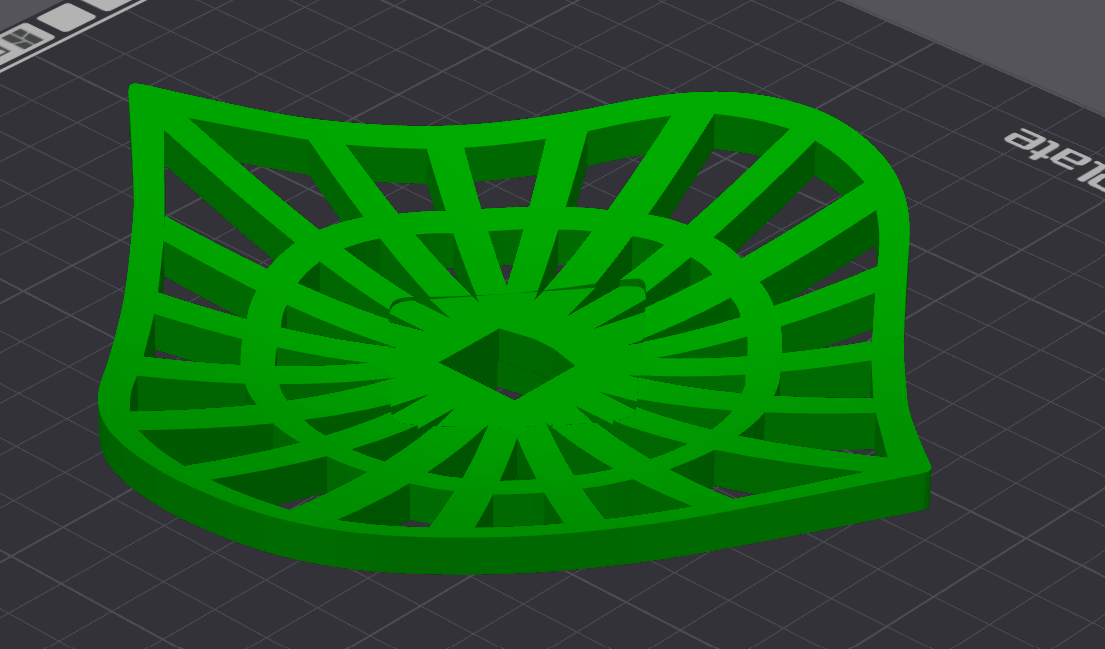
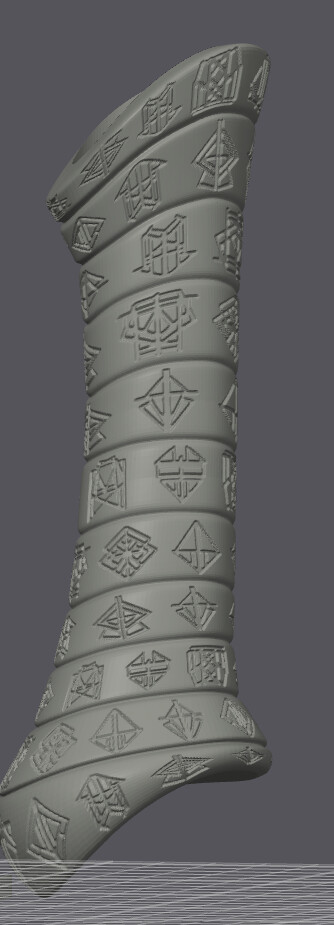
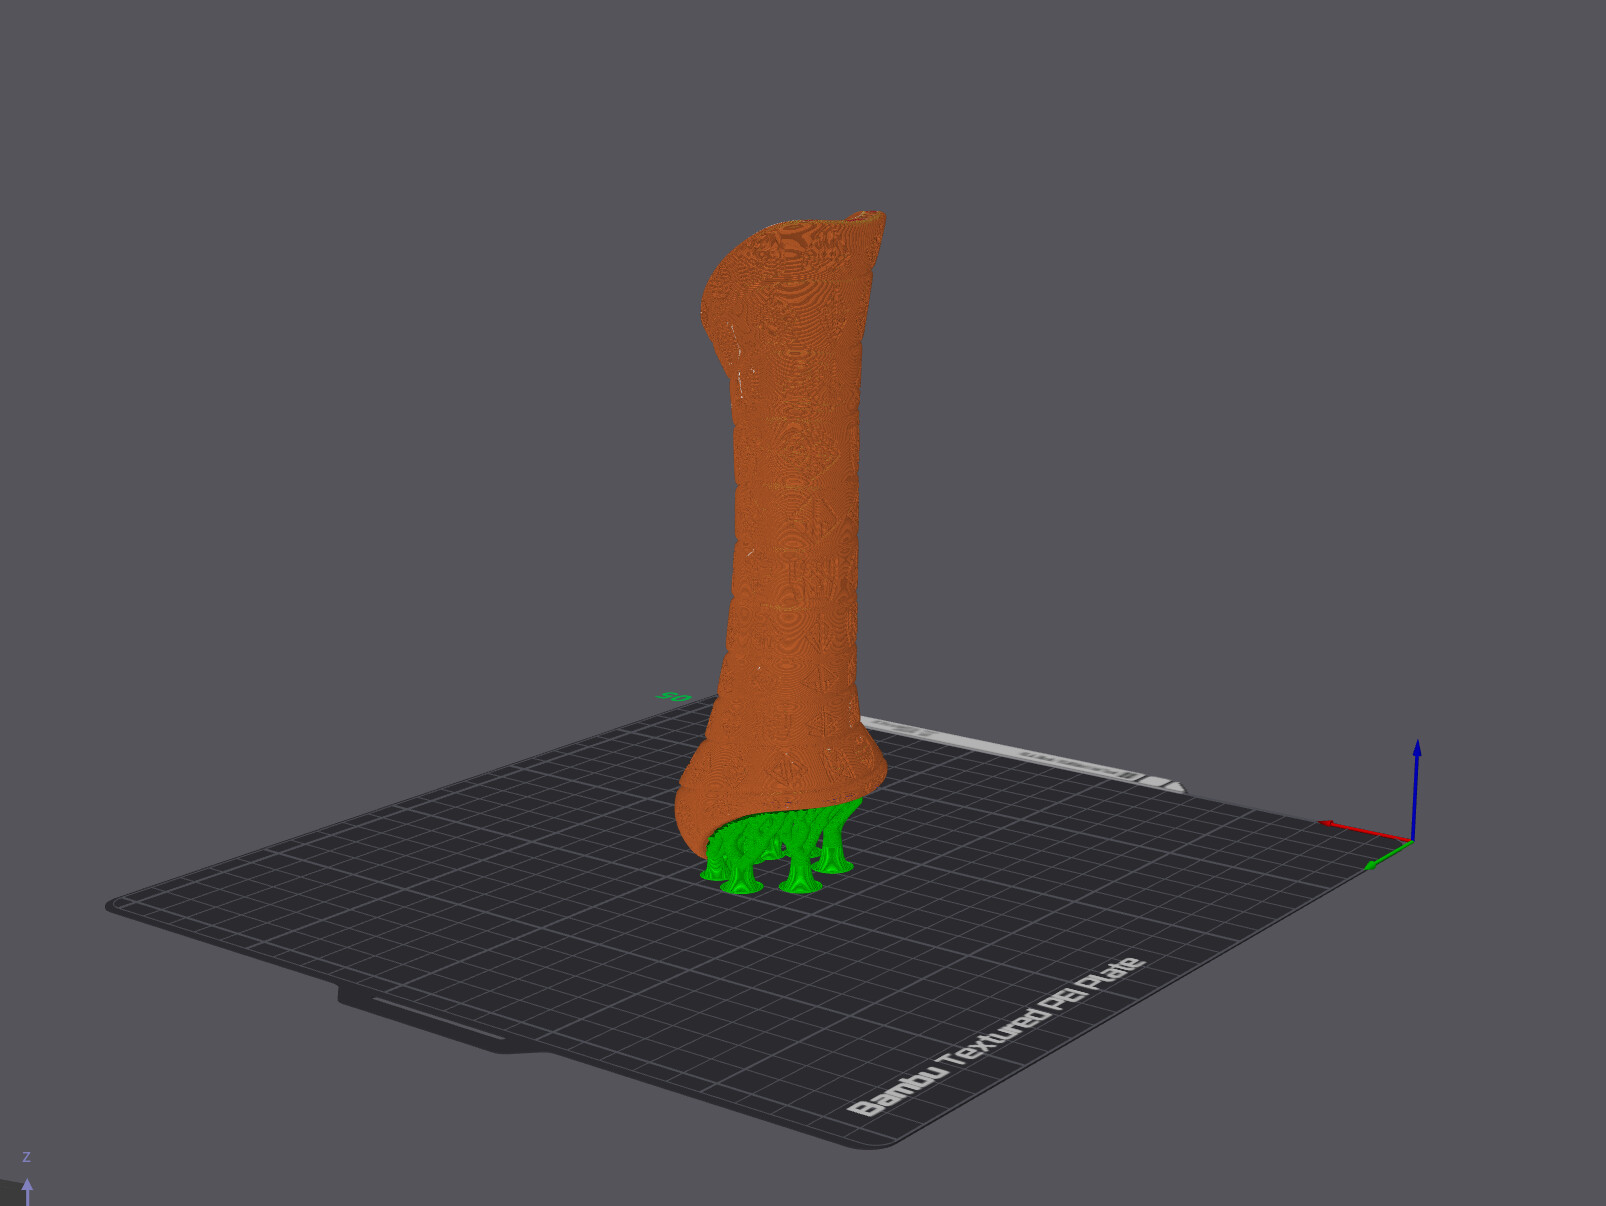
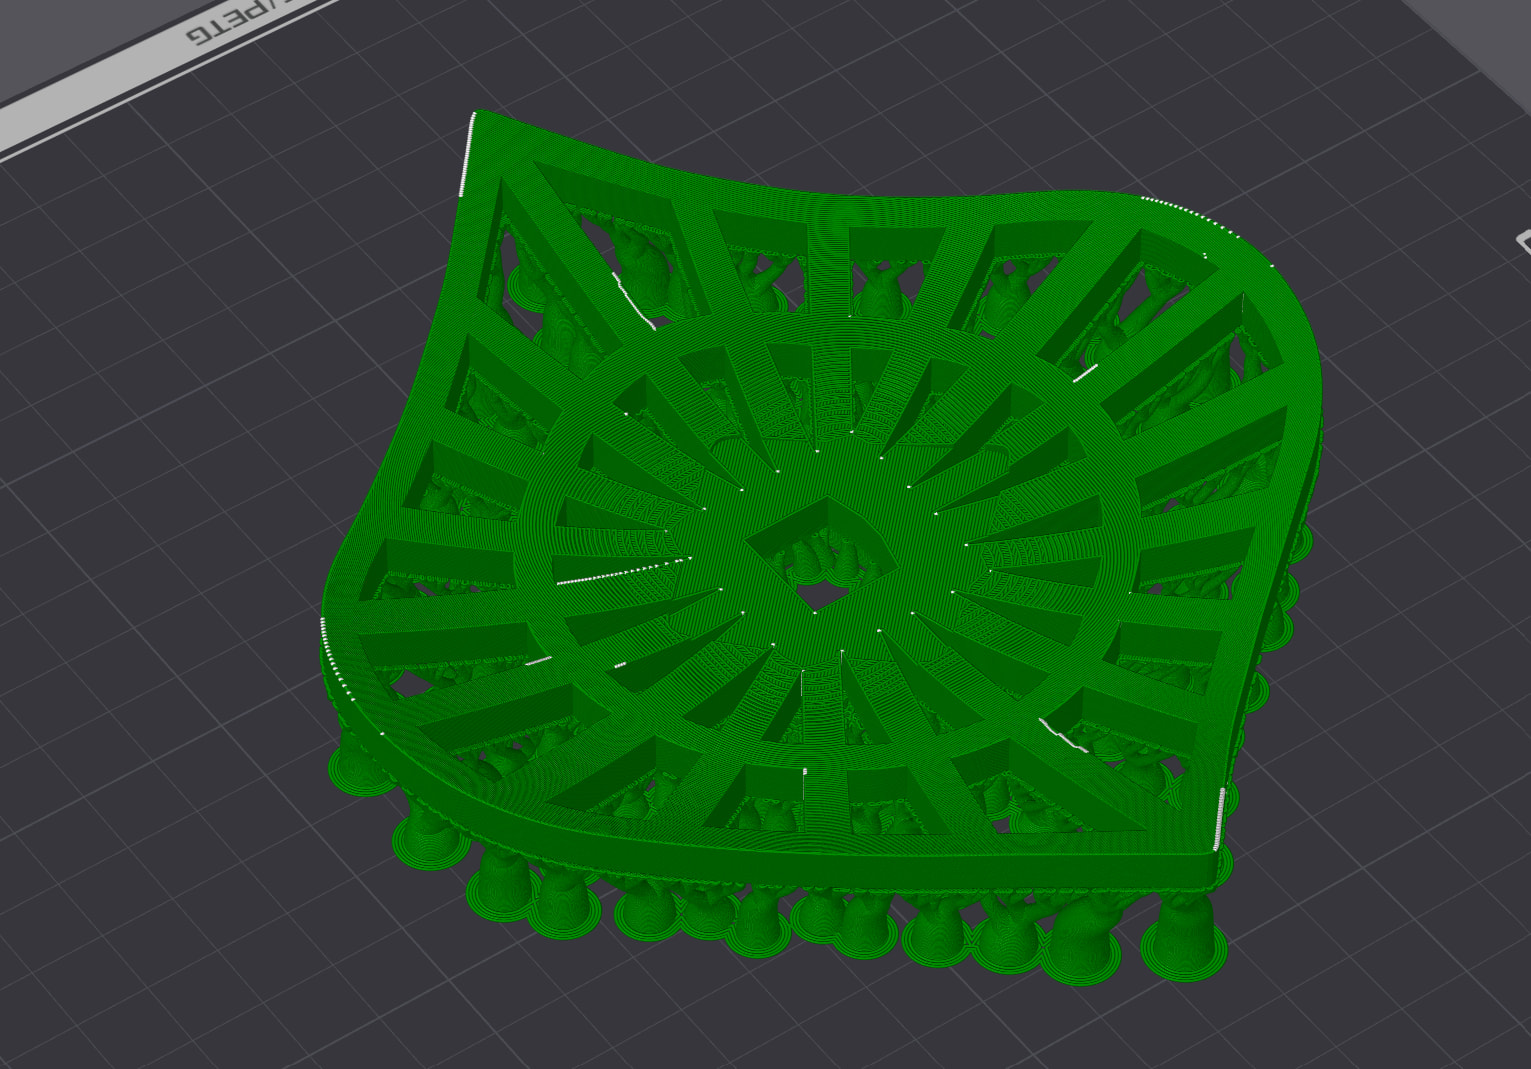
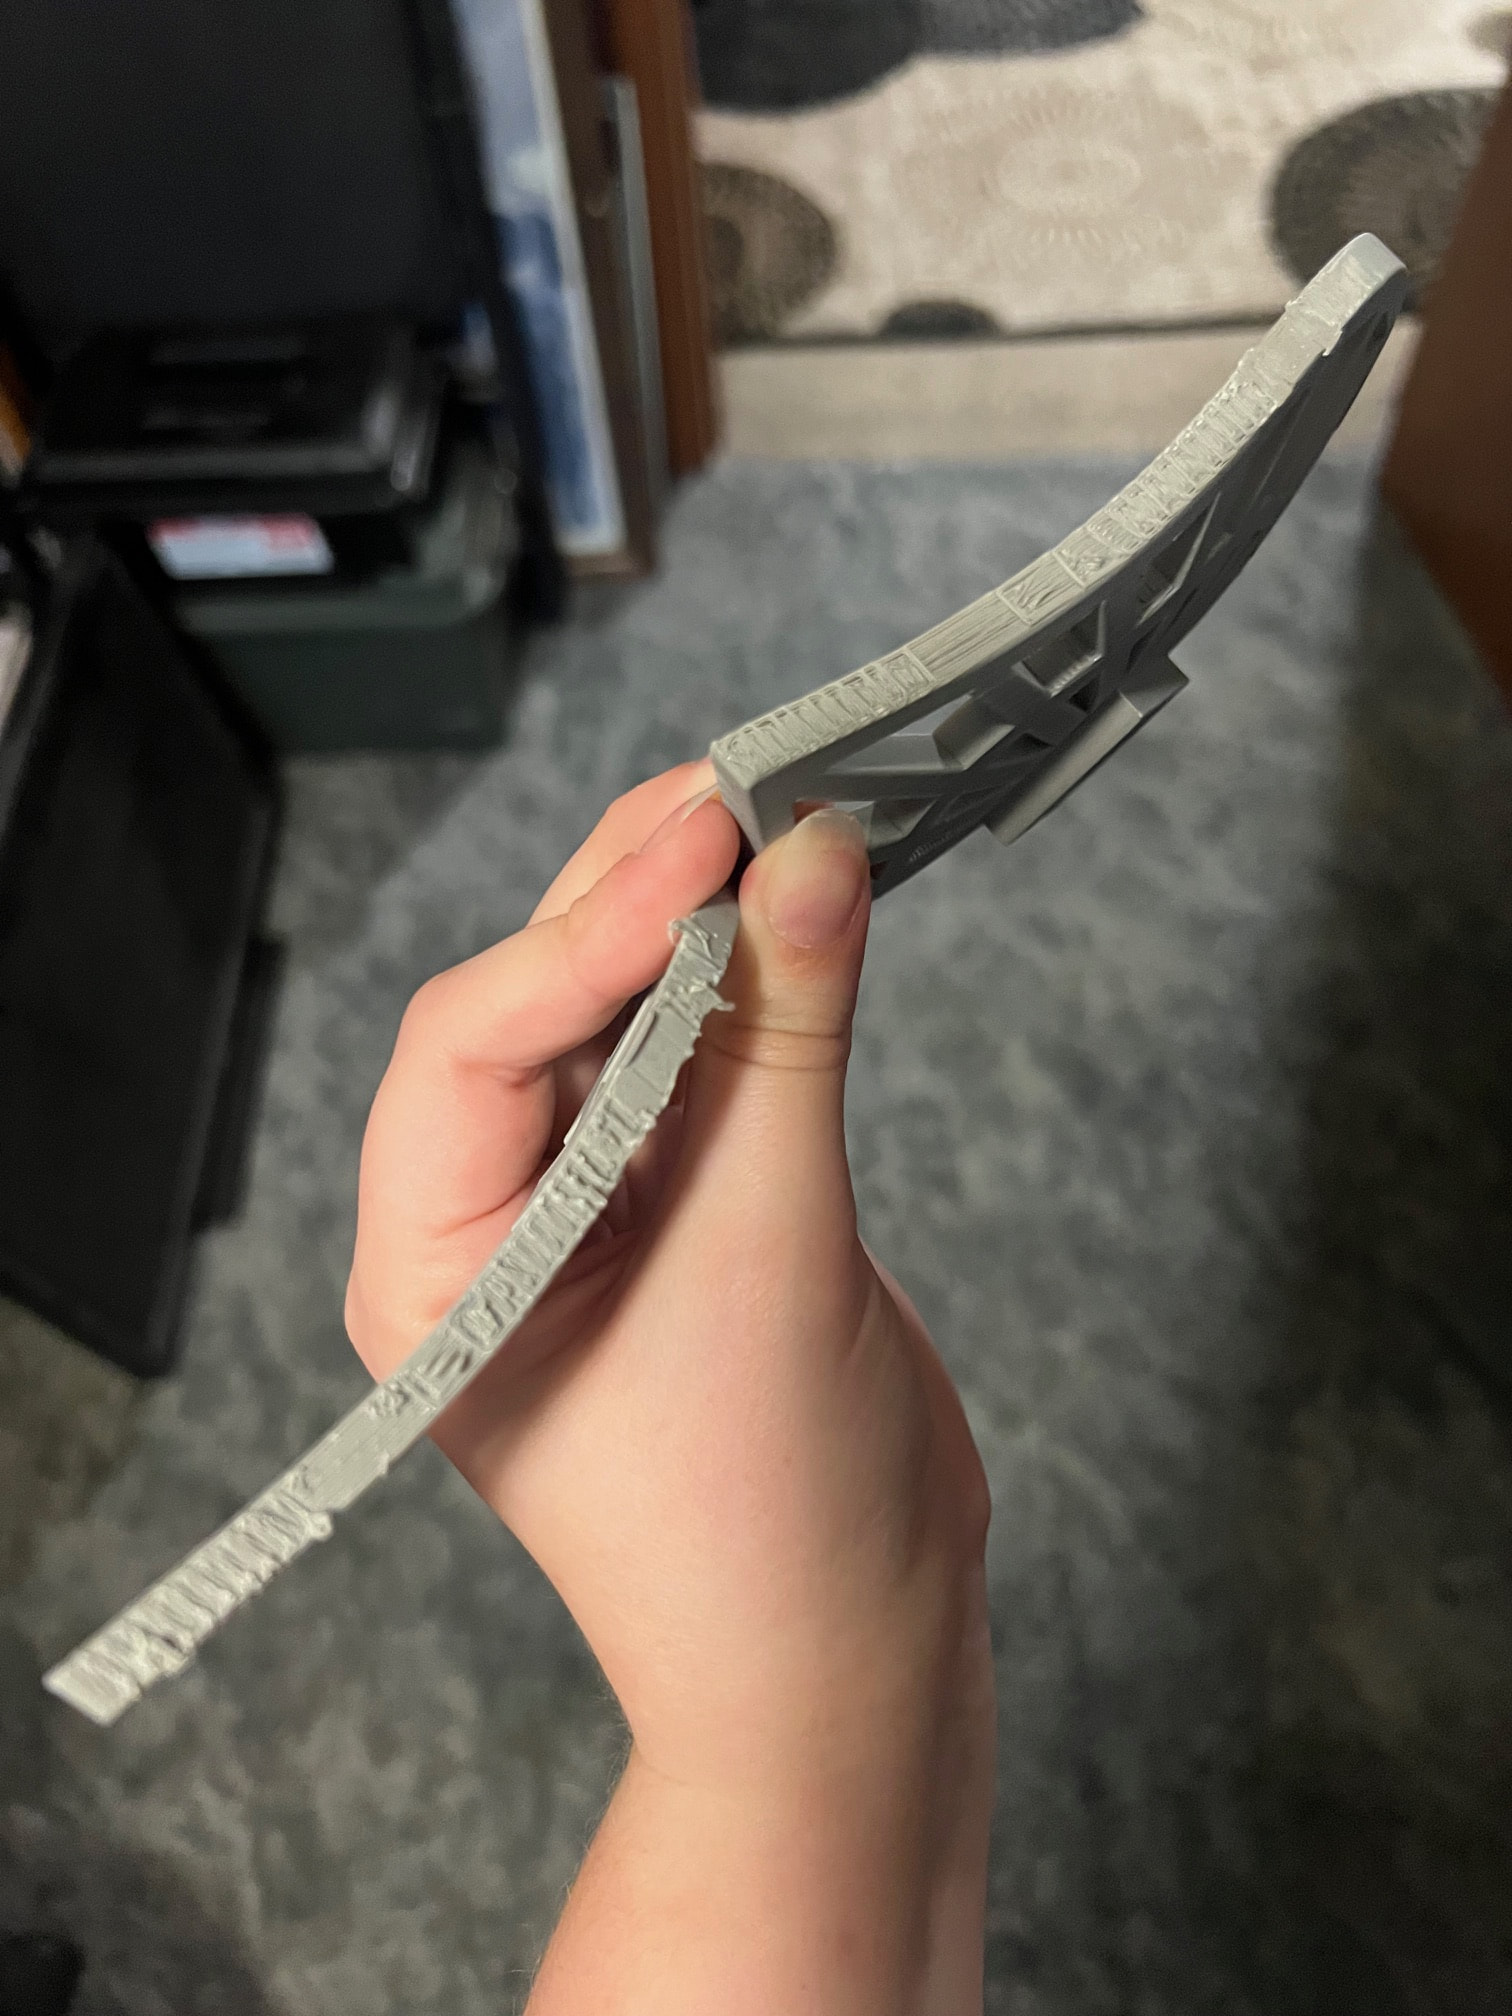
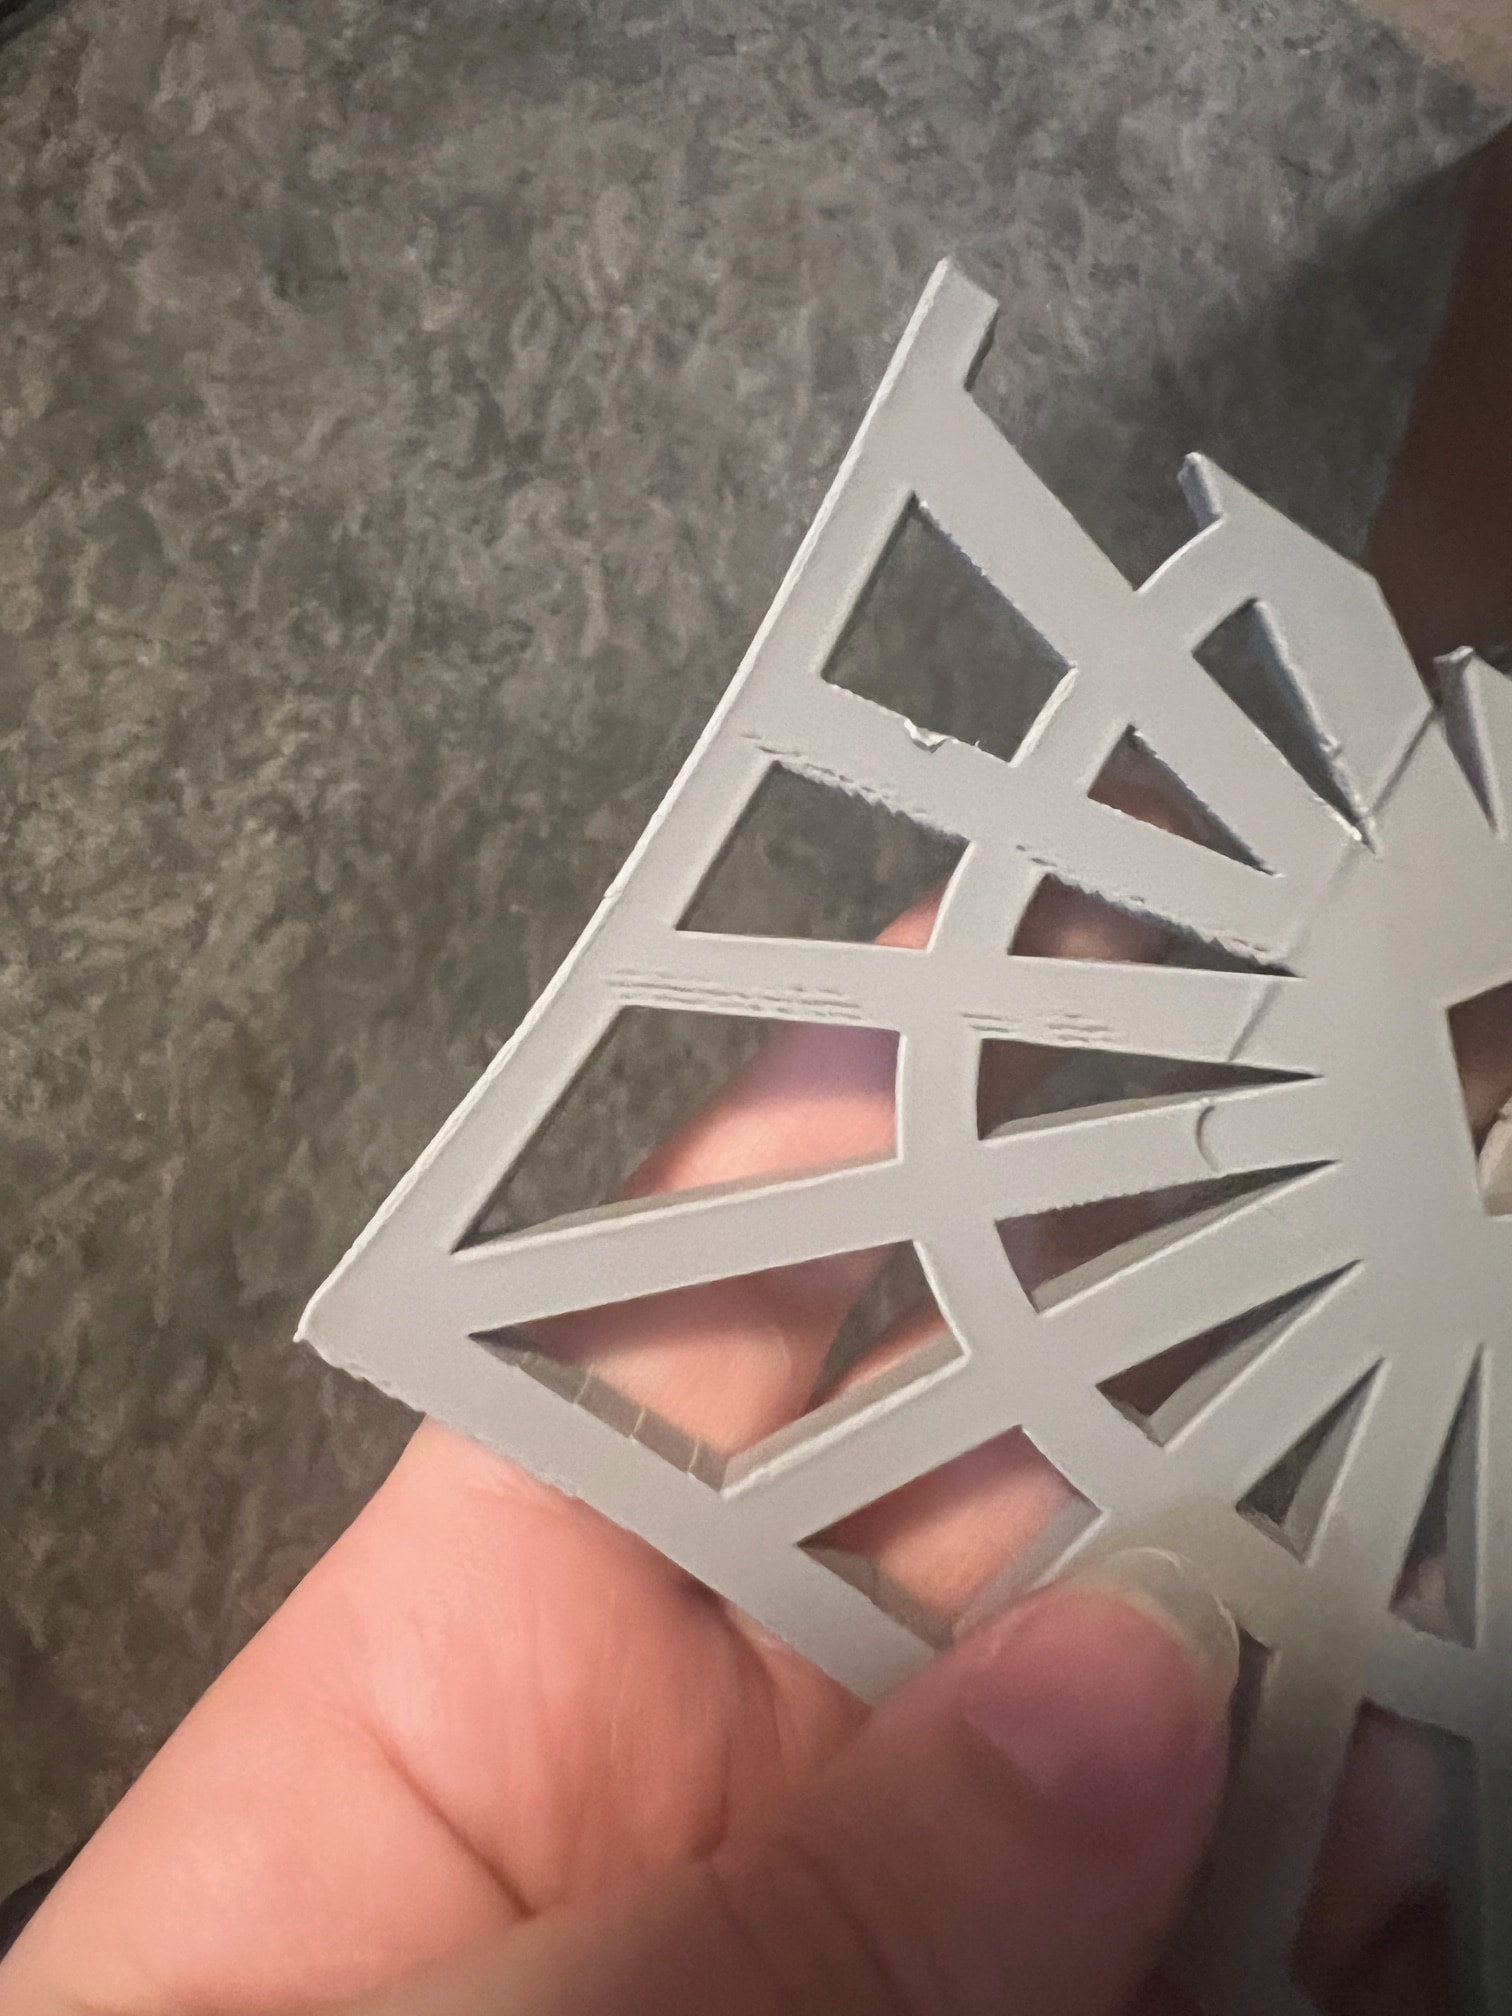
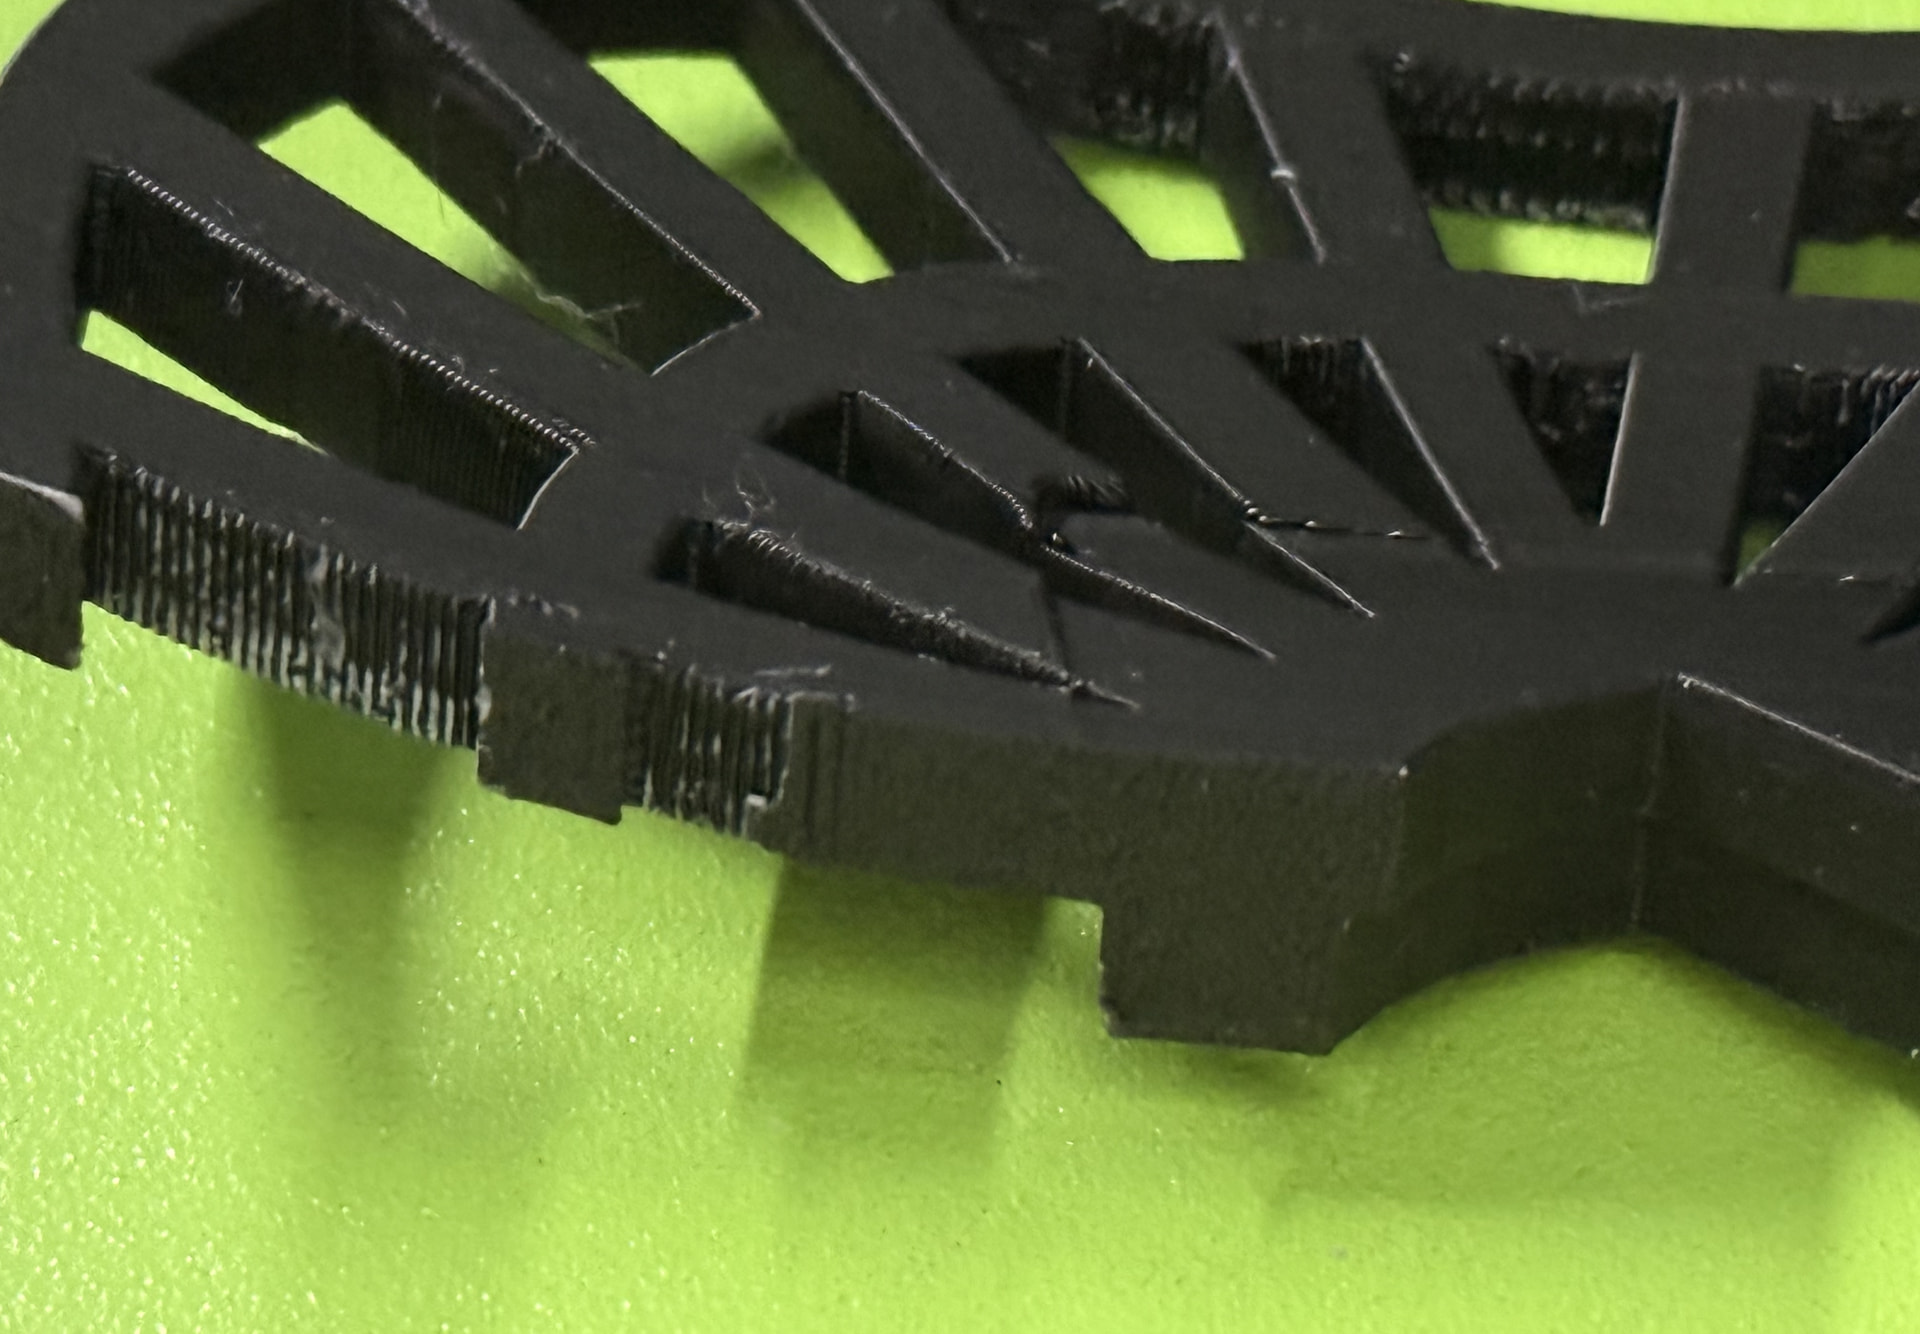
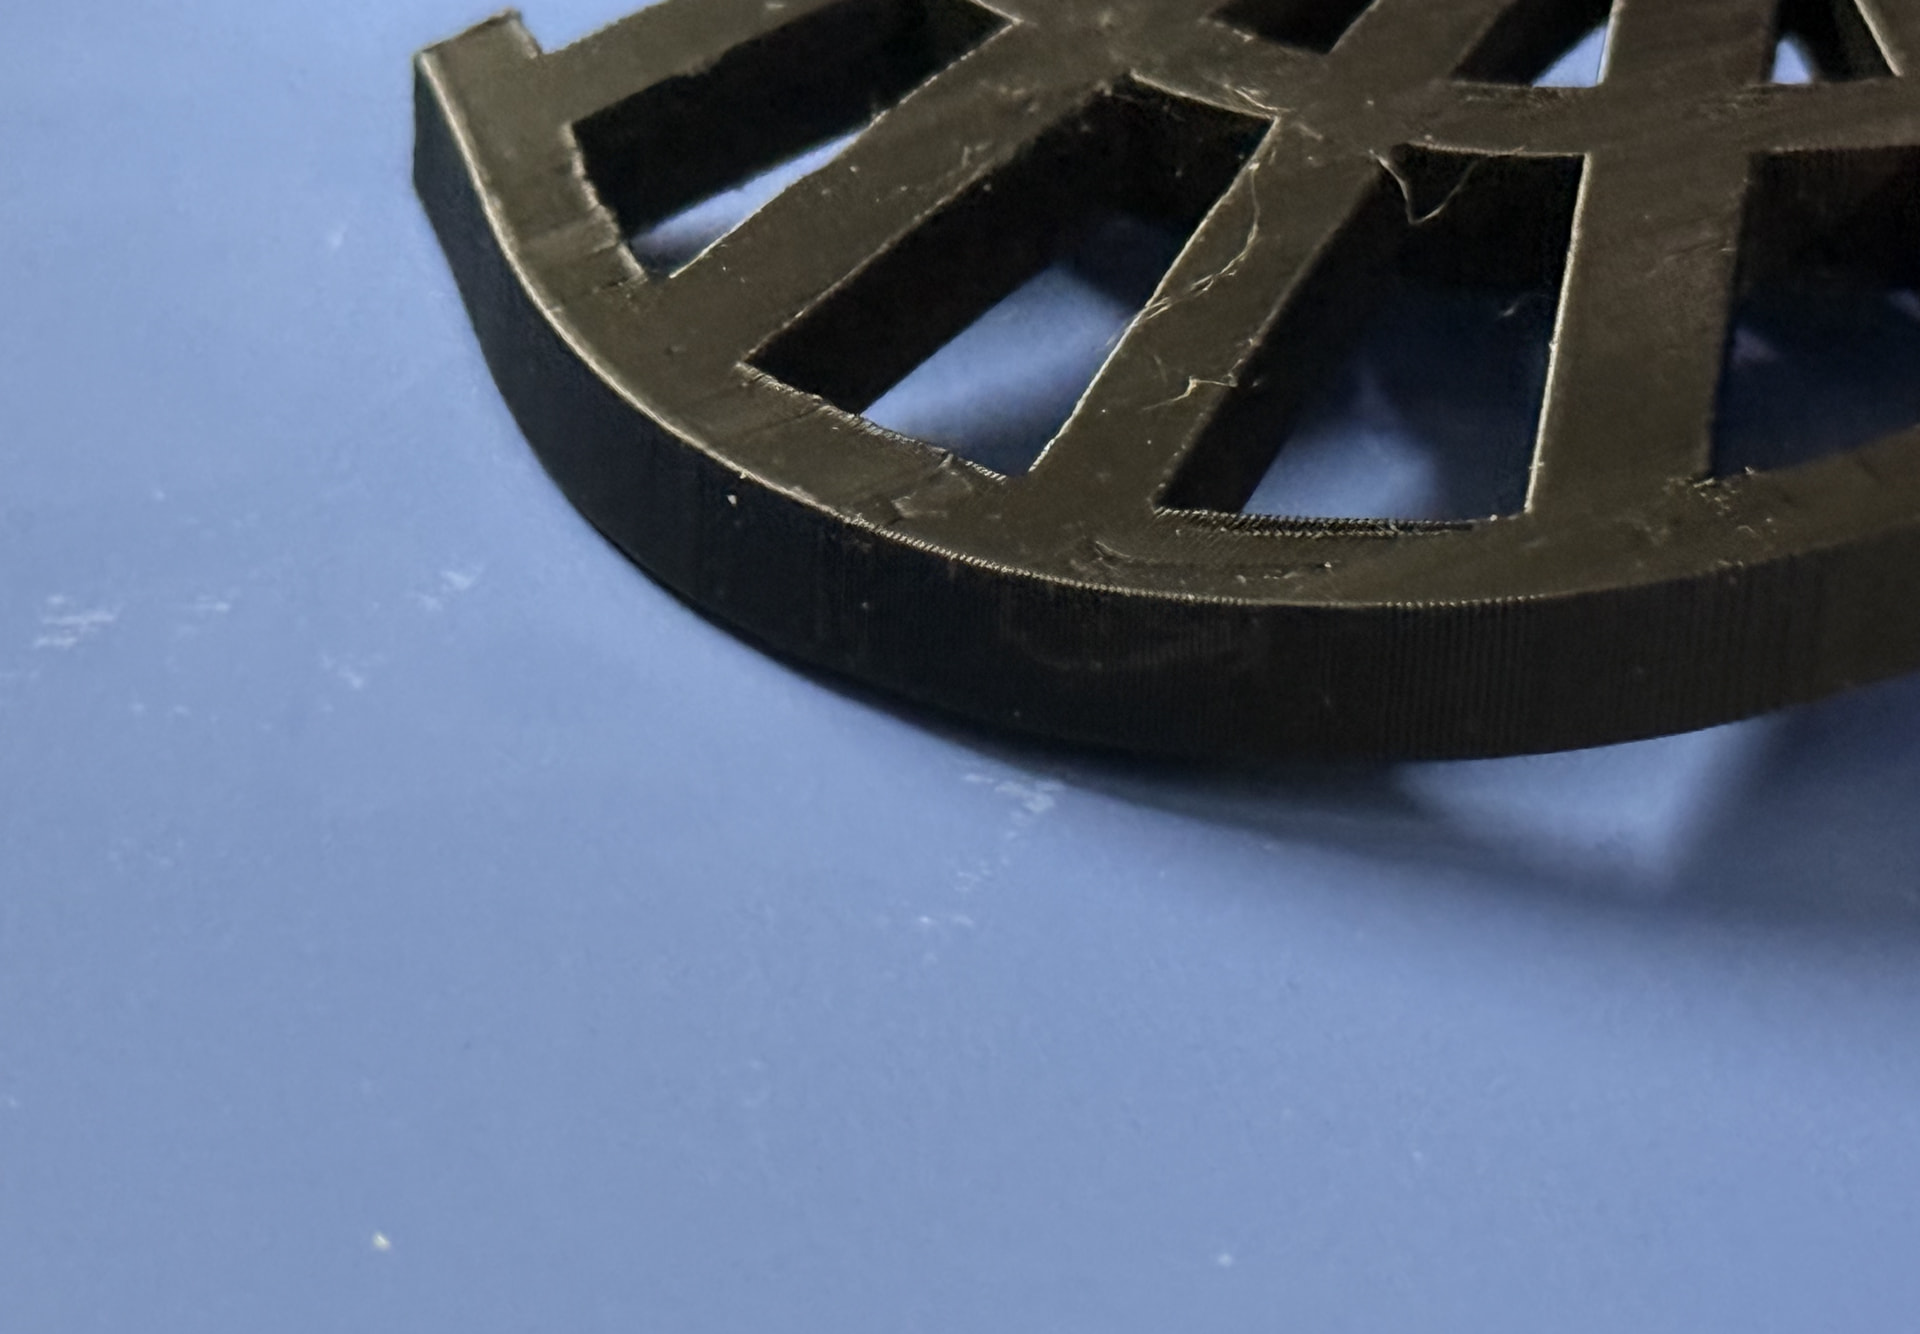
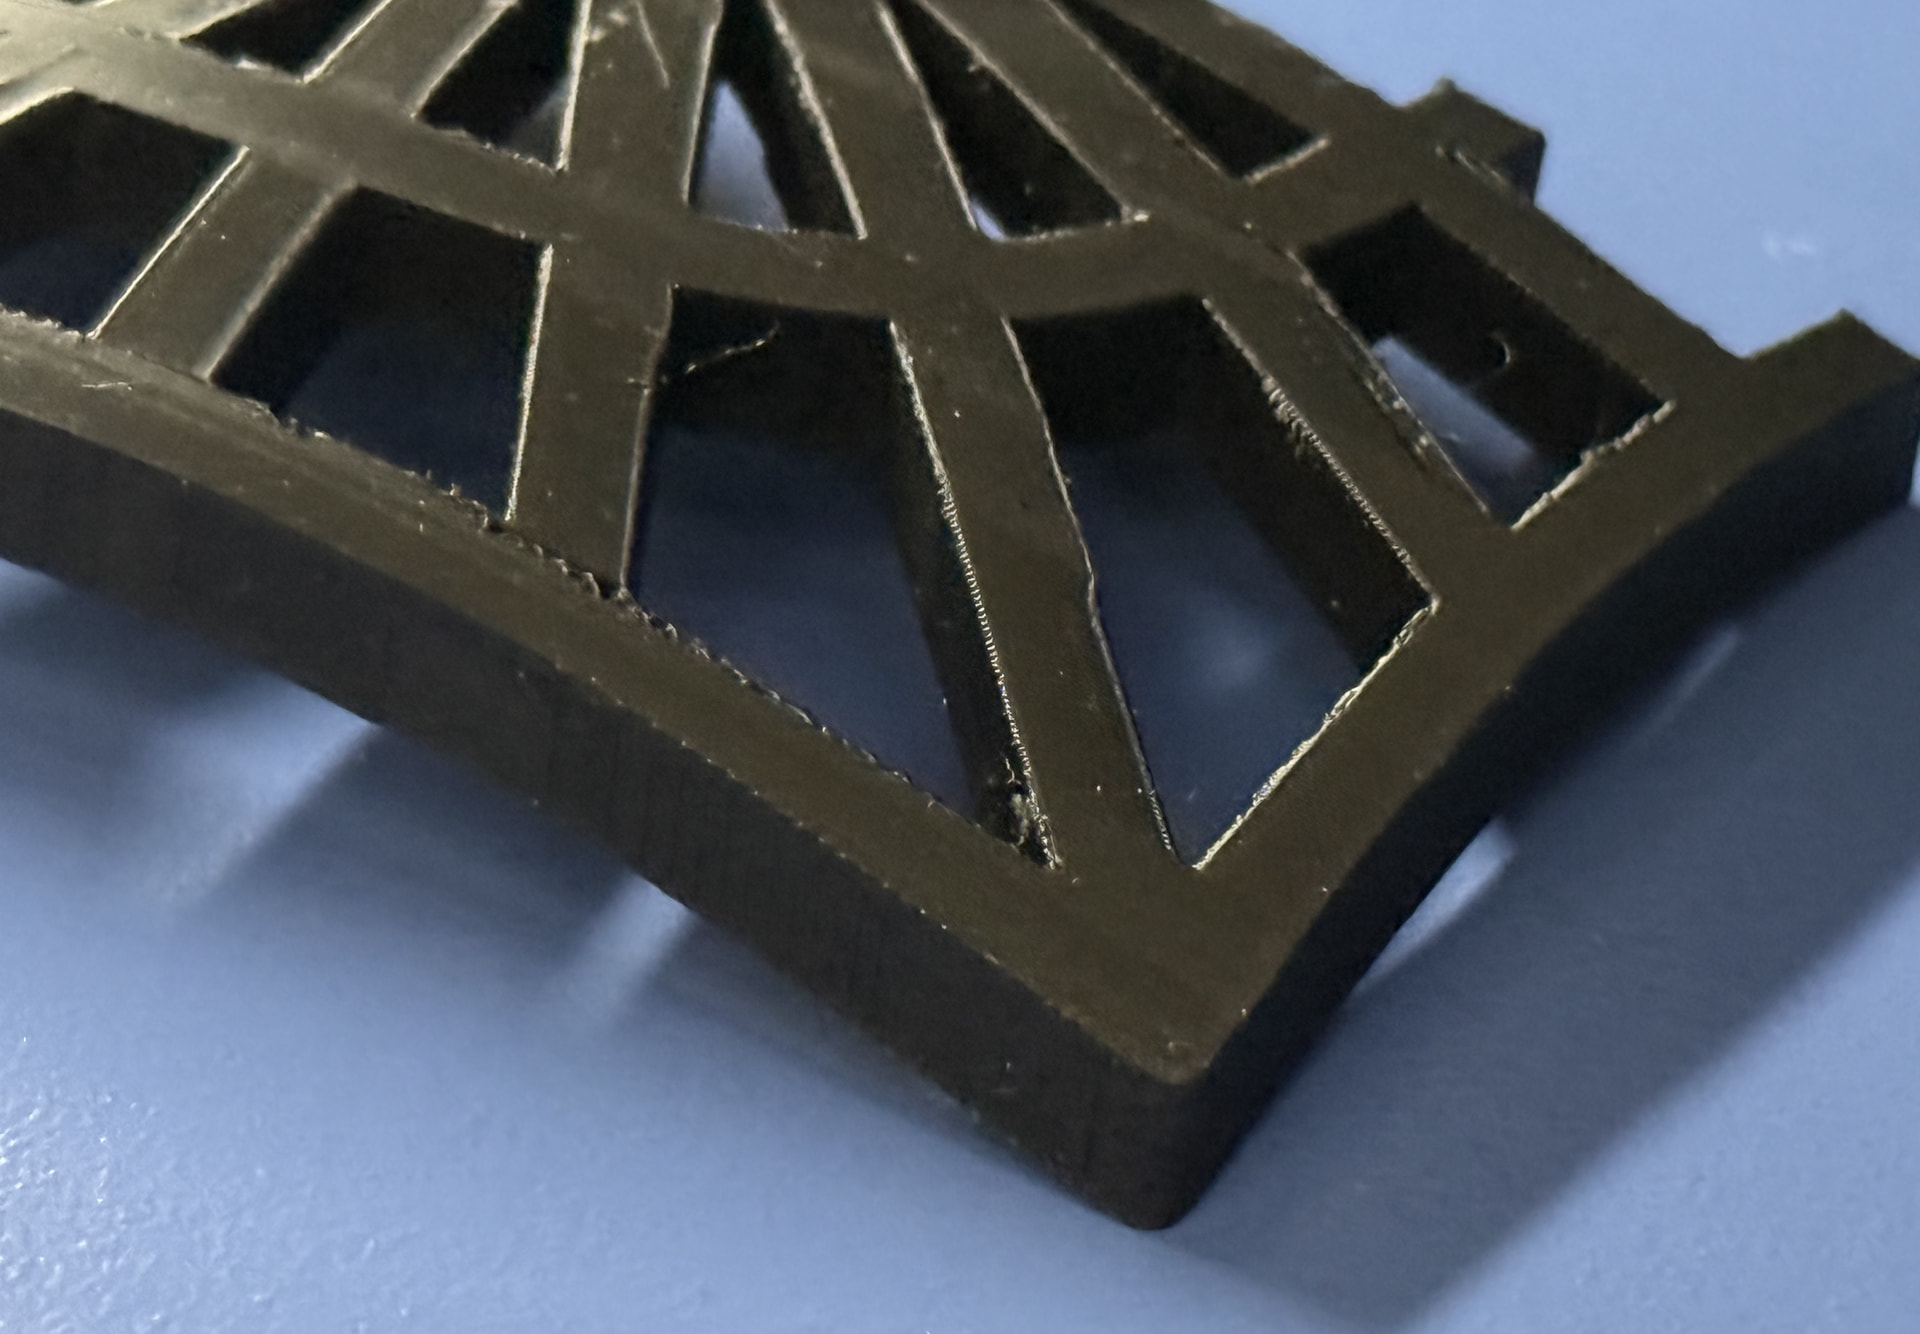
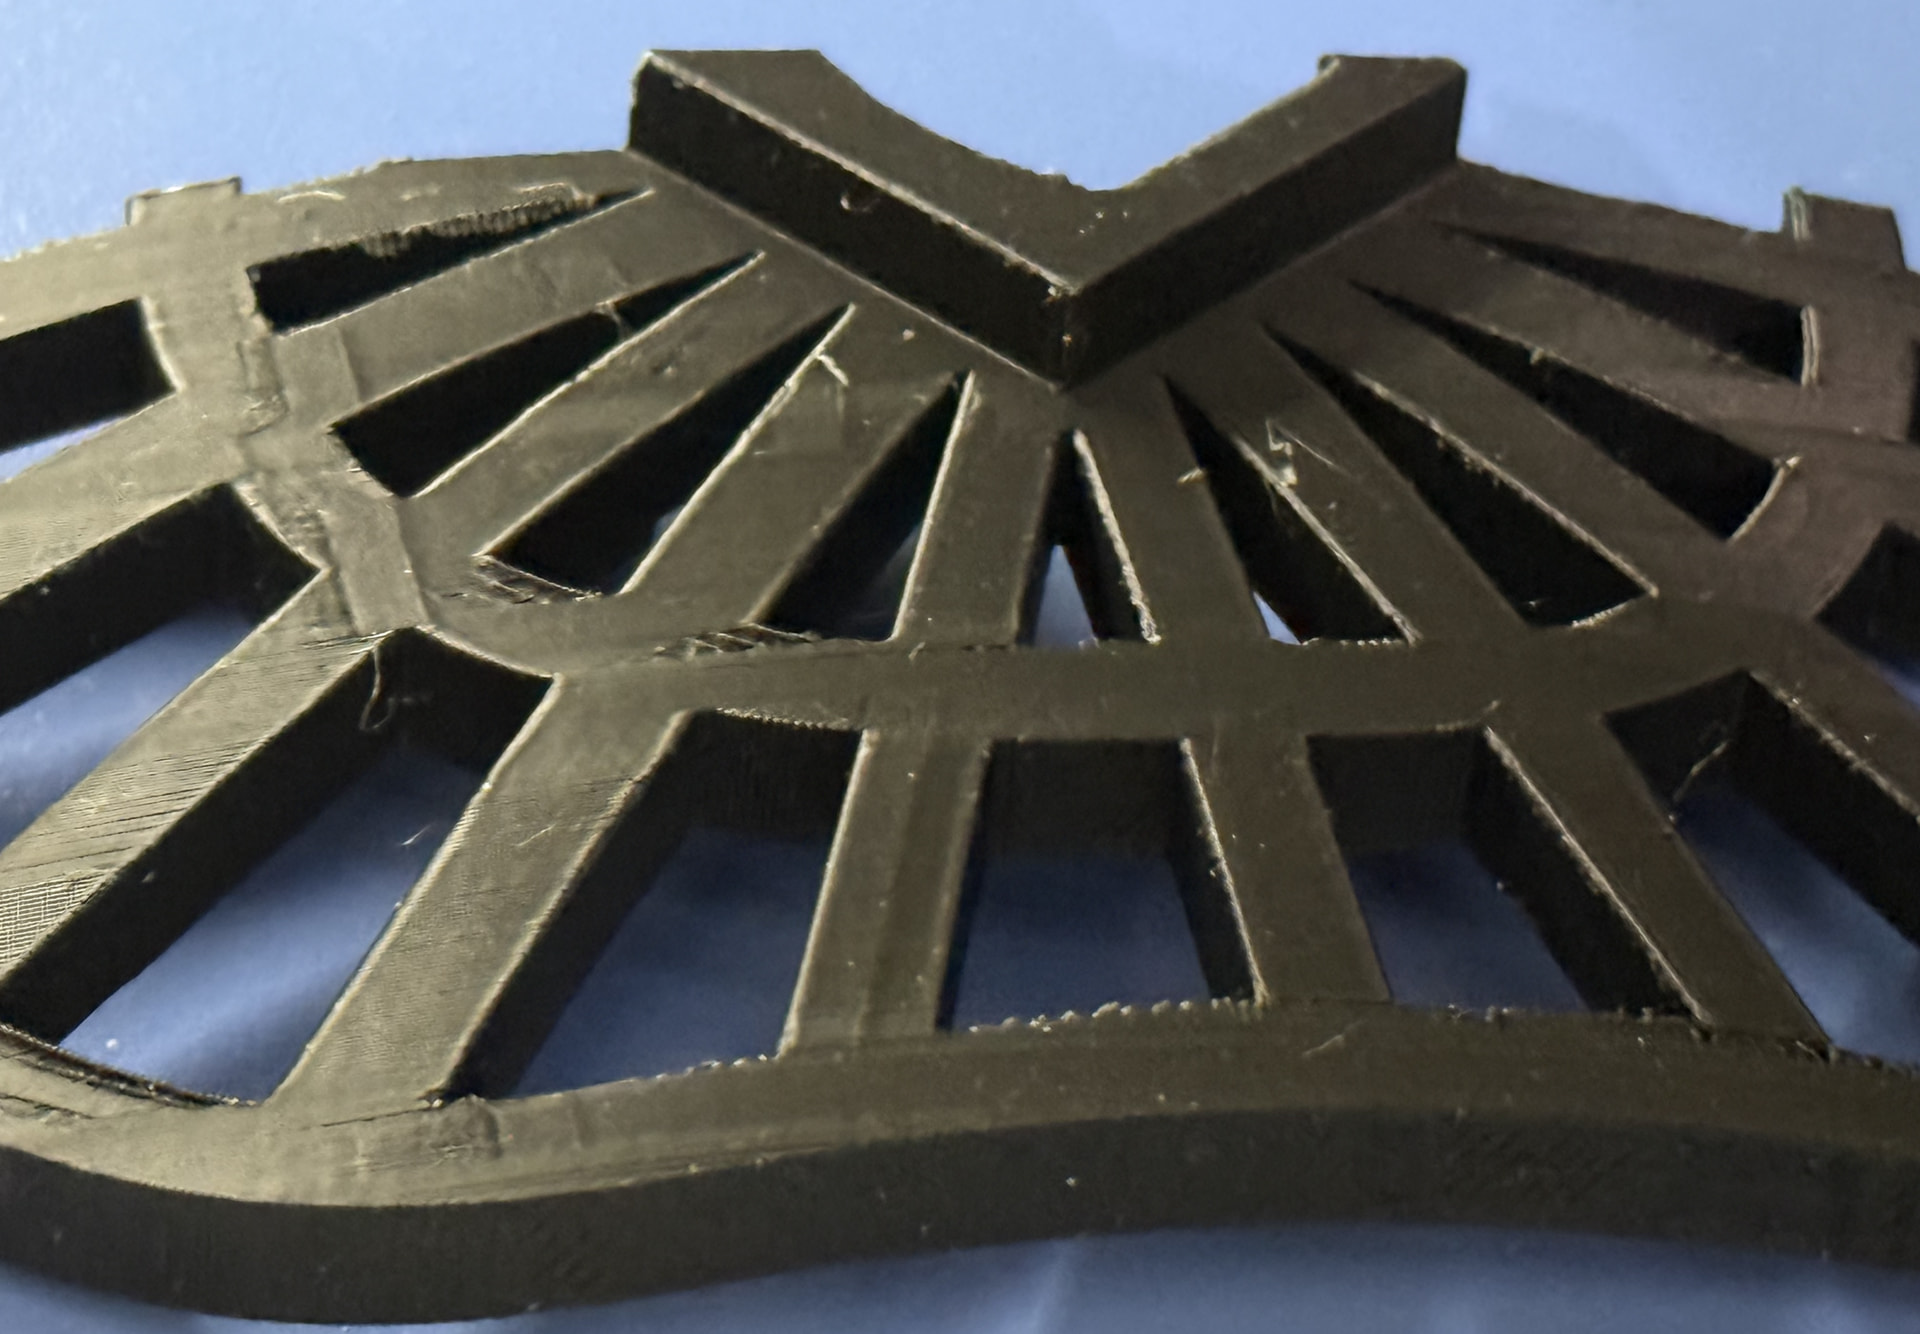
I’m new-ish to 3D printing and have a P2S which I struggl when it comes to supports. I have two big pieces that aren’t easy to layout on the plate with their organic shapes and outer details. I’ve tried printing the shorter guard piece a few times but get horrible underside scarring from the supports. I know my overhang test was great up until 55 or 60.
I’ve recently tried using PETG as support interfacing - worked great fro small flat pieces but not these curvy, organic shapes. I got weird under extrusions when using it even after switching back to just PLA. I’m at the point of just going back to PLA but nervous I’ll spend a lot of print time on these big pieces and end up with bad quality.
Any advice on orientating these objects and support settings to help print these with protecting the deatils and minimal scarring on the outside?
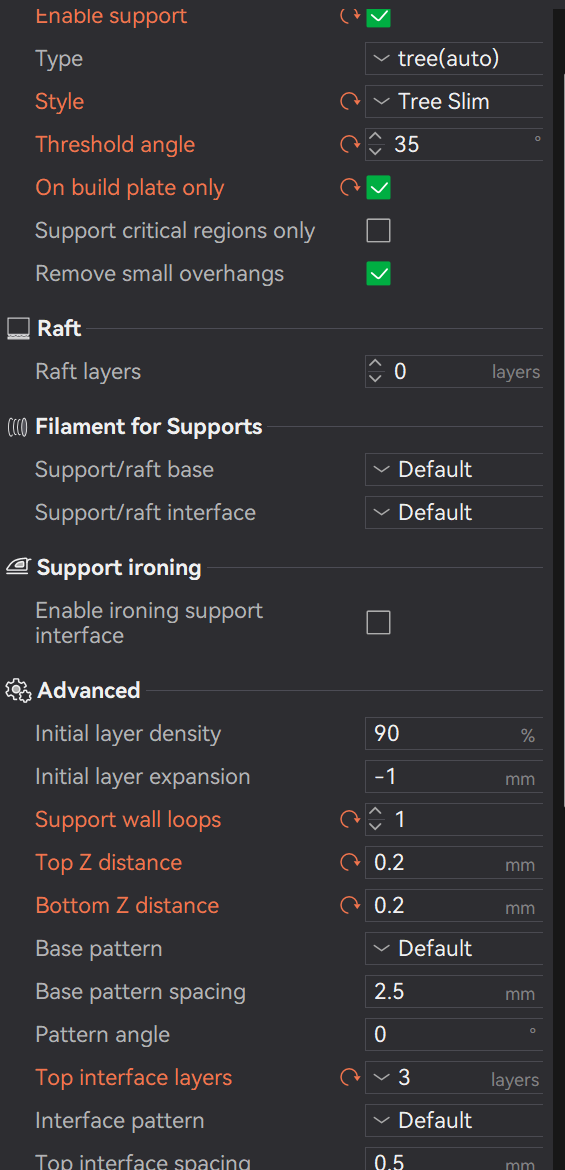
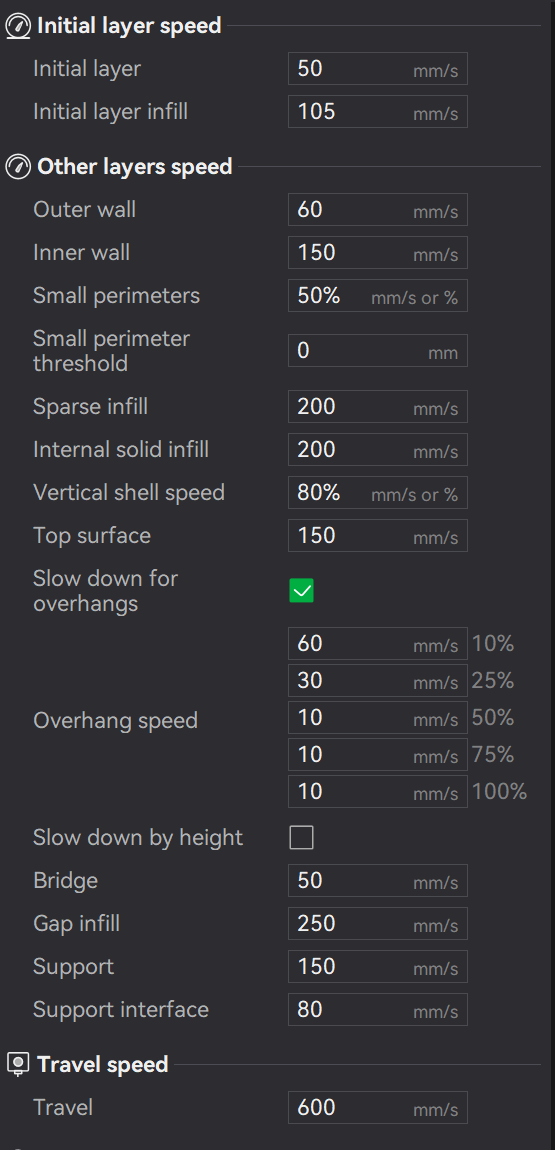
(Settings listed below images)
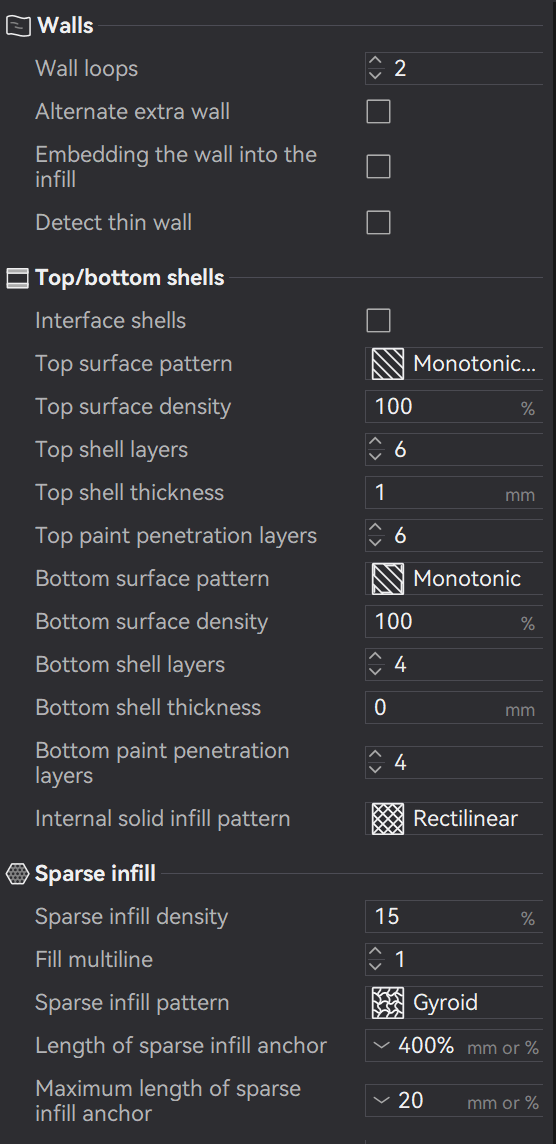
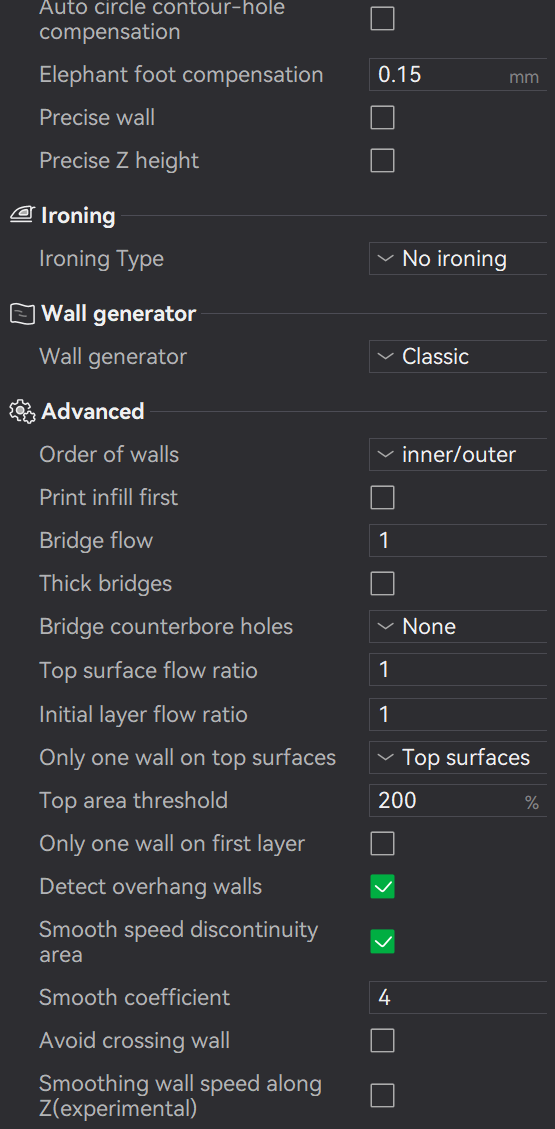
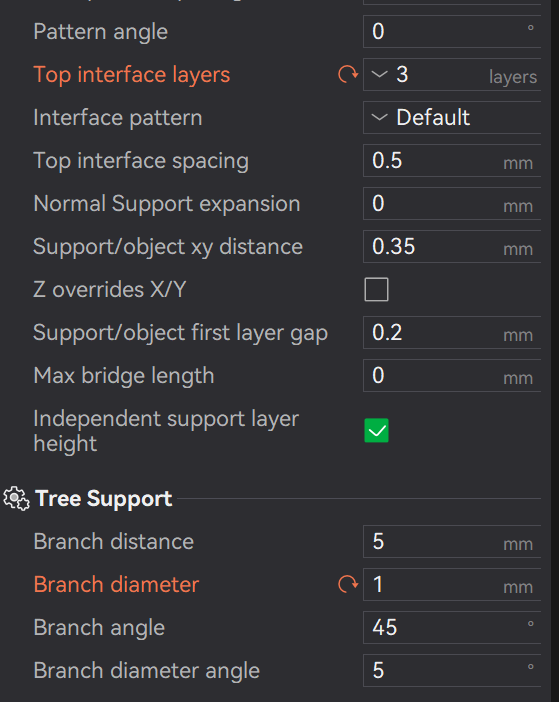
Bambu Labs Studios settings:
Thank you! I actually thought about some of these but was unsure. I honestly haven’t tried normal type supports since I was under the impress they are best for shapes that aren’t as round or organic - maybe I’m wrong in thinking that.
I did debate cutting the pieces in half prevously to have a completely flat surface against he plate. These pieces are the hilt and hand guard for a cosplay rapier so I’m trying to get it all in one piece if possible to avoid any extra bonded points with glue. I might give option 2 a try just to see what happens for the guard.
I acutally do have some questions when it comes to using PETG for the interfacing though. You mentioned keeping temps similar between both filament types -would this cause the nozzel to clog if PETG is set on the lower end and PLA is set on the higher end?
I was orginally thinking my previous under extrusion issue was from the PETG sticking or partially clogging the nozzel between transitions / flushing. I’ve had the prime tower look rough in one attempt and actually stopped it because I thought it was clogging the machine - their were some extrusion issues on the edges of the guard print too when I stopped it. I did have some blobs build up at the end of the nozzel about halfway through the print when I stopped it. My purge volumes were set to 600 though so maybe it was still too low. Was just curious if there’s something else going on when I use both filament types or if it’s just temp and purge volume like you mentioned.
I’m new at this stuff, too, LauranRJ. But I discovered Brims and that fixed a lot of my ailments.
Recently I added some supports to a print and used fine Trees. I like to try and use the Auto settings at first. Then will shut off the auto if it doesn’t do what I’d like it to.
But the fine trees were much more to my liking as A. Less material waste. and B. much easier to remove.
I don’t mess with filament changes like one for supports, while using another for what I’m making. I just use the same filament for everything, generally.
I would suggest you try a print with a 10mm outside brim and see if it doesn’t work for you. If not, try supports that attach to your plate.
You models appear to want trees on the outer reaches, in my limited experience.
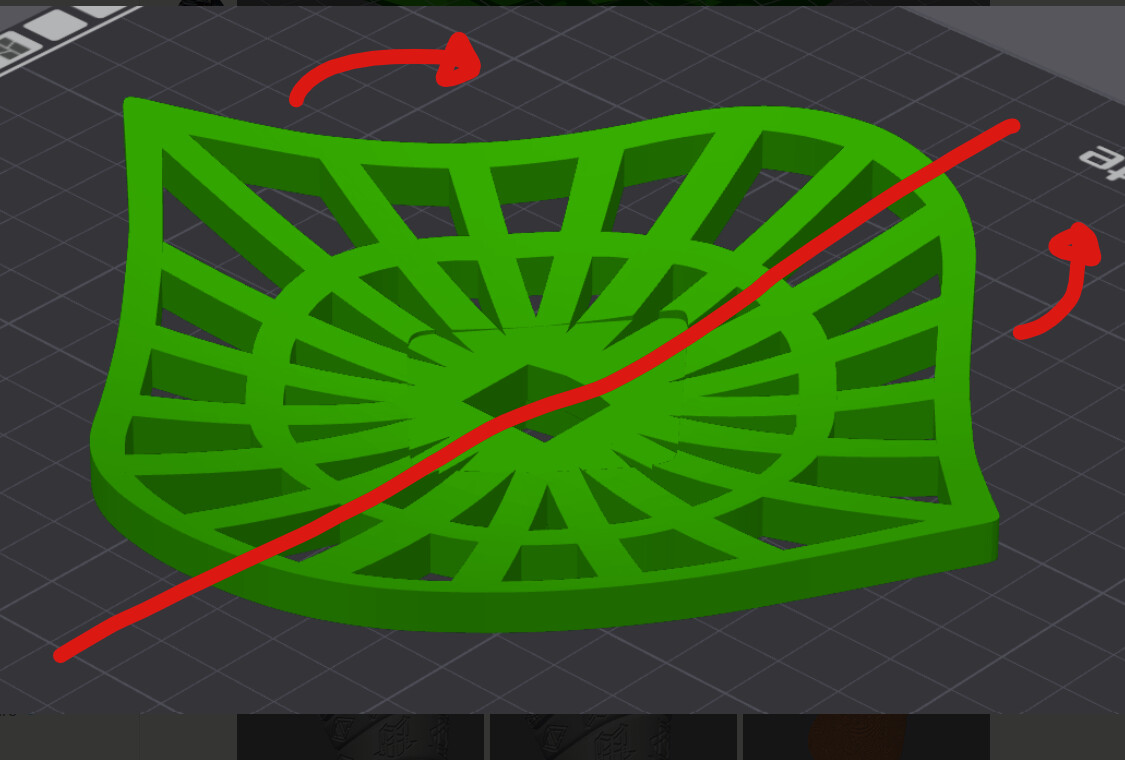
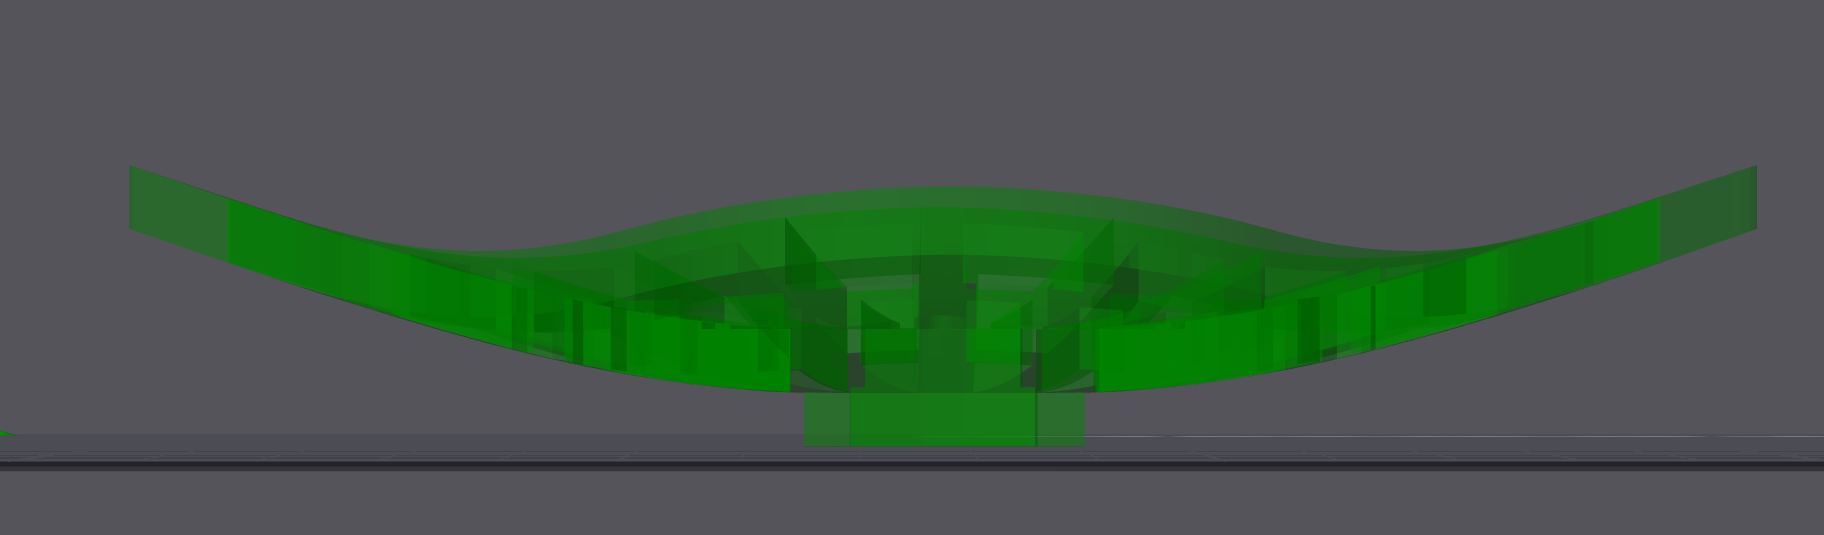
Not wrong, but look at it from below. The surface youre supporting is mostly flat and wide, just undulating up a little bit.
Keep the nozzle temps for whatever works, just think about the bed/plate. I dont have good luck with PETG being the interface only, [slips off the stalks, could be a ‘me’ problem] I tend to need it to be the whole support structure, so its gotta attach to the plate. Too cold and it wont  Too warm and your PLA melts. A lil glue helps make them both happy.
Ok, that’s helpful. I’ll give it a shot and keep that in mind when I adjust settings. I can try out a couple different things and come back with what I find out.
I’ve typically used trees but with this one it tends to cover the entire underside when I generate them. Maybe with the gradual angle I can remove some of these manually. Or the top of the branches might not be thin enough so it makes removal and scarring a pain.
Well I’ve tried testing some over the last few days but I’ve had no luck. I orientated it on its side so it’s standing up more. The scarring seems to be worse and now I have some weird pits in the layer lines, especially around curves. Not sure if that could be from a partially clogged nozzle but any extrusion tests with the PLA looks to be coming out normally. I’m at a loss for what’s going on at this point. 
Left side is my last print and right is the test before.
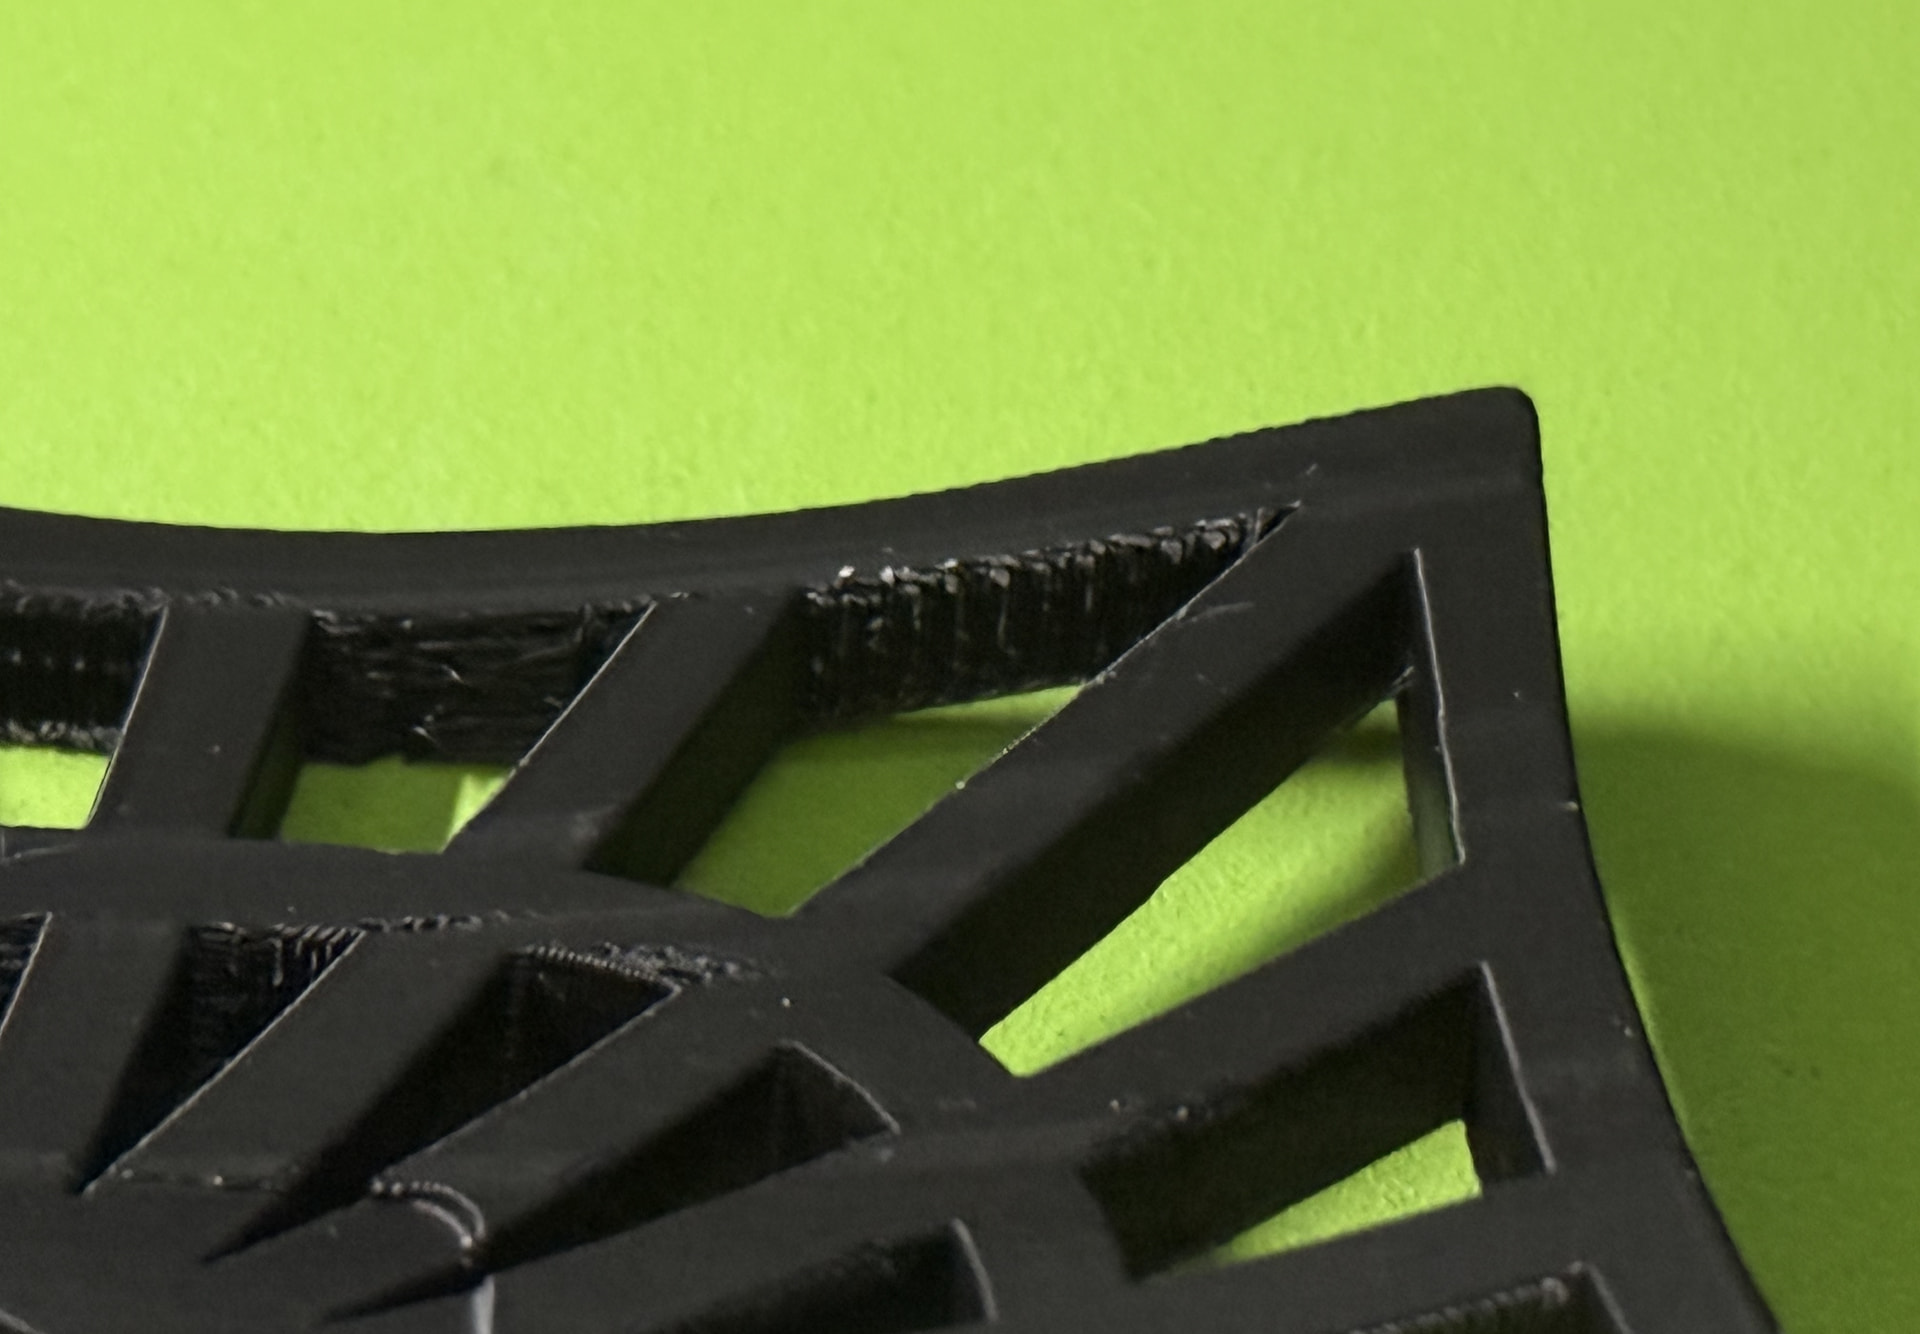
Pitting on the main surface:
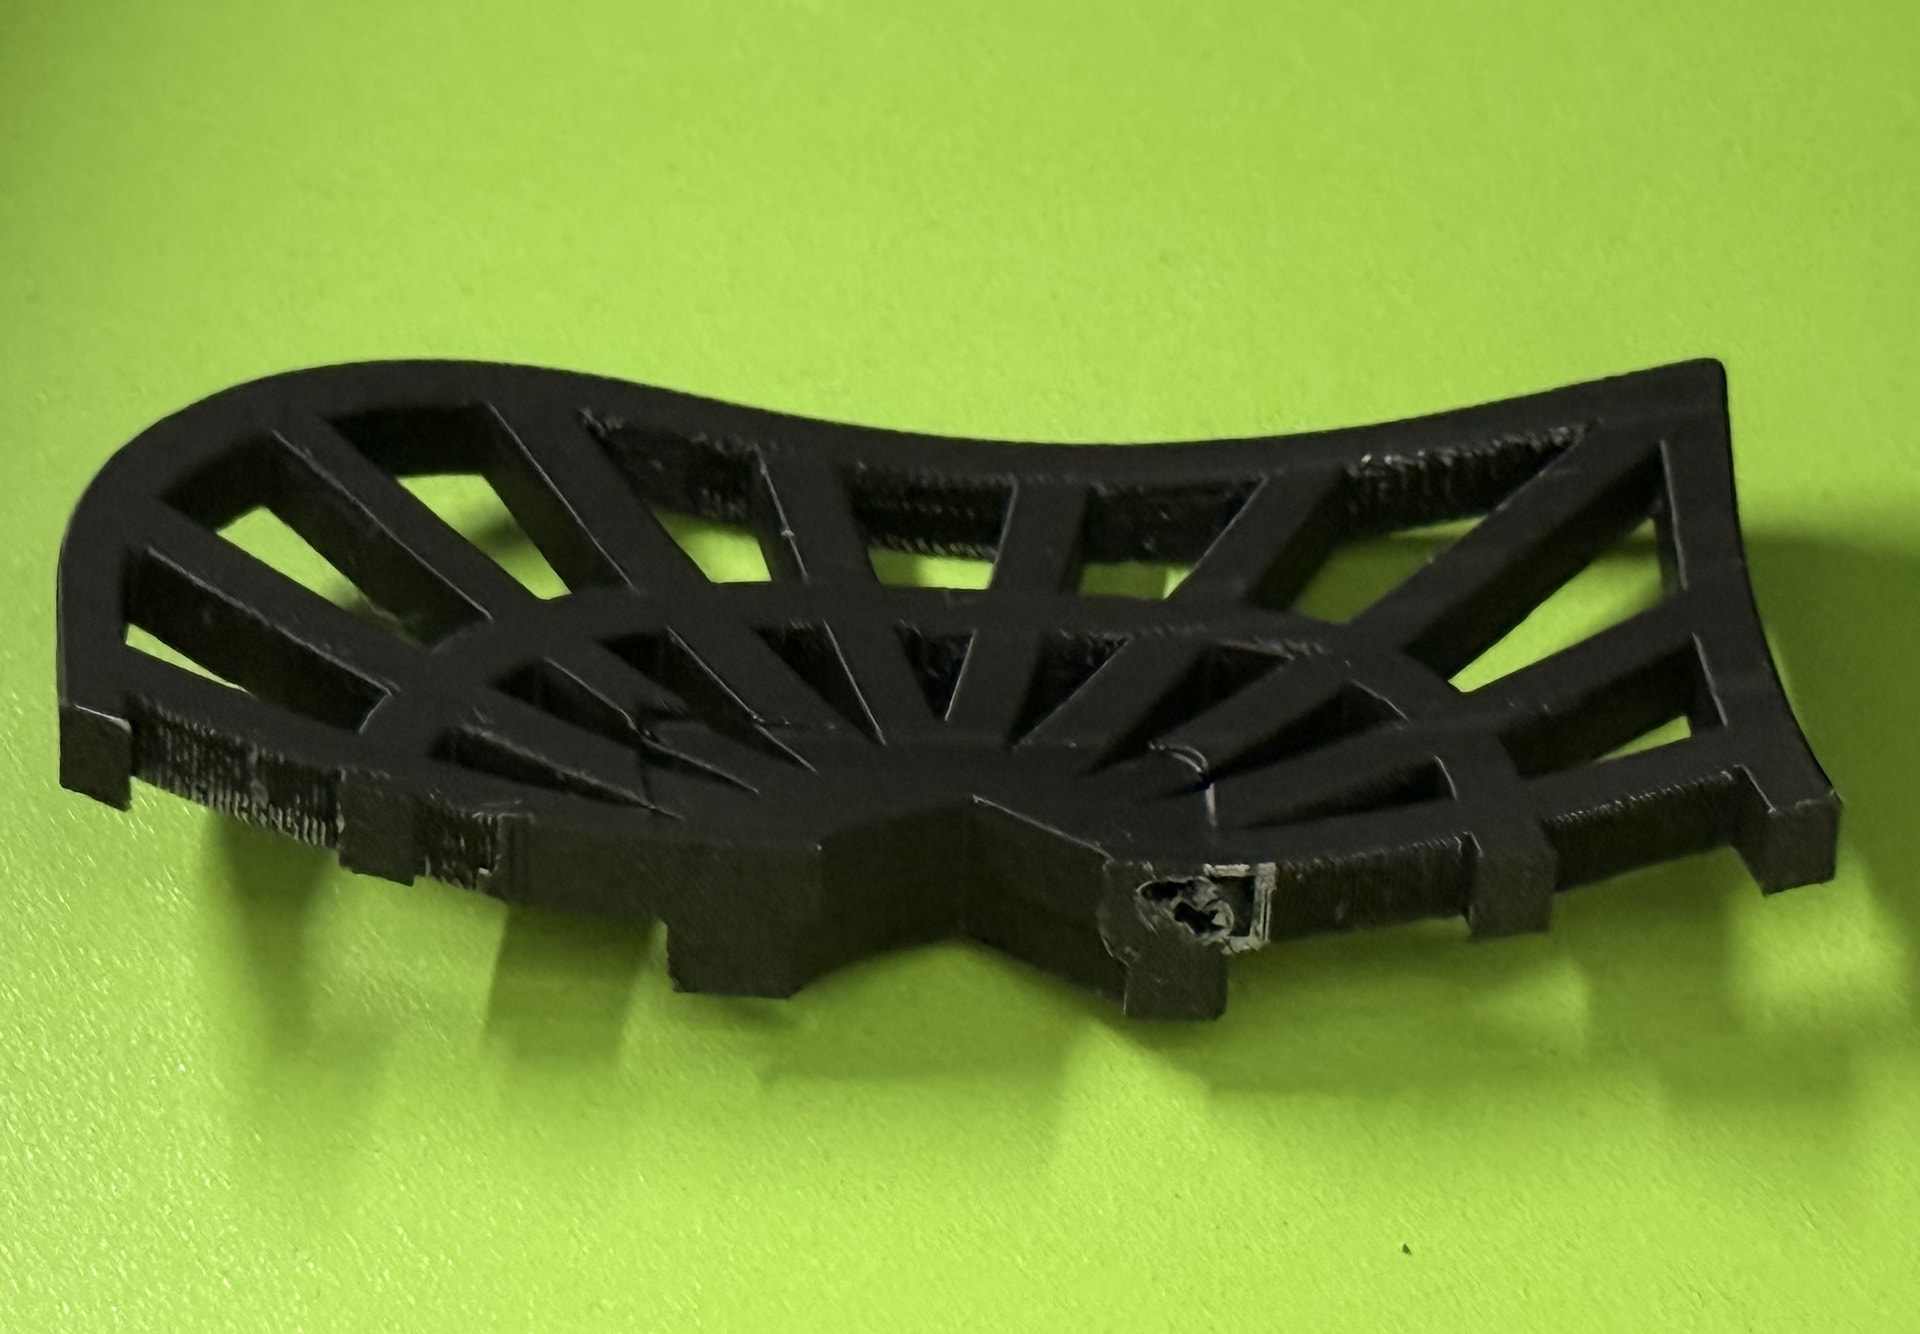
Share the model from the latest photo as some of us may wish to give it a try.
Either way, select the object and apply variable layer height from the toolbar. Just hit the first button (adaptive I think, from memory) and apply.
This will aid some of the harshest angles to be smoother.
Add support, likely ‘tree > hybrid’ would be a good start.
The base should be the smoothest edges, I am not sure which side you showed in the photo.
It looks like it may require a brim.
LED Guard & Grip - Test Settings.3mf (3.9 MB)
This file has both the guard and grip pieces with the settings I have been using. I included plates for both angles of the guard that I have tried (flat and upright). For some extra info, I’ve tried Top Z Distance between 0.2 - 0.25 but set this one inbetween (I beliveve I set it to 0.24). Variable Layer Height has always been on with Adaptive at 0 and Smooth at 10. I’ve tried Trees set to Default, Slim, and Strong just to see if something worked better than others (not really anything significant though). I’ve also tried narrower tree tops to minimize scar marks with connection points.
My prints are generally super smooth but recently has the weird layer line pitting and horrible support surfaces / removals on pieces. Feel free to try these out and let me know what you find - Thank you!
Printing now.
I have used the suggestion of printing half, so you could add a peg and socket join (or PLA glue) and my own suggestions.
It will take less than 3 hours for the half, I may report later or tomorrow (as it is late).
Awesome, thank you so much! If you don’t have any weird line pitting then it’s 100% just my printing messing with me. Let me know if you have a decent time with supports as well - that’s something mine always struggle to do properly as of late.
It has finished.
I have removed the support, done easy, some with a little effort.
It looks relatively smooth. I will need to use a flame (lighter) to clean a couple of areas.
I will take before and after photos.
I will also provide you my 3MF. As it is 2am and I am very tired, I will do this tomorrow.
You will need to design a plug and socket to join the two sides together or use a PLA suitable glue like Cyanoacrylate (CA) super glue, such as Loctite or Gorilla Super Glue or a specialty glue like PLA Gloop.
Thanks again! Absolutly no rush. Would you mind also sharing your filament settings when you send photos? I’m just curious even if it might be different filament.
I couldn’t find my lighter, but it would only make the white stress marks become the filament colour.
I used almost all your settings for the model and filament, I only changed the colour I used, it was also BL.
The only setting change can be found on the model part settings. Support, hybrid and not slim.
I positioned the model halfway through the plate so it only prints the portion above the build surface.
Almost all the imperfections are only viewable ion the photos.
The first photo has a surface error (bottom right of centre), I went a bit mental while removing the support, that was me, not the model.
LED Guard & Grip - Test Settings.3mf (3.9 MB)
Oh wow! Yeah some of the stuff you’re seeing is what I’ve been getting in terms of surface imperfections and troublesome supports. I’m just glad someone else is getting this and it’s not just something with my printer. This makes me thing it’s something in the settings that’s messing with both issues.