X1C prints much better than X2C

I recently purchased a x2d. I did so for the heated chamber and support material for auxiliary nozzle. I print functional parts, using a lot of ASA and PA-CF, PC and PCTG materials. It was my understanding this was what the x2d was designed to do.

I Properly dry and store all my filaments. Wet filaments is NOT this issue here.

Also I am bypassing the AMS for PPA-CF and PAHT-CF

So far for me, the x2d just has terrible quality for many of the engineering materials. and I am referring to the main nozzle. I am not going into any issues here related to Aux nozzle. So basically I am treating the x2D as a single Nozzle printer for now. Since if it can’t do basic things with main nozzle what’s the point of added Aux into the equation.

Below is an example of the poor quality. At the same time the X1c will print as expected (almost flawlessly) using the same spool of material back to back. So this is not a wet filament issue.

I have been using the x1c for 1.5yrs. I try to keep in running almost 24/7… more or less. I use both .6 and .4 nozzles without any issues. And even after this amount of use, it seems to print better than x2D
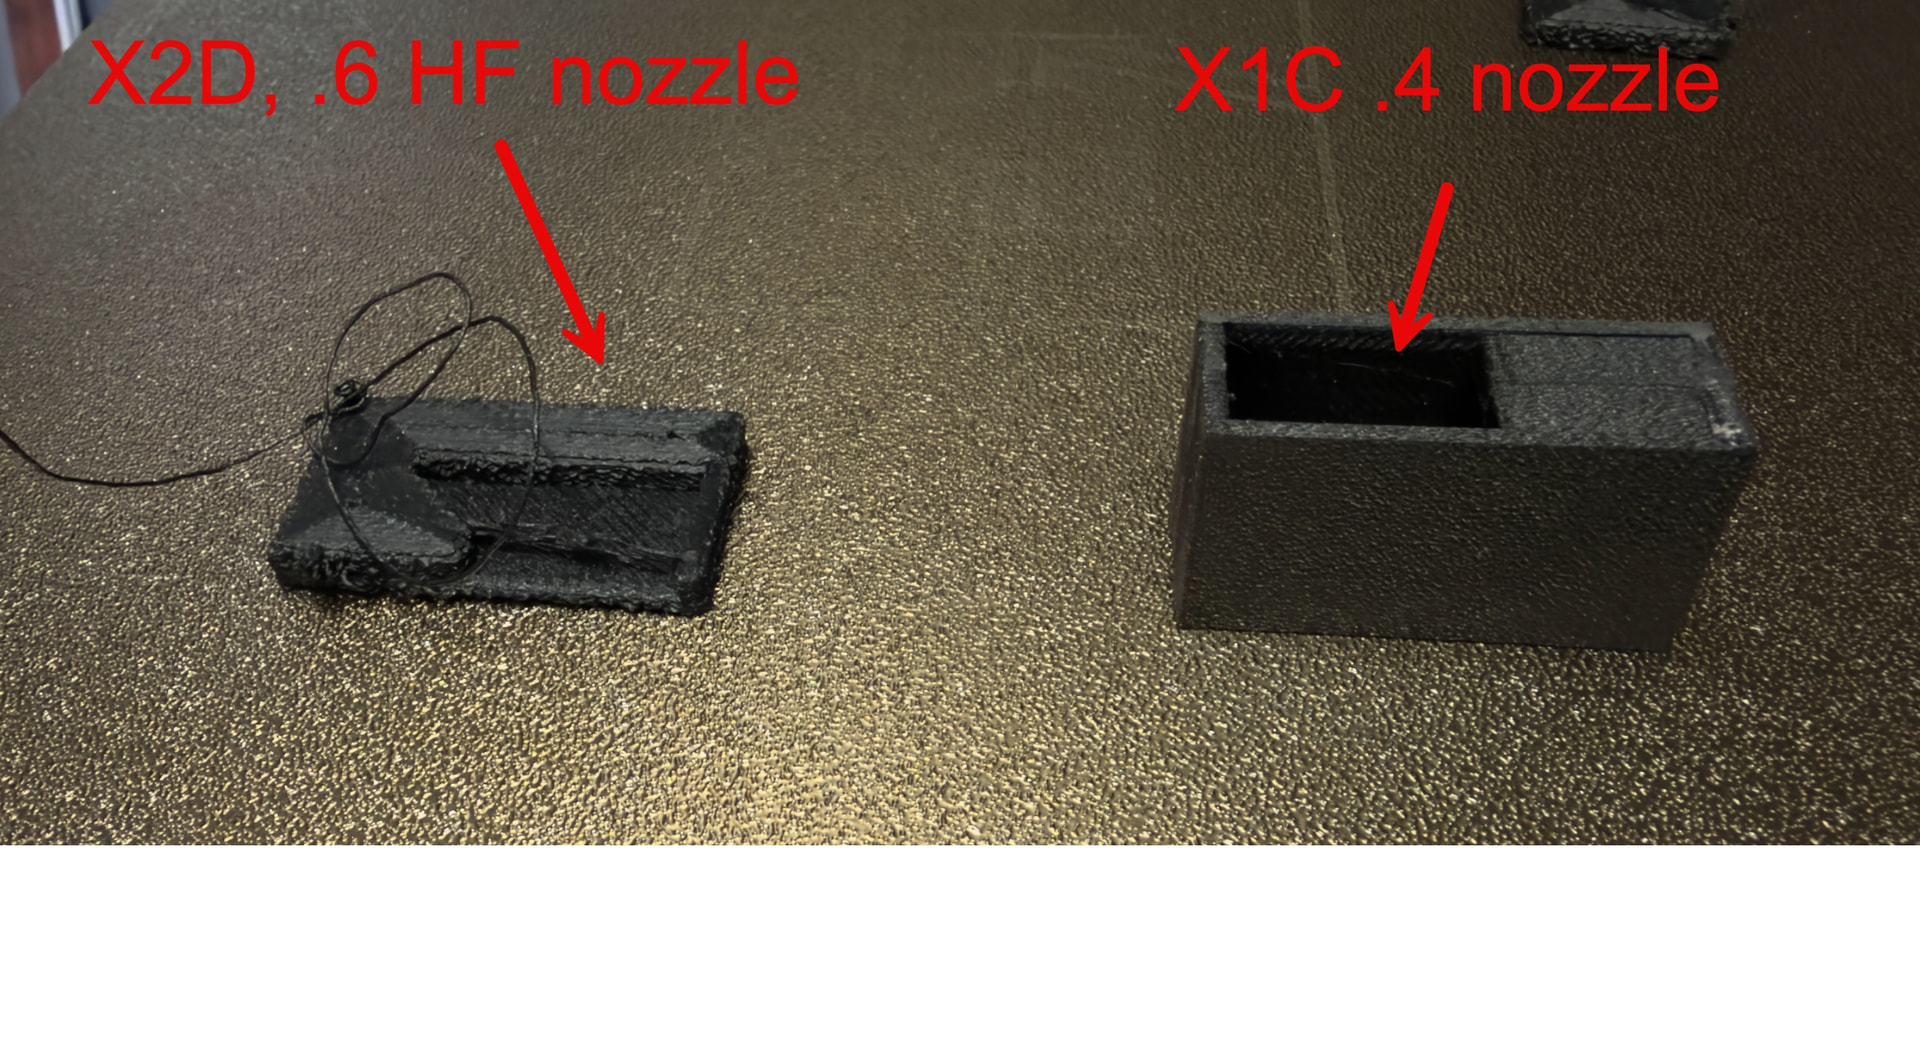
I am kind of at my wits end. I have iterated on speeds, print profiles etc…

  • I suspect the poor quality is a lack of proper .6 profiles for x2D.
  • Or perhaps the HF nozzles are an issue for CF filled materials?
  • Or its the heating/cooling modes? these modes seems to override (ignore) filament settings.

PLA prints great on the x2D. ASA has printed well too. But the engineering materials with CF fill are disaster.

Anybody else have this issue?

First, I applaud the lengths you went to isolate the root cause. I wish more people would do that before posting a one-sentence “need help” post.

One thing still stands out to me in your comparison: have you tried a 0.4 mm nozzle on the X2D?

In the example shown, you’re comparing the X2D with a 0.6 mm HF nozzle against the X1C with a 0.4 mm nozzle. That means the printer, nozzle, and associated profile are all changing at the same time. Since the same spool prints correctly on the X1C, you’ve done a good job ruling out wet filament, but I don’t think the test yet isolates the X2D itself.

I ask because my experience with Bambu Studio profiles outside of the default 0.4 mm profiles has been very poor. I’ve tested quite a few of the supplied 0.2, 0.6, and 0.8 mm profiles, and so far I’ve had a 100% failure rate among the profiles I’ve tested. Because of that, I now calibrate them myself rather than assuming the supplied profile is properly tuned.

Given that you already suspect the 0.6 mm profile or HF nozzle, I’d be very interested to see what happens if you put a 0.4 mm nozzle on the X2D and rerun the same material. That would remove one of the biggest variables from the comparison.

Check into this aspect. I found that the default cooling profile was overly aggressive for TPU on my X2D, at least for the items I was printing. You may find that cooling fans are turning on at unexpected times, or at higher intensity than desired.

The X2d fans are not very good IMO for hot boxes. They do fine printing PLA, but I also did not have very good ASA luck, found the hacks re: fan gcode, and decided to just do my ASA on the Qidi lol. If you scrape around the forums here you can find others who have done fan mods and fan gcode overrides to get it behaving better.

thanks for the noticing :slight_smile:

I do agree with switching back to .4 standard nozzle is worth trying. . Don’t want to. I print mostly large parts. and .6 is my main size. for speed. but it is what it is.

I just did one more test. Where I slowed the speeds down to less than 30mm/s for everything… then made a test print, it looked pretty good, Since this was just a quick test I left wall thicknesses to default of 2.

Since the test looked good, I bumped up the walls count such that the part is fully infilled. This is a small part (hook) that is going to hang a concrete object on the wall. So I need to make it as strong as possible given its small size..I am mostly worried about creep over time.

This solid part looks like crap. The outside walls look like a fuzzy, globby mess. Its unusable

Anybody have ideas why added wall thickness part would screw up the quality? FWIW, X1C does not have an issue printing this part/material will full solid part… with a .4 nozzle of course.

The price of x2d looked too good to be true. I was hesitant with the Bowden extruder. But I never expected the hassle I am having printing engineering grade materials on the none Bowden nozzle. I have been a big fan of BL. x1c spoiled me I guess.

Perhaps I am going to have to pull the trigger on a H2… I just want rock solid reliability printing the higher end materials.

I can deal with warping issues. But I cannot solve the printer just printing like crap in the first place.

Anyway thanks for the responses.

That result would have me looking pretty hard at extrusion/flow calibration, especially since slowing everything below 30 mm/s materially improved the print.

One quick diagnostic I’d try is deliberately dropping the flow ratio to something unusually low, say 0.85. At that setting I would expect obvious under-extrusion and probably some voids. I’m not suggesting 0.85 as a solution; the point is simply to see whether a large reduction in commanded flow materially changes the fuzzy/globby surface.

If the surface improves significantly, I’d go back to square one and calibrate that specific filament/0.6 mm nozzle combination rather than trust the supplied profile.

The fact that reducing speed helped also makes me suspicious of the volumetric-flow side of the profile. With the higher wall count you’re asking the nozzle to spend much more of the layer in continuous extrusion, so a flow, temperature, or volumetric-rate problem that was marginal before may become much more obvious.

quick update

I switched to .4 default nozzle. This had a drastic effect. The x2d now prints now print as expected with PPA-CF. kind of good news.

I guess x2d cannot use .6 HF nozzles on anything other than basic materials like PLA… At least I could not figure out how to do so. 4-5 days of trial and error. I personally think its something to do to with the HF nozzle vs .6 nozzle size.

This is not the first time I have problems with HF nozzle. I have found HF nozzles get clogs and filament breaks in the head when using material with CF. I have not had these issue with using non-HF nozzles.

Correct me I am wrong, but HF nozzles have a more complex pathway inside the nozzle? they do so for added heated surface area? That also seems to result in more clogging potential with materials like CF filled.

I could be wrong. But I think I am done with the BL HF nozzles for now. Benefits are marginal IMO… And I am sick of having to pull apart the printer and filament path to diagnose and fix clogging problems… Let alone poor print quality on some materials

Dear Bambu Labs

You should have worked out the kinks and developed a comprehensive set of profiles for material and nozzle combinations for x2d… You did not. I go with Bambu Labs products for the Ecosystem. I just want to use the printer.

With the x2d I have been forced into developing my own material/printer profiles for your materials and nozzles. Kind of sucks… I don’t want to spend time doing this.

The automatic heating/cooling modes on x2d SUCK. You are overriding user settings. it’s unpredictable and confusing. I think I get what you are going for. But since you did not put in the work to get x2d to work well with all the combinations of material and nozzles you offer. you are just causing print failures and frustration. Seems like you only payed attention to PLA.

You need to add a “disable Strong cooling mode and heating mode” option for users.

Fingers crossed BL addresses some of this soon

I would call your test a success. The good news is that, knowing the rest of the process works with the 0.4 nozzle, you have isolated the problem considerably. It now comes down to determining what the 0.6 HF nozzle/PPA-CF combination will reliably tolerate.

I had suspected this might be the outcome based on my own experience. As I may have mentioned earlier, Bambu Lab, and frankly much of the rest of the 3D-printing industry, appears to put the majority of its profile-development effort into 0.4 mm nozzles. If you search this forum over the last few years, there are plenty of unhappy stories involving 0.2, 0.6, 0.8, etc., particularly once you move beyond basic materials such as PLA.

You may want to start with the following order:

  1. Temperature tower - Often this does not yield a single obvious winner, but it is a good starting point and should give you a useful operating range. If you want help interpreting the tower, upload a photo and I can point to the likely best temperature.

  2. Maximum volumetric flow - Based on what you just proved, this is where I would focus first. The 0.6 HF nozzle may simply be trying to push PPA-CF faster than that particular hotend/material combination can melt and move reliably. Set the maximum volumetric speed conservatively and see whether the wall degradation disappears.

  3. Flow rate - Once you know you are operating below the volumetric limit, calibrate the flow ratio. That will correct systematic over- or under-extrusion, but it will not compensate for exceeding the hotend’s sustainable melt rate.

I would also be cautious about concluding that the problem is simply the 0.6 mm nozzle size. Your test really isolates it to the 0.6 HF configuration, not nozzle diameter alone. The HF internal geometry may itself be part of the problem with CF-filled materials, which would also be consistent with the clogging and filament-break behavior you described.

Thanks Olias

great recommendations. I did use the built in calibrations tools for the material before trying to use. Obviously that was not effective.

I have reached my tolerance for debugging x2d at this point it time. I will just use the .4 nozzle and deal with longer print times and slightly weaker parts…

Question for those of us trying to use other calibration methods you recommend. I have found many 3dm files with test heat towers or flow rate. Thing is they are all designed for other machines and .4 nozzle size. I try to adjust them, pointing towards my printer and nozzle. The test settings are removed. So I don’t get how to use an existing heat tower built for a different printer/nozzle.

Insult to injury, I have also tried to use the orca slicer directly. Problem with that is the only way I see to get the orca slicer output into Bambu Studio is to save as gcode then open gcode from Bambu Studio. Problem with that is Bambu Studio just crashes when trying to open gcode… I have never been able to open Gcode in Bambu Studio. I am on MacOS. I assume this must work on Windows. But Mac, not so much

I just wish BL would add the orca calibration options into Bambu Studio.

Bambu Labs

Still a Bambu Labs fan. I have been in this industry for a LONG time. And 3D printing used to a hacker only domain. You guys really changed the industry.

However the launch of x2D is not living up to this expectation. This entire thread is a result of you not putting in the work before launch. You should have have robust and comprehensive profiles, and options in the software. specifically for your filaments and nozzle.

Are you aware that at least some of the Orca calibrations are available in Studio?

Enable Develop mode in Preferences.

Choose the calibration in OrcaSlicer, slice and save it to a flash stick, plug the stick into the printer and print it.

I’ve seen this advice being dispensed before. Unfortunately, what you are suggesting often will not work.

The problem is that simply saving a calibration as a 3MF and expecting it to load back into another slicer, such as moving from OrcaSlicer to Bambu Studio, does not necessarily preserve the calibration behavior.

The calibration tower itself is just geometry. The actual test depends on the slicer generating the required parameter changes at specific points in the print. Depending on the calibration, those changes may include temperature, speed, volumetric flow, retraction, or other parameters.

The safest approach is to generate the actual G-code from the calibration and use that printer-ready file, rather than assuming that the calibration behavior survived being saved, reopened, or transferred between slicers.

I’ll give a simple example using a temperature tower.

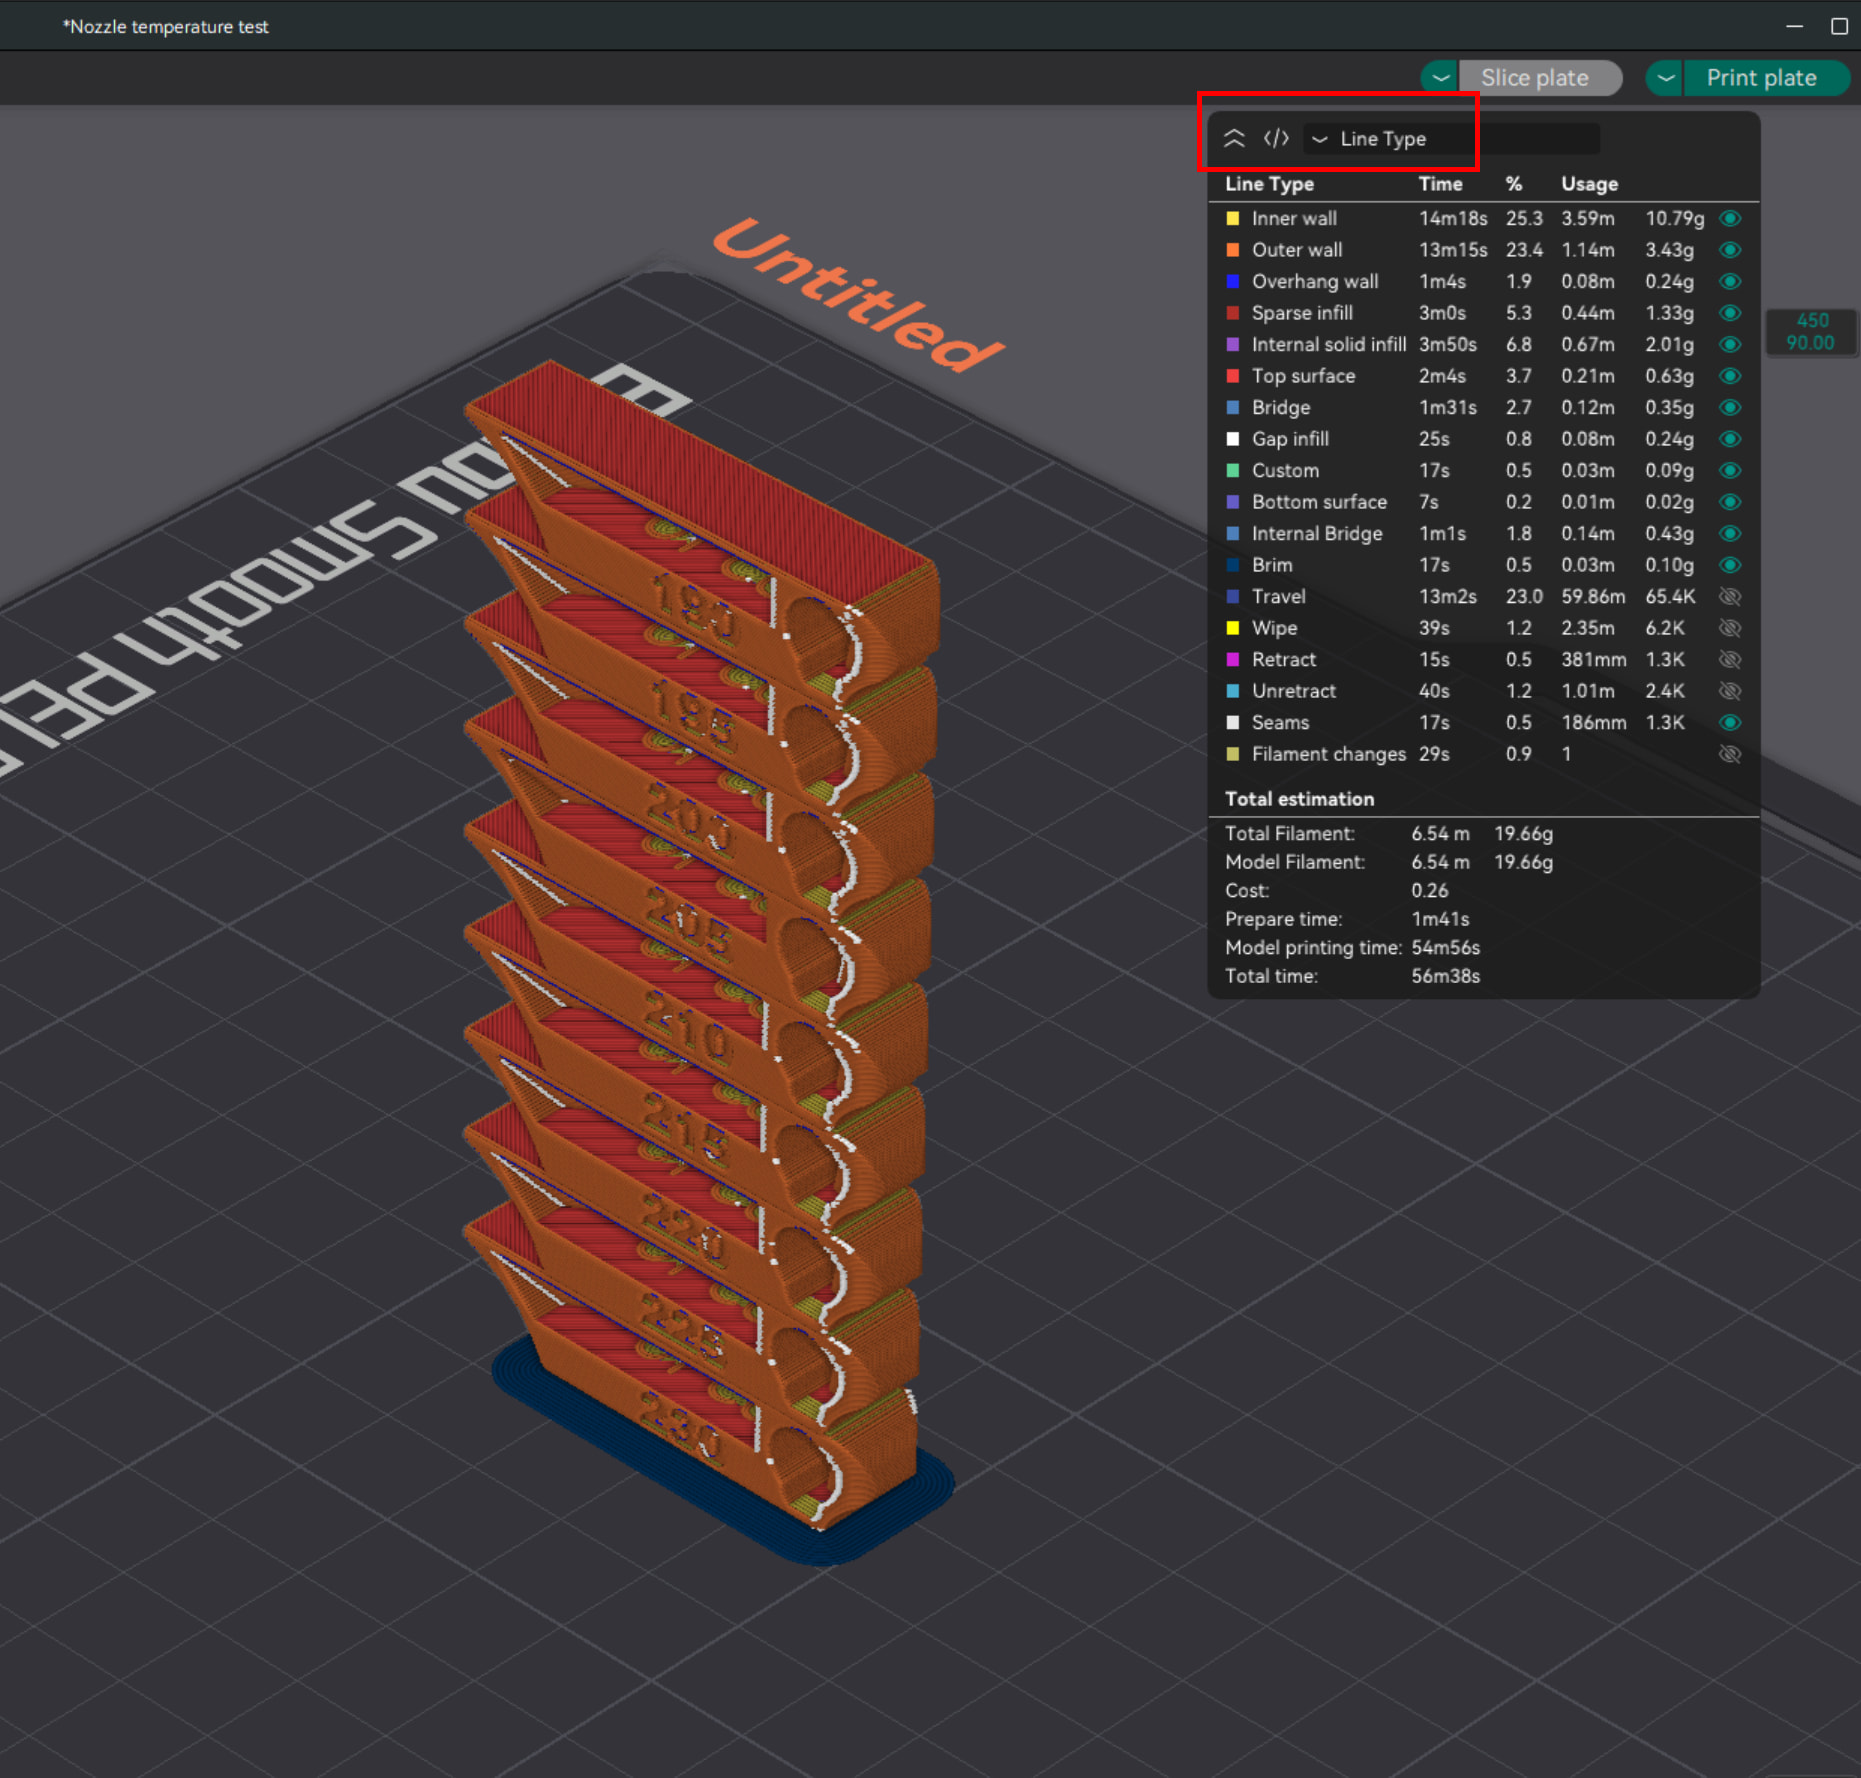
We all recognize this slice, but the default view is to show line type.

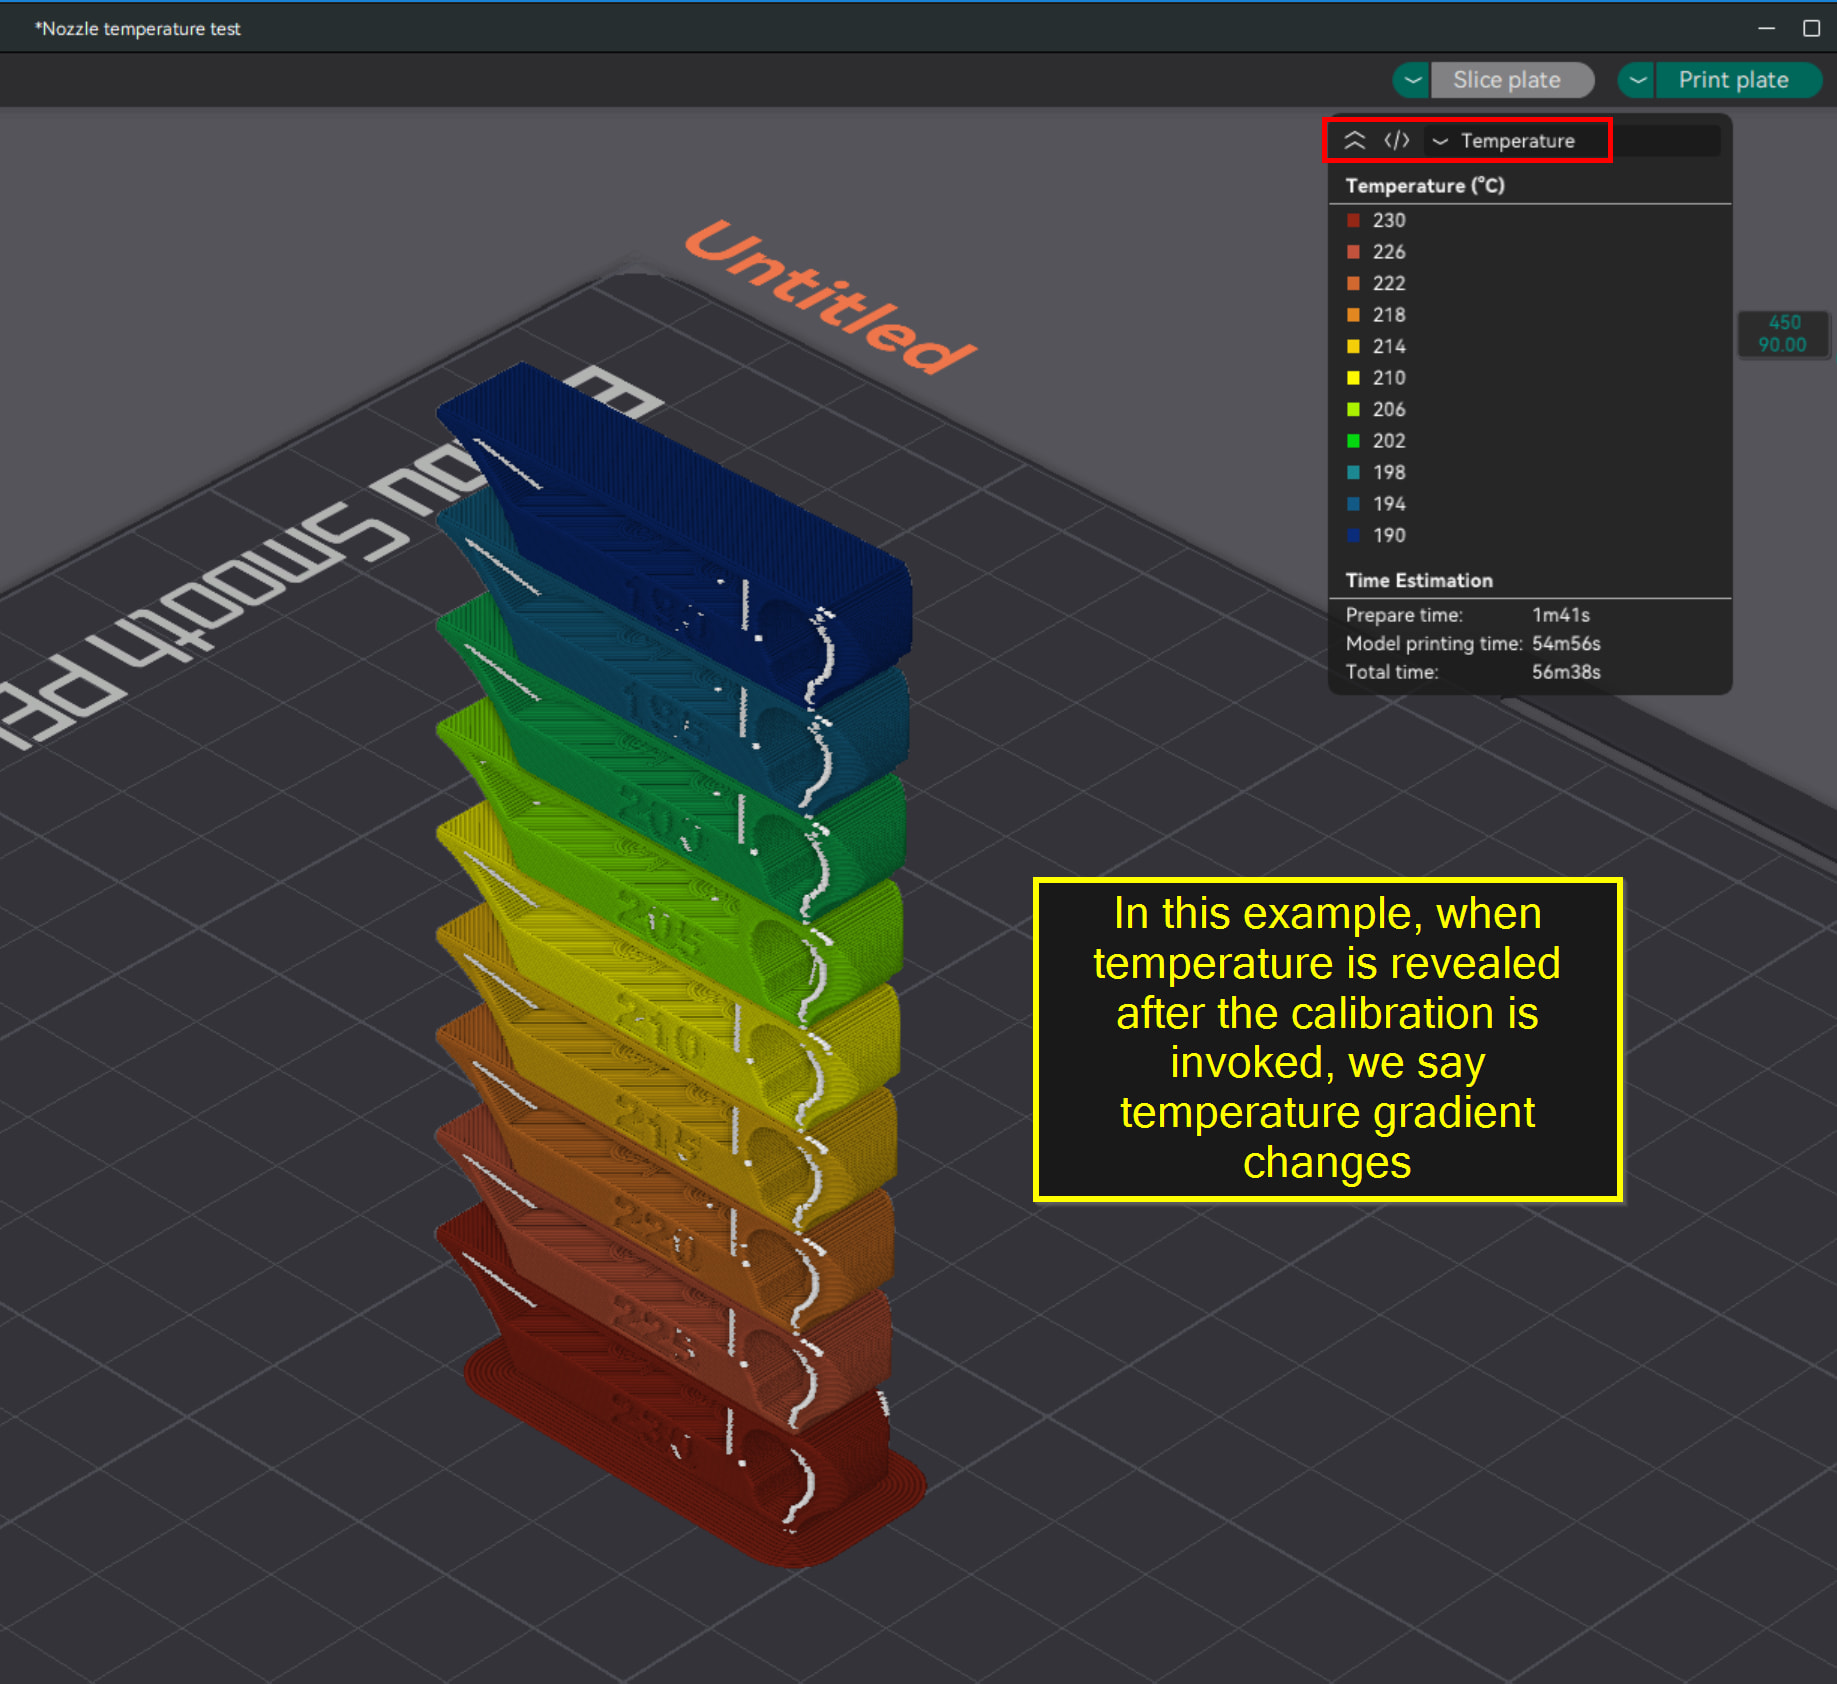
If we turn on Temperature view, we can see the gradient of the programmed temperature changes in the G-code.

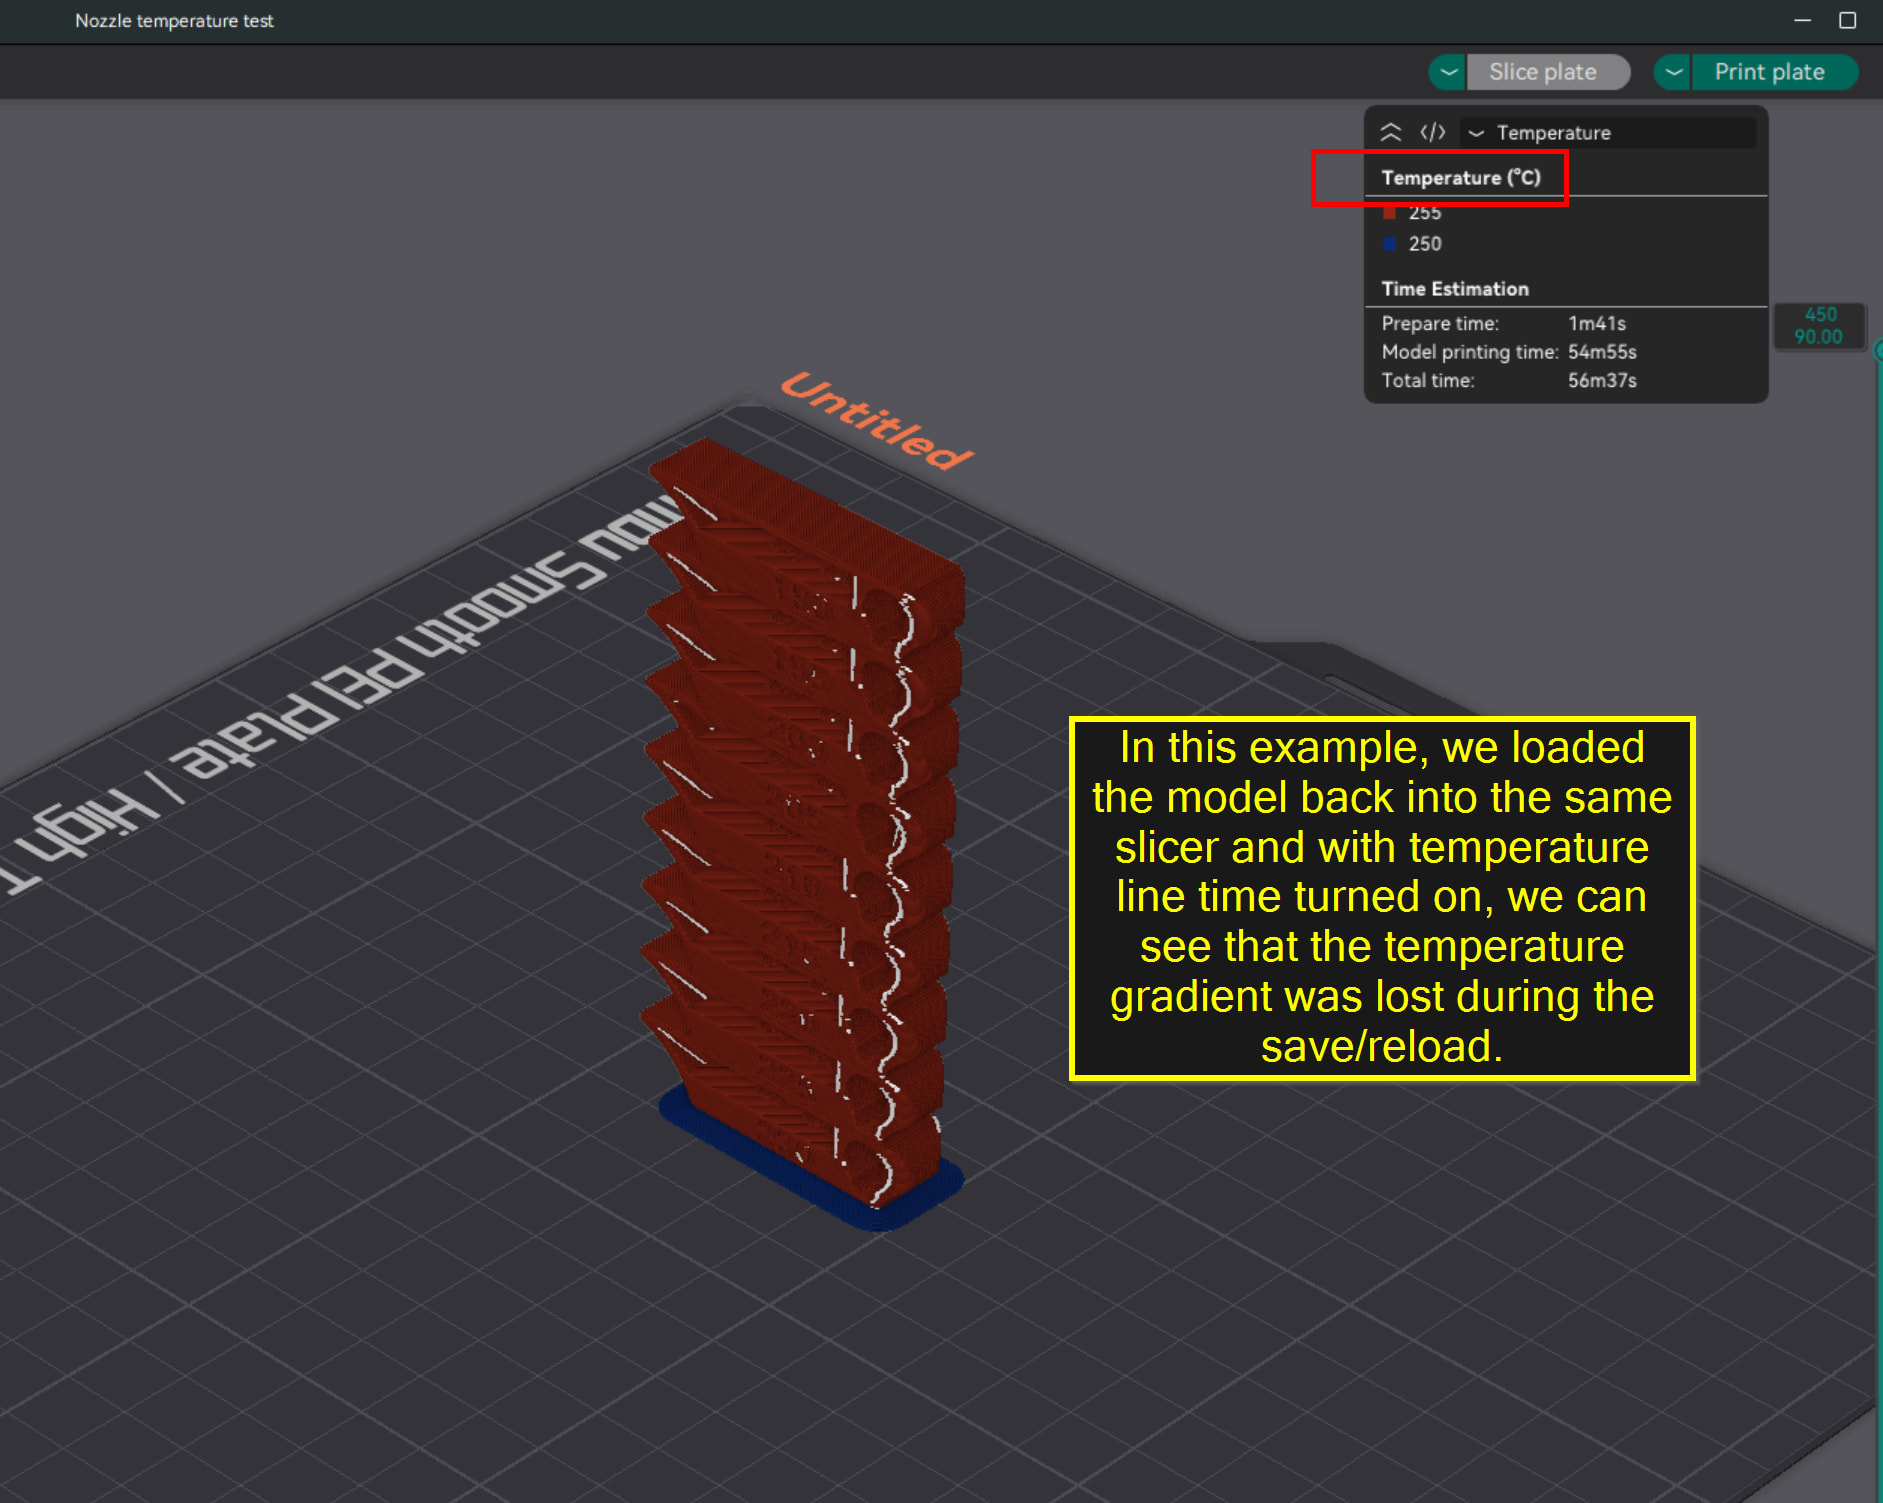
Now we save that file, load it back into the slicer, reslice it, and show the temperature.

This does not always happen, but unless one goes the extra step to verify that the calibration changes have actually been implemented, all one may be doing is printing a uniform model, not performing a true temperature calibration.

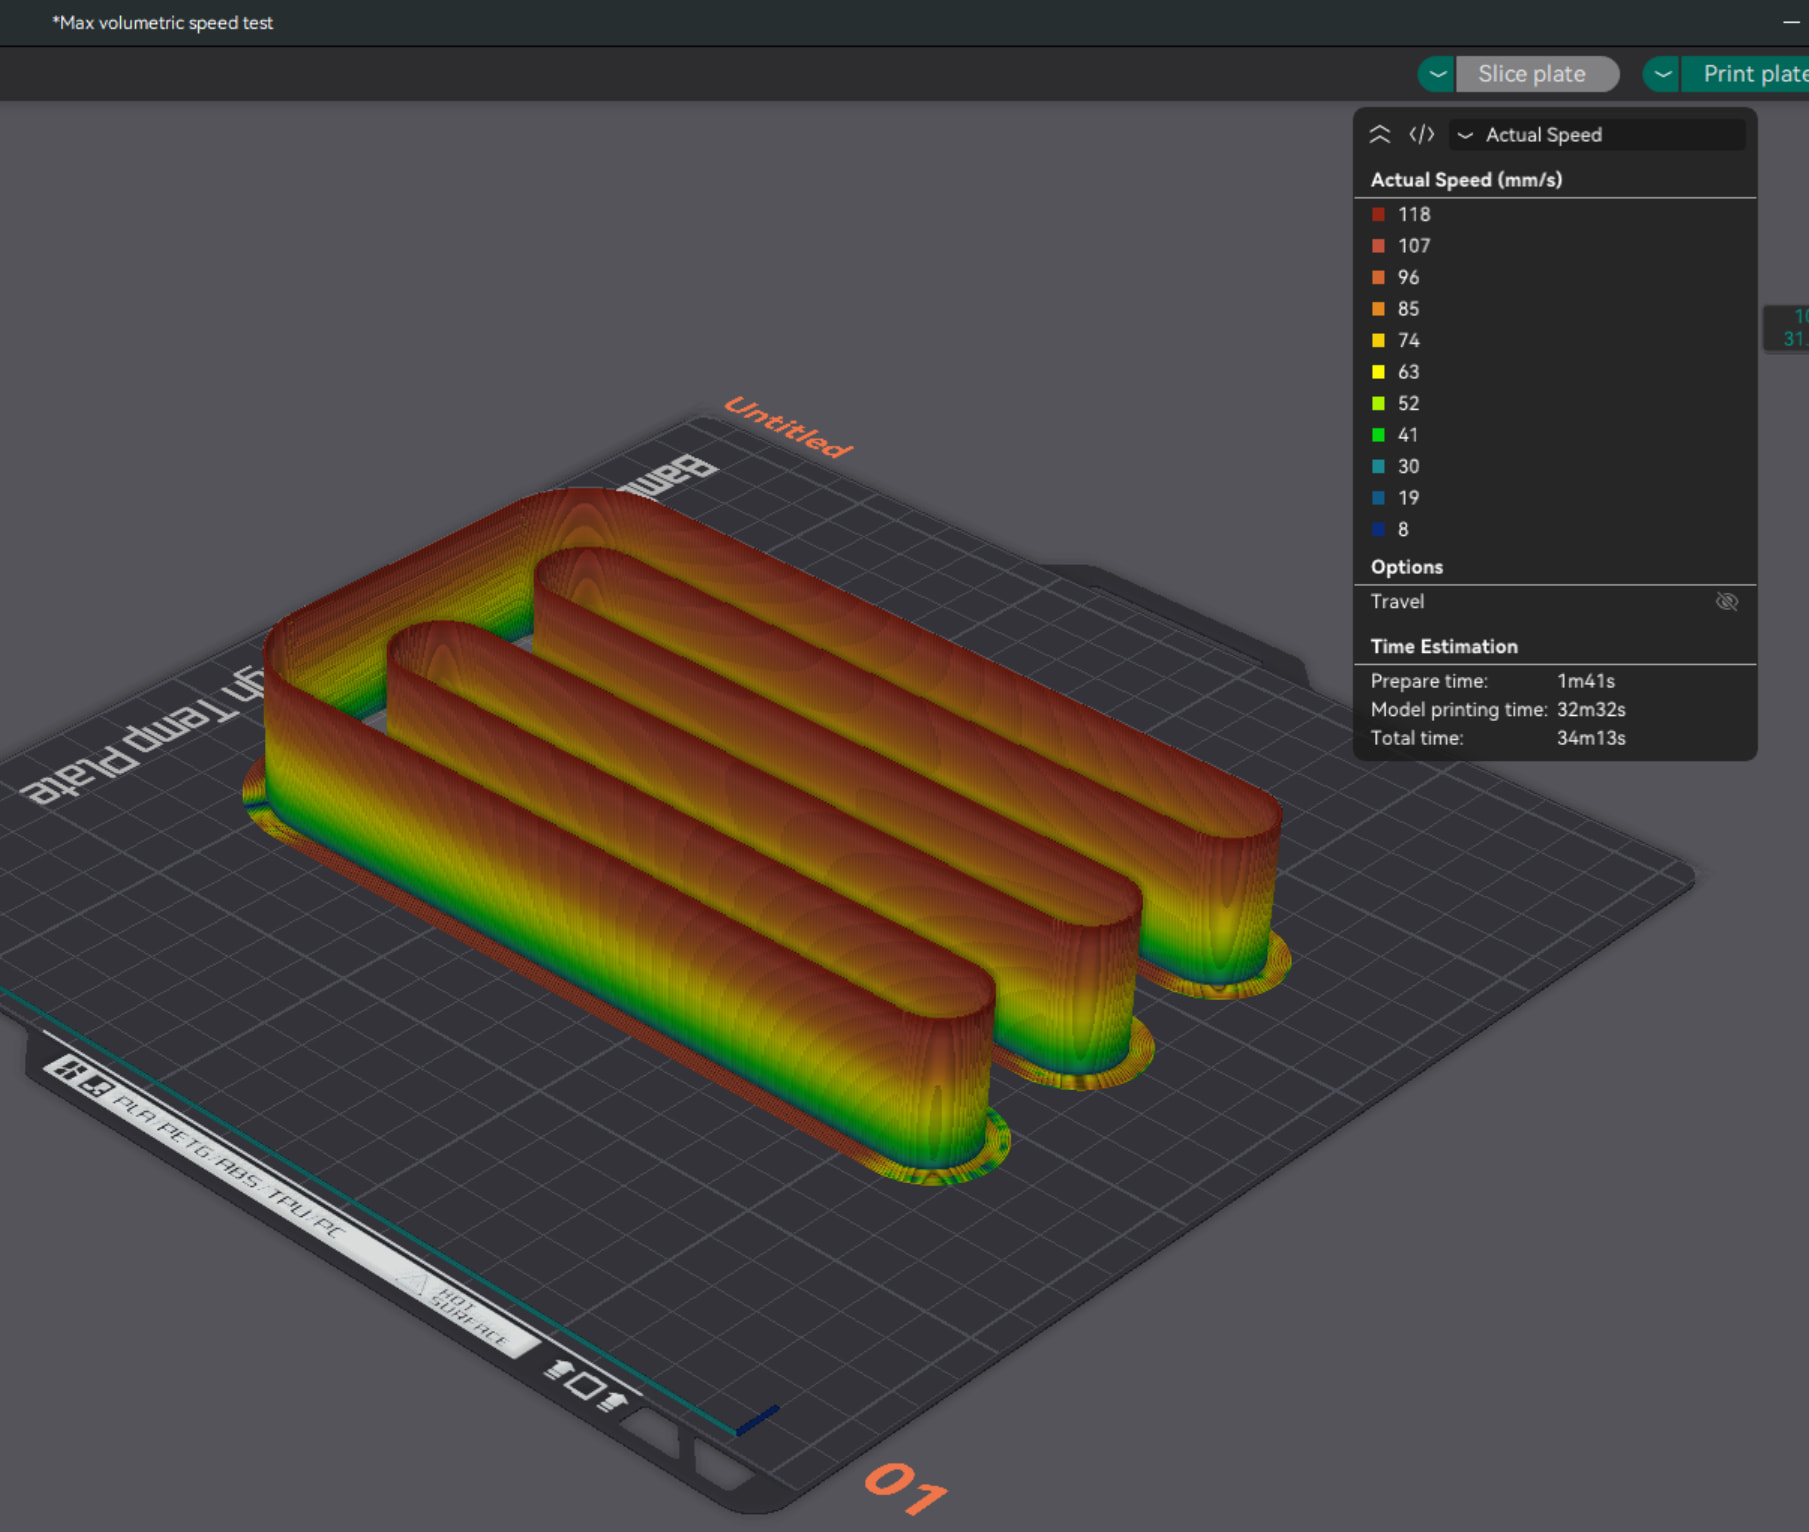
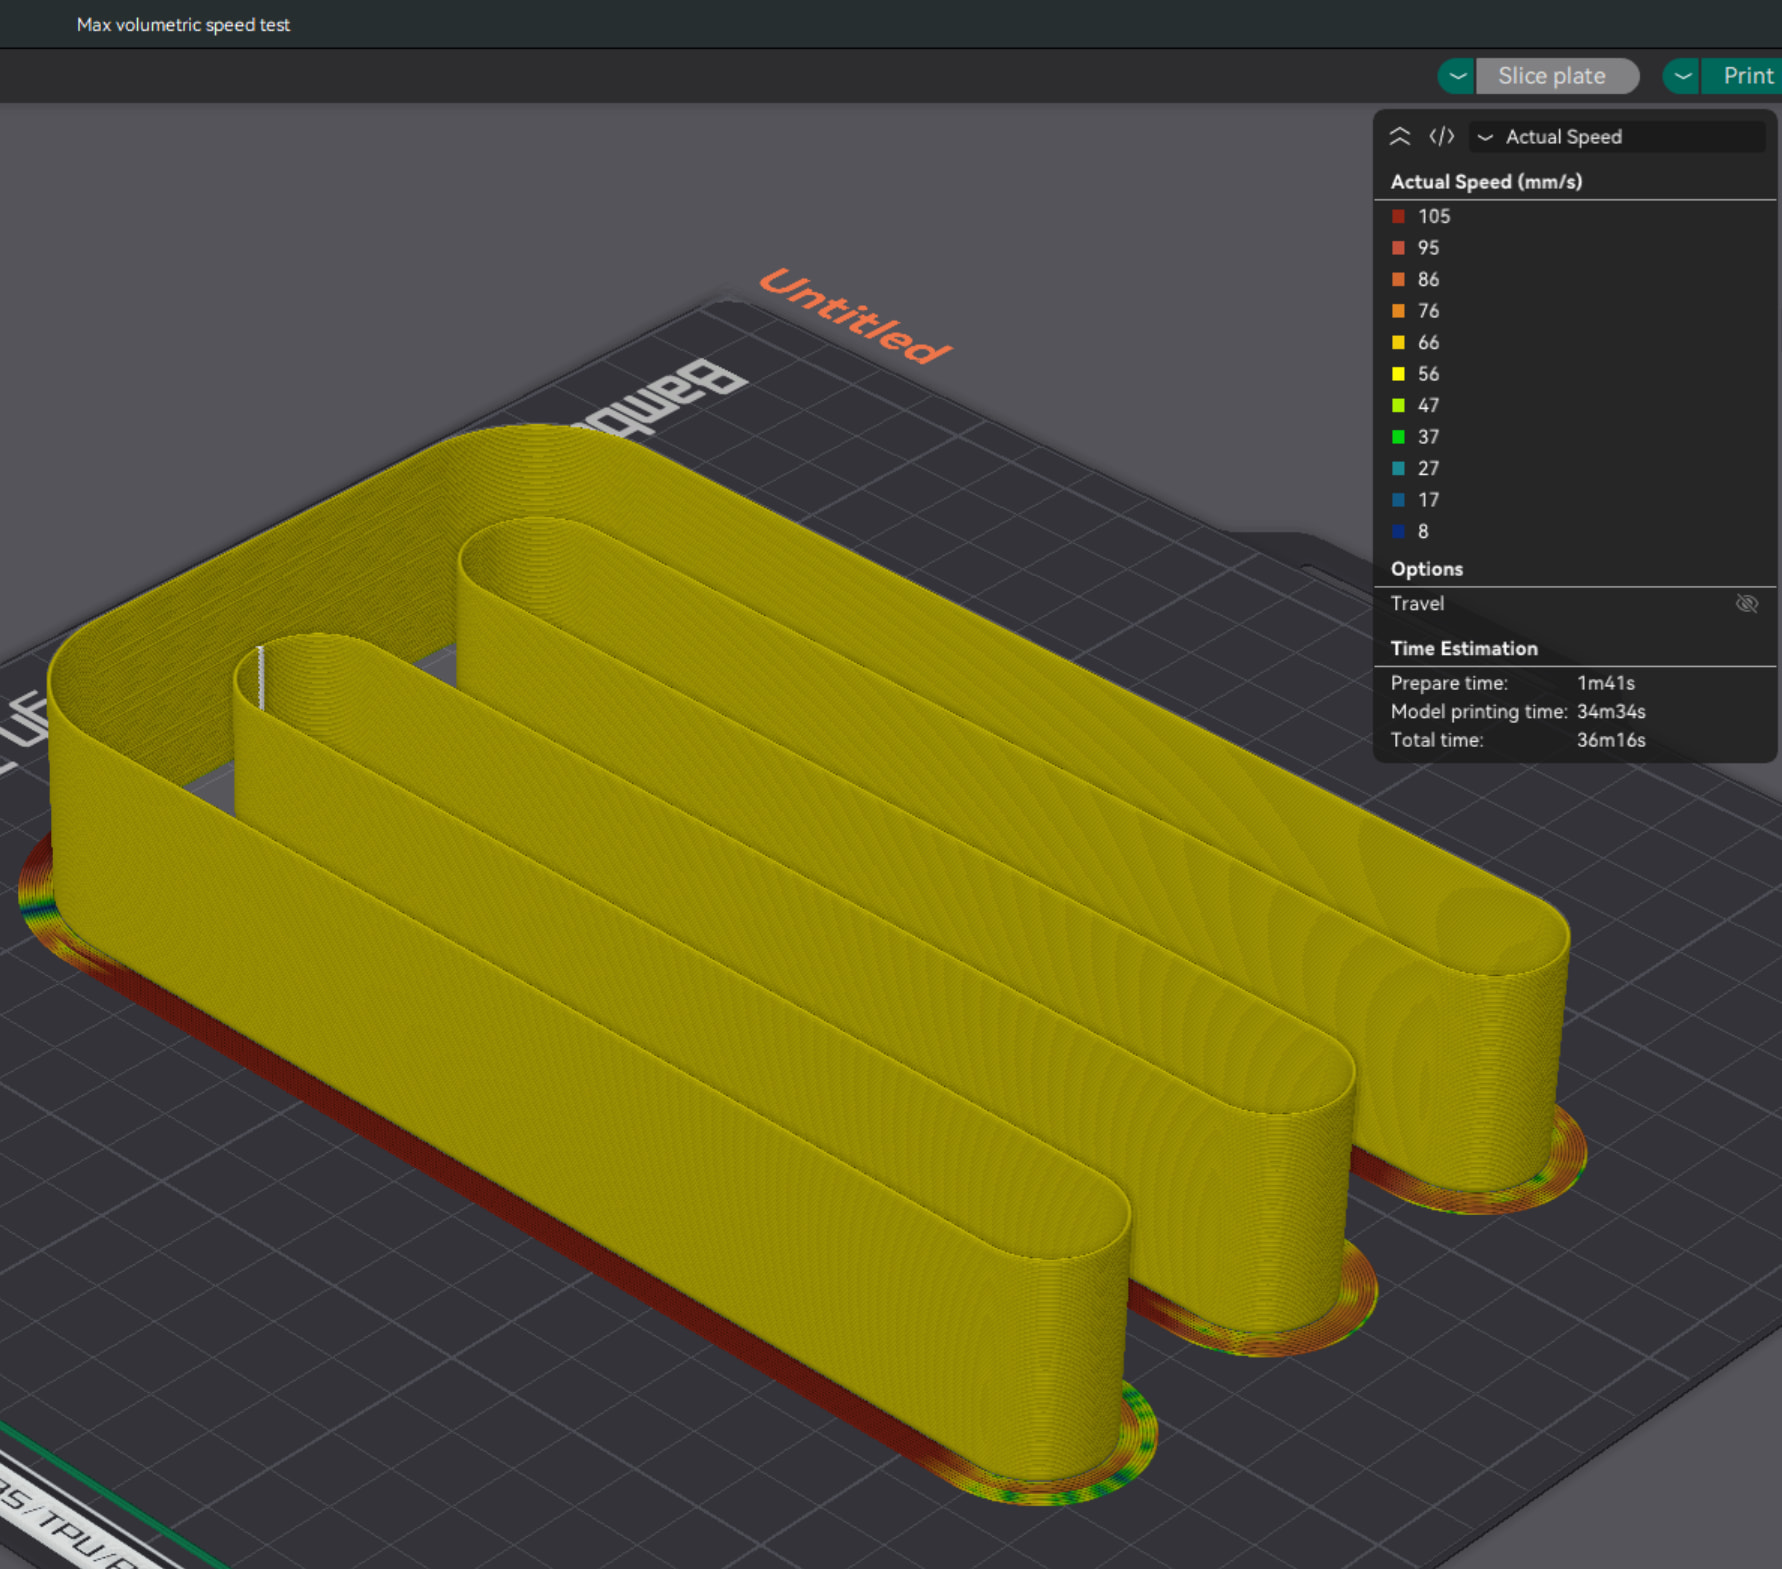
Another example with the max volumetric flow test

Now save the model and load it back in.

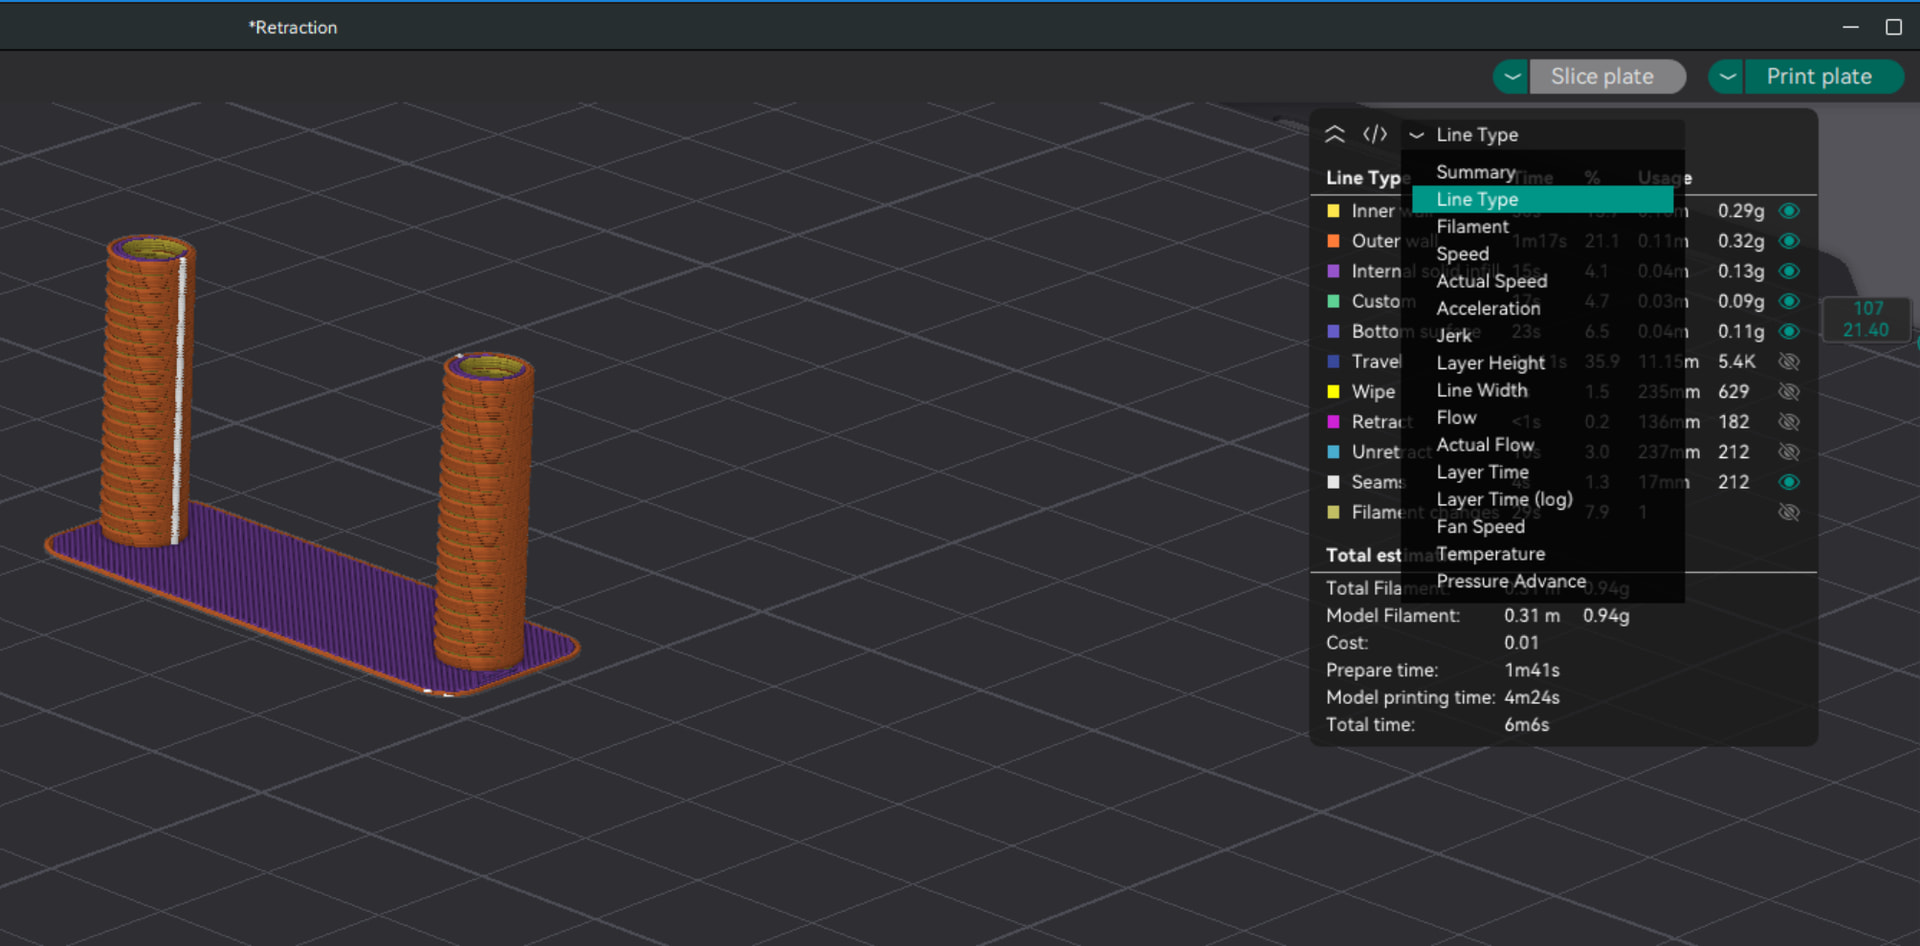
And, of course, with some tests such as retraction speed, there is no convenient preview mode that clearly displays the changing retraction-speed values. So one may not be able to visually confirm whether the test is actually being implemented, yet the tower will still print.

I see this a lot when someone says, “I downloaded an XYZ temperature tower from ABC site…”

That can create a false sense of security that they have a bona fide calibration test when, in reality, they may simply have a static model shaped like a calibration tower.

The model is only the test fixture. The changing G-code parameters are the actual test.

I was not aware of this. Great tip, thanks

Not something I was aware of, but I’ve never tried saving a calibration as a 3mf and loading it into a different slicer. Only ever sliced the calibration tests in OrcaSlicer and copied that directly to the printer using a USB stick. I know this works because the prints show the expected varying results.

I was told to avoid using filaments containing fibres or particles with a high flow nozzle regardless of printer model or brand.

I don’t know where that is coming from. If it came from a YouTuber or some other source, I’d like to see the technical basis for the statement because, as written, it doesn’t make much sense.

Perhaps there was a misunderstanding, because the more common warning is about using fiber-filled, glitter, or other particle-filled filaments with very small nozzles, particularly 0.2mm nozzles. That has a straightforward mechanical explanation. The fibers and particles don’t melt, and if they are large enough relative to the nozzle opening or internal flow path, they can bridge and cause a clog. This is why manufacturers generally recommend larger nozzle diameters for filled filaments.

That said, I’ve tested that theory with quite a few CF filaments through 0.2mm nozzles and, so far, I haven’t experienced a clog. But I also micromanage my filament profiles and calibrate each one manually.

I think two different issues often get mixed together in these discussions: the mechanical limitations of the nozzle and poorly calibrated filament profiles. There is ample evidence that manufacturers put considerably more development and support effort into their standard 0.4mm profiles. When I see blanket statements that a particular filament shouldn’t be used with a particular nozzle, I often ask one question: “Did you calibrate the filament manually?” The answer is usually either no or silence.

If there is one thing I’ve learned from these forums, it is not to accept something simply because you “were told” it or “heard” it somewhere. Verify it in your own use case. That includes anything I say. What works in my application does not automatically translate to someone else’s printer, filament, settings, or application.

High flow nozzles are of course effectively multiple smaller nozzles, so an increased likelihood of clogging is quite reasonable. Also harder to unclog due to the narrow channels.

This is why I’m taking this post, and the earlier one, to task. Claims like this take a particular nozzle design and turn it into a general rule without evidence. That is how “I was told…” or “I heard that…” becomes Internet folklore and eventually gets repeated to newer users as fact.

High-flow nozzles are not simply “multiple smaller nozzles.” There are several different approaches to increasing melt capacity and heat transfer, and their internal geometries can be substantially different.

E3D specifically describes its High Flow ObXidian nozzle for the Creality K2 Plus as using a custom internal geometry to increase heat transfer and volumetric flow, while also explicitly promoting it for abrasive materials such as carbon-fiber and glass-fiber-filled filaments:

Phaetus makes the point even more directly. Its K2 Plus silicon-carbide nozzle is specifically sold as a high-flow design, yet Phaetus lists carbon fiber, glass fiber, steel-filled, wood-filled, tungsten-filled, and glow-in-the-dark filament among its intended applications:

As I stated earlier that does not mean every filled filament will work with every nozzle diameter or every internal geometry. Particle size, fiber size, nozzle diameter, and the particular nozzle design obviously matter. What the manufacturer documentation does show is that the blanket claim that high-flow nozzles are inherently unsuitable or more prone to clogging with filled filament is not supportable.

___________________________________________

For anyone interested in how modern high-flow nozzles actually work, Thomas Sanladerer recently did a useful analysis and test of several different internal geometries. The video is worth watching because it demonstrates that “high flow” describes the objective, not one universal internal design. Some designs split the filament path, while others increase melt-surface area in very different ways. His conclusions are based on physical nozzle designs, extrusion-pressure measurements, and flow testing rather than conjecture:

https://www.youtube.com/watch?v=DdrrrM_IjnA

If there is evidence showing that high-flow nozzles as a class are inherently more prone to clogging with CF, glitter, or other filled materials, please cite the source so we can examine it.