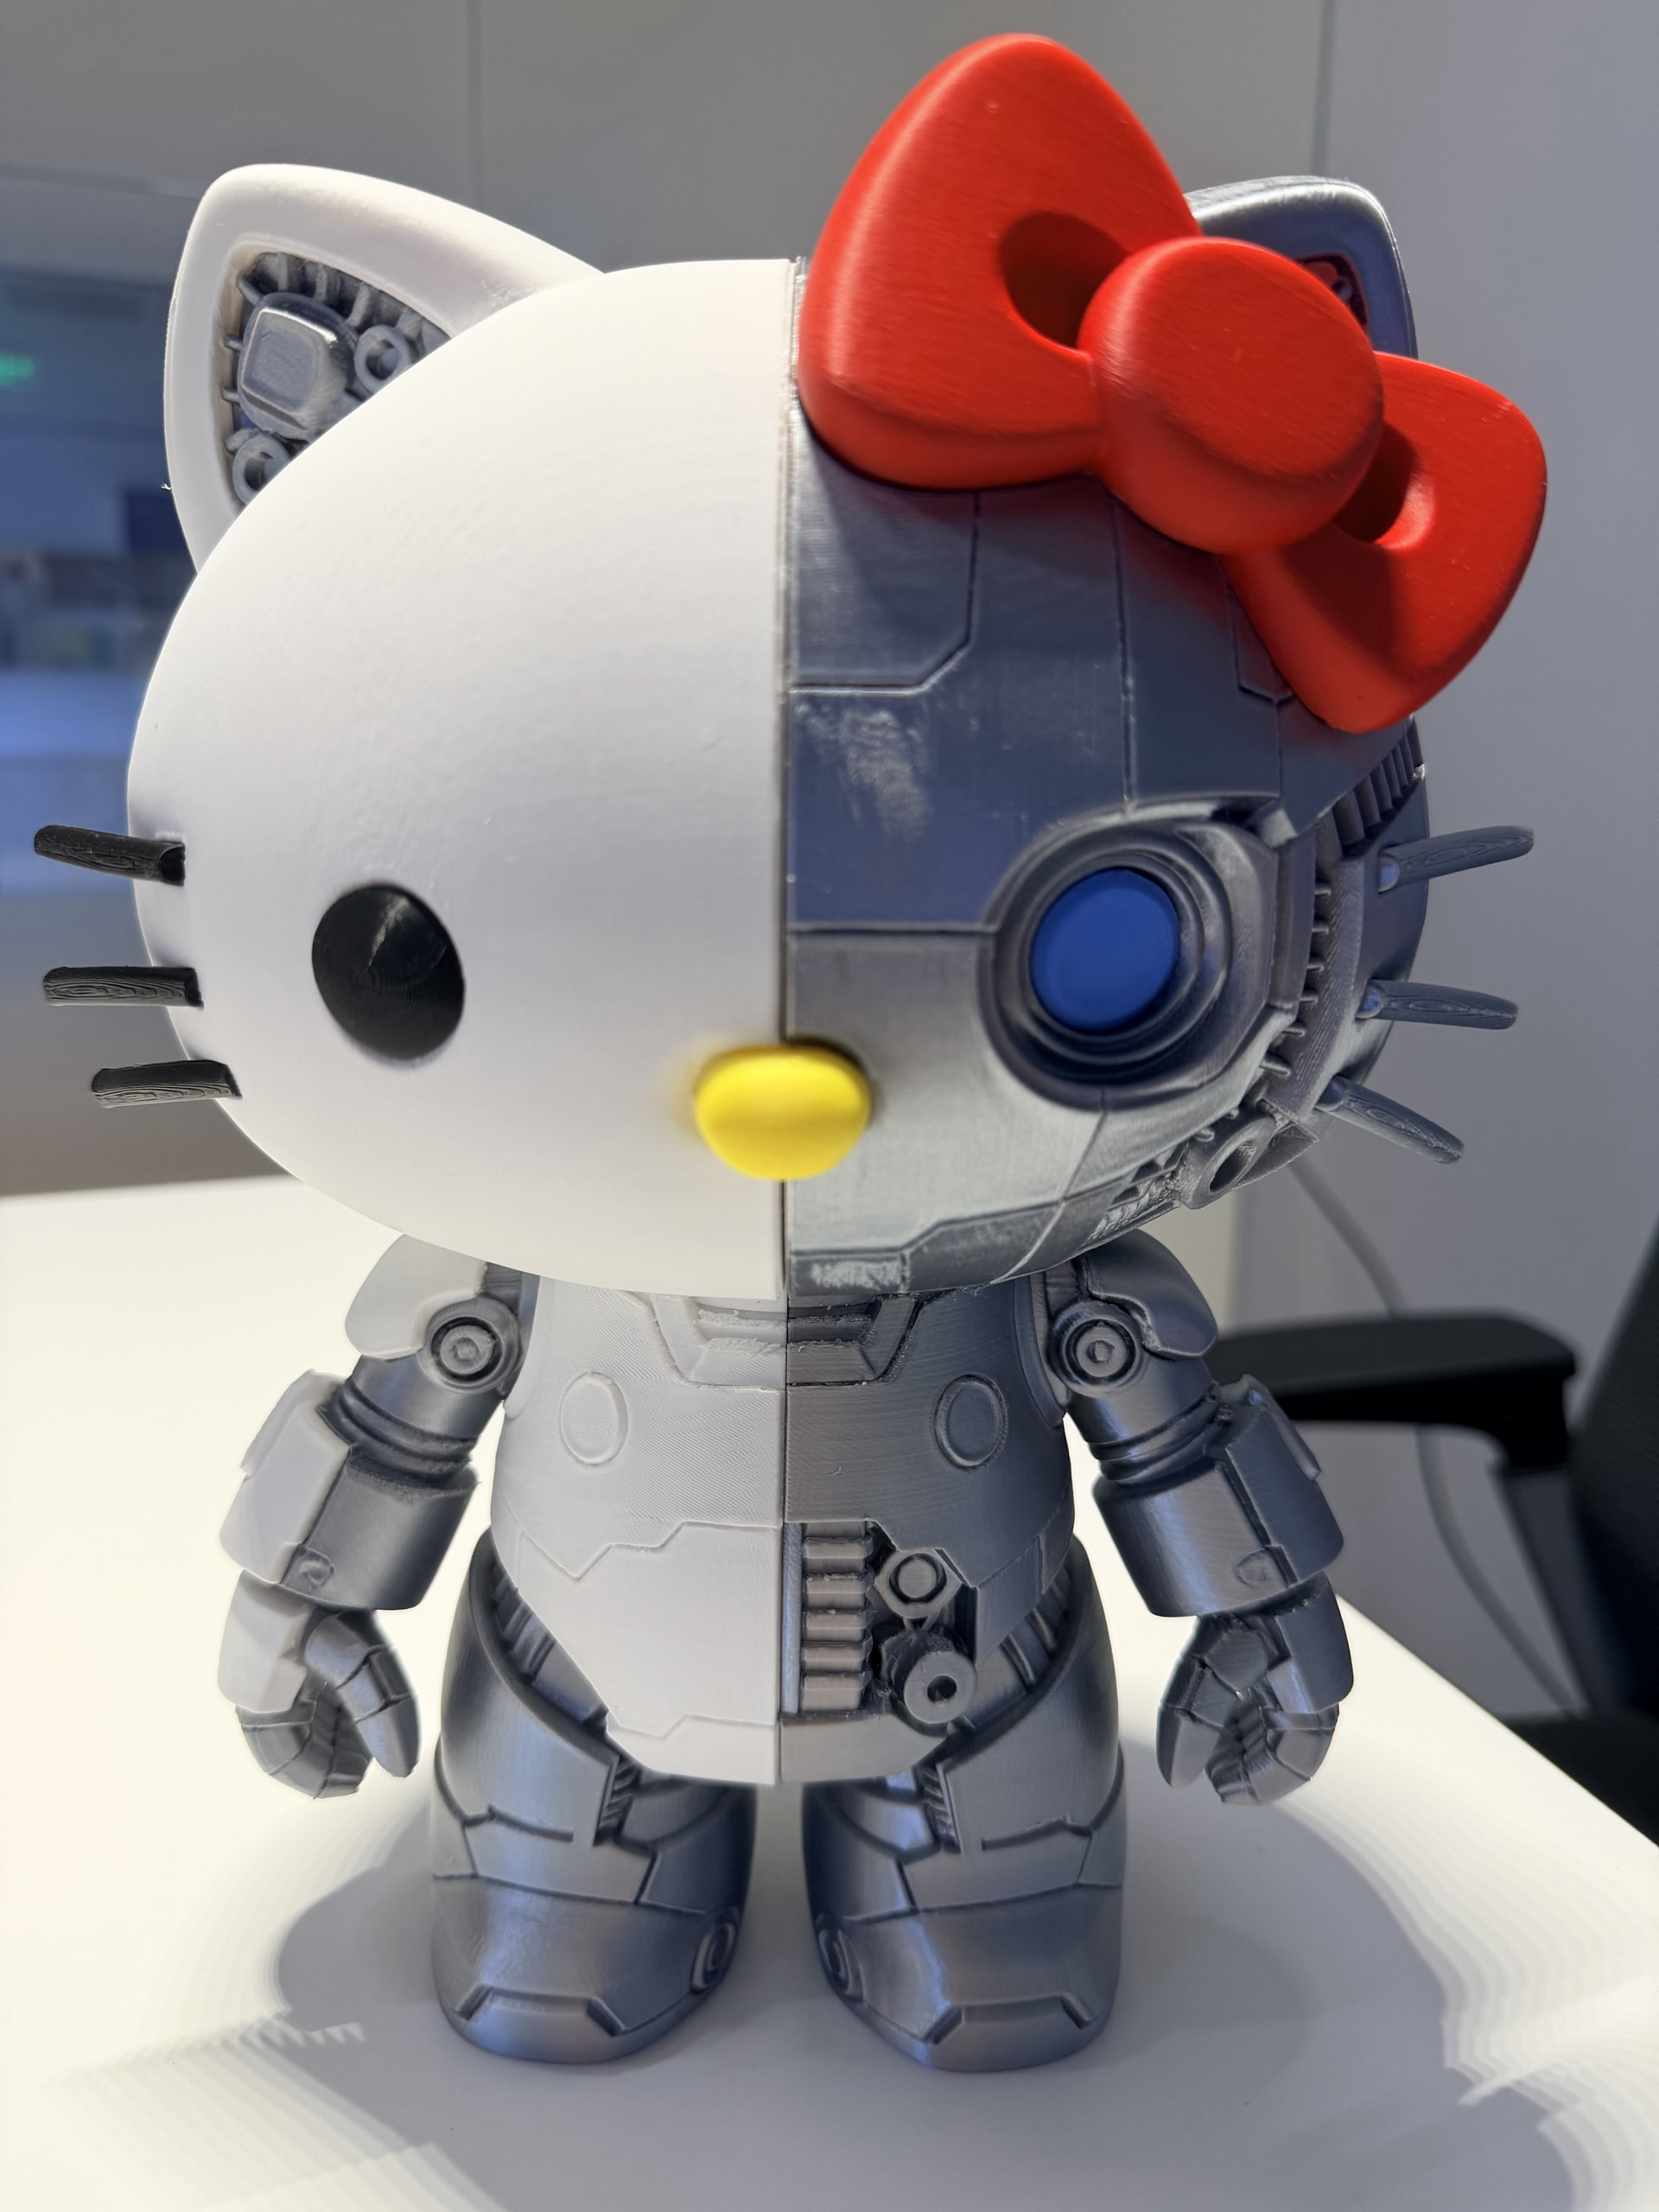
As part of our ongoing material testing at our studio, we recently pushed the limits of surface finish on a complex multi-color model—a Mecha Hello Kitty with intricate mechanical details.
We wanted to test how PLA Silk+ (Metallic Silver) performs alongside standard PLA Basic (White, Red, Yellow, Black) when printed at an ultra-fine 0.08mm layer height. Printing silk filaments at such thin layer heights often leads to stringing, heat creep, or loss of sheen if temperatures and cooling aren’t dialed in perfectly.
Here are the exact profile parameters and thermal settings that gave us this injection-molded quality finish:
Preventing Silk Stringing at 0.08mm: Because 0.08mm layers restrict backpressure in the hotend, standard retraction can cause heat creep. Keeping the nozzle at 220°C ensured fluid extrusion, while capping the Max Volumetric Speed at 12 mm³/s prevented blobbing on the silver mechanical half.
Multi-Material Flush Volume: Transitioning from high-pigment red/black to pure white PLA Basic requires strict flushing to avoid color bleeding. We set flushing volumes to 1.2x the default when purging back into white.
Layer Bonding & Sheen: The combination of a 220°C nozzle temp and slower outer speeds allowed the PLA Silk+ to melt completely, creating a mirror-like robotic metallic finish without sacrificing structural layer strength.
It would have been interesting to compare the results between 0.08, 0.16, and maybe even 0.20. It wouldn’t need to be the full figure - just a representative section. Then you could place the samples side by side and have people look at them from a distance of about one meter to see whether they can tell which one was printed with which setting.
I understand the intention to push the printer to its limits - and I think your post does a great job of showing that. In this context, though, it would also be interesting to see whether people can tell the difference from a viewing distance of about one meter, which is roughly how such figures would be displayed. With Silk filament and 0.08, it would be especially interesting to see whether people can spot any difference on the surface to 0.16.
So, basically, a trade-off comparison:
printing time - waste - quality - can the viewer tell the difference from a meter away.
Disclaimer: If someone doesn’t know what a meter is, they can just replace it with 3.2 feet or 3.240756e-17 parsec.
You may like this chain of trials on minimum layer height:
0.04mm is pretty doable with the Bambu’s but below that, the lower bound issue is flow control.
So to get to a 0.02mm layer height (where layer lines can hardly be felt (!) anymore), printing speeds need to go up. That is how the color mixing sublayer works. Which in turn limits its use to PLA.
Of course, print times explode at these layer heights so multi-nozzle-diameter printing would be really interesting. Unfortunately, artificial limitations I encountered limited my trials to a single combination of 0.2 and 0.4mm nozzles. Haven’t tried layer heights below 0.08mm with that though.


 &
