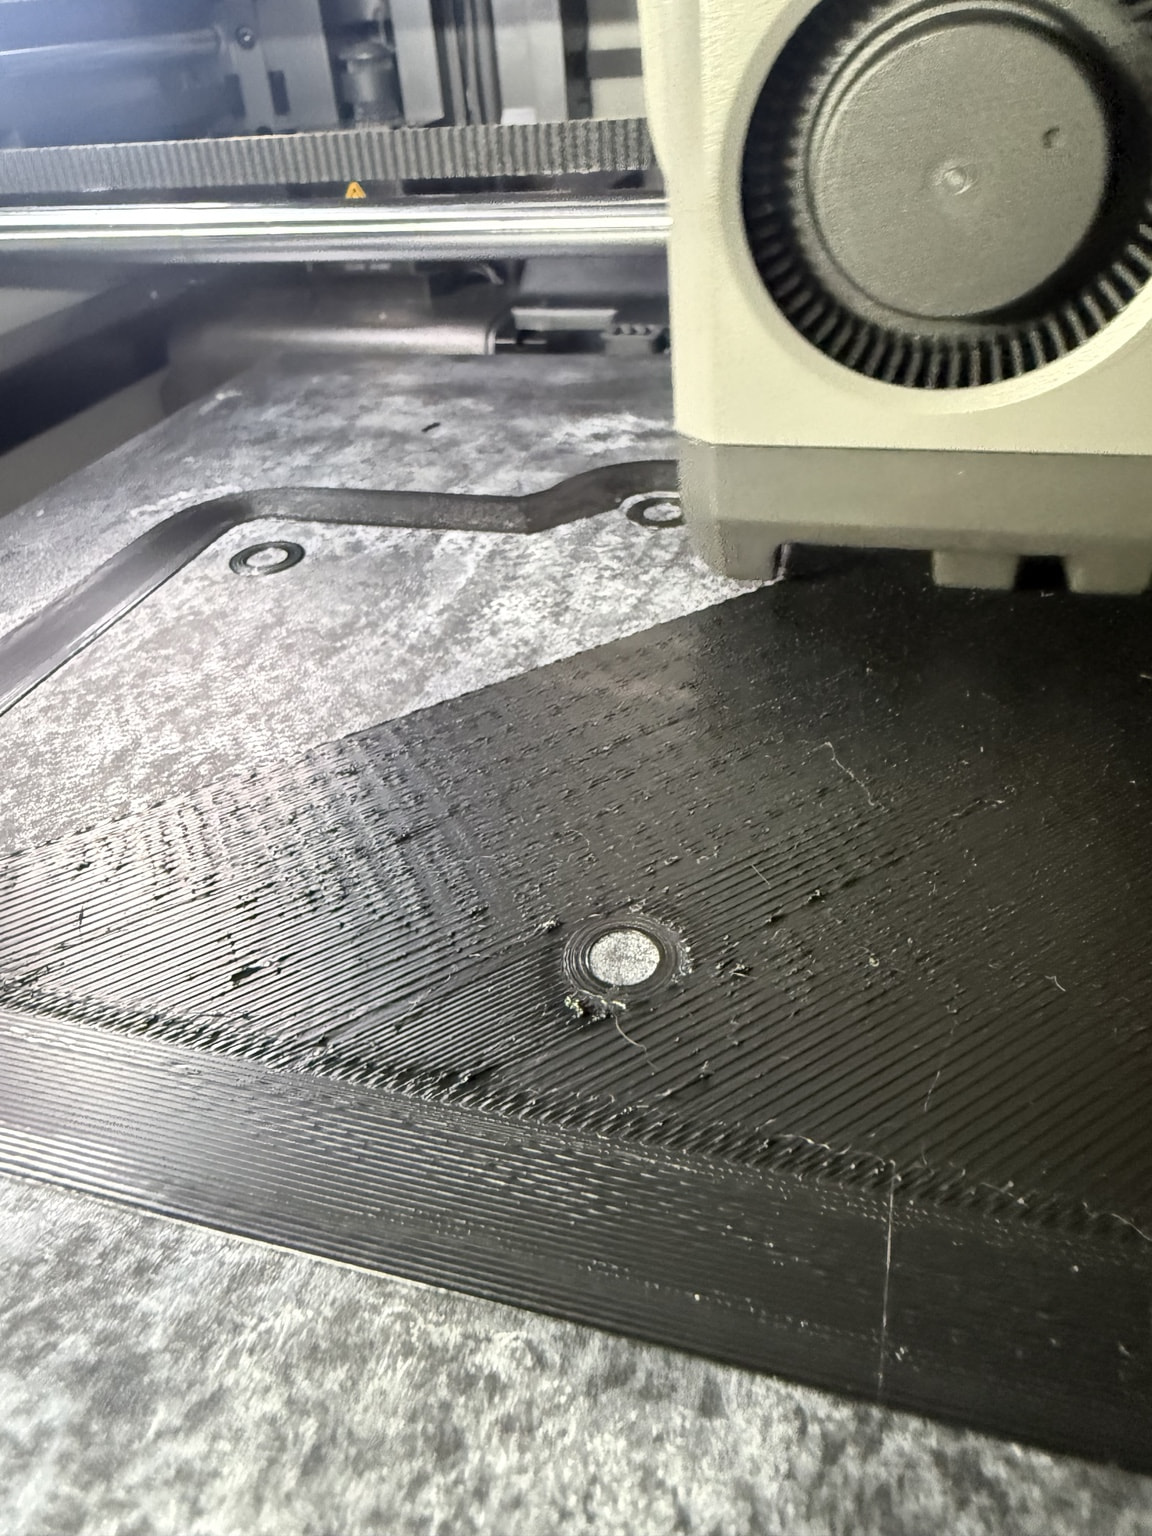
I’m having some print quality issues with ABS on my Bambu Lab printer using a 0.4/0.6mm nozzle. All models print well and I never really have a problem but this model has extremely rough first solid layers and top surfaces; to the point the nozzle is dragging on those layers.
I’ve already performed bed leveling and started calibrating the filament.
Filament has been dried as well in Sunlu.
Current settings:
Nozzle: 0.6mm
Material: ABS
Layer height: 0.24mm
K-factor: 0.038 (calibrated)
Maximum volumetric speed: 16mm³/s
Initial layer: 35mm/s
Initial layer infill: 55mm/s
Internal solid infill: 250mm/s
Top surface: 150mm/s
I noticed in Bambu Studio’s Flow preview that the initial layers and first solid layers above infill show higher volumetric flow than the surrounding layers.
I’m trying to figure out whether this is a flow calibration issue, a slicer setting, or something related to the model itself.
Would anyone be willing to take a look at my settings or possibly test-print the model on their Bambu printer? I’d like to see whether someone else experiences the same issues with the same model.
I’ve been using it set for textured on the engineering plate because with PLA I was never able to get any decent bed adhesion unit it did that (read about doing it somewhere) and it worked well. I’m lost on this one. I can print other files and have no problem but this file which I made in Fusion just does not like the bottom and top layers.
I’ve done both Calibrations listed in the calibration tab.
looks like the first layer flow ratio is a bit high (over extruding). try reducing the Initial layer flow ratio (quality tab) and/or the filament flow ratio (filament tab).
Seemingly random bursts of overextrusion are very often due to moisture… I know noone likes to hear that but… Any stringing in travels as you let the print progress?
Given the only pic is from first layer though, I strongly agree with krellboy - use the proper plate type in your slicer, it actually does matter for z offset absolute positioning, check machine start gcode if you dont believe me/him.