Using an X1c. 3200 hrs. Pla Spaghetti results. I’ve never had this problem. My X1c has always been right on the mark. I print a model twice and the results were correct. On the third print using the same PLA spool I started getting jams. When it would print I could only get about 2 layers before getting the fine spaghetti. I’ve changed filament, different brands, build plates, hot ends, drives and still get the same results. The build pates are clean and glue stick added. have always printed withe top on and door open about 1/2 inch.
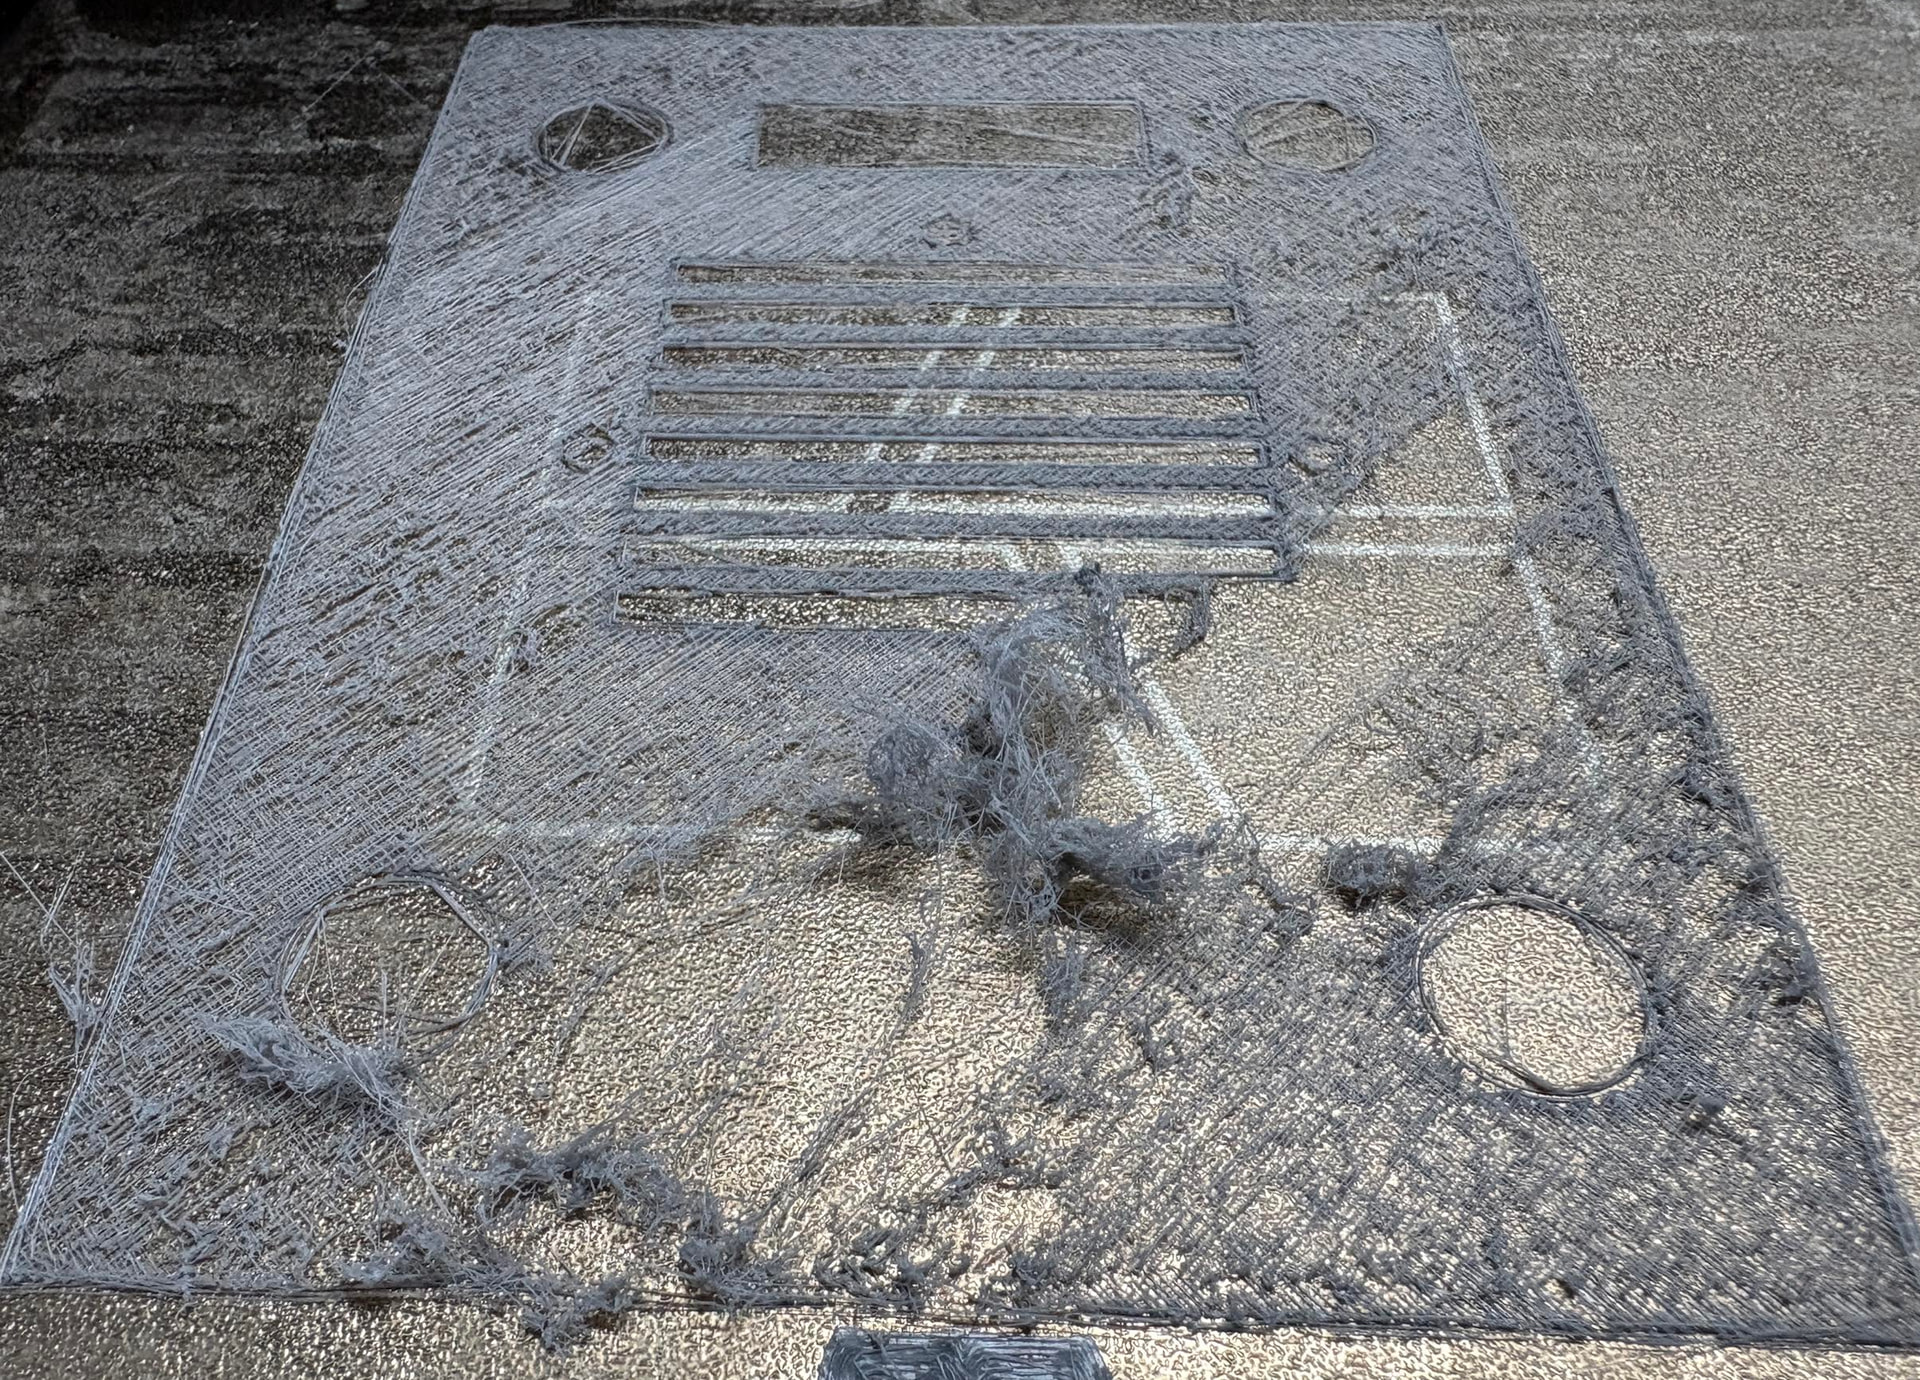
Is the filament DRY? Like 12h in the dryer. New spool doesn’t mean dry. Also, is the build plate really clean? Warm water and a brush may solve the issue. Also, have you tried doing the flow dynamics calibration and pressure advance? And full printer calibration?
Just to double check:
- After an initial jam, prints failed like this?
- You did already try different hotends?
- This also occurs when printing from the external spool only (with a fresh hotend or one which extrudes fine with a direct manual feed)?
In such a case, I’d try to carefully follow the path of the filament from the nozzle back to the external holder. Particular items of note are
- extruder contamination or
- gear/motor problems (play) and the
- filament sensor PTFE-coupler and
- PTFE.
Beware that extruder contamination can travel to the nozzle. So if the extruder contains a lot of residue, clean it out and, before running another trial, do a number of hot hex key cold pulls on the nozzle. Took me days to to get to the bottom of that one when it happened to me…
 &

Dry Filament: The room is at less than 45% humidity. All filament is stored in sealed cereal containers with desiccant and a hydrometer that reads about 25%. The spool that was used in the photo was just taken from the Sunlu dryer (5 1/2 hrs).
Hotends: Brand new.
Feed gears: Brand new.
Filament Path: AMS. PTFE tubes clear. Tried switching to a different reel in the AMS with no better results. Switched filaments spools from container storage. No better results.
I’ve never had this problem in 3,200 hours of printing with this machine.
Also in the print right before the photo the object printed up about 1" and the filament stopped adhering to the previous layer. It was like a stack of threads in a uniform shape.
Do you have a spool in a cereal container that’s reading significantly below 25%?
Poor bed adhesion and layer-layer bonding can be due to moisture. 25% is around where I start having issues with PLA but that can depend on other stuff too. It’s a fuzzy line.
If you have a low-reading spool (like below 20%) you could try that and see if there’s a difference?
Have you double-checked the electrical connections for the hot end?
Just checked the electrical connection. It seemed snug. Ran a test print using same model and noticed that it started out skipping and laying down a very thin line.
I checked and Firmware is up to date.
