Yeah, there’s lots of text, Jay. But most is only important if you want the background or answers to “why?”.
The short answer is it absolutely works. Feeding dry air into the common filament dryers helps to sweep out moist air while helping make the air in the filament dryer more “water hungry”. Filament dries faster and you can dry to pretty much whatever humidity in the filament dryer you want. It removes the guesswork that ambient humidity brought to filament drying.
Not a scientific test but where I had slight stringing and lifting printing PETG-HF parts straight from the shipping bag, after drying the filament using dry air to 21% RH in the Sunlu S2 I don’t. I had been drying to 19% in the S2 with PLA so didn’t even go quite as low with a filament type that Bambu pretty forcefully recommends drying. I also used the PLA temperature and reduced at that. I’ve been drying PLA at 53C so just used that for the PETG-HF too.
And just to emphasize, I can’t tell you how low is low enough. Others have said just dry enough to print well and I agree but have no guidance on where that is for different filament types. The excellent Bambu Wiki entry on filament drying says you want filament really dry for best strength and appearance. At any rate, if you want really dry filament this stands the best chance of getting you there that I have seen so far available now. (May have missed some though if they are out there.)
But not everyone even has moisture issues. Depends on the filaments used and their environment. But for those having moisture issues it should help.
If I’m understanding right, you’re relying on an interference fit to do the seal, is that right? Nothing wrong with that approach, I was just wondering. Water filter housings, for example, generally seem to use the threads to apply pressure on an o-ring, and in their case it’s the o-ring that does the sealing. Then again, I suppose that would be yet another part to source… so it works without, then all the better.
That’s exactly what’s going on. The part of the filter disk where the gasket rides is actually pretty rough. I had to use support on that because of needing to print the keyways that align the filter disk.
So it’s rough. But I left a gasket thickness of thread clearance so the gasket outside edge rides against relatively smooth wall. Similarly, the gasket inside edge rides against a smooth outer wall of the filter disk. Those are really the sealing faces now. The channel the gasket rides in is the same width as the gasket so when the bottle gets screwed in, the bottle compresses the gasket and forces it against the inner and outer walls. That makes the seal.
In the directions I mention using superglue on that rough area of the filter disk where the gasket rides, but I don’t think it’s really necessary.
Apologies I didn’t get to this sooner, Never. That is excellent you saw that. I saw the same thing in bits and pieces. These are some of the hidden bits that have made filament drying such a mystery.
Hopefully we’ll see some builds and results posts that should provide more proof for others.
And I did clearance the threads a little but that was just knocking down the points on the threads to give more clearance for the filter disk. I didn’t know how to open them up more in other dimensions.
With the bottles I have it’s still a close fit. I hope there’s not much variation bottle to bottle or it could possibly be an issue. But while it’s close, there just isn’t much play. There is still some and the bottle isn’t tight in the threads at all. But I don’t know about trying to seal the threads with superglue. Maybe the thin well brushed out, but I didn’t recommend it and the thread model I printed first to test was very tight with no sealing at all. And that was even printing with 2 walls instead of 4, and 3 floors/ceilings instead of 4. But much smaller part so not as many opportunities for leaks.
But that’s why I included the test piece for bottle threads. It’s disabled in Studio but if people want, they can print that at small cost to check a bottle to make sure it fits.
If you’re using fusion360, a way to do it is to select the thread surfaces and then do an offset of, say, 0.2mm or whatever it is you decide. I found it works overall better at loosening the threads up than just truncating the points. If you want, I could point you at a youtube that walks you through it.
I set the time index to the offset method. You kinda have to see it demoed to catch the idea. It’s a very powerful technique, but luckily easy to do once you grok it.
Anyway, just background info. If your model works as-is, then I suppose it’s overkill.
Yes, a bit later for one of my COTS filament dryers. At the moment I’m going balls out on an almost industrial version of this concept for my blast oven, but I’ll circle back after I get that working. The ultimate paradigm is keeping a drybox dry while you print from it, and yours could be an all-in-one drier-drybox which dries and guarantees that. For instance, the AMS can only fit so much desiccant into it, and yours could blow dry air into it and guarantee it stays dry inside.
Hadn’t even considered that but it probably could do that and with a very low flow since it would probably just be left running, or put on a timer to run every so often. The stock desiccant does pretty well though but you probably wouldn’t even need it.
Probably other uses for “dry” air, too. What I’d really love would be to find those same hygrometers but with a lower read capability where we’d actually have a good handle on the dryness level instead of only when it goes above 10%. Knowing the actual exit humidity might make it applicable to other uses.
I looked at the threads and I am thinking they are probably loose enough. I can wobble the reservoir a little with the threads engaged fully the bottle lip not up against the gasket. It wobbles enough that I get concerned any looser and it might be too loose.
There is a thread model included where people can test the fit without printing a full base. Without knowing how consistent those bottles are though, it’s impossible to know for sure there is enough clearance for all of them, but those bottles look fairly precision around the threads.
If anyone has a tight bottle, I’ll be happy to loosen up the threads since it would prove a need, but I think it might be confusing to even have the choice.
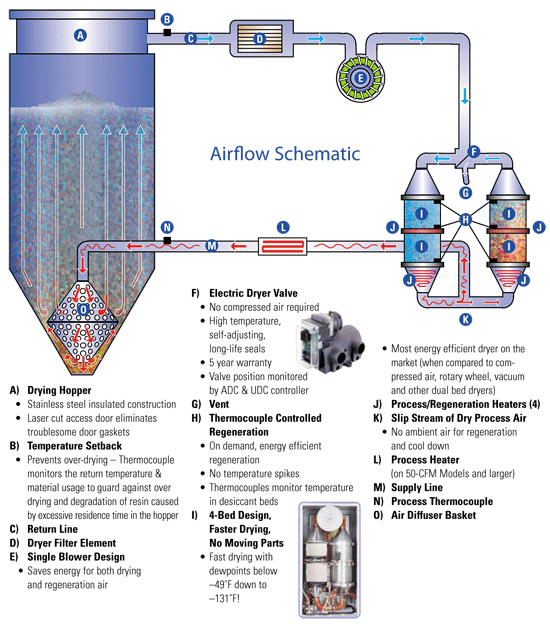
Hey @NeverDie - was looking to see if anyone else might use air drying in the plastics industry and yes they do. They don’t have much in the way of real details but use desiccant beds to dry air that is used to condition plastics before injection molding. They have all sorts of sizes and capacities and the customer testimonials are interesting. There’s even a truck fitted with their units that is available for companies that get “wet” plastics or something happens that raises the water content. They automate desiccant regeneration with a dual arm / 4 bed design. They also have compressed air dryers but not much detail. They want to talk directly it seems. Still, it looks like this was all pioneered years ago.
When I last went looking the least expensive brand new ones I could find cost around $1,000. IIRC, that delivered around 5 CFM of ultra dry air and achieved continuous duty cycle by switching between columns. When one was depleted, it would switch to the other and recharge the depleted one.
Worthy of note in the picture you just posted is the “Fast drying with dewpoints below -49F down to -131F.” Left unsaid is whether it dries the plastic pellets all the way down that low, or whether it uses air that dry merely to speed up the drying process. I still haven’t found a satisfactory answer to that question.
The dew point defines at which temperature would be able to condensate.
It is NOT any fixed temperature you could measure in the system.
It is a very important value with no real merit - sort of.
In a humid environment water will condenses on a surface or on particles/droplets in the air once the temperature goes below the dew point.
You can see this nicely in the summer when you grab a cold drink from the fridge.
In a closed system not only the dew point matters but also the air flow and possible restrictions where turbulences might form.
Your system might be still far away from the dew point but in a few small spots it might not - condensation happens.
A large difference between operating temp and dew point ensures that all moisture that is released will stay IN THE AIR - it can’t condensate anywhere.
The benefit of that is that the removal of this moisture can work much faster and far more efficient than with a dew point hovering 20 or 30 degrees higher.
Freezer burn is another example of dew point usage.
The air in the freezer gets really dry as all water condenses on those evaporator coils.
And unsealed food will then start to dry out, even through the frozen sections.
The ‘burn’ is actually freeze dried not burned.