I doubt they dry the plastics to that low of a water content but don’t know that for a fact. I think it’s for the same reason I found - it speeds up the drying. Only thing I base that on is they have equipment in there to make sure plastics don’t stay in the drying chamber too long where it can undergo degradation. I bet they are running high air flow and high temperature to get the throughput on the plastic so it can be used for production. But don’t know that.
I think it was you that pointed to the air dryer units that just supply dry air and that’s the basis for these air dryers. The automation (which I think you also suggested) just makes it turnkey. It’s actually the automated and closed loop version of the Arid Air. I don’t know what desiccant they are using but maybe molecular sieves with that low of dew point?
Anyway, I just thought it was interesting the plastics industry needs to dry their material too, they are using dry air and heat, and filament makers probably even use the same equipment on their feed stocks.
then you find it described as using activated alumina, with an option for molecular sieve. Silica Gel beads become very inefficient at very low RH’s, which explains why they are dismissed.
I setup version 0.1 of my desiccated air filament dryer today. I’m calling it version 0.1 because at the moment it’s more like a dry fitting than a proper build. Nonetheless, I can see that it is generating dry air and pumping it into the blast oven. Most likely it has leaks. I’ve segmented it with a number of ball valves, so I’ll try using a pressure sensor to help track down where the leaks might be coming from.
Using TH sensors I can show that the air coming out of the compressor has a lower dewpoint than the ambient air, and I can also see a further drop in the dewpoint for the air which then subsequently passes through the desiccant.
One unexpected problem: I have three different TH sensors in the heated chamber that comprises the filament dryer, and all 3 are very different in the humidity that they’re reporting inside there. The temperature inside it is a steady 60C. Two of the three humidity sensors supposedly have an operating temperature range that goes up to 70C. The third one has 60C as its nominal upper end of its operating temperature range. I don’t see anything on amazon which looks any more promising, so I’ll just have to roll my own if I want to monitor the humidity there, which I do very much want to monitor.
I picked up this Sensiron SHT85 breakout board:
It claims an operating temperature range that goes all the way to 125C, so I’m hoping against hope that it will do a decent job of measuring the humidity in the 60C drying chamber.
No reply, so I’ll attempt to answer my own question. I think it’s because typical drying equipment understands temperature, and that’s where it ends. So, you set a blast oven to achieve and maintain a fixed temperature, and it uses PID to do that very well. But what you really care about is both temperature and RH in the drying chamber. That’s why even though in theory you could build a blast oven to achieve a certain RH, it would be foolish to do so: it might keep raising the temperature to achieve the RH target, but in the process cook and then melt your filament.
So, what does all that mean? It means what we have today. You set the temperature target on the blast oven, and it’s your job to guarantee that the make-up air going into the drying chamber has a dewpoint no higher than some fixed value that you calculate will give you an RH no higher than what you want and need inside the drying chamber. Therefore, I would argue the truth is exactly the opposite of what @user_3026326371 contends. It is NOT the case that dewpoint has “no real merit.” Rather, it is a criticalnumber to know about your make-up air, and if you don’t know it and manage it, you’re at risk of undermining the entire operation.
But even more true is that you probably simply want the driest make-up air you can economically make going into your heating chamber, because then the drying time will be shorter and/or the filament will be dried even better. So, how do you express that? The easiest way is still dewpoint. And that’s what we see in the literature.
Which is exactly what the Arid Air dryer does. The only thing is after some amount of use (and I didn’t see it even after drying 26 spools) is the humidity of the make-up air will start to increase, which while not as efficient as when the beads are fresh still results in better drying than with ambient air. Few locations see 11% RH in their ambient air. Antarctica, maybe?
(That’s qualified about not seeing any increases because it was an instrumentation issue. The exit air was probably increasing in humidity even though I didn’t see it simply because the hygrometer monitoring exit air stops registering below 10%.)
In my Version 0.1 I was throttling the air just after the air pump, but as a temporary workaround to current unidentified leaks in the system, for version 0.11 I’m going to move the throttle to just prior to injection into the heating chamber. That way I’ll also be better able to measure the flow going into the chamber, which is what matters most, instead of just the amount of flow going into my (currently) leaky system. The side-effect is that this will pressurize almost the entire system, which will increase the pace of the leaks, but so be it. Also, the current drying chamber has some amount of back-pressure to it, and I don’t think much of my version 0.1 dry air is able to overcome that to get inside the chamber.
I’m doing all this in baby steps, in part because it takes some amount of time for the effects of a change to fully manifest in the drying chamber.
No merit… - Ok, let me try to explain WHY I said that:
The dew point of a given body of air is the temperature to which it must be cooled to become saturated with water vapor.
This temperature depends on the pressure and water content of the air.
When the air is cooled below the dew point, its moisture capacity is reduced and airborne water vapor will condense to form liquid water known as dew.
When this occurs through the air’s contact with a colder surface, dew will form on that surface.
So why does something THAT important does NOT have any real merit for our low level attempts?
We heat the air to at least 55 degrees Celsius.
If you check the air’s capacity of taking on water at just this temp and not higher you will find that the air is unable to take on or hold much water.
The humidity levels (in OUR application) can go basically only go down in two ways:
Replacing the saturated air with air of lower humidity level.
Removing the water from air using desiccant, cold traps, molecular sieves or whatever one has at the disposal.
Number one can be done like number 2:
We either circulate the hot air through desiccant or cool the air prior to the drying if the temps are too high as the desiccant won’t work at too high temps.
OR we dry/heat the incoming air so that its moisture level will be below that of the ambient air AND the air in the drying chamber.
The dew point in this application really does not matter as literally all parts of the system stay above the dew point, nothing can condense on surfaces.
If we do it the other way around and DO use a cold trap or similar the dew point DOES matter.
Simply because in THIS application we have to make the water condense on the cold trap.
That only happens if the trap is BELOW the dew point, preferably way below as this increase the condensation effect.
In industrial applications for drying the dew point is always mentioned and properly calculated.
Here it is a vital factor for process control while WE only really care that the filament dries fast, well and to a low enough moisture content.
We don’t need to reach and maintain a specific moisture level in a product
If you state that in our application the dew point IS of importance than the air temperature and its moisture content has to be seen with equal importance and monitoring - which we already do.
What we don’t is doing anything that requires to know how bloody low the dew point is - we only need to know it is low enough for the desiccant to work.
Starting to pick up some nuances with more experience with this thing. When you put a spool for drying in a filament dryer the humidity rises at first because water is coming off/out of the filament faster than it gets swept out by the aquarium pump flow. Depending on ambient humidity, you can knock a fair amount of time off the dry by “burping” the dryer to just do a wholesale change of air to get rid of excess moisture.
The aquarium pump is a fairly low flow and filament dryers are fair volumes so effective as purging the filament dryer with dry air is, when the filament dryer humidity is higher than room air, that air exchange by burping helps get rid of even more moisture.
It’s not required. Just noticed it and have started burping the filament dryer during humidity spikes. After the humidity spike, the aquarium pump flow is fine for purging out the humidity.
Another thing is I’ve been backing off on drying temperature a little to see how that affects things. With dry air it seems temperatures can come down a little. Had some black PLA get a little sticky with other loops around the spool so want to avoid that. No numbers yet and this one will need weighing since chamber RH might not be pushed as high at too much lower temperatures. So far knocking 3 degrees off temps has had little effect on drying but no problems with the filaments yet. I need to do weights to know better.
FWIW, I just today noticed this guy plugging his closed loop system on the anycubic models collection:
He claims it works, at least to his criteria of success. He says he’s heating his interior air to 75C. I have my doubts as to how thorough a job it does at drying, given the temps and the seemingly small amount of desiccant, but to his credit it’s also the first closed-loop hobbyist build I’ve seen to date.
He doesn’t give much detail but it should work. He did say he got humidity in the box down to 15% - fairly low but there are some issues I see. The fan is in the warm air flow and the desiccant gets heated. It’s probably hard on the fan and warm desiccant has reduced water capacity. I agree on the low volume of desiccant but he might be in a dry environment where he doesn’t have to change it out a lot?
Fans are happiest and last longest in cool air and at least silica gel beads have highest water grabbing capacity also in cool air. Never been a fan of heating silica gel beads unless you want to drive water out of them.
But no reason it shouldn’t work at least to some extent. I’d rather purge dry boxes with dry air rather than hang heaters and fans on them, though. Powerful heaters aren’t something I want to leave running unattended.
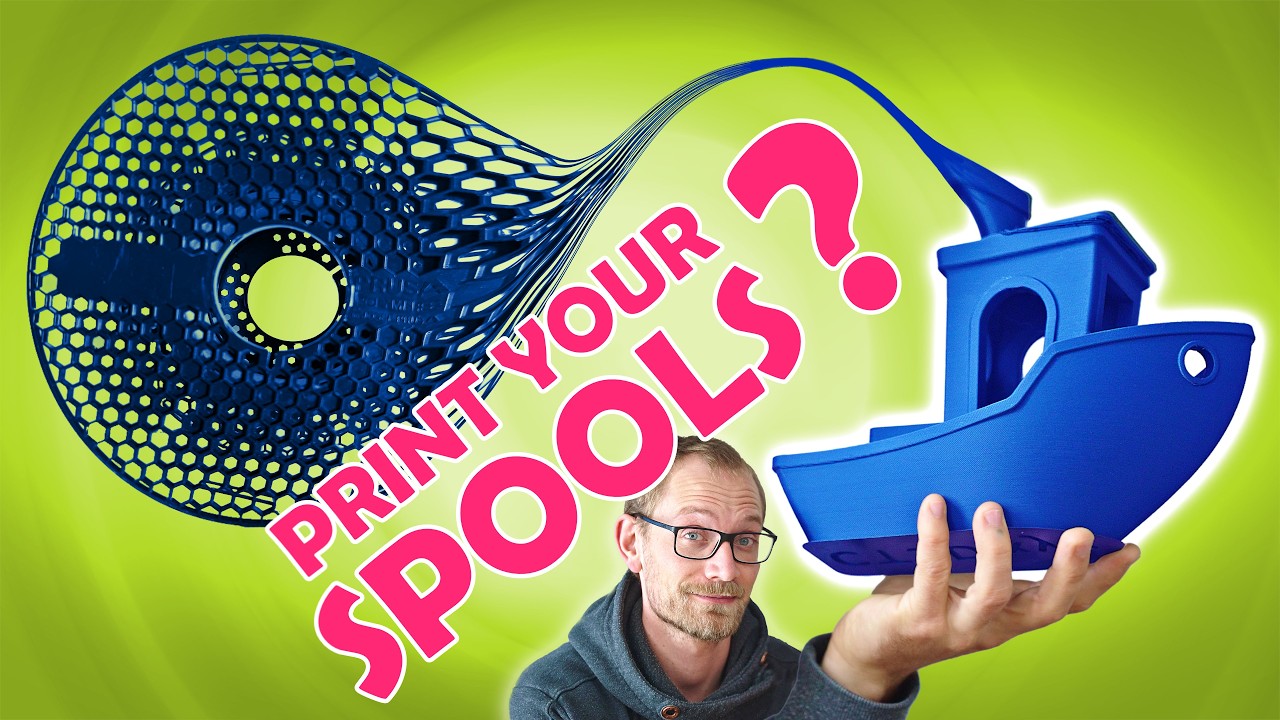
Although we all recognized how cardboard spools can act like moisture sponges, thereby putting a higher burden on drying a spool of filament, I hadn’t really considered that plastic spools might impose a similar burden. Well, at least in the case of ABS spools, it’s a thing, as demonstrated by Tom in his video about shredding down ABS spools into granulate and then re-extruding it as recycled filament:
It turns out that even Tom also forgot about how an ABS spool might hold a lot of extra moisture, but it became obvious when he extruded the granulate and he found all kinds of bubbles in the filament, because the moisture became steam during the extrusion process.
All of which begs the question: what’s the best kind of spool to have, especially if you’re prepared to rewind store bought filament onto a better spool. Cardboard? No. ABS? No again, as just proven. Metal? Maybe.
Guess what plastic the Bambu Lab spools are made from? Yup, ABS. Ouch. I didn’t pay attention earlier, but but rewinding onto a Bambu Lab spools now almost seems like shooting myself in the foot. The allure was the perfect fit for the AMS.
What would be the best kind of plastic for a spool to be made out of? Which plastic just naturally stays the most dry?
I’m not sure plastic or cardboard matters much but have only thought about this a little. Reasoning is once filament is wound onto spools, the spool sees the same environment as the filament. If it gets dried in a blast oven before packing, the spool sees it too. If it gets dried by the user, the spool sees that, storage situations, etc.
User drying will see a little more water load to remove, but it’s also another water sink for any humidity that finds its way to a “dry” spool of filament much like desiccant in a poly cereal box with filament is also a water sink for any humidity that finds its way in.
I think ultimately it’s just an extra load of water to remove when drying but once dry can actually be a small built-in desiccant?
A new interesting topic has appeared. If a dry spool can act as a desiccant, the opposite can be true. If we are putting already dry refill filaments rolls onto the Bambu spools, we could be introducing a source of moisture if the spool has been left to sit in a humid environment. Not sure if it’s all that critical, but is interesting thing to think about when we are throwing refillable rolls onto spools and then storing them on containers. Just need someone to dry a spool and weigh the water loss
Absolutely. It works both ways. But I also think intact spools aren’t a big problem. Reason is surfaces should be fairly smooth and not very porous.
The spools are injection molded and get a pretty smooth surface finish that shouldn’t have many pits and holes increasing surface area. It’s like the holographic and carbon fiber patterned build plates - the plastic takes on the surface characteristics of what it solidifies against.
Grinding them up as granules to turn back into filament and as filament the plastic gets lots more surface area and shorter paths to the interior of granules.
The big one seems to be the extrusion process into filament. Micrographs of filament show very rough and pitted surfaces leading to large surface areas for water. As a spool it should be much smoother with less pitting and less affinity for water.
I can see how the porous vs non-porous surface finish on, say, an ABS spool could affect the rate of uptake or release of moisture, but if I was respooling store bought filament onto a Bambu spool, drying it and then storing it, I’m guessing that I won’t entirely succeed in drying the moisture in the spool, because the rate will be slow. However, when it’s all packed away and in storage for a long time, maybe then the internal moisture has enough time to migrate outward and affect the moisture content of the dried filament? It’s the reverse process of how the spool got wet int he first place. By that I mean, most industrial processes would dry the ABS granulate used to injection mold the spool, so it should have started out life as dry. Nonetheless, afterward, the moisture slowly found its way inside of it.
I can’t say for certain on that but I do think seeing the same environment as the filament might make it moot? But put a dry refill on a wet spool and hard to say. @RandomKhaos had the suggestion to just test weights before/after drying and see. That would tell the tale of how much water it can be in practice?
Well I tried with one of my Bambu high temp reusable spools, which is apparently a ABS and PC blend material. It’s a new spool I got two weeks ago that I hadn’t used yet; it’s the only one that isn’t in use and in a dry box. I dried it in my filament drier at 70c for 6 hours and it had no change in weight. So not the best test since the spool may not have had enough time to absorb moisture, but I figured I’d at least give it a shot.
 The temperature inside it is a steady 60C. Two of the three humidity sensors supposedly have an operating temperature range that goes up to 70C. The third one has 60C as its nominal upper end of its operating temperature range. I don’t see anything on amazon which looks any more promising, so I’ll just have to roll my own if I want to monitor the humidity there, which I do very much want to monitor.


 Ouch. I didn’t pay attention earlier, but but rewinding onto a Bambu Lab spools now almost seems like shooting myself in the foot. The allure was the perfect fit for the AMS.
