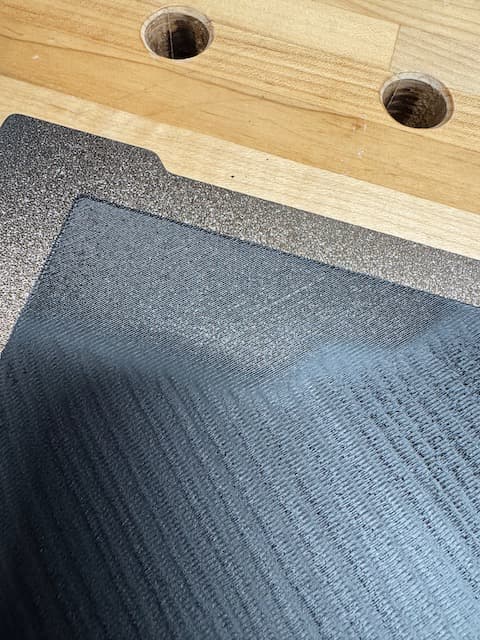
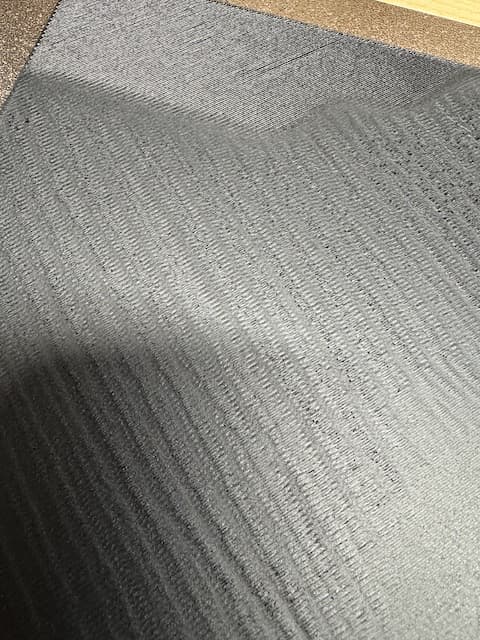
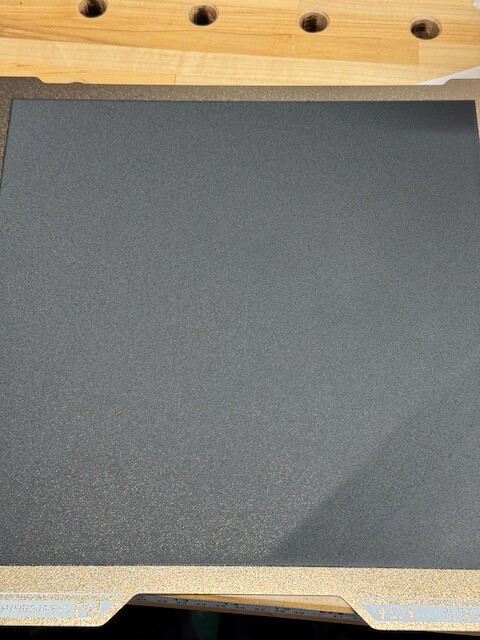
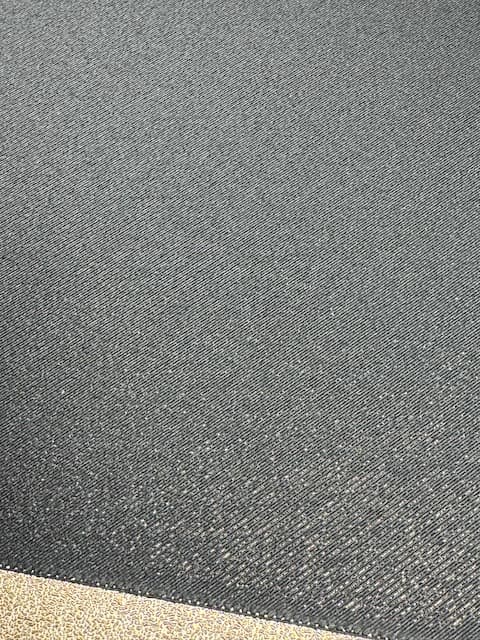
Bambu seems to not have an idea. After a while with support (no solution) the service person told me they will consult with their team to see what is next. Like I said though I would say after using a Dial Indicator, my bed is 90% level, but only on the left nozzle still, there remains some weird defects on certain parts of the bed. Right nozzle prints in those areas just fine.
First layers are great, now if only I could get my top surfaces to look as good. They always seem to have some kind of under extrusion somewhere.
I further dove into my first layer issues. As a last resort, I replaced my 0.4 HF nozzles by 2 brand new ones (non-HF). To my big surprise, my first layers are now perfect. Both with left and right nozzle. Go figure…
I’m sort of thinking this may be my top surface issue as well. The original hot ends look great when installed but both of my HF hot ends seem slightly skewed, kind of like they’re slightly bent. Judging by how parallel the top of the heat sink is to the part of the tool head right above it. That’s how they came though so I didn’t think much of it till lately.
Same here, especially the left HF nozzle looks like it’s not parallel with the rest of the hotend assembly.
I just swapped my HF 0.6 hot ends in last night and they’re definitely not as crooked looking as the HF 0.4’s that I had in there.
I’m having problems with ASA-CF first layers in the same place on the print bed every time. This occurs on both textured and smooth PEI build plates in the same location, which leads me to believe it’s not the build plate. PLA prints a perfect first layer.
Any suggestions? Could it be a build plate heating issue?
high resolution photos would be helpful, more details of your filaments would be helpful as well. you mentioned about different plates, but have you tried different prints? more importantly, have you done your High Temperature bed calibration?
Apologies, the board won’t let me upload photos nor include links – any suggestions on how to share photos?
I tried a proper print which failed repeatedly, which is why I moved on to first layer printing. I was not aware of high temperature bed calibration; running that now.
The high temp bed calibration significantly improved the consistency of the first layer. It looks much better than before. However, about 2/3rds of the first layer appears to be extruding too high, with there being clear separation between each filament line – they did not fuse together at all. I’m going to reprint in case it was due to foreign material being stuck to the nozzle during bed probing.
yeah definitely clean the nozzles before you do the high temp bed probing. residues might ooze after the nozzle was primed.
I haven’t gotten a bad layer on either one of my “guys” in a very long time… Honestly I’m trying to think if I got a bad 1st layer on either of my devices… Hmm, now I really need to think back… The second one, I definitely was more lax on watching the beginning of the first few test prints…
But then honestly, I only think I watched the first layer on maybe the first 5 to 10 prints (on the 1st machine), and was like “man… I don’t need to watch this thing, it’s got it”… And that was, whew, between the machines about 6 to 700 hours ago… Now I’m simply like “click print, go on about my day”…