Hello,
I wanted to document an experiment carried out on a Bambu Lab H2C using two different nozzle diameters in the same print job.
The objective was to test whether a print could start with a 0.4 mm nozzle and then continue with a 0.8 mm nozzle, while preserving the native H2C tool-change sequence generated by Bambu Studio.
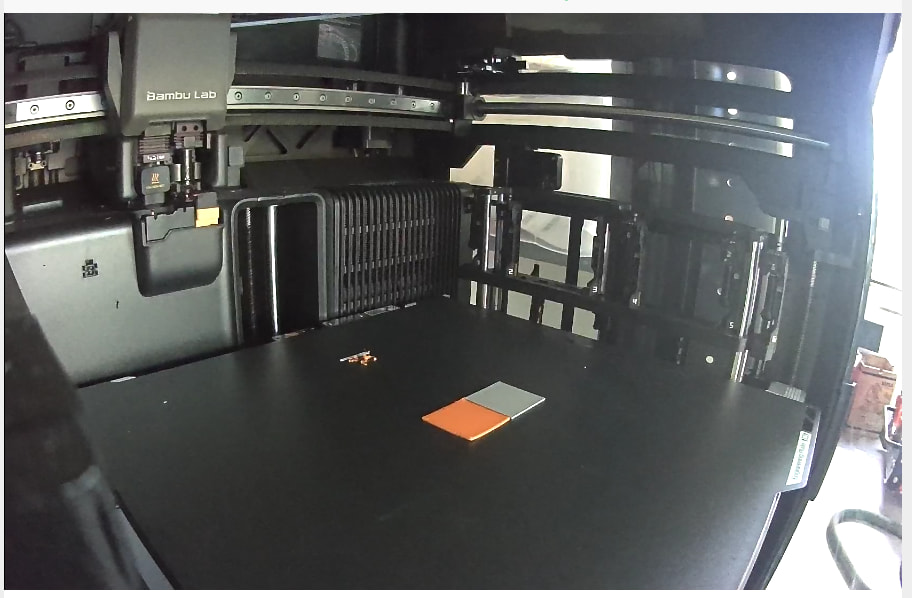
For the first test, two cubes were placed side by side:
- Right hotend: 0.4 mm nozzle, PLA
- Left hotend: 0.8 mm nozzle, PETG
Separate G-code files were generated for each nozzle size.
A third standard dual-hotend file, using a supported configuration, was used to recover the native H2C tool-change sequence.
A hybrid .gcode.3mf was then assembled while keeping the original H2C initialization, tool-change and firmware commands.
During the print, the H2C displayed a warning indicating that the hotend configuration did not match the expected configuration, but the printer allowed the print to continue.
The machine then:
- initialized and calibrated normally;
- selected the 0.4 mm right hotend;
- purged the PLA;
- performed nozzle-offset calibration and the normal startup sequence;
- performed bed leveling once;
- printed the first cube with the 0.4 mm nozzle;
- changed automatically to the left hotend;
- loaded and purged the PETG;
- printed the second cube with the 0.8 mm nozzle at the expected position.
The second cube was printed correctly next to the first one.
This test suggests that the H2C firmware is capable of executing a print using two different nozzle diameters, provided that the native H2C tool-change workflow is preserved.
This is not a supported Bambu Studio workflow. It is only an experimental test at this stage.
The next step will be to test a more practical use case: printing fine details with the 0.4 mm nozzle for the first few layers, then switching to the 0.8 mm nozzle to print the surrounding geometry and continue the rest of the part.
The hybrid .gcode.3mf used for this test is attached below.
Important: this file was generated specifically for this H2C configuration and should be considered experimental. Please verify nozzle positions and configuration before attempting to print it.
I will update this thread with the next test results.
H2C_test_mixte_04_droite_08_gauche_UN_NIVELLEMENT.gcode.3mf (54,4 Ko)
 &
