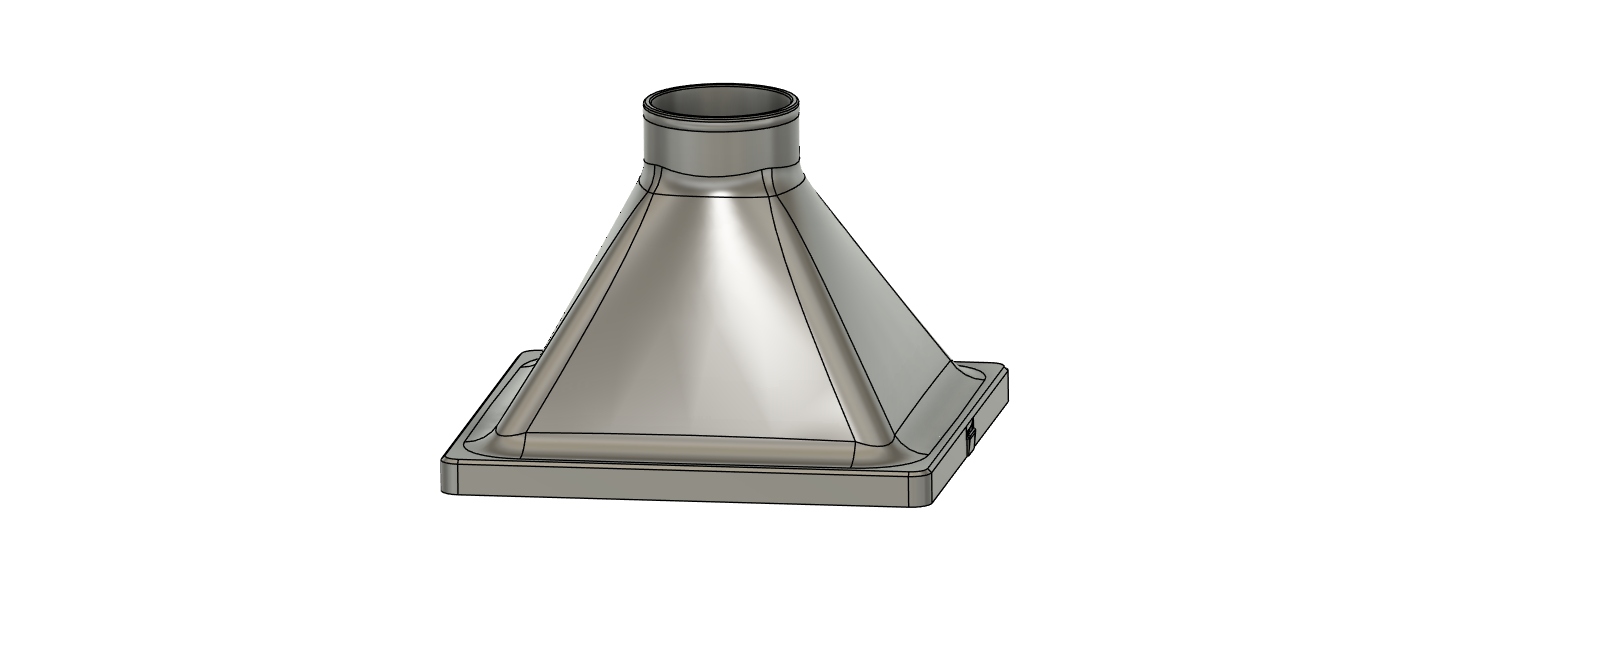
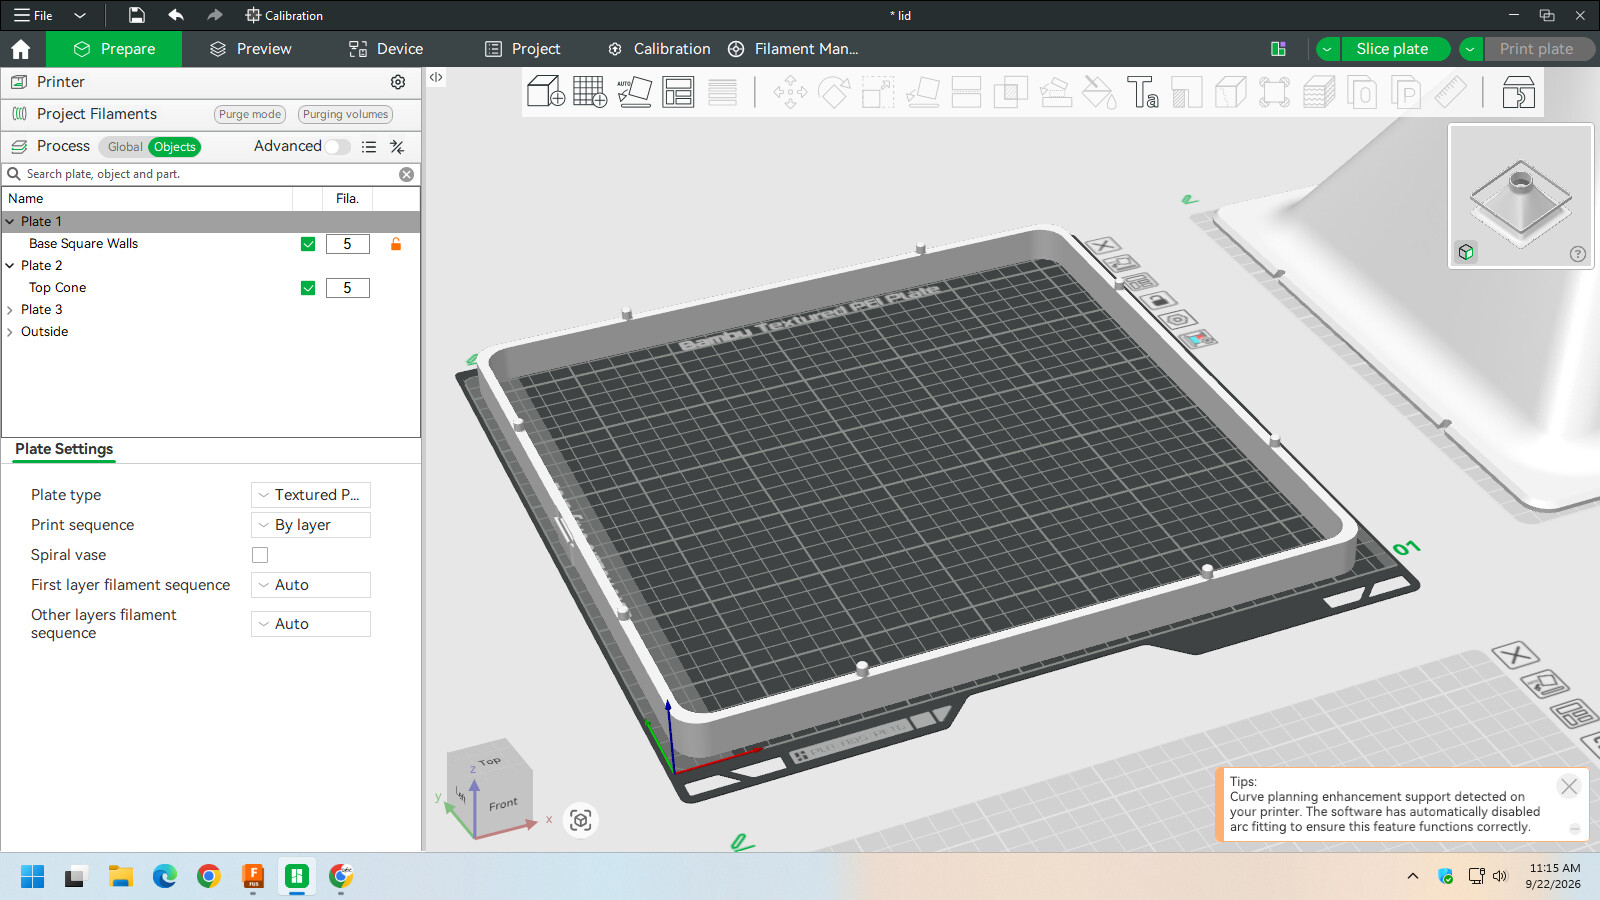
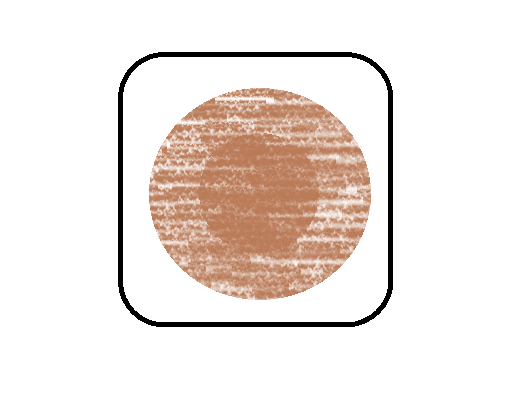
hey guys, I designed an upgraded lid for the smoke detector to take advantage of the entire top surface of the filter. The issue is it BARELY fits on my plate.
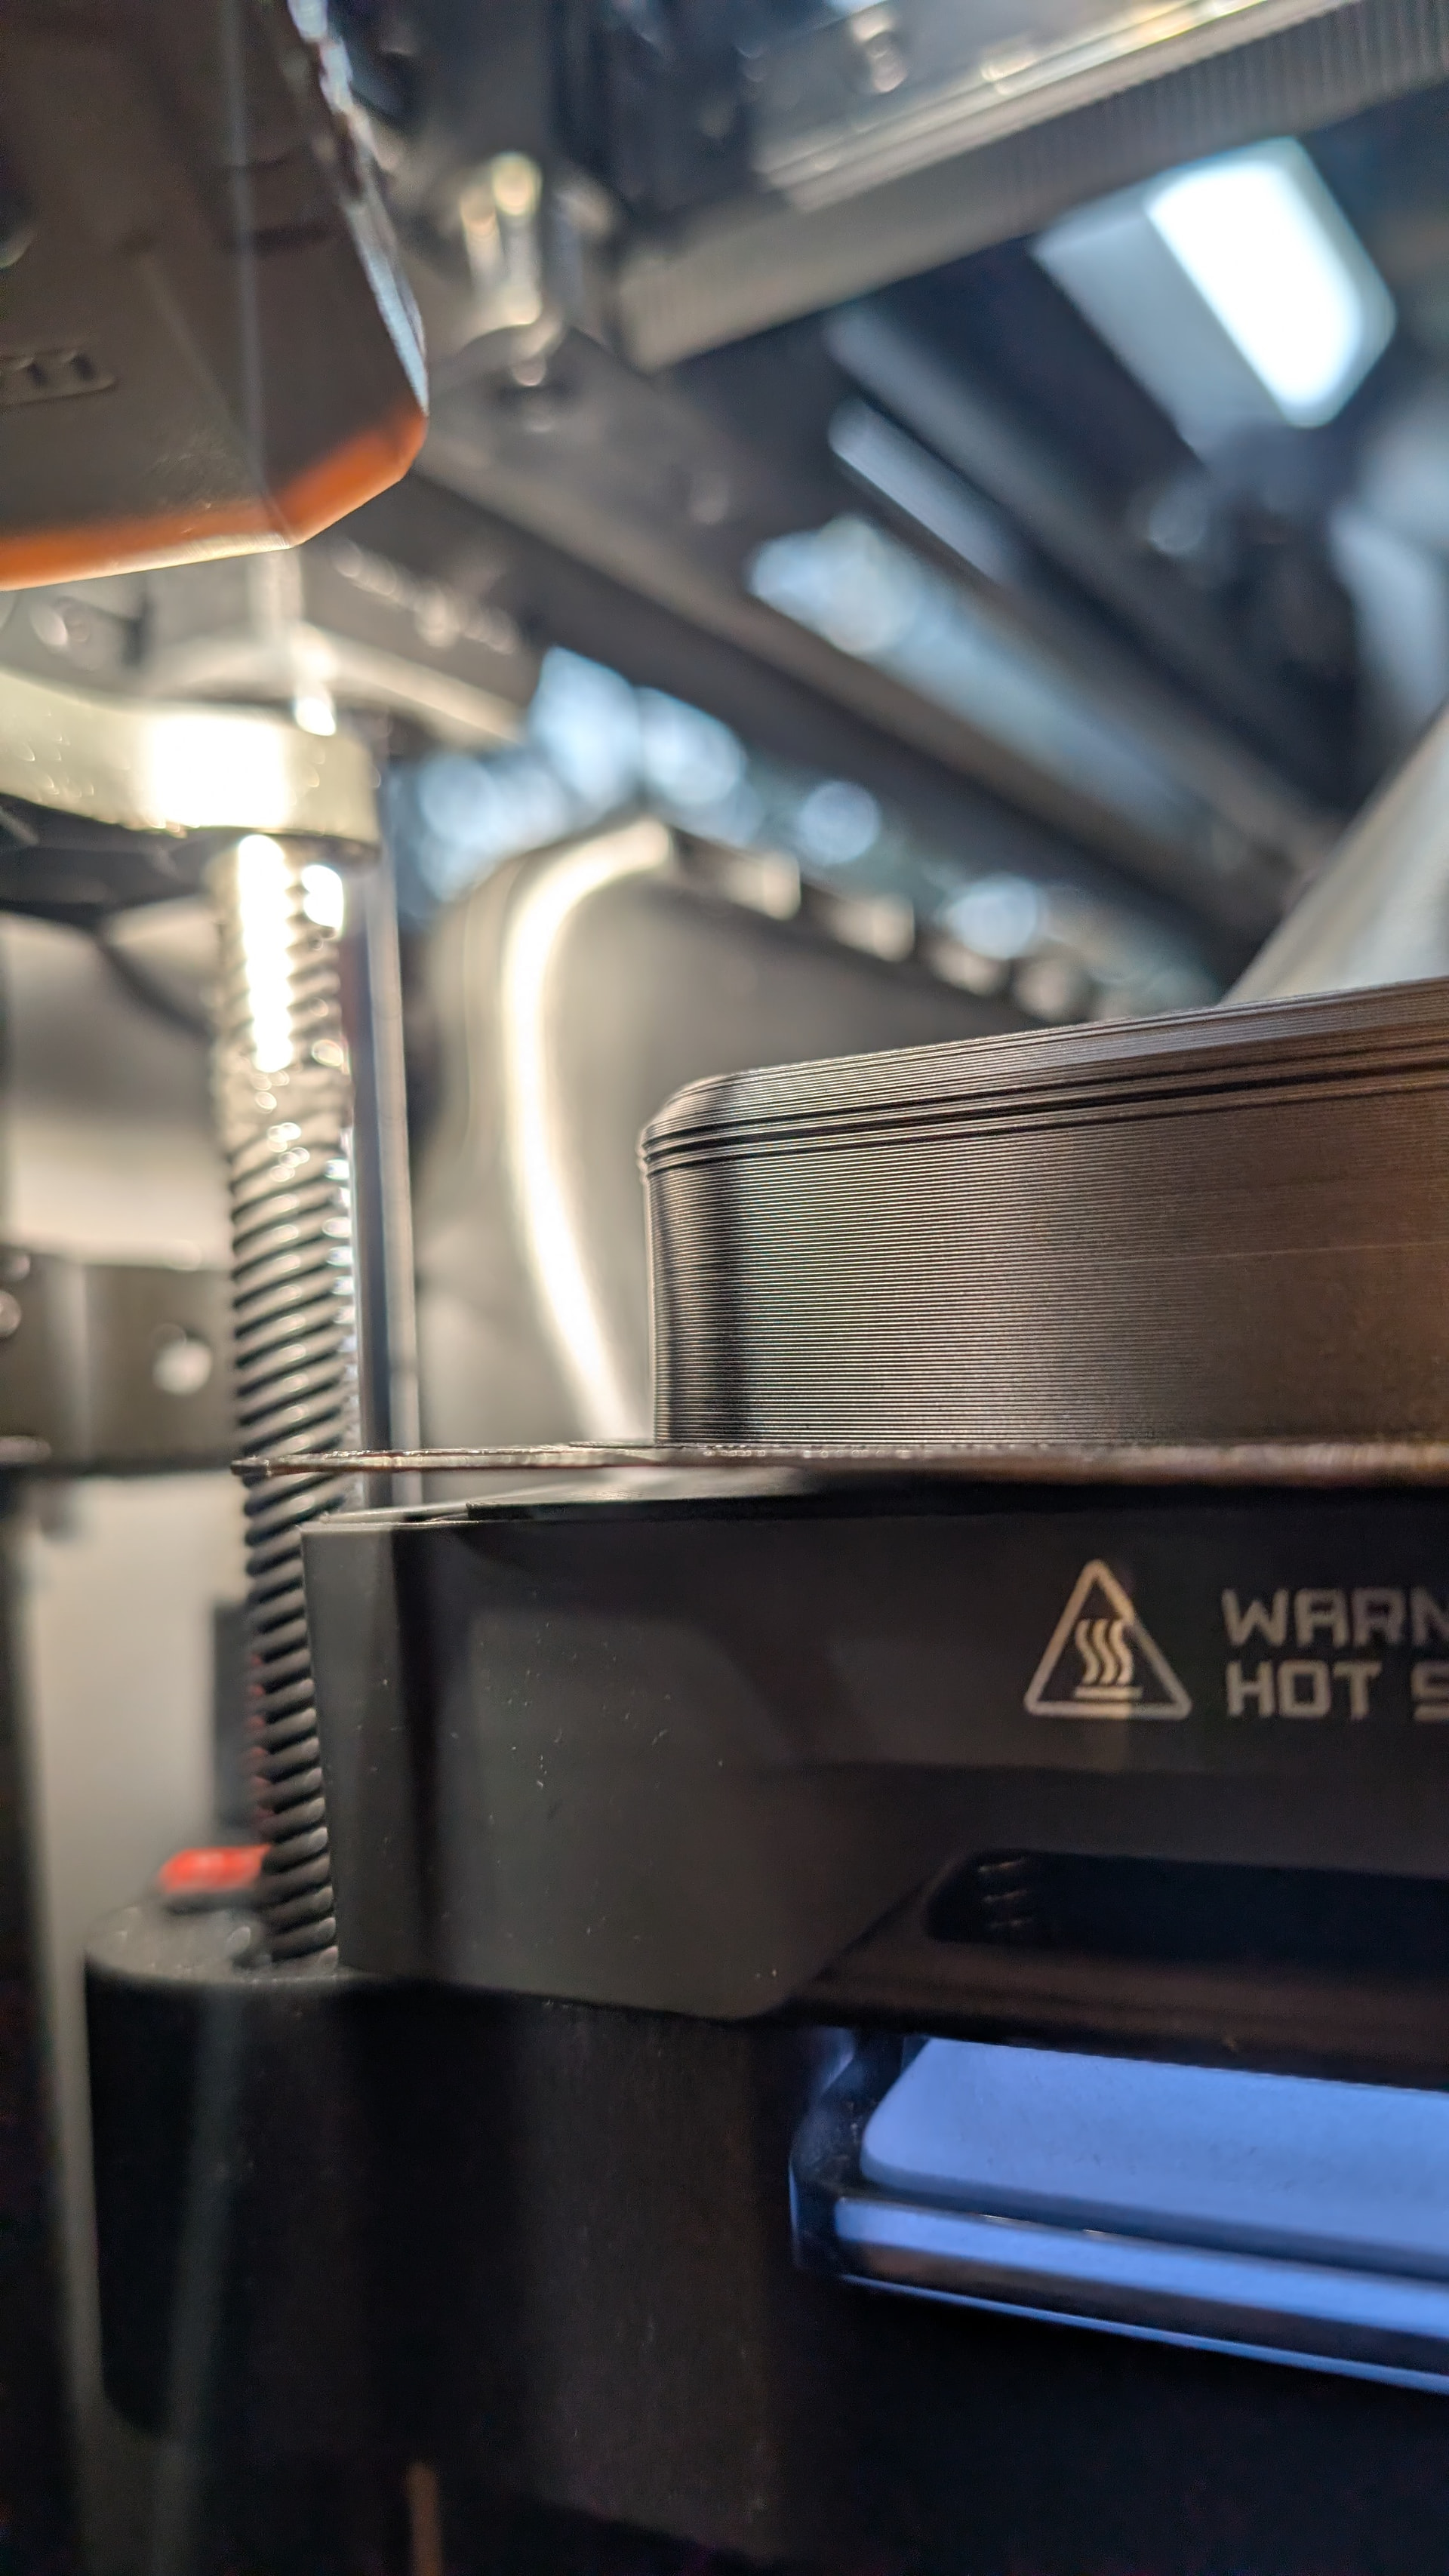
I finally got it to not pull away from the textured PEI plate but now it’s sticking so well that it’s pulling my plate up from the magnetic bed at the corners! any ideas?
There are a number of things you can do to decrease the stresses that lift those corners. Part of the issue is just the size. The closer you get to the corners the easier it is to lift those corners.
Depending on what that surface on the build plate looks like you can add some relief holes that reduce the strength of the shrinkage. Raising the chamber temperature can help keep the part warmer to reduce shrinkage during the print.
Maybe worst case is you split it into two parts that can print properly and assemble them after printing?
There are a number of threads here on build plates being curled up with a number of possible fixes.
My guess is you are printing an exhaust duct so not much bottom surfaces to work with.
Practical advice: 1. If possible, make the bottom square section thinner; 2. make it taller: in my experience, steep inward walls exert much greater pulling forces vs. straight-ish walls; 3. split up your model (square section, funnel section) 4. (easiest) use something like PETG-CF/GF, skip the trial and error.
Assuming you are using the new Basic. PETG is just going to do PETG thing, aka shrink. Part of the package. But with the right combinations I still regularly print full size models with it, including wall-heavy, tiny bottom-surface exhaust ducts/connectors.
I can’t really do relief holes… since this goes on top of the smoke purifier it needs to be fully sealed. I also have a tpu gasket to print.
I’m thinking I may have to split it up like you said… it barely fits the entire print bed but it does fit. It would be nice to take advantage of the full H2C bed but not sure how.
Are there any other cheap-ish filaments i should consider that would warp less and be semi durable like PETG?
the warp transferred up about 1" to the top of the edges of the flange part… obviously this is NOT doable because that will cause an air gap at the corners of the smoke purifier so you are thinking I could just extend the walls down to maybe the 2" mark?
Hard to find stuff as cheap as PETG but PLA is a second? If it’s for the H2 lasers, both should work as the smoke shouldn’t typically exceed 50C.
A flat bottom plus assembled funnel section, which should eliminate much of the warping, with some gap-filling glues kind of sounds like the appropriate solution here.
The starting assumption - that your entire filter surface isn’t being used - is somewhat mistaken.
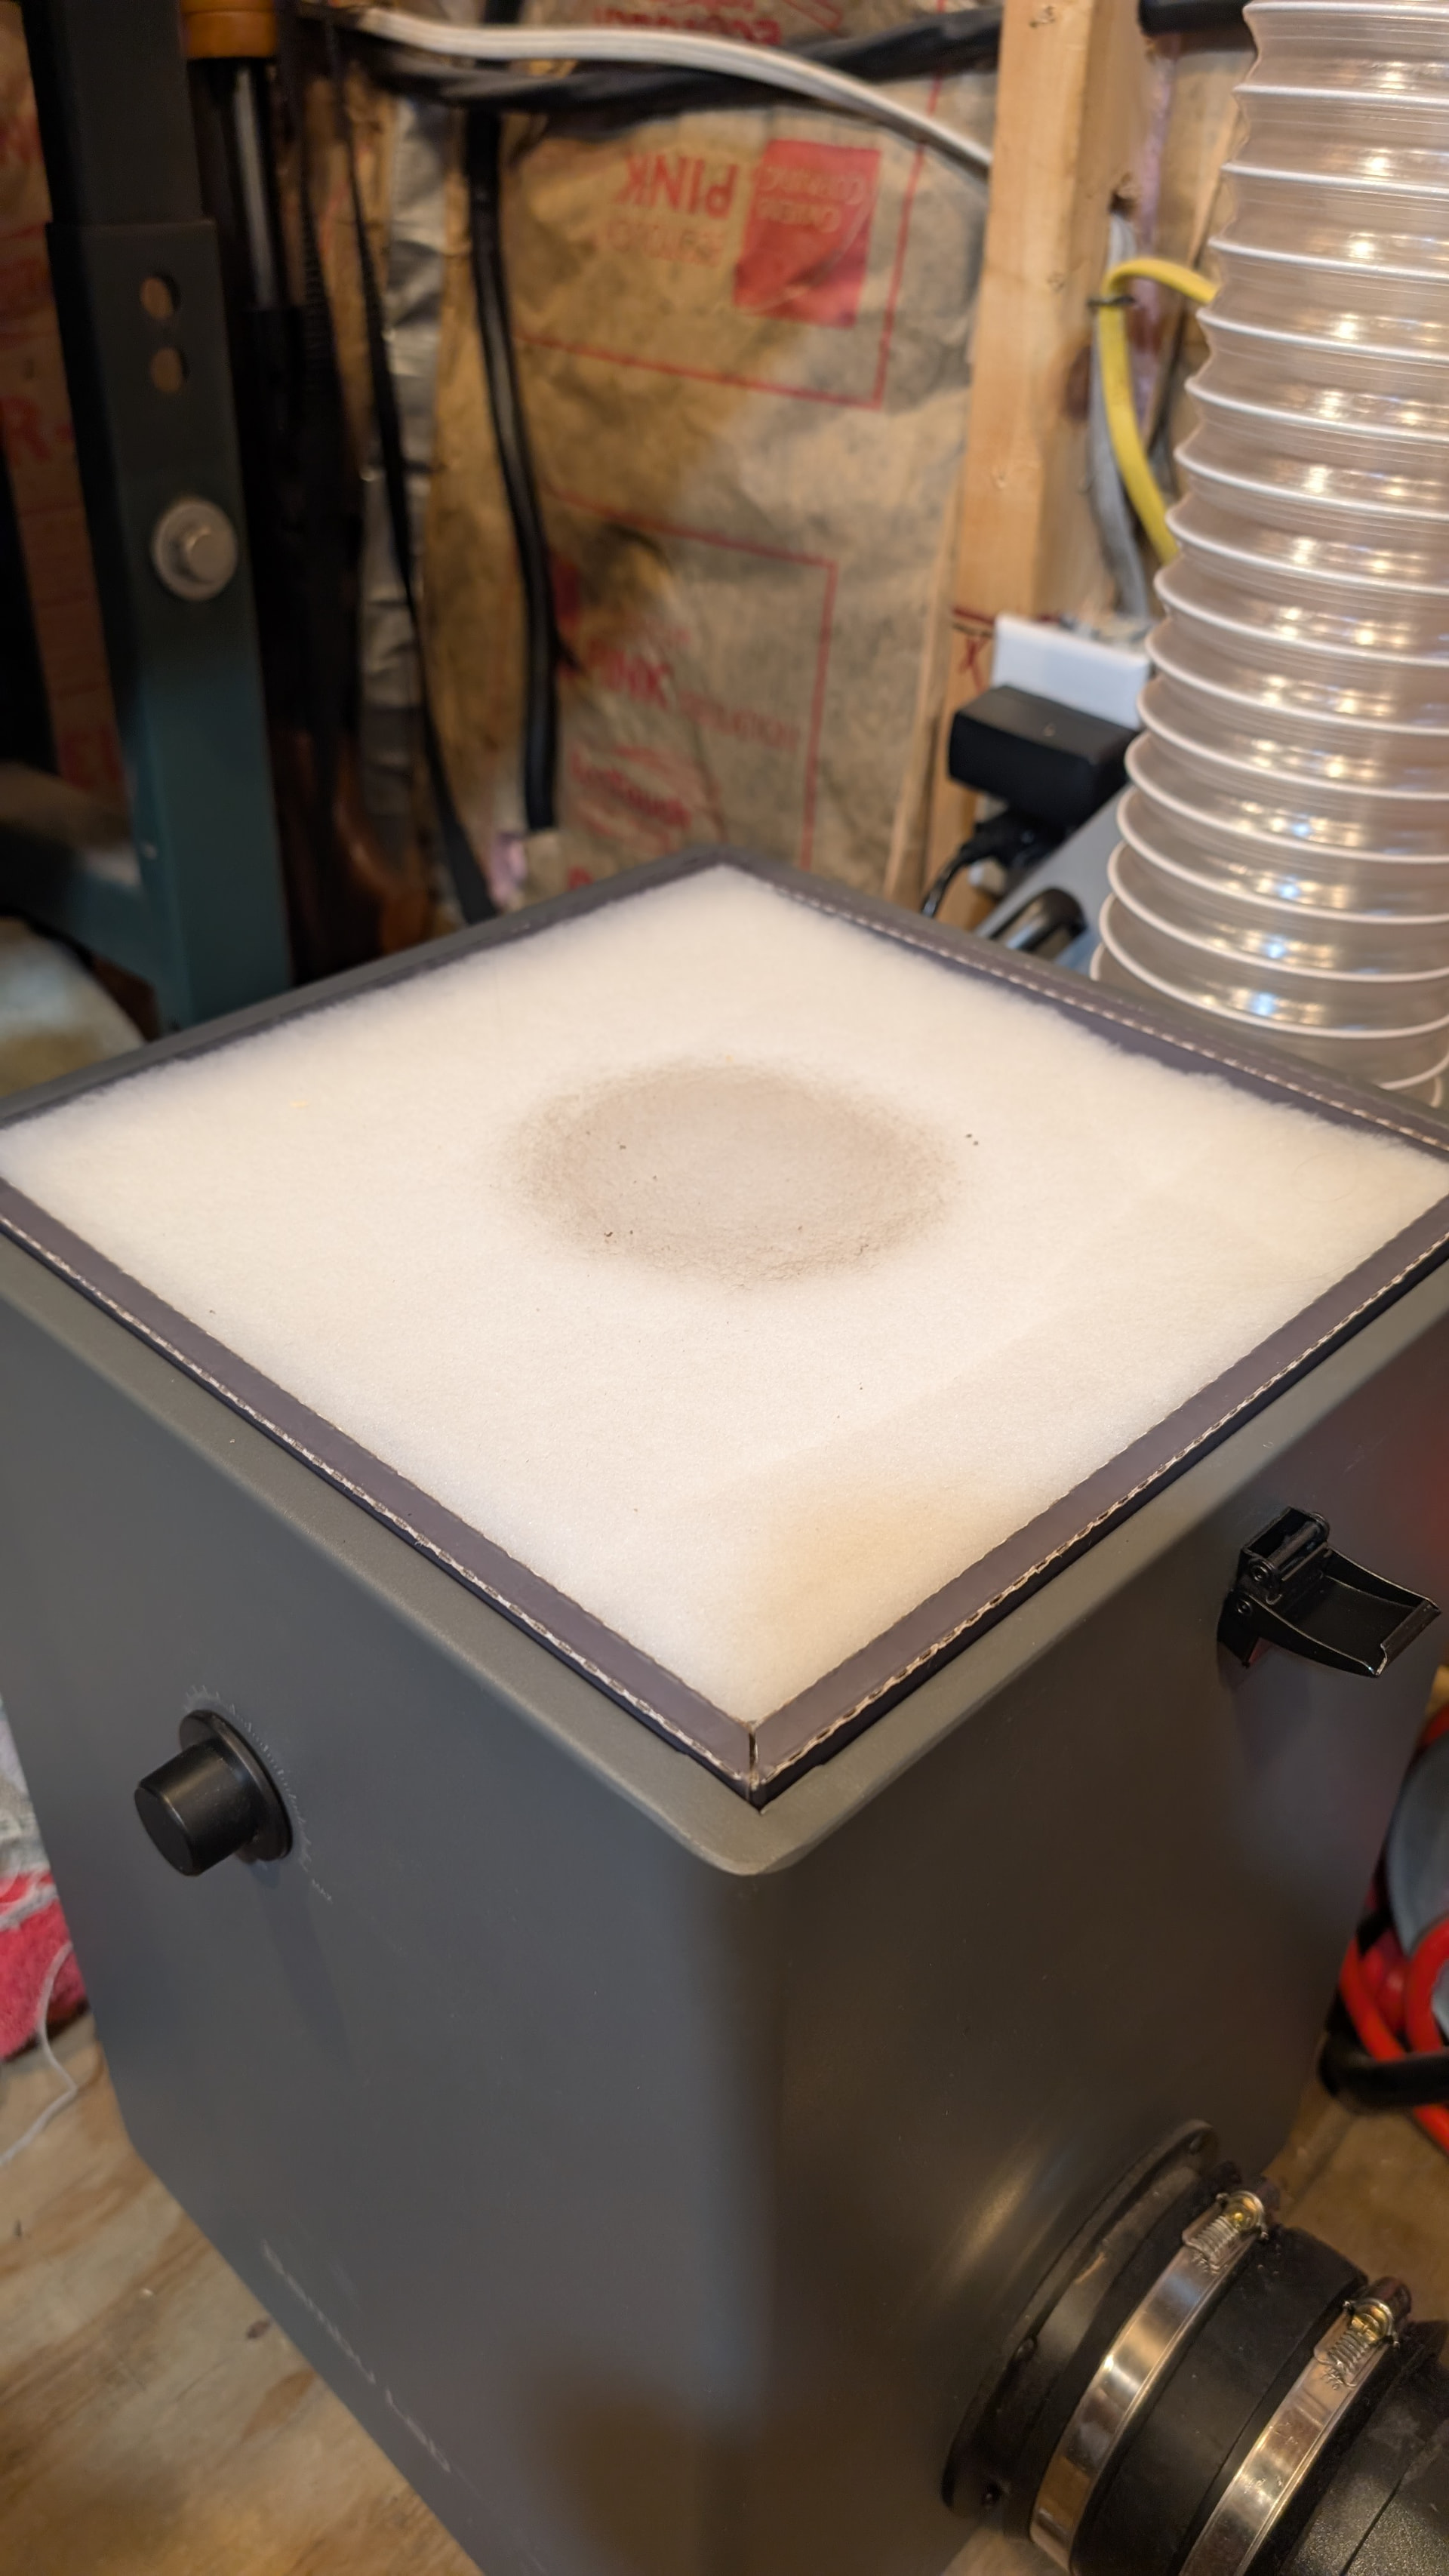
Yes, on the top filter you’ll see a darker section in the middle, but as that section of the filter becomes more used the airflow spreads out toward the outsides of the element. Even when new, the overall area of the filter flows air, this is why the pressure drop of a large area filter is less than the pressure drop of the same media of smaller surface area. The whole filter contributes the whole time.
Also - small air leaks aren’t a problem on the suction side, it just allows a bit of non-printer air to sneak in.
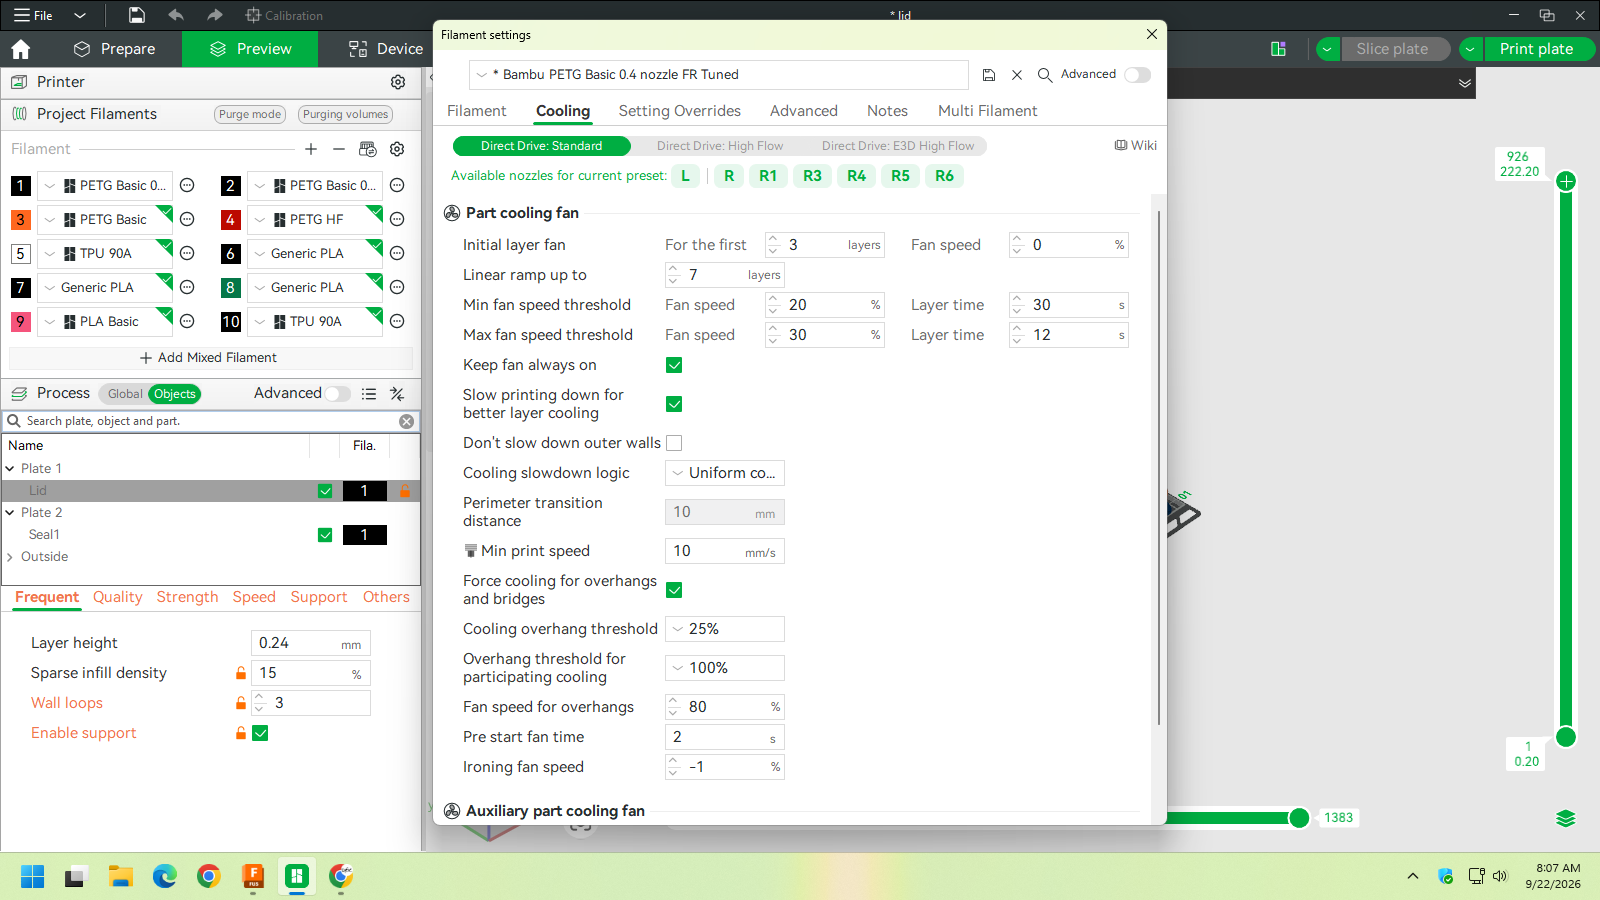
A screenshot of PETG cooling settings is posted in that link. On large PETG items cooling can be tuned off completely. On your specific item, I would turn off cooling until the neck, so at least 100+ layers.
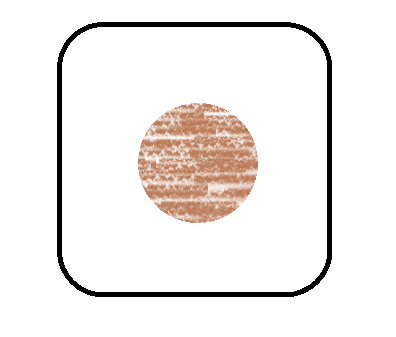
i’m going to have to disagree. when the lid is flat and pressed up against the pre-filter media all the air has to go through that 4" diameter circle. maybe it won’t affect the hepa filter as much but once once the pre-filter is clogged/used up in that 4" diameter section the air flow will not be the same and you are not getting full life or max air flow from your filters. it just makes sense to me the way air flows.
Separate funnel section from the plate, print the flate plate upside down.
Plate funnel section separately
Fasten together with a gasket, rubber cord, etc.
Don’t be afraid of the small air leaks. On the suction side it’s not super important.
Side comment, would be interesting to see results, although I don’t think it would change anything. Visual staining on the pre-filter is usually misleading. If it clogs up, then it would create a higher-pressure spot and the air would go to the side with a lower-resistance. Up until a point where the filter will be clogged and wouldn’t be able to perform.
well if you see staining what is that other than dust/smoke accumulation on the filter? the more it accumulates the less efficient the filter is. and even if air goes to the side it will have to go through that clogged spot which just means less efficiency overall.
Pre-filter can capture only large particles, like dust and may be a bit staining from the smoke. It’s porous enough that it will not get clogged unless you start using your smoke purifier as a carpet cleaner.
That would be true, only if the filter has the diameter of the opening hole. However, if the pre-filter is clogged it will travel through the path of least resistance. The air will not go through the clogged path. That’s not how physics work.
What you are doing, is essentially changing how the filter media would be consumed.
Let me do a paint master race to show what I’m saying:
As long and large area infill slices increase warp significantly, maybe this consideration on top of all the given advice:
Lower the corners a bit (5-7mm). In other words, make sure the top face is not flat (horizontal). This gives smaller area slices which reduces stress also.
It should not significantly reduce the strength towards the corners.
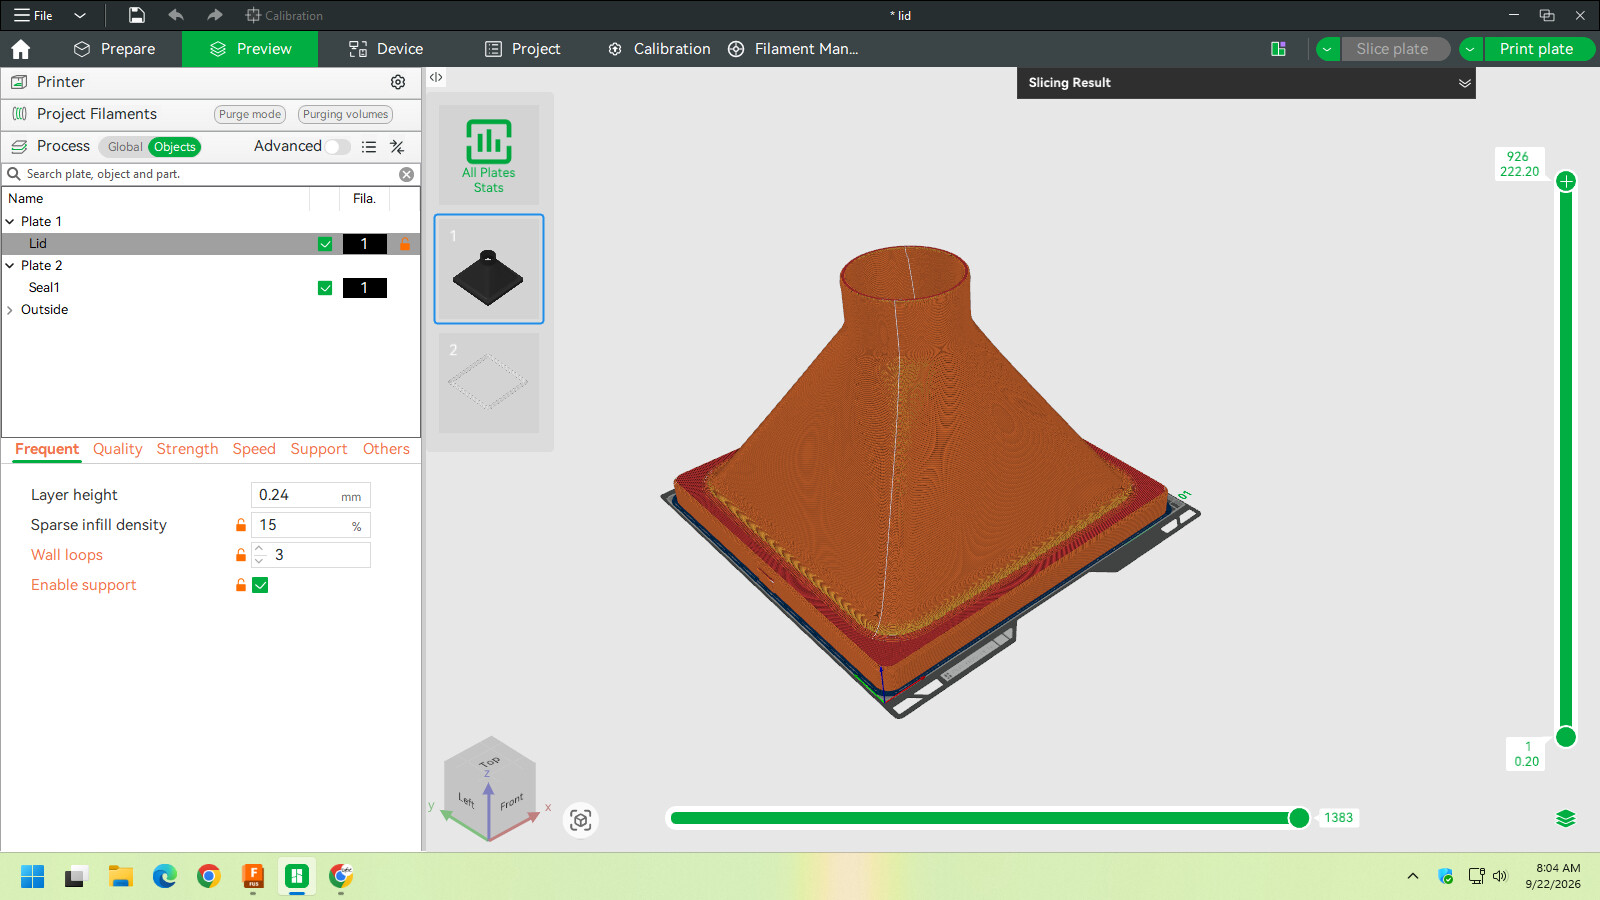

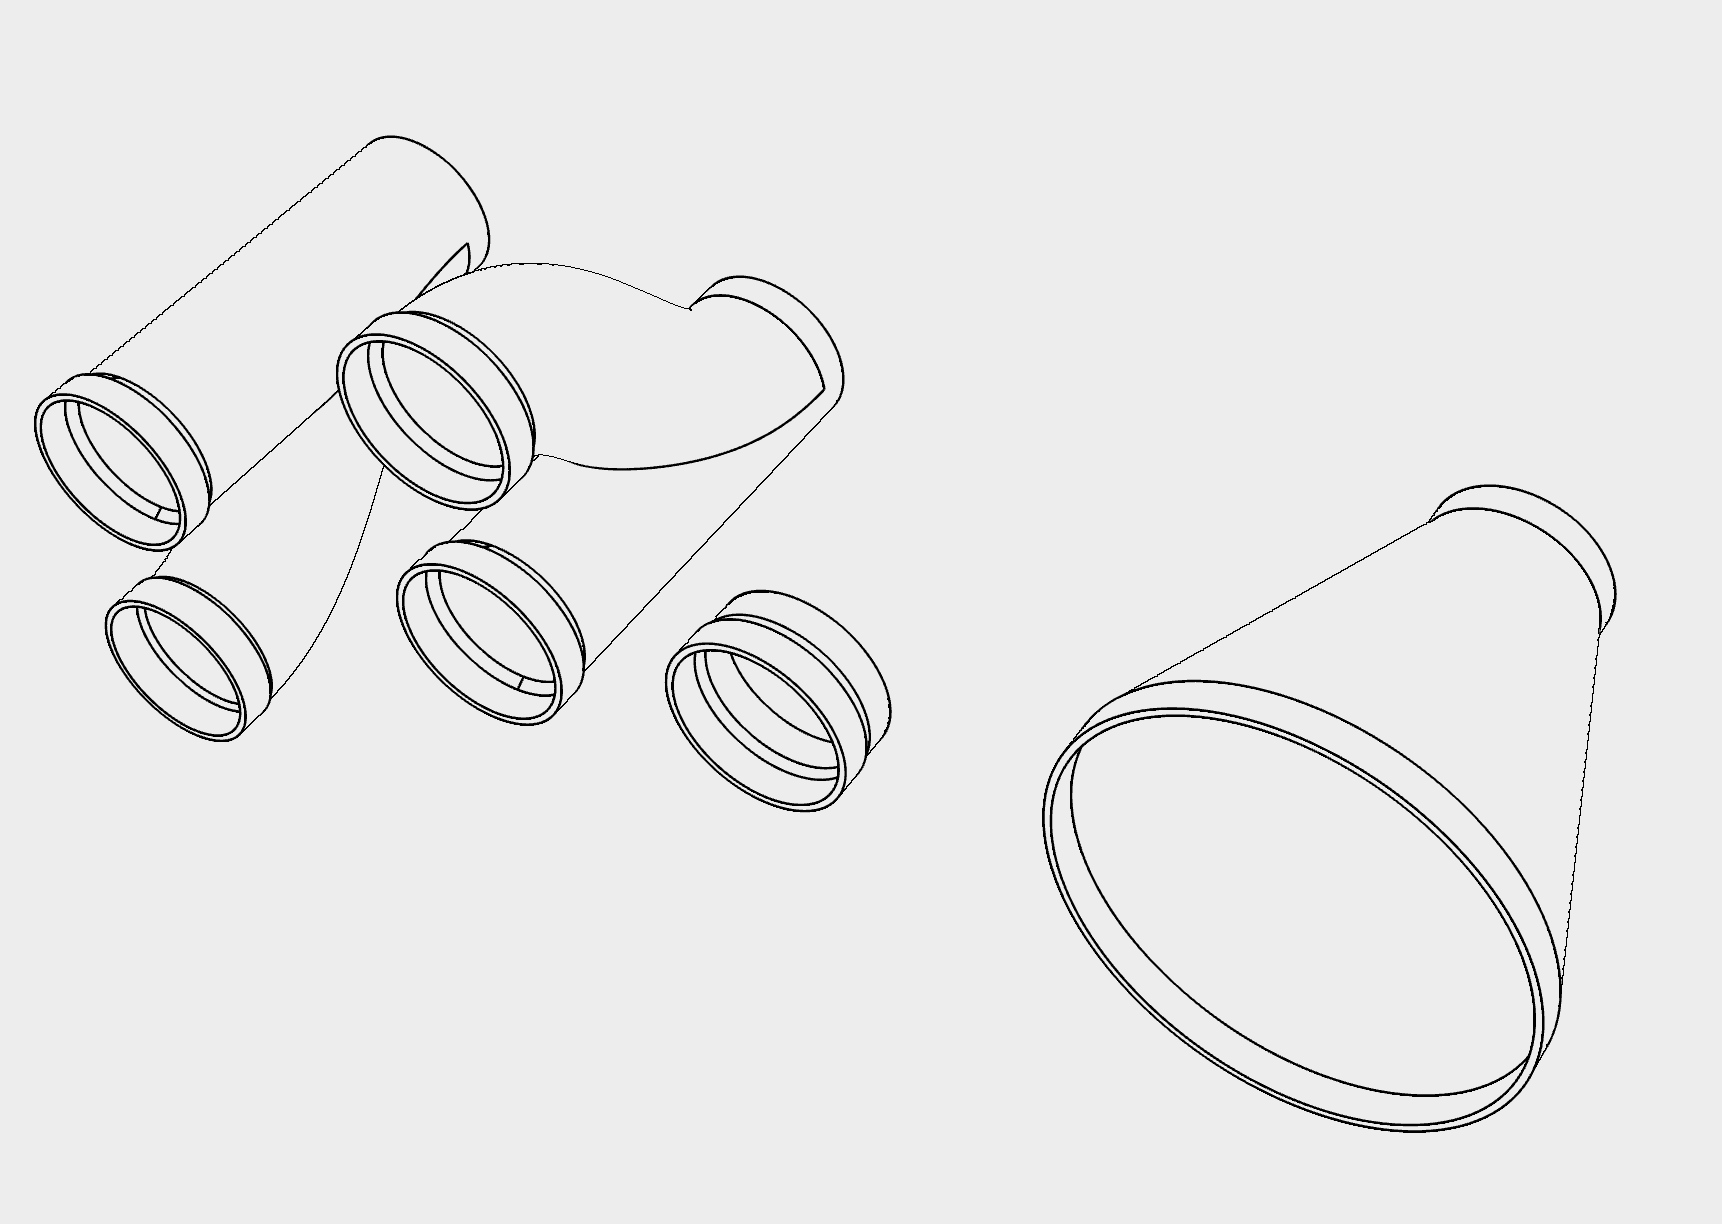
 so you are thinking I could just extend the walls down to maybe the 2" mark?