I know there are people who like to experiment with such things, so hopefully someone can answer the question in the title. I’d obviously prefer answers based on direct experience, rather than “I read somewhere…”.
As for the specific question about the infill pattern: No, I didn’t notice any difference in that respect, although that’s not entirely representative. However, I did notice a difference based on the infill percentage:
- Does the object cover the entire width of the print plate? Significantly.
- Does the object mainly increase in height? If so, then not at all, actually.
As I said, both points relate to the infill percentage. The pattern itself didn’t make a difference to me, but they’re still related, of course. Other factors usually counteract this, but that wasn’t the question. I just make sure I don’t overdo it with the infill percentage.
From my personal experience: The more material a 3D object contains, the more likely it is to develop stresses that can cause warping. The pattern is not important; it’s the total amount of material that matters. I prefer to address this issue using alternative solutions.
Bear in mind, however, that this is just my experience. 

Perhaps you should include the infill percentage in the question. This would provide a clearer overall picture, given that one person might use 10%, while another might use 60%.
Thanks, that’s all good info. I agree that the infill percentage should be expected to make a difference. My reason for asking the question is that I do a number of projects that have large bases and I was kind of hoping there might be a pattern that produces a bit less warping.
Straight lines = faster print = but also more warping.
So as long as you’re breaking the straight lines, you’re safe, say use gyroid.
However that doesn’t save you from warping caused by other issues, like long straight surface with sharp corners, or large overhangs, …etc.
I know that wasn’t the question, but have you considered other ways to optimise it yet? Have you considered using a print plate with better adhesion? What about brim? Or optimising temperatures and cooling settings? Or optimising the 3D model itself?
There are so many possibilities. One idea would be to post a picture of what you want to print, along with the material you’re using. I’m sure you’ll get lots of advice that way.
I certainly have. All those things you listed. I design as best I can to alleviate a variety of problems but of course there are always limits. Brims and fillets are something I use extensively but sometimes, like the print that just finished, still lift a bit, especially in the corners. Fortunately, my own designs are always functional, rather than cosmetic. Nevertheless, I do endeavour to make them look as good as I can.
I’ll certainly keep that in mind. I’ve only had my printer about 3 months (about 1,000 hours of printing), so there has been, and will continue to be, a lot to learn.
I’ve found it very hard to gauge the impacts of sparse infills alone, but from a thermochemistry PoV, Infills and other Line Types are really not that different, so, a more useful case study here is that wall count in percentage to total object volume and geometries can absolutely warp things.
You probably have also read somewhere else that infill directions can increase likelihood of warps and somewhere along that line they’d recommend things like concentric infills. In a sense, walls are just the worst case of the same dynamic, so in theory, they are likely correct. It’s just that infills usually have a lesser impacts to be easily measured.
A straightforward past example of mine:
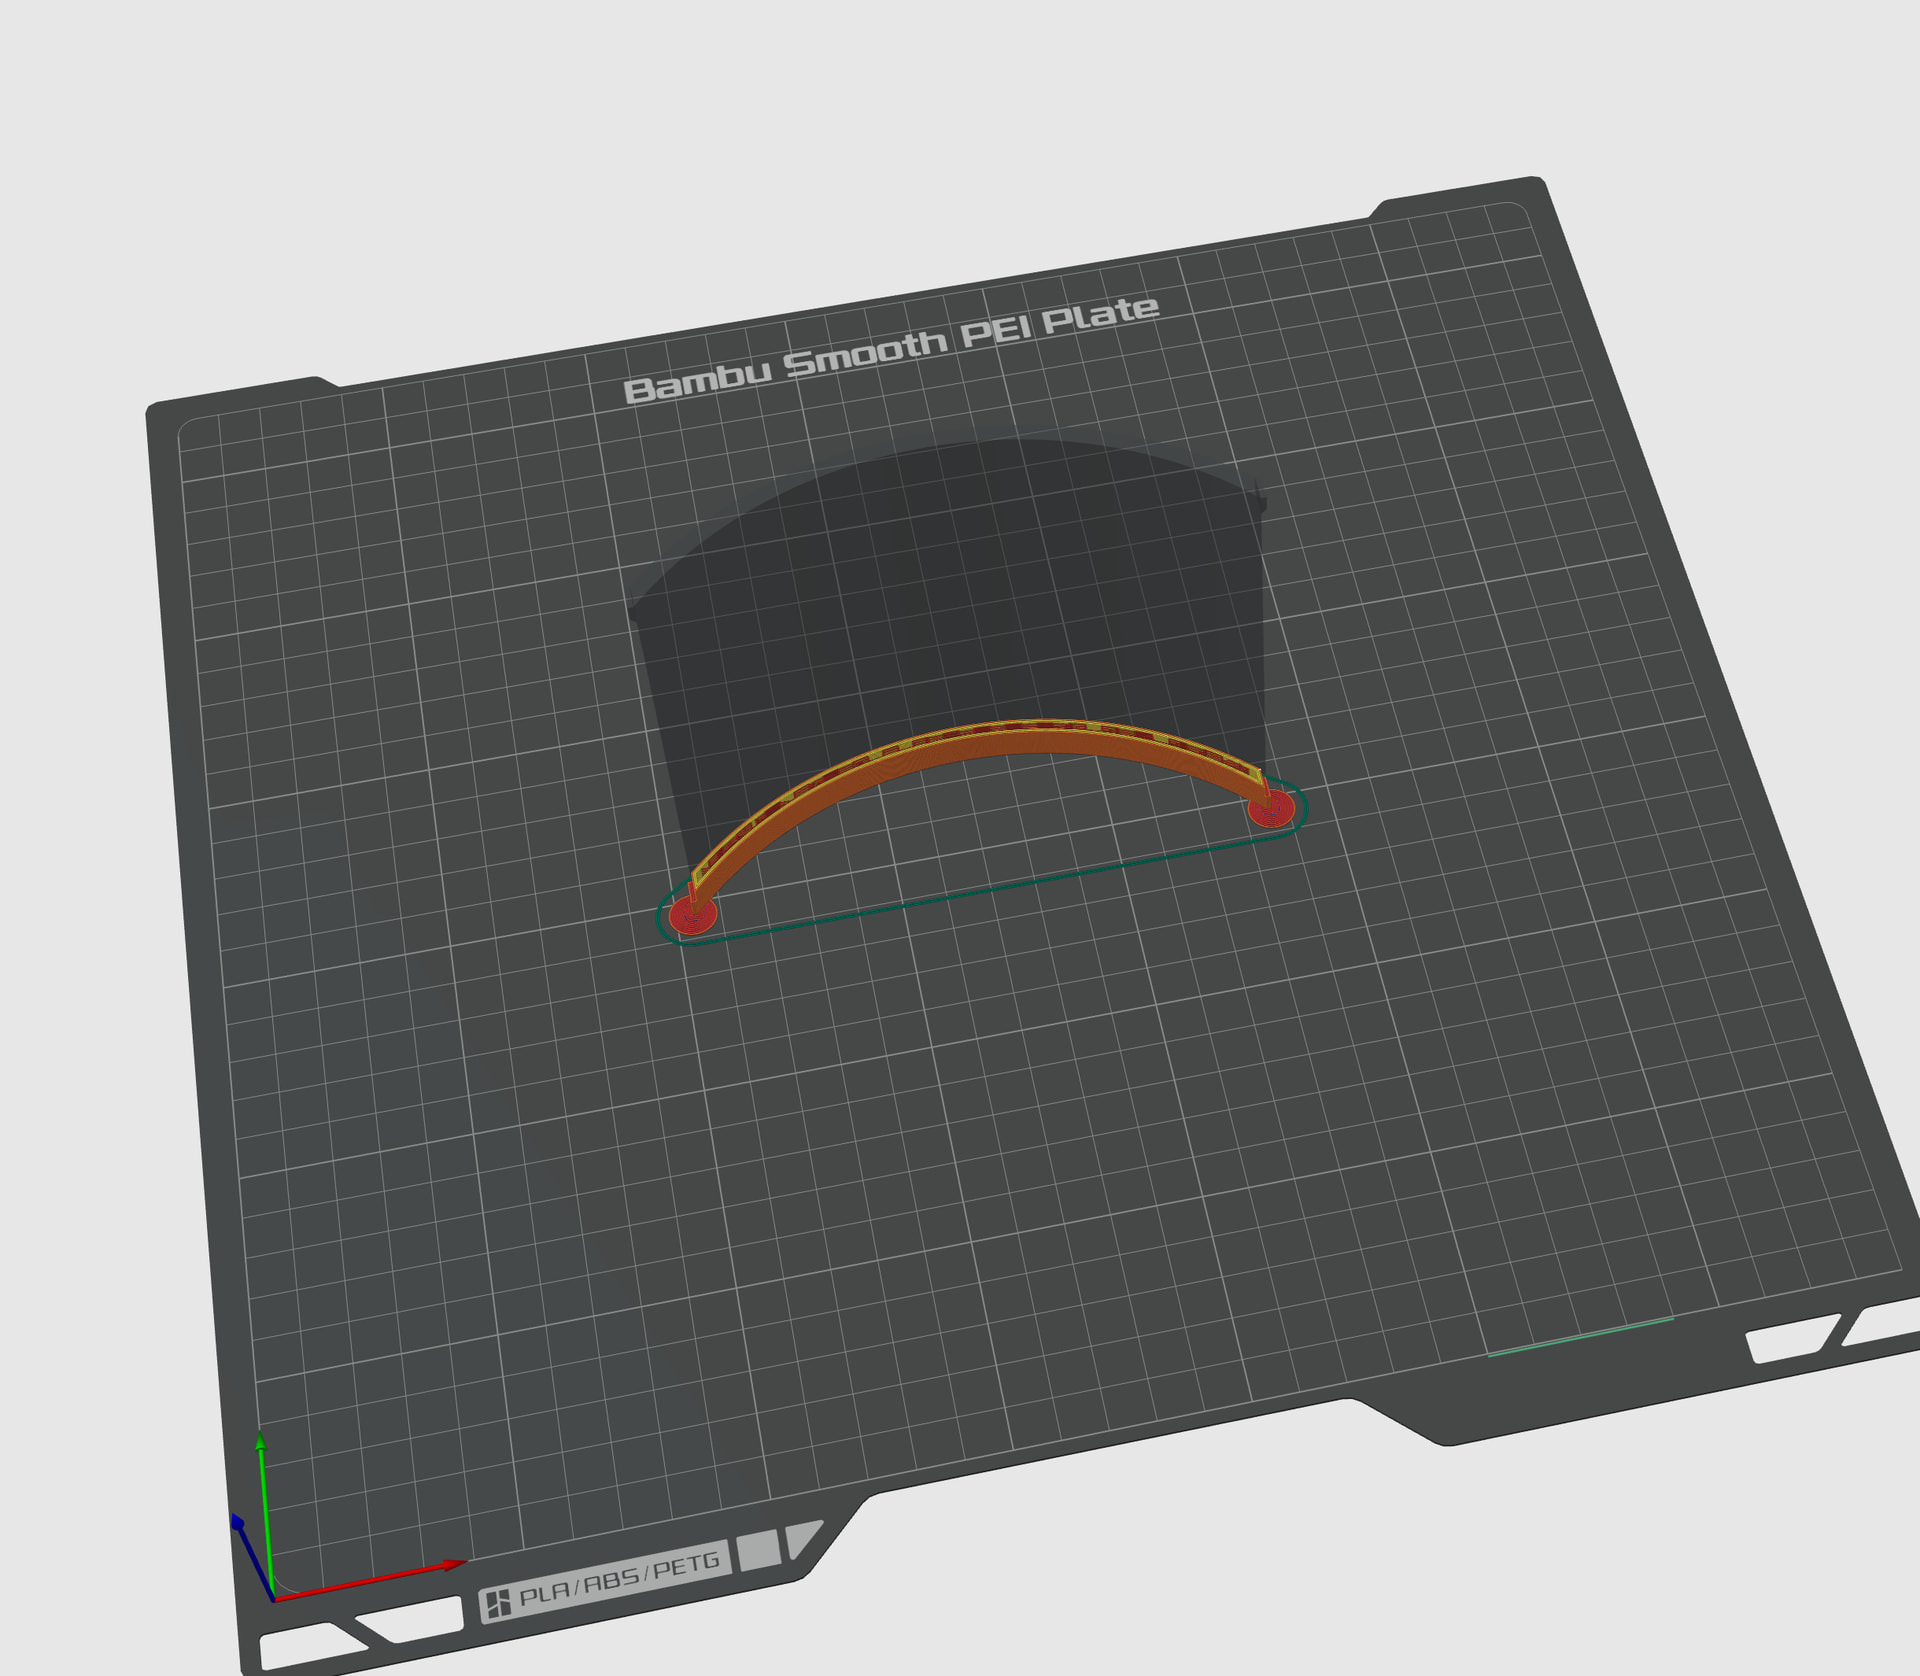
With PETG, this model warps like crazy, even with no infills at all. There’s just too many walls in relation to the thin bottom surfaces. Not even a brim would solve it as this object needs 0 warps for tight assembly. I just switched to PLA-CF, absolutely 0 warps.
Realistically speaking, if you are unsure, it doesn’t hurt to pick infills like Gyroid from the start, but sometimes you just won’t know until you printed it out  , kind of unavoidable.
Thanks for that info.
No, I’ve not come across that yet.
I’ve been use Gyroid mostly of late, although for a separate reason. Quite a few of my models have to sit diagonally on the plate and the infills composed of straight lines are not as strong then, whereas Gyroid isn’t so sensetive to model orientation. I just wish there was a way I could set such things as a default.
Are you able to put cuts into the bases to relieve the warping stress?
Good suggestion, thanks, and I’ll certainly keep the idea it in mind for the future for other projects. The box I previously refered to is actually the lower part of what will be a (very nearly) airtight enclosure. The last one of the four I need has just started on layer 2, so perhaps it’s a bit late to be thinking of changing anything.
Not to divert from the main topic (+1 to everything said above!), but you could save your desired defaults as custom presets, in this case of the “Process” type (vs. printer or filament) to capture settings like infill. Doesn’t entirely eliminate redundancy, but can definitely be helpful.
-Max
You can set Infill direction to 90/0 degree (Strength-Advanced) for those diagonally placed models
Please, divert all you want. As a beginner I’m eager to learn what I can. When I get a chance tomorrow I’ll dig into the process files I have, which are mostly from eSun, and see what I can do. Once I work out what I want to set I can easily enough create new process files for the other filaments. Thank you.
Ok, that’s one of the numerous settings I hadn’t noticed. Still, I think setting Gyroid as my default would be the simplest option, especially as I expect it to produce stronger results.