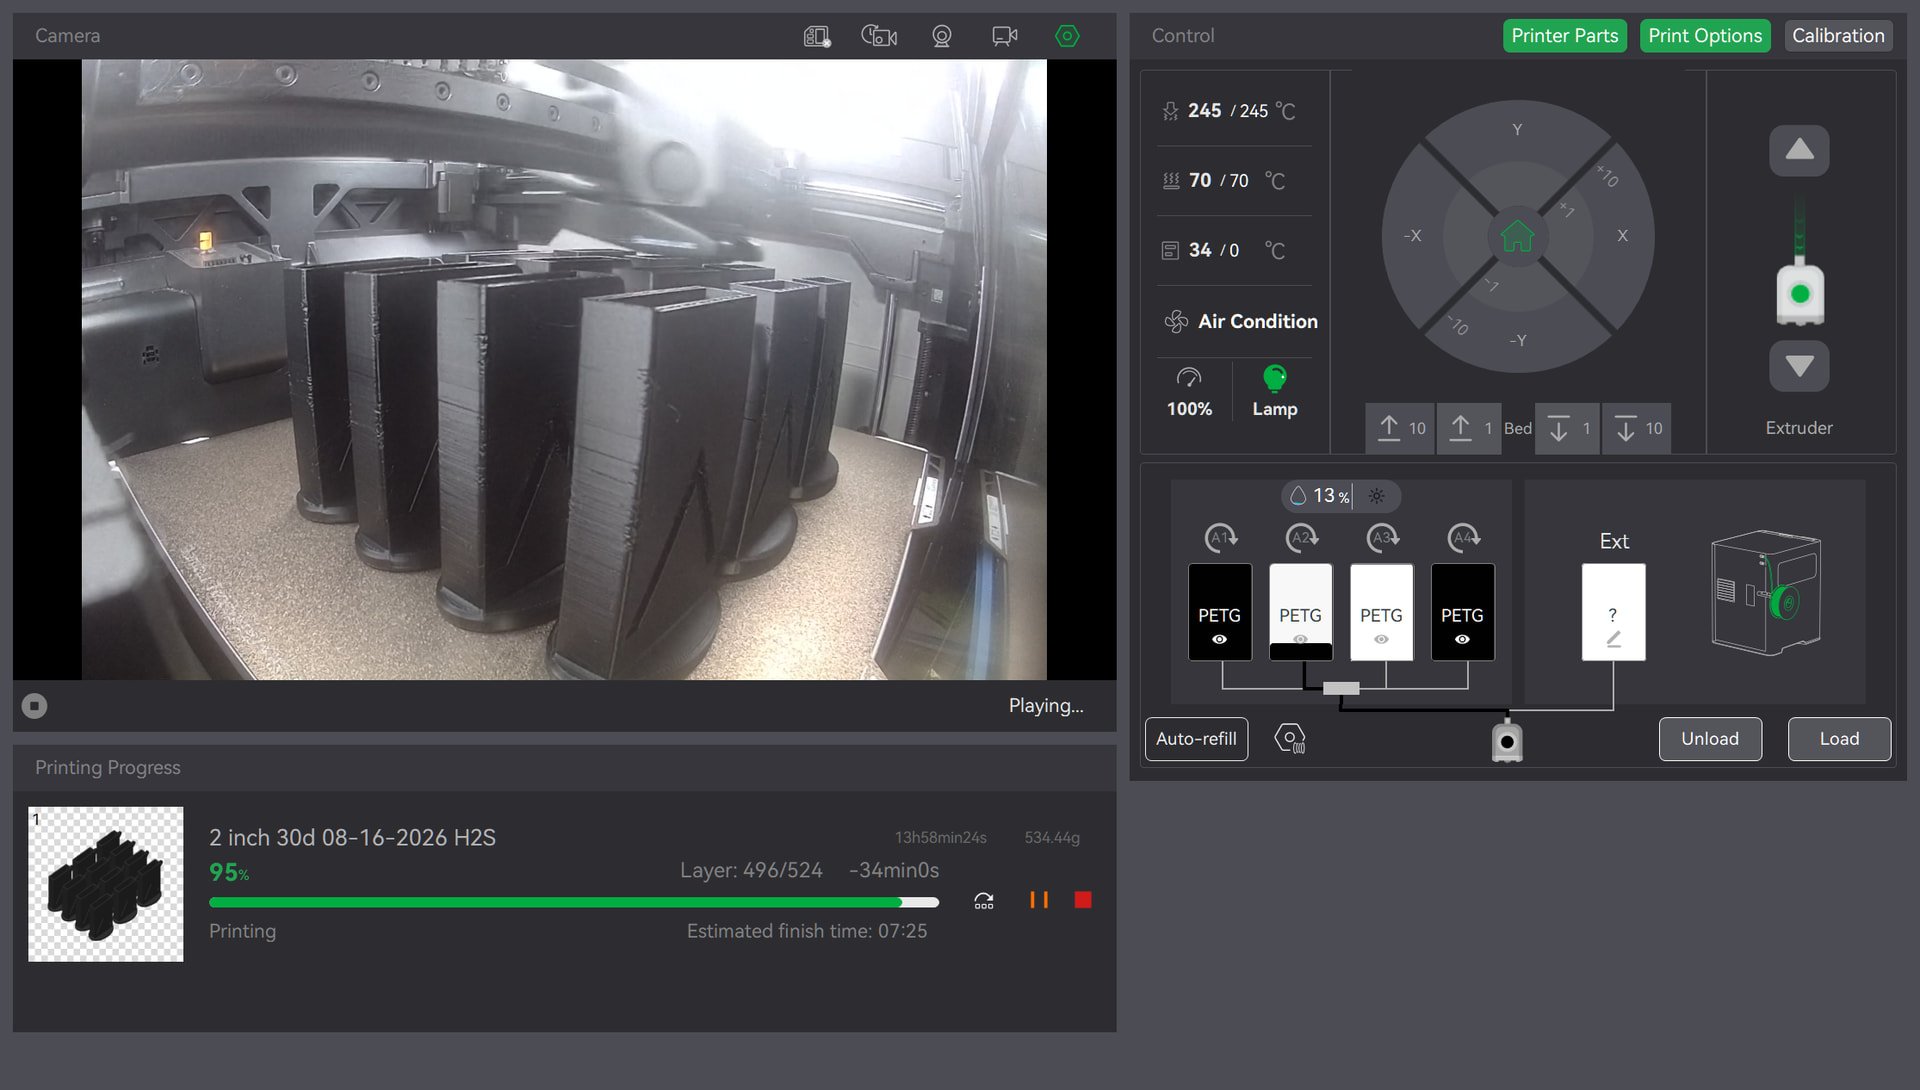
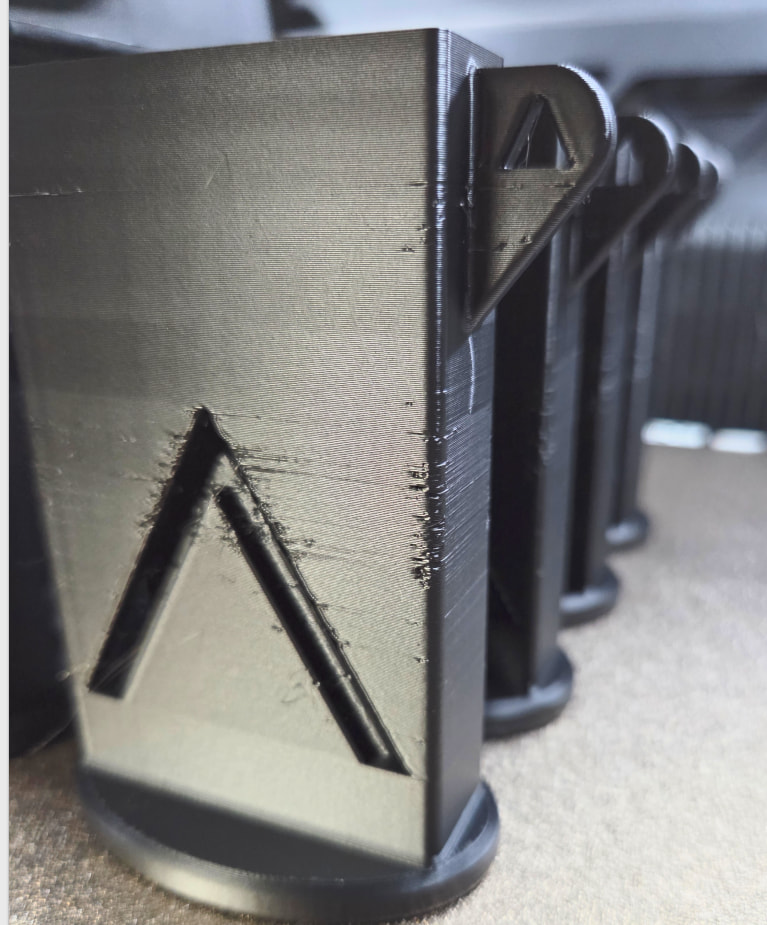
I have been printing these part for almost a year and am just having trouble doing them on my H2S.
If I print just 1, it comes out good. I have printed a few plates and most come out like this.
I figured the nozzle, since I recently printed some PHAT-CF, so I changed to a new nozzle. I am using PETG-HF and have been for a few years. Also, with the filament, I always dry in a Creality SpacePi for at least 8 hours, but typically 24 hours. Also, this it my 3rd for 4th spool, but have also been using this black for a couple years.
Before this last plate, I ran the complete calibration, just to make sure. But the previous plate wasn’t as bad, I don’t get it?
Other than doing a run out of a different color and filament, I’m at a loss, although it does look like a wet filament thing?
I’ve run into this problem before when trying to print multiples and what I found was that the models were cooling more as layer times were much longer and there were more surface defects as the nozzle was entering/exiting between the parts. That said, if the parts were printing in multiples without issues before it would point more to a filament issue? Also, are you reslicing the parts or using already run gcode from previously know good multiple prints?
Good question on the slicing. I was using the same sliced G-code as prevoius good prints. Then I decided to re-slice to see if that would solved it and it didn’t.
My next step is to use a different, known good material and see what happens. But as I mentioned, I went through a few different spools with the same result, although they were all black petg-hf from BL, so maybe a bad batch? IDK
I would say wet filament, but you said its dried, I dont know. the background is out of focus but appears like all the prints have defects at similar, if not the same, height. Might here be contaminates on the nozzle, something sticking? I wish I had a better answer for you. Perhaps it may be a bad batch…
Yeah, I put a new nozzle in right before that run. I have the filament drying again for 24 hours and will rerun and see. If the problem is still there, I will use a different filament and take it from there.
Just throwing this out based on nothing really, are you on the same version of Studio and firmware as when you were getting good prints before? @JonRaymond 's comment on cooling made me wonder if something may have tweaked your fan speed/settings and response to chamber/bed temps? I don’t know if something like that would manifest itself this way (your issue) or not.
I’d say you are if that print takes a year! Just throwing some levity into the mess.
Yes, maybe a bad batch, but what machine were you using before? Was it the same H2S or something else?
What else has changed, firmware, software, or something else? The key question is, what’s changed? Make a list and try eliminating those items one by one.
Another wild thought, if you reduce the number of objects down to say 4 and then try print by object (if possible) do they show the same issues? These look pretty tall, so you may not be able to try something like that.
May not be related, but I was getting the same sort of issue when printing the filament track switch tube guides. I could only print 1 tube guide at a time. I used PETG-HF with PLA/PETG Support Material, both from BL. If I printed more tube guide on the same build plate, the supports would get knocked over, the filament wouldn’t ‘stick’ correctly to the Support material or it literally just wouldn’t print properly. I think as JonRaymond mentioned, it has something to do with the cooling during the prints.
No firmware or software updates in between. Not a fan of Studio updates unless absolutely necessary. It seems that every time there is a Studio update, I have to delete and reinstall a couple of times.
Multiple parts. I always use the Clone feature in Bambu Studio and never had any issues. This feature for me is especially useful when each part has painting on it, a logo in a different color in my case.
I don’t know if anyone has suggested this yet but did you try having Arachne on? That really helps have nice walls and has been suggezted for this issue before.
I just finished a print of the same part with 12 on the build plate on my X1C and it printed perfectly.
I now remember, right before the issue came up on my H2S, I had a extruder feed error on the black and I just fed another color and it fed ok. I’m wondering if I have some filament stuck in the extruder gear that is giving me some periodic trouble?
I have since printed a set of parts with a layer height of 25 twice and they turned out ok???
I think I will take a look inside the extruder and make sure all is clear.