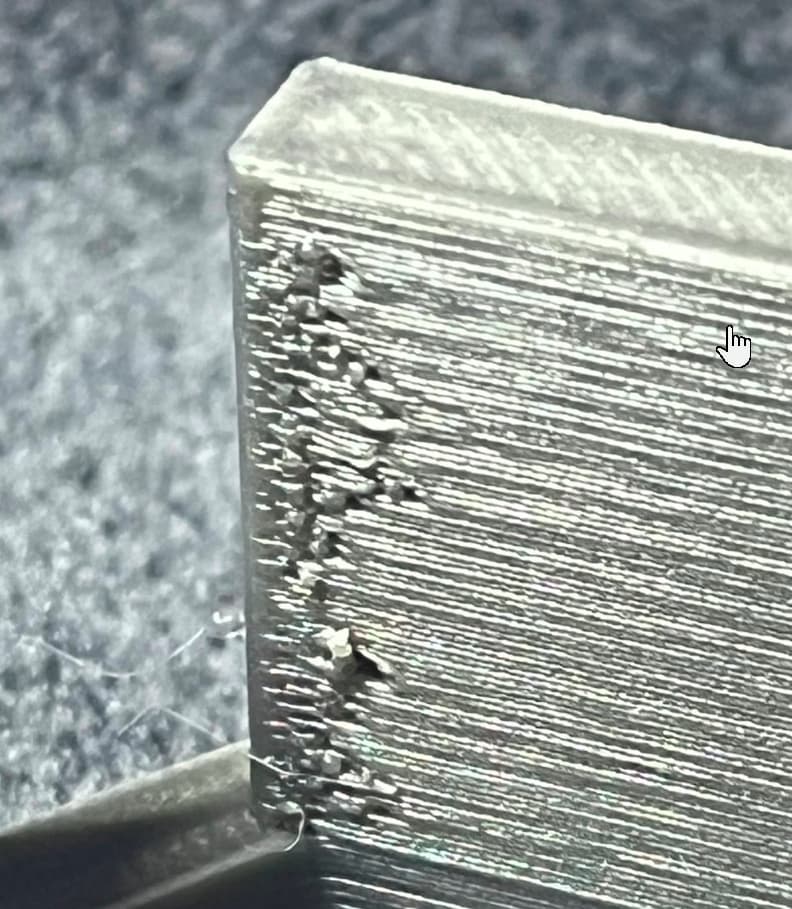
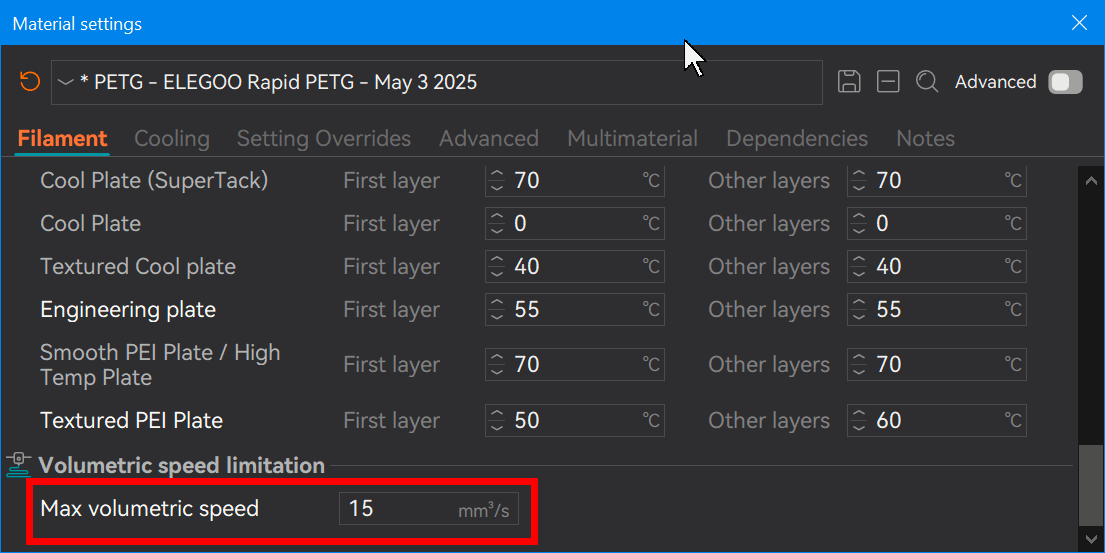
If you’re referring to this segment, my guess is that you’re exceeding the max volumetric flow for your filament. Moisture in the filament is the most likely culprit but you can tweak the profile to get some - not a lot - but some relief.
I’m assuming you either don’t use Orca or aren’t on Beta 2.3 of Bambu Studio. Orca has had built-in calibration tools for over a year, including max volumetric flow. BS just added this in Beta 2.3, but I moved to Orca permanently and deleted Bambu Studio after Bambu’s January stunt with Bambu Connect and their forced privacy compromise under the false flag of “security.” Orca has always been five or six steps ahead of BS anyway. Here’s where that Calibration tool that will help you calibrate max flowrate in Orca, I believe I also saw it now in BS Beta 2.3:

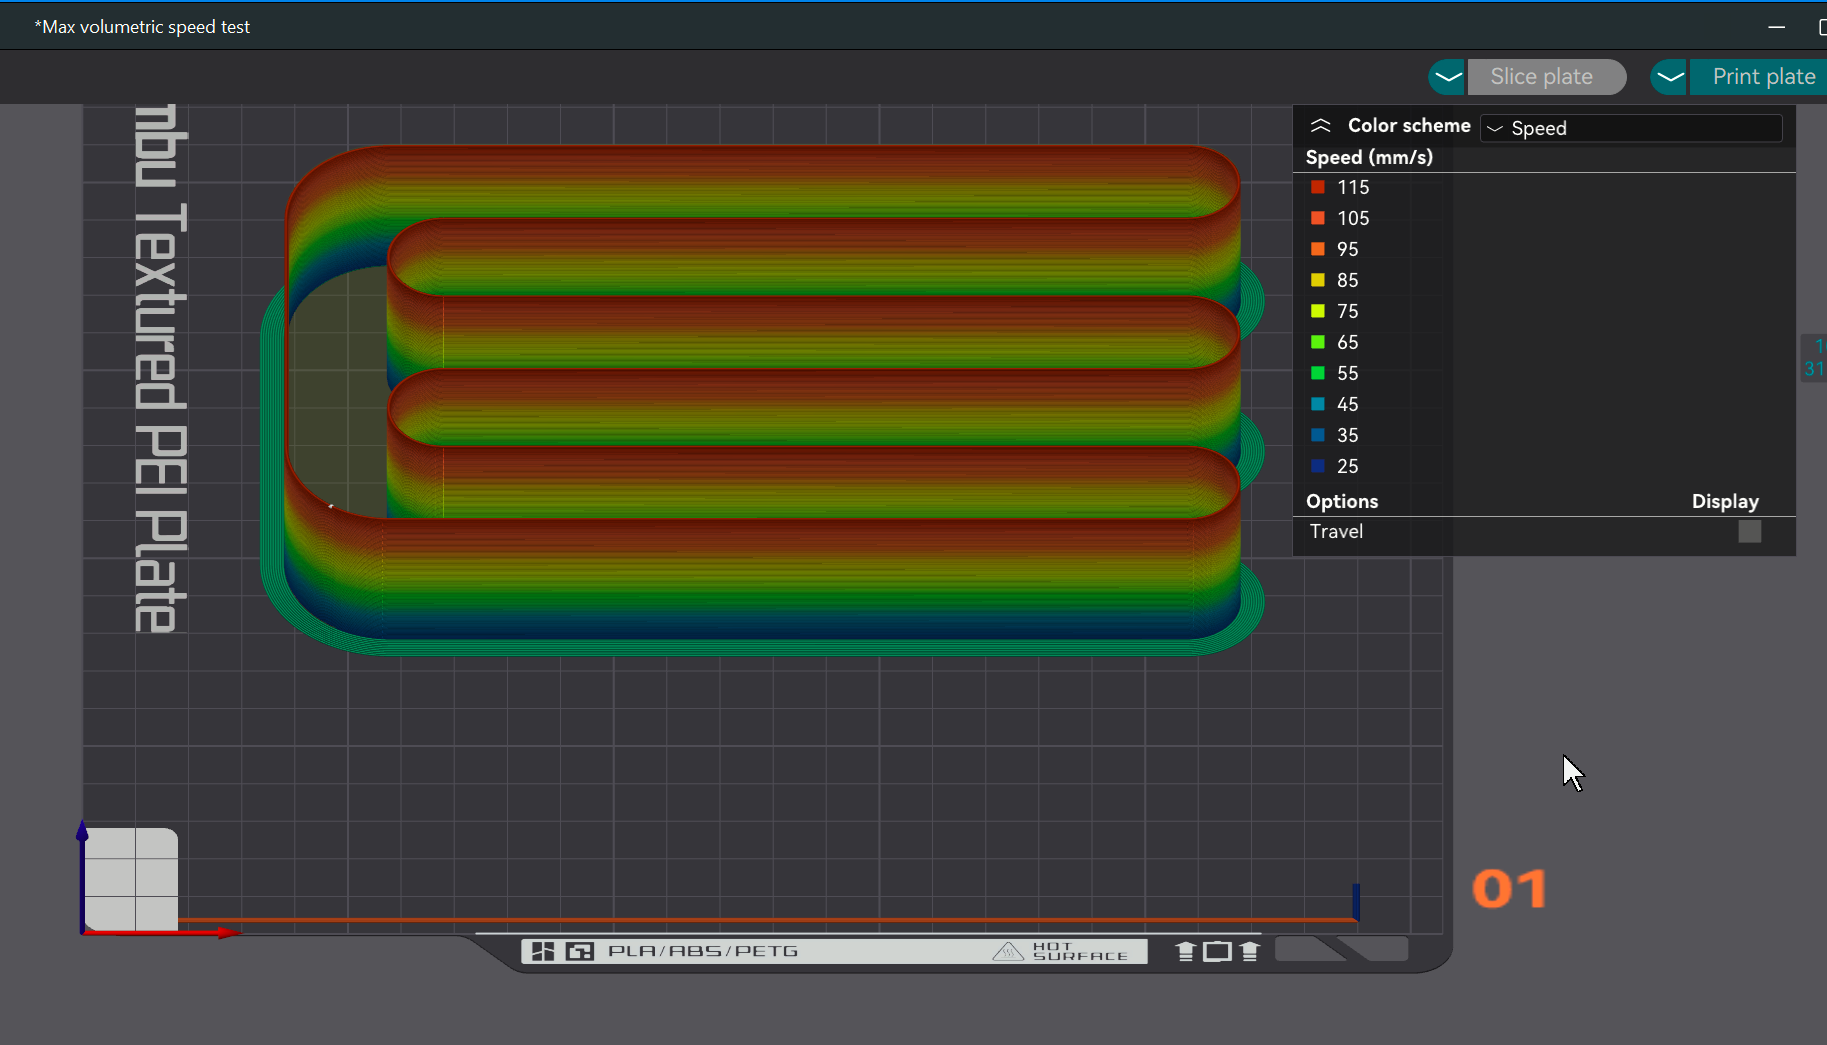
That tool generates this model:
Tutorial: home · OrcaSlicer/OrcaSlicer Wiki · GitHub
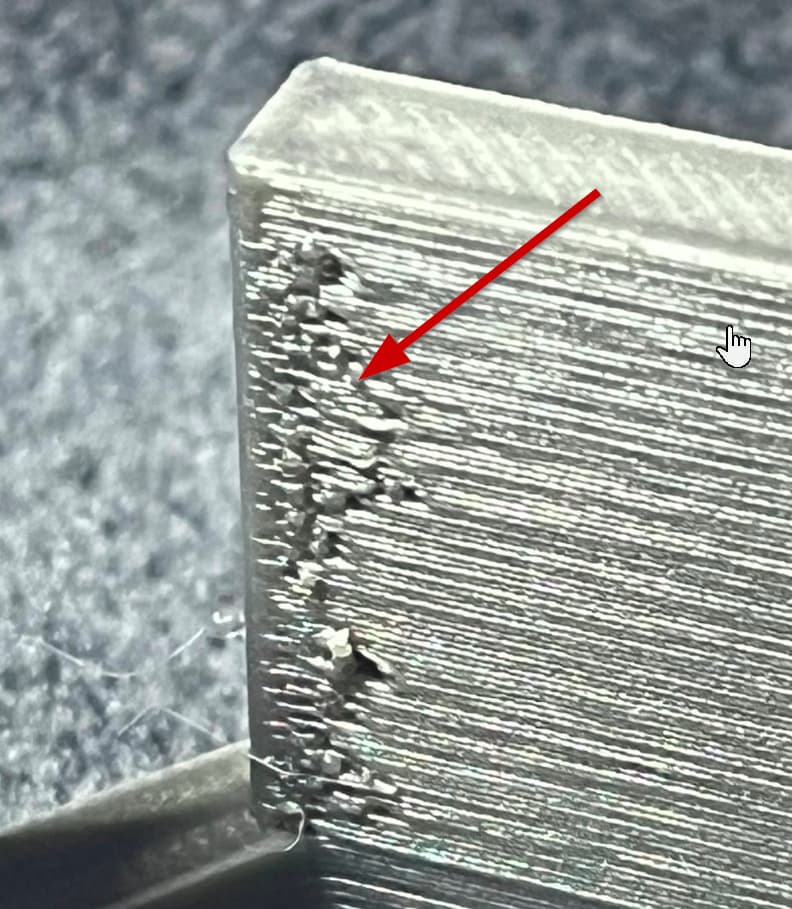
Max volumetric flow (unlike flow rate) measures how fast filament can flow at max temp and max nozzle speed. The rainbow effect in the above picture shows increasing speeds. You know you’re exceeding flow when it looks like this and that measurement point is what you want to put in the filament profile:
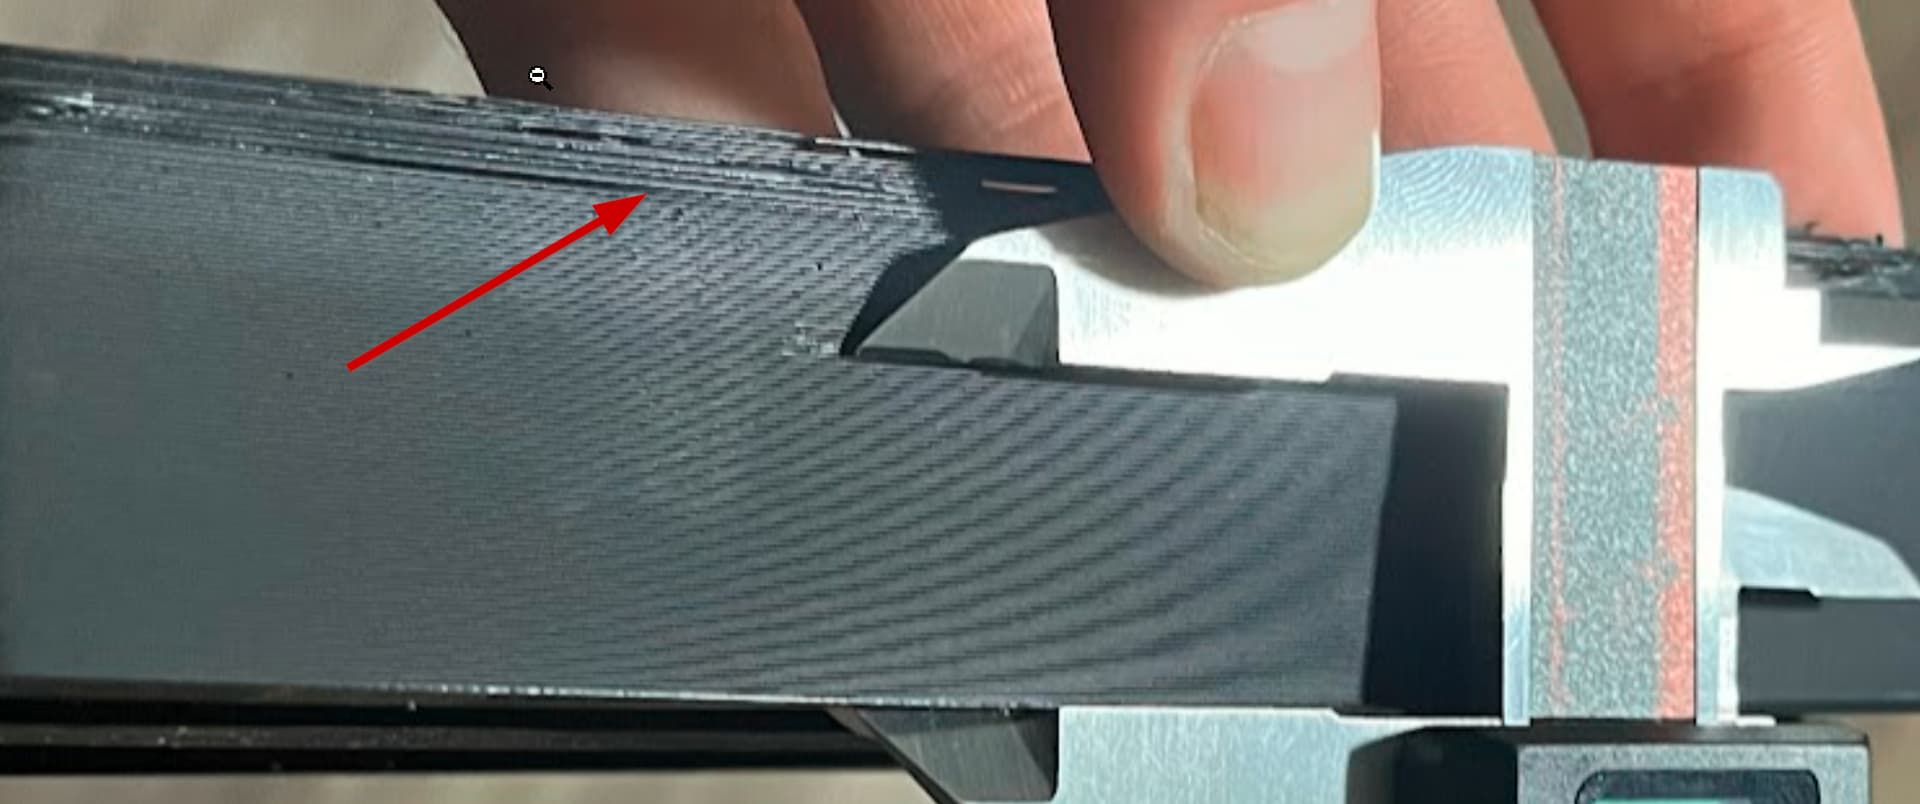
Or, in your case:
Once determined, enter that number here:
If you don’t use Orca or BS 2.3, try this MakerWorld test model. It varies G-code speed similarly:
https://makerworld.com/en/models/85600-bambu-slicer-max-flow-test-tower?from=search#profileId-91491
(I haven’t tested it since I use Orca.)
NOTE: Calibrating Max Flow Rate is not a substitute for drying filament.
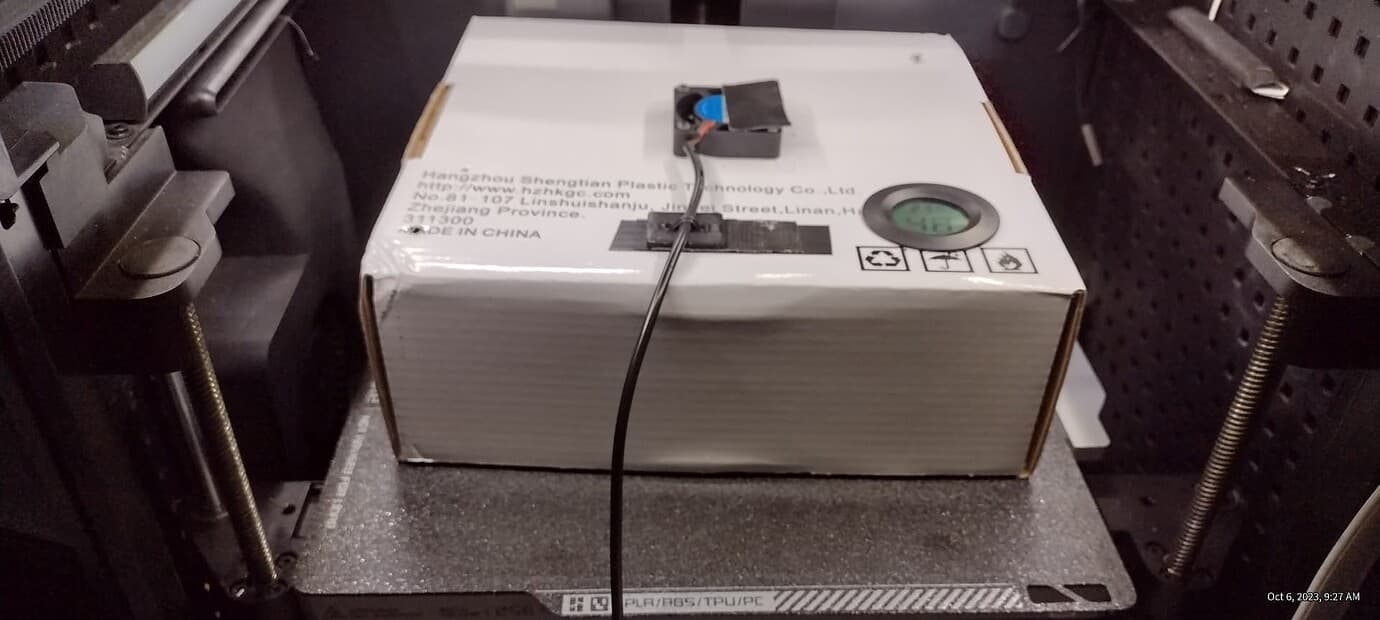
Even if this helps with corners, dry your filament. No dryer? Use your build plate and the cardboard box it came in:
Here’s my P1 setup (yes, I overdid it with a fan and hygrometer):
Weigh your filament before and after drying.
Moisture may not be the cause, but weighing confirms it. Elegoo PETG’s cardboard spool alone can hold 4-6g of water. If you lose 6g, it may have been the spool, but now you know it’s dry.
How to confirm: weigh every 4-6 hours. Flip the spool every 12 hours over 24 hours using the printbed method (≈60°C). Closing the box can increase heat but risks warping one side of the spool.