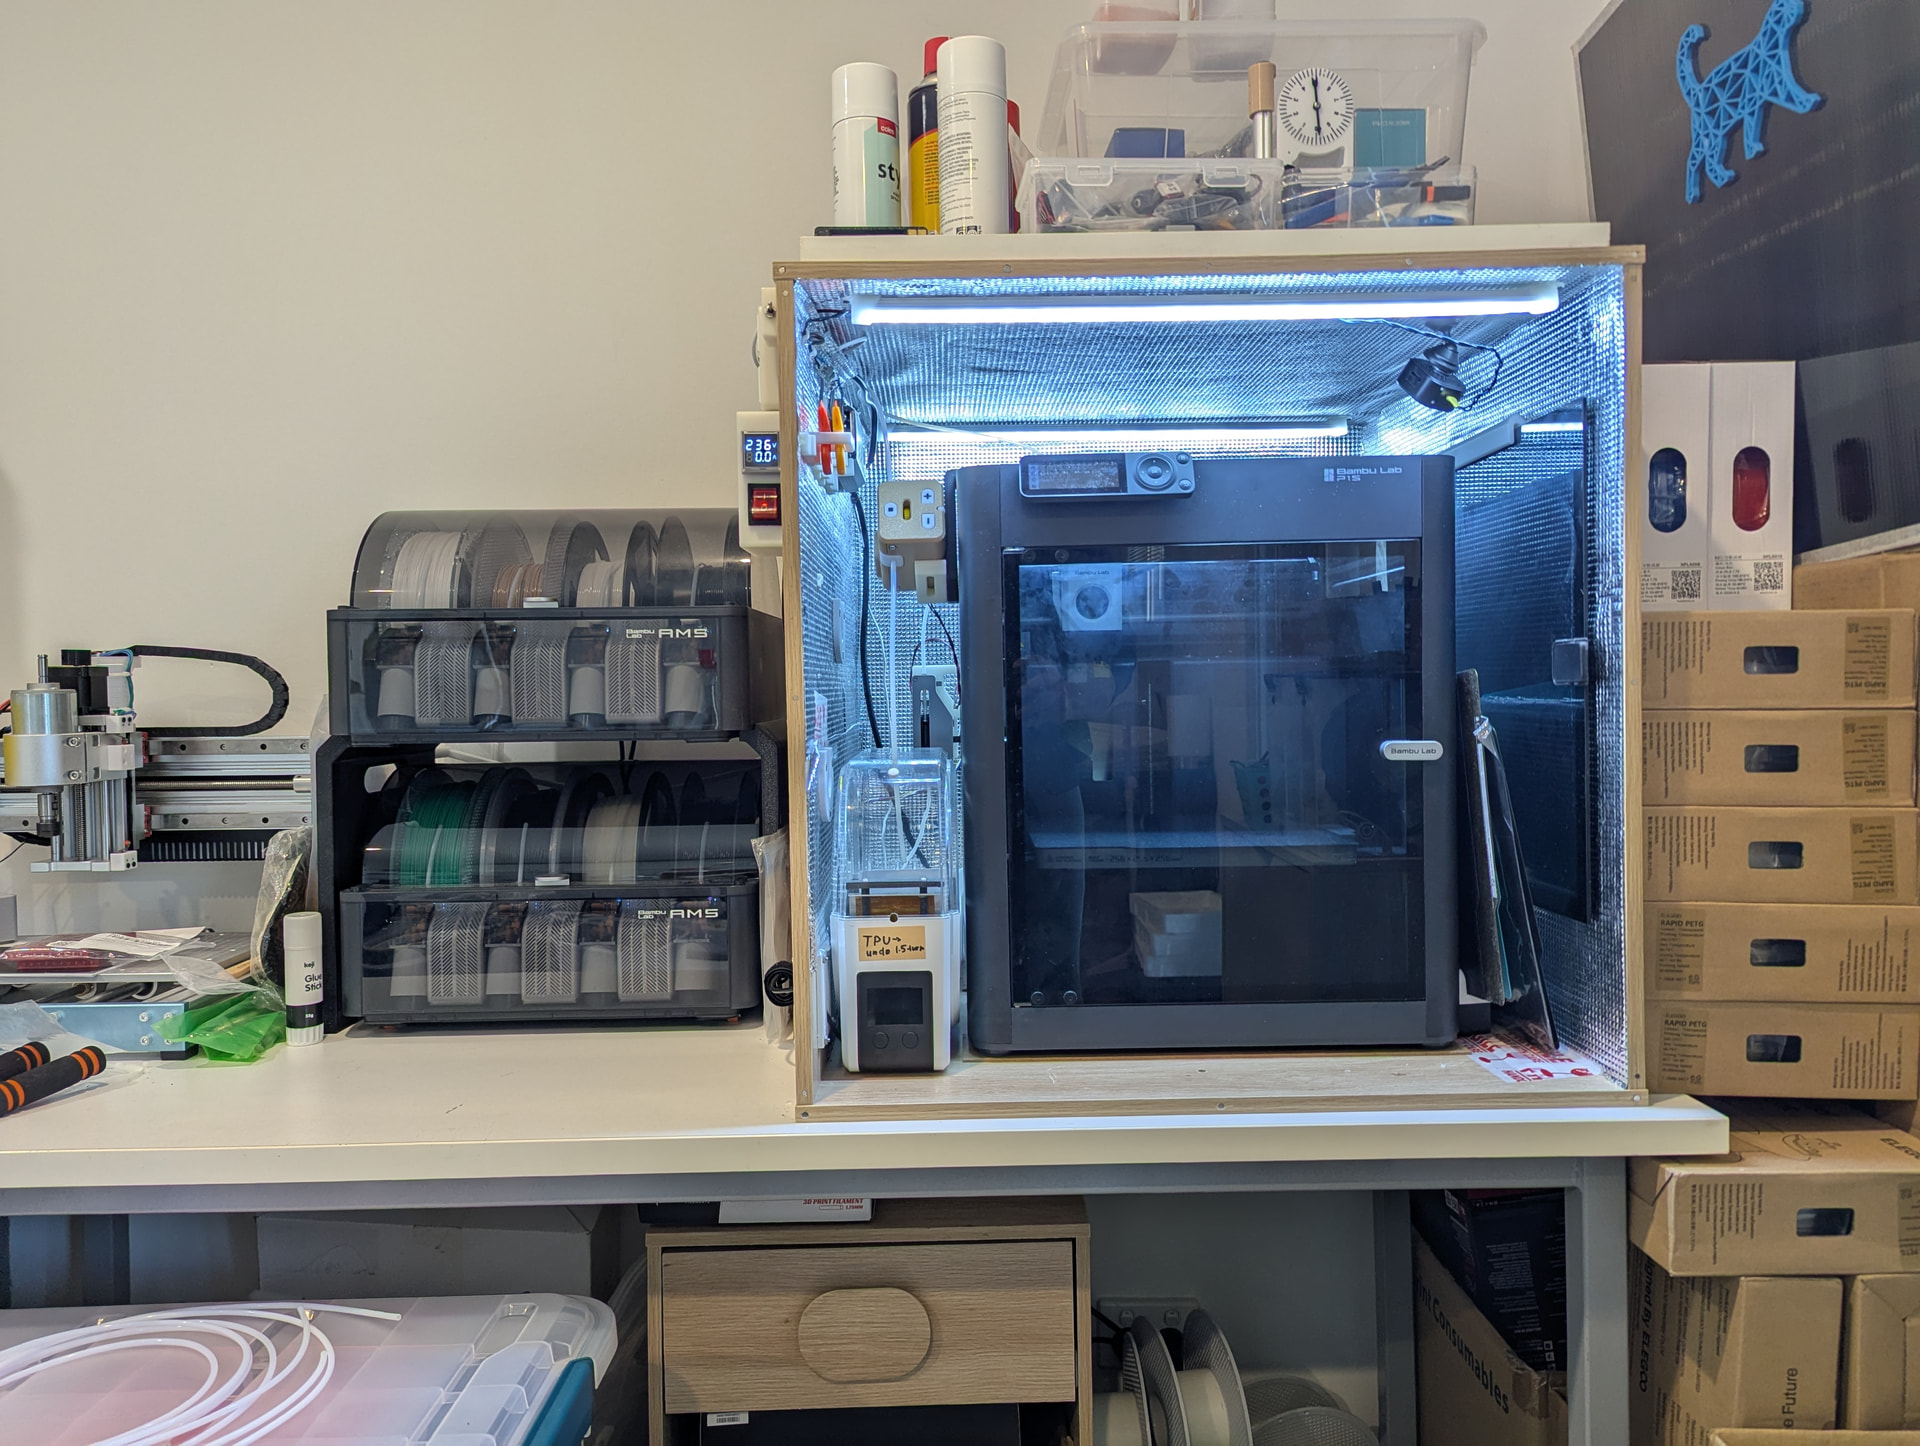
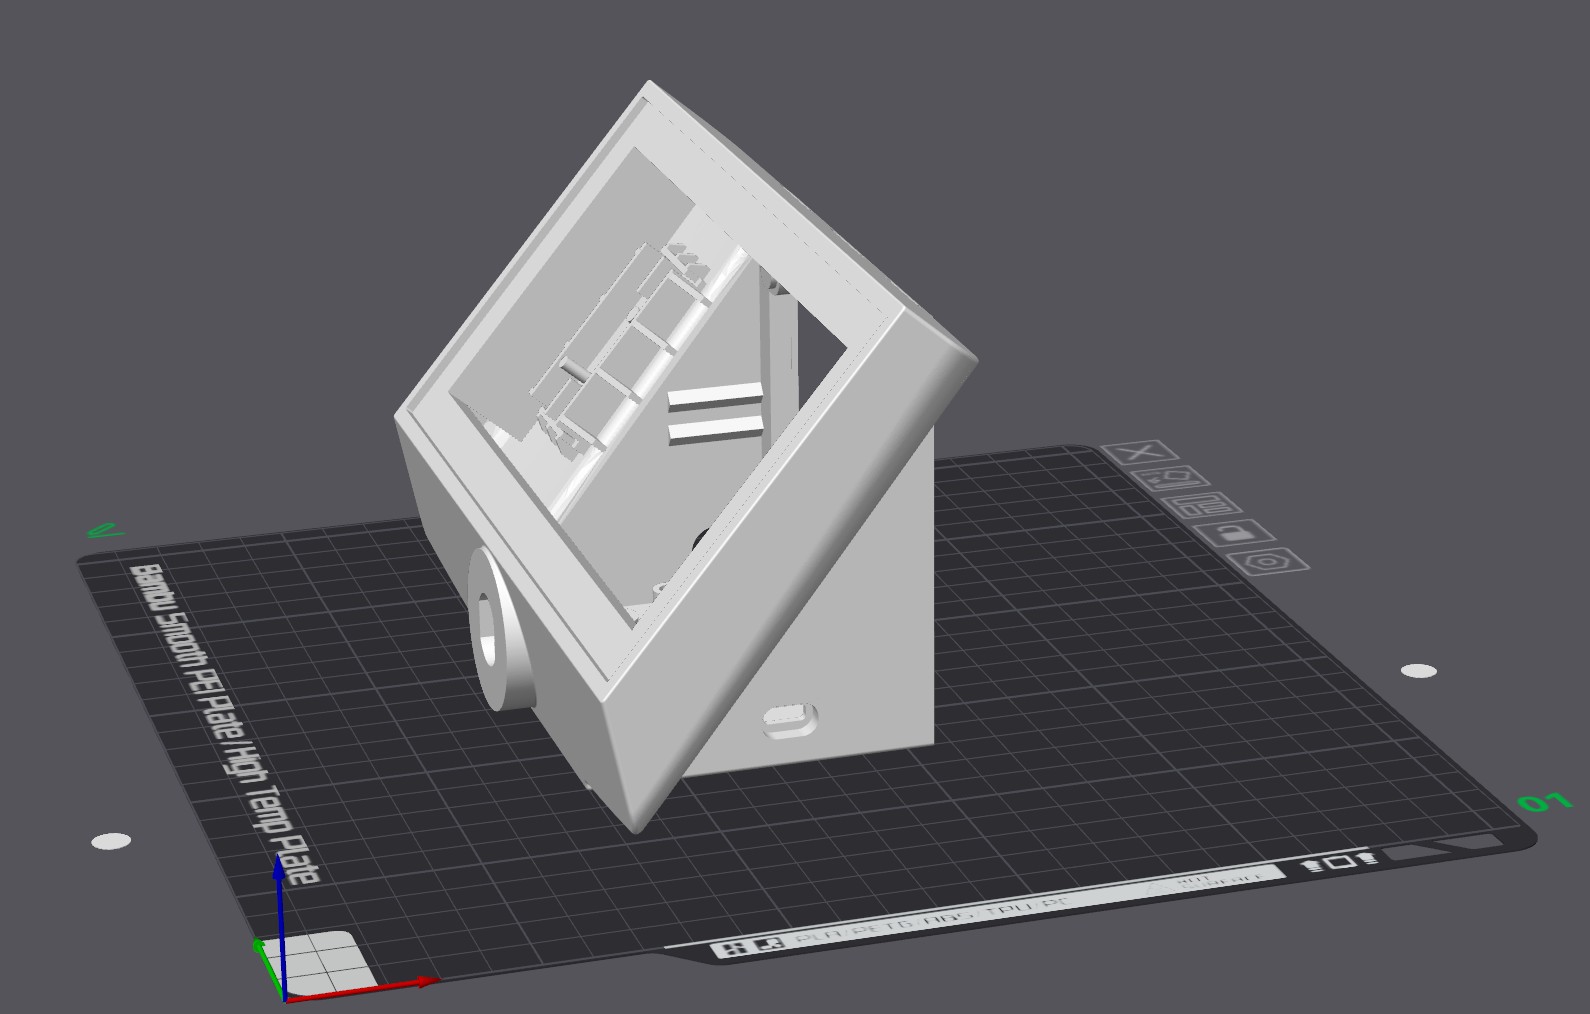
Hello everyone. I am already in despair as it can’t seem to get even close to a quality print from ASA. The problem is that the key dimensions are drifting. The long side of a 180mm x 90mm rectangular opening ends up every time warped, as shown in the image. I am printing with Flashforge ASA filament.
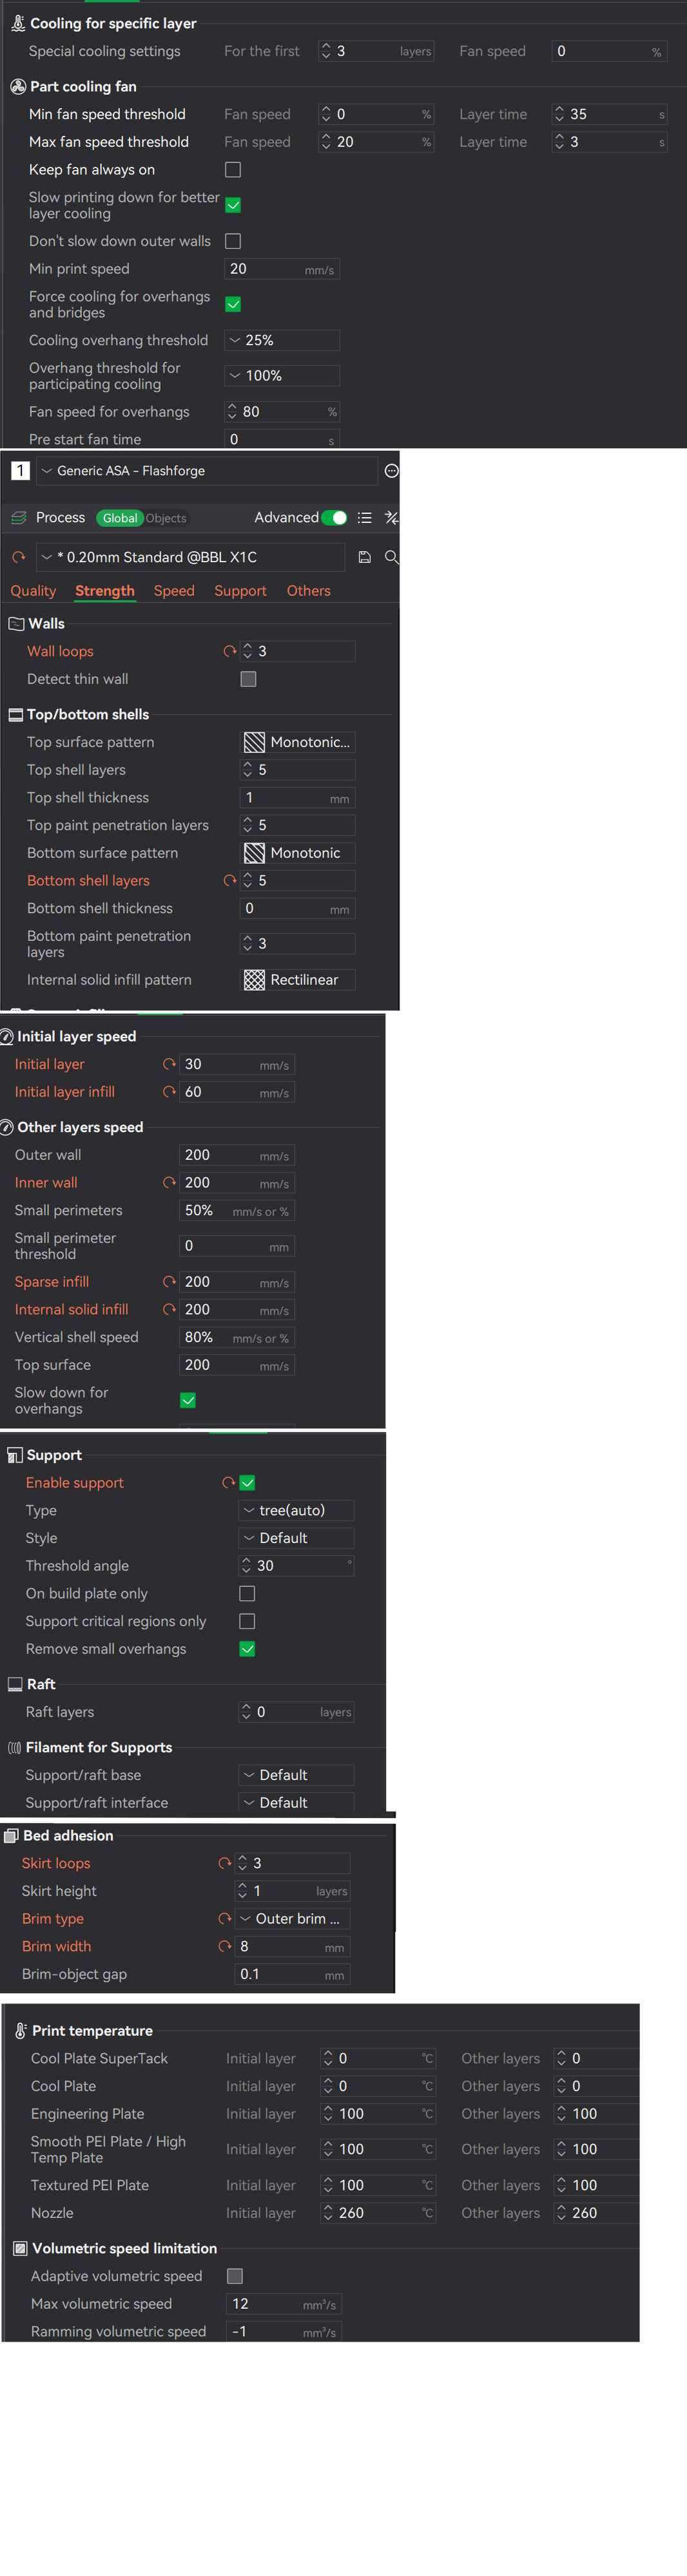
The filament is calibrated, I preheat the chamber to 45°C (I can’t go any higher with the P1S), and I leave the part in the chamber until it cools completely after printing. I have listed all my print settings below. What am I doing wrong? Is it just the filament? Low chamber temperature? Filament temperature? Print speeds? Flow dynamics? Infill? Highly appreciate your help.
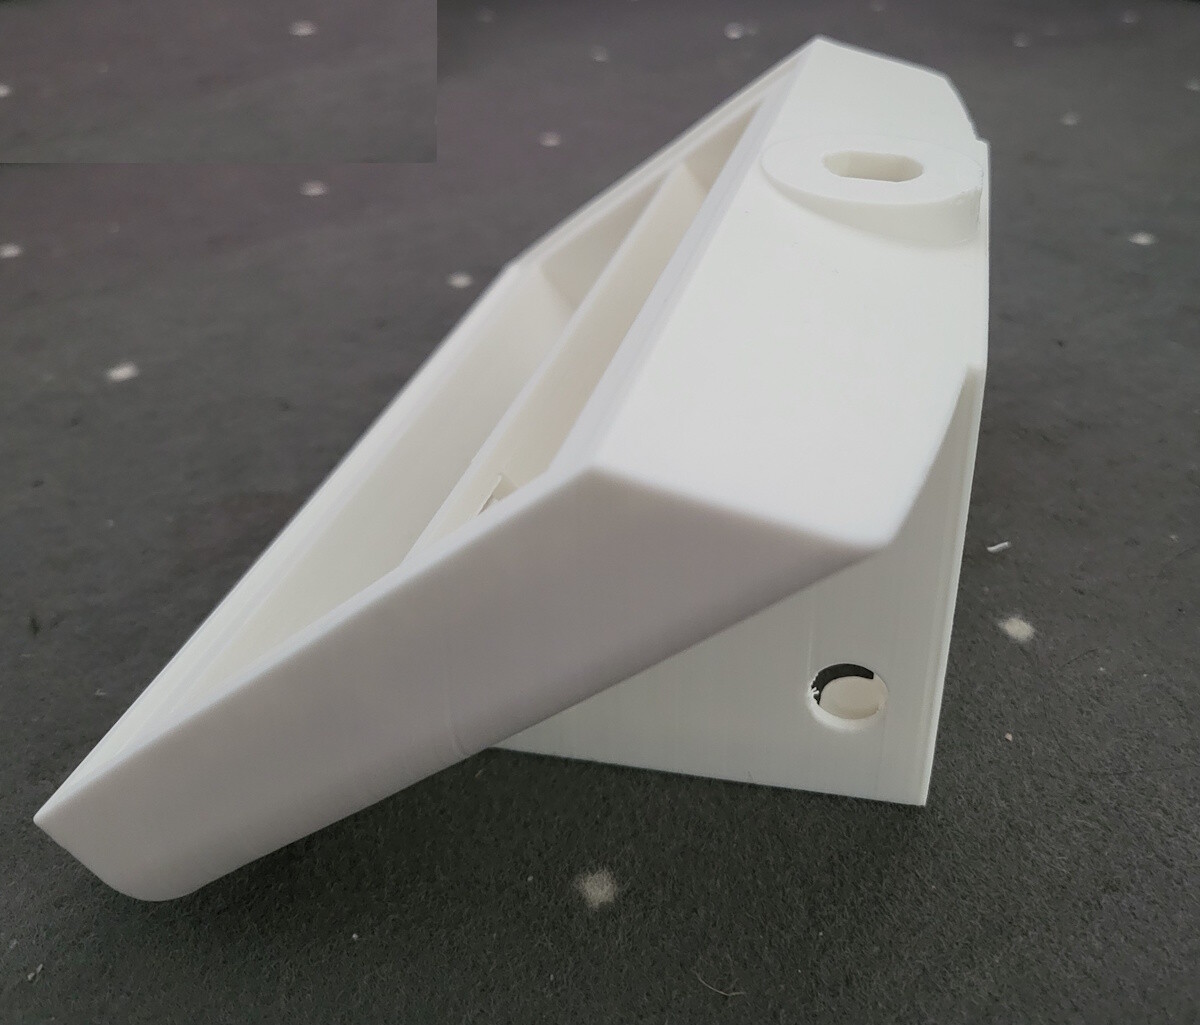
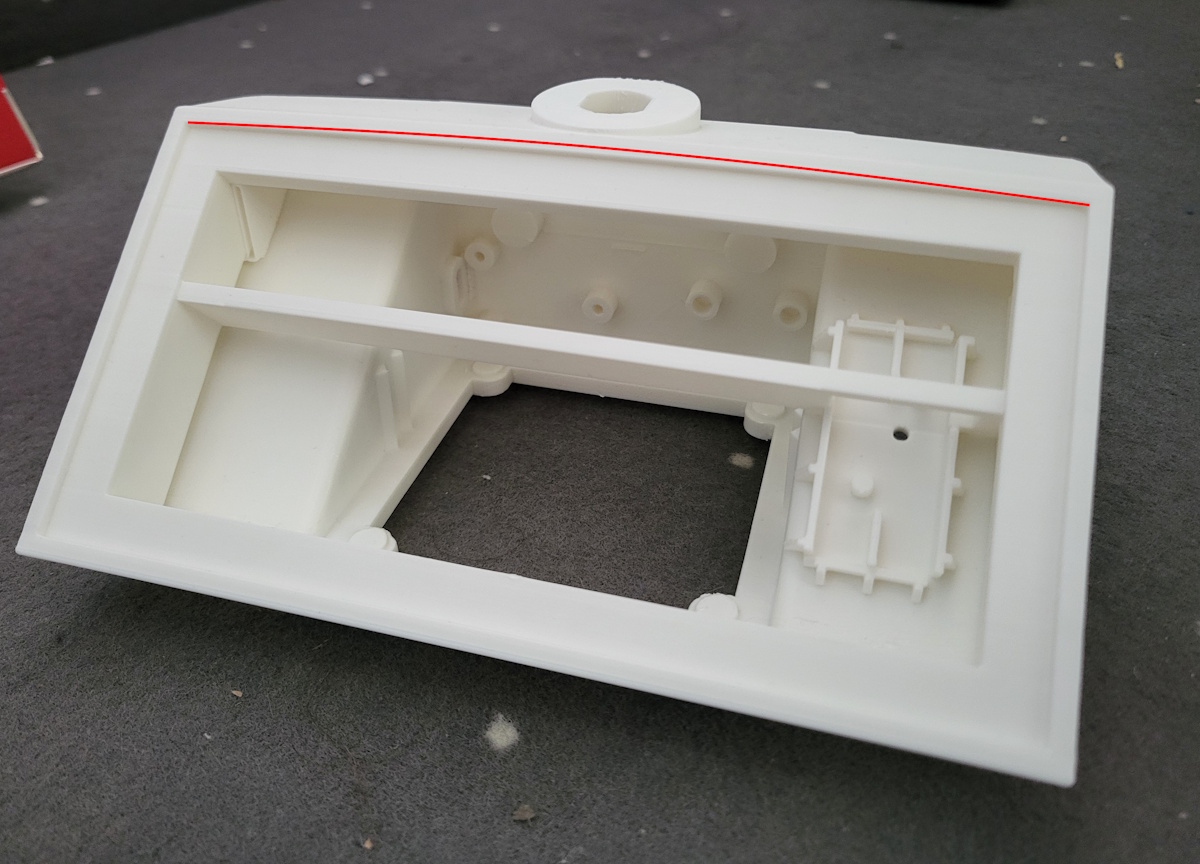

ASA is prone to warping. As it cools, it shrinks, and this causes it to warp.
There are many guides on reducing warping that will tell you howe to manage the temperature in the chamber so it cools less, and more evenly, or how to change the geometry such as adding “cuts” to the model that will take up the pressure when shrinking.
(For example, putting a square grid of grooves into the base of a large flat object, so that the grooves take up the shrink and stop the corners - or the middle in your case - lifting; )
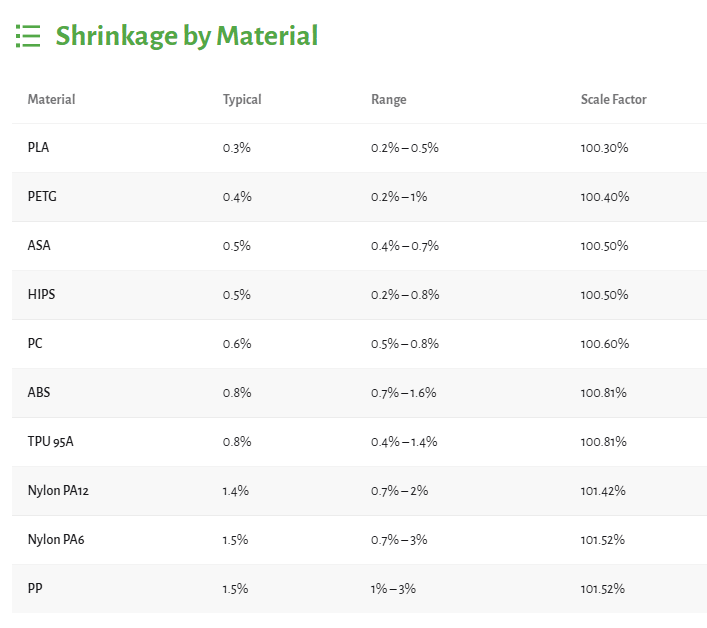
At some point you may also have to scale up the model slightly to allow for all around shrinkage.
45°C is not enough to reduce warping during ASA print. So you might have to make investment in active chamber heater or insulate the printer somehow to reduce the heat loss to the room.
A general knowledge: heat exchange happens faster if one side is a lot hotter than other side. Heat loss will be higher when chamber temperature becomes higher.
I suggest you choose ASA-GF. The glass fibre does not change much of ASA properties except for making it easier to print, and maybe it comes the matte surface to hide layer lines.
Thank you. I must say that I’m using during the printing an external exhausting filter, which might even reduce the temperature from the 45C. But I read that people printed ASA even without heating the chamber at all. So could it be a filament ‘issue’?
Thank you, interesting idea with the grooves. How they should look like in terms of its depth/ width?
I’ve been printing w/ ASA all day, and have opened my door numerous times to remove prints. Currently, the chamber is sitting at 53C as I head to bed to let a 6 1/2 hour print run.
I’ve been managing to keep my P1s’ internal temp hovering around or above 50C pretty consistently using two methods:
-
Printing “plugs” for the many holes in the P1s enclosure that end up allowing for significant air exchange. You can start with the easier ones, then move to things like gaskets for the door/lid glass, and other things, if necessary. There are many profiles for these pieces on Makerworld. Look for ones that specifically are designed for ABS/ASA, and you’ll have much better results.
-
Purchasing and installing a Bentobox (in the US, can be purchased from VoxelPLA) in-chamber HEPA/Carbon air filter, and using that to circulate the air within the chamber, while turning off the external fans.
These two steps have had the added benefit of significantly reducing (but not eliminating!) the smell of the ABS / ASA escaping into the outside room. If I’m only printing PLA or PETG, I just leave the bentobox off, saving it for the ASA / ABS prints.
I haven’t really bothered with trying to using blankets or insulation on the outside of the P1s yet, as this seems to have been enough for printing ASA and ABS.
Thanks for sharing. What ASA brand do you use and what speeds are when printing ASA?
So far I’ve only used BambuLab ASA and FlashForge ASA and ASA-CF.
I’ll also note that my printer is housed in my garage, so I don’t lose use of a room inside my home while printing with ABS or ASA.