After trying TPU for the first on my H2D and getting a lot of string, I saw the temp was 20 over manufacturer’s recommendation. I updated it in the TPU generic profile and saved it, when I choose that in the prepare section, and slice, the machine seems to use the generic settings temp anyway. Anyone else running into this?
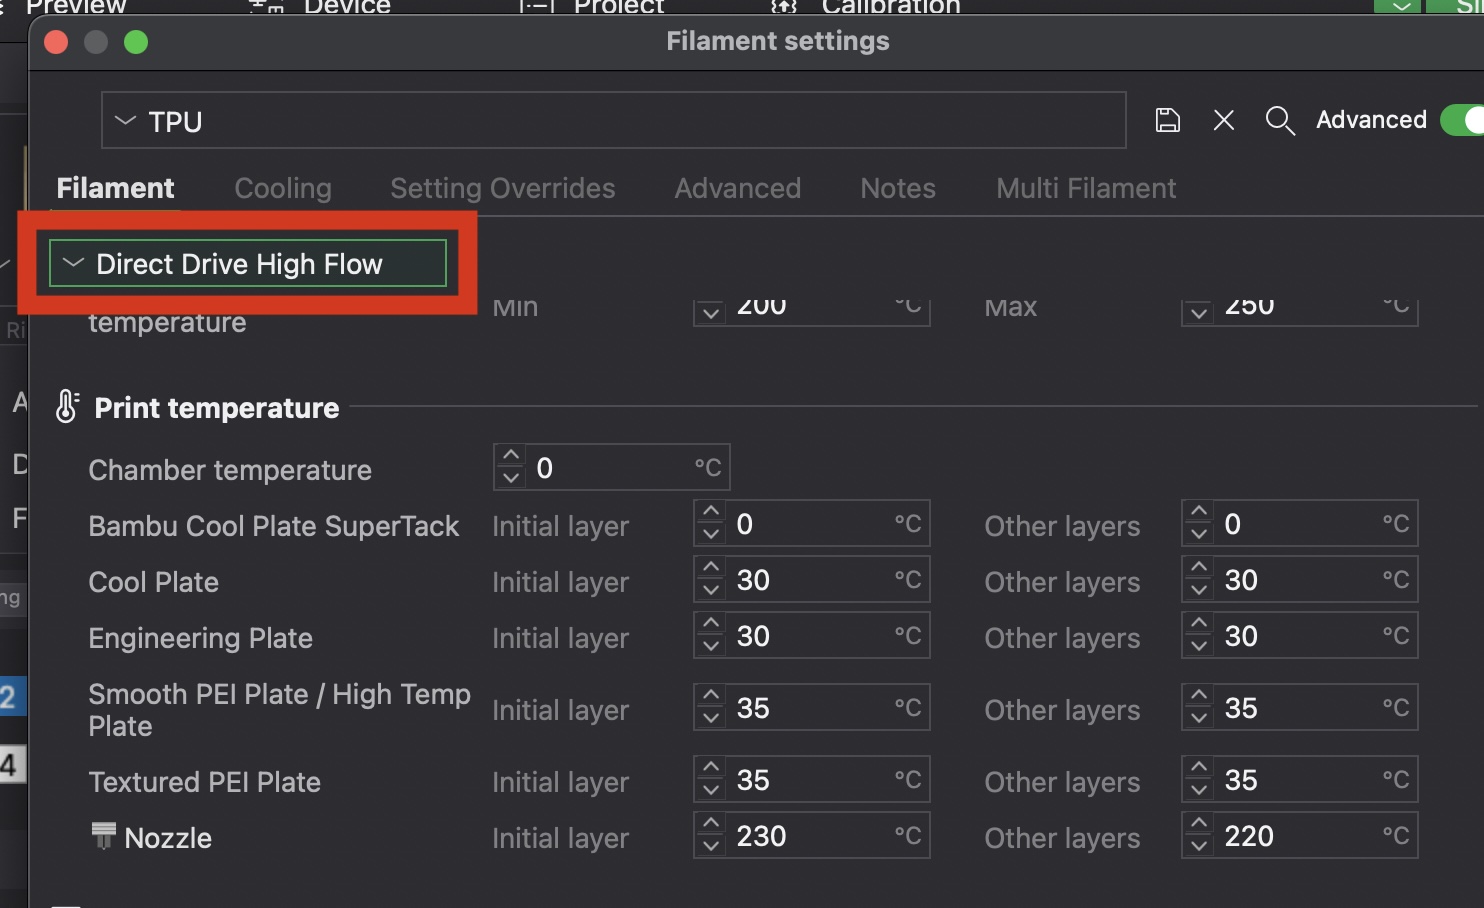
Thank you. I am using HF nozzles but changing the standard nozzle settings. It never occurred to me to click that dropdown and see that there are separate settings based on type of nozzle. I will try those other suggestions as well.
Thanx again.
Also after a lot of testing with H2D with HF hot ends and TPU I found the best way to reduce stringing is by lowering the temps. I pretty much completely eliminated stringing with generic 95A TPU and Bambu TPU 95A HF by lowering the temp to 230c for HF and 220c for regular TPU.