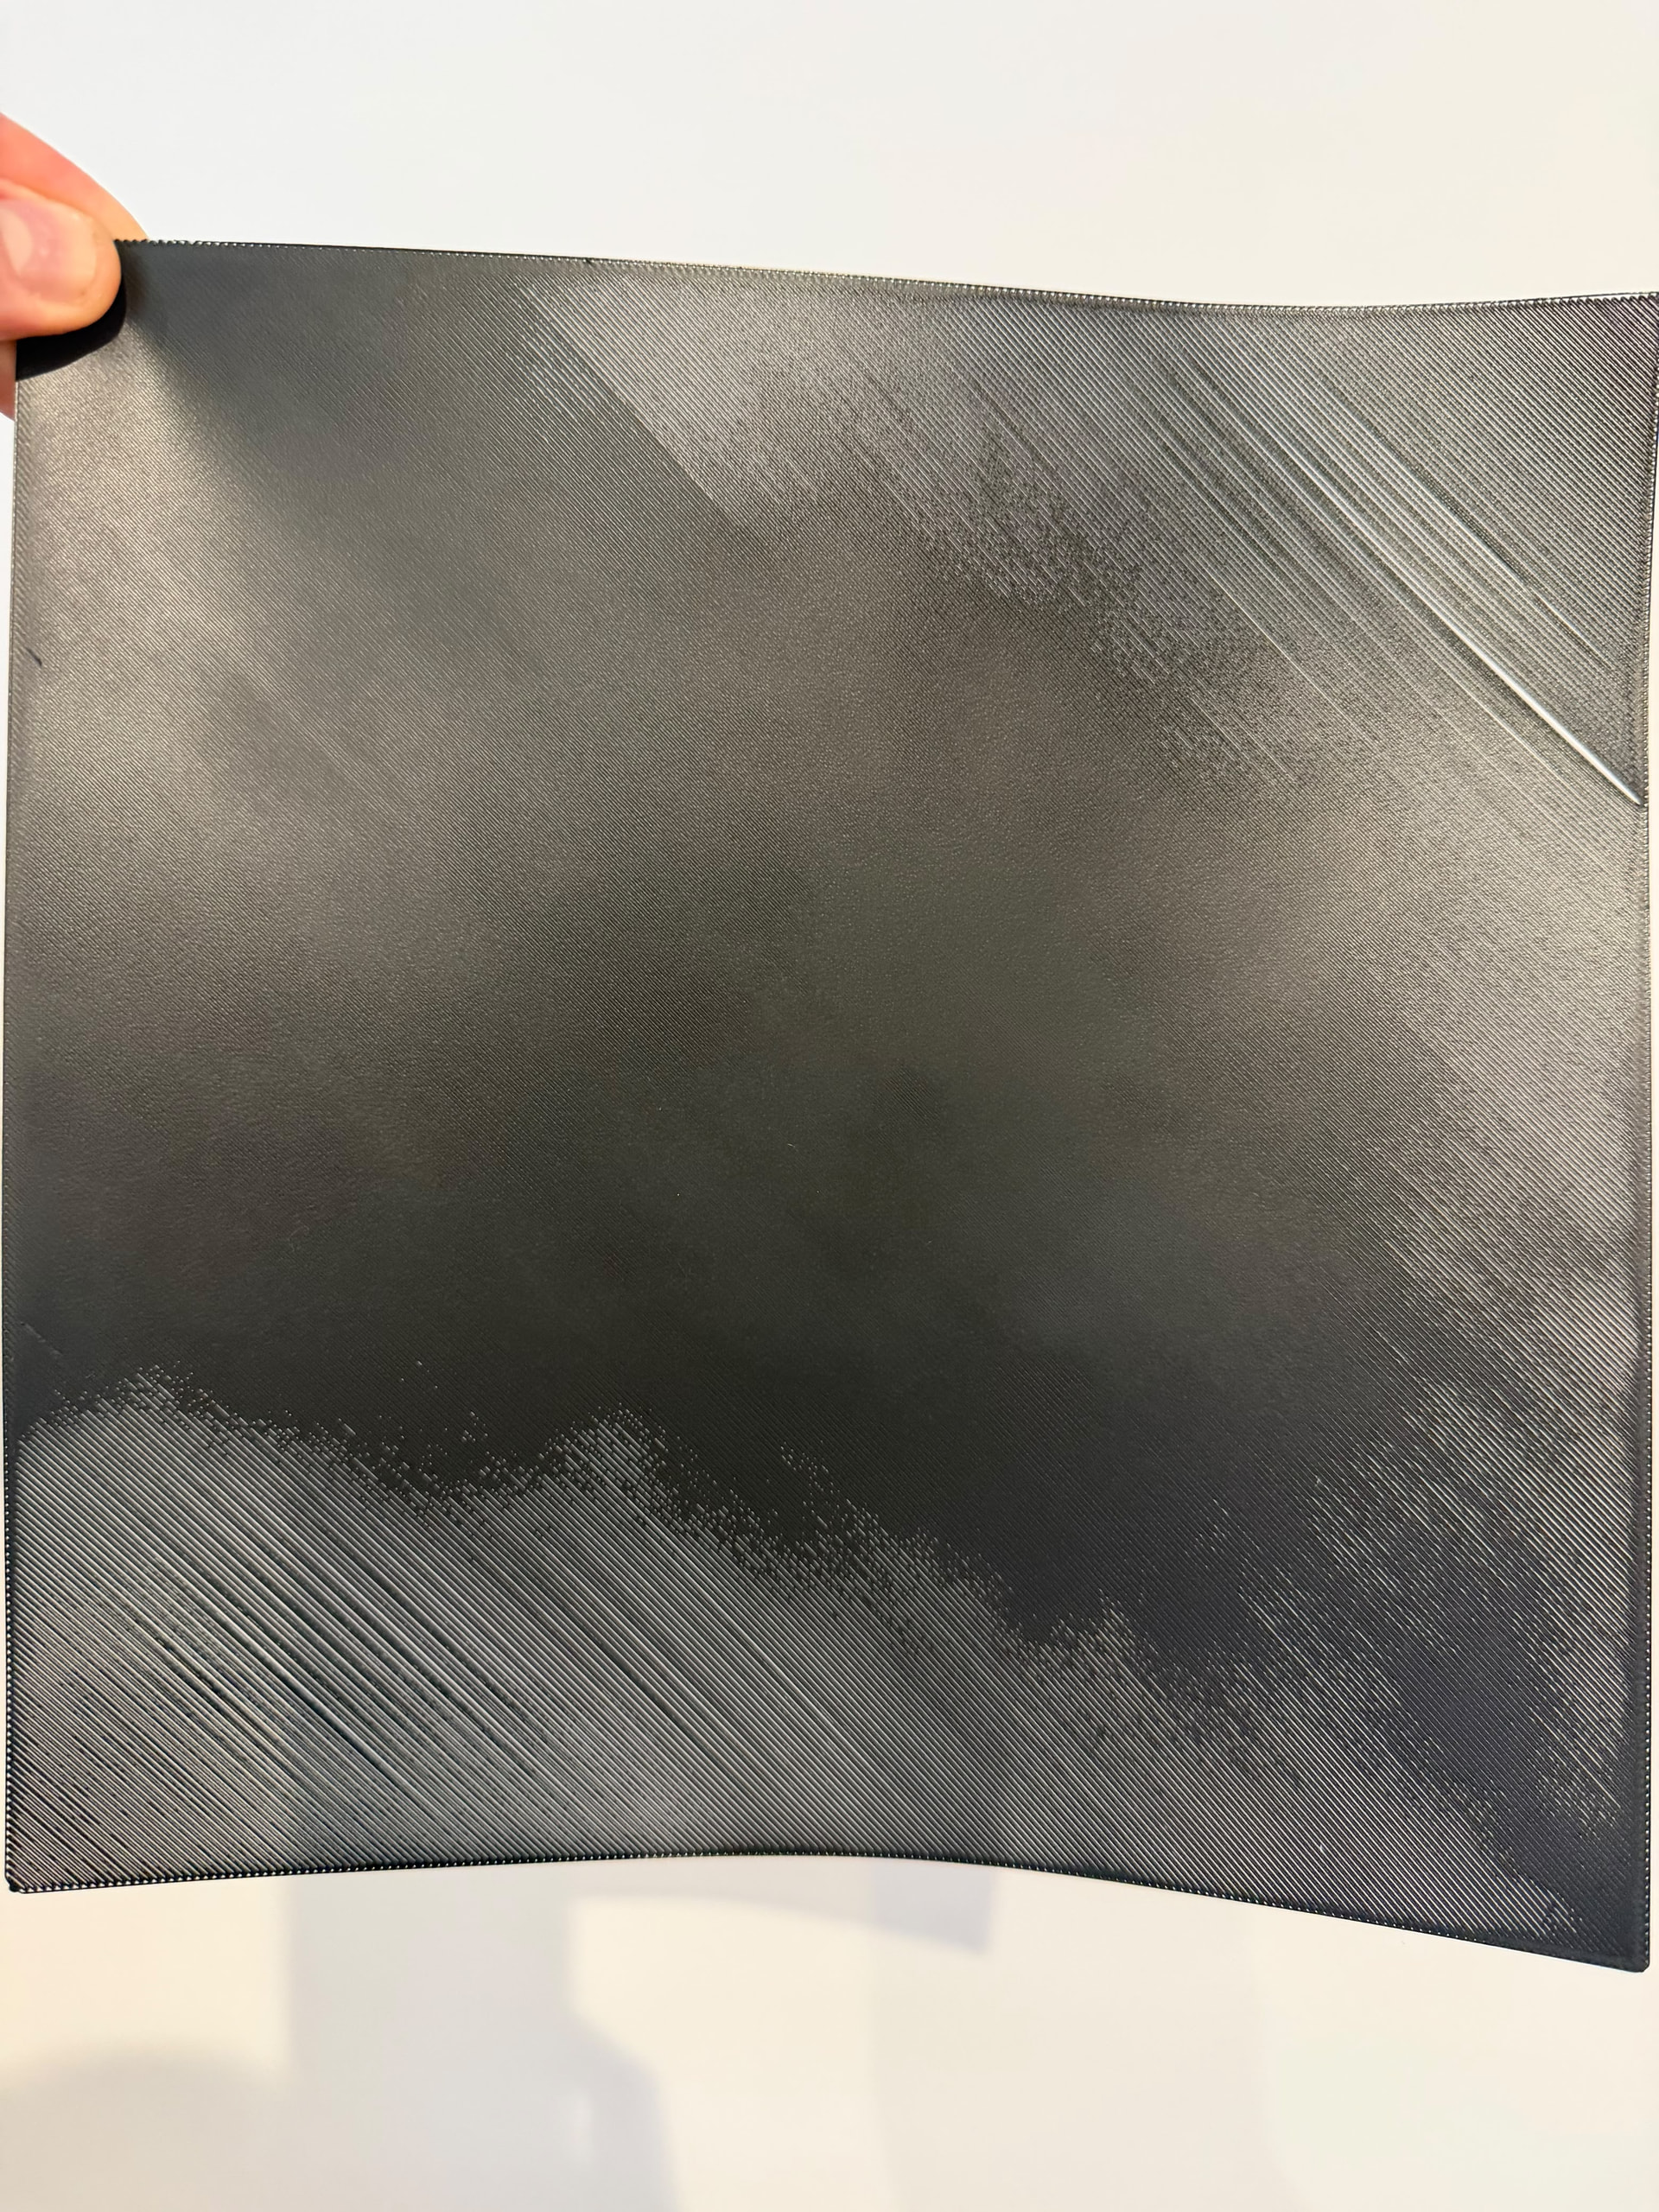
I find the auto calibration results are always way off the manual calibration results. All my PETG is around 0.034-0.038 and 0.95 flow rate.
I have the same issue. Brand new X2D with 30h of print time.


After manual bed levelling and auto-calibration from printer menu:

After rotating plate 180° (don’t mind the bits at the top edge, it just printed outside the plate).
I should note that I did not run the bed calibration from the printer menu. It only did the auto-bed levelling at the start of the print (what’s the difference?).

Has anyone else tried printing a 1-layer sheet successfully? This feels like a firmware issue to me. Nothing seems to be loose.
The only slightly odd thing I noticed is that I have a bit of plastic squeaking when the Z axis moves, but it’s minor.
I have contacted support and they suggested to do the manual levelling, plus a bunch of things that shouldn’t be relevant: increasing nozzle/bed temperature, reducing print speed, flow calibration. Temperatures and speeds are set by Bambu and everything including the filament is their own hardware. The first layer is just a bunch of lines extruded at constant speed, so I don’t see what flow rate has to do with it.
It can’t be a filament issue because I first noticed the problem on the first layer on a different roll of filament. And if it was, it would happen at random spots.
The OP said PETG and dried for 6 hours but gave no details. Lots of hardware changes/tuning/tightening and the problem persists.
I don’t know it’s moisture in the filament but I suspect it is. PETG loves water and needs to be well-dried for best results. 6 hours is possibly a bit short for drying.
Those seeing this can sort if it might be water by placing the spool of filament in a sealed ziplock bag or sealing poly cereal box with a hygrometer (no desiccant) and sealing it. In about an hour the filament will dominate the humidity reading and the humidity reading will be proportional to filament moisture. With PETG, if you’re much above 20%, water could be the issue.
It actually can be a filament issue. If it is filament moisture (not saying it is), then it could be symptomatic of how filament is being dried and stored where multiple spools behave similarly.
When filament gets iffy and more subject to exhibiting problems you can see issues appear in various locations like near doors and fans and it would be somewhat repeatable.
That squeaking in the z axis can be the belt tensioner angled a little and the toothed belt rubbing against the flanged edge of a pulley. Check the wiki but Bambu advises using a little of the supplied grease on the edge of the belt to quieten it. It sounded like squeaking plastic on mine but was belt rubbing. But check the wiki for more info.
It can’t be a problem with the plastic, since the unprinted areas are almost in the same places. I also tried printing with orange plastic and the effect is the same.
I’m not saying that it is a problem with the plastic — just that it might be. But you can indeed have print problems show up in the same locations from a filament issue. And if you follow the same drying/storage procedures either by luck or design, you can have different spools of filament behave similarly.
There’s lots of examples of this in the forum. You don’t have to take my word for it. And it might not be your problem. But it also might be.
MZip
When filament gets iffy and more subject to exhibiting problems you can see issues appear in various locations like near doors and fans and it would be somewhat repeatable.
The filament rolls I noticed the issue with are both brand-new Bambu PLA Matte that I ordered with the printer. I also printed PETG and ASA, but there was little contact surface so I didn’t check/notice.
I never dried filament with my previous printer and never had this sort of issue. I had micro-bubbles on PETG which gave the part a bad surface, but never first layer patches like this.
As both me and @homyak046 pointed out, if there was something wrong with the filament (like non-constant diameter), the issue would manifest at random spots in the plate. I understand the argument about some locations of the printer possibly slightly cooler due to proximity to fans etc, but the part is stuck really well to the plate. So, I believe the root issue can’t be lack of adhesion at those spots. When I print the next test, I might try to nudge the lines on those spots to check if they’re sticking or not before pulling the whole sheet off.
I have loosened and re-tightened the screws that fix the bed to the 2 Z ledscrews at the front. This seems to have fixed the minor squeak I mentioned earlier.
I have re-washed the plate and printed another test but got the same result.
Something that leaves me puzzled is that on the problematic spots the lines seem to be joined in pairs (gaps between 2 lines, not between every line):

I wonder if this could have something to do with XY instead of Z. @homyak046 is it the same for you?
Anyway… I’m done for today.
We hear that a lot. One of the provoking issues is these printers print pretty fast and the filament doesn’t spend much time warming before it gets shoved into the molten pool.
My old Makerbot also didn’t care much about filament moisture though I can see some slight moisture issues in the prints. But never failures or scarring. Slowing down printing is a way to reduce water issues because the filament has more time for water to vaporize before it gets trapped in the melt.
The microbubbles comment is a clue on water. It sounds like you were close with your previous printer. And if you never dried it before, I’m guessing you aren’t drying now? Storage in the open?
And new spools of filament are not a guarantee of dryness. The plastic bags are permeable to water vapor. That’s why the desiccant pack is in there — to scavenge water that leaks in. “New” filament can have too high of moisture content depending on its history sitting on docks and in warehouses.
And I’m not saying anything about filament diameter. That could certainly cause random issues not in the same places on build plates. Moisture content and filament diameter uniformity are two very different things with very different symptoms.
Above, I showed a comparison of manual and automatic calibration (the result is obvious). The problem is definitely not the plastic; the problem is saving the table height. For some reason, it doesn’t save. Resetting to factory settings doesn’t help. I haven’t had any creaking noises on the Z-axis.
I’m confused… my understanding is that the “manual levelling” doesn’t save any calibration, it just makes you physically adjust the bed so that it’s mostly parallel to the XY plane of the printhead. The g-code they give you to do the calibration simply moves the head to 3 spots, it doesn’t do anything special.
Once the bed is parallel to the XY plane, auto-levelling can be used to:
- Apply a more precise correction that what one might be able to achieve by turning the screws
- More importantly, compensate for the bed not being perfectly flat. For instance, if the bed is banana-shaped, no matter how well you do the manual levelling with the screws, you’ll always have a dip in the center.
Since you got a good result after doing the manual levelling, I wonder if the compensation remained disabled. The manual-levelling g-code contains this line:
G29.2 S0 ; turn off pos comp
I assume it disables the compensation so the head remains at a fixed height to let you level the bed. Perhaps you disabled the auto-levelling on the next print and it ran the print with compensation still disabled from that g-code?
That sounds like under extrusion. Look for anything that might be restricting filament movement. Remove any non-stock PTFE tubing guides, and check for sharp bends in the tubing at all positions of the print head.
Ok, so I think I have fixed the problem.
I’ve done 3 things:
- Dried the PLA 6h at 45° in the AMS 2 Pro
- Re-tightened the heating assembly
- Re-adjusted the left nozzle eddy current sensor
I’m not sure which one fixed it, but I would bet on the sensor.
The PLA wasn’t that wet. Humidity in the AMS was 34% before and it went down to 24% but now is 29%. Hard to tell the humidity in the filament by measuring the air.
The heating assembly wasn’t loose either.
The eddy current sensor is fiddly to adjust. The guide doesn’t quite explain it well, you’ve got to put the paper between the heatsink and the sensor, on either side of the filament collar (if that’s the word). I found it easier to just check visually. There’s not much room for adjustment. I tried to push it down as much as possible, but it’s still a bit too far compared to the right nozzle.
This is the result:

Not perfect but good enough for me. You can’t see any imperfection on the bottom side, which was the issue for me.
BTW, all my PTFE tubing is stock, no sharp bends.
@homyak046 I suggest to try to adjust the eddy current sensor and see what happens.
In filament dryers humidities need the temperature they were measured at. Relative humidity is normalized to temperature and the numbers vary a lot with temperature. For example you can go from 10% humidity at high temperature to 100% humidity at low temperature - same air, same amount of water. What changes is the ability of the air to hold more water.
But it’s also precisely how you can measure the moisture content of filament - by measuring the humidity of surrounding air. You just have to be aware that temperature matters.
If you take a spool of filament (the more full the better) and put it in a ziplock bag or sealing polyethylene cereal box at room temperature and with a hygrometer, the water in the filament will equilibrate with the water in the air. After about an hour the reading will be stable and though it isn’t actually the water content of the filament, it’s physically tied to the water content of the filament and you can treat humidity like you would water content.
In short, you can find no-go humidities that if you measure a humidity higher than that, you can know beforehand if it will print well or not. For my setup, 20% RH with PETG is the limit. Above that I know I’ll see water issues. It’s 25% for PLA. What works for you depends on your particulars and what defects are acceptable. I do my humidity measurements at “room temperature” which varies a few degrees. For these purposes that’s negligible and room temperature differences are generally able to be disregarded.
But you absolutely can measure filament moisture indirectly. It works and it makes sense. It’s also how the silica gel industry measures water content in pre-conditioned beads they sell to museums and archival storage industries. You can buy silica gel with water contents that give humidities in 5% RH steps from inventory and 1% RH steps by special order.
I have exactly the same problem with the first layer. On the front of the bed, it looks like the nozzle is too close to the build plate, while the back seems to be fine.
You can even see on the prints that the nozzle is getting very close to the bed at the front.
I have had the printer for only one month, and this problem is still present.
Me too : (
I contacted customer support and they told me to do levelling calibration each time before any print.
And a print quality getting worse and worse with every print. : (
@homyak046 Another X2D owner with similar first-layer issues here. Mine is under two months old. After several days tuning dimensional accuracy, flow and top surfaces, I’ve spent the last two days troubleshooting the first layer. Small test patches could look excellent, but full-bed sheets still have localized gaps. A longer print also developed severe damage on its internal top surface; I don’t yet know whether the causes are related.
Already tried:
- Washed/reseated the plates; tested Bambu Textured PEI and BIQU CryoGrip Pro Frostbite; checked nozzle cleanliness and secure installation.
- Full automatic calibrations, including precision calibration with the Vision Encoder plate; first-layer flow and nozzle-gap adjustments.
- Manual bed tramming with Bambu’s G-code/paper procedure, as support requested.
- Replaced the left/main nozzle with a new one, repeated tramming, factory-reset the printer and completed startup calibration again.
Latest comparisons used stock Bambu Studio filament/process profiles with automatic bed leveling enabled:
- Left/main, new nozzle + black Bambu PLA Lite: localized open gaps.
- Right/auxiliary + white Bambu PLA Lite: severely uneven sheet, restricted to that nozzle’s reachable area.
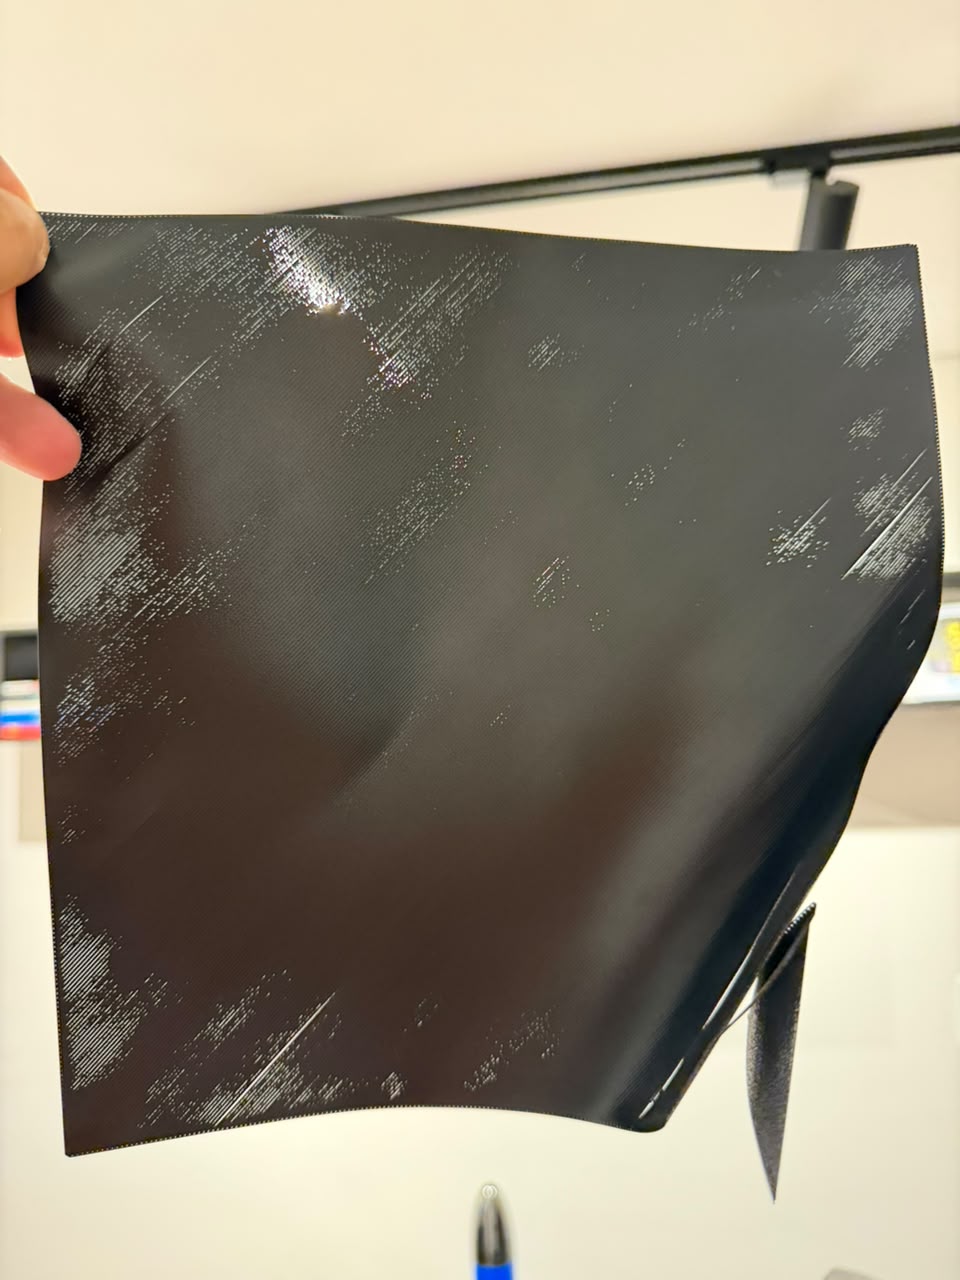
- Left/main + black Bambu PETG: widespread gaps, visible against the light.
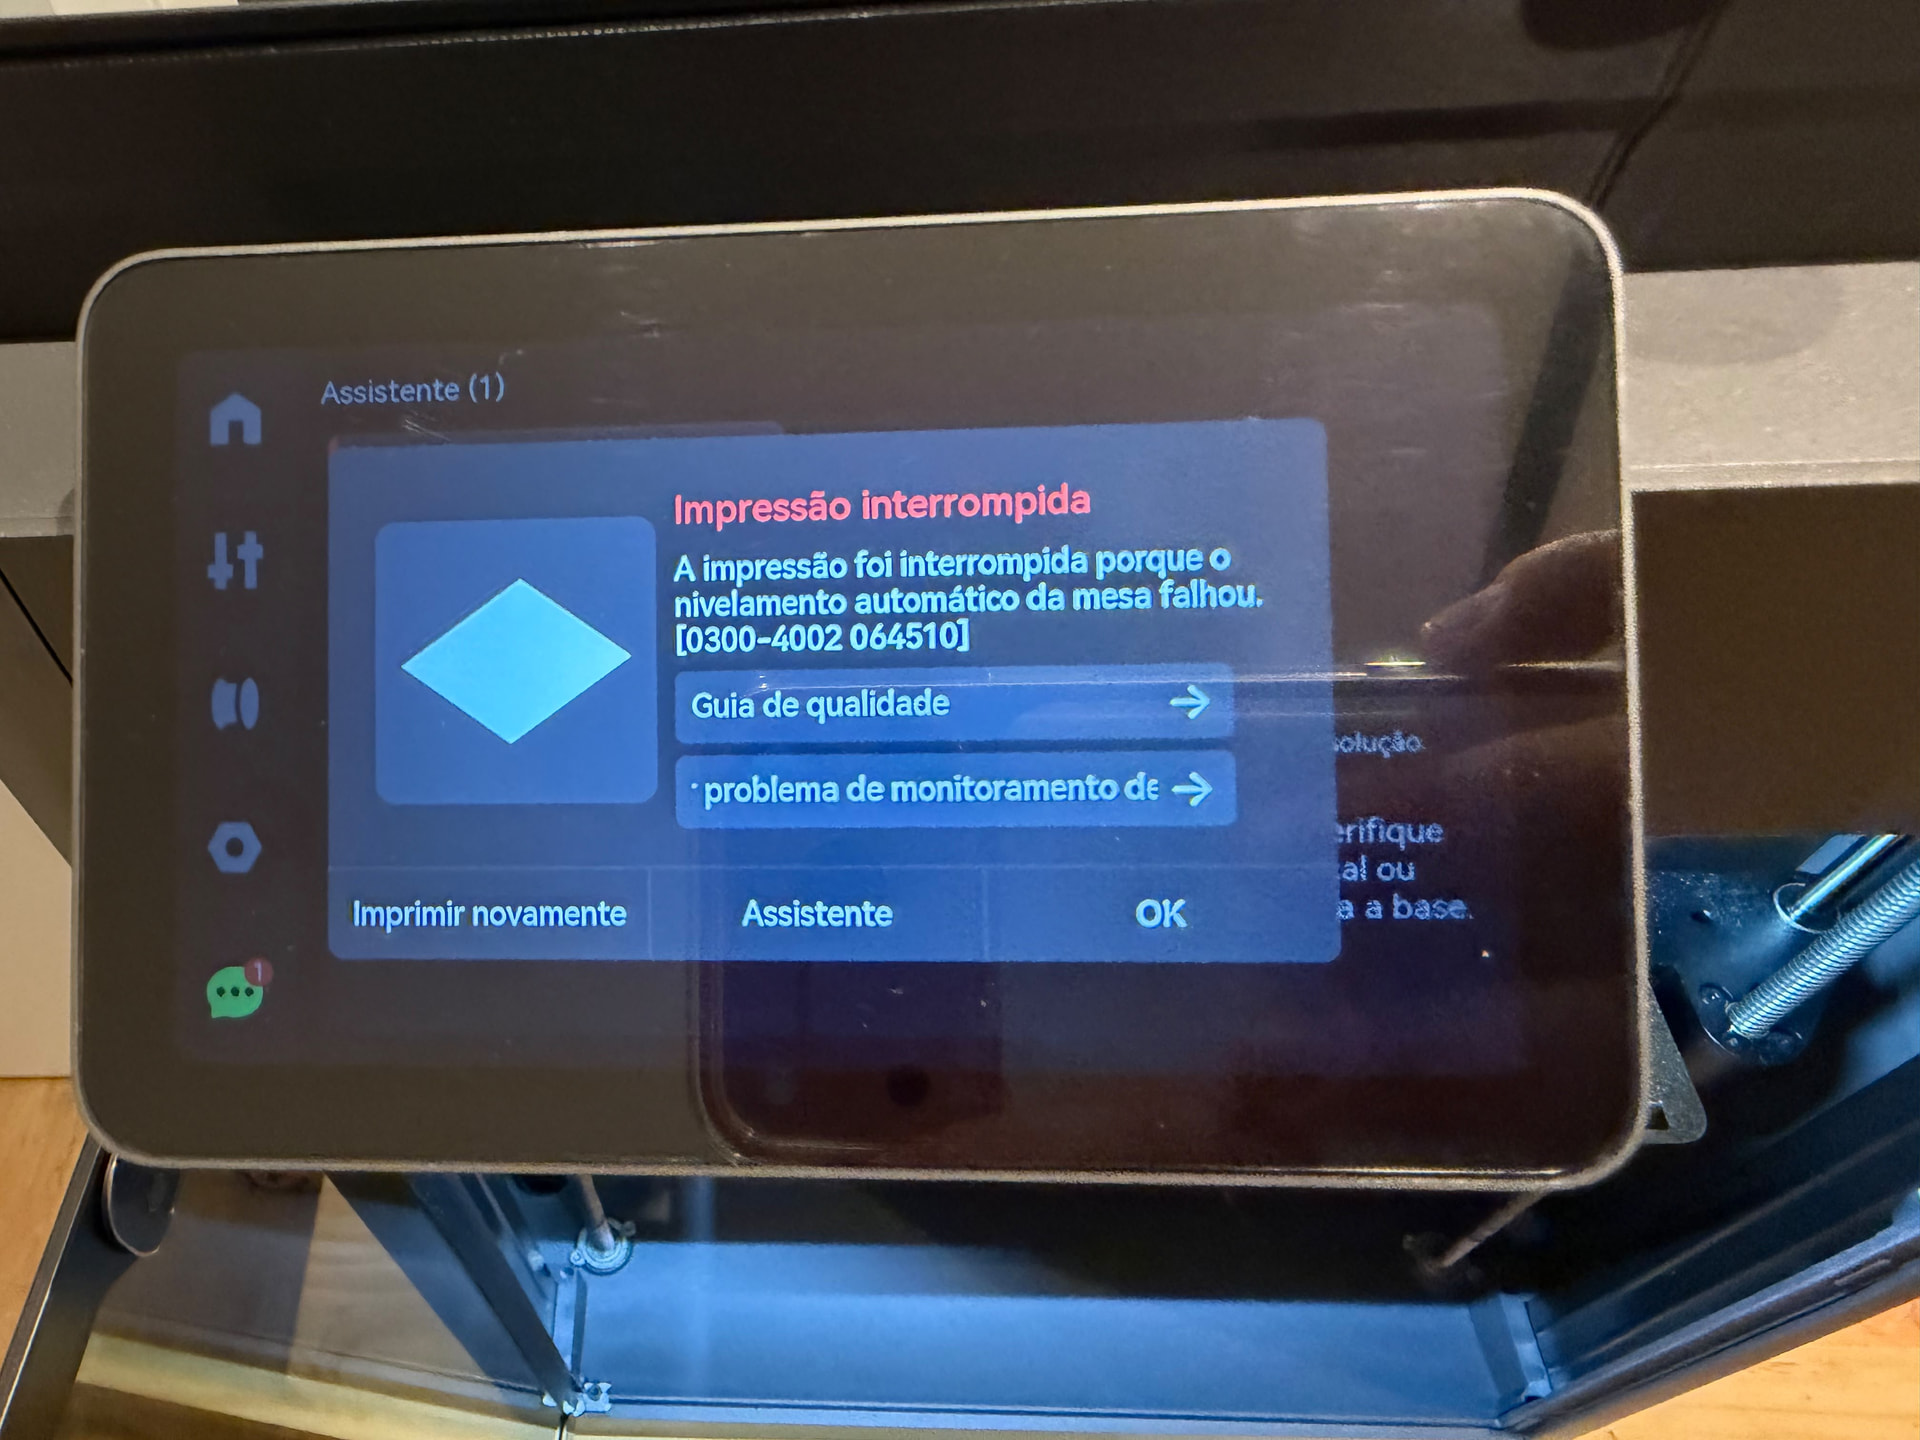
The first auxiliary-nozzle attempt stopped with 0300-4002 064510: automatic bed leveling failed. After the wiki checks, the second attempt repeatedly probed/revisited points for an unusually long time, then printed badly. This was separate from the timed thermal-preconditioning wait.
Support asked for manual tramming, another material (PETG), and comparisons with both nozzles. I’ve completed those tests and sent the photos/results; no diagnosis yet.
I’ve seen hundreds of users showing clean, fully joined first-layer sheets from an A1. Bambu’s own first-layer guide explains how to achieve a high-quality first layer, so I find these results on a new X2D hard to accept. I don’t want to settle for visible open gaps after all this calibration and troubleshooting.
@zmaster I also have plastic squeaking during Z movement. I traced mine to a small cover underneath the printer; tightening it helped but hasn’t eliminated it. Support initially described the noise as normal and suggested lubrication. I don’t know whether it’s connected to the leveling issue. I saw that drying, retightening the heating assembly and adjusting the eddy sensor improved yours: has that improvement held up through subsequent automatic leveling cycles?
1. Left/main, new nozzle — Bambu PLA Lite, black. Sheet on the plate.
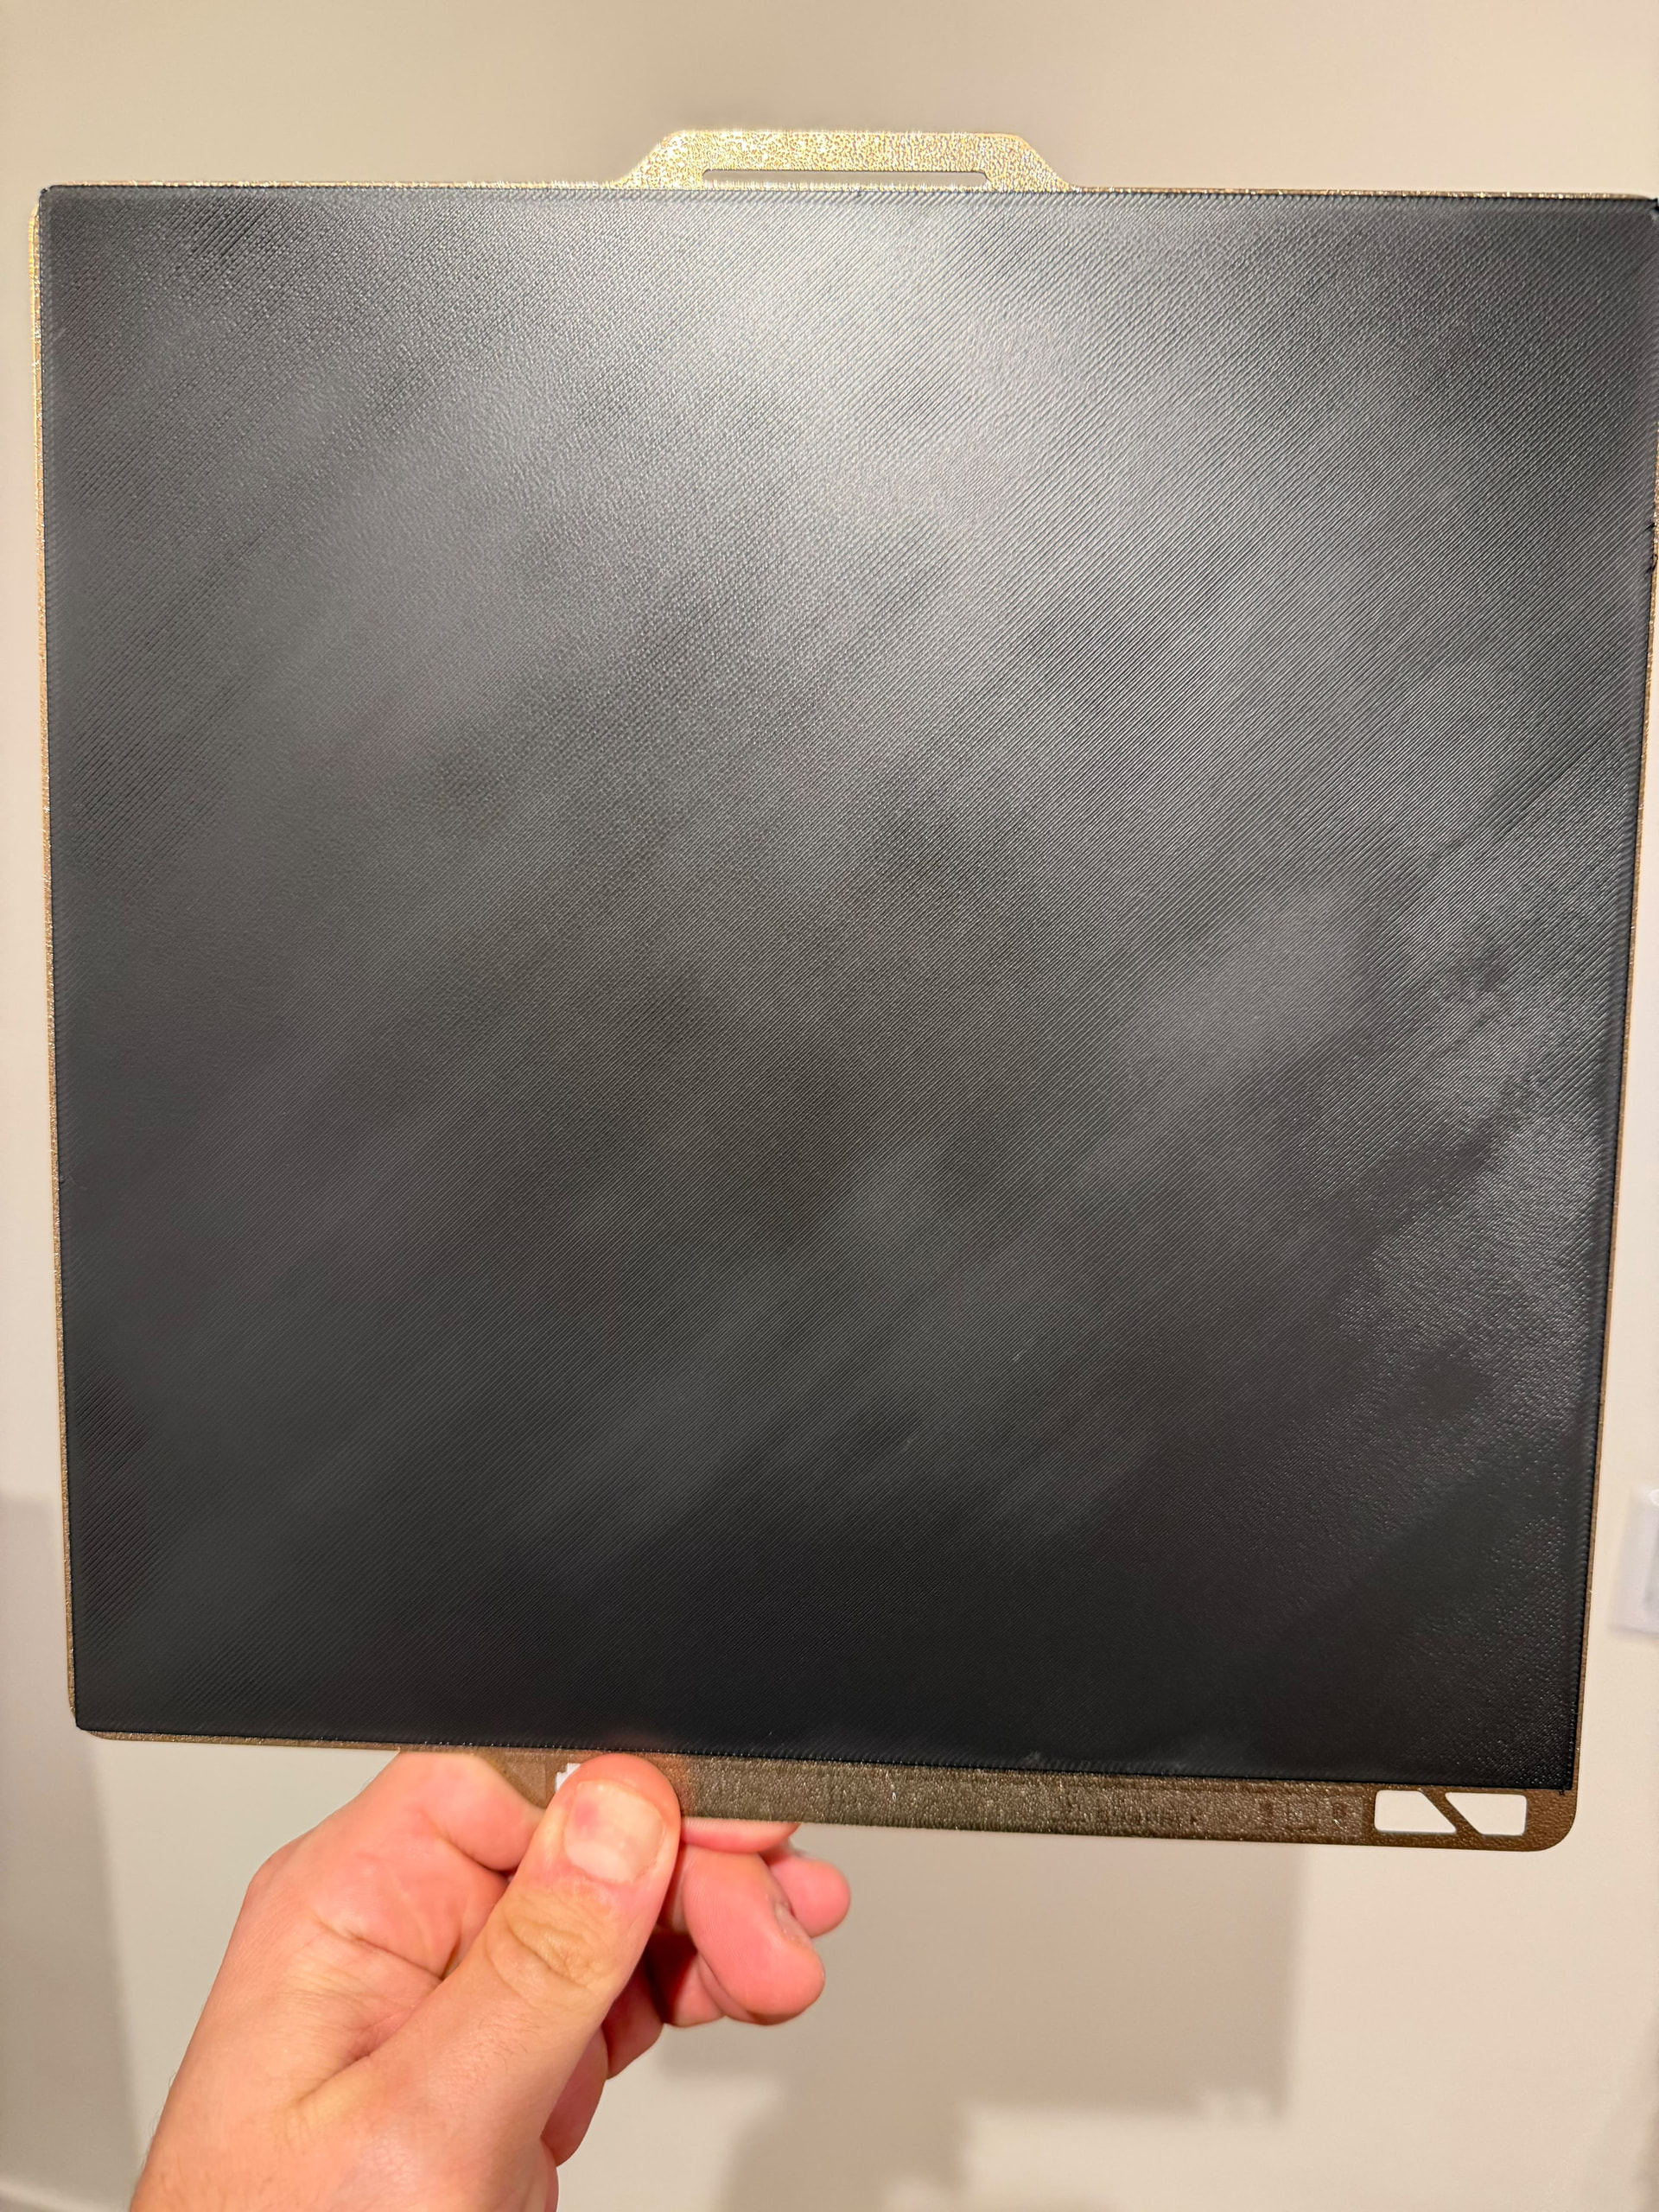
2. Left/main, new nozzle — Bambu PLA Lite, black. Removed sheet held against the light, showing the localized gaps.
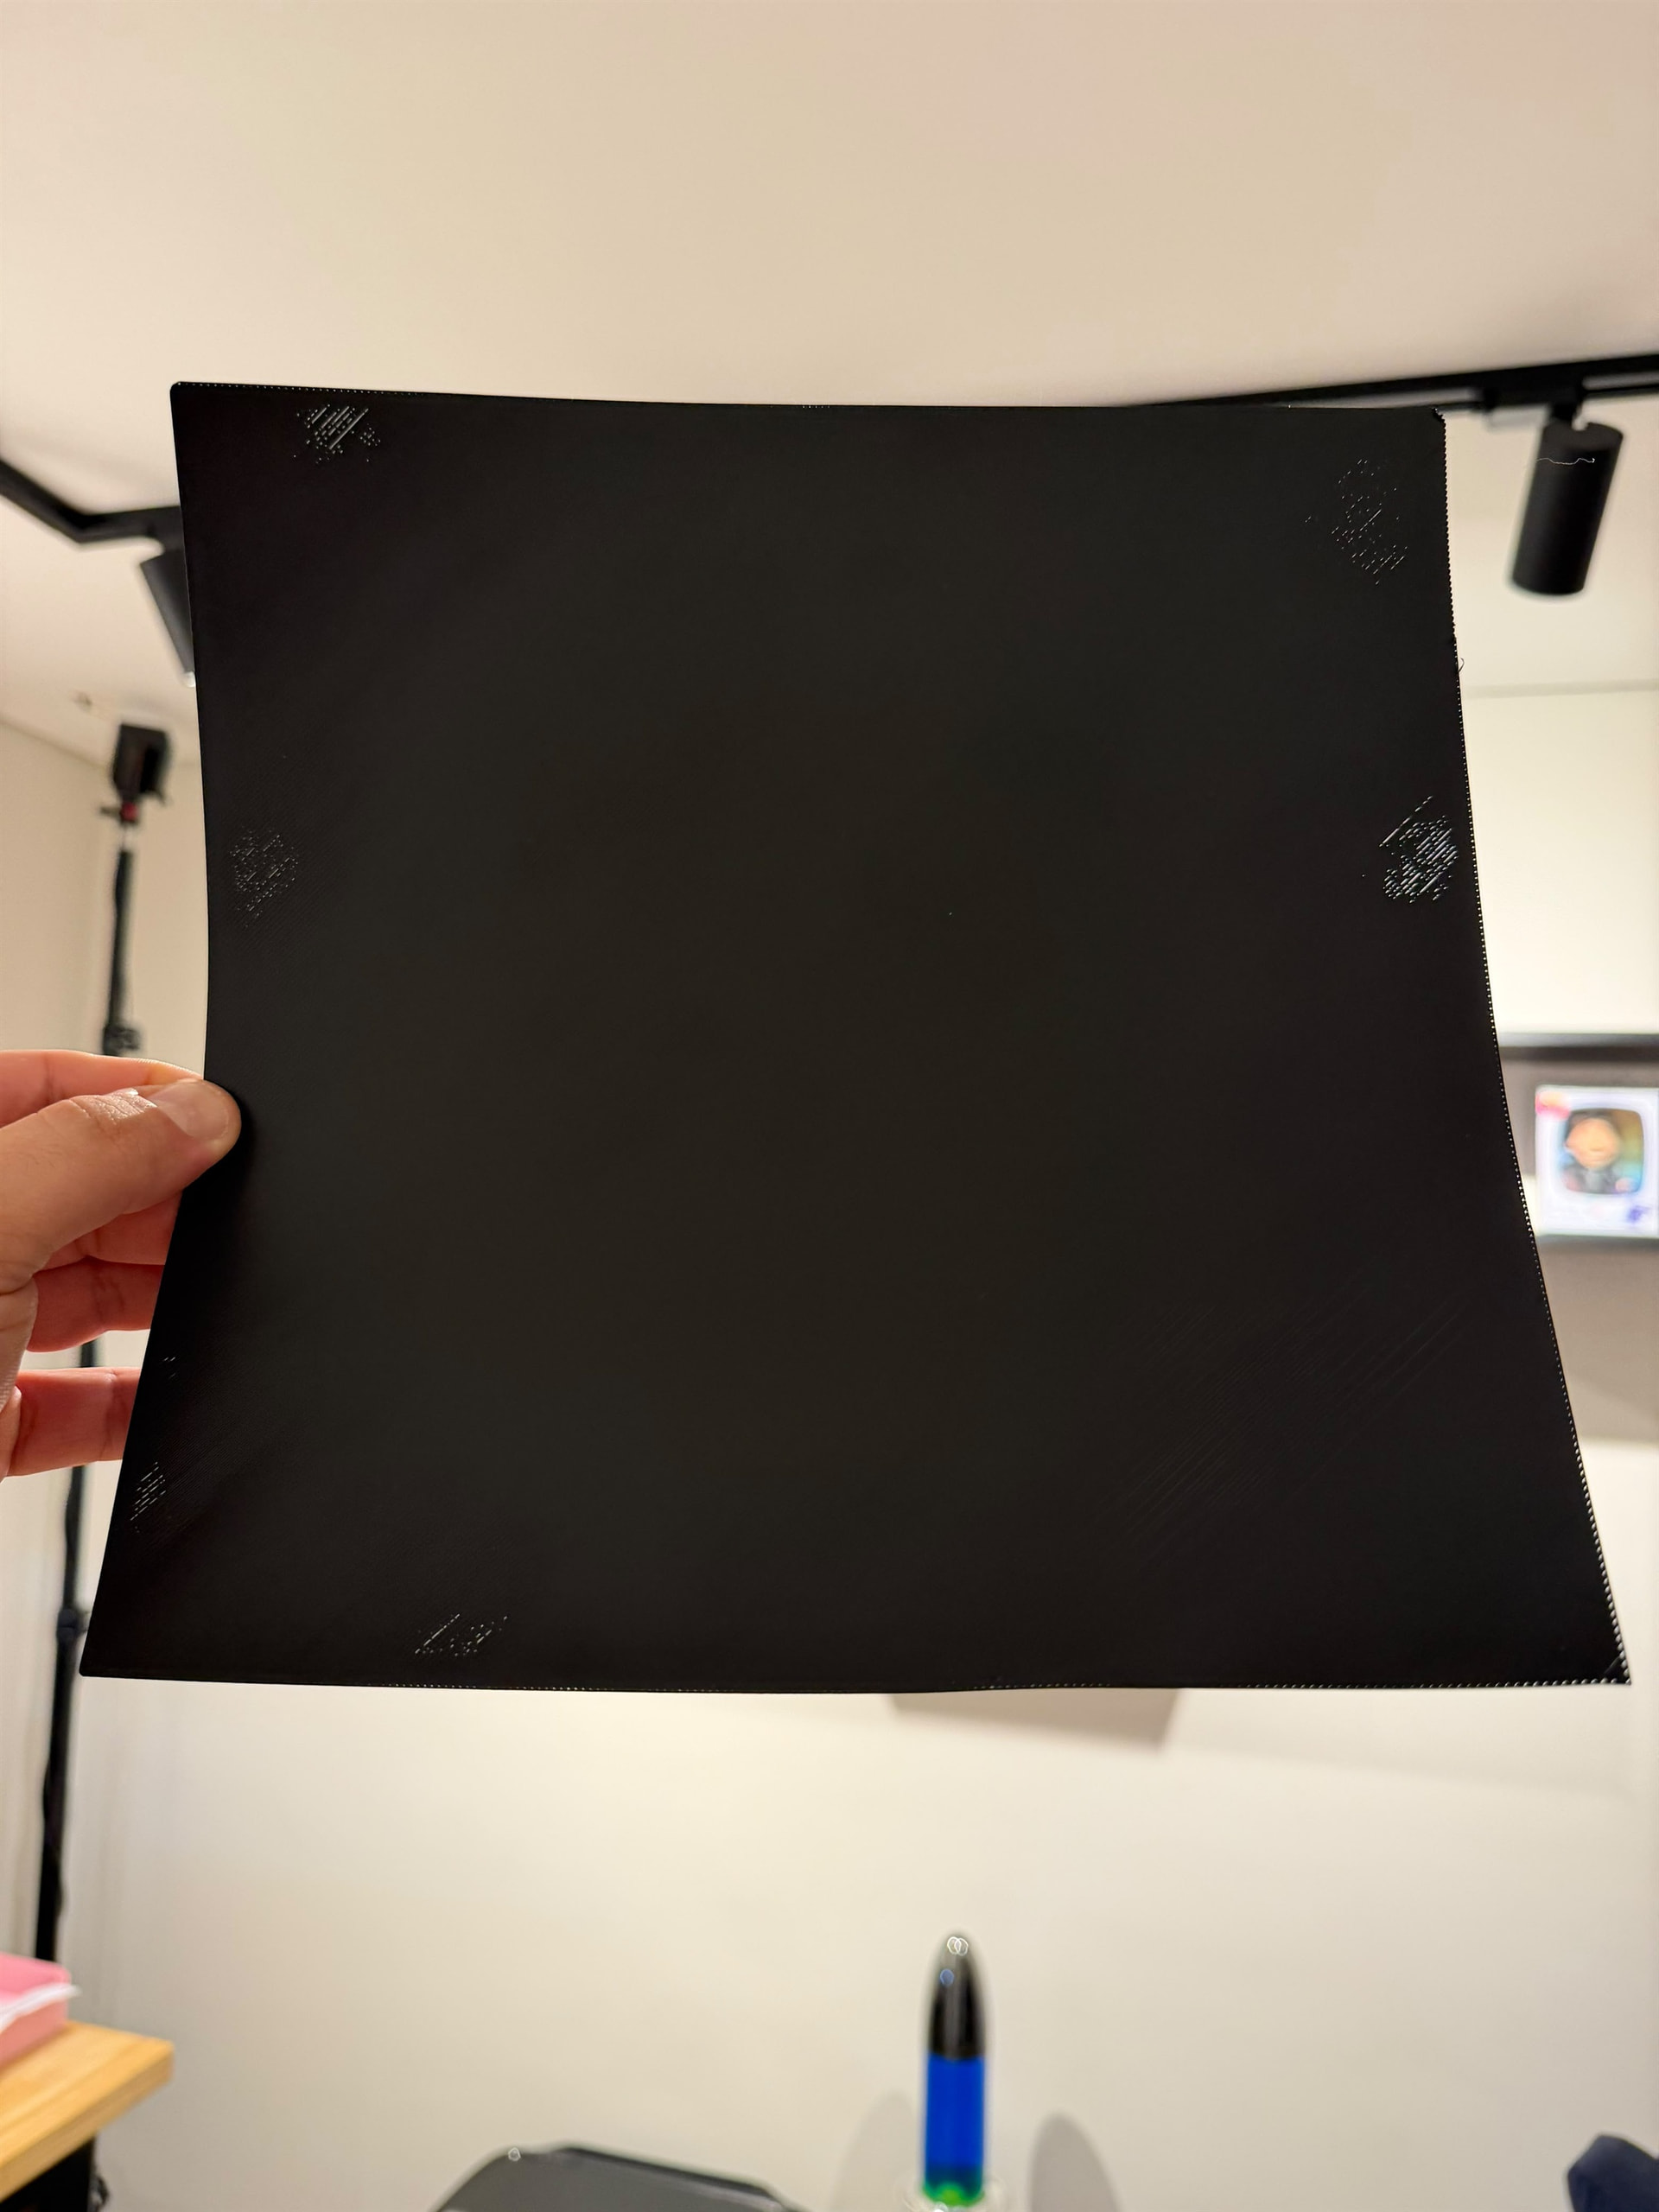
3. Right/auxiliary — Bambu PLA Lite, white. Sheet on the plate.
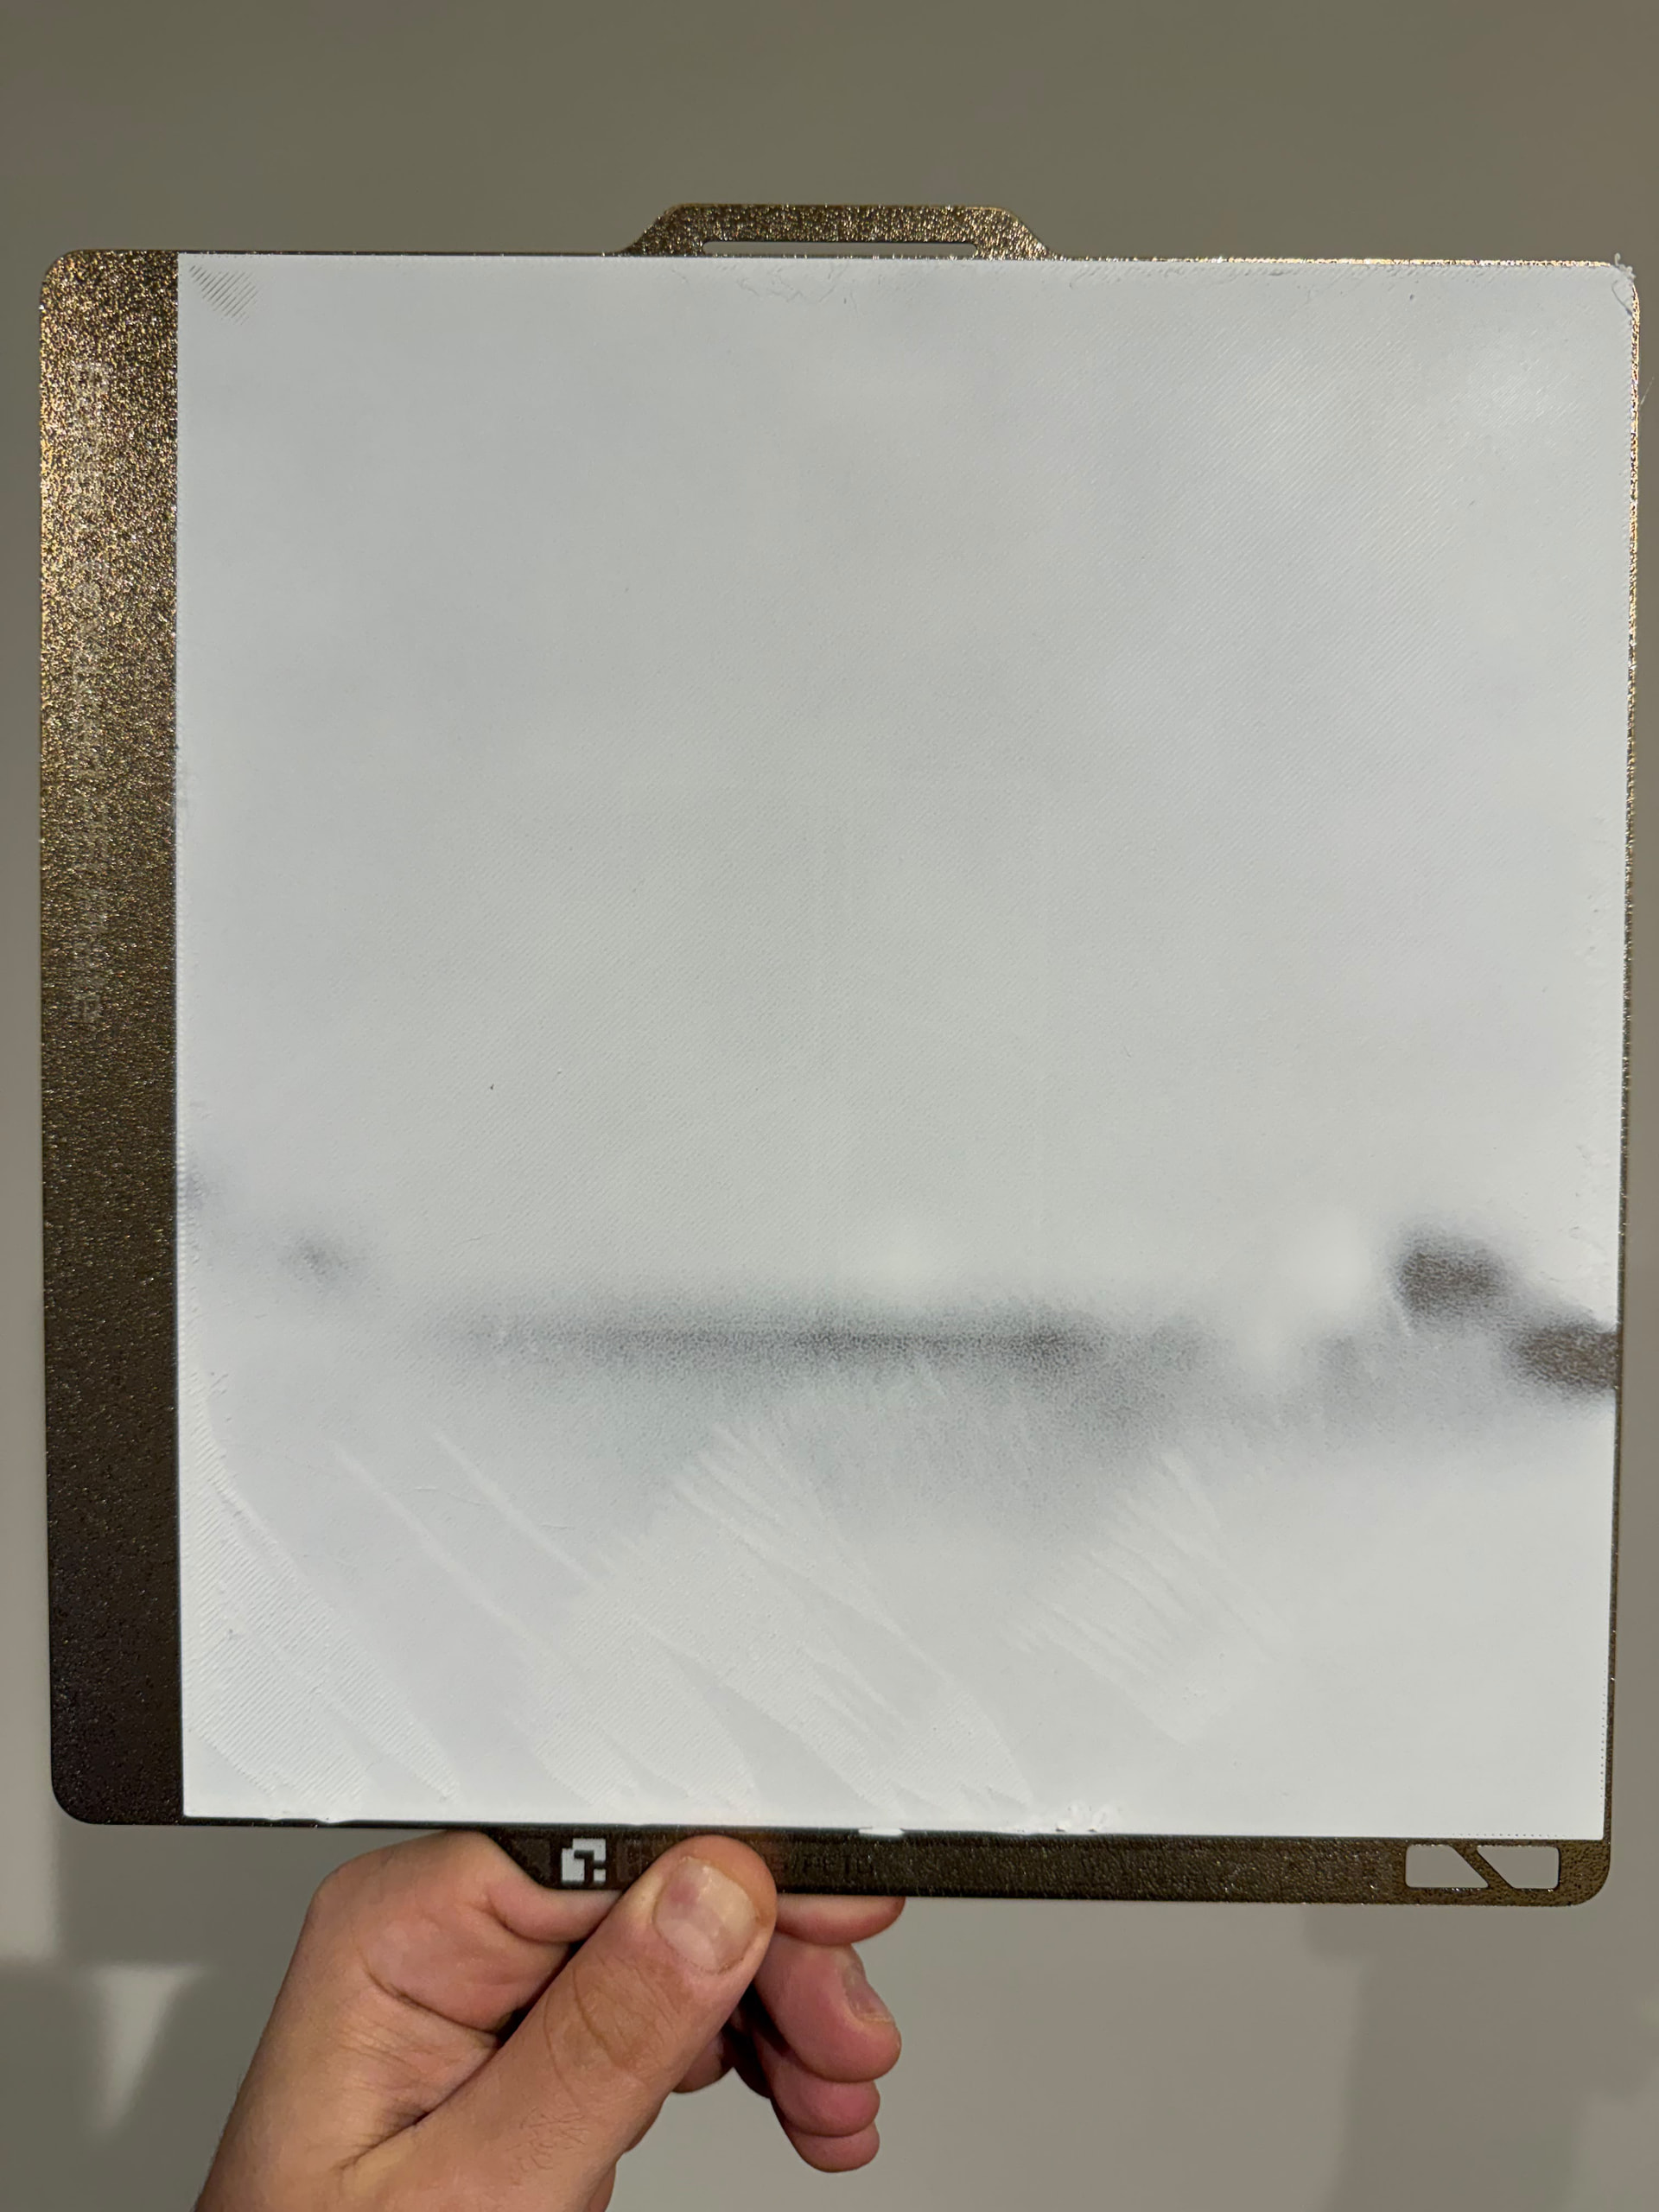
4. Left/main, new nozzle — Bambu PETG, black. Sheet held against the light.
5. Error from the first right/auxiliary PLA Lite attempt.
Colleagues! Here is how I solved the problem:
- First, I performed a manual calibration by adjusting the three screws and placing a sheet of paper under the three corners. Before doing this, I unscrewed the three screws completely, as they were very stiff to turn (X2D First-Layer Printing Optimization Guide | Bambu Lab Wiki).
- After completing step 1, I went into the printer menu and selected bed calibration.
- Since then, I no longer run the automatic bed calibration before printing.
P.S. I still think this is a firmware issue. If I enable automatic calibration before printing, the settings made during manual calibration get wiped out. And it has nothing to do with the filament or its condition.
Thanks for sharing! Glad you found something that worked.
Just to make sure I understood: which screws did you loosen — the three bed-leveling screws (015.jpg), the side mounting screws (014.jpg), or the three screws on the nozzle assembly (012.png)? And by ‘unscrewed completely,’ do you mean you removed them or just loosened them?
After the paper adjustment, did you run only Auto Bed Leveling in the printer menu, or also High-temperature Bed Leveling, and then leave bed leveling unchecked before subsequent prints?
And how does the first layer look now — fully joined across the plate, without gaps, or are there still a few small imperfections? We’re trying to understand whether we’re seeing the same issue. Thanks for your help!
Reference images from the Bambu wiki:
015.jpg — Three bed-leveling screws
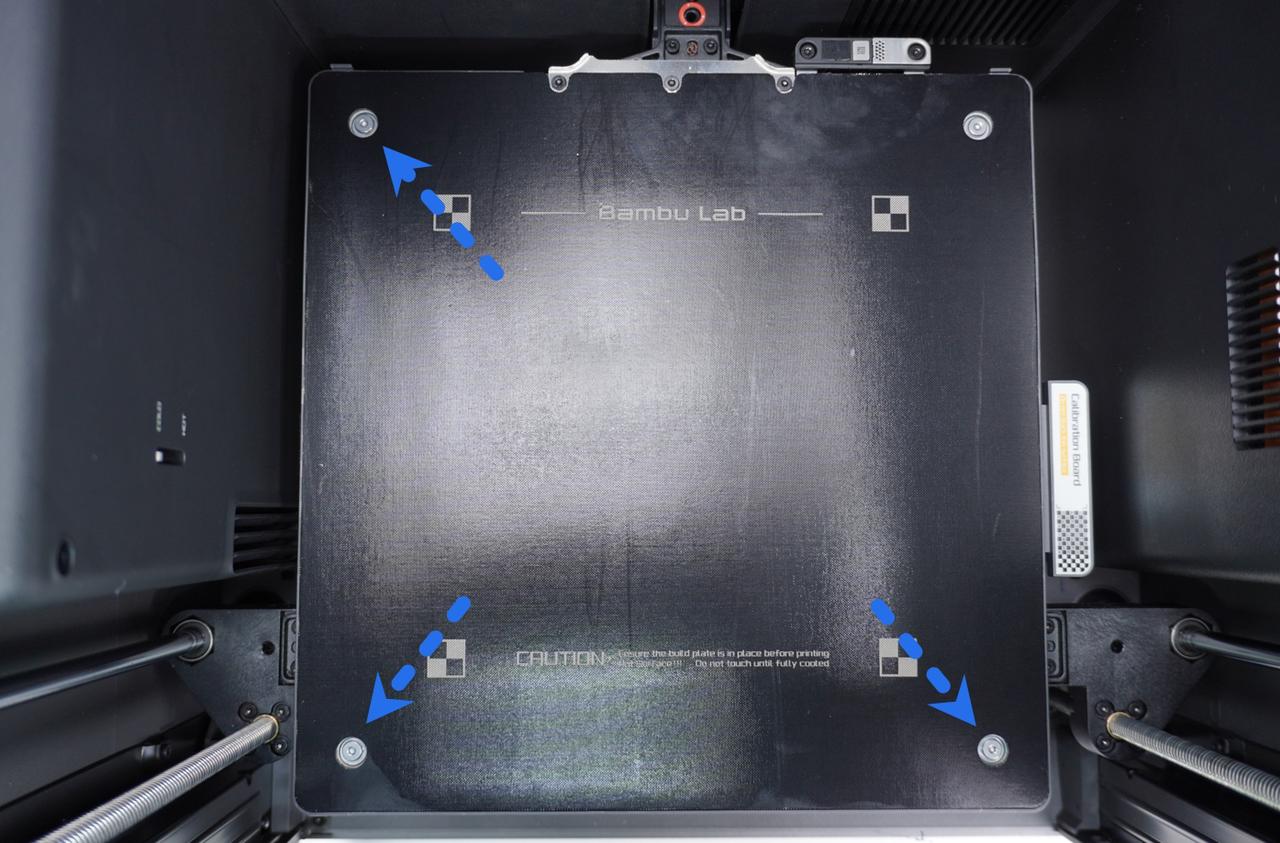
014.jpg — Side mounting screws
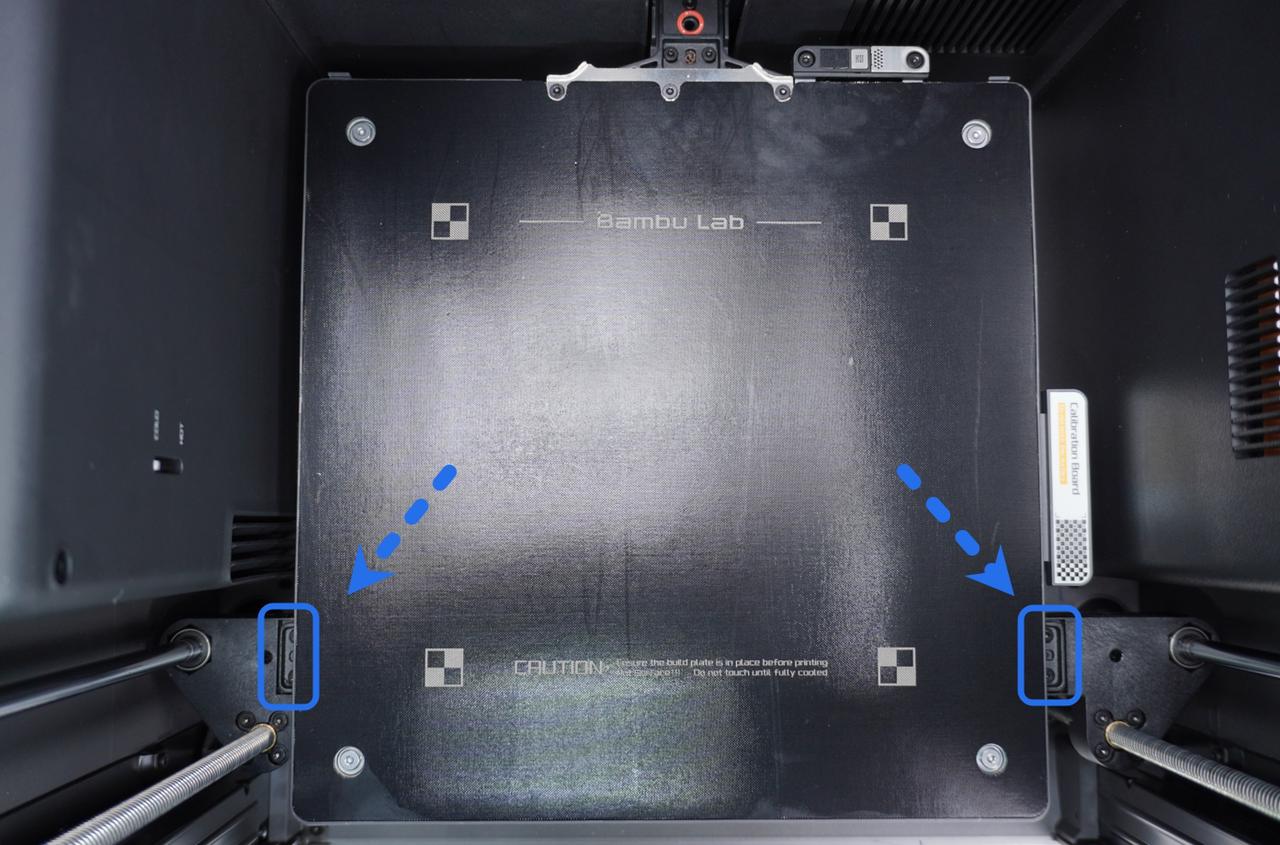
012.png — Three screws on the nozzle assembly
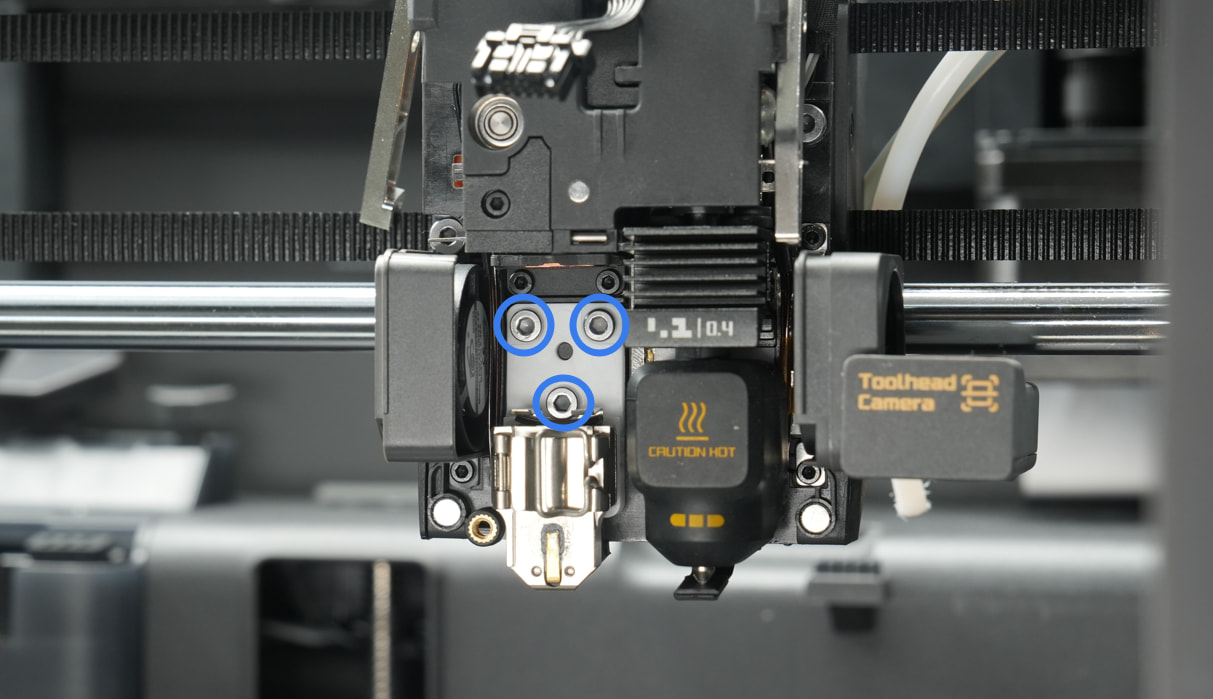
@Foca I have only printed small parts after my fix. I will try to print another sheet this weekend.
Another quick feedback:
I tried to do the same strategy from @homyak046 . I literally removed all the screws, from the noozle, from the bed, did the calibration.
Then i tried to print it everything as default and later loading the filament calibration that i did before.
No automatic bed calibration for both: