Hi all,
After lots of hours with PLA, PETG, ABS & Co. I started playing around with TPU 95 HF. I used it for small use cases like small key chains, etc. I use the external spool holder on the left to feed the primary nozzle (0.4 hardened Steel). The roll has two cycles of drying at 65 degrees Celsius for each 12h in the AMS 2 Pro behind.
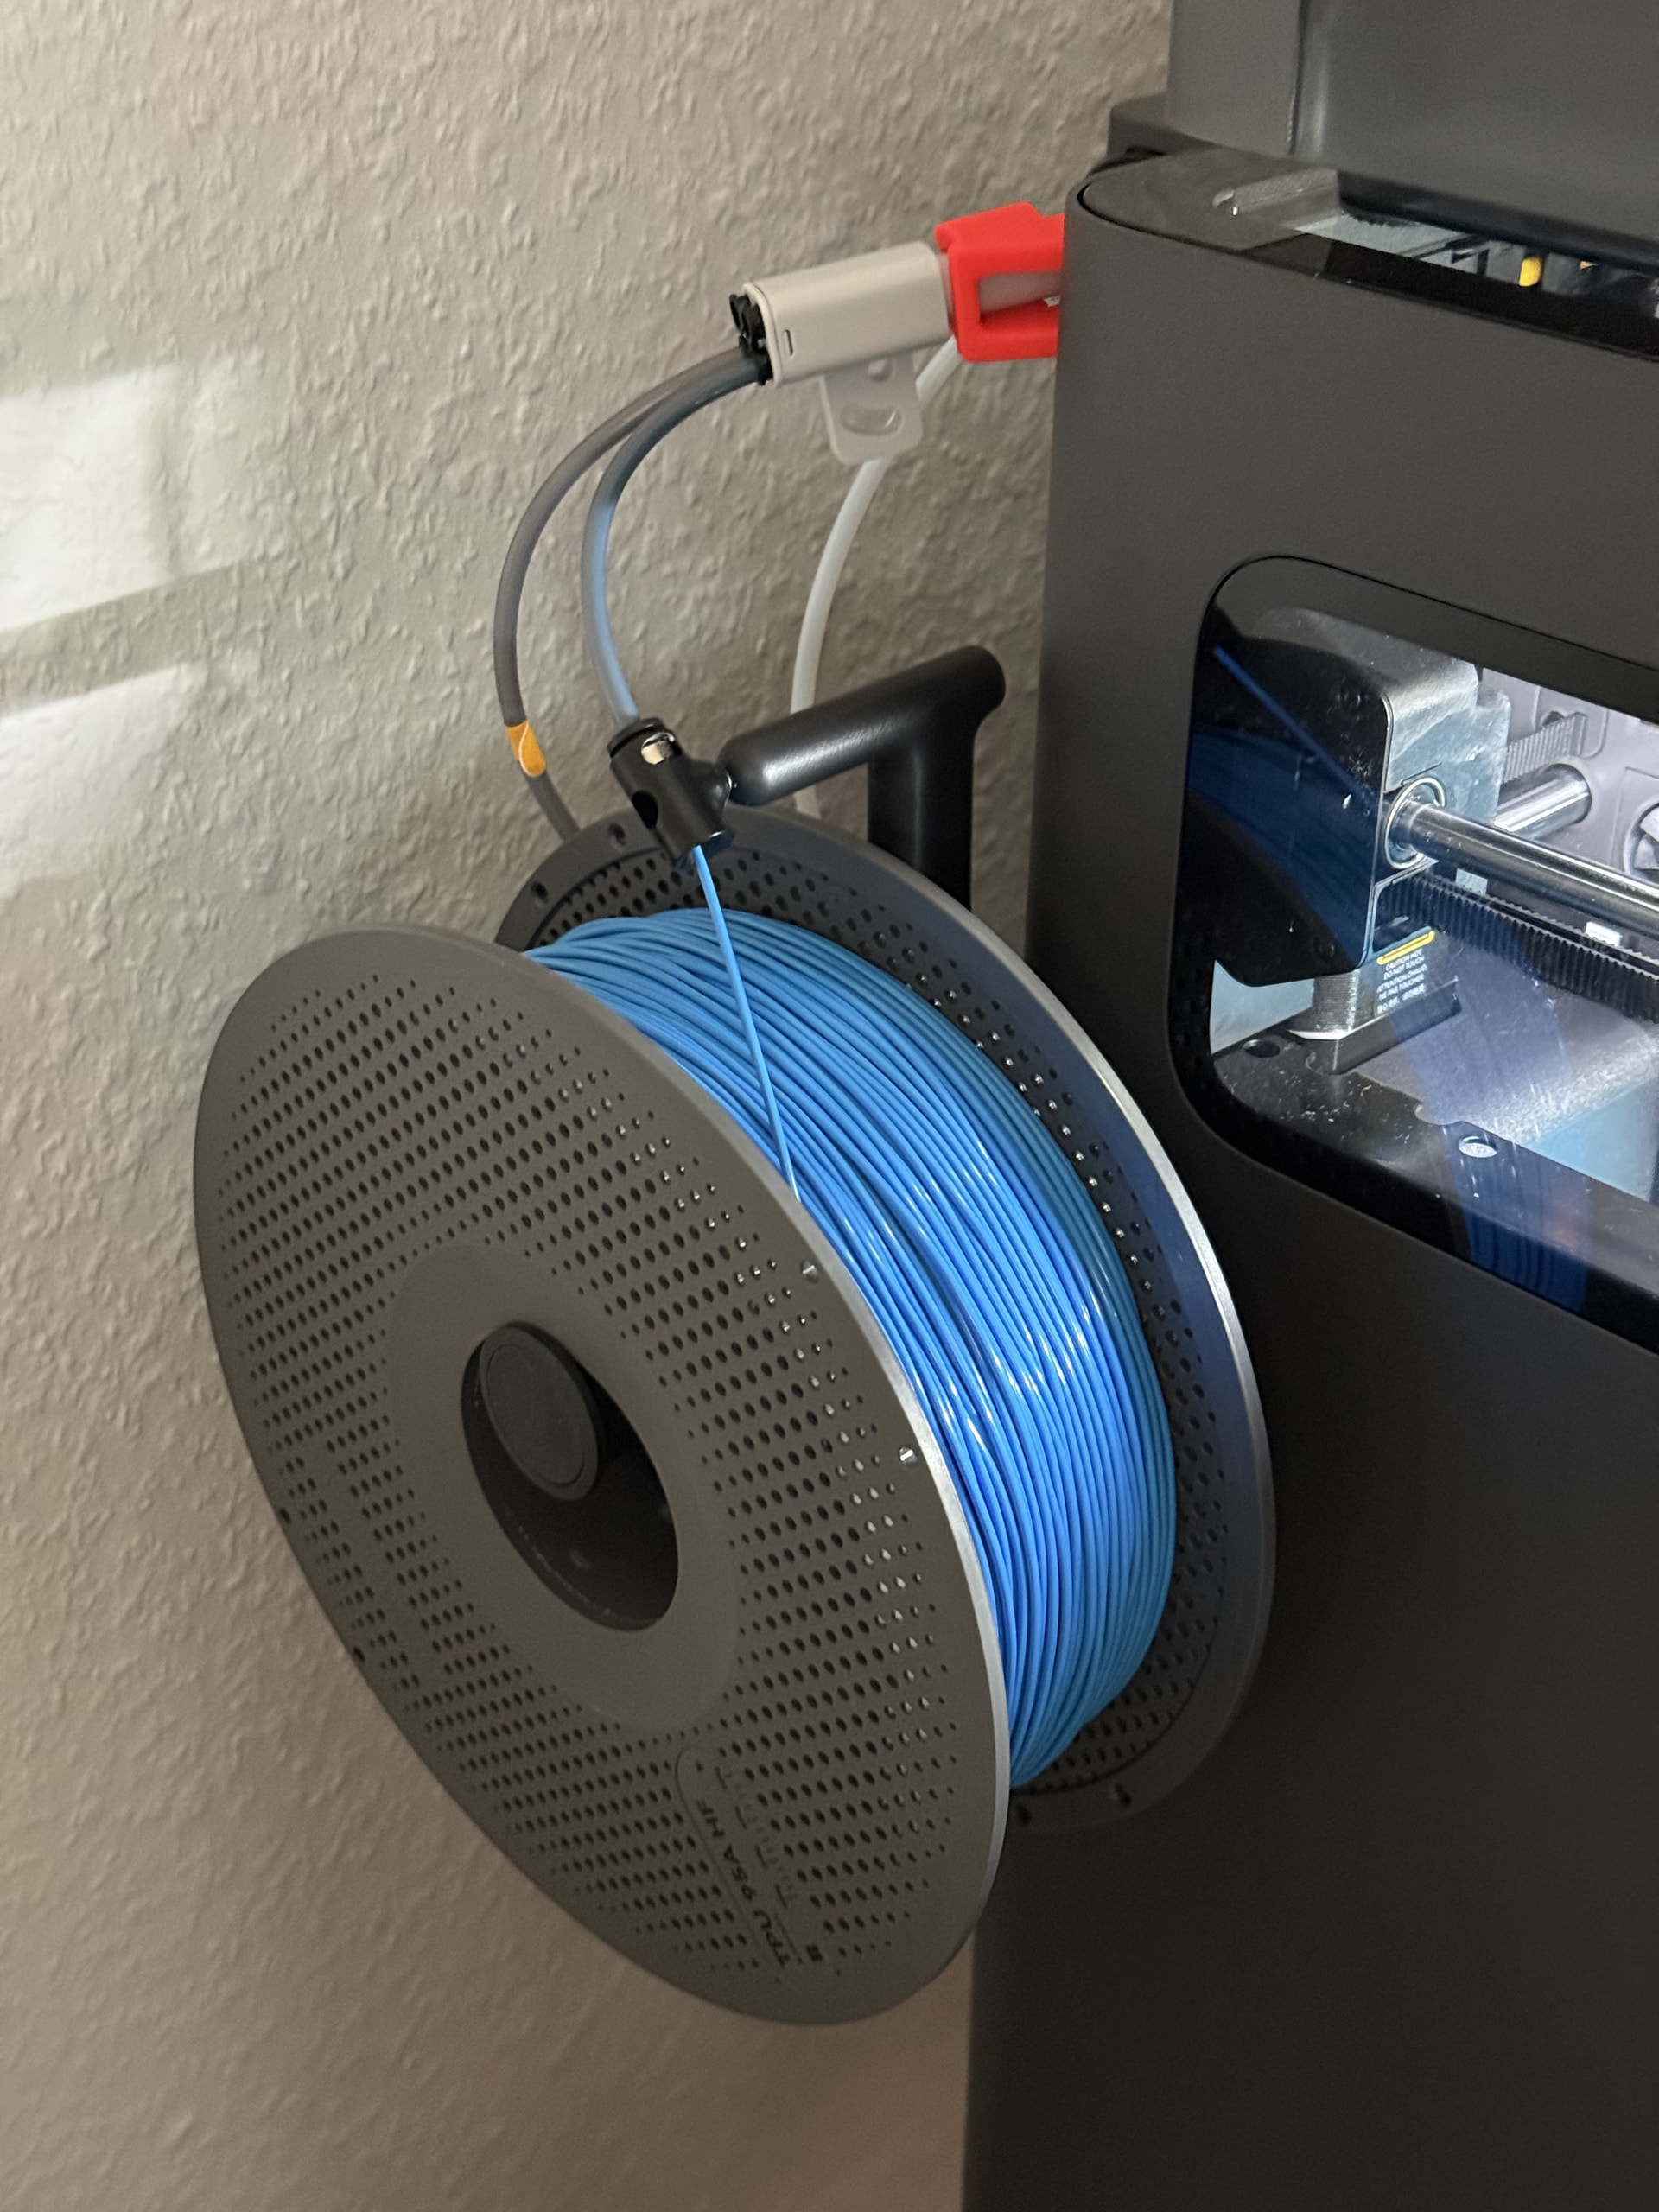
I found early though that there’s significant under extrusion going on. I’m aware that the X2D tends to struggle with slight under extrusion. Hence I looked into the manual flow calibration. The result to me looked off though. A closed surface was only achieved at +20 where details and corners seem to suffer in quality significantly though accompanied with stringing. To me it seems like I’m fighting a symptom but not a root cause.
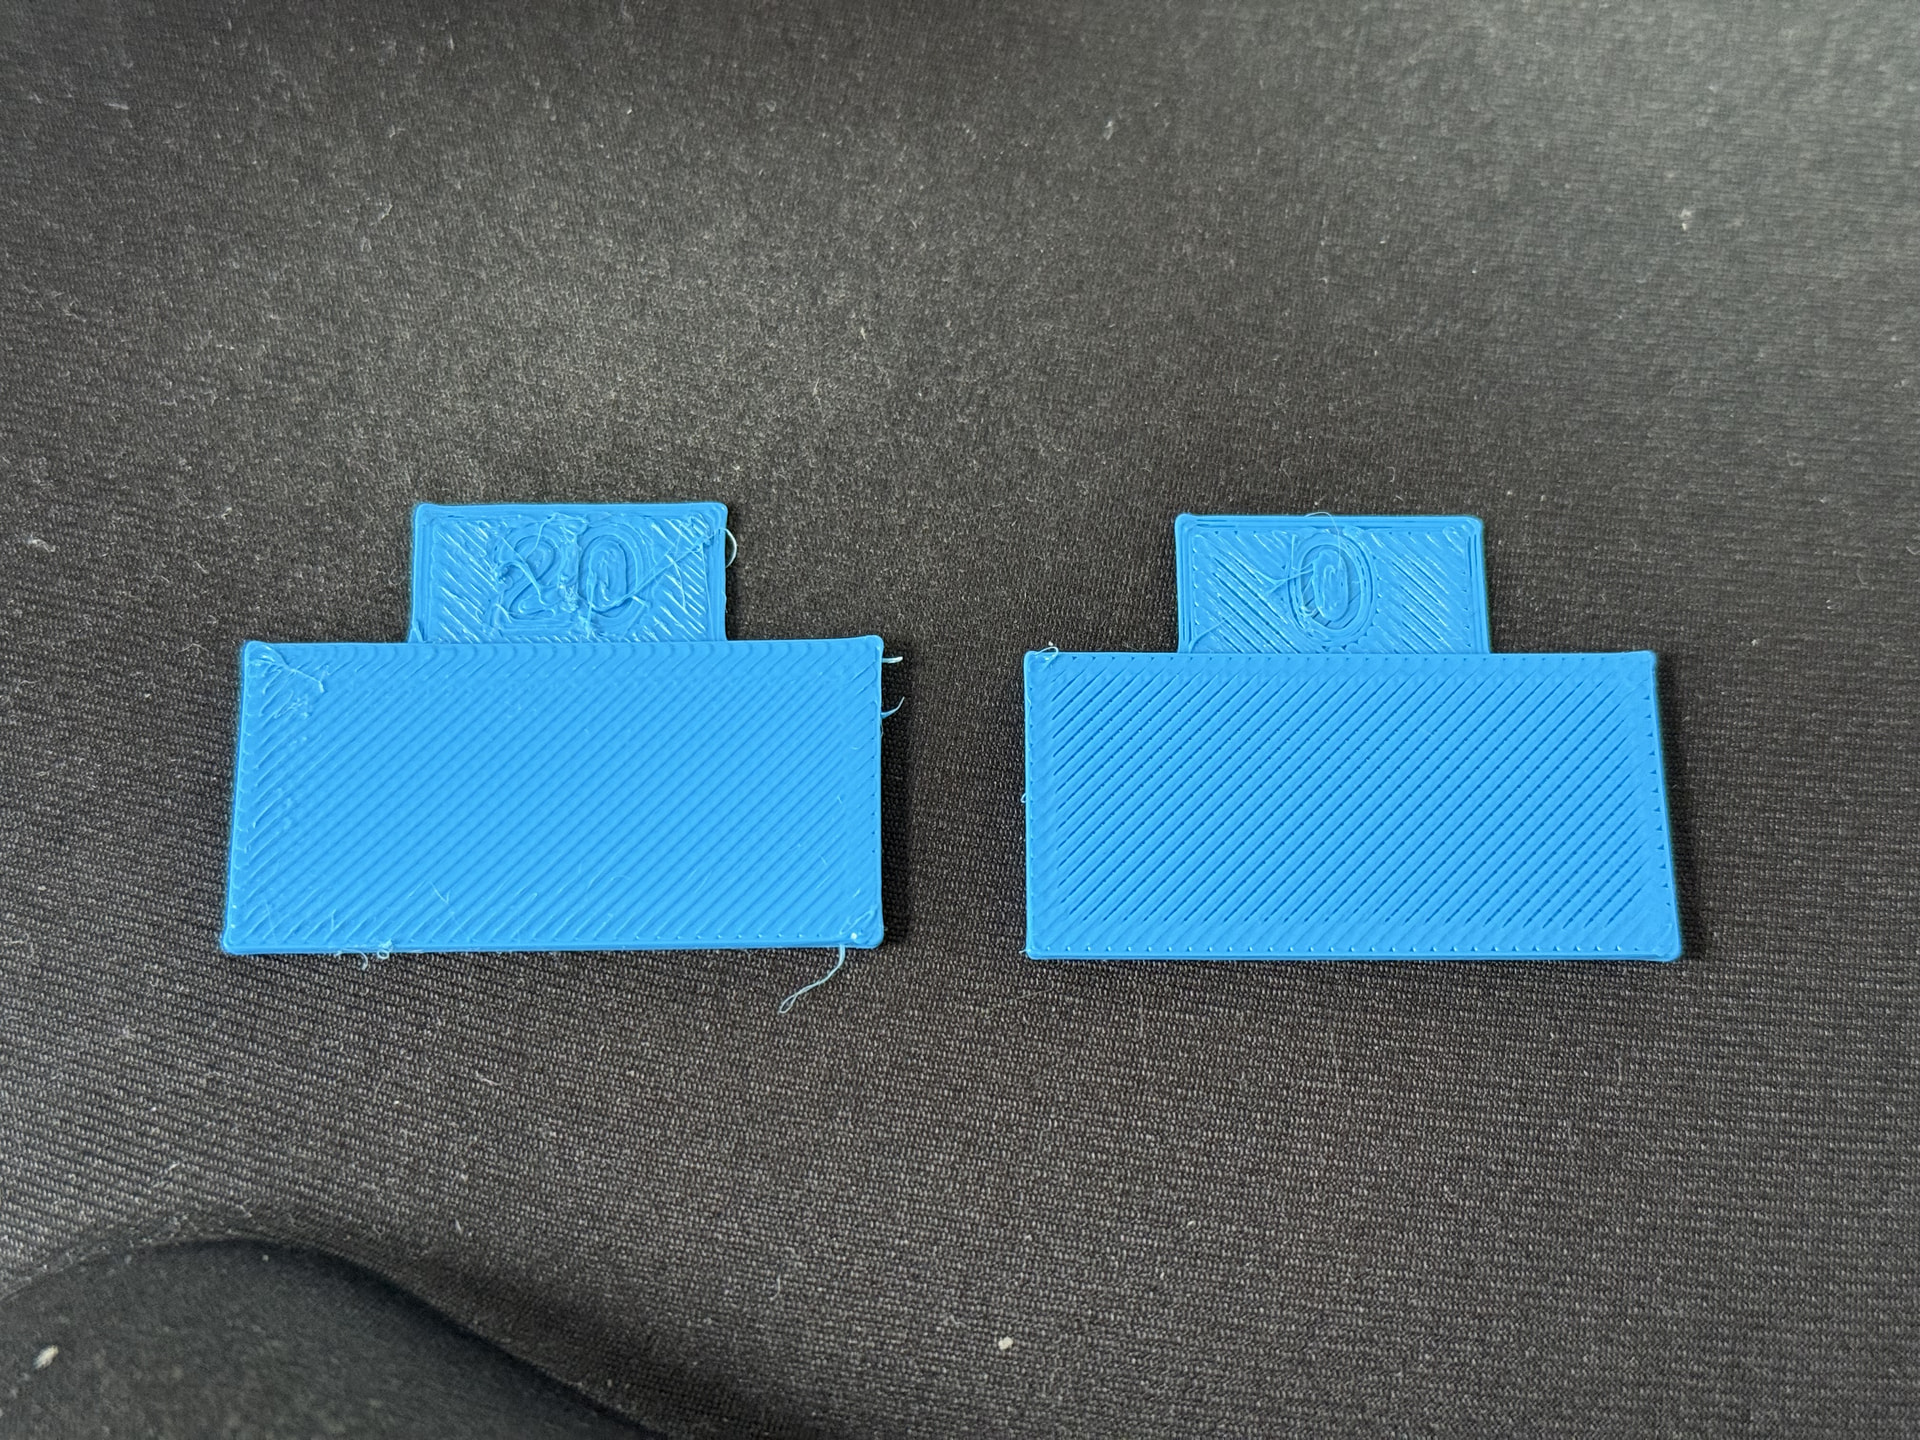
I tried various different parameters like reducing the volumetric flow by half, increasing nozzle temperature by 10 degrees but it doesn’t seem to help. Dynamic Flow Calibration was disabled at the prints as recommended in the wiki.
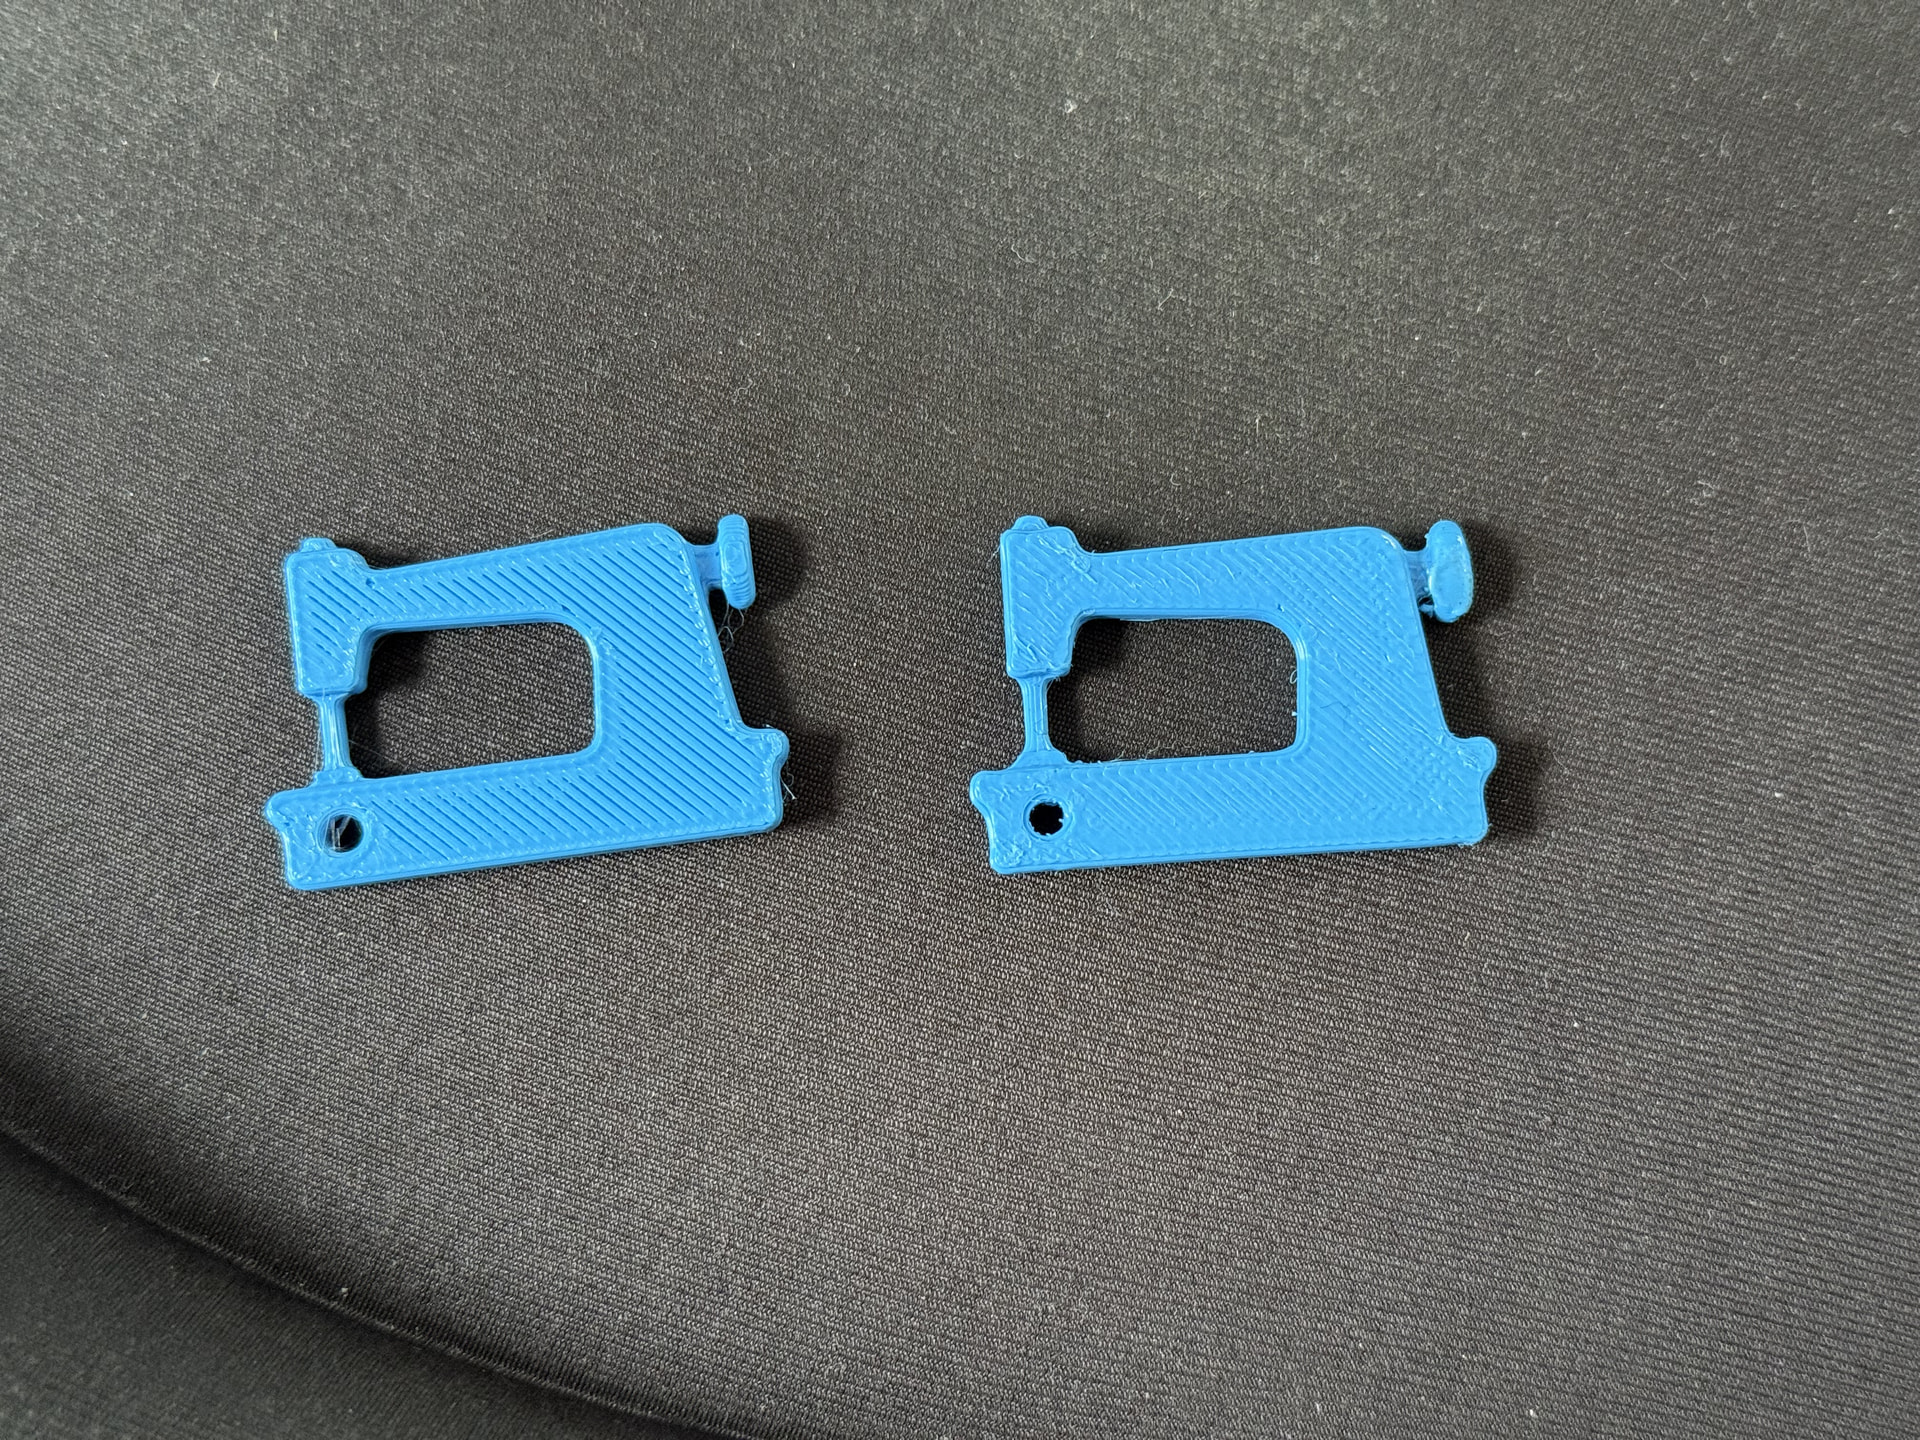
Does anyone have any ideas what I can look into?
Thanks a lot in advance!
Kevin
 &
