Strong Cooling control

I am really struggling with x2d and fan cooling. I am trying to dial in PCTG filament workflows using PLA as a support interface. I have print profiles and material profiles set up specifically for this. Fan speeds are set per vender recommended setting.

Does x2D work well with this scenerio? No? Why? Because the BL PLA seems to trigger a “Strong Cooling” overide for the whole print whenever BL PLA is present in a print. The result warping and terrible layer adhesion throughout the PCTG print. Turn off PLA as interface support and prints look great. But then I did not need a dual nozzle for this.

The single reason I purchased a dual nozzle machine, was to speed up using separate interface material for prints. That is also the marketing positioning of x2D by BL…

BL labs need to add a user setting to control super cooling mode on x2D. Since their product is basically failing at a very basic use case its purportedly designed to solve.

I have tried using the recommended gcode hacks in other threads to trick x2D super cool mode. hacks like this should not be required. And I am not utterly confused as to what is controlling what from where? is this in my machine settings? printer profile setttings? does it work when I change nozzle sizes? And I still seem to see fans speeds having a life of their own.

Super cool should be a user controlled option. Hardware overriding software/printer/fillament settings is not a good thing. Especially with no notification or user control

I recall seeing a YouTube video about this exact problem but I cannot find the video now to link to it. From what I recall, he fixed it by changing the temp on the PLA filament from 45 degrees to 65 degrees (to match the PETG temp). This stopped the cooling fans from coming on. He saved it as new profile (PLA support for PETG) so he could use it when he was using PLA as support.

And when you do this, you are likely going to get clogs because PLA will swell inside the aux hotend. The default response from many will be: “bambu doesnt recommend this, use specific support filament, user error“

I had the PLA swelling issue on my first ever printer, a DIY, on freaking repetier FW, 10 years ago. Its f^%7ing hilarious/ sad to see the same problem on such a “high end machine“. Really? Cant properly cool the one place that needs it? What are these some cheap crap fans? Oh… apprently they are, judging by how many failed already when printing at high temps for longer.

Yeah they have really made it for “special” support materials. All else is on your own risk … and they automated everything for your own safety and easy life! But could not able to figure that the plastic on the side panel will deform from the heat, the side fans will blow things wile printing, and PTFE paths are somehow “not very optimal” :smiley:

And yeah I never thought that I will see cheap sleeve bearing fans in not so cheap products and in places where you need to dig really deep to reach it….. but ….

Obligatory cross-link to the “main” thread for this issue: X2D Manual Aux fan control in cooling mode and disable autocooling for PETG+PLA

Anybody have luck getting consistent results printing PCTG with PLA support interface on x2d?

All I get is warping and failures… over and over. I have been trying to adjust temps, and fan speeds etc… x2d damn strong cool mode is the VERY likely culprit.

I am using 3d Fuel Pro PCTG. I am also using 3d Fuel supplied print profiles and settings, And I printed and added the fan diverters to help with over cooling.

I have been going back and forth with 3d fuel. They too have replicated the warping on x2d… But so far, no solution. Since this seems to be a x2d specific problem.

PCTG is a great material. It does not require a heated chamber. VOCs are not strong. You would think the x2d is the perfect match.

I have found ASA in combination with abs support filament is much more reliable. But that is not a solution for me. I do not want the VOCs from ASA or ABS.

Bambu please fix your strong cooling behavior. Give us a user setting to disable. x2d dual nozzle is supposed to be made for support material on aux nozzle. PLA is a support material for some filaments. So stop f*(& it up. :slight_smile:

Joe

PS

I have even tried using the gcode recommendations listed on this forum to override the override. But TBH, it’s confusing and I am not sure what is controlling what anymore. Do I have to stand in front of the printer for each wait for the first layer to finish then turn off the fans? All I know is fan speeds seem to do whatever they feel like even with the gcode changes

I am really struggling trying to get a handle on printing with x2d. Seems to work fine with BL materials like PLA or ASA and the BL supplied profiles… But I am getting utter failure when trying to use some other materials

Specifically I am trying to print PCTG, using a .6 nozzle.

It seems the temperature control on x2D just has a life of its own. I have tried to create my own material by customizing either the generic PCTG material profile or the PETG profile.

First concern is that even after changing the settings and saving as a new name… When printing using these new profiles, the device shows that it either goes into Heat mode for the old PCTG or Strong cooling for the old PETG. So I guess Bambu is still has some setting that makes it think the profile I created is still the old one…

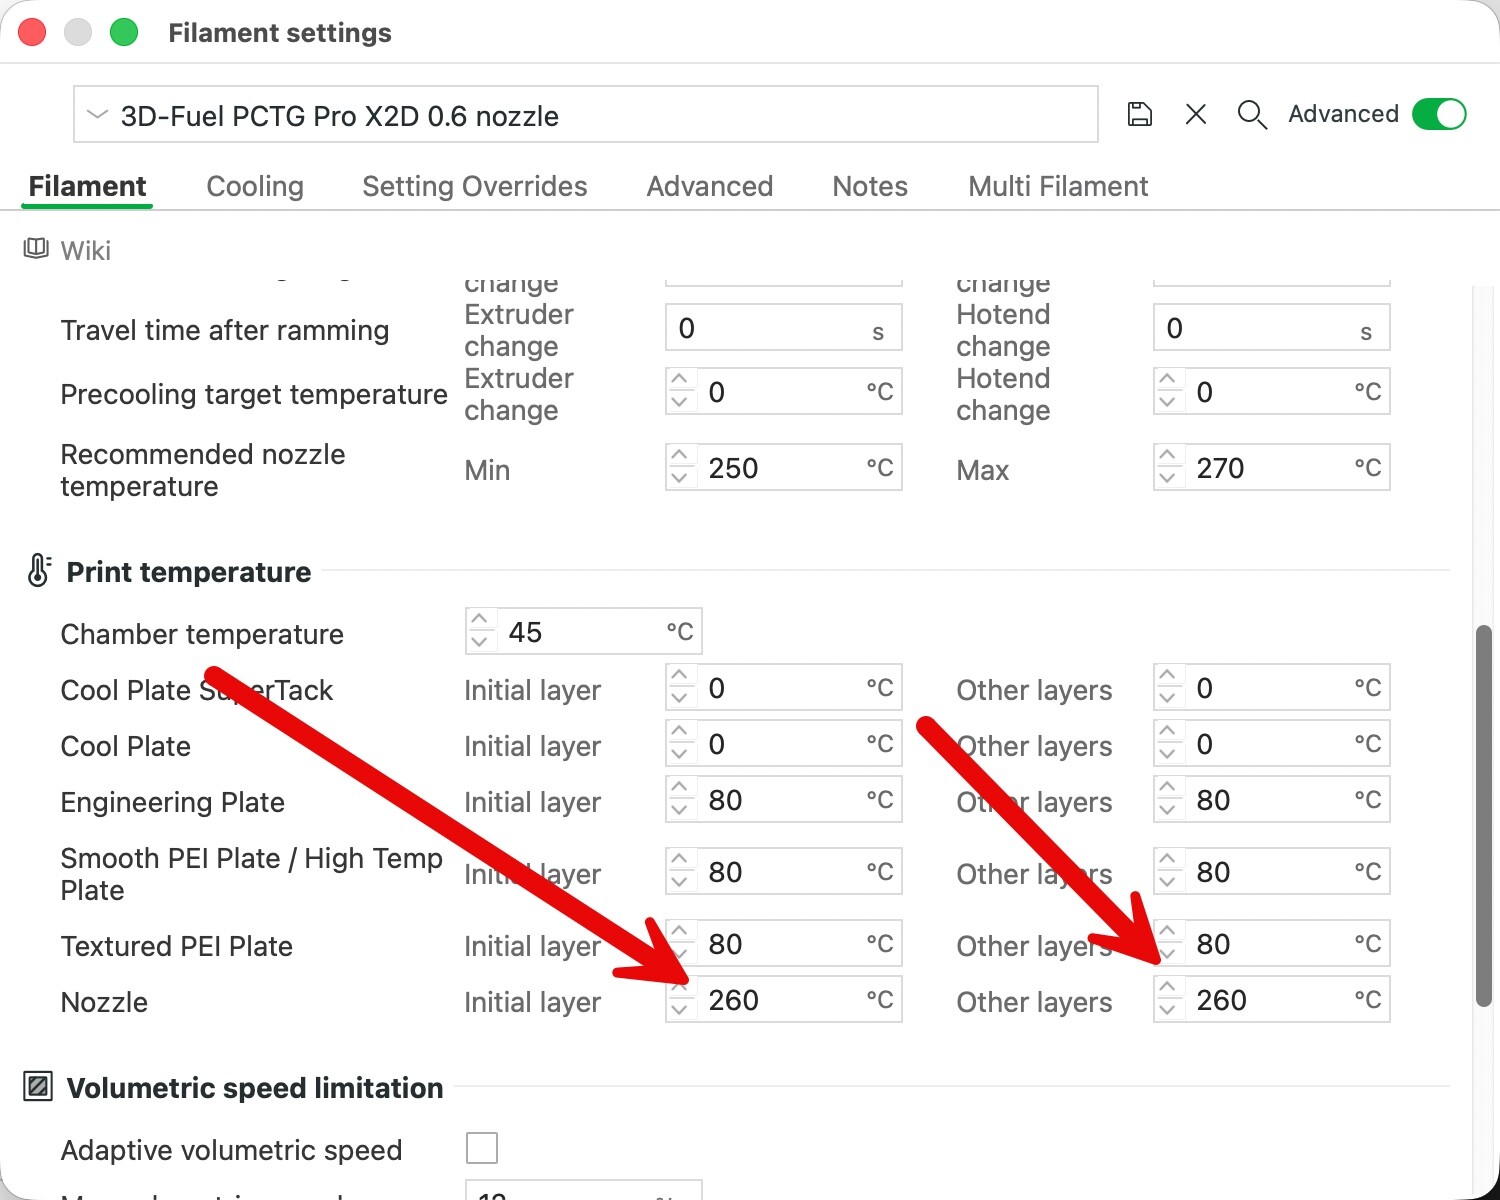
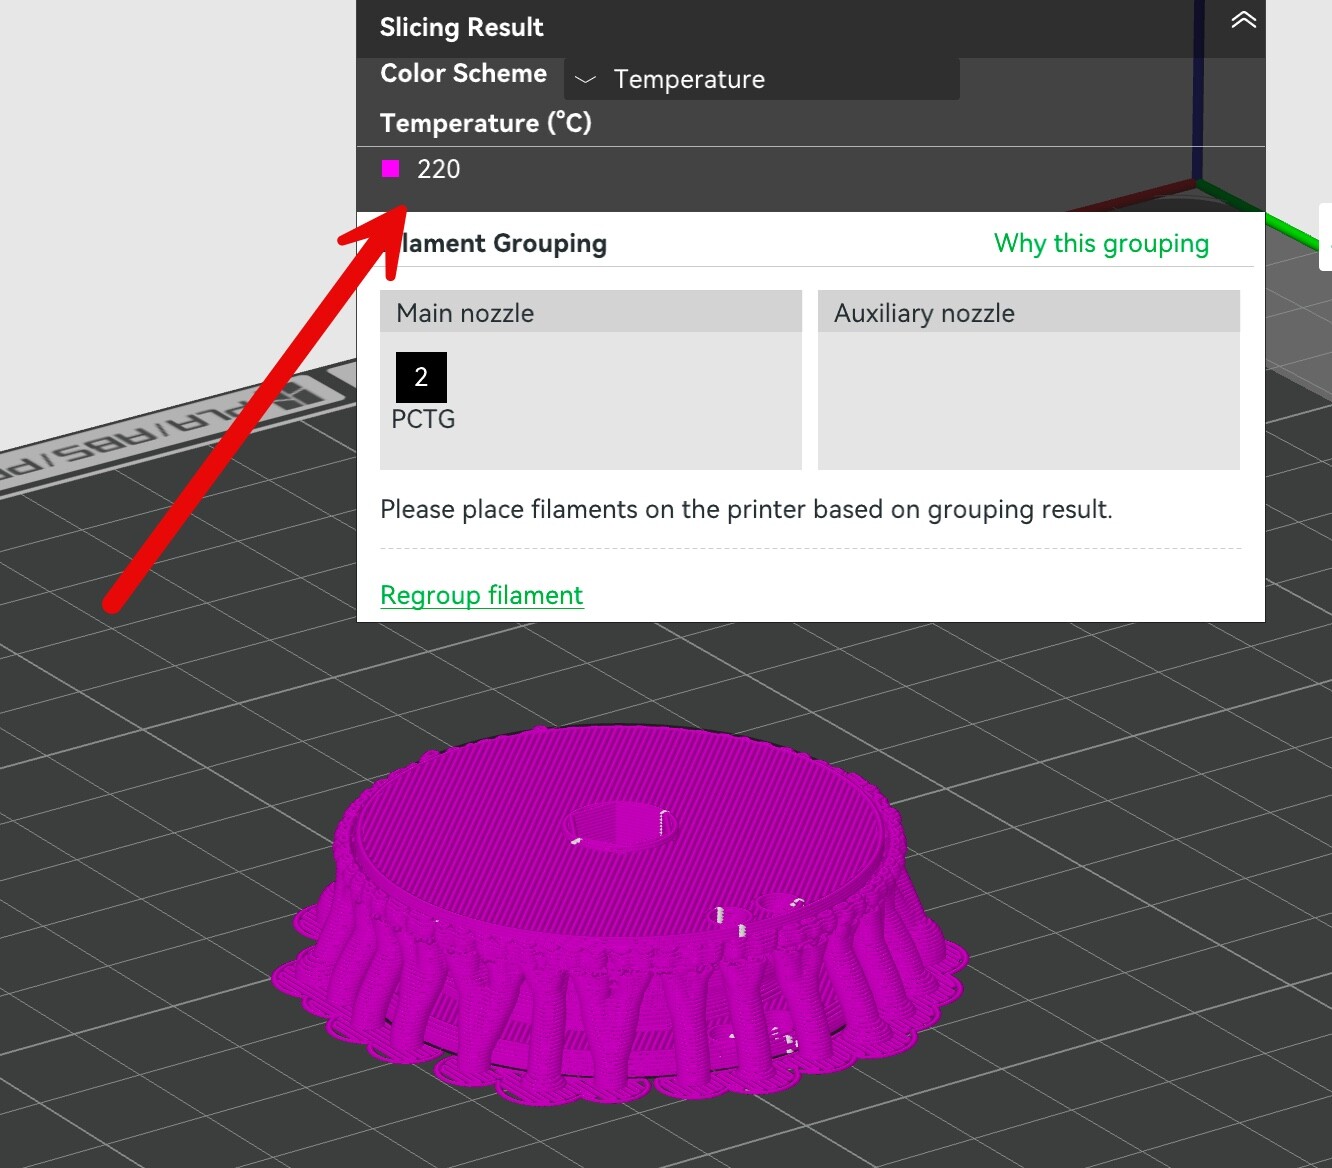
I notice what seems to me to be a real problem. the nozzle temp on my material profile is set to 260C… but the slicer sets the gcode to 220C.

here is are material settings

after slicing here is what BS shows in preview

Where/how is x2d getting this value???

I should note, on my x1c, the fans and nozzle temps behave as expected…

The whole point of the x2D is the heated chamber with dual nozzle for support material. But I give-up on even using the aux nozzle with support PLA interface, due to what I thought was PLA overriding fans and enabling strong cool model.. I don’t know, it just would not work And even 3d Fuel has duplicated problem printing PCTG with PLA support material on x2d. It does not work…

So I am just trying to get plan B to work… printing single material PCTG on x2d. So far utter failure

I know this was kind of a rant. But I really have put in too much time just trying to get PCTG to work on x2d… I expected an upgrade for better printing engineering materials with heated chamber and dual nozzle.

So far x1c works better.. Something is not right here.

re: 220 showing, but you declare 260

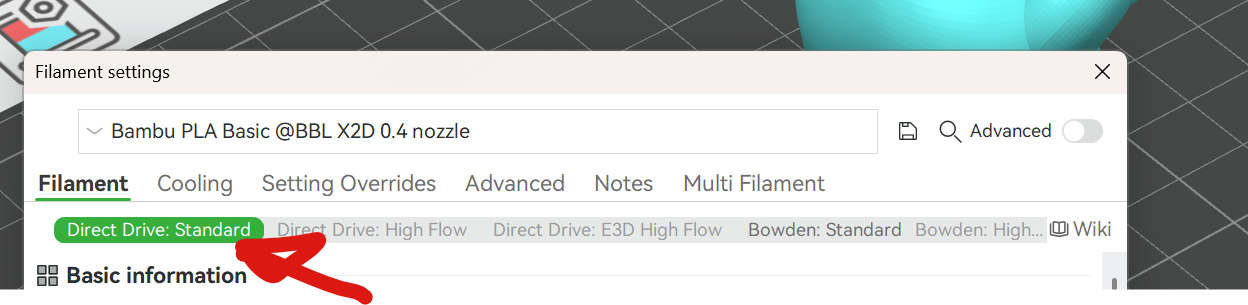
welcome to x2d’s configuration nightmare, be sure the active subtab you have selected is the nozzle archetype AND extruder you plan to use. These sub menus are on a LOT of screens.

If you notice the material I am editing does not have any of these tabs since I started with a generic material… I guess the software could be using some hidden values for hf nozzle. Settings we can’t edit…

So confusing…

I hope Bambu Labs plans to get this mess under control.

If all you want to do is use defaults with Bambu Labs material. x2d works well.

On the other hand, x2d is kind of a disaster with custom materials and settings on other materials.

IMO they need to overhaul the custom material/machine settings. Or they need to fix some bugs.

I don’t know where to go from here

thanks

Joe