Got a small issue regarding supports on my A2L, issue is they seem to keep breaking. I have no issues with them sticking to the plate but as they get further up some seem to snap. I’ve also noticed if the support is coming off the model rather than the build plate you can be your last buck these will snap.
I’ve tried moving the z hop but this didn’t help, is this a matter of making the supports stronger when using the bed slinger or am I maybe missing something?
I haven’t had this issue with the same file in my X2D or P1S so I’m assuming this may be a bed slinger issue here.
I have It mounted on what I would consider to be a solid structure so I’m assuming this isn’t a vibration issue
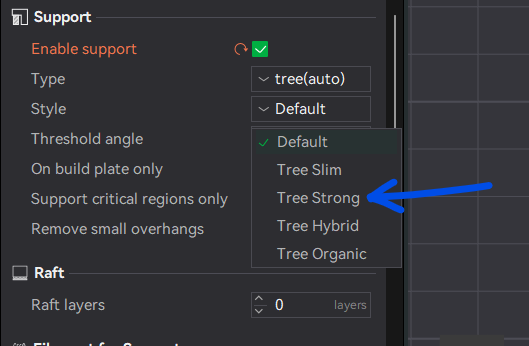
Hi, I did switch to this but the supports looked overkill for what I was doing. I haven’t ruled this out as an option but I thought perhaps there may be a setting or two I should be changing before going in with the strong supports… Appreciate the comment and reply
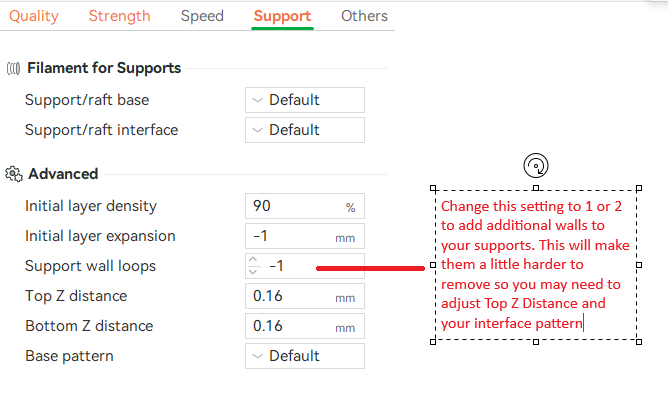
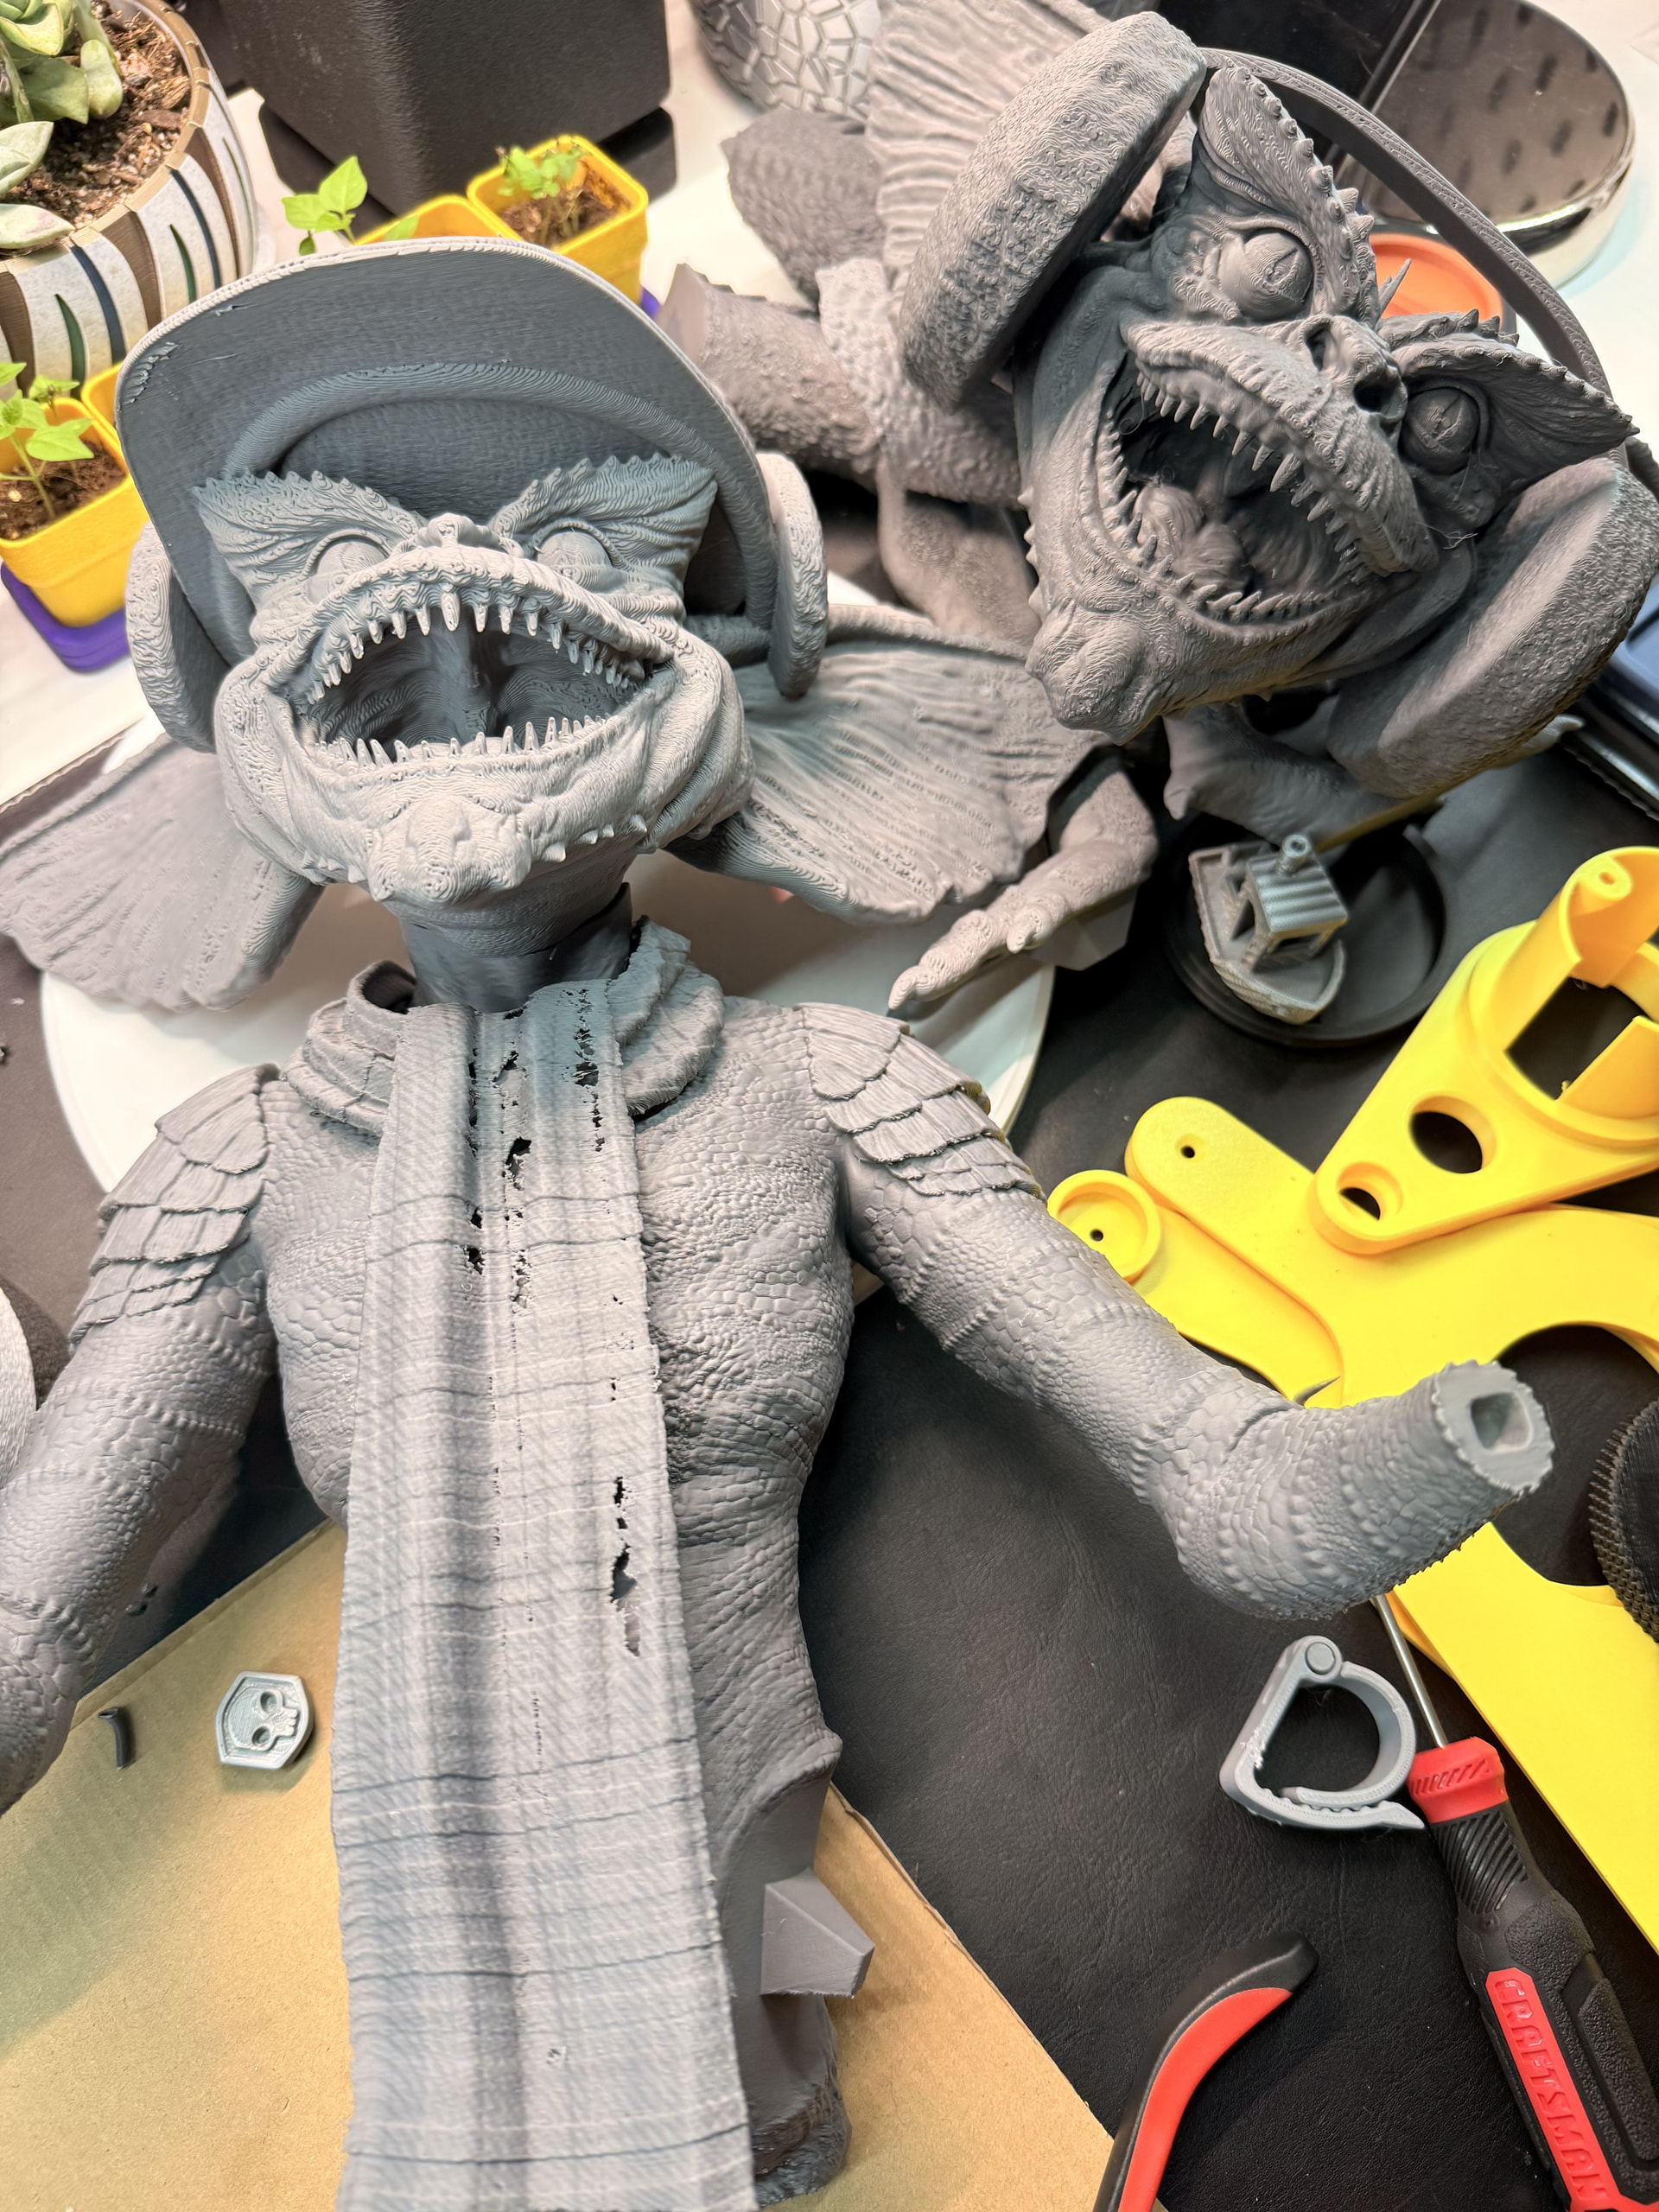
I’ve been working on 26 - 30" Gremlins and this was the specific setting that fixed my supports from breaking. I’ve done more testing with supports in the past two weeks than I want to admit.
It sounds like the movement of the bed could be putting extra stress on the taller supports, especially when they are attached to the model. I’d try increasing support density or contact strength and checking the support interface settings before changing Z-hop further.
Another point of note is that your other printers are closed while the A1 is open. Hence the “chamber” temp is lower leading to an increased risk of curling. It tends to happen on supports pretty quickly.
So check you room temp and observe the observe the print to see if this is the issue.
Common remedies against curling are
Newly dryed filament
Increased chamber/room temp
Lower layer height
Decreased speed
With PLA, the first 2 are usually sufficient. PLA likes 30 to 35°C but that is a bit over the top for an open printer
I have thought about temperature myself, more so it’s not happening on my enclosed printers. The room is pretty warm though but obviously the open bed is still exposed.
I have this feeling it’s due to either open conditions or movement, Purley because it’s the only things that make sense to me
I think it’s movement buddy, but I’m not sure how to add further prevention. It’s sitting in a fairly sturdy unit but I can feel movement/vibration if I lean on the bench and the printer is running.
I’m not sure if I can fit some other kind of foot to the printer like my X2D has to compensate for more movement as it’s basically just sitting on what seems like high density foam pads
Regarding movement, there are two failure causes that come to mind. Tree inertia and nozzle collisions.
Regarding inertia, a stronger tree would have more mass, but its added strength would more than make up for that if bed adhesion is good. Furthermore, lowering accelerations would show an immediate improvement.
Nozzle collisions are far more likely. They do happen quite frequently and can usually be traced back to
unfortunate (default) sparse infill settings (“Grid” is the death of many prints…)
Edge curling: faster layer cooling and hence layer shrinkage on edges and overhangs pulling the edge of the object up, in particular if the underlying layers are still warm and pliable
For me (X1, H2, Plus4 closed printers), edge curling is a sign that I need to dry my filament (again) before going down the rabbit hole of lowering speeds and/or layer height.
Although I do admit that in days gone by, I did crank up the heating in the house well above comfortable levels when I still had PETG on a bed slinger
Blamed it on the (at the time) new automatic heat control in the house My wife accepted that explanation
&
PS: On the topic of vibration isolation, I use these to good effect on my X1C HULA v1.0 Anti-Vibration Feet for 3D Printers - Free 3D Print Model - MakerWorld
Unfortunately, spring stiffness is not tuned to the printer so your mileage may vary for an A-series.
Also, keep in mind that you want to isolate X & Y while having a hard Z-direction interface. To achieve this, I simply moved the rubber feet down below the print bed in the slicer so that only 3 layers are used as an anti-skid. This avoids turning a single degree-of-freedom system into a 12 degree-of-freedom system.
The printer moves a lot more with these, leading to reduced vibration transmission and reduced relative loads in the frame of the printer. If tuned well, the transmitted vibrations will be noticeably lower but improvements in print quality are not really observable. These printers are pretty good already.
Or you could go completely crazy and build a true vibration absorber. Only an educational toy print though Definitely not the type of thing you’d want to use longer term. But the concept works and is easily tunable. Anti-Vibration Pad Mk I - Free 3D Print Model - MakerWorld
Had a little look at your reply, honestly some made sense, some didn’t . Your explanation was spot on just my lack of knowledge…
On the subject of vibration/movement. I have been doing a bit of research and some people are suggesting putting Eva high density pads on the workspace then a slab on top, rest the printer on this. I have went out and bought these items to give it a go.
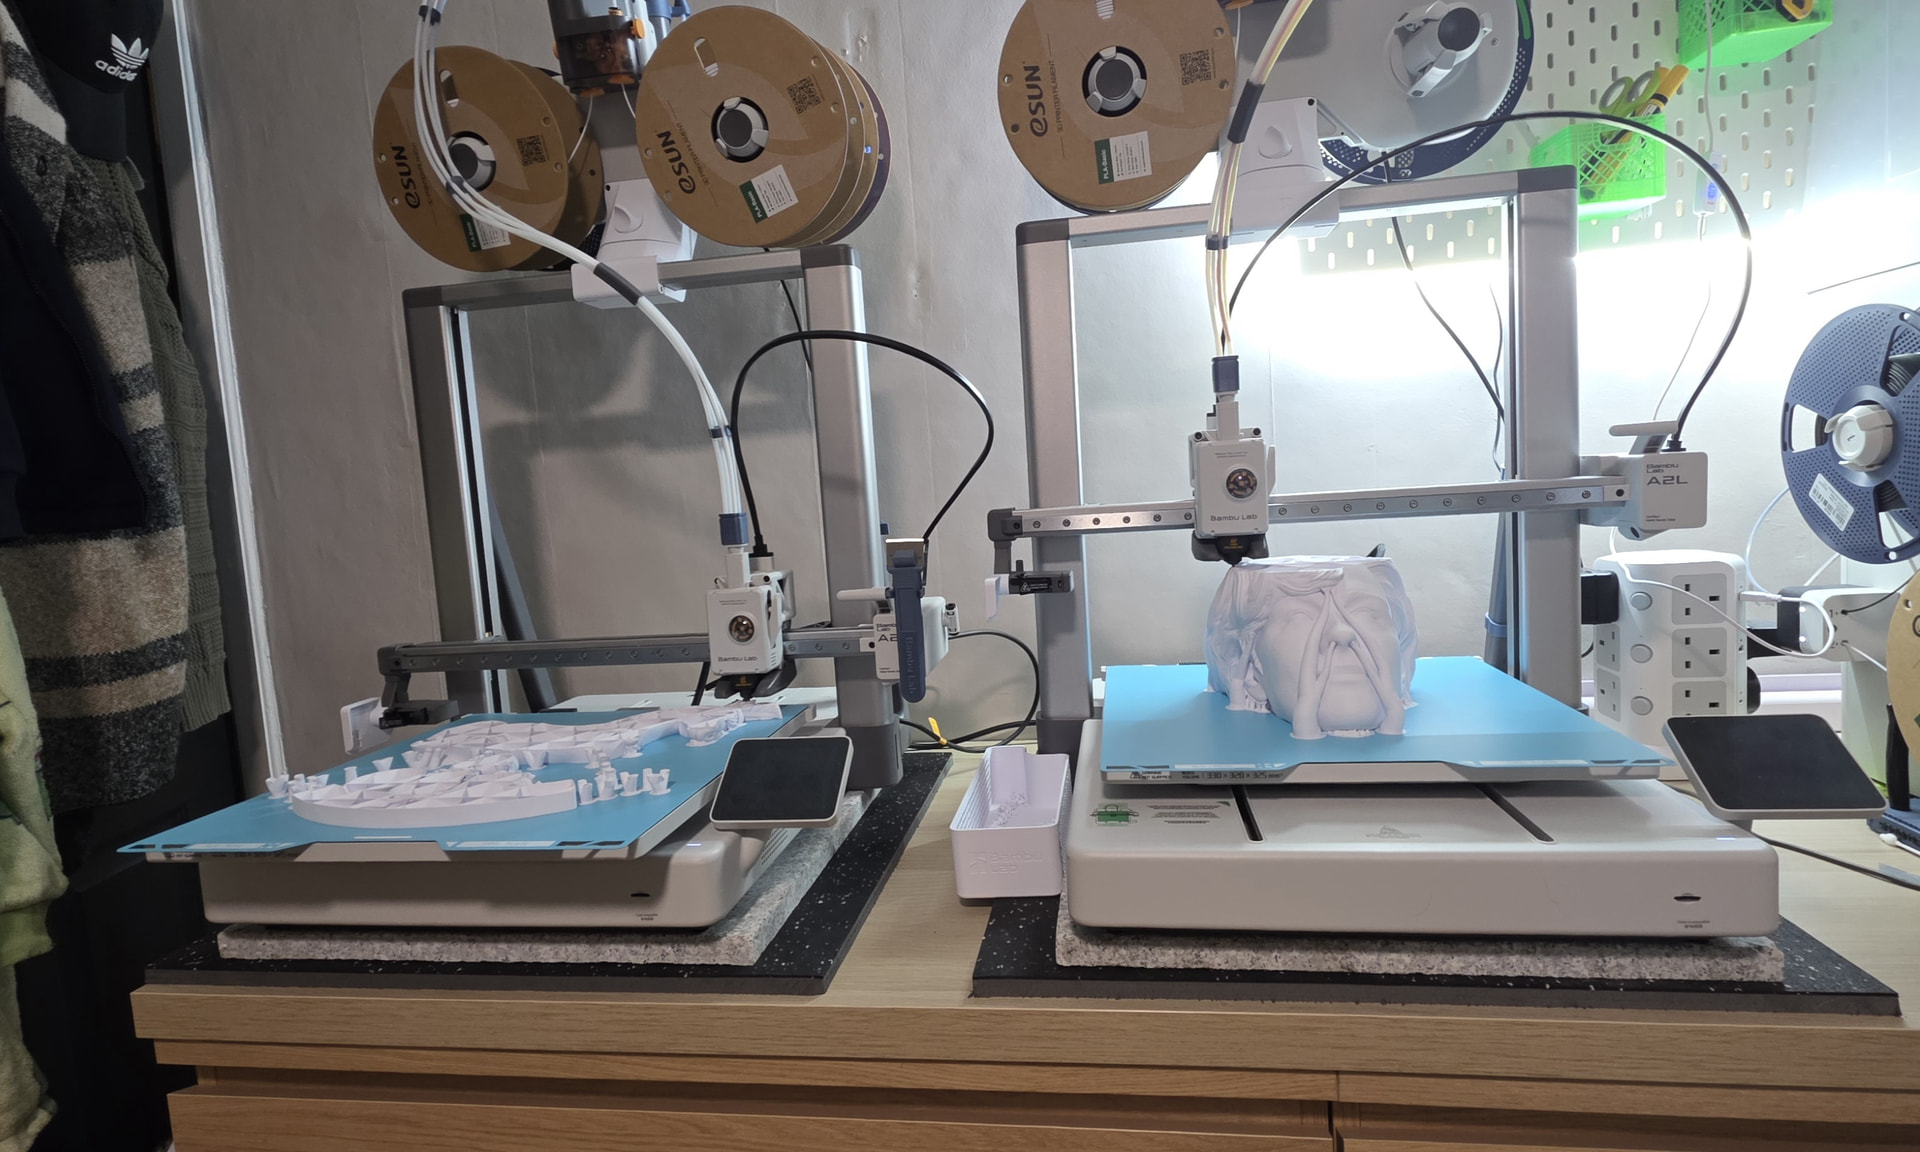
I’m not sure if I mentioned but I have two of these A2L printers next to each other on the same area, although I still get snapped supports even if I’m running just one
Yes, applying extra mass is usually the cheapest and quickest way to tackle vibrations. And below the mechanisms Eigenfrequency, pretty much the only means anyway. When my X1 was living in the shed, that was also my way to go (simple paver).
I did not use the eva foam though. Although it has been a couple of years since I dug unto my old textbooks, I remember spring stiffness being key for tuning rather than damping.
But it protects the table top and should give some freedom of movement. With the additional mass on top of it, amplitudes are much smaller so only little freedom of movement is needed.
Just make sure to run the printer calibration again after the new set-up. Otherwise print quality can suffer as the printer is optimizing a vibrational environment that no longer exists.
Sometimes a timelapse can help in the diagnosis. I have had plenty of support failures to date which I can all trace back to nozzle collisions from curling or myself accidentally setting a 0 wall count (all enclosed printers though).
&
Edit: Addendum: You may have seen it already but just in case as it may be of interest:
Well, seems to have done the trick, I have had zero issues since this setup. Kinda blows my mind it worked but hey-■■, fingers crossed it stays this way


 &


 My wife accepted that explanation




 ,
