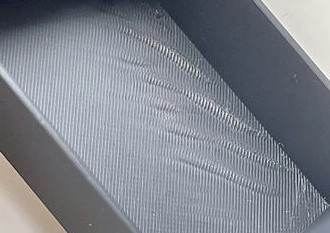
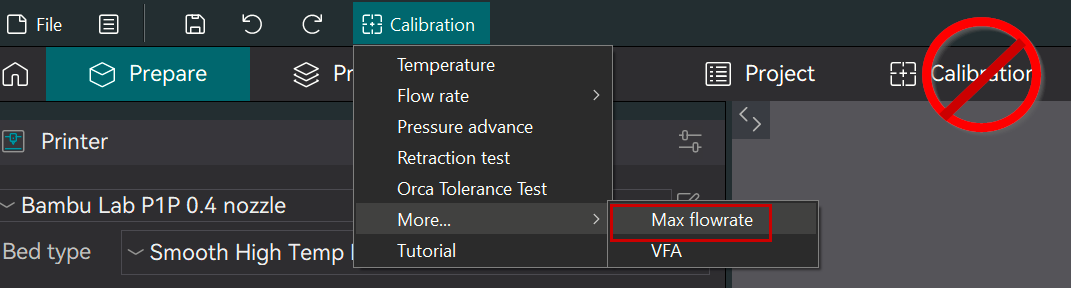
This is something of a sore point for me because I wasted a great deal of time and filament early on while drinking the Bambu Lab Kool-Aid. Hopefully, my experience as an early P1-series adopter will help you avoid making the same mistakes.
K factor and flow ratio are not the same setting, and treating either one as a near-universal constant defeats the purpose of calibration.
K factor is the numerical value used for pressure advance. It compensates for the delay between extruder movement and the corresponding pressure change inside the nozzle during acceleration and deceleration. An incorrect value commonly produces bulging, thinning, or inconsistent extrusion around corners and abrupt speed changes.
Flow ratio is the extrusion multiplier. It controls the overall quantity of filament extruded. An incorrect value produces broader under-extrusion or over-extrusion across walls, top surfaces, and infill.
When I got my P1P in 2023, I initially got caught up in what I now call “Bambu Speak”:
- “Flow Dynamics” is Bambu’s name for pressure advance calibration.
- “K factor” is the resulting pressure advance value.
- “Flow Ratio” is the extrusion multiplier.
After adopting OrcaSlicer early on, I began using its calibration tools because they were clearer, more complete, and more transparent than Bambu’s original implementation.
It is also important to understand the software lineage. OrcaSlicer is a fork of Bambu Studio. Bambu Studio is based on PrusaSlicer, which originated from Slic3r. Bambu did not build this technology from scratch, despite surrounding established open-source concepts with enough proprietary terminology to make them appear uniquely Bambu.
Bambu later incorporated similar calibration tools into Bambu Studio. That fits a recurring pattern with the company: build on open-source foundations, rename familiar functions, surround them with proprietary services, and then blur the distinction between what Bambu developed and what it inherited.
To be fair and technically accurate, the Bambu Studio slicer core is open source. The more troubling proprietary control exists largely in the networking, authorization, cloud, and printer-control layers. That distinction matters because those layers determine whether owners and third-party applications can communicate freely with hardware the customer already purchased.
Unfortunately, my knowledge of current Bambu Studio behavior is limited because I stopped using it during the January 2025 Bambu Connect and authorization controversy.
I removed Bambu Studio because I no longer trusted Bambu’s software and firmware strategy or wanted its software controlling my local workflow. The instructions below therefore apply to OrcaSlicer. Bambu Studio may now contain comparable calibration functions, but I no longer follow it closely enough to provide reliable instructions for its current interface.
Do not blindly accept Bambu’s stored or default K values. Perform the Orca calibrations or use the one in Bambu Studio if they exist.
Do not assume that 0.015 or 0.020 is correct merely because those values are common. A default is a starting point, not a calibration result.
The correct pressure advance value can vary with:
- Filament material and formulation.
- Manufacturer and production batch.
- Nozzle diameter and geometry.
- Nozzle condition.
- Printing temperature.
- Extruder configuration.
- Volumetric flow rate.
Flow ratio must be calibrated independently. A filament can require an ordinary K factor while still needing a substantially different flow ratio, or vice versa.
You also need to determine which pressure advance value the printer is actually using. Depending on the workflow and configuration, a value may exist in:
- The OrcaSlicer filament profile.
- The printer’s stored filament settings.
- An AMS slot assignment.
- A result produced by automatic Flow Dynamics calibration.
Bambu’s multiple storage locations and calibration paths create needless ambiguity. The owner should not have to reverse-engineer the slicer, AMS, printer, and automatic-calibration hierarchy merely to determine which K value is active.
Before troubleshooting print quality, verify whether pressure advance is enabled in the OrcaSlicer filament profile and whether the printer or AMS has another K value associated with the selected filament. Do not assume the value visible in one location is necessarily the value controlling the print.
That is one reason I prefer manual calibration in OrcaSlicer. It produces a known result under controlled conditions and allows the value to be defined explicitly instead of relying blindly on Bambu’s defaults, stored values, or automatic routines.
X1 series’ users have automatic calibration and it is convenient, but convenience is not proof of accuracy. Those of us on the P1 platform must do this manually and in my experience, mastering manual calibration places one in a better position to control results.
That observation may be relevant, but the current print example you provided does not prove that the defect is caused by the left side of the bed.
One way you can validated this is to rotate the model 180° around the Z axis while leaving it in approximately the same location on the build plate.
- If the defect remains on the same physical side of the printer, uneven airflow, cooling, or another location-dependent condition becomes more likely.
- If the defect rotates with the model, the cause is more likely related to model geometry, seam placement, toolpath direction, acceleration, or extrusion behavior.
- If the result remains ambiguous, move the model to the opposite side of the bed without changing its orientation and print it again.
That sequence separates three variables:
- Model geometry.
- Model orientation.
- Physical location on the bed.
Uneven cooling is plausible, particularly if the printer is using a strong side-mounted auxiliary fan. Bambu relies heavily on aggressive directed cooling to support its high-speed printing claims, but asymmetric airflow can create visibly different surface conditions on opposite sides of a model. More fan is not automatically better cooling.
The fact that the straight walls look acceptable does not eliminate cooling as the cause. Straight vertical walls are generally less sensitive to asymmetric airflow than corners, curves, overhangs, bridges, and areas where the toolhead changes speed rapidly.
Pressure advance defects normally follow the geometry and toolpath rather than remaining tied to one physical side of the printer. The 180° rotation test is therefore a useful way to determine whether K factor is relevant to this defect at all.
Even if you can’t use Orca, consult these resources and adapt them to Bambu Studio, they should work the same:
These three tutorials are old by YouTube standards, but they cover the fundamentals clearly and still hold up well after three years. There are newer tutorials available, but none I have found explain the basics as effectively as this creator.
As always with YouTube, do not treat any single presenter as authoritative. Compare explanations, understand what each calibration changes, and verify the result on your own printer rather than blindly copying someone else’s values.