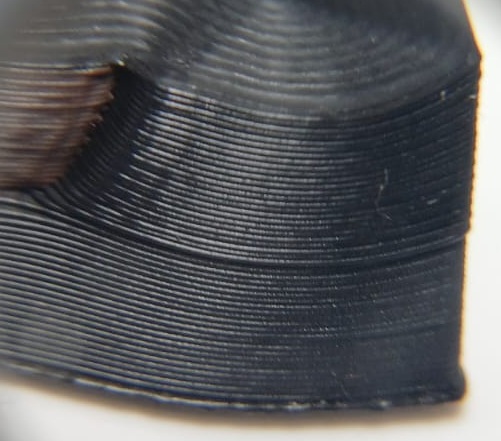
This is a known anomaly and is generally referred to as the “Benchy Hull” line. It is caused by a sudden shift in thermal contraction and cooling rates when transitioning from hollow perimeters to solid infill layers or in you case colour changes or pauses.
That makes a lot of sense. I just tested this with a plain single-color cube: I paused the print at layer 20 for about 10 seconds, resumed it, and got a wider layer. I repeated the same at layer 40 with almost exactly the same result. A third, very brief pause produced a weaker effect. In each case, the bulge gradually disappeared over about three layers. With the AMS, however, the effect starts after the first color change and the subsequent layers remain slightly wider. Do you think the AMS color-change sequence could be producing the same thermal-contraction effect, but in a more persistent way?
I did another test using a simple cube with two colors. The result is very interesting. A manual pause produces one wider layer followed by about three transition layers until the dimensions return to normal. With the AMS color changes, the exact same effect occurs, but every layer containing a filament change produces its own transition. Since the color changes can happen on consecutive layers, the thermal effect never has time to fully recover, creating a continuous band of slightly wider layers.
Do you think this is consistent with the Benchy Hull Line mechanism? And is there a recommended way to mitigate this specifically in multi-color prints?
It can happen. It is much more noticeable if you have multiple color changes on one layer.
The fix is to slow down the other layers to more closely match. Looking at the speed section on the prepare tab will help with this.
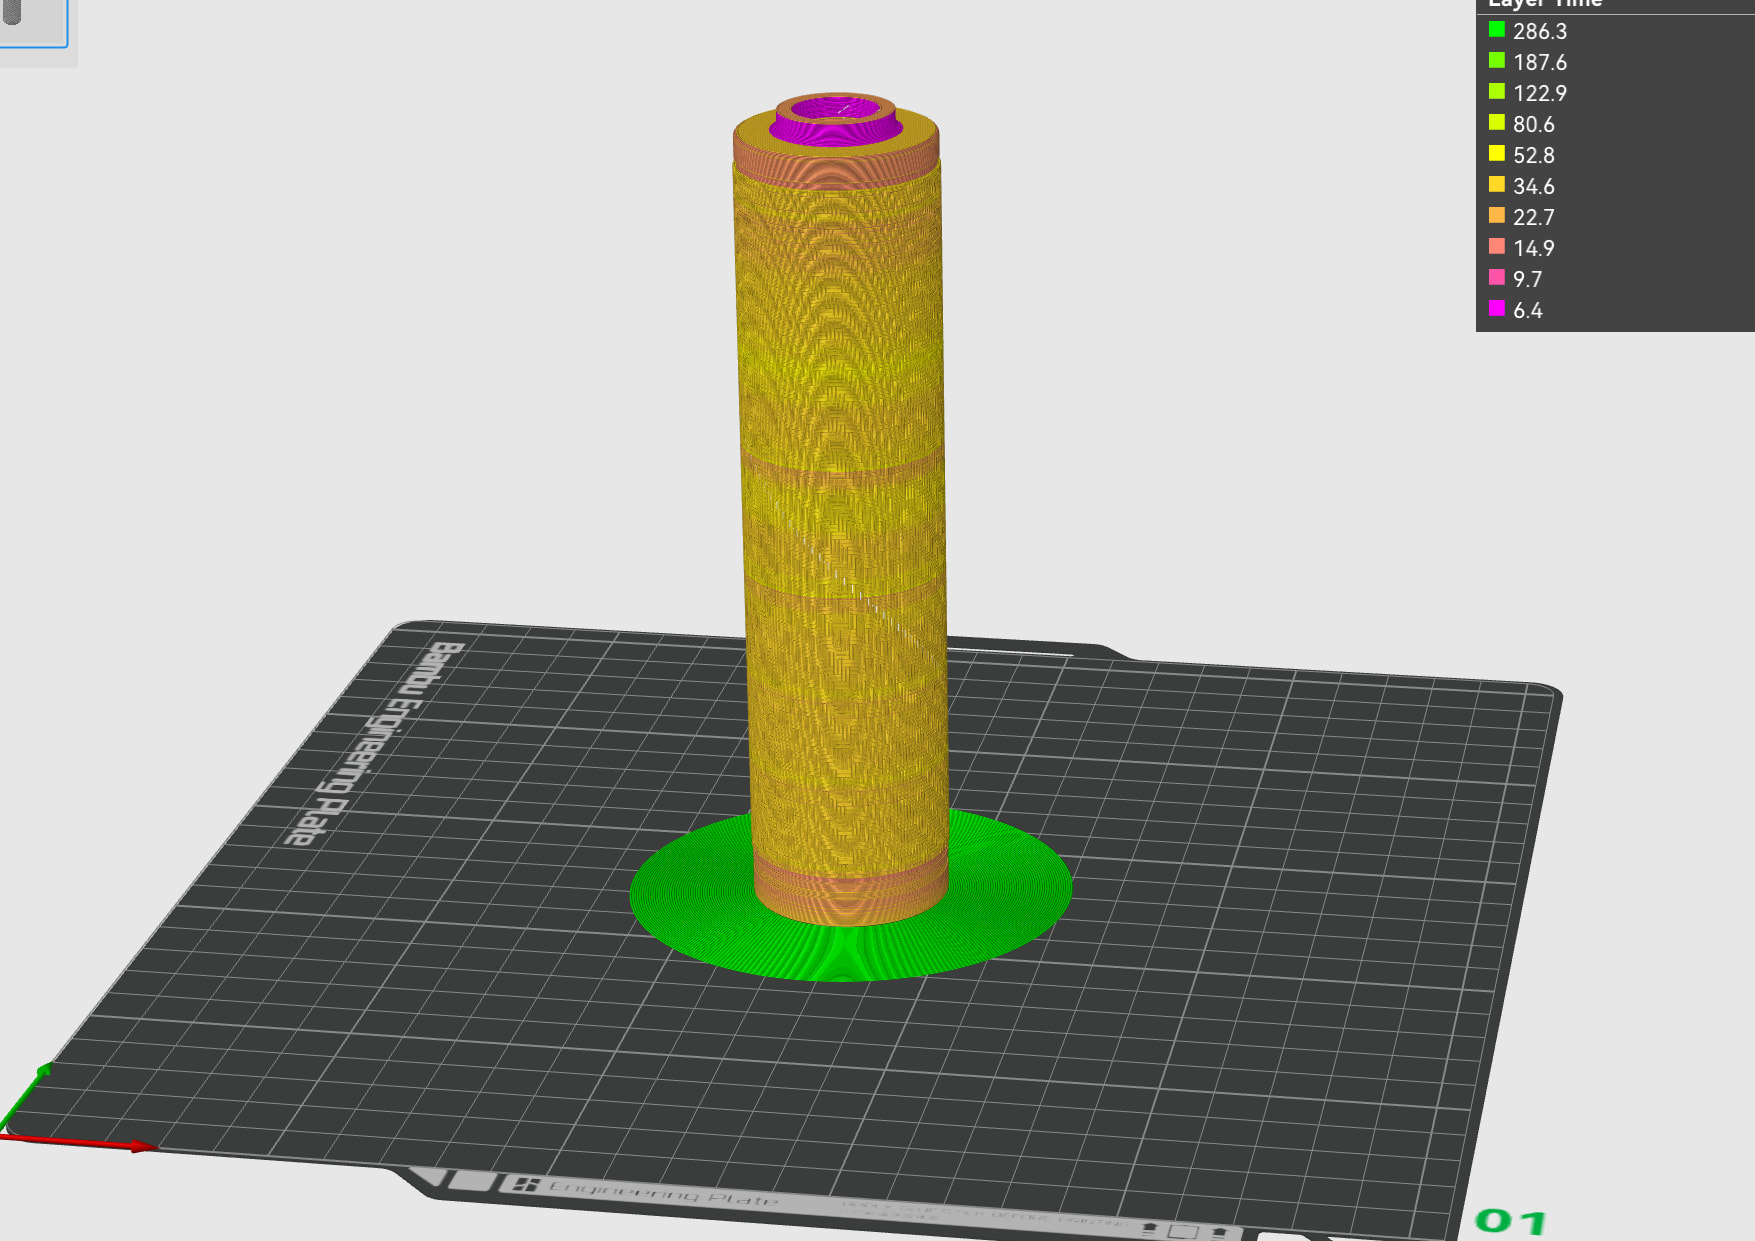
Thanks, that makes sense. I noticed that the layer time changes dramatically when the AMS starts changing colors (for example, from about 12 seconds to over 120 seconds). So I understand that the goal is to reduce this difference in layer time.
Would you recommend slowing down the normal layers so that their total layer time is closer to the layers containing color changes, rather than simply reducing the overall print speed?
Sorry, I could have been more clear. You are looking for the layer times to be more consistent between layers with color changes and layers that do not have them. That does not mean slowing down the entire print, but slowing down the faster sections.
You want it to be generally similar like this. It doesn’t have to be perfect. You just don’t want to see huge differences because that is where the shrinking will show the most.
These printers from the factory are tuned a little more for speed than they are quality.
A better way to fix this is to hide it in the design, but that is not always an option.
Thanks again for the guidance — I gave it a try and wanted to share what happened.
I raised the “Max Fan Speed threshold – layer time” from 8s to 140s, and also lowered “Min print speed” from 20mm/s down to 10mm/s. The normal (non-swap) layers did slow down somewhat — from ~12s up to about 34s — but they won’t go any higher than that, even after lowering min print speed further. Meanwhile the AMS swap layers are still taking ~160s, so there’s still a big gap between them.
It seems like most of that 34s might not actually be wall-printing time that the speed settings can act on — maybe it’s dominated by other fixed overhead (travel moves, fan ramp-up, etc.) that doesn’t scale with print speed. Does that match what you’d expect, or is there another setting I should be looking at to push the normal layers closer to that 160s mark?
Also curious: in your experience, does the layer time need to match closely (like within 20-30s of each other), or is even a partial reduction in the gap usually enough to noticeably reduce the bulge?